
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Apr. 18, 2023
The rapid transition toward Electric Vehicles (EVs) and high-density electric powertrain architectures has fundamentally changed automotive fastener engineering.
To maximize driving range, structural efficiency, and packaging density, automakers are increasingly adopting lightweight structural materials,
including extruded aluminum profiles, aluminum castings, magnesium-aluminum components, and ultra-high-strength steel (UHSS) sheets.

These material combinations create complex fastening challenges. Joining dissimilar metals can introduce galvanic corrosion, differential thermal expansion,
preload variation, thread damage, and long-term joint relaxation. At the same time, EV battery enclosures, battery modules, electric drive units (EDUs), power electronics,
chassis systems, and thermal management assemblies require fasteners capable of maintaining mechanical performance under vibration, temperature cycling, and repeated assembly loads.
For EV battery pack and automotive structural applications, fastener selection must therefore consider not only tensile strength,
but also fatigue resistance, corrosion protection, thread accuracy, coating friction, assembly torque, material compatibility, and manufacturing consistency.
This technical guide provides automotive design engineers, EV battery engineers, procurement managers, and strategic sourcing specialists with a unified framework covering:
Lightweight Joining & Multi-Material Compatibility: Managing galvanic corrosion, thermal expansion, and interface compatibility between steel, aluminum, magnesium, and engineered materials.
Ultra-High-Strength & High-Performance Fasteners: Selecting Class 10.9, 12.9, and other high-strength automotive fasteners for EV battery packs, electric motors, chassis systems, and structural assemblies.
EV Battery Stud & Tie-Rod Applications: Understanding long battery pack studs, enclosure tie rods, module fastening systems, and dimensional control requirements.
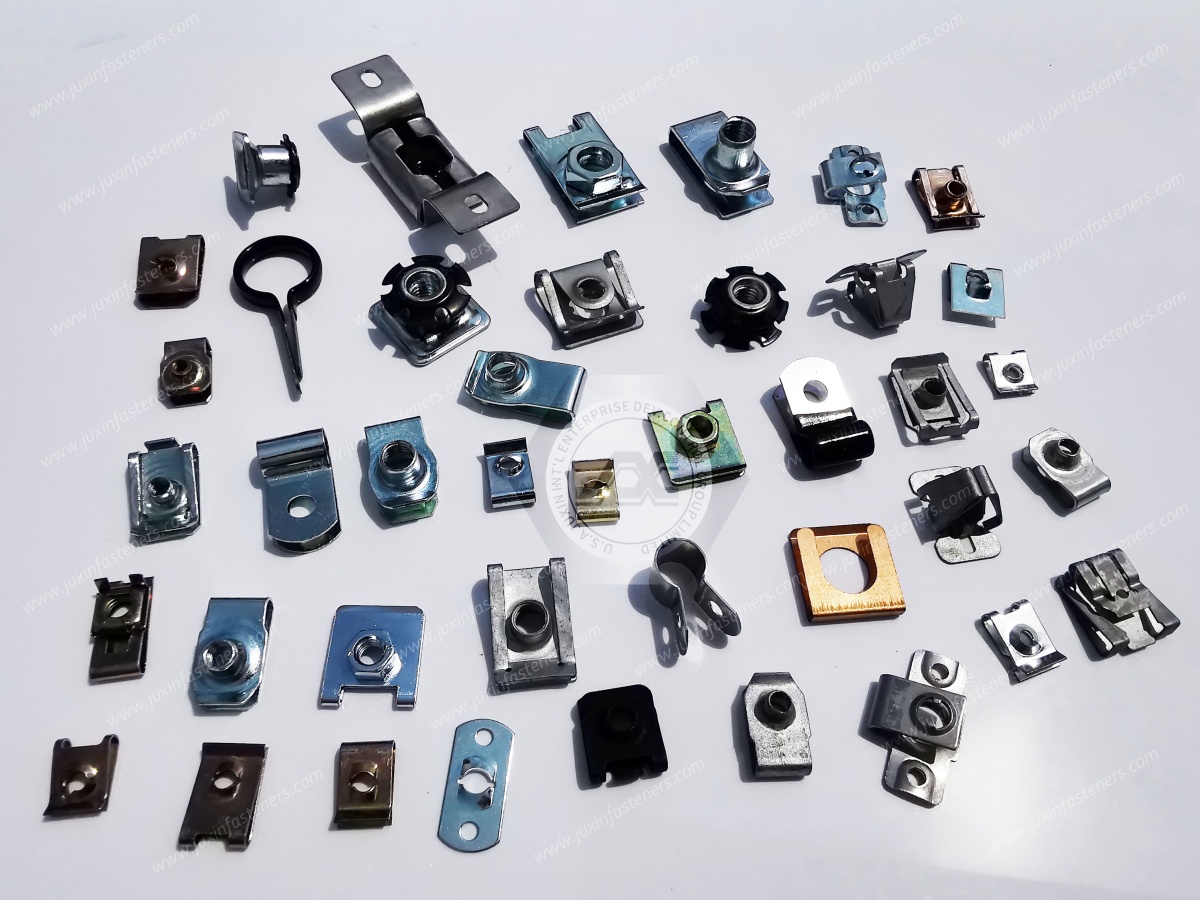
Sheet Metal & BIW Fastening: Applying self-clinching nuts, self-clinching studs, weld studs, weld nuts, and other automotive sheet metal fasteners where permanent or removable threaded attachment points are required.
High-Temperature Fastening: Selecting stainless steel and nickel-based alloy fasteners for thermal management systems, exhaust-related assemblies, electric powertrain components, and other high-temperature environments.
Strategic Procurement: Aligning material, coating, mechanical class, dimensional tolerances, inspection requirements, and production capability with automotive OEM and Tier-1 sourcing requirements.
 |  |
Automotive OEM and Tier-1 supply chains require fasteners manufactured and inspected against internationally recognized specifications.
For EV applications, the selection process should consider mechanical property class, material grade, thread system, coating technology, corrosion resistance, fatigue performance, and production traceability.
| Fastener Classification | Governing Standards / Specifications | Material / Metallurgical Grade | Mechanical Properties & Strengths | Primary EV / Automotive Application |
|---|---|---|---|---|
| Ultra-High-Strength Bolts | ISO 898-1 Class 10.9 / 12.9 / applicable high-strength specifications | 35CrMo / 42CrMo4 / 40CrNiMo and equivalent alloy steels | High tensile and yield strength; suitable for high preload and compact joint designs | EV battery pack frame bolts, electric motor housings, drive systems, chassis and suspension assemblies |
| High-Strength Automotive Studs | ISO 898-1 / applicable DIN and EN specifications | Boron steel, micro-alloy steel, alloy steel | High tensile strength, fatigue resistance, controlled straightness and thread accuracy | EV battery module tie rods, battery enclosure studs, long fastening systems and structural mounts |
| Self-Clinching & Sheet Fasteners | Applicable ISO / DIN / EN product specifications and OEM requirements | Carbon steel, stainless steel, and application-specific alloys | High push-out and torque-out resistance when installed into suitable sheet thickness | BIW panels, battery enclosure panels, electrical brackets, door structures and interior mounting points |
| High-Temperature / Heat-Resistant Fasteners | ASTM A638 / ASTM B637 and applicable ISO / EN material specifications | A286 / EN 1.4980, Inconel 718 / UNS N07718 | High-temperature tensile strength, creep resistance and oxidation resistance | Thermal management systems, high-temperature powertrain assemblies and exhaust-related components |
| Corrosion-Resistant Automotive Fasteners | ISO 10683, ISO 19598 and applicable coating specifications | Zinc-flake coated alloy steel, zinc-nickel coated steel, stainless steel | Controlled friction, high corrosion resistance and improved environmental durability | EV battery enclosures, underbody assemblies, aluminum-steel joints and chassis systems |
For production automotive fasteners, the applicable standard should always be matched to the exact fastener geometry, material, property class,
coating system, and OEM drawing requirement rather than assuming that one general standard covers every application.
 |  |
Integrating aluminum or magnesium components with high-strength steel fasteners creates a potential galvanic couple.
When moisture, condensation, road salt, or other electrolytes are present, differences in electrochemical potential can accelerate corrosion at the interface.
This is particularly important for EV battery enclosures and lightweight automotive structures because aluminum is widely used for battery trays, covers, extrusions, castings, and structural profiles.
                      MULTI-MATERIAL FASTENING INTERFACE       [MAGNESIUM / ALUMINUM STRUCTURE]
                    |
                    |  Moisture / Electrolyte
                    v
          +-----------------------+
          | Galvanic Interface    |
          | Corrosion Risk        |
          +-----------------------+
                    |
                    v       [STEEL / ALLOY STEEL FASTENER]

                    ENGINEERED SOLUTION

      Corrosion-Resistant Coating + Isolation
                    +
      Controlled Friction Coefficient
                    +
      Compatible Washer / Interface Material
                    +
      Appropriate Fastener Material Selection
Electrolytic Corrosion Barrier: When steel fasteners are installed into aluminum or magnesium structures, the fastener system should be designed to reduce direct electrochemical interaction.
Appropriate zinc-flake, zinc-nickel, passivation, topcoat, washer, or insulating interface systems can help control corrosion risk.
Zinc-Flake Coatings: Zinc-flake coating systems specified according to applicable ISO 10683 requirements can
provide corrosion protection while avoiding some of the hydrogen-embrittlement concerns associated with conventional electroplating of high-strength fasteners.
Zinc-Nickel Coatings: Zinc-nickel systems specified according to applicable ISO 19598 requirements
can provide enhanced corrosion resistance for demanding automotive and EV environments when the coating system, thickness, friction range,
and substrate compatibility are properly controlled.
Aluminum Fasteners: Aluminum fasteners can reduce galvanic potential when joining aluminum components, but the fastener's mechanical strength, fatigue resistance,
thread durability, and installation torque must be evaluated before replacing steel fasteners.
The correct solution is therefore not simply "use aluminum fasteners." The fastener material, host material, coating, joint geometry, operating environment,
and required preload must be evaluated as a complete joint system.
EV battery systems can experience substantial temperature variation during charging, discharging, fast charging, regenerative braking, and environmental exposure.
When a steel fastener is installed into an aluminum housing, the difference in thermal expansion coefficient can change the relationship between bolt elongation and joint compression.
Typical approximate values are:
Steel: $\alpha_{\text{steel}} \approx 12 \times 10^{-6}/K$
Aluminum: $\alpha_{\text{aluminum}} \approx 23 \times 10^{-6}/K$
A simplified relationship for evaluating thermal preload variation can be expressed as:
$$\Delta F_v \approx E_b \cdot A_s \cdot (\alpha_{\text{housing}}-\alpha_{\text{bolt}})\cdot\Delta T$$
Where:
$E_b$ = Elastic modulus of the bolt material
$A_s$ = Tensile stress area of the bolt
$\Delta T$ = Operating temperature differential
$\alpha_{\text{housing}}$ = Thermal expansion coefficient of the housing
$\alpha_{\text{bolt}}$ = Thermal expansion coefficient of the fastener
In an actual bolted joint, the result also depends on the stiffness of the clamped components, joint length, contact conditions, temperature distribution, and elastic properties of all components.
If thermal effects are not properly considered, repeated temperature cycling can contribute to preload variation, embedding, local yielding, or joint relaxation.
For aluminum battery housings and structural components, engineers can evaluate:
Fastener material selection
Joint length
Bolt elasticity
Washer configuration
Thread engagement
Surface treatment
Coating friction
Operating temperature range
Required residual clamping force
This system-level approach is particularly important for EV battery enclosure fasteners, battery pack studs, and electric powertrain fasteners.
In EV engineering, mass reduction is important because vehicle mass directly influences energy consumption and driving range.
Higher-strength fasteners can sometimes enable engineers to reduce fastener diameter, optimize joint geometry, or reduce the size of surrounding bosses and brackets.
However, moving from Class 8.8 or 10.9 to Class 12.9 or higher should never be treated as an automatic weight-saving solution.
Joint stiffness, fatigue performance, preload requirements, thread stripping, hydrogen embrittlement risk, coating technology, and host material strength must all be evaluated.
                 FASTENER STRENGTH & PACKAGING OPTIMIZATION

  Existing Joint
  +-------------------------------+
  | Larger Fastener / Larger Boss |
  | Higher Packaging Requirement  |
  +-------------------------------+
                 |
                 | Engineering Evaluation
                 v
  Higher Strength / Optimized Joint
  +-------------------------------+
  | Smaller Fastener Where Valid  |
  | Reduced Packaging Envelope    |
  | Potential Mass Reduction      |
  +-------------------------------+

  IMPORTANT:
  Fastener downsizing must be validated by joint-load,
  fatigue, preload, thread engagement and assembly analysis.
Traditional high-strength automotive fasteners commonly rely on controlled heat treatment to achieve the required mechanical property class.
Depending on the material and manufacturing route, modern cold-heading and micro-alloy approaches can reduce processing requirements and improve production efficiency.
Potential advantages include:
Manufacturing Efficiency: Properly engineered micro-alloyed and cold-work-hardened materials can reduce or simplify certain heat-treatment operations
while maintaining the required mechanical performance for the specified application.
Cold Heading Compatibility: Appropriate wire grades can be processed through precision cold heading to achieve consistent head geometry, shank dimensions, and material utilization.
Long Battery Studs: EV battery systems may use long studs or tie rods to clamp battery modules, enclosure components, structural rails, and internal assemblies.
Long components require careful control of straightness, thread concentricity, surface condition, and residual stress.
For example, long battery studs such as M6 or M8 configurations may require significantly tighter dimensional and straightness controls than conventional short bolts
because even small deviations become more significant over extended lengths.
Typical requirements may include:
Controlled straightness
Accurate thread rolling
Stable tensile properties
Consistent surface treatment
End-face squareness
Thread concentricity
Batch traceability
100% dimensional or optical inspection where specified
The exact specification should always be established according to the customer's drawing and validation requirements rather than applying a universal fatigue value to every EV battery stud.
In addition to structural joining technologies, sheet-metal fastening is essential throughout EV battery enclosures,
Body-in-White (BIW) structures, electrical systems, brackets, control units, and interior assemblies.
+--------------------------------------------------------------------------------------------------+
|                                  SHEET METAL FASTENING MATRIX                                    |
+------------------------------------+--------------------------------+----------------------------+
|  SELF-CLINCHING NUTS / STUDS       |  WELDED STUDS & WELD NUTS      |  PRE-APPLIED THREAD LOCK  |
|  - Press-fit into suitable sheet  |  - Permanent welded joint     |  - Vibration resistance    |
|  - High torque-out resistance     |  - Structural attachment      |  - Controlled assembly     |
|  - No additional nut required     |  - Fast repeatable assembly   |  - Thread retention        |
+------------------------------------+--------------------------------+----------------------------+
Self-clinching nuts and self-clinching studs provide permanent threaded attachment points in suitable ductile sheet metal.
During installation, the fastener's specially designed clinching feature displaces and cold-flows the surrounding sheet material into an undercut or retaining groove.
This creates mechanical interlocking without requiring conventional welding.
Typical applications include:
EV battery enclosure panels
Electronic control unit brackets
Automotive electrical boxes
Door structures
Interior mounting brackets
Instrument panels
HVAC assemblies
Telecom and electrical enclosures
Key procurement parameters include:
Sheet material
Sheet thickness
Hole diameter
Fastener material
Thread size
Thread engagement
Push-out resistance
Torque-out resistance
Corrosion resistance
Installation force
OEM drawing requirements
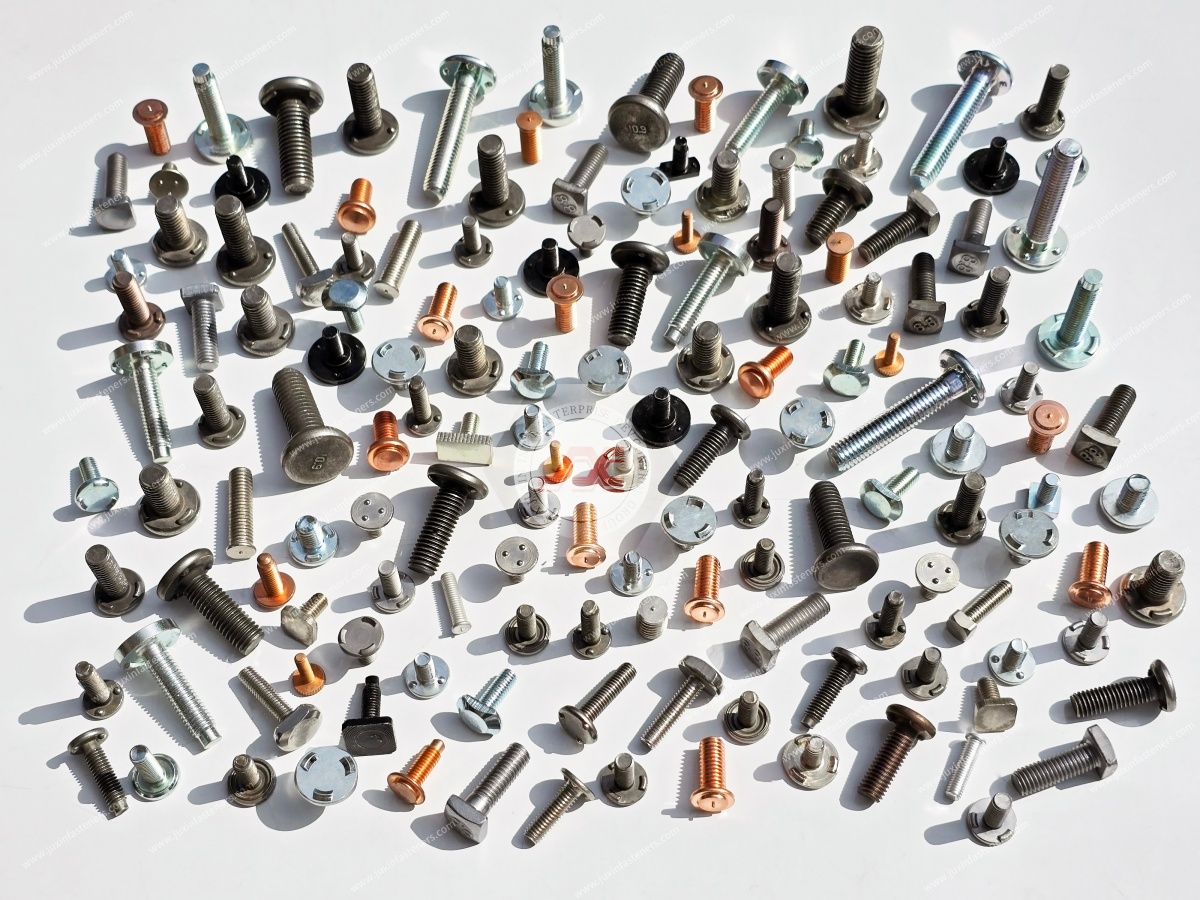
Weld studs and weld nuts provide permanent attachment points on automotive sheet metal and structural components.
They are commonly used where a threaded connection must be integrated directly into a stamped or fabricated panel.
Typical applications include:
Battery enclosure brackets
Grounding points
Wiring harness supports
Heat shields
Door structures
Seat structures
Underbody brackets
Automotive electrical assemblies
Welded fasteners can provide high production efficiency, but welding parameters, electrode access, sheet thickness, coating condition, weld integrity, distortion, and corrosion protection must be controlled.
For safety-critical applications, validation should include appropriate dimensional inspection, weld integrity testing, torque testing, pull-out testing, and OEM-specific validation requirements.
EV assemblies exposed to vibration and thermal cycling may require controlled thread-locking systems.
Micro-encapsulated or pre-applied thread-locking materials can provide:
Improved resistance to vibration-induced rotation
Controlled assembly torque
Reduced need for liquid threadlocker at the assembly line
Cleaner automated installation
Improved process consistency
The locking system must be selected according to operating temperature, chemical exposure, assembly torque, curing requirements, storage conditions, and customer specifications.
The EV battery pack is one of the most demanding fastening environments because it combines lightweight materials, high vibration exposure,
thermal cycling, dimensional constraints, corrosion requirements, and high production volumes.
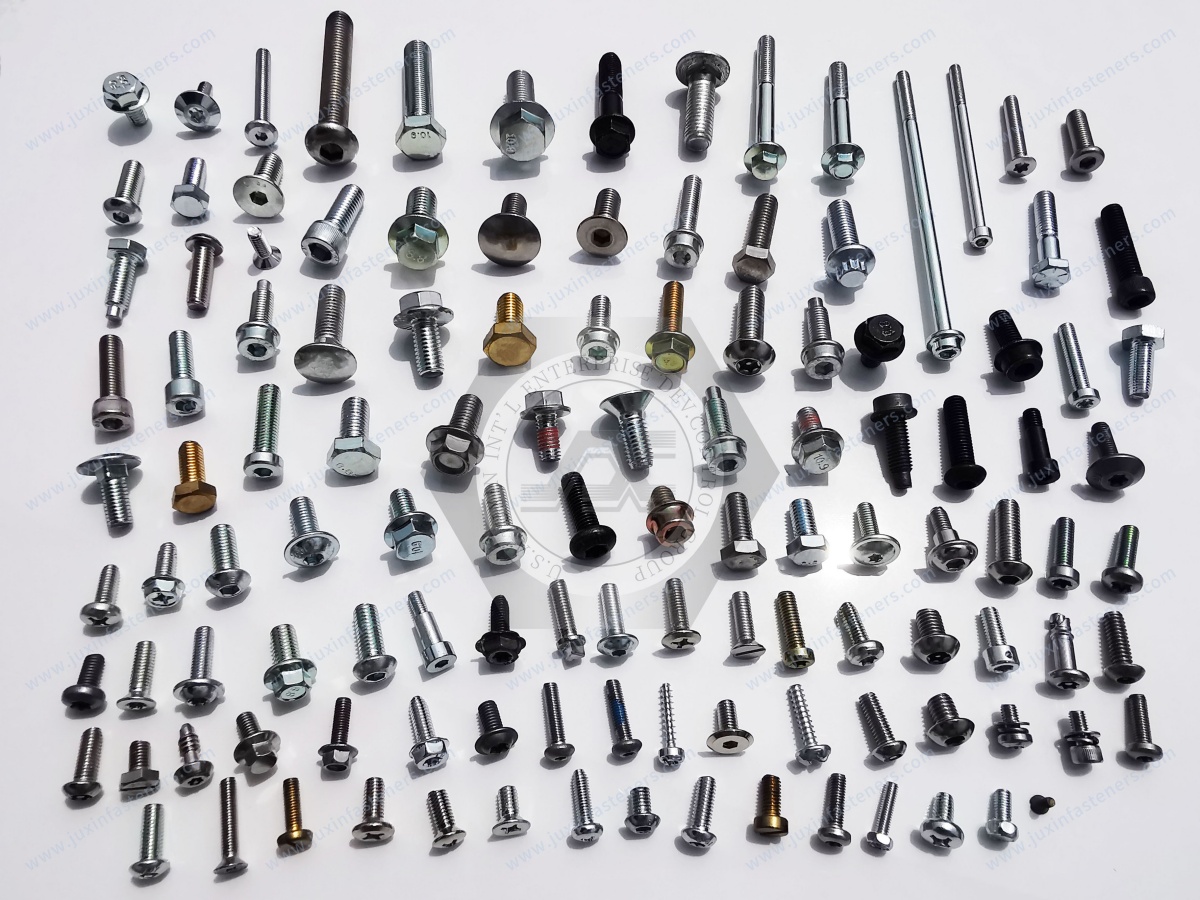
Typical EV battery fasteners include:
Battery pack bolts
Battery enclosure bolts
Long battery studs
Battery module tie rods
Self-clinching nuts
Self-clinching studs
Weld studs
Weld nuts
Threaded inserts
High-strength structural bolts
Aluminum and stainless steel fastening components
For battery enclosure systems, engineers should evaluate:
Required clamping force
Battery enclosure material
Thread engagement
Joint stiffness
Thermal expansion
Corrosion resistance
Electrical isolation requirements
Sealing requirements
Assembly torque
Serviceability
Production cycle time
Long-term vibration resistance
For high-volume EV production, the fastener must also be compatible with automated feeding, robotic installation, torque-controlled assembly, optical inspection, and traceability systems.
Electric vehicles contain numerous components exposed to elevated temperatures, including electric motors,
reduction gear systems, thermal management assemblies, heat exchangers, coolant systems, and other power electronics.
Where operating temperatures exceed the practical range of conventional carbon steel fasteners, stainless steel or nickel-based alloys may be required.
Potential materials include:
A286 / EN 1.4980
Inconel 718 / UNS N07718
Austenitic stainless steels
Other application-specific heat-resistant alloys
Selection should consider:
Tensile strength at temperature
Creep resistance
Oxidation resistance
Thermal expansion
Thread galling
Corrosion environment
Surface treatment
Assembly torque
Long-term fatigue performance
For high-temperature threaded assemblies, material compatibility and anti-galling measures can be just as important as nominal tensile strength.
This decision matrix aligns fastener selection with manufacturing efficiency, joint load requirements, environmental exposure, and EV supply-chain objectives.
| Application Target | Primary Fastener Choice | Engineering Selection Criteria | Strategic Procurement Focus | Target Role |
|---|---|---|---|---|
| EV Battery Pack Enclosures | Long Battery Studs / High-Strength Bolts / Self-Clinching Hardware | Fatigue performance, straightness, thread accuracy, corrosion protection, thermal cycling and joint preload | Cost, dimensional consistency, batch traceability, automated assembly compatibility | EV Battery Lead / Purchasing Manager |
| Battery Module Tie-Rod Systems | Long M6 / M8 Battery Studs and Tie Rods | Length, straightness, tensile properties, thread concentricity and end geometry | Stable cold-forming capability, thread rolling, 100% or specified inspection | Battery Structural Engineer / Sourcing Specialist |
| Electric Powertrain / Motors | High-Strength Bolts Class 10.9 / 12.9 | High preload, fatigue resistance, controlled friction and compact packaging | Torque-tension testing, coating consistency, optical sorting and batch traceability | Drive System Engineer / Sourcing Specialist |
| Aluminum-Steel BIW Joinery | Corrosion-Controlled Steel Fasteners / Self-Clinching Inserts | Galvanic corrosion protection, coating compatibility and joint stiffness | Zinc-flake / zinc-nickel coating, RoHS / REACH compliance and corrosion validation | Body Engineer / Supply Chain Lead |
| EV Sheet Metal Structures | Self-Clinching Nuts / Self-Clinching Studs / Weld Fasteners | Sheet thickness, hole size, push-out resistance and torque-out resistance | Automated installation, dimensional consistency and OEM validation | BIW Engineer / Procurement Manager |
| Automotive Wiring & Grounding Points | Weld Studs / Weld Nuts | Weld integrity, conductivity where required, positioning accuracy and corrosion protection | Stable welding process, inspection and traceability | Electrical Engineer / Strategic Sourcing |
| High-Temperature Thermal Systems | A286 Stainless / Inconel 718 Alloy Fasteners | High-temperature strength, creep resistance, oxidation resistance and galling control | Material certification, heat-treatment records and MTRs | Thermal Engineer / Strategic Sourcing |
For automotive and EV programs, fastener quality depends on the consistency of the complete manufacturing process rather than only the final mechanical test.
A robust production process may include:
Raw Material Verification
        ↓
Wire / Bar Preparation
        ↓
Cold Heading / CNC Machining
        ↓
Thread Rolling / Thread Forming
        ↓
Heat Treatment Where Required
        ↓
Surface Treatment / Coating
        ↓
Dimensional Inspection
        ↓
Mechanical Testing
        ↓
Torque / Clamp-Force Verification
        ↓
Optical Sorting
        ↓
Packaging & Batch Traceability
Important quality-control characteristics can include:
Material certificates
Chemical composition verification
Tensile strength
Yield / proof load
Hardness
Thread dimensions
Thread gauge inspection
Head dimensions
Shank diameter
Straightness
Surface defects
Coating thickness
Coating adhesion
Friction coefficient
Torque-tension relationship
Corrosion resistance
Optical sorting
Lot traceability
For EV battery fasteners and automotive structural hardware, the final inspection plan should be agreed according to the customer's engineering drawing, control plan,
PPAP requirements, and applicable international standards.
Expand your technical knowledge by exploring adjacent JUXIN FASTENERS engineering documentation:
Automotive Wheel Fasteners & Lightweight Aluminum Joinery Guide
https://www.juxinfasteners.com/automotive-solutions/wheel-hub-bolts-nuts-aluminum-body-fasteners/
Mechanics of wheel bolts, wheel studs, lug nuts, flow drill screws (FDS), self-piercing rivets (SPR), and lightweight aluminum automotive structures.
Preventing Bolt Loosening & Fatigue Failure Solutions
https://www.juxinfasteners.com/technical-guide/bolt-loosening-fatigue-failure-prevention-solutions/
Engineering analysis of rotational loosening, preload loss, transverse vibration, fatigue failure, and high-vibration fastener solutions.
Specialized Nut Engineering Guide: Cap Nuts, Wing Nuts & Titanium Flange Nuts
https://www.juxinfasteners.com/industrial-solutions/cap-nuts-wing-nuts-titanium-flange-nuts-engineering-guide/
Material selection and engineering considerations for lightweight, corrosion-resistant, and application-specific nut assemblies.
Threaded Inserts for Plastics: Engineering Installation Guide
https://www.juxinfasteners.com/industrial-solutions/thread-insert-nuts-engineering-installation-guide/
Post-mold thread insert selection, polymer boss design, installation methods, and engineering considerations for plastic housings.
Precision Knurled Brass Threaded Inserts Guide
https://www.juxinfasteners.com/industrial-solutions/knurled-brass-inserts-after-molding-installation-guide/
Heat-staking, ultrasonic insertion, knurled brass insert geometry, and after-molding installation for automotive electronics and industrial plastic components.
JUXIN FASTENERS manufactures and supplies high-precision automotive and industrial fastening components for OEM, Tier-1, and industrial customers.
Our manufacturing capabilities include multi-station cold heading, precision thread rolling, CNC machining, automated inspection, and application-specific surface treatment.
For EV and automotive programs, JUXIN FASTENERS can support requirements involving:
EV battery pack fasteners
EV battery enclosure fasteners
Long battery studs
Battery module tie rods
High-strength automotive bolts
Class 8.8 / 10.9 / 12.9 fasteners
Self-clinching nuts
Self-clinching studs
Automotive weld studs
Automotive weld nuts
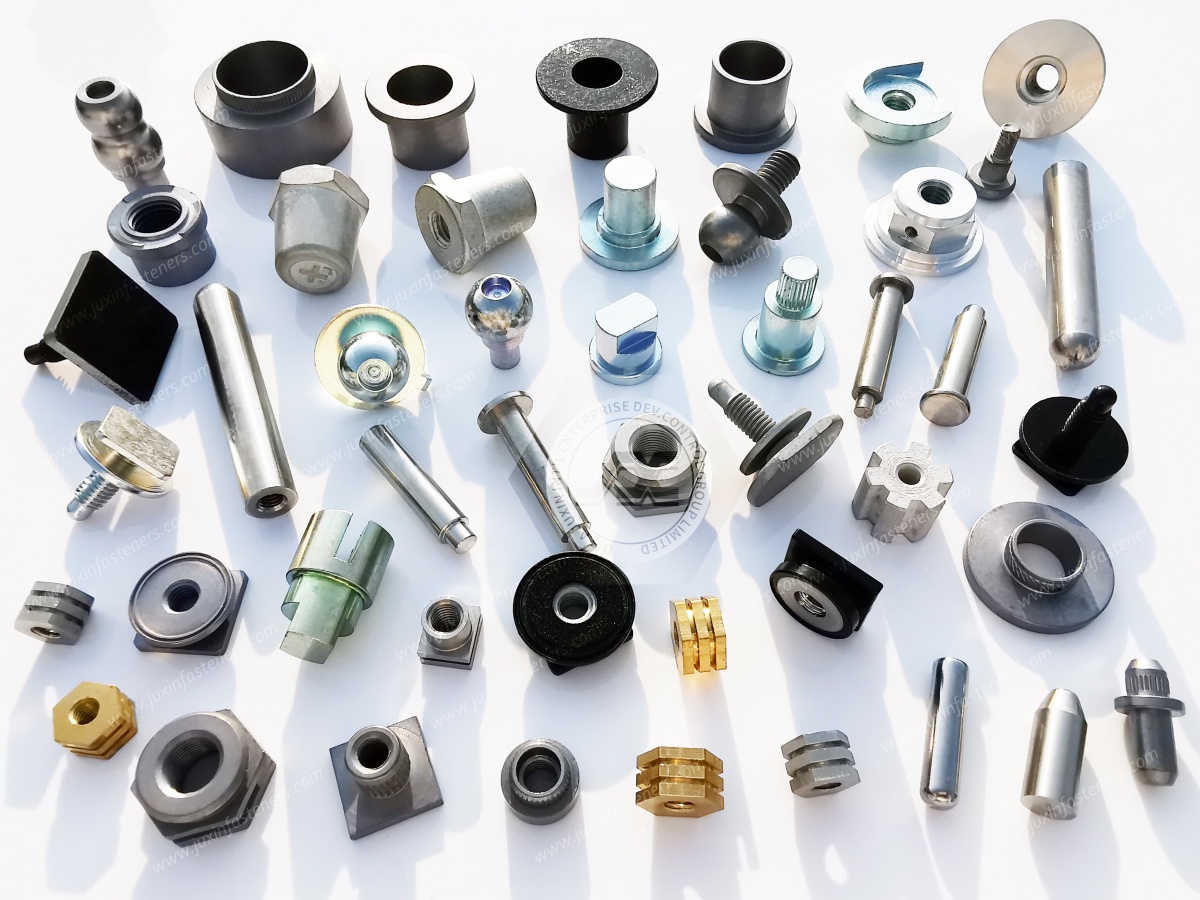
Threaded inserts
Aluminum joining fasteners
Corrosion-resistant automotive fasteners
High-temperature alloy fasteners
Custom cold-formed automotive hardware
Custom CNC-machined fasteners
For engineering and procurement teams, technical documentation can be developed according to project requirements, including dimensional drawings,
material documentation, inspection reports, PPAP documentation, samples, and application-specific specifications.
Contact our technical application team for 3D CAD files, PPAP documentation, samples, custom fastener development, or RFQ support.
Official Corporate Website:
https://www.juxinfasteners.com
Engineering & Sourcing Email:
info@juxinfasteners.com
Manufacturing Portfolio:
EV Battery Studs, EV Battery Pack Fasteners, Ultra-High-Strength Automotive Fasteners, Class 10.9 / 12.9 Bolts, Self-Clinching Hardware,
Automotive Weld Studs, Weld Nuts, High-Temperature Alloy Fasteners, Precision Cold-Formed Components, and Custom CNC Turned Hardware.
 MORE NEWS

Sep. 25, 2026

Sep. 25, 2026

Sep. 25, 2026
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY