Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809
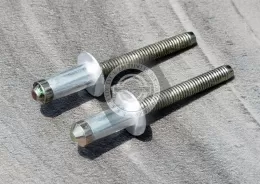
High-Strength Lockbolts (Ring-Groove Locking-Collar Rivets)
JUXIN FASTENERS offers ring-groove lockbolt fastening solutions for OEM structural assemblies requiring a two-piece pin-and-collar connection.
Available product families for technical review include:
(A) Aluminum — JX-D-L-AL
(B) Steel — JX-D-L-ST
(C) Stainless Steel — JX-D-L-SS
A compatible locking collar is swaged into the pin grooves using dedicated installation tooling, producing a permanent mechanically locked connection. Installation normally requires access to both sides of the assembly.
Break-pintail, continuous-groove and pintail-less designs have different installation requirements and must not be treated as interchangeable. Actual materials, compatible collars, dimensions, mechanical strength, grip ranges and tooling require verification against the approved product specification.
Technical reference: Original PDF/CAD, pages 109–110.
Product Specification
High-Strength Lockbolts and Ring-Groove Locking-Collar Rivets for OEM Structural Assemblies
Product Overview
JUXIN FASTENERS supplies ring-groove locking-collar fastening solutions for OEM manufacturing, industrial equipment and structural metal assemblies.
These fasteners are commonly described in the international market as:
High-Strength Lockbolts
Locking-Collar Rivets
Ring-Groove Rivets
Ring-Groove Lockbolts
Two-Piece Structural Fasteners
Swage-Collar Fasteners
Pin-and-Collar Fasteners
Unlike conventional blind rivets, typical two-piece lockbolts consist of a grooved pin and a separate deformable locking collar.
During installation, a compatible tool develops the required joint clamp and swages the collar into the locking grooves of the pin.
This creates a permanent mechanically locked connection.
Typical lockbolt installation requires access to both sides of the joined components.
Lockbolt systems are used where engineers require controlled fastening, vibration resistance, installation efficiency and structural joint performance appropriate to the selected fastener.
Actual mechanical properties depend on the pin material, collar material, geometry, installation system and approved engineering specification.
Available JUXIN Material Families
JUXIN identifies three material families for technical evaluation and quotation.
| Material Family | JUXIN Reference | Original Material Description |
|---|---|---|
| Aluminum | JX-D-L-AL | Aluminum pin and aluminum collar components |
| Steel | JX-D-L-ST | Steel pin and steel collar components |
| Stainless Steel | JX-D-L-SS | Stainless steel pin and stainless steel collar components |
These references identify the product families provided in the original JUXIN documentation.
The actual pin alloy, collar alloy, material condition, coating and mechanical performance must be verified for each selected part number.
The pin and collar should be specified as separate components rather than described as a rivet body and blind-rivet mandrel.
Product Identification and Technical Specifications
| Item | Specification |
|---|---|
| Product Name | High-Strength Lockbolts / Ring-Groove Locking-Collar Rivets |
| Product Category | Structural / High-Strength Fasteners |
| Fastener Construction | Two-Piece Pin and Collar |
| Pin Geometry | Ring-Groove / Lock-Groove Design |
| Locking Mechanism | Swaged Collar |
| Material Families | Aluminum, Steel, Stainless Steel |
| Installation Access | Normally Two-Sided |
| Installation Method | Dedicated Lockbolt Installation Tool |
| Pin Head Style | According to approved drawing |
| Pin Diameter | According to approved drawing |
| Grip Range | According to selected system |
| Locking Collar | Compatible collar required |
| Pintail Configuration | Product-specific |
| Mechanical Performance | Verified product data required |
| Corrosion Protection | According to approved specification |
| Technical Reference | Original PDF/CAD, pages 109–110 |
Engineering Solution 1 — How a Lockbolt Works
A conventional two-piece lockbolt assembly consists of a pin and a collar.
The pin passes through the aligned mounting holes of the joined components.
The collar is positioned over the pin on the opposite side.
A compatible installation tool applies the required pulling and swaging forces.
As the tool operates, the joint is drawn together and the collar is plastically deformed into the pin's locking grooves.
The swaged collar creates a permanent mechanical connection with the grooved pin.
Depending on the system, the installation may conclude with a designed pintail break or with release of the tool from an unbroken pin.
The exact installation sequence must follow the approved fastener and tooling instructions.
Engineering Solution 2 — Lockbolts vs. Structural Blind Rivets
| Engineering Factor | Two-Piece Lockbolt | Structural Blind Rivet |
|---|---|---|
| Main Components | Pin and separate collar | Rivet body and pull mandrel |
| Installation Access | Normally both sides | One side |
| Joint Formation | Collar swaged into pin grooves | Blind-side rivet body deformation |
| Fastening Method | Dedicated lockbolt tool | Compatible blind-rivet tool |
| Pin or Mandrel Break | Depends on lockbolt design | Typically designed mandrel break |
| Clamp and Strength | System-specific | System-specific |
| Typical Selection | Accessible structural joints | Restricted rear-side access |
The two fastener types should not be substituted without engineering evaluation.
Engineering Solution 3 — Ring-Groove and Collar Locking Mechanism
The ring grooves provide a mechanical interface between the pin and the swaged collar.
During installation, the collar material flows into the grooves.
The resulting connection resists separation through mechanical engagement between the two components.
Important design parameters include:
Pin diameter
Groove geometry
Groove spacing
Collar dimensions
Collar material
Pin material
Grip length
Installation force
Tool nose assembly
Installed collar condition
A compatible pin and collar combination is essential.
Collars from different product systems must not be assumed interchangeable.
Engineering Solution 4 — Break-Pintail Lockbolts
Certain lockbolt systems use a break-pintail design.
The installation tool grips the pulling section of the pin.
As the tool applies force, the joint is tightened and the collar is swaged into the locking grooves.
After the required installation sequence, the excess pintail breaks at a designed location.
Engineering considerations include:
Breakneck geometry
Required pulling force
Swage completion
Break location
Pintail collection
Tool recoil
Installed pin projection
The pintail must break only as intended by the approved system.
Engineering Solution 5 — Pintail-Less Lockbolts
Other lockbolt systems use a pintail-less or non-break-stem design.
These systems are designed to complete the collar swaging operation without breaking off an installation tail.
Potential system-level advantages may include reduced discarded metal, reduced installation noise and simplified handling of spent tails.
However, these characteristics depend on the actual fastener and tooling design.
Huck BobTail is a proprietary example of a pintail-less lockbolt system.
The original JUXIN information does not establish that JX-D-L-AL, JX-D-L-ST or JX-D-L-SS are equivalent to Huck BobTail.
Engineering Solution 6 — Continuous-Groove Lockbolts
Certain lockbolt systems incorporate an extended or continuous groove configuration.
This can affect the available grip range and collar positioning.
Engineers should verify:
Groove length
Effective grip range
Pin projection
Collar compatibility
Installation tooling
Final installed dimensions
Continuous-groove construction should not be assumed for every ring-groove fastener.
Engineering Solution 7 — Aluminum Lockbolts
JUXIN Reference: JX-D-L-AL
The aluminum material family may be considered for applications where weight reduction and compatible material selection are important.
Potential applications include lightweight equipment frames, selected transportation components and aluminum structural assemblies.
Engineering considerations include:
Pin alloy
Collar alloy
Material temper
Shear strength
Tensile strength
Joint clamp requirements
Corrosion compatibility
Fatigue performance
Installation tooling
The original documentation mentions 7A03 aluminum for the pin and 5052 aluminum for the collar.
These exact grades require verification before being adopted as confirmed product specifications.
Aluminum lockbolts should not automatically be assigned the same mechanical performance as steel lockbolts.
Engineering Solution 8 — Steel Lockbolts
JUXIN Reference: JX-D-L-ST
Steel lockbolts may be considered for mechanically demanding industrial assemblies.
Potential applications include commercial vehicles, heavy equipment, steel structures and industrial machinery.
Important engineering considerations include:
Pin steel grade
Collar steel grade
Mechanical properties
Heat treatment
Surface coating
Joint clamp requirements
Shear and tensile capacity
Fatigue performance
Corrosion exposure
The original documentation refers to 35 steel and 10 steel.
These descriptions require verification against current material specifications and actual manufacturing records.
No strength class, coating performance or structural approval is claimed without supporting evidence.
Engineering Solution 9 — Stainless Steel Lockbolts
JUXIN Reference: JX-D-L-SS
Stainless steel lockbolts may be considered for applications where appropriate corrosion resistance is required.
Potential applications include industrial equipment, outdoor enclosures, stainless steel structures and selected transportation equipment.
Important considerations include:
Pin stainless steel grade
Collar stainless steel grade
Mechanical properties
Material compatibility
Corrosion resistance
Chloride exposure
Galling behavior
Installation force
Joint fatigue performance
The original documentation refers to 0Cr18Ni9 and 1Cr18Ni9 stainless steel.
These are legacy material designations and should not automatically be converted to a current international grade without verification.
No specific AISI 304, AISI 316, A2 or A4 specification is claimed.
Engineering Solution 10 — Shear Strength
Shear loading acts across the fastener and joint interface.
Lockbolt shear capacity depends on:
Pin diameter
Pin material
Pin geometry
Shear-plane location
Joint thickness
Hole dimensions
Installation quality
The connected materials may also fail through bearing deformation or edge failure.
Actual shear performance must be verified for the selected lockbolt system.
Engineering Solution 11 — Tensile Strength
Tensile loading acts primarily along the fastener axis.
Potential failure mechanisms include:
Pin fracture
Collar failure
Collar disengagement
Head-side pull-through
Panel deformation
Local material failure
The collar's engagement with the pin grooves is a critical part of the tensile load path.
Actual tensile performance must be verified using the applicable product specification.
Engineering Solution 12 — Clamp Force and Joint Integrity
Clamp force is an important characteristic of many lockbolt systems.
During installation, the pin and collar system draws the joined components together.
The resulting clamp depends on the fastener design, material properties, tool operation and joint characteristics.
Relevant parameters include:
Joint thickness
Material stiffness
Surface condition
Installation force
Collar swaging
Joint relaxation
Thermal cycling
No numerical clamp force is claimed without verified product data.
Engineering Solution 13 — Vibration and Fatigue Resistance
Properly engineered lockbolt connections can provide useful resistance to loosening in vibration-exposed assemblies.
However, vibration resistance is not universal across every material or geometry.
Engineers should evaluate:
Joint stiffness
Clamp retention
Pin and collar engagement
Hole fit
Fastener spacing
Cyclic loading
Fatigue
Corrosion
Installation quality
Critical applications should use representative joint testing and approved acceptance criteria.
Engineering Solution 14 — Thermal Expansion and Contraction
Industrial equipment may experience repeated temperature changes.
Differential thermal expansion between the pin, collar and joined components can affect joint loading.
Important considerations include:
Pin material
Collar material
Mating material
Operating temperature
Temperature cycling
Joint stiffness
Clamp relaxation
Lockbolts should not be described as universally unaffected by thermal expansion or contraction.
Engineering Solution 15 — Hole Diameter and Joint Preparation
Hole quality is essential for reliable lockbolt installation.
Engineers should verify:
Hole diameter
Hole tolerance
Hole alignment
Burr condition
Material thickness
Edge distance
Fastener spacing
Joint gap
Surface coatings
Oversized, slotted or damaged holes require specific engineering approval.
A lockbolt should not be used to compensate for an unacceptable hole condition without validation.
Engineering Solution 16 — Grip Range and Pin Length
The selected pin must accommodate the complete material stack-up and the compatible collar.
Important parameters include:
Minimum grip
Maximum grip
Pin length
Collar thickness
Available locking grooves
Tool engagement length
Installed pin projection
Incorrect grip selection may prevent full collar swaging or proper joint formation.
Engineering Solution 17 — Collar Compatibility
A lockbolt collar is an engineered component, not a generic washer or nut.
The collar must be compatible with:
Pin diameter
Groove geometry
Material grade
Collar hardness
Swaging force
Nose assembly
Required joint performance
A collar sold separately by a distributor does not establish interchangeability with every lockbolt pin.
For OEM purchasing, the pin and collar should be specified as a matched system.
Engineering Solution 18 — Installation Tooling
Lockbolts generally require dedicated hydraulic, pneumatic or other approved installation equipment.
Tool selection depends on:
Pin diameter
Pin geometry
Collar dimensions
Pulling force
Swaging force
Tool stroke
Nose assembly
Installation access
Production cycle time
Tool maintenance
Some lockbolt systems use different tooling for break-pintail and pintail-less configurations.
The actual JUXIN fastener must be matched to its approved tool and nose assembly.
Typical Installation Procedure
The following is a general procedure for a conventional two-piece lockbolt system.
Confirm the approved pin and collar part numbers.
Verify pin and collar material specifications.
Check the complete joint stack-up.
Select the correct grip range.
Prepare aligned mounting holes within the approved tolerances.
Remove burrs and inspect the joint surfaces.
Insert the pin through the assembled components.
Position the compatible collar on the opposite side.
Select the approved installation tool and nose assembly.
Engage the tool with the pin.
Activate the tool according to the approved installation procedure.
Allow the collar to be swaged into the locking grooves.
Complete the pintail break if required by the selected design.
Release the tool after the specified installation cycle.
Inspect the collar swage, pin projection and joint condition.
Verify the installation against the approved acceptance criteria.
Pintail-less systems follow their own installation sequence and must not be treated as break-pintail systems.
Engineering Solution 19 — Production Inspection
Production quality control should include:
Pin identification
Collar identification
Material verification
Dimensional inspection
Hole diameter
Grip range
Tool identification
Nose assembly condition
Collar orientation
Swage completion
Installed collar geometry
Pin projection
Pintail break condition, where applicable
Joint gap
Sampling and traceability
Certain proprietary lockbolt systems include dedicated installation indicators or inspection gauges.
Such features should not be assumed for JUXIN products without verification.
Engineering Solution 20 — Metric and Inch Size Reference
Common industrial lockbolt diameter references may include:
| Metric Reference | Approximate Inch Reference |
|---|---|
| 4.8 mm | 3/16 in |
| 6.4 mm | 1/4 in |
| 7.9 mm | 5/16 in |
| 9.5 mm | 3/8 in |
| 12.7 mm | 1/2 in |
| 15.9 mm | 5/8 in |
These are general dimensional references, not confirmed available sizes for the JUXIN JX-D-L series.
Actual metric and inch-designated lockbolts must be verified for pin diameter, hole size, grip range, collar compatibility and tooling before substitution.
Industrial Applications and Engineering Solutions
Lockbolts may be evaluated for industrial assemblies requiring permanent two-piece mechanical fastening and appropriate structural performance.
The following applications are potential engineering uses, not product-specific approvals.
1. Commercial Vehicle Manufacturing
Lockbolts may be considered for selected truck and commercial vehicle assemblies requiring permanent structural fastening.
Relevant factors include fatigue, vibration, corrosion, installation access and OEM qualification.
2. Trailer Manufacturing
Trailers may incorporate steel and aluminum structural assemblies.
Lockbolts may be evaluated where the approved design requires a mechanically locked pin-and-collar connection.
3. Heavy Equipment
Construction and mining equipment may require permanent fastening in vibration-exposed assemblies.
Mechanical strength, fatigue, corrosion and service conditions must be validated.
4. Agricultural Machinery
Agricultural equipment may incorporate structural frames, brackets and machinery components.
Lockbolts may be evaluated for suitable permanent connections.
5. Rail Equipment
Rail equipment may use lockbolt fastening systems in approved structural or auxiliary assemblies.
Fatigue, vibration, fire and smoke, traceability and project-specific requirements must be reviewed.
6. Industrial Steel Structures
Steel structures may incorporate mechanically fastened joints.
Any use of lockbolts in load-bearing construction requires compliance with the applicable structural design and qualification requirements.
7. Industrial Machinery Frames
Machinery frames may require controlled permanent mechanical connections.
Joint stiffness, alignment, loading and maintenance requirements must be evaluated.
8. Material Handling Equipment
Conveyors, lifting-related equipment and handling systems may include structurally loaded metal assemblies.
Safety-critical applications require appropriate engineering qualification.
9. Energy Infrastructure
Energy equipment may incorporate structural frames, brackets and support assemblies.
Lockbolts may be evaluated where the selected material and mechanical properties meet the design requirements.
10. Power Distribution Equipment
Power distribution infrastructure may use structural support frames and auxiliary equipment assemblies.
Electrical bonding and grounding must be evaluated separately.
11. Data Center Infrastructure
Data center projects may include heavy equipment supports, power-system frames and auxiliary structural assemblies.
Lockbolts may be considered where two-sided access and permanent fastening are appropriate.
12. Industrial Enclosures
Large industrial enclosures may use lockbolts for selected structural connections.
The joint must be evaluated for strength, access, corrosion and maintenance requirements.
13. Container and Modular Equipment
Containers and modular equipment may include structural steel or aluminum connections.
Lockbolts may be considered for suitable approved joints.
14. Marine Auxiliary Structures
Marine-related equipment may require corrosion-resistant fastening.
Stainless steel or protected steel lockbolts must be selected according to the actual exposure conditions.
15. OEM Metal Fabrication
OEM manufacturers may specify lockbolts for repetitive production assemblies requiring defined installation procedures and consistent mechanical fastening.
Material Selection Matrix
| Application Requirement | Engineering Consideration |
|---|---|
| Lightweight assembly | Evaluate aluminum pin-and-collar system |
| High mechanical loading | Evaluate verified steel lockbolt data |
| Corrosion-sensitive environment | Evaluate stainless steel or protected steel |
| Vibration exposure | Validate complete joint fatigue performance |
| Wide material stack-up variation | Verify actual grip capability |
| Two-sided installation access | Confirm pin and collar accessibility |
| High-volume assembly | Evaluate installation tooling and cycle time |
| Low-noise installation | Consider verified pintail-less systems |
| Structural qualification | Require applicable test data and approvals |
| Outdoor exposure | Evaluate corrosion and coating compatibility |
International Standards and Technical Qualification
Lockbolt systems may be specified using manufacturer technical specifications, customer-approved engineering drawings and applicable industry standards.
The term ring-groove rivet does not identify one universal international product standard.
Different lockbolt systems use different groove geometries, collars, installation procedures and mechanical performance requirements.
Technical qualification should establish:
Pin material grade
Collar material grade
Pin dimensions
Collar dimensions
Groove geometry
Grip range
Hole requirements
Shear and tensile strength
Clamp requirements
Fatigue performance
Installation tooling
Corrosion protection
Inspection criteria
Where ISO, DIN, EN, ASTM, SAE or customer-specific requirements apply, conformity must be verified against the actual fastener.
Huck Magna-Grip and Huck BobTail are proprietary fastening systems. Product equivalence must not be inferred from appearance or generic lockbolt terminology.
No unverified certification or proprietary system equivalence is claimed.
OEM Procurement and Supplier Development
For purchasing managers, supply chain managers, production managers and engineers, lockbolts should be sourced as complete fastening systems.
A technical RFQ should identify:
Approved pin drawing
Approved collar drawing
Material family
Pin material grade
Collar material grade
Pin diameter
Pin length
Head style
Grip range
Hole diameter
Lock-groove configuration
Break-pintail or pintail-less design
Required shear strength
Required tensile strength
Required clamp performance
Corrosion requirements
Installation tooling
Inspection requirements
Annual demand forecast
Purchasing teams should confirm whether quotations include pins only, collars only or matched pin-and-collar assemblies.
The total installed cost should consider fastener cost, tooling, installation cycle time, inspection, scrap and maintenance.
Frequently Asked Questions
What is a locking-collar rivet?
It is a two-piece fastener consisting of a grooved pin and a collar that is mechanically swaged into the pin grooves during installation.
Are locking-collar rivets the same as lockbolts?
Locking-collar rivets is a common market description for certain two-piece lockbolt systems. Exact designs vary.
Are ring-groove rivets blind rivets?
Typical two-piece ring-groove lockbolts require access to both sides of the assembly and are not conventional one-sided blind rivets.
What is the difference between Magna-Grip and BobTail?
They refer to distinct proprietary lockbolt product systems. Their pin geometry, installation method and tooling requirements must be evaluated separately.
Does every lockbolt break off a pintail?
No. Some designs use a break-pintail, while pintail-less systems complete installation without a pin break.
Can lockbolt pins and collars be purchased separately?
Some suppliers offer separate components. However, the pin and collar must be verified as a compatible fastening system.
Are aluminum lockbolts as strong as steel lockbolts?
Not necessarily. Mechanical strength depends on the actual material grades, geometry and verified product data.
Are stainless steel lockbolts corrosion-proof?
No. Corrosion resistance depends on the alloy, environment and joint design.
Can lockbolts withstand vibration?
Properly engineered lockbolt systems can provide useful vibration resistance, but the complete joint must be validated.
Can a lockbolt replace a conventional bolt and nut?
Only after engineering review of the mechanical requirements, installation access, serviceability and applicable specifications.
Can JUXIN review custom ring-groove lockbolt drawings?
Customer drawings, material specifications, collar requirements, mechanical performance targets and annual demand can be submitted for technical review and quotation.
Request a High-Strength Lockbolt OEM Quotation
JUXIN FASTENERS supplies industrial fastening solutions for OEM manufacturing, heavy equipment and structural metal assemblies.
For technical review and quotation, please provide:
2D engineering drawing or 3D CAD model
JUXIN reference: JX-D-L-AL, JX-D-L-ST or JX-D-L-SS
Pin material specification
Collar material specification
Pin diameter and length
Head style
Groove geometry
Grip range
Hole diameter and tolerance
Required shear and tensile performance
Clamp and fatigue requirements
Break-pintail or pintail-less configuration
Installation tooling and nose assembly requirements
Surface coating and corrosion requirements
Inspection and traceability requirements
Pin and collar packaging requirements
Expected order quantity
Annual demand forecast
Target delivery schedule
Email: info@juxinfasteners.com
Website: https://www.juxinfasteners.com/
JUXIN FASTENERS — High-Strength Lockbolts and Ring-Groove Locking-Collar Rivets for Global OEM Manufacturing.
Product Packaging
Packaging Standard
At Juxin Fasteners, we apply standardized export packaging to ensure product protection, traceability, and compliance with international logistics requirements.
1. Standard Export Packaging
Unless otherwise specified, all products will be packed according to our factory standard export packaging, which includes:
Moisture-resistant inner protection
Poly bag or small box packing as required
Reinforced export cartons
Clear labeling with part number, specification, batch number, and quantity
Palletizing for sea or air shipment when necessary
Our standard packaging is designed to ensure safe transportation, efficient warehousing, and long-distance international shipping.
2. Customized Packaging Options
We also provide customized packaging solutions according to customer requirements, including but not limited to:
Private labeling
Customized barcodes
Specific carton dimensions
Retail packaging
Special pallet configuration
Customer-specific marking and identification
So that you know, customized packaging may involve additional costs and extended lead time depending on the complexity of the requirements.
3. Compliance & Quality Assurance
All packaging processes are controlled under our ISO 9001 quality management system to ensure consistency, traceability, and product integrity throughout the supply chain.
Product Pictures


Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY