Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809
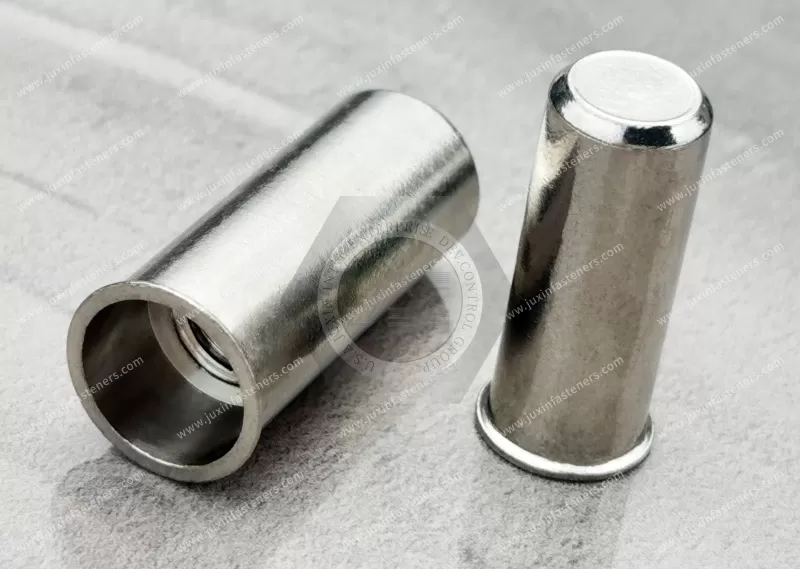
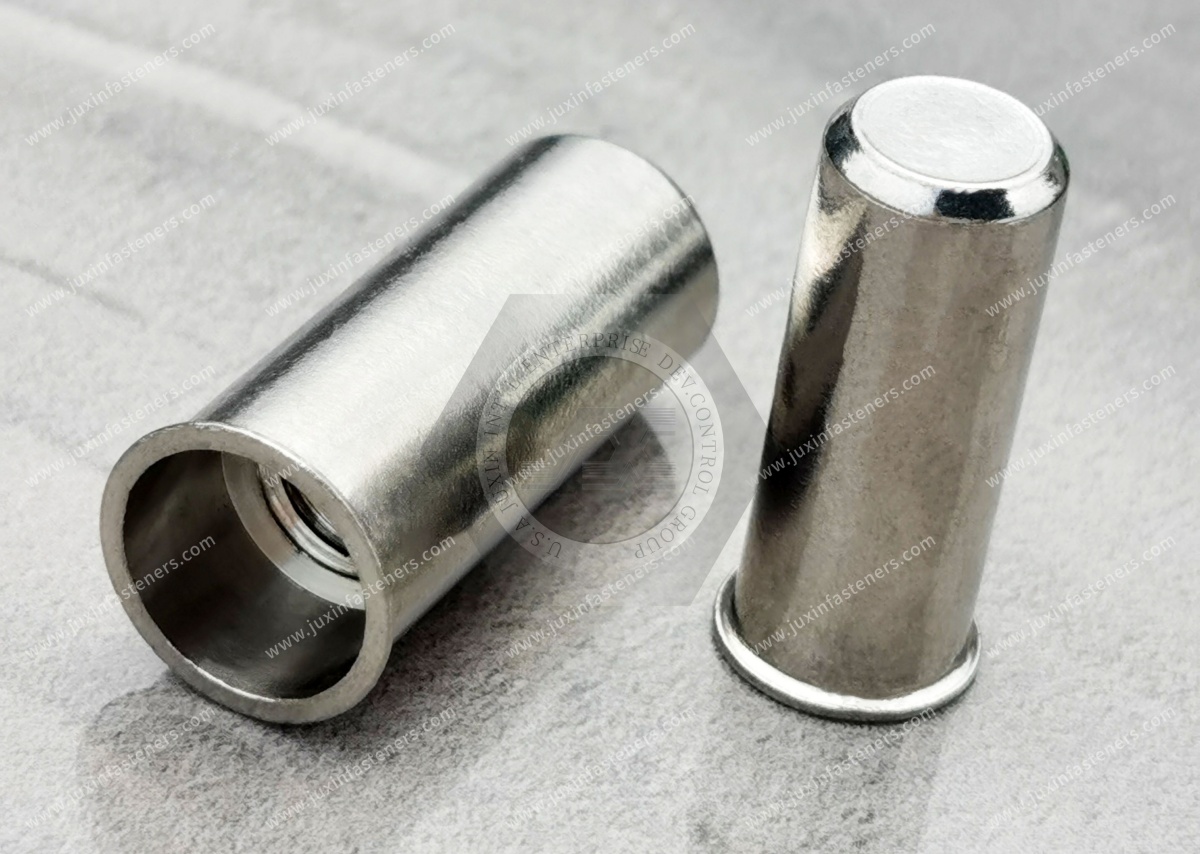
JUXIN FASTENERS manufactures stainless steel thin head, closed-end plain body blind rivet nuts for creating reusable internal threads in thin sheet metal, compact enclosures, and OEM assemblies requiring one-sided installation.
The low-profile flange reduces head projection compared with conventional flat-head rivet nuts, while the smooth cylindrical body fits compatible round mounting holes. The closed-end barrel prevents screws from passing through the insert and blocks direct passage through the threaded cavity.
Product Features
Metric threads: M3, M4, M5, M6, M8, M10
Inch-series threads: Custom OEM requirements subject to drawing review
Material: Stainless steel (grade subject to confirmation)
Grip range: 0.5–3.5 mm (approx. 0.020–0.138 in), depending on size
Head: Thin head / Low-profile flange
Body: Plain / Smooth round body
End: Closed end
Mounting hole: Round hole, according to product drawing
Installation: One-sided blind installation
Applications include electrical enclosures, automotive components, electronics housings, industrial machinery, HVAC equipment, and compact OEM sheet-metal assemblies requiring low-profile enclosed threaded inserts.
Product Specification
Technical Specifications — Stainless Steel Thin Head Closed-End Plain Body Blind Rivet Nuts
Low-Profile Closed-End Threaded Insert Engineering
JUXIN FASTENERS stainless steel thin head closed-end plain body blind rivet nuts are designed to create mechanically retained internal threads in thin sheet metal, hollow sections and fabricated equipment housings.
The product incorporates a low-profile flange, a smooth cylindrical body and a closed-end threaded cavity.
Its principal engineering characteristics are reduced flange projection, one-sided installation and controlled mating bolt penetration.
The plain round-body configuration is intended for a suitably dimensioned round mounting hole.
Unlike knurled or hexagonal body designs, it does not introduce external ribs or noncircular geometry for additional rotational engagement.
The correct product must therefore be selected according to panel thickness, hole dimensions, required tightening torque, usable thread depth and installation conditions.
Product Technical Data
| Technical Parameter | Specification |
|---|---|
| Product Type | Stainless Steel Low-Profile Closed-End Blind Rivet Nut |
| Head Configuration | Thin Head / Low-Profile Flange |
| Body Configuration | Plain Round Body / Smooth Cylindrical Body |
| End Configuration | Closed End |
| Material | Stainless Steel |
| Metric Thread Sizes | M3, M4, M5, M6, M8, M10 |
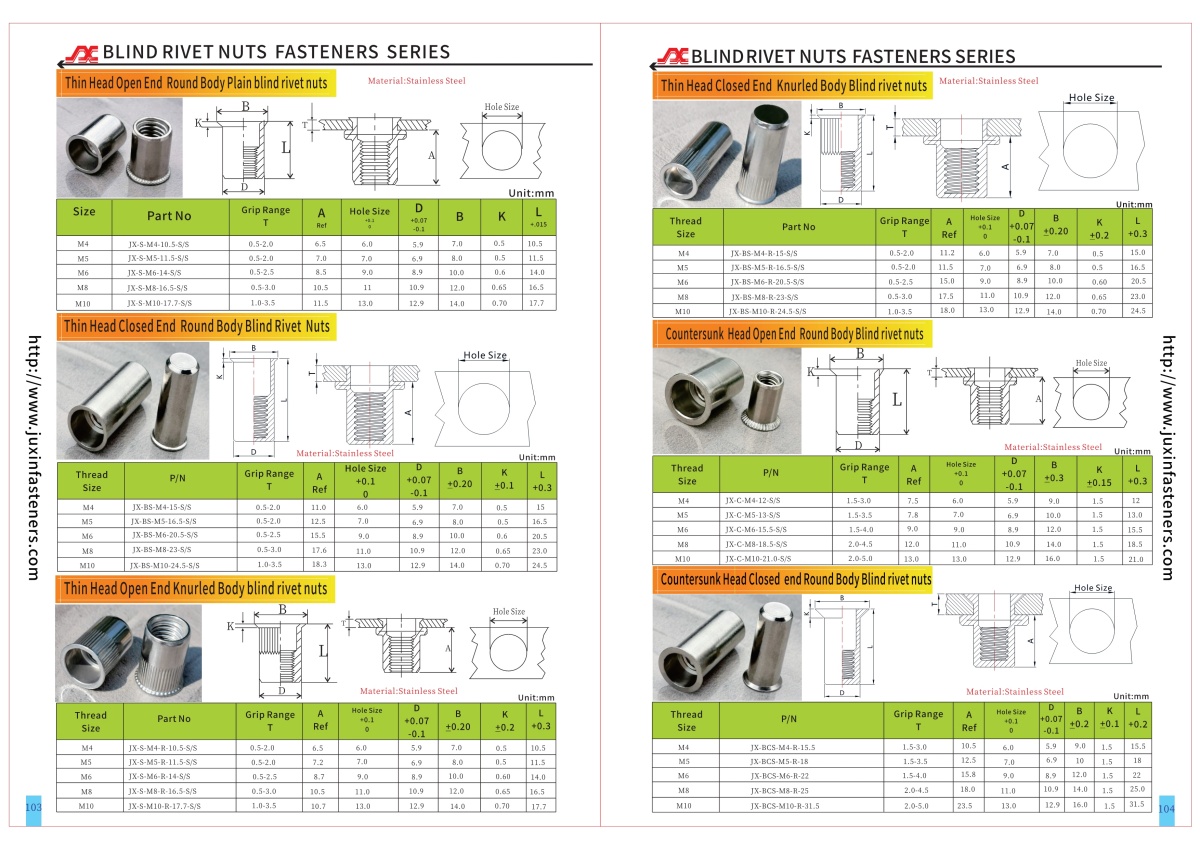
| Product-Family Grip Range | 0.5–3.5 mm |
| Installation Method | One-Sided Blind Installation |
| Mounting Hole | Round Hole per Approved Drawing |
| Material Grade | Confirm for Selected Variant |
| Dimensional Reference | Product Technical PDF, Pages 103–104, Subject to Drawing Confirmation |
| Customization | Drawing-Specific OEM Requirements |
The stated grip range applies to the product family and should not be interpreted as the permitted grip thickness for every individual thread size.
Final dimensions, tolerances and installation requirements must be confirmed using the approved product drawing.
Thin Head Geometry and Installed Surface Height
The low-profile flange is designed to minimize the height of the fastening point above the mounting surface.
This can be beneficial where covers, brackets and adjacent components require limited clearance.
The installed flange height depends on the actual head thickness, seating condition, panel flatness and mounting-hole quality.
A thin-head rivet nut should not automatically be considered flush with the panel.
Where the application specifies a maximum allowable surface projection, the required dimension should be identified on the engineering drawing.
If the assembly requires a completely flush surface, a suitable countersunk rivet nut may be more appropriate.
Low-Profile Head Versus Conventional Flat Head
A conventional flat-head rivet nut generally provides a more substantial flange-bearing surface.
A thin-head configuration prioritizes reduced surface projection.
This creates an engineering trade-off between installation clearance and flange-bearing geometry.
For thin or relatively soft panels, the surrounding material must be capable of supporting the expected axial loading.
The low-profile flange should not be assumed to provide the same pull-through performance as a larger flange design without appropriate evaluation.
The correct head style depends on the parent material, mounting-hole dimensions, expected loading and available assembly clearance.
Closed-End Cavity and Bolt Bottoming Prevention
The closed-end cavity prevents the mating bolt from passing completely through the rivet nut.
This can be advantageous in compact housings where internal components are located close to the fastening point.
However, the usable internal thread depth is finite.
If the mating bolt is too long, it may contact the closed end before the assembled components are properly clamped.
In this situation, the tightening torque may increase without producing the intended joint preload.
The engineer should therefore evaluate the mating bolt length, attached component thickness, required thread engagement and usable cavity depth.
The usable internal thread depth must be confirmed from the approved drawing or suitable dimensional inspection.
Overall body length alone is not a reliable substitute for usable thread depth.
Closed-End Versus Open-End Selection
A closed-end rivet nut blocks direct passage through the internal threaded bore.
An open-end rivet nut permits bolt protrusion through the insert when sufficient blind-side clearance is available.
The closed-end configuration may be preferred where unrestricted bolt penetration is undesirable.
The open-end configuration may be preferred where greater flexibility in bolt length or engagement is required.
Neither configuration should be selected solely on the basis of nominal thread size.
The final choice should consider the equipment layout, available clearance, bolt engagement and environmental requirements.
Closed-End Construction and Environmental Protection
The enclosed threaded cavity blocks a direct through-bore passage.
This can reduce one potential pathway for moisture, dust or other contaminants entering through a fastening point.
However, the interface between the rivet nut flange and the surrounding panel remains a separate possible leakage path.
A standard closed-end rivet nut does not automatically provide a watertight or airtight connection.
Where environmental sealing is required, the complete fastening interface should be evaluated, including the mounting hole, flange seating, panel surface and any additional sealing material.
For applications requiring a validated sealing function, a dedicated sealed closed-end rivet nut may be more appropriate.
Plain Round Body and Rotational Retention
The smooth cylindrical body is intended for installation in a round mounting hole of the specified diameter.
During setting, the deformable body section collapses behind the panel and forms a retaining bulge.
The flange and blind-side deformation secure the insert mechanically.
Because the body is smooth, rotational retention depends on the installed deformation, contact conditions, parent-material properties and mounting-hole geometry.
An oversized hole may reduce resistance to rotation.
An incorrectly set insert may rotate when the mating bolt is tightened or removed.
For demanding anti-rotation requirements, engineers should evaluate whether a knurled or full-hex alternative provides a more suitable solution.
Where torque-to-turn performance is critical, representative installed-joint testing should be specified.
Grip Range and Parent-Material Thickness
The stated product-family grip range is 0.5–3.5 mm.
Grip range describes the thickness of the parent material or captured material stack that a particular rivet nut configuration is designed to retain.
The selected body length must correspond to the actual workpiece thickness.
If the material is outside the permitted grip range, the retaining bulge may form incorrectly.
This can affect axial retention, rotational resistance and installation consistency.
For assemblies containing multiple sheets, the actual captured stack thickness should be established before selecting the rivet nut.
The correct grip range must be verified for each individual product variant.
Mounting-Hole Dimensions and Preparation
Mounting-hole geometry is essential to the performance of plain-body rivet nuts.
The hole must allow correct insertion while supporting the required mechanical retention.
An oversized hole may reduce rotational resistance or permit unwanted movement.
An undersized hole may prevent correct seating or damage the fastener and parent material.
Hole roundness, burr condition, panel flatness and surface coatings can also influence the installation result.
For punched holes, the engineer should consider edge quality and burr direction.
For drilled holes, dimensional accuracy and appropriate deburring are important.
The required installation-hole diameter and tolerance must be obtained from the approved product drawing.
Installation in Coated or Painted Sheet Metal
Low-profile rivet nuts may be used in selected pre-coated or painted sheet-metal assemblies when the installation process is compatible with the coating system.
However, installation produces local contact pressure and deformation around the mounting hole.
The process should not be assumed to leave every coating undamaged.
Where coating integrity is important, the engineer should evaluate flange seating, possible abrasion, coating thickness and local deformation.
Representative installation trials may be required to establish whether the coating system remains suitable after setting.
One-Sided Installation and Tool Compatibility
Stainless steel thin-head closed-end rivet nuts can be installed using compatible manual, pneumatic, hydro-pneumatic or automated setting equipment,
depending on the selected product and production requirements.
The setting tool engages the internal thread and applies axial force to compress the deformable section behind the panel.
The resulting retaining bulge secures the rivet nut without requiring rear-side access.
The setting mandrel must match the internal thread, and the nosepiece must support the low-profile flange correctly.
For closed-end designs, the mandrel engagement and installation process must also be compatible with the available internal thread depth.
Insufficient setting can result in inadequate retention.
Excessive setting can damage the internal thread, distort the flange or deform the surrounding material.
For OEM production, setting parameters should be established through representative installation trials.
Blind-Side Clearance and Installed Geometry
Although the product is installed from one accessible side, sufficient space is still required behind the panel.
The rivet nut body extends beyond the workpiece, and installation creates a retaining bulge on the blind side.
The designer must verify clearance for the uninstalled body and the final installed geometry.
The closed-end cavity prevents the mating bolt from passing through the insert, but it does not eliminate the space occupied by the rivet nut body.
For compact equipment, the body length and blind-side deformation may be significant design constraints.
Torque-to-Turn Resistance and Joint Reliability
Torque-to-turn resistance describes the ability of the installed rivet nut to resist rotation within the parent material.
This is different from the strength of the internal thread and from the tightening torque applied to the mating bolt.
Plain-body rivet nuts may provide adequate rotational retention in correctly designed and installed assemblies.
However, their performance depends on mounting-hole dimensions, panel material, grip thickness and setting conditions.
Where repeated servicing or higher tightening torque is expected, rotational retention should be evaluated using representative installed samples.
The acceptance criteria should reflect the actual assembly and intended service conditions.
Pull-Out, Pull-Through and Thread Integrity
The axial retention of a blind rivet nut depends on the mechanical interaction between the flange, retaining bulge and parent material.
Under excessive axial loading, the insert may pull out of the panel or the surrounding material may deform.
The flange-bearing region may also become a limiting factor.
For thin-head configurations, the relationship between flange geometry and parent-material strength deserves particular attention.
Thread stripping is a separate failure mechanism associated with the internal thread, mating bolt and engagement conditions.
For closed-end designs, premature bolt bottoming is an additional assembly risk.
These failure mechanisms should be evaluated separately.
Stainless Steel Material Selection
The supplied technical description references A2 stainless steel.
A2 stainless steel is commonly associated with 304-type austenitic stainless steel.
A4 stainless steel, commonly associated with 316-type compositions, may be evaluated where the application requires improved resistance to certain chloride-containing environments.
The actual grade and availability for this product must be confirmed through the approved material specification.
Corrosion performance depends on the complete joint, including material combinations, moisture exposure, surface condition and service temperature.
Where stainless steel is installed in aluminum or coated carbon steel, galvanic corrosion should be considered if an electrolyte is present.
International Engineering References
Metric thread designations may be established using ISO 261, with applicable thread tolerances defined under ISO 965.
Where Unified inch-thread configurations are requested as custom options, ASME B1.1 may provide a relevant reference.
The standard size range supplied for this page is metric M3–M10. UNC and UNF availability should not be assumed without separate confirmation.
Relevant ASTM or EN material specifications may be selected according to the actual stainless steel grade and customer requirements.
Where environmental ingress protection is required for the completed enclosure, IEC 60529 may provide a relevant testing framework.
These references support engineering specification development but do not independently establish product certification.
Electrical Enclosure Engineering
Electrical cabinets and control panels may require retained internal threads in thin sheet-metal walls.
The low-profile head can reduce interference with covers and mounting brackets.
The closed-end cavity limits mating bolt penetration and blocks a direct passage through the internal threaded bore.
Where environmental sealing is required, the flange interface must be evaluated separately.
Electronics and Instrumentation Engineering
Compact electronics housings and industrial instruments may have limited internal clearance.
A closed-end threaded insert can help restrict bolt penetration into the equipment cavity.
The thin-head design may reduce surface interference with adjacent components.
Engineers should verify usable thread depth, installed body length and blind-side clearance.
Automotive and Transportation Engineering
Selected automotive brackets, equipment housings and service panels may require threaded fastening points in thin sheet metal.
Low-profile closed-end rivet nuts can be evaluated where one-sided installation and controlled bolt penetration are important.
For vibration-sensitive applications, the engineer should assess tightening torque, rotational retention, joint preload and installation repeatability.
Safety-critical applications require project-specific validation.
Industrial Machinery and Equipment Covers
Machinery housings, removable guards and equipment panels may require permanent female threads that remain attached during maintenance.
A low-profile closed-end rivet nut can be useful where a conventional flange would interfere with nearby components.
The closed cavity may also help control mating bolt penetration into the equipment interior.
HVAC and General Fabrication
HVAC housings, ventilation equipment and fabricated sheet-metal assemblies may benefit from one-sided threaded installation.
The low-profile head can reduce surface projection, while the closed-end configuration limits bolt penetration.
Product selection should consider panel thickness, installation-hole geometry, corrosion exposure and required mechanical performance.
OEM Manufacturing and Custom Engineering
JUXIN FASTENERS manufactures industrial fasteners and drawing-specific components using production processes selected according to material, geometry and functional requirements.
Our manufacturing capabilities include cold heading, cold forming, secondary CNC machining and turning,
metal stamping, plastic injection molding and combined manufacturing processes where appropriate.
For suitable custom metal components, cold forming may be followed by secondary machining to achieve specified dimensions, tolerances and functional features.
JUXIN can review OEM requirements involving thin-head flange dimensions, smooth body geometry, closed-end cavity depth, grip ranges, stainless steel grades and custom thread configurations.
Manufacturing feasibility is determined according to the approved drawing, material specification, tooling requirements and order quantity.
Quality Inspection and Production Approval
For OEM production, inspection requirements should reflect the approved drawing and intended application.
Relevant dimensional characteristics may include thread size, flange thickness, flange diameter, body diameter, overall length and usable internal thread depth.
Installed-joint evaluation may include flange seating, retaining bulge formation, thread integrity, rotational retention and axial retention where required.
For closed-end designs, mating bolt compatibility should also be verified.
The inspection plan should distinguish product dimensional conformity from installed-joint mechanical performance.
Technical RFQ and Procurement Requirements
For an accurate quotation, please provide the required thread size, stainless steel grade, parent-material thickness, mounting-hole dimensions and product drawing.
For low-profile applications, the maximum permitted flange projection is particularly important.
For closed-end applications, the usable internal thread depth and mating bolt length must also be considered.
Where mechanical performance is critical, the required torque-to-turn, pull-out or other acceptance criteria should be specified.
Estimated annual demand, order quantity, sample requirements, inspection expectations and packaging instructions will support the technical and commercial review.
Why Choose a Thin Head Closed-End Rivet Nut?
Many industrial assemblies have limited clearance above the mounting surface.
A conventional flat-head rivet nut may project too far above the panel and interfere with a closely fitted cover, mounting bracket or adjacent component.
A thin-head rivet nut reduces this projection while providing a mechanically retained internal thread.
The closed-end construction introduces a second design benefit by limiting mating bolt penetration into the space behind the workpiece.
This can be useful in compact equipment housings where internal components are located close to the fastening point.
However, the closed-end cavity also limits usable thread depth. Engineers must therefore select the mating bolt carefully to avoid bottoming out before the joint develops its intended clamp load.
Low-Profile Flange for Reduced Surface Projection
The thin flange is the defining external feature of this product.
Compared with a conventional larger-profile flange, the low-profile head reduces the height of the fastening point above the accessible panel surface.
This can simplify the installation of close-fitting equipment covers and brackets.
The flange also provides a bearing surface during installation and contributes to mechanical retention after the blind-side bulge has formed.
A low-profile head should not automatically be considered completely flush with the panel.
The final projection depends on the actual flange thickness, panel condition and installation geometry.
Where a precisely flush surface is required, a countersunk configuration may be more appropriate.
Closed-End Design for Controlled Bolt Penetration
The enclosed threaded cavity prevents a mating bolt from passing completely through the rivet nut.
This distinguishes the product from an open-end threaded insert, which allows bolt protrusion through the body when sufficient blind-side clearance is available.
A closed-end rivet nut may be useful where unrestricted bolt penetration could interfere with internal equipment components.
It can also reduce a direct contamination pathway through the threaded bore.
However, the flange-to-panel interface remains a separate potential route for moisture or dust.
Where environmental sealing is required, the complete fastening point should be evaluated, including the mounting hole, flange seating and any gasket or sealing compound.
The closed-end configuration alone does not establish a watertight or airtight connection.
Plain Round Body for Round-Hole Installation
The smooth cylindrical body is intended for installation in a round mounting hole of the specified diameter.
During setting, the deformable portion of the rivet nut collapses behind the panel to form a retaining bulge.
The flange and blind-side deformation secure the insert mechanically.
Unlike a knurled or full-hex rivet nut, the plain round body does not provide external ribs or noncircular geometry for additional anti-rotation engagement.
Its rotational resistance therefore depends on the installation conditions, mounting-hole dimensions and parent-material properties.
For applications involving higher tightening torque or repeated maintenance, engineers should evaluate whether a knurled or full-hex alternative would provide more suitable rotational retention.
Stainless Steel Construction for Industrial Applications
Stainless steel is commonly selected for threaded inserts where corrosion resistance, durability and material compatibility are important.
A2 stainless steel is commonly associated with 304-type austenitic stainless steel.
For certain environments involving chloride exposure, A4 stainless steel may be evaluated as an alternative material, subject to product availability and engineering review.
The exact grade supplied for this product should be confirmed through the approved material specification.
For outdoor or industrial applications, corrosion performance depends on the complete assembly, including moisture exposure, temperature, surface condition and contact with dissimilar metals.
One-Sided Installation in Thin and Hollow Structures
Blind rivet nuts provide permanent female threads without requiring rear-side access during installation.
A compatible setting tool engages the internal thread and applies an axial force that compresses the deformable body section behind the panel.
The resulting retaining bulge secures the insert between the flange and the blind-side deformation.
This method can be useful for sheet-metal cabinets, tubular sections, fabricated equipment housings and hollow profiles.
The stated product-family grip range of 0.5–3.5 mm supports selection for suitable thin-material applications.
However, the correct grip range and installation-hole dimensions must be verified for each product size.
Engineering Applications
Electrical Enclosures and Control Cabinets
Low-profile closed-end rivet nuts may be evaluated for removable panels, mounting brackets and internal equipment supports.
The reduced flange projection can help accommodate close-fitting components.
The closed-end cavity limits bolt penetration and blocks a direct passage through the internal threaded bore.
Where the enclosure requires a specific ingress protection rating, the flange-to-panel interface and complete assembly must be evaluated separately.
Electronics and Industrial Instrumentation
Compact electronics housings and instrument enclosures often have limited internal clearance.
A closed-end threaded insert can help restrict mating bolt penetration into the equipment cavity.
The thin-head design may also reduce interference between the mounting panel and attached components.
Engineers should verify usable thread depth, bolt length, installed body geometry and blind-side clearance.
Automotive and Transportation Equipment
Selected automotive brackets, equipment housings and service panels may require one-sided threaded fastening in thin sheet metal.
Low-profile closed-end rivet nuts can be considered where surface clearance and controlled bolt penetration are important.
For vibration-sensitive applications, joint preload, rotational retention and installation consistency should be validated.
Industrial Machinery and Equipment Covers
Machinery housings, removable guards and service panels may require retained internal threads in fabricated structures.
A low-profile closed-end rivet nut can provide a threaded connection where a thicker flange would interfere with adjacent components.
The closed cavity may also be useful where internal components are located close to the fastening point.
HVAC and Climate-Control Equipment
HVAC housings, ventilation equipment and fabricated sheet-metal components may benefit from one-sided threaded installation.
The low-profile head can reduce surface projection, while the closed-end construction limits bolt penetration.
The correct product should be selected according to panel thickness, corrosion exposure and required mechanical performance.
Domestic Appliances and General Fabrication
Appliance housings, sheet-metal covers and fabricated equipment panels may require retained threads where direct tapping is unsuitable.
Thin-head closed-end rivet nuts can be evaluated where a compact fastening profile and limited bolt penetration are desirable.
OEM Manufacturing and Custom Engineering
JUXIN FASTENERS manufactures industrial fasteners and drawing-specific components for OEM applications.
Our manufacturing capabilities include cold heading, cold forming, secondary CNC machining and turning, metal stamping, plastic injection molding and combined manufacturing processes where appropriate.
For suitable custom metal components, cold forming may be followed by secondary machining to achieve specified dimensions, tolerances and functional features.
JUXIN can review OEM requirements involving thin-head flange dimensions, smooth body geometry, closed-end cavity depth, grip ranges, stainless steel grades and custom thread configurations.
Manufacturing feasibility is evaluated according to the approved drawing, material specification, tooling requirements and production quantity.
Engineering and Procurement Support
For design engineers, the critical selection factors include available head clearance, panel thickness, mounting-hole dimensions, usable internal thread depth, mating bolt length and blind-side clearance.
For purchasing managers, sourcing engineers and supplier development teams, important considerations include material specification, dimensional consistency,
inspection requirements, production volume and delivery planning.
JUXIN FASTENERS supports drawing-based OEM inquiries and customer-specific industrial fastening projects.
Request an OEM Quotation
For technical review and quotation, please provide the required thread size, stainless steel grade, panel thickness, mounting-hole dimensions, head-clearance requirements, mating bolt details and technical drawing.
For closed-end designs, the usable thread depth and required bolt engagement are particularly important.
Estimated annual demand, sample requirements and inspection criteria can also be reviewed.
JUXIN FASTENERS
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Product Packaging
Product Packaging — Stainless Steel Thin Head Closed-End Plain Body Blind Rivet Nuts
Industrial Packaging for Stainless Steel Low-Profile Closed-End Rivet Nuts
JUXIN FASTENERS provides industrial packaging arrangements for stainless steel thin head closed-end plain body blind rivet nuts supplied to OEM manufacturers,
industrial equipment producers, distributors and international purchasing programs.
Packaging is selected according to the product dimensions, thread size, material requirements, order quantity and customer-specific handling instructions.
The packaging arrangement should protect the functional features of the rivet nuts while supporting efficient transportation, storage, inventory management and production-line handling.
Protection of Low-Profile Flanges and Closed-End Bodies
The thin flange is an important dimensional feature of this product.
Packaging and handling should minimize unnecessary impact or deformation that could affect flange flatness and installed head projection.
The internal threads should remain protected against contamination or mechanical damage that could interfere with setting-tool engagement or mating bolt installation.
The closed-end body should also be protected against deformation that could affect installation geometry or usable internal thread depth.
Where surface cleanliness is important, suitable handling and protective packaging arrangements should be selected.
Inner Packaging and Outer Cartons
Suitable inner protective packaging and outer cartons can be reviewed according to the selected product and confirmed purchase order.
Inner packaging materials, quantities per package, carton dimensions and carton weights are established according to the actual product dimensions and order requirements.
Different thread sizes and body lengths may require different packing quantities or protective arrangements.
The final packaging configuration is confirmed during order preparation.
Stainless Steel Handling and Storage
Stainless steel rivet nuts should be stored and handled under conditions compatible with the approved material specification.
Where surface cleanliness or corrosion resistance is important, handling procedures should reduce unnecessary contamination from carbon steel particles, moisture or unsuitable storage environments.
Special protective packaging can be reviewed where the customer requires additional surface protection or cleanliness control.
Palletized Packaging for International Shipment
For larger industrial orders, palletized packaging can be arranged according to shipment quantity, carton dimensions and transportation requirements.
Pallet loading, protective arrangements and shipment weights are confirmed for the actual order.
Packaging should support safe handling and efficient receiving operations at the customer's facility.
OEM Packaging Identification
For OEM manufacturing programs, packaging identification can be coordinated with customer requirements for product descriptions, part numbers,
thread sizes, material specifications, batch identification and shipment marking.
Customers may specify preferred packing quantities and labeling formats to support receiving inspection, warehouse management and production-line replenishment.
Where traceability or supporting documentation is required, the relevant identification and record requirements should be agreed during order confirmation.
Custom Packaging for OEM and Distribution Programs
JUXIN FASTENERS can review customer-specific packaging arrangements for industrial purchasing and distribution programs.
Requirements may include preferred packing quantities, product separation, carton identification, palletization and warehouse handling.
The final packaging method is established according to the confirmed product specification and purchase order.
Request Packaging Information or an OEM Quotation
For accurate packaging coordination, please provide the required thread size, product drawing or part number, stainless steel grade,
order quantity, preferred packaging arrangement and shipping destination.
JUXIN FASTENERS
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Stainless Steel Low-Profile Closed-End Rivet Nuts | OEM Manufacturing | Industrial Packaging Solutions
Product Pictures
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY