Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

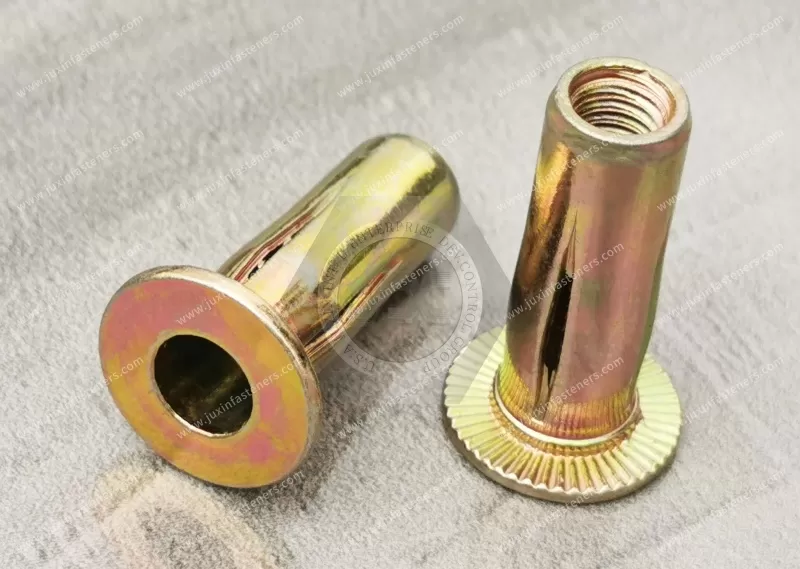
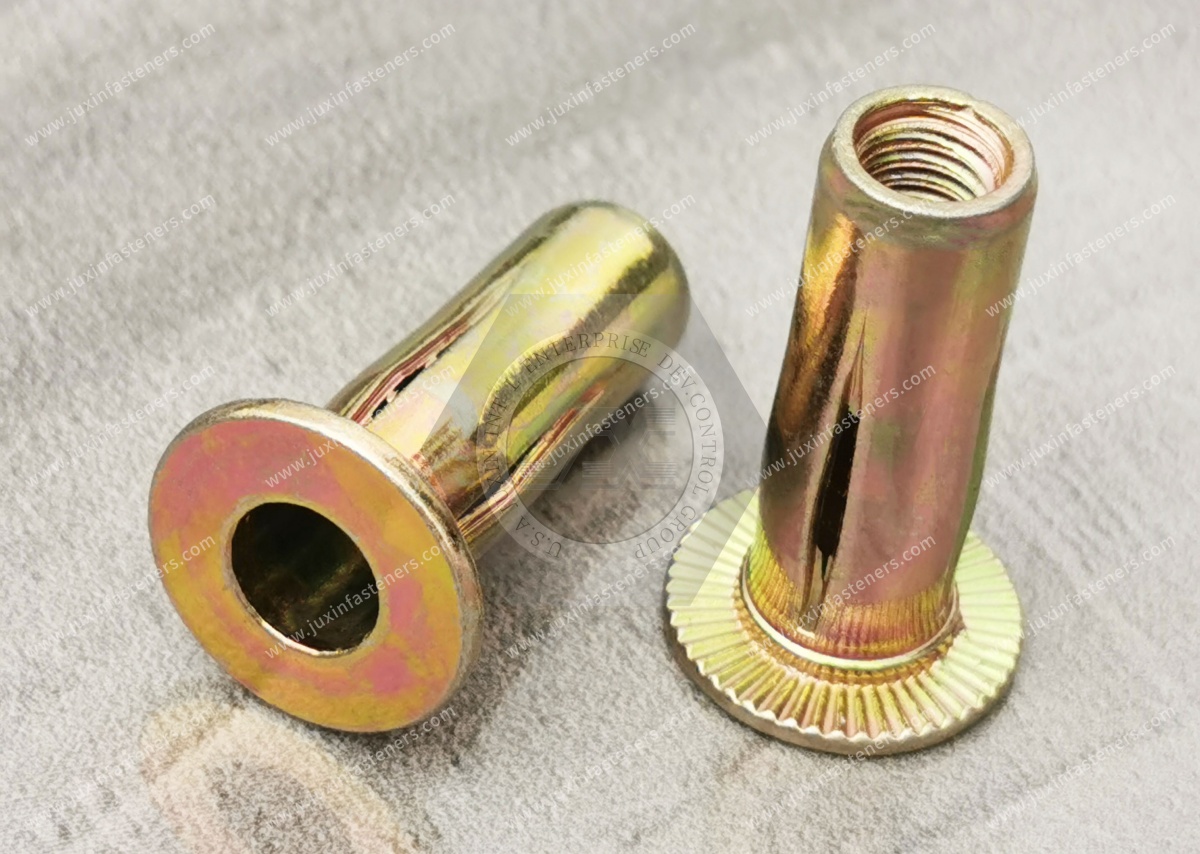
JUXIN FASTENERS supplies steel flat head open-end slotted shank blind rivet nuts for OEM manufacturers requiring reusable internal threads and one-sided installation in sheet-metal panels and other suitable fabricated materials.
The slotted shank is designed to deform behind the parent panel during installation. Depending on the insert geometry and installation conditions, the slotted sections can expand outward to create a broader backside bearing area than some conventional rivet nut configurations. This design may be useful where axial retention and load distribution require particular attention.
The flat-head flange supports the accessible side of the panel, while the open-end barrel allows mating screw extension where sufficient backside clearance is available.
Product Features
Metric threads: M5, M6, M8, M10
Unified inch threads: #10-32 UNF, 1/4-20 UNC, 5/16-18 UNC, 3/8-16 UNC
Material: Steel
Product-family grip range: 0.5–7.1 mm (approx. 0.020–0.280 in)
Head: Flat head / Flanged head
Body: Slotted shank
End: Open end
Installation: One-sided blind installation
Surface treatment options: Color Zinc or RoHS Blue Zinc, subject to approved specification
Steel grade: Subject to confirmation
Mounting-hole dimensions: According to approved drawing
Mechanical retention performance: Subject to application-specific testing
Potential applications include industrial equipment housings, fabricated panels, commercial vehicle components, agricultural machinery, transportation equipment, HVAC assemblies, and selected soft-material or composite structures where the slotted-body installation behavior has been validated.
For OEM drawings, technical review, and quotations, contact info@juxinfasteners.com.
Website: www.juxinfasteners.com
Product Specification
Steel Flat Head Open-End Slotted Shank Blind Rivet Nuts – OEM High-Retention Panel Fastening Solutions
JUXIN FASTENERS supplies steel flat head open-end slotted shank blind rivet nuts for OEM engineers, equipment manufacturers, purchasing managers, and supplier development teams requiring reusable threaded fastening points in thin-walled panels and other suitable fabricated structures.
Unlike conventional round-body blind rivet nuts, slotted shank rivet nuts incorporate longitudinal slots in the body. During installation, the slotted sections are designed to deform outward behind the parent panel.
Depending on the specific design, this deformation can create an enlarged backside bearing footprint and distribute axial loading over a broader area.
The actual mechanical benefit depends on the insert dimensions, parent material, panel thickness, hole geometry, and installation conditions.
The product family includes both ISO metric and Unified inch-thread options, supporting OEM programs using different fastening systems.
PRODUCT SPECIFICATIONS
Product type: Steel Flat Head Open-End Slotted Shank Blind Rivet Nut
Material: Steel
Metric thread sizes: M5, M6, M8, M10
Unified inch thread sizes: #10-32, 1/4-20, 5/16-18, 3/8-16
Thread designation:
#10-32 UNF
1/4-20 UNC
5/16-18 UNC
3/8-16 UNC
Head configuration: Flat head / Flanged head
Body configuration: Slotted shank
End configuration: Open end
Product-family grip range: 0.5–7.1 mm
Approximate inch reference: 0.020–0.280 in
Installation method: One-sided blind installation
Surface treatment options: Color Zinc or RoHS Blue Zinc
Steel grade: Subject to confirmation
Thread tolerance class: According to approved drawing
Mounting-hole diameter: According to approved drawing
Flange diameter and thickness: According to approved drawing
Body diameter and length: According to approved drawing
Slot geometry: According to approved drawing
Installed backside expansion: Subject to installation validation
Coating thickness and corrosion performance: Subject to approved specification
Mechanical retention performance: Subject to product-specific testing
The stated grip range represents the product family. The approved grip range for each thread size and body configuration must be confirmed against the selected drawing.
ENGINEERING DESIGN AND SELECTION
What Is a Slotted Shank Blind Rivet Nut?
A slotted shank blind rivet nut is a threaded insert with longitudinal slots in its body.
It is installed from one accessible side of a compatible workpiece.
During setting, axial force causes designated body sections to deform behind the parent panel.
The resulting backside geometry helps retain the insert within the mounting hole.
Some slotted-body designs are also described as bulbing rivet nuts because of their expanded backside installation geometry.
However, not every slotted rivet nut has the same deformation pattern or mechanical performance.
The exact product drawing and installation instructions determine the intended behavior.
How Does the Slotted Shank Work?
A conventional blind rivet nut generally forms a retaining bulge through deformation of its unthreaded body section.
A slotted shank design incorporates longitudinal openings that influence how the body deforms.
During installation, the slotted sections may move outward and form an enlarged backside bearing structure.
The final geometry depends on:
Slot length
Slot width
Number of slots
Body diameter
Body wall thickness
Steel grade
Grip thickness
Setting force or stroke
The installation process must produce the intended backside deformation without damaging the internal thread or parent panel.
Backside Bearing Area and Load Distribution
One potential advantage of slotted shank rivet nuts is the ability to create a broader backside bearing footprint.
This may help distribute axial loads over a larger area of suitable parent material.
The benefit can be relevant where a conventional retaining bulge would create high localized loading.
However, a larger visible bearing footprint does not automatically guarantee higher pull-out strength.
The actual result depends on the complete joint geometry and material properties.
Representative testing is required to establish mechanical performance.
Pull-Out Resistance: What Engineers Must Verify
Pull-out resistance concerns the axial force required to remove the installed insert under a defined test arrangement.
The failure mechanism may involve:
Parent-panel deformation
Local material tearing
Insert displacement
Slotted-section deformation
Flange pull-through
Insert fracture
The governing failure mode depends on the application.
For OEM qualification, engineers should define:
Parent material
Panel thickness
Mounting-hole dimensions
Installation parameters
Loading direction
Test fixture
Acceptance criteria
No universal pull-out force value is claimed for this product family.
Why Slotted Shank Does Not Automatically Mean Maximum Pull-Out Strength
A slotted shank may provide an advantageous backside bearing geometry.
However, pull-out performance is not determined by bearing area alone.
Other factors include:
Parent-material tensile and shear strength
Hole edge quality
Panel thickness
Insert material
Installation deformation
Flange geometry
Applied load distribution
A slotted-body rivet nut may outperform a conventional configuration in one assembly but not another.
Therefore, terms such as "ultimate pull-out strength" should be supported by specific comparative test results rather than used as an unconditional product claim.
Slotted Shank vs. Conventional Round Body Rivet Nuts
Conventional round-body rivet nuts generally use a continuous cylindrical shank.
Slotted shank rivet nuts incorporate longitudinal openings that modify the deformation behavior.
Potential differences include:
Backside bearing footprint
Installation stroke
Body deformation
Grip range
Axial retention
Rotational retention
Hole requirements
Tool compatibility
The appropriate configuration depends on the intended joint.
Slotted Shank vs. Knurled Body Rivet Nuts
Knurled-body rivet nuts incorporate external surface features intended to engage the surrounding parent material.
Slotted-body rivet nuts use slots to influence the backside deformation pattern.
These features address different aspects of joint performance.
Knurling may contribute to rotational retention.
Slotted-body expansion may influence axial retention and load distribution.
Neither feature alone establishes the overall performance of the installed joint.
Slotted Shank vs. Hex Body Rivet Nuts
Hex-body rivet nuts use geometric engagement with a matching hexagonal hole to resist rotation.
Slotted-body rivet nuts are primarily distinguished by their deformation geometry.
A slotted-body insert should not automatically be assumed to provide the same rotational resistance as a full hex-body design.
Where both axial retention and rotational retention are critical, engineers should evaluate the complete fastening system.
Suitability for Thin Sheet Metal
Thin sheet metal may provide insufficient thickness for direct tapping.
A blind rivet nut can introduce a reusable internal thread without requiring a thick parent section.
Slotted-body designs may be considered where backside bearing distribution is important.
However, the parent panel must have sufficient strength and geometry to support the installed insert.
The nominal grip range alone does not establish suitability.
Suitability for Soft Materials
Certain slotted-body rivet nut designs may be useful in relatively soft parent materials.
The expanded backside geometry can potentially reduce localized bearing pressure.
However, soft materials may also deform, creep, or tear under load.
Relevant considerations include:
Material strength
Panel thickness
Hole quality
Local bearing stress
Long-term loading
Temperature
Environmental exposure
The selected insert must be validated in the actual parent material.
Suitability for Plastics and Composites
Slotted-body rivet nuts may be considered for selected plastic or composite assemblies where the insert geometry and installation process are appropriate.
However, these materials behave differently from ductile steel or aluminum sheet.
For plastics, engineers should consider:
Material stiffness
Creep
Temperature sensitivity
Local deformation
Hole quality
Installation load
For fiber-reinforced composites, additional considerations may include:
Delamination
Fiber damage
Local crushing
Edge distance
Through-thickness strength
A slotted-body rivet nut should not be approved for plastic or composite use without application-specific validation.
Grip Range: 0.5–7.1 mm
This product family is specified with a grip range of 0.5–7.1 mm.
The approved grip range for each individual thread size and body configuration must be confirmed.
Grip range refers to the parent-material thickness accommodated by the selected insert.
Installation outside the approved range may affect the intended backside expansion and mechanical retention.
Where the application approaches a grip limit, representative installation trials may be appropriate.
Mounting-Hole Diameter and Tolerance
The mounting hole must be compatible with the selected rivet nut.
An oversized hole may reduce engagement or allow unwanted movement.
An undersized hole may prevent insertion or damage the body.
The approved drawing should define:
Hole diameter
Hole tolerance
Hole roundness
Edge condition
Burr limits
Panel thickness
Hole position
The nominal internal thread size does not establish the required mounting-hole diameter.
Hole Edge Quality and Parent-Material Damage
Poor hole preparation can affect installation consistency.
Burrs, cracks, excessive clearance, or damaged material may influence the final joint.
For soft or composite materials, hole preparation can be particularly important.
Production controls should address the material-specific risks associated with drilling, punching, machining, or other hole-making processes.
Minimum Edge Distance and Hole Spacing
The expanded backside geometry requires adequate surrounding material.
If the mounting hole is too close to a panel edge or another opening, the parent material may deform or tear under load.
The required edge distance depends on:
Insert geometry
Installed backside footprint
Parent material
Panel thickness
Applied loading
Nearby holes and cutouts
No universal minimum edge distance is assumed.
Backside Clearance and Expanded Footprint
Slotted-body rivet nuts may require additional backside space to accommodate the installed expansion geometry.
Engineers should verify:
Available axial clearance
Available radial clearance
Nearby components
Adjacent fasteners
Internal ribs or bends
Mating screw projection
A product may fit into the mounting hole before installation but interfere with surrounding components after setting.
The installed geometry must be reviewed.
Flat Head Flange and Front-Side Bearing
The flat-head flange provides a bearing surface against the accessible side of the parent panel.
It supports the installed insert around the mounting hole.
The flange dimensions influence:
Bearing contact
Head projection
Local panel loading
Axial retention
Assembly stack height
Where a cover or bracket must fit closely against the panel, flange thickness should be included in the assembly stack-up.
Open-End Construction and Screw Projection
The open-end barrel allows the mating screw to extend through the insert where sufficient backside clearance is available.
This provides flexibility in screw-length selection.
However, the screw tip must not interfere with nearby components.
Engineers should verify:
Mating screw length
Joint stack thickness
Required thread engagement
Available backside clearance
Permissible screw projection
Open-end construction does not inherently provide environmental sealing.
Metric and Unified Inch Thread Options
This product family includes both metric and Unified inch-thread sizes.
Metric options:
M5
M6
M8
M10
Unified inch-thread options:
#10-32 UNF
1/4-20 UNC
5/16-18 UNC
3/8-16 UNC
Metric threads should be specified using the applicable ISO metric thread requirements.
Unified inch threads should be specified using the applicable ASME B1.1 requirements.
Metric and UNC/UNF threads are not directly interchangeable.
A similar nominal diameter does not establish thread compatibility.
Why American OEMs Specify UNC and UNF Threads
US OEM programs frequently use Unified inch-thread systems.
For this product family, the available inch-thread options support applications requiring:
#10-32 UNF
1/4-20 UNC
5/16-18 UNC
3/8-16 UNC
Procurement teams should specify the complete thread designation.
The nominal diameter alone is insufficient.
The internal thread must match the intended mating screw.
Thread Strength and Mating Screw Selection
The allowable tightening torque depends on the complete joint.
Relevant factors include:
Steel grade
Thread size and pitch
Mating screw material
Thread engagement
Friction conditions
Insert retention
Parent-material strength
A torque specification developed for a conventional steel nut should not automatically be applied to a blind rivet nut.
The complete assembly should be evaluated.
Spin-Out Resistance
Spin-out resistance describes the installed insert's resistance to rotation within the mounting hole.
A slotted-body rivet nut may provide suitable rotational retention when properly installed.
However, its actual performance depends on the body geometry, hole fit, parent material, and installation conditions.
Where defined spin-out resistance is required, the selected insert should be tested.
Insert Spin-Out vs. Screw Loosening
Insert spin-out and screw loosening are separate engineering concerns.
Spin-out occurs when the rivet nut rotates within the mounting hole.
Screw loosening occurs when the mating screw loses its intended clamping condition or rotates relative to the internal thread.
The slotted-body design does not automatically prevent screw loosening under vibration.
Where vibration resistance is required, the complete bolted joint should be evaluated.
Installation Tooling and Setting Parameters
Blind rivet nuts are installed using compatible setting tools that deform the body behind the parent panel.
Slotted-body designs may require specific setting parameters to produce the intended expansion.
Production validation should include:
Correct installation mandrel
Tool capacity
Mounting-hole dimensions
Insert orientation
Flange seating
Setting stroke or force
Slotted-section expansion
Internal thread condition
Axial retention
Rotational retention
The installation parameters must be established for the actual product.
Under-Setting and Over-Setting
Under-setting may produce insufficient backside expansion and reduced retention.
Over-setting may damage the slotted sections, internal thread, or parent material.
The correct setting parameters depend on:
Insert geometry
Steel grade
Panel thickness
Parent-material strength
Installation tooling
Production settings should be validated rather than estimated from thread size alone.
Steel Material and Mechanical Performance
Steel provides a range of mechanical properties depending on the selected grade and condition.
The actual performance of the rivet nut depends on:
Steel grade
Material hardness
Body geometry
Thread geometry
Installation deformation
Parent-material strength
No specific steel grade or mechanical strength class is assumed without supporting documentation.
Color Zinc Surface Treatment
Color Zinc is a specified surface-treatment option for this product family.
However, the term alone does not fully define the coating system.
The approved specification should identify:
Zinc coating type
Coating thickness
Conversion coating or passivation
Sealant or topcoat, if required
Appearance requirements
Corrosion-test method
Acceptance criteria
Restricted-substance requirements
A particular color does not establish a corrosion-resistance rating.
RoHS Blue Zinc Surface Treatment
RoHS Blue Zinc is another specified finish option.
For OEM procurement, the term should be translated into a defined coating specification.
The OEM should confirm:
Zinc coating type
Coating thickness
Passivation chemistry
Restricted-substance requirements
Applicable documentation
Corrosion-test requirements
Appearance requirements
A blue or silver-colored zinc finish does not automatically establish RoHS compliance.
Compliance should be supported by appropriate documentation for the applicable requirements.
Coating Integrity After Slotted-Body Expansion
The installation process involves plastic deformation of the slotted sections.
This deformation may affect the coating in areas of high local strain.
For corrosion-sensitive applications, engineers should consider:
Coating ductility
Deformation geometry
Installation process
Exposed steel after setting
Environmental exposure
Where necessary, corrosion testing should use installed components rather than only uninstalled fasteners.
Hydrogen Embrittlement Risk
Electroplating processes can introduce hydrogen into susceptible steel fasteners.
The risk depends on steel strength, hardness, tensile stress, and processing conditions.
For higher-strength or hardened steel components, the coating process should be reviewed against applicable requirements.
ISO 4042 addresses electroplated fastener coating systems and hydrogen embrittlement considerations.
The actual steel grade and hardness must be confirmed before determining the necessary controls.
Galvanic Corrosion and Dissimilar Metals
Zinc-plated steel rivet nuts may be installed in panels made from steel, aluminum, or other materials.
Where dissimilar metals are electrically connected in the presence of an electrolyte, galvanic corrosion may occur.
Relevant factors include:
Parent-panel material
Insert coating system
Mating screw material
Moisture exposure
Relative exposed surface areas
Environmental conditions
Suitable corrosion-control measures should be evaluated where necessary.
Long-Term Loading and Parent-Material Creep
For soft materials and plastics, long-term loading can affect the installed joint.
Some materials may deform gradually under sustained stress.
This can reduce local bearing support or change the installed retention condition.
Engineers should evaluate:
Sustained load
Operating temperature
Parent-material creep behavior
Backside bearing pressure
Joint geometry
Expected service life
A short-term pull-out test alone may not establish long-term performance.
Repeated Maintenance and Thread Wear
Slotted-body rivet nuts provide reusable internal threads.
However, repeated screw installation and removal can affect thread condition and installed retention.
For serviceable equipment, engineers should evaluate:
Expected maintenance cycles
Mating screw material
Thread engagement
Tightening torque
Thread wear
Spin-out resistance
Parent-material condition
Where frequent servicing is required, the selected insert should be qualified for the expected service conditions.
INDUSTRIAL APPLICATIONS AND OEM FASTENING SOLUTIONS
Industrial Machinery and Automation
Potential applications include equipment housings, maintenance panels, fabricated brackets, and machine structures.
The slotted-body configuration may be considered where backside load distribution is important.
Automotive and Commercial Vehicle Components
Potential applications include selected fabricated panels, equipment housings, brackets, and interior structures.
Vibration, mechanical loading, corrosion, and retention requirements must be validated.
Agricultural Machinery
Potential applications include equipment covers, fabricated panels, serviceable brackets, and machinery housings.
The coating system should be selected according to the expected exposure environment.
Construction Equipment
Potential applications include selected equipment housings, guards, brackets, and access panels.
Mechanical loading and corrosion requirements should be reviewed before approval.
Electrical Equipment and Control Cabinets
Potential applications include fabricated electrical enclosures, mounting panels, control cabinets, and equipment housings.
The open-end configuration requires verification of screw projection and internal component clearance.
Electrical bonding, grounding, and environmental sealing requirements must be evaluated separately.
HVAC and Appliance Manufacturing
Potential applications include equipment cabinets, appliance housings, sheet-metal covers, and mounting structures.
Mounting-hole geometry, grip thickness, and installation consistency should be verified.
Transportation and Railway Equipment
Potential applications include selected non-safety-critical interior panels, equipment enclosures, and fabricated components.
Vibration exposure, fatigue, corrosion, and mechanical retention requirements should be reviewed before approval.
Plastic and Composite Equipment Panels
Potential applications include selected plastic housings, reinforced panels, and composite structures where the insert has been validated for the parent material.
Installation deformation, local bearing pressure, creep, and material damage must be evaluated.
General OEM Sheet-Metal Fabrication
Potential applications include hollow sections, fabricated cabinets, removable panels, and threaded mounting points.
The selected insert should be validated for the actual parent material and expected service loads.
ENGINEERING DECISION: WHEN IS A SLOTTED SHANK RIVET NUT THE WRONG CHOICE?
A slotted shank rivet nut may not be the best solution when:
Backside clearance is insufficient for the expanded sections
The parent material cannot support the required bearing loads
The installation equipment is incompatible
The application requires a different head geometry
The mounting surface requires a flush or recessed head
The required rotational retention has not been validated
The selected configuration does not meet the required axial retention
The material is susceptible to unacceptable creep or damage
The manufacturing process cannot control the installation parameters
In these cases, a conventional round-body, knurled-body, hex-body, square-body, or other suitable threaded insert may be worth evaluating.
The correct alternative depends on the complete joint design.
OEM ENGINEERING SELECTION CHECKLIST
Before approving a steel slotted shank blind rivet nut, confirm:
Required metric or Unified inch thread size
Steel grade and hardness
Parent material and panel thickness
Approved grip range for the selected size
Mounting-hole diameter and tolerance
Hole edge condition
Flange diameter and thickness
Body dimensions
Slot geometry
Installed backside expansion
Available backside clearance
Mating screw material and length
Required thread engagement
Installation tool compatibility
Setting stroke or force
Required pull-out and push-out resistance
Required spin-out resistance
Tightening torque requirements
Coating specification
Corrosion requirements
Restricted-substance compliance requirements
Hydrogen embrittlement risk, where applicable
Environmental exposure
Inspection and traceability requirements
ENGINEERING STANDARDS AND TECHNICAL VERIFICATION
Product selection should be based on the approved dimensional drawing and the requirements of the intended assembly.
Applicable ISO metric thread standards may include ISO 261 and ISO 965 where relevant.
Unified inch threads should be specified according to applicable ASME B1.1 requirements.
ISO 4042 addresses electroplated coating systems for fasteners, including zinc-based coatings and hydrogen embrittlement considerations.
Where applicable, the OEM should define coating requirements using the appropriate ISO, EN, ASTM, or other recognized technical specification.
Corrosion testing may be specified using an appropriate method such as ISO 9227 or ASTM B117, together with agreed exposure conditions and acceptance criteria.
A test method alone does not establish a required corrosion-performance rating.
Metric and UNC/UNF thread systems are not directly interchangeable.
No specific certification, mechanical performance value, coating performance, or standard conformity should be assumed without supporting documentation.
OEM PROCUREMENT AND SUPPLIER QUALIFICATION
For purchasing managers and supplier development teams, steel slotted shank rivet nuts require careful dimensional, material, and installation comparison before supplier substitution.
Two products described as M6 slotted-body rivet nuts may differ in:
Steel grade
Slot geometry
Body dimensions
Flange dimensions
Mounting-hole requirements
Grip range
Installation parameters
Backside expansion
Thread strength
Coating system
Mechanical retention performance
These differences may affect assembly compatibility and joint reliability.
Before approving an alternative supplier, procurement teams should compare complete dimensional drawings, material specifications, coating requirements, and representative installation test results.
For recurring OEM programs, inspection criteria, traceability, packaging requirements, annual demand, and delivery expectations should be established during sourcing.
TOTAL INSTALLED COST CONSIDERATIONS
For OEM procurement, the rivet nut purchase price is only one component of the installed cost.
The total installed cost may include:
Rivet nut purchase price
Mounting-hole preparation
Installation tooling
Installation cycle time
Inspection
Rework
Scrap risk
Coating requirements
Supplier qualification
Inventory management
Where improved backside load distribution is required, a slotted-body configuration may justify additional qualification or tooling requirements.
Where a conventional rivet nut meets the mechanical requirements, a simpler configuration may be more economical.
CUSTOM OEM STEEL SLOTTED SHANK RIVET NUT RFQ REQUIREMENTS
Please provide:
2D drawing or 3D CAD model
Required metric or Unified inch thread size
Steel grade and hardness requirements
Parent material and panel thickness
Mounting-hole diameter and tolerance
Flange diameter and thickness
Body and slot dimensions
Approved grip range
Available backside clearance
Mating screw material and length
Installation method and tooling requirements
Required axial and rotational retention
Tightening torque requirements
Color Zinc or RoHS Blue Zinc finish requirement
Coating thickness and corrosion requirements
Restricted-substance documentation requirements
Inspection and traceability requirements
Prototype or production quantity
Estimated annual demand
Delivery destination
JUXIN FASTENERS supports drawing-based technical reviews and OEM sourcing discussions for steel flat head open-end slotted shank blind rivet nuts and related custom threaded fastening components.
Final dimensions, steel grade availability, coating specifications, installation compatibility, mechanical performance, and inspection requirements should be confirmed before production approval.
RELATED FASTENING SOLUTIONS
Stainless Steel Rivet Nuts for Plastic and Composites – Slotted Body
An alternative material configuration for selected plastic and composite assemblies requiring application-specific validation.
Steel Flat Head Open-End Square Body Blind Rivet Nuts
An alternative where geometric anti-rotation engagement with a square mounting hole is required.
Aluminum Flat Head Open-End Knurled Round Body Blind Rivet Nuts
An alternative where lightweight construction and compatible round-hole installation are preferred.
Aluminum Flat Head Open-End Full Hex Body Blind Rivet Nuts
An alternative where reduced component weight and hexagonal anti-rotation engagement are important.
Stainless Steel Flat Head Open-End Partial Hex Body Blind Rivet Nuts
An alternative material and non-round body configuration for suitable assemblies.
REQUEST AN OEM QUOTATION
Looking for steel flat head open-end slotted shank blind rivet nuts in M5, M6, M8, M10, #10-32, 1/4-20, 5/16-18, or 3/8-16?
Send JUXIN FASTENERS your engineering drawings, steel material requirements, panel thickness, mounting-hole dimensions, installation specifications, coating requirements, and estimated purchasing quantities.
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
JUXIN FASTENERS – Industrial Blind Rivet Nuts and Custom OEM Fastening Solutions.
Product Packaging
Packaging and Delivery – Steel Flat Head Open-End Slotted Shank Blind Rivet Nuts
JUXIN FASTENERS reviews packaging arrangements according to product dimensions, order quantities, handling conditions, and OEM purchasing requirements.
Packaging Requirements
Material: Steel
Metric thread sizes: M5, M6, M8, M10
Unified inch thread sizes: #10-32 UNF, 1/4-20 UNC, 5/16-18 UNC, 3/8-16 UNC
Product-family grip range: 0.5–7.1 mm
Surface finish options: Color Zinc or RoHS Blue Zinc, subject to approved specification
Packaging quantity: Subject to order confirmation
Inner packaging: According to approved packing instructions
Outer packaging: According to shipment requirements
Product identification: Part number, thread designation, steel grade, and coating specification as required
Batch identification: According to agreed traceability requirements
Custom packaging: Subject to technical and commercial confirmation
Packaging Protection
Steel slotted shank rivet nuts should be protected from unnecessary mechanical damage, flange deformation, thread contamination, and coating damage during handling, storage, and transportation.
Particular attention should be given to preserving the slotted-body geometry, flange dimensions, and internal thread condition.
Where appearance or coating integrity is specified, appropriate protection should be agreed upon before shipment.
Metric and Unified inch-thread products should be clearly identified and segregated to reduce the risk of assembly mix-ups.
OEM Supply and Documentation
For recurring OEM programs, packaging quantities, labeling, inspection documentation, coating records, material records, and delivery arrangements should be agreed upon before shipment.
Final packaging specifications are confirmed according to the approved purchase order.
For OEM packaging requirements and quotations, contact info@juxinfasteners.com.
Website: www.juxinfasteners.com
Product Pictures
Tags
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY