Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809
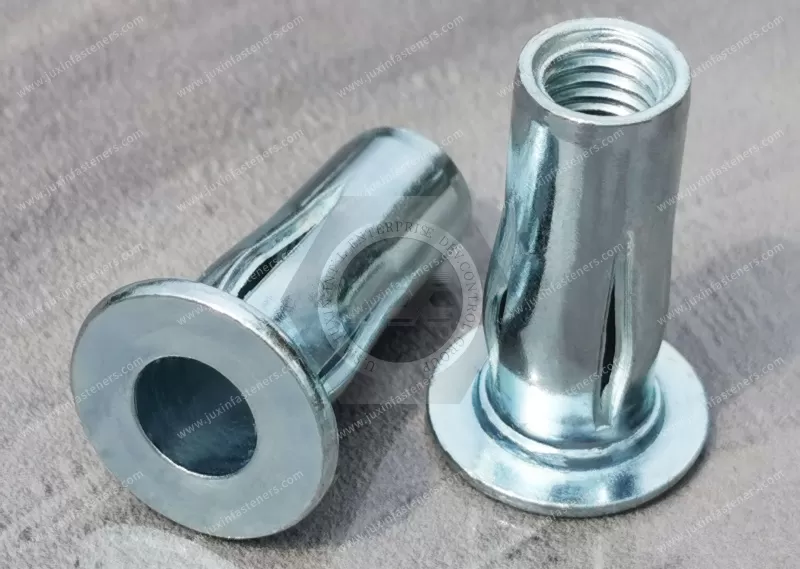
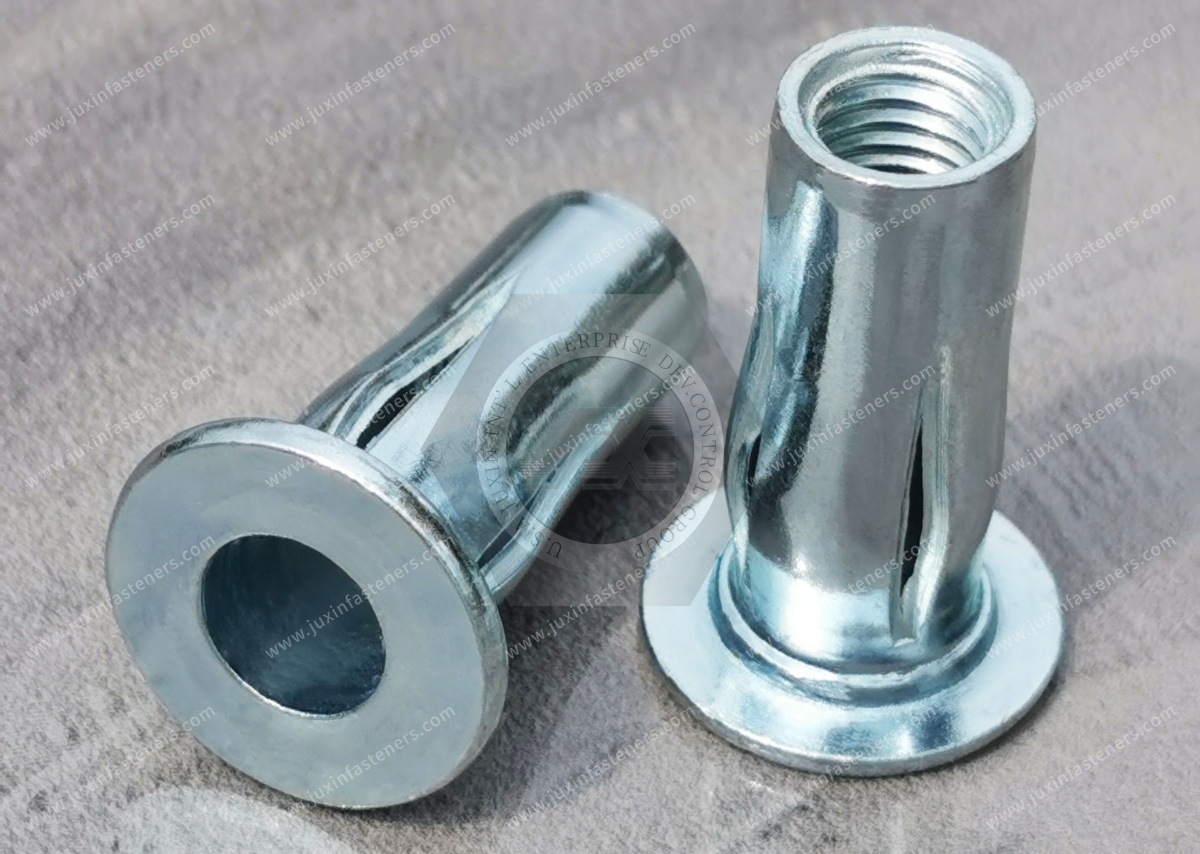
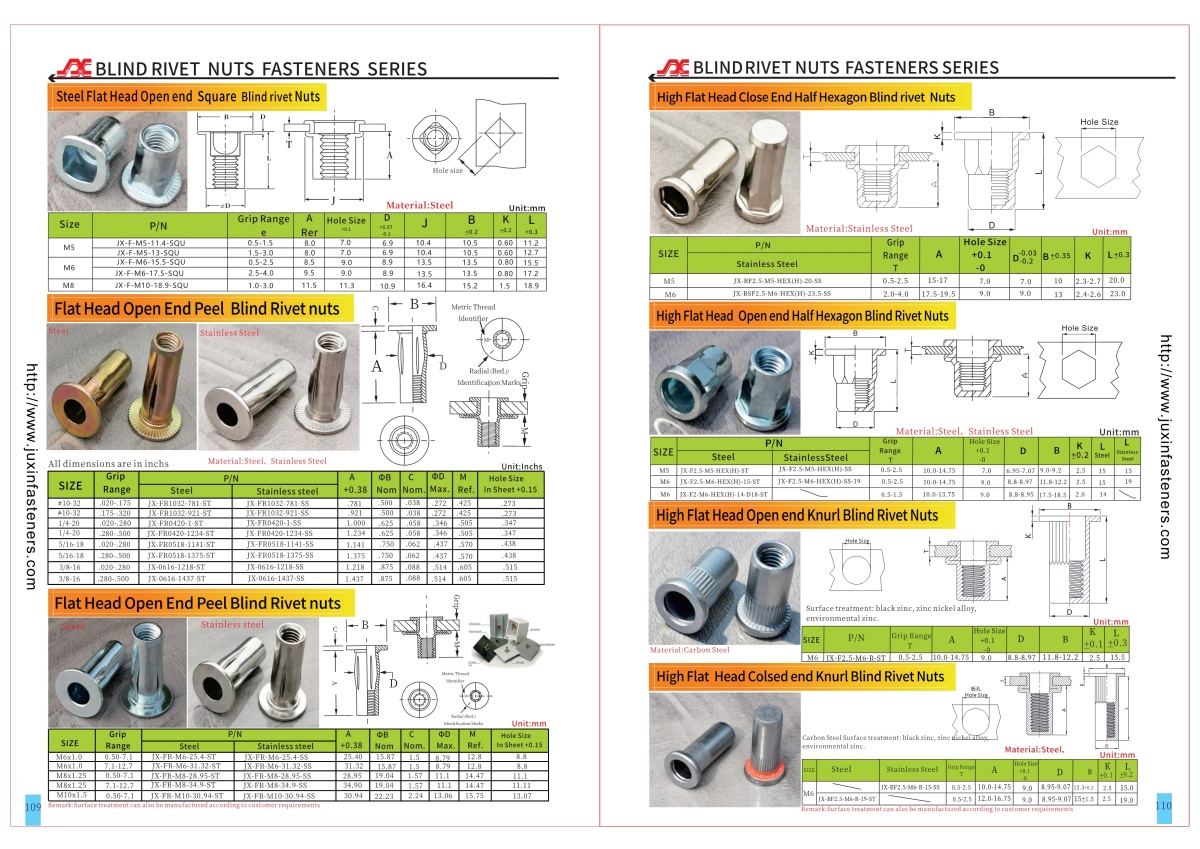
JUXIN FASTENERS supplies steel rivet nuts for plastic and composites, featuring a slotted bulbing body designed to create reusable internal threads in suitable plastic, fiberglass-reinforced, composite, and other relatively soft panels.
Unlike conventional blind rivet nuts that form a localized retaining bulge, this slotted-body design is intended to expand behind the panel and form a larger bearing footprint. The expanded sections help distribute installation and service loads over a broader backside area, potentially reducing localized pressure in materials that are vulnerable to crushing, indentation, or damage.
These fasteners are installed from one accessible side through a compatible drilled or punched round hole using an appropriate blind rivet nut setting tool. Their suitability depends on the actual panel material, thickness, hole geometry, and installation conditions.
Product Features
Product type: Rivet Nuts for Plastic and Composites
Body design: Slotted bulbing body
Head: Flat head / Flanged head
End: Open end
Material: Steel
Metric thread sizes: M5, M6, M8, M10
Unified inch threads: #10-32 UNF, 1/4-20 UNC, 5/16-18 UNC, 3/8-16 UNC
Product-family grip range: 0.5–7.1 mm (approx. 0.020–0.280 in)
Installation: One-sided blind installation
Mounting hole: Compatible round hole
Surface treatment options: Color Zinc or RoHS Blue Zinc, subject to approved specification
Installed backside expansion: According to approved product geometry and installation conditions
Mechanical performance: Subject to application-specific validation
Potential applications include plastic equipment housings, fiberglass panels, selected fiber-reinforced composite structures, industrial machine covers, commercial vehicle panels, agricultural equipment housings, HVAC components, and removable service panels.
The expanded backside geometry is intended to improve load distribution, but the insert must be qualified for the actual parent material. No universal crush-proof performance or pull-out rating is assumed.
For OEM technical review, drawings, and quotations, contact info@juxinfasteners.com.
Website: www.juxinfasteners.com
Product Specification
Steel Rivet Nuts for Plastic and Composites – Slotted Bulbing Body Fastening Solutions
JUXIN FASTENERS supplies steel rivet nuts for plastic and composite panels for OEM manufacturers, product design engineers, structural engineers, purchasing managers, and supplier development teams requiring reusable threaded fastening points in suitable non-metallic panels.
The defining feature of this product is its slotted bulbing body.
During installation, the slotted sections are designed to expand behind the parent panel, creating a larger backside bearing footprint than certain conventional blind rivet nut configurations.
This geometry can help distribute axial loads over a broader area and may reduce localized pressure on suitable plastic and composite materials.
However, installation and service performance depend on the parent material, hole geometry, grip thickness, insert design, and setting process.
The product is not automatically suitable for every thermoplastic, thermoset, fiberglass, carbon-fiber composite, or sandwich panel.
PRODUCT SPECIFICATIONS
Product name: Steel Rivet Nuts for Plastic and Composites – Slotted Bulbing Body
Product category: Steel Special Rivet Nuts
Material: Steel
Head type: Flat head / Flanged head
Body type: Slotted bulbing body
End type: Open end
Metric thread sizes:
M5
M6
M8
M10
Unified inch thread sizes:
#10-32 UNF
1/4-20 UNC
5/16-18 UNC
3/8-16 UNC
Product-family grip range: 0.5–7.1 mm
Approximate inch reference: 0.020–0.280 in
Installation method: One-sided blind installation
Mounting-hole type: Compatible round hole
Surface treatment options: Color Zinc or RoHS Blue Zinc
Steel grade: Subject to confirmation
Thread tolerance class: According to approved drawing
Flange dimensions: According to approved drawing
Body diameter and length: According to approved drawing
Slot dimensions: According to approved drawing
Installed backside expansion: Subject to installation validation
Mechanical retention: Subject to product-specific testing
The stated grip range represents the product family. The approved grip range for each thread size and body configuration must be confirmed against the selected drawing.
ENGINEERING DESIGN AND MATERIAL SELECTION
What Are Rivet Nuts for Plastic and Composites?
Rivet nuts for plastic and composites are threaded inserts intended for suitable non-metallic panels where direct tapping or conventional fastening methods may not provide the required connection.
They are installed from one accessible side of the workpiece.
The insert provides a metal internal thread for mating screws or bolts.
This can be useful where a panel requires removable covers, brackets, or serviceable components.
The fastening method must be selected according to the parent material and expected loading conditions.
How Does the Slotted Bulbing Body Work?
The slotted shank contains longitudinal openings that influence how the body deforms during installation.
When the insert is set, the slotted sections expand behind the panel.
The expanded sections form a backside bearing structure that helps retain the insert.
Depending on the design, this structure may provide a broader bearing footprint than a conventional retaining bulge.
The final installed geometry depends on:
Slot length
Slot width
Number of slots
Body diameter
Body wall thickness
Steel grade
Grip thickness
Setting stroke or force
The installation process must produce the intended expansion without damaging the internal thread or parent panel.
Why Backside Bearing Area Matters in Plastics
Many plastics have different mechanical behavior from metals.
Under concentrated loading, some plastics may experience:
Local indentation
Permanent deformation
Cracking
Creep
Loss of joint retention
A larger backside bearing footprint can potentially reduce localized bearing pressure.
However, the actual benefit depends on the load path and parent-material properties.
The insert must be tested in the intended material.
Plastic Crushing and Installation Damage
Plastic crushing can occur when local compressive stress exceeds the material's capacity.
Installation damage may also result from excessive setting force or unsuitable hole geometry.
Engineers should consider:
Plastic material grade
Panel thickness
Local compressive strength
Temperature
Installation force
Backside bearing area
Hole quality
A slotted bulbing rivet nut is designed to distribute load, but it does not guarantee that crushing cannot occur.
Plastic Creep Under Sustained Loading
Many polymers exhibit time-dependent deformation under sustained stress.
This behavior is commonly referred to as creep.
Creep can affect the installed joint by changing local contact pressure or allowing gradual deformation around the insert.
Relevant factors include:
Polymer type
Operating temperature
Sustained load
Installation deformation
Service duration
Environmental exposure
For long-term applications, short-term pull-out testing alone may be insufficient.
Thermoplastic Panel Applications
Potential thermoplastic applications include selected equipment housings, protective covers, and fabricated panels.
However, different thermoplastics have different stiffness, strength, and creep behavior.
For example, a fastening solution suitable for one thermoplastic grade may not be suitable for another.
The OEM should identify the exact material and validate the installation.
Thermoset Composite Applications
Thermoset composites may exhibit relatively high stiffness but can be sensitive to localized damage.
Depending on the laminate construction, installation loading may produce cracking or other damage.
Engineers should consider:
Resin system
Reinforcement type
Laminate thickness
Hole preparation
Local bearing stress
Through-thickness strength
The installed rivet nut should be qualified using representative production panels.
Fiberglass-Reinforced Plastic Panels
Fiberglass-reinforced plastic, or FRP, is used in various industrial housings, covers, and structural panels.
A slotted bulbing rivet nut may be considered where a reusable threaded connection is required.
However, FRP properties depend on the reinforcement, resin, laminate construction, and manufacturing process.
Installation should be evaluated for:
Local crushing
Cracking
Delamination
Hole damage
Axial retention
Long-term loading
No universal FRP compatibility is assumed.
Carbon-Fiber Composite Panels
Carbon-fiber-reinforced polymer panels require particular attention to local bearing loads, laminate damage, and galvanic compatibility.
A steel insert may introduce corrosion concerns when electrically connected to carbon fibers in the presence of an electrolyte.
Suitable isolation or protective measures may be necessary.
The insert should not be approved solely because the bulbing body creates a larger bearing area.
Sandwich Panel Considerations
Some composite panels use a lightweight core between stronger face sheets.
These structures behave differently from solid laminates.
Installation may cause:
Core crushing
Face-sheet indentation
Delamination
Local buckling
Loss of retention
A slotted bulbing rivet nut may not be appropriate for every sandwich panel.
The complete panel construction and fastening method must be evaluated.
Slotted Bulbing Body vs. Conventional Rivet Nuts
Conventional rivet nuts generally form a localized retaining bulge behind the parent panel.
Slotted bulbing designs are intended to create an expanded backside structure.
Potential differences include:
Bearing footprint
Installation stroke
Deformation pattern
Grip range
Axial retention
Rotational retention
Tool compatibility
The correct configuration depends on the actual parent material and loading requirements.
Slotted Bulbing Body vs. Heat-Set Inserts
Heat-set inserts are typically installed into suitable thermoplastic materials using controlled heating.
The surrounding plastic softens and flows around designated retention features.
Slotted bulbing rivet nuts use a mechanical blind installation process.
The two products differ in:
Installation method
Parent-material requirements
Retention mechanism
Tooling
Qualification testing
A slotted bulbing rivet nut should not be described as a standard heat-set insert.
Slotted Bulbing Body vs. Mold-In Inserts
Mold-in inserts are positioned within a mold before or during the molding process.
The molded material surrounds the insert to establish retention.
A blind rivet nut is generally installed after the parent component has been manufactured.
The appropriate fastening method depends on the manufacturing sequence, material, mechanical requirements, and production cost.
Slotted Bulbing Body vs. Bonded Inserts
Bonded inserts use an adhesive system to establish retention.
Their performance depends on adhesive selection, surface preparation, curing, and environmental exposure.
Slotted bulbing rivet nuts use mechanical deformation for retention.
The correct method depends on the application and required performance.
Mounting-Hole Preparation
These rivet nuts are installed into compatible round holes.
Depending on the parent material, holes may be drilled, punched, machined, or produced by another approved method.
The hole must meet the dimensional and quality requirements of the selected insert.
For plastics and composites, hole preparation should avoid excessive damage.
The approved drawing should define:
Hole diameter
Hole tolerance
Hole edge condition
Burr limits
Panel thickness
Hole position
Drilled vs. Punched Holes
Drilled holes may be appropriate for many plastic and composite panels.
Punching may be appropriate for certain sheet materials where the process does not cause unacceptable damage.
However, punching is not suitable for every composite laminate.
The hole-making process should be selected according to the material and manufacturing requirements.
Hole Edge Damage and Delamination
Poor hole preparation can reduce the strength of the parent material around the insert.
For composite panels, drilling may produce fiber damage or delamination if the process is not controlled.
For plastics, unsuitable cutting conditions may produce cracking, melting, or dimensional defects.
The hole quality should be inspected before installation.
Grip Range: 0.5–7.1 mm
This product family is specified with a grip range of 0.5–7.1 mm.
The approved grip range for each thread size must be confirmed.
Grip range refers to the parent-material thickness accommodated by the selected insert.
Installation outside the approved range may affect the intended backside expansion and retention.
Backside Clearance
The expanded body requires sufficient space behind the panel.
Engineers should verify:
Axial clearance
Radial clearance
Nearby ribs
Adjacent components
Internal structures
Mating screw projection
A rivet nut may fit into the hole before installation but interfere with surrounding components after setting.
Edge Distance and Hole Spacing
The expanded backside geometry requires adequate surrounding material.
If the mounting hole is too close to a panel edge or another opening, the parent material may crack or deform.
The required edge distance depends on:
Insert geometry
Installed bearing footprint
Parent material
Panel thickness
Applied loading
Nearby cutouts
No universal minimum edge distance is assumed.
Flat Head Flange
The flat-head flange provides a bearing surface against the accessible side of the panel.
It helps support the insert around the mounting hole.
The flange dimensions influence:
Bearing contact
Head projection
Local panel loading
Axial retention
Assembly stack height
The flange should be included in the joint stack-up.
Open-End Construction
The open-end barrel allows the mating screw to extend through the insert where sufficient backside clearance is available.
This provides flexibility in screw-length selection.
However, the screw tip must not interfere with internal components.
Open-end construction does not inherently provide environmental sealing.
Metric Thread Options
Available metric thread sizes include:
M5
M6
M8
M10
Metric thread compatibility should be verified using the applicable ISO requirements.
The exact pitch and tolerance class should be confirmed against the approved drawing.
Unified Inch Thread Options
Available Unified inch-thread sizes include:
#10-32 UNF
1/4-20 UNC
5/16-18 UNC
3/8-16 UNC
These sizes are relevant to OEM programs using Unified inch-thread systems.
The internal thread must match the intended mating screw.
Metric and UNC/UNF threads are not directly interchangeable.
Thread Strength and Tightening Torque
The allowable tightening torque depends on the complete joint.
Relevant factors include:
Steel grade
Thread size and pitch
Mating screw material
Thread engagement
Friction conditions
Insert retention
Parent-material strength
A torque specification developed for a conventional steel nut should not automatically be applied to a blind rivet nut.
Pull-Out Resistance
Pull-out resistance concerns the axial force required to remove the installed insert under a defined test arrangement.
For plastic and composite panels, failure may involve:
Parent-material cracking
Local crushing
Delamination
Insert displacement
Slotted-section deformation
Flange pull-through
The governing failure mode depends on the application.
No numerical pull-out rating is claimed without supporting test data.
Push-Out Resistance
Push-out resistance concerns displacement of the installed insert in the opposite axial direction under a defined test arrangement.
The result depends on:
Insert geometry
Parent material
Panel thickness
Hole dimensions
Installation parameters
Test method
Pull-out and push-out performance should be evaluated separately where relevant.
Spin-Out Resistance
Spin-out resistance describes the installed insert's resistance to rotation within the mounting hole.
For slotted bulbing rivet nuts, rotational retention depends on the body geometry, hole fit, parent material, and installation conditions.
Where defined spin-out resistance is required, the selected insert should be tested.
Insert Spin-Out vs. Screw Loosening
Insert spin-out and screw loosening are separate engineering concerns.
Spin-out occurs when the rivet nut rotates within the parent panel.
Screw loosening occurs when the mating screw loses its intended clamping condition or rotates relative to the internal thread.
The slotted bulbing body does not automatically prevent screw loosening under vibration.
Installation Tooling
These rivet nuts are installed using compatible blind rivet nut setting tools.
Manual, pneumatic, or battery-powered tools may be appropriate depending on the product and production requirements.
Tool selection should consider:
Thread size
Insert geometry
Steel grade
Setting force
Setting stroke
Production volume
Operator access
The tool must be compatible with the selected insert.
Installation Stroke and Force Control
The setting process must produce the intended backside expansion without damaging the parent material.
Excessive force or stroke may cause crushing, cracking, or other damage.
Insufficient setting may reduce retention.
Production parameters should be validated using representative panels.
Under-Setting and Over-Setting
Under-setting may produce insufficient backside expansion and reduced retention.
Over-setting may damage the slotted sections, internal thread, or parent material.
The correct setting parameters depend on:
Insert geometry
Steel grade
Panel thickness
Parent-material strength
Installation tooling
Color Zinc Surface Treatment
Color Zinc is a specified surface-treatment option for this product family.
However, the term alone does not fully define the coating system.
The approved specification should identify:
Zinc coating type
Coating thickness
Conversion coating or passivation
Sealant or topcoat, if required
Appearance requirements
Corrosion-test method
Acceptance criteria
Restricted-substance requirements
RoHS Blue Zinc Surface Treatment
RoHS Blue Zinc is another specified finish option.
For OEM procurement, the term should be translated into a defined coating specification.
A blue or silver-colored zinc finish does not automatically establish RoHS compliance.
Compliance should be supported by appropriate documentation for the applicable requirements.
Zinc-Yellow-Chromate-Plated Steel
Zinc-yellow-chromate-plated steel is a commonly recognized product description in industrial fastening catalogs.
However, the exact conversion-coating chemistry and restricted-substance status must be verified.
Traditional yellow chromate systems may contain hexavalent chromium.
Where RoHS compliance is required, the approved coating specification and supporting documentation must establish compliance.
A yellow appearance alone does not determine whether the coating is compliant.
Coating Integrity After Bulbing
The installation process involves plastic deformation of the slotted sections.
This deformation may affect the coating in areas of high local strain.
For corrosion-sensitive applications, engineers should consider:
Coating ductility
Deformation geometry
Installation process
Exposed steel after setting
Environmental exposure
Hydrogen Embrittlement Risk
Electroplating processes can introduce hydrogen into susceptible steel fasteners.
The risk depends on steel strength, hardness, tensile stress, and processing conditions.
For higher-strength or hardened steel components, the coating process should be reviewed against applicable requirements.
ISO 4042 addresses electroplated fastener coating systems and hydrogen embrittlement considerations.
Galvanic Corrosion and Dissimilar Materials
Zinc-plated steel inserts may be installed in assemblies containing aluminum, carbon-fiber composites, or other materials.
Where dissimilar conductive materials are electrically connected in the presence of an electrolyte, galvanic corrosion may occur.
The complete assembly should be reviewed for corrosion compatibility.
Long-Term Service Performance
Long-term performance depends on more than the initial installation.
Relevant factors include:
Sustained load
Temperature
Humidity
Parent-material creep
Vibration
Repeated maintenance
Corrosion
Mechanical fatigue
Where the application is critical, qualification should include the relevant service conditions.
INDUSTRIAL APPLICATIONS AND OEM FASTENING SOLUTIONS
Plastic Equipment Housings
Potential applications include industrial equipment housings, protective covers, and removable panels.
The slotted bulbing body may help distribute backside loads in suitable plastic materials.
Composite Equipment Panels
Potential applications include selected fiberglass-reinforced and other composite panels requiring reusable threaded fastening points.
Installation must be validated for laminate damage and retention.
Commercial Vehicle Components
Potential applications include selected non-critical composite panels, interior equipment housings, and serviceable covers.
Vibration, corrosion, and mechanical retention requirements must be evaluated.
Agricultural Machinery
Potential applications include equipment covers, fabricated panels, and protective housings.
The coating system should be selected according to the expected exposure environment.
Industrial Machinery and Automation
Potential applications include machine covers, protective guards, access panels, and equipment housings.
The selected insert should be qualified for the actual parent material and service loading.
HVAC and Appliance Equipment
Potential applications include equipment cabinets, plastic housings, and serviceable mounting structures.
Installation consistency and long-term retention should be verified.
Transportation Equipment
Potential applications include selected non-safety-critical interior panels and equipment enclosures.
Vibration, fatigue, and environmental requirements must be reviewed.
ENGINEERING DECISION: WHEN IS A SLOTTED BULBING RIVET NUT THE WRONG CHOICE?
A slotted bulbing rivet nut may not be the best solution when:
The parent material cannot support the installation loads
The panel is susceptible to unacceptable crushing or delamination
Backside clearance is insufficient
The installation tool is incompatible
The required rotational retention has not been validated
The application requires a flush or recessed head
The panel construction is unsuitable for the expansion geometry
Long-term creep or environmental exposure creates unacceptable risk
In these cases, alternative fastening methods should be evaluated.
OEM ENGINEERING SELECTION CHECKLIST
Before approving a steel rivet nut for plastic or composite panels, confirm:
Required metric or Unified inch thread size
Steel grade and hardness
Parent material and panel construction
Panel thickness
Approved grip range
Mounting-hole diameter and tolerance
Hole edge condition
Flange dimensions
Body and slot dimensions
Installed backside expansion
Available backside clearance
Mating screw material and length
Required thread engagement
Installation tool compatibility
Setting stroke or force
Required pull-out and push-out resistance
Required spin-out resistance
Tightening torque requirements
Coating specification
Corrosion requirements
Restricted-substance compliance requirements
Environmental exposure
Inspection and traceability requirements
ENGINEERING STANDARDS AND TECHNICAL VERIFICATION
Product selection should be based on the approved dimensional drawing and the requirements of the intended assembly.
Applicable ISO metric thread standards may include ISO 261 and ISO 965 where relevant.
Unified inch threads should be specified according to applicable ASME B1.1 requirements.
ISO 4042 addresses electroplated coating systems for fasteners, including zinc-based coatings and hydrogen embrittlement considerations.
Where applicable, the OEM should define coating requirements using the appropriate ISO, EN, ASTM, or other recognized technical specification.
Corrosion testing may be specified using an appropriate method such as ISO 9227 or ASTM B117, together with agreed exposure conditions and acceptance criteria.
A test method alone does not establish a required corrosion-performance rating.
Metric and UNC/UNF thread systems are not directly interchangeable.
No specific certification, mechanical performance value, coating performance, or standard conformity should be assumed without supporting documentation.
OEM PROCUREMENT AND SUPPLIER QUALIFICATION
For purchasing managers and supplier development teams, steel rivet nuts for plastic and composites require careful dimensional, material, and installation comparison before supplier substitution.
Two products described as M6 slotted bulbing rivet nuts may differ in:
Steel grade
Slot geometry
Body dimensions
Flange dimensions
Mounting-hole requirements
Grip range
Installation parameters
Backside expansion
Thread strength
Coating system
Mechanical retention performance
These differences may affect assembly compatibility and joint reliability.
Before approving an alternative supplier, procurement teams should compare complete dimensional drawings, material specifications, coating requirements, and representative installation test results.
For recurring OEM programs, inspection criteria, traceability, packaging requirements, annual demand, and delivery expectations should be established during sourcing.
TOTAL INSTALLED COST CONSIDERATIONS
For OEM procurement, the rivet nut purchase price is only one component of the installed cost.
The total installed cost may include:
Rivet nut purchase price
Mounting-hole preparation
Installation tooling
Installation cycle time
Inspection
Rework
Scrap risk
Coating requirements
Supplier qualification
Inventory management
Where improved backside load distribution is required, a slotted bulbing configuration may justify additional qualification or tooling requirements.
CUSTOM OEM RIVET NUT RFQ REQUIREMENTS
Please provide:
2D drawing or 3D CAD model
Required metric or Unified inch thread size
Steel grade and hardness requirements
Parent material and panel thickness
Mounting-hole diameter and tolerance
Flange diameter and thickness
Body and slot dimensions
Approved grip range
Available backside clearance
Mating screw material and length
Installation method and tooling requirements
Required axial and rotational retention
Tightening torque requirements
Color Zinc or RoHS Blue Zinc finish requirement
Coating thickness and corrosion requirements
Restricted-substance documentation requirements
Inspection and traceability requirements
Prototype or production quantity
Estimated annual demand
Delivery destination
JUXIN FASTENERS supports drawing-based technical reviews and OEM sourcing discussions for steel rivet nuts for plastic and composites and related custom threaded fastening components.
Final dimensions, steel grade availability, coating specifications, installation compatibility, mechanical performance, and inspection requirements should be confirmed before production approval.
RELATED FASTENING SOLUTIONS
Stainless Steel Rivet Nuts for Plastic and Composites – Slotted Body
An alternative material configuration for selected plastic and composite assemblies requiring application-specific validation.
Steel Flat Head Open-End Slotted Shank Blind Rivet Nuts
A related steel slotted-body configuration for general OEM panel fastening applications.
Steel Flat Head Open-End Square Body Blind Rivet Nuts
An alternative where geometric anti-rotation engagement with a square mounting hole is required.
Aluminum Flat Head Open-End Knurled Round Body Blind Rivet Nuts
An alternative where lightweight construction and compatible round-hole installation are preferred.
Aluminum Flat Head Open-End Full Hex Body Blind Rivet Nuts
An alternative where reduced component weight and hexagonal anti-rotation engagement are important.
REQUEST AN OEM QUOTATION
Looking for steel rivet nuts for plastic and composites in M5, M6, M8, M10, #10-32, 1/4-20, 5/16-18, or 3/8-16?
Send JUXIN FASTENERS your engineering drawings, parent-material specifications, panel thickness, mounting-hole dimensions, installation requirements, coating specifications, and estimated purchasing quantities.
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
JUXIN FASTENERS – Industrial Blind Rivet Nuts and Custom OEM Fastening Solutions.
Product Packaging
Packaging and Delivery – Steel Rivet Nuts for Plastic and Composites
JUXIN FASTENERS reviews packaging arrangements according to product dimensions, order quantities, handling conditions, and OEM purchasing requirements.
Packaging Requirements
Material: Steel
Metric thread sizes: M5, M6, M8, M10
Unified inch thread sizes: #10-32 UNF, 1/4-20 UNC, 5/16-18 UNC, 3/8-16 UNC
Product-family grip range: 0.5–7.1 mm
Surface finish options: Color Zinc or RoHS Blue Zinc, subject to approved specification
Packaging quantity: Subject to order confirmation
Inner packaging: According to approved packing instructions
Outer packaging: According to shipment requirements
Product identification: Part number, thread designation, steel grade, and coating specification as required
Batch identification: According to agreed traceability requirements
Custom packaging: Subject to technical and commercial confirmation
Packaging Protection
Steel slotted bulbing rivet nuts should be protected from unnecessary mechanical damage, flange deformation, thread contamination, and coating damage during handling, storage, and transportation.
Particular attention should be given to preserving the slotted-body geometry, flange dimensions, and internal thread condition.
Where appearance or coating integrity is specified, appropriate protection should be agreed upon before shipment.
Metric and Unified inch-thread products should be clearly identified and segregated to reduce the risk of assembly mix-ups.
OEM Supply and Documentation
For recurring OEM programs, packaging quantities, labeling, inspection documentation, coating records, material records, and delivery arrangements should be agreed upon before shipment.
Final packaging specifications are confirmed according to the approved purchase order.
For OEM packaging requirements and quotations, contact info@juxinfasteners.com.
Website: www.juxinfasteners.com
Product Pictures
Tags
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY