Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

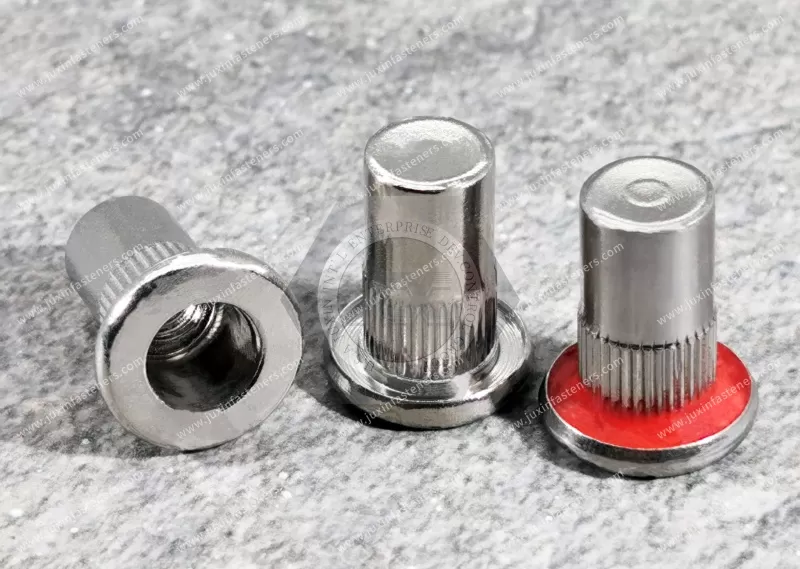
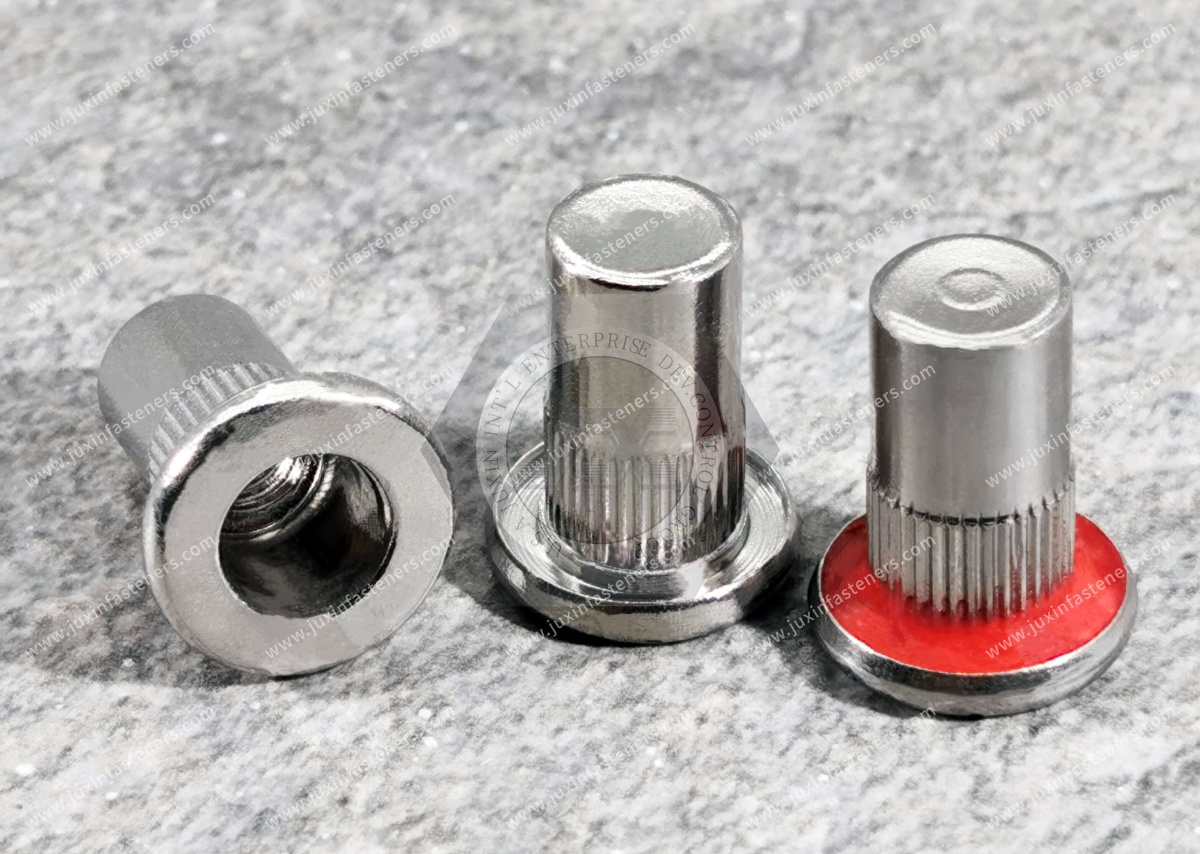
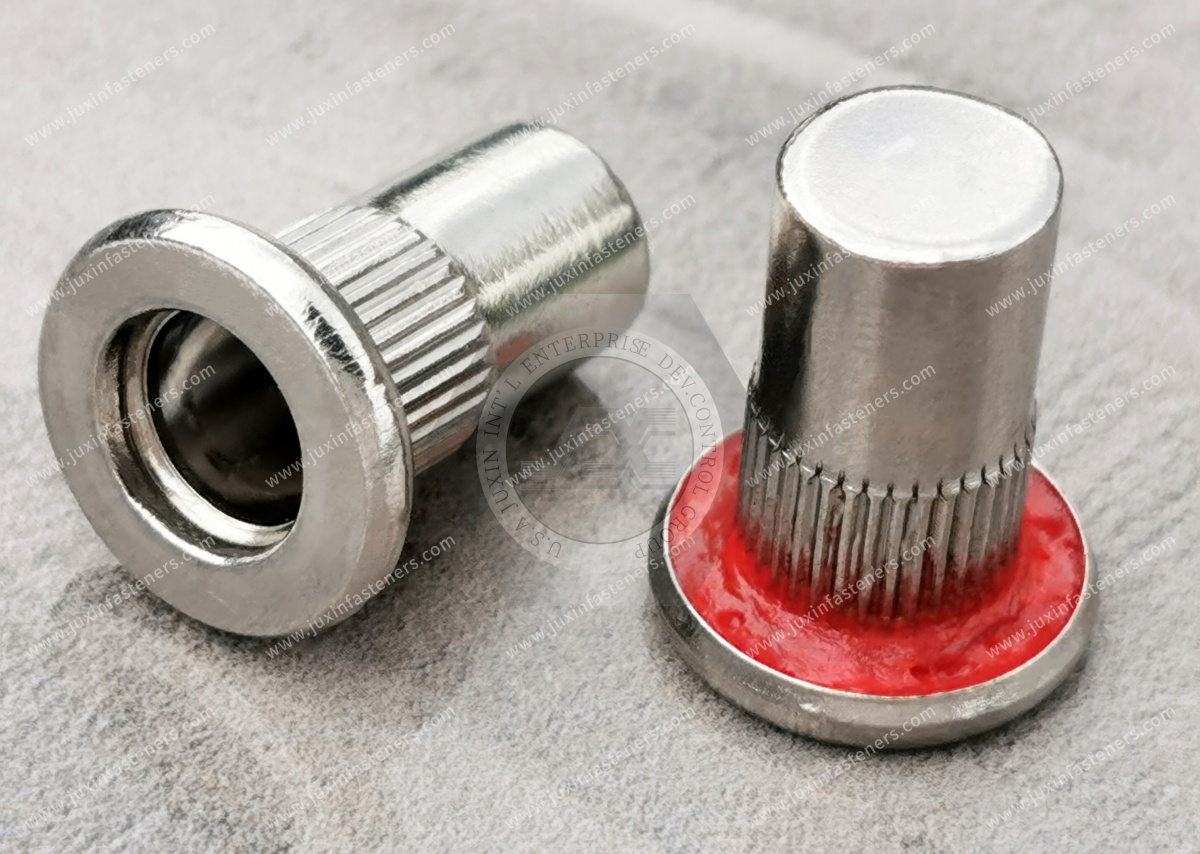
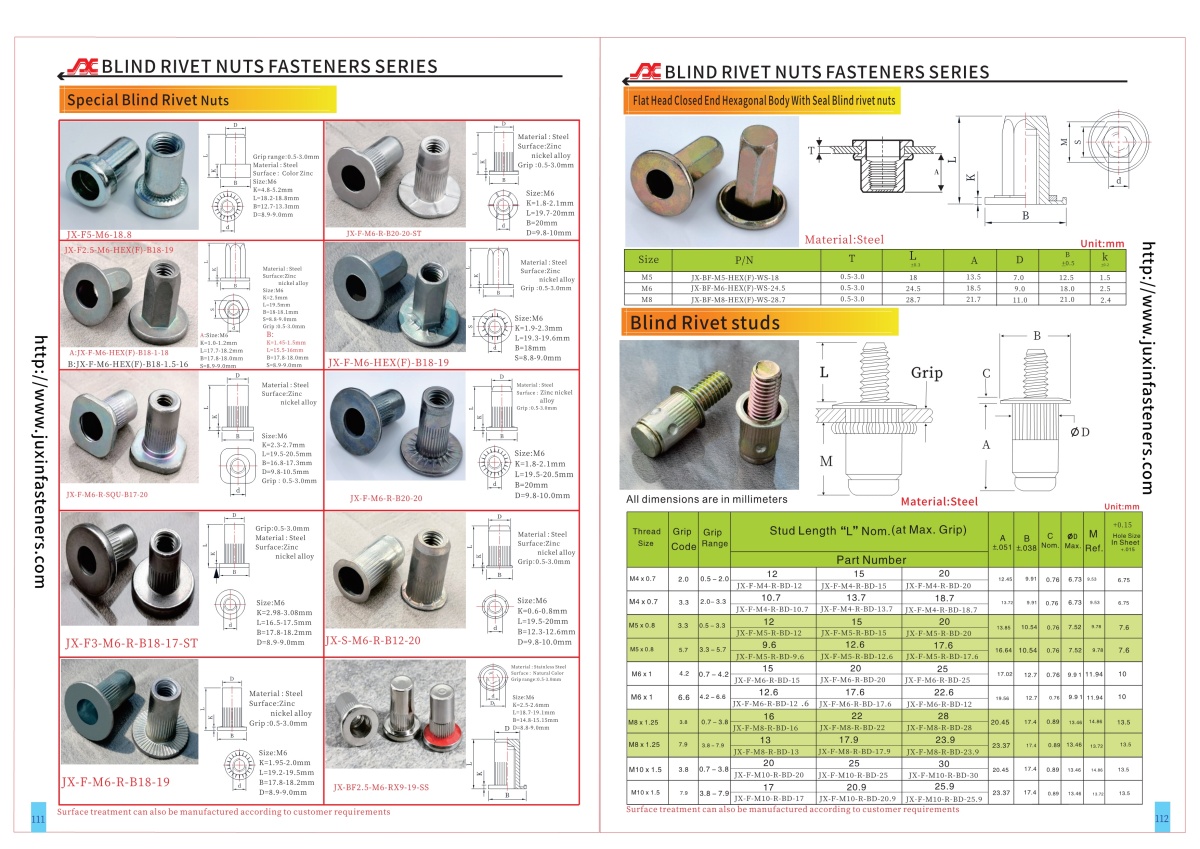
JUXIN FASTENERS supplies custom M6 Stainless Steel Closed-End Knurled Body Blind Rivet Nuts for automotive sheet-metal assemblies. The limited-height flat head supports compact installation, while the knurled body helps resist insert rotation. The closed end prevents screw projection beyond the barrel.
Part No.: JX-BF2.5-M6-RX9-19-SS
Thread Size: M6
Material: Stainless Steel
Grip Range: 0.5–2.5 mm
Finish: Natural Stainless Steel
Additional Treatment: Anti-Loosening Adhesive
Head Type: Limited-Height Flat Head
Body Type: Knurled Round Body
End Type: Closed End
Product Specification
Product Specifications
Product Name: M6 Stainless Steel Closed-End Twist-Resistant Rivet Nuts
Part Number: JX-BF2.5-M6-RX9-19-SS
Product Type: Custom Automotive Blind Rivet Nut
Material: Stainless Steel
Stainless Steel Grade: According to the approved material specification
Thread Size: M6
Thread Pitch and Tolerance: According to the approved drawing
Head Type: Limited-Height Flat Head
Body Type: Knurled / Ribbed Round Body
End Type: Closed End / Blind End
Grip Range: 0.5–2.5 mm (approximately 0.020–0.098 in)
Surface Finish: Natural Stainless Steel
Additional Treatment: Anti-Loosening Adhesive
Adhesive Location, Chemistry and Performance: According to the approved drawing and application specification
Installation Method: One-Sided Blind Installation
Mounting Hole: Compatible Round Hole
Flange, Body and Closed-End Dimensions: According to the approved drawing
Primary Application: Automotive OEM and Electric Vehicle Assemblies
Mechanical Performance: Subject to product-specific validation
Product Overview
JUXIN FASTENERS supplies custom stainless steel closed-end twist-resistant rivet nuts for automotive OEMs, electric vehicle component manufacturers, and industrial equipment suppliers requiring reusable internal threads in thin sheet-metal assemblies.
Part number JX-BF2.5-M6-RX9-19-SS combines four application-specific design characteristics: a limited-height flat head, a knurled round body, a closed-end barrel, and an anti-loosening adhesive treatment.
The limited-height head addresses front-side packaging constraints. The knurled body helps resist insert rotation. The closed end prevents a correctly selected screw from projecting beyond the rear of the insert.
The specified stainless steel material and natural finish provide a different material and corrosion-management approach from zinc-plated carbon steel alternatives.
The supplied anti-loosening adhesive introduces an additional joint-design consideration that must be evaluated separately from insert retention.
This configuration is intended for a riveted plate thickness of 0.5–2.5 mm.
Closed-End Twist-Resistant Rivet Nuts: Engineering Function
A closed-end twist-resistant rivet nut performs several different functions within a fastening system.
The internal thread provides a reusable attachment point for the mating screw.
The closed barrel end limits screw penetration and separates the internal threaded cavity from the space behind the insert.
The knurled exterior provides mechanical engagement with the parent material to help resist insert rotation.
The deformed barrel section provides backside retention after installation.
These functions must be evaluated separately.
A rivet nut may resist rotation but still have insufficient axial retention for a particular assembly.
Similarly, a closed-end insert may protect the space behind its barrel without sealing the interface between its flange and the parent panel.
The complete joint must meet the intended installation, mechanical and environmental requirements.
Limited-Height Flat Head for Automotive Packaging
The limited-height flat head is an important distinction from conventional high-profile flange designs.
Automotive equipment is often packaged within restricted spaces, especially around electrical modules, mounting brackets, covers and serviceable assemblies.
A reduced flange height may help manage interference with adjacent components.
Potential engineering benefits include:
Reduced front-side flange projection
Improved compatibility with selected close-clearance assemblies
More flexibility in equipment mounting layouts
Reduced risk of unintended contact with nearby components
However, a limited-height head should not automatically be described as flush-mounted or countersunk.
Its actual projection depends on the approved flange thickness and mounting arrangement.
A thinner head may also provide different bearing characteristics from a conventional thicker flange.
Engineers should evaluate flange seating, parent-panel strength, local bearing stress and installation-tool compatibility.
Automotive and Electric Vehicle Applications
Custom closed-end stainless steel rivet nuts may be evaluated for automotive applications where restricted installation space, backside clearance, and serviceability are important.
Potential applications include:
Electric vehicle electrical equipment housings
Automotive control module mounting brackets
Battery management system accessory panels
EV power electronics equipment covers
Automotive interior equipment brackets
Vehicle electrical enclosure mounting points
Thermal management equipment supports
Commercial vehicle equipment panels
Automotive service access panels
Thin stainless steel or compatible sheet-metal assemblies
For electric vehicle systems, the suitability of the fastener depends on the actual mechanical, electrical, corrosion and environmental requirements.
The product should not be assumed to provide high-voltage electrical isolation, enclosure sealing, or structural crash-load performance.
Applications involving battery safety, crash loads or other safety-critical functions require separate engineering qualification.
Closed-End Protection and Screw Clearance
The closed-end design is particularly relevant where a screw must not extend into the space behind the mounting panel.
This may help avoid contact with nearby wiring, covers, equipment housings or other components.
However, the mating screw must be selected according to the usable internal thread depth.
A screw that is too long may bottom out against the closed end before the joint develops the intended clamp load.
This can create a misleading tightening condition.
The installer may reach the specified torque without achieving the required joint clamping force.
For automotive assembly validation, engineers should verify:
Available internal thread depth
Mating screw length
Required thread engagement
Joint stack-up
Screw-tip clearance
Tightening torque
Required clamp load
Closed-end deformation under installation conditions
This is especially important for custom rivet nuts with restricted overall length.
Closed End vs. Sealed Rivet Nut
A closed-end rivet nut is not necessarily a fully sealed rivet nut assembly.
The closed barrel blocks a direct opening through the rear of the insert.
However, moisture, gas or contaminants may still pass through the interface between the flange, body and parent panel if that interface is not sealed.
For applications requiring environmental sealing, engineers should evaluate:
Flange sealing geometry
Gasket or sealing washer requirements
Panel surface condition
Mounting-hole clearance
Seal compression
Temperature exposure
Fluid compatibility
Required ingress-protection performance
A sealing test may be required for the complete installed assembly.
The closed-end construction alone does not establish an IP rating, pressure-tight seal or gas-tight connection.
Knurled Body and Anti-Rotation Performance
The external ribs on the round body are designed to engage the surrounding parent material after installation.
This helps resist rotation of the insert when a mating screw is tightened or removed.
For automotive production, consistent anti-rotation performance depends on the interaction among the insert geometry, mounting hole, parent material and setting process.
Important variables include:
Knurl profile
Body diameter
Mounting-hole diameter
Parent-material hardness
Panel thickness
Installation stroke or force
Backside deformation
Applied screw torque
An oversized mounting hole may reduce knurl engagement.
An undersized hole may interfere with insertion or damage the parent material.
The required spin-out torque should be defined and validated using representative production components.
The knurled body does not independently prevent the mating screw from loosening under vibration.
Anti-Loosening Adhesive: A Separate Joint Function
This product is specified with an anti-loosening adhesive treatment.
The adhesive must be evaluated separately from the knurled body's mechanical anti-rotation function.
Knurling addresses rotation of the installed rivet nut within the parent panel.
A suitable thread-locking adhesive, when applied to the intended threaded interface and correctly activated or cured, may help resist relative rotation between the mating screw and the internal thread.
However, the precise adhesive location and mechanism have not been established from the supplied product information.
Before describing the treatment as a pre-applied threadlocker, prevailing-torque feature or locking patch, the approved specification should identify:
Adhesive location
Adhesive chemistry
Application coverage
Activation or curing conditions
Required assembly torque
Breakaway or prevailing-torque requirements
Temperature limits
Chemical compatibility
Reuse limitations
Shelf-life and storage conditions
These requirements matter because some locking compounds affect tightening torque, clamp-load development and repeated service performance.
The presence of adhesive alone does not establish a guaranteed vibration-resistance rating.
Stainless Steel Material and Natural Finish
The confirmed base material is stainless steel, supplied with a natural finish.
Stainless steel may offer corrosion-resistance advantages over uncoated carbon steel in suitable environments.
However, corrosion behavior depends on the stainless steel grade, manufacturing condition, surface condition and service environment.
The exact grade has not been supplied.
Therefore, this product should not be advertised specifically as AISI 304, AISI 316, 18-8 or another stainless steel grade without material verification.
For automotive procurement, the material specification should establish:
Stainless steel grade
Chemical composition
Mechanical properties
Manufacturing condition
Surface finish
Corrosion requirements
Material inspection criteria
Relevant stainless steel material specifications may include appropriate ASTM or EN standards, depending on the confirmed material grade and product form.
Natural stainless steel should not be described as zinc plated or zinc-nickel plated.
Stainless Steel and Galvanic Corrosion in Aluminum Panels
Electric vehicle manufacturers frequently use aluminum alloys alongside stainless steel components.
In wet or electrolyte-containing environments, direct contact between stainless steel and aluminum may contribute to galvanic corrosion.
For an M6 stainless steel rivet nut installed in an aluminum panel, engineers should consider:
Aluminum alloy and surface treatment
Stainless steel grade
Contact geometry
Moisture exposure
Electrical continuity
Protective coatings
Isolation materials
Sealing arrangements
Stainless steel corrosion resistance does not automatically mean the surrounding aluminum assembly is protected against galvanic corrosion.
The complete joint should be evaluated for its intended environment.
Grip Range: 0.5–2.5 mm
The specified riveted plate thickness is 0.5–2.5 mm.
This corresponds approximately to 0.020–0.098 in.
The grip range identifies the parent-material thickness intended for the specified insert.
It is not equivalent to overall body length, flange thickness or internal thread depth.
For automotive applications, engineers should verify the actual thickness engaged by the rivet nut.
Installation outside the approved grip range may result in inadequate backside deformation, reduced retention or damage to the assembly.
The grip range should not be extended without validation.
M6 Metric Thread and North American Inch Reference
The confirmed nominal thread size is M6.
Its nominal diameter is 6.0 mm, approximately 0.2362 in.
M6 × 1.0 is a common ISO metric coarse-thread designation, but the actual thread pitch and tolerance must be verified from the approved drawing.
Relevant metric thread references include ISO 261 and ISO 965.
For North American purchasing, M6 must not be confused with 1/4-20 UNC or 1/4-28 UNF.
These are different thread systems and are not directly interchangeable.
ASME B1.1 may be used when reviewing Unified inch-thread requirements.
An inch-thread version should be considered a separate configuration requiring confirmed availability and engineering approval.
Round-Hole Installation Requirements
This product uses a knurled round body intended for installation in a compatible round mounting hole.
The hole may be drilled, punched or produced using another approved manufacturing process.
Mounting-hole quality should be controlled for:
Diameter and tolerance
Roundness
Burr condition
Parent-panel thickness
Material hardness
Surface condition
Hole-position accuracy
The correct mounting-hole dimensions must be obtained from the approved product drawing.
Standard M6 rivet nut hole dimensions should not be substituted without verification.
Installation Process and Tooling
The rivet nut is installed using compatible blind rivet nut setting equipment.
The setting tool applies axial force to deform the designated barrel section behind the parent panel.
This produces backside retention while the flange seats against the accessible panel surface.
For high-volume automotive production, pneumatic or battery-powered setting tools may be evaluated according to the assembly requirements.
Important installation checks include:
Correct hole dimensions
Panel thickness within the approved grip range
Compatible mandrel and nosepiece
Setting force or stroke
Flange seating
Backside deformation
Internal thread condition
Closed-end integrity
Axial retention
Spin-out resistance
Under-setting may produce inadequate retention.
Over-setting may damage the insert, deform the panel or affect the internal thread.
Installation conditions should be validated using representative production components.
Mechanical Retention and Joint Reliability
The mechanical performance of a closed-end rivet nut depends on the complete installed joint.
For automotive qualification, engineers should distinguish among:
Pull-out resistance
Push-out resistance
Spin-out torque
Thread stripping resistance
Parent-panel deformation
Screw tightening behavior
Clamp-load retention
Vibration performance
These characteristics represent different failure mechanisms.
A product with strong rotational retention may still require separate evaluation for axial loading.
The closed-end design may also introduce screw-bottoming considerations that are not present in the same way with open-end inserts.
No numerical mechanical performance is claimed without product-specific testing.
Vibration, Thread Locking and Repeated Service
Automotive assemblies may experience vibration, thermal cycling, shock and repeated maintenance.
The knurled body helps resist insert rotation.
The anti-loosening adhesive may provide a separate locking function, depending on its verified specification.
The complete joint should be assessed for:
Tightening torque
Clamp-load retention
Adhesive behavior
Temperature exposure
Vibration loading
Breakaway torque
Repeated disassembly
Replacement or reapplication requirements
Repeated service may affect the performance of certain adhesive locking systems.
The approved adhesive specification should define whether reuse is permitted.
Automotive OEM and Tier 1 Qualification
For automotive OEM and Tier 1 supplier qualification, the complete product definition should be reviewed.
Important requirements include:
Approved product drawing
Part number and drawing revision
Stainless steel grade
M6 thread specification
Limited-height flange dimensions
Knurled body geometry
Closed-end depth
Grip range
Mounting-hole dimensions
Adhesive specification
Installation parameters
Axial and rotational retention
Inspection and traceability requirements
Customer-specific programs may require first article inspection, dimensional records, material documentation, mechanical test results, PPAP submissions or additional quality records.
APQP, PPAP, IMDS and IATF 16949-related requirements should be addressed according to the actual customer program.
No particular certification, PPAP approval or automotive OEM qualification is implied without supporting documentation.
Automotive Procurement and Total Installed Cost
For purchasing managers and supplier development engineers, this custom rivet nut should be evaluated as a complete fastening solution rather than solely by unit price.
Important cost and supply considerations include:
Custom flange dimensions
Stainless steel grade
Closed-end manufacturing requirements
Knurled body consistency
Adhesive treatment requirements
Installation-tool compatibility
Mechanical testing
Inspection procedures
Packaging and traceability
Annual purchasing volume
Delivery planning
The combination of closed-end construction, restricted flange height and adhesive treatment may affect manufacturing and inspection requirements.
These characteristics should be included in the approved purchasing specification.
Other Industrial Applications
Beyond automotive manufacturing, similar closed-end stainless steel rivet nuts may be evaluated for:
Electrical equipment enclosures
Industrial control cabinets
Commercial vehicle equipment
Industrial automation systems
Maintenance access panels
Stainless steel sheet-metal assemblies
Equipment covers and housings
Application suitability must be verified against the actual material, loading and environmental requirements.
Related Fastening Solutions and Internal Linking
Steel High Flat Head Open-End Knurled Body Blind Rivet Nuts
A related open-end configuration for applications where screw projection and backside clearance requirements differ.
Steel Thin Head Open-End Knurled Body Blind Rivet Nuts
An alternative for restricted front-side projection where an open-end barrel is acceptable.
Steel High Flat Head Closed-End Knurled Body Blind Rivet Nuts
A related closed-end design family that should be compared by actual material, head geometry and approved specifications.
Steel Full Hex Body Blind Rivet Nuts
An alternative anti-rotation design for compatible hexagonal mounting holes.
Steel Square Flange Knurled Body Blind Rivet Nuts
An alternative custom flange geometry for drawing-specific assemblies.
Internal links should point to the corresponding verified product pages using descriptive anchor text. These related configurations are not automatically interchangeable.
OEM RFQ and Engineering Information
For technical review and quotation, please provide:
Part Number: JX-BF2.5-M6-RX9-19-SS
Approved 2D drawing or 3D CAD model
Required stainless steel grade
M6 thread pitch and tolerance
Parent-panel material
Panel thickness
Mounting-hole dimensions
Limited-height flange dimensions
Knurled body dimensions
Closed-end internal depth
Mating screw specifications
Anti-loosening adhesive requirements
Required installation parameters
Spin-out torque requirements
Pull-out and push-out requirements
Environmental and corrosion requirements
Inspection and traceability requirements
Prototype or production quantities
Estimated annual purchasing volume
Delivery destination
Why Source Custom Closed-End Rivet Nuts from JUXIN FASTENERS?
JUXIN FASTENERS supplies industrial fastening products for drawing-based OEM purchasing and engineering requirements.
For automotive customers, technical discussions can focus on restricted flange height, knurled body engagement, closed-end screw clearance, stainless steel material selection, adhesive treatment and installation reliability.
JX-BF2.5-M6-RX9-19-SS is identified as an M6 stainless steel closed-end knurled body blind rivet nut with a limited-height flat head, natural finish, anti-loosening adhesive treatment and 0.5–2.5 mm grip range.
Final dimensions, stainless steel grade, adhesive specifications and mechanical acceptance criteria must be confirmed before production approval.
Request an Automotive OEM Quotation
Looking for M6 stainless steel closed-end twist-resistant rivet nuts, custom automotive blind rivet nuts or stainless steel threaded inserts with anti-loosening treatment?
Send your engineering drawings, technical specifications and estimated purchasing quantities to JUXIN FASTENERS.
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Product Packaging
Product Packaging
JUXIN FASTENERS arranges packaging for custom M6 stainless steel closed-end knurled body blind rivet nuts according to confirmed order quantities, product dimensions, anti-loosening adhesive requirements and automotive OEM customer instructions.
Packaging Configuration
Inner Packaging: Suitable protective bags, trays or containers, as agreed.
Outer Packaging: Cartons according to confirmed shipping requirements.
Pallet Packaging: Subject to order and logistics arrangements.
Custom OEM Packaging: According to approved customer specifications.
Quantity per Package: Confirmed during order processing.
Product Identification
Where required, packaging labels may include:
Product Name: M6 Stainless Steel Closed-End Knurled Body Blind Rivet Nut
Part Number: JX-BF2.5-M6-RX9-19-SS
Thread Size: M6
Material: Stainless Steel
Grip Range: 0.5–2.5 mm
Finish: Natural Stainless Steel
Additional Treatment: Anti-Loosening Adhesive
Lot or Batch Number
Package Quantity
Customer Purchase Order Number
Product Protection
Packaging should protect the limited-height flange, knurled body, internal threads and closed-end barrel against unnecessary damage during storage, handling and transportation.
Where adhesive treatment is present, packaging should also protect the treated surfaces from contamination and damage.
Adhesive Handling and Storage
Any specific temperature limits, storage conditions, shelf-life requirements or handling precautions must follow the approved adhesive specification.
Adhesive-treated parts should be identified and managed according to the confirmed product requirements.
Automotive OEM Packaging and Traceability
For automotive OEM and Tier 1 purchasing programs, packaging and labeling requirements may be agreed according to customer-specific logistics procedures.
Where required, arrangements may include lot identification, barcode labeling, batch segregation, material identification, adhesive-treatment identification and supporting inspection documentation.
Final packaging quantities, carton configurations, labeling formats and shipment arrangements are confirmed before delivery.
Product Pictures
Tags
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY