Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809
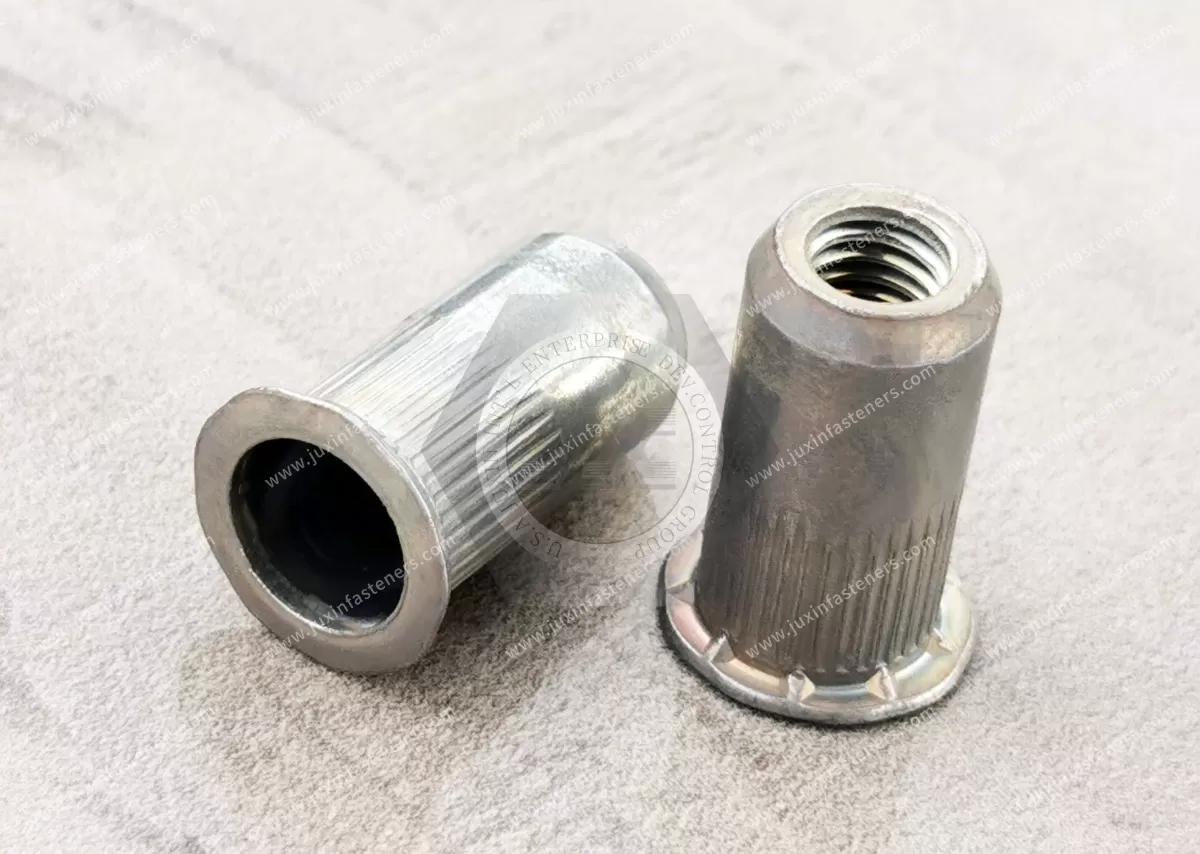
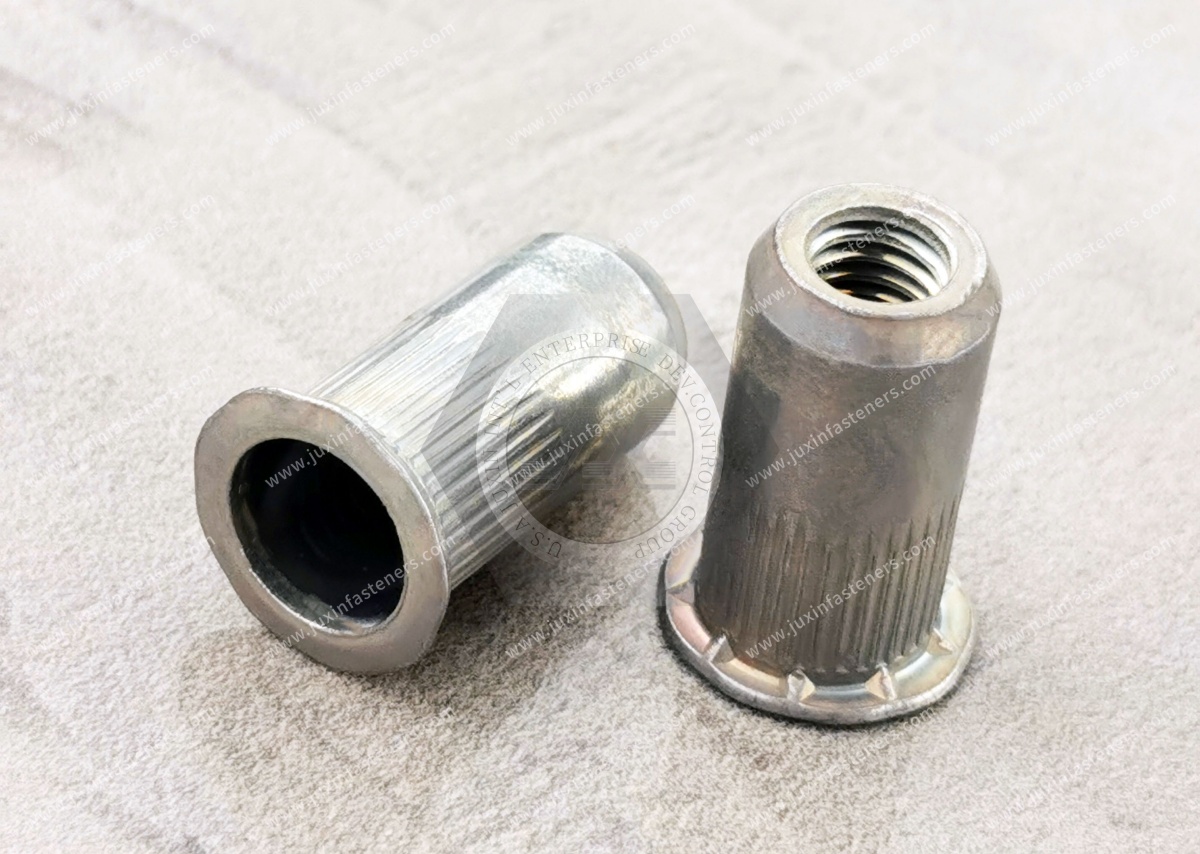
JUXIN FASTENERS supplies custom M6 Thin Head Open-End Knurled Body Blind Rivet Nuts for automotive sheet-metal assemblies. The thin flange reduces front-side projection, while the knurled round body helps resist rotation in a compatible mounting hole.
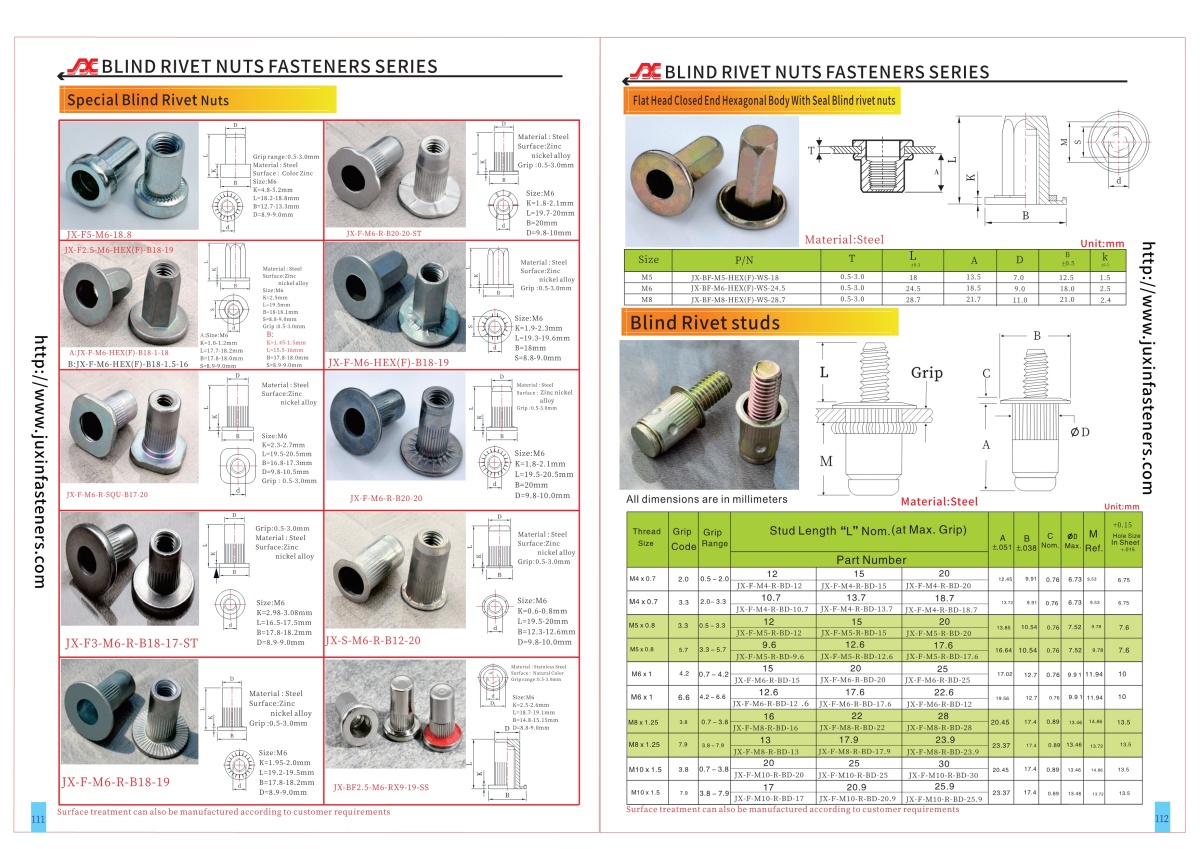
Part No.: JX-1358Q-S-M6-R-B12-20
Thread Size: M6
Material: Steel
Grip Range: 0.5–3.0 mm
Surface Treatment: Zinc-Nickel Alloy
Head Type: Thin Head
Body Type: Knurled Round Body
End Type: Open End
Product Specification
Product Specifications
Product Name: M6 Thin Head Open-End Twist-Resistant Knurled Body Rivet Nuts
Alternative Names: Open-End Twist-Resistant Rivet Nuts; Thin Flange Knurled Blind Rivet Nuts; Low-Profile Head Rivet Nuts
Part Number: JX-1358Q-S-M6-R-B12-20
Product Category: Custom Steel Blind Rivet Nuts
Thread Size: M6
Material: Steel
Head Type: Thin Head / Thin Flange
Body Type: Knurled Round Body
End Configuration: Open End
Grip Range: 0.5–3.0 mm (approximately 0.020–0.118 in)
Surface Treatment: Zinc-Nickel Alloy Plating (Zn-Ni)
Installation Method: One-Sided Blind Installation
Mounting Hole: Compatible Round Hole
Thread Pitch and Tolerance: According to the approved drawing
Flange Thickness and Diameter: According to the approved drawing
Body Dimensions: According to the approved drawing
Mechanical Retention: Subject to application-specific validation
Primary Market: Automotive OEM and Electric Vehicle Assemblies
Product Overview
JUXIN FASTENERS supplies custom M6 thin head open-end knurled body blind rivet nuts for automotive manufacturers, electric vehicle component suppliers, and industrial OEMs requiring threaded fastening points with reduced front-side flange projection.
This special-design rivet nut combines a thin-head flange, knurled round body, open-end threaded barrel, and zinc-nickel alloy surface treatment.
The knurled body is designed to engage the surrounding parent material during installation, helping resist insert rotation when a mating screw is tightened or removed.
The deformable barrel creates backside retention, allowing the insert to be installed from one accessible side of the parent panel.
The thin-head configuration is particularly relevant where flange projection and adjacent-component clearance must be considered.
The product is identified by part number JX-1358Q-S-M6-R-B12-20.
Final dimensions, mounting-hole requirements, installation parameters, and mechanical performance must be verified against the approved drawing.
Thin Head vs. Standard Flat Head Rivet Nuts
The defining feature of this product is its thin-head flange.
A conventional flat-head blind rivet nut typically provides a more pronounced front-side flange profile.
A thin-head design is intended to reduce the flange projection above the parent-panel surface.
This may be useful in automotive assemblies where the rivet nut is positioned beneath another component or where available installation space is limited.
Potential advantages include:
Reduced front-side projection
Improved compatibility with selected close-clearance assemblies
Reduced interference with adjacent components
More flexibility in certain sheet-metal packaging arrangements
However, a thin-head rivet nut should not automatically be considered flush-mounted.
A flush surface requires a specific compatible installation geometry.
Thin-head construction also does not automatically provide the same flange bearing performance as a thicker-head design.
The correct selection depends on flange dimensions, parent-panel material, and joint loading.
Automotive and Electric Vehicle Applications
Automotive OEMs frequently require compact threaded fastening solutions in equipment housings, sheet-metal brackets, and serviceable assemblies.
Thin-head knurled body rivet nuts may be evaluated where front-side projection is an important design consideration.
Potential applications include:
Electric vehicle equipment mounting brackets
Automotive sheet-metal support panels
EV battery system accessory mounting points
Battery management system equipment housings
Automotive electrical equipment enclosures
Electric vehicle power electronics mounting panels
Automotive interior equipment brackets
Vehicle service access panels
Commercial vehicle equipment housings
Thermal management equipment mounting points
Automotive control unit mounting brackets
Selected body equipment supports
These are potential engineering applications rather than confirmed approvals for every vehicle system.
For structural, crash-related, or battery-safety-critical connections, the complete fastening system must be qualified against the relevant OEM requirements.
Why Thin-Head Geometry Matters in Automotive Assembly
Automotive packaging constraints can affect fastener selection as much as thread size.
In some assemblies, the rivet nut flange is located beneath a bracket, cover, or mating component.
Excessive flange projection may affect the intended contact condition or introduce interference.
A thin-head rivet nut can be evaluated as a possible solution where reduced projection is required.
However, engineers must consider the complete joint stack-up.
Important factors include:
Actual flange thickness
Parent-panel thickness
Mating-component geometry
Required contact area
Local panel bearing
Installation-tool clearance
Screw engagement
Joint clamp load
The thin-head design should be selected based on the approved assembly drawing rather than flange appearance alone.
Knurled Round Body and Twist Resistance
The external knurling is designed to engage the surrounding parent material after installation.
This engagement helps resist rotation of the installed rivet nut when a mating screw is tightened or removed.
For automotive assemblies, insert rotation may cause installation problems, loss of serviceability, or difficulty removing a component.
The knurled body addresses this concern through mechanical interaction with the mounting-hole wall.
Actual spin-out performance depends on:
Knurl geometry
Body diameter
Mounting-hole dimensions
Parent-panel material
Material hardness
Panel thickness
Installation deformation
Applied screw torque
A knurled body does not provide unlimited rotational resistance.
The required spin-out torque must be established through representative testing.
Knurled Round Body vs. Full Hex Body
Automotive engineers may compare knurled round-body rivet nuts with full hex body designs.
Knurled Round Body
Uses external knurling to engage the surrounding material in a compatible round hole.
This may be appropriate where round-hole manufacturing is preferred and the required rotational retention can be achieved.
Full Hex Body
Uses flat-sided geometric engagement in a compatible hexagonal mounting hole.
This may be appropriate where the assembly is designed around hexagonal hole preparation and a geometric anti-rotation mechanism.
The selection should consider:
Parent-panel material
Required spin-out resistance
Hole manufacturing process
Installation tooling
Mechanical retention
Assembly cost
Service requirements
These designs should not be treated as interchangeable simply because they use the same M6 thread.
Round-Hole Installation Requirements
The knurled round-body design is intended for installation in a compatible round mounting hole.
The hole may be drilled, punched, or produced using another approved manufacturing process.
For automotive production, hole quality should be controlled for:
Diameter and tolerance
Roundness
Burr condition
Panel thickness
Material hardness
Hole-position accuracy
Surface coating
An oversized hole may reduce rotational retention.
An undersized hole may interfere with installation or damage the insert or parent panel.
The required hole dimensions must be obtained from the approved product drawing.
Standard M6 rivet nut hole dimensions should not be substituted without verification.
Grip Range: 0.5–3.0 mm
The confirmed grip range for this product is 0.5–3.0 mm.
This identifies the parent-material thickness range intended for the specified rivet nut configuration.
The grip range is not the same as overall insert length, flange thickness, or internal thread engagement.
For automotive sheet-metal assemblies, the effective panel thickness must be checked against the approved grip range.
Where multiple layers are involved, engineers should determine the actual material thickness engaged by the insert.
Installation outside the approved grip range may affect backside deformation, axial retention, and rotational resistance.
The stated grip range must not be extended to other product variants without dimensional verification.
M6 Metric Thread and Inch Reference
The confirmed nominal thread size is M6.
M6 has a nominal diameter of 6.0 mm, approximately 0.2362 in.
M6 × 1.0 is a common ISO metric coarse-thread designation, but the actual pitch and tolerance must be confirmed from the approved drawing.
Relevant metric thread references include ISO 261 and ISO 965.
For North American automotive sourcing, M6 must not be substituted with 1/4-20 UNC or 1/4-28 UNF.
These thread forms are not directly interchangeable.
ASME B1.1 may be relevant when comparing Unified inch-thread requirements, but it does not replace the approved metric specification.
The grip range of 0.5–3.0 mm corresponds approximately to 0.020–0.118 in.
These inch values are dimensional references only.
Open-End Design and Screw Engagement
The open-end threaded barrel allows the mating screw to extend through the insert where sufficient backside clearance is available.
This may be useful when coordinating screw length and joint stack-up.
For automotive applications, engineers should verify:
Thread compatibility
Required thread engagement
Screw projection
Backside clearance
Adjacent component interference
Required clamp load
An open-end rivet nut does not provide a sealed threaded connection.
It should not be described as preventing contamination from entering through the open barrel.
Where moisture, dust, or fluid ingress must be controlled, a separate sealing solution may be required.
Zinc-Nickel Alloy Plating for Automotive Applications
The specified surface treatment for this product is zinc-nickel alloy plating.
Zinc-nickel coatings are used in automotive and industrial fastening applications where a defined corrosion-protection system is required.
For OEM sourcing, the coating specification should establish:
Zinc-nickel alloy coating requirements
Alloy composition
Coating thickness
Passivation chemistry
Optional sealing or topcoat
Corrosion-performance requirements
Thread fit after coating
Restricted-substance requirements
Coating inspection criteria
The term "zinc-nickel alloy" does not establish a particular salt-spray rating or service life.
Relevant technical references may include ISO 4042 for electroplated fastener coating systems, ISO 19598 for zinc and zinc-alloy coatings on iron or steel with supplementary treatments, and ISO 9227 or ASTM B117 where specified for corrosion testing.
Customer-specific automotive coating specifications may impose additional requirements.
No particular coating thickness, nickel percentage, corrosion-test duration, or OEM approval is claimed without supporting documentation.
Zinc-Nickel vs. Conventional Zinc Plating
Zinc-nickel and conventional zinc coatings may differ in corrosion behavior, process requirements, and cost.
For automotive procurement, the appropriate comparison should be based on the complete coating specifications rather than coating appearance.
Purchasing teams should review:
Approved coating designation
Coating thickness
Passivation and topcoat
Corrosion-test requirements
Restricted-substance documentation
Compatibility with the parent material
Cost and production requirements
A zinc-nickel plated rivet nut should not be substituted with a conventional zinc-plated version without engineering approval.
Galvanic Corrosion in EV Assemblies
Electric vehicles frequently combine steel fasteners with aluminum alloys and other lightweight materials.
Where dissimilar conductive materials are connected in the presence of moisture or electrolytes, galvanic corrosion may occur.
For zinc-nickel plated steel rivet nuts installed in aluminum panels, engineers should consider:
Parent-panel alloy
Coating system
Mating screw material
Moisture exposure
Electrical contact
Surface protection
Sealing arrangements
Environmental service conditions
The complete joint should be evaluated for the intended operating environment.
Zinc-nickel plating does not automatically eliminate galvanic corrosion risks.
Installation Process for Automotive Production
The rivet nut is installed using compatible blind rivet nut setting equipment.
During installation, the tool applies axial force to deform the designated barrel section behind the parent panel.
This creates the backside retention needed to secure the threaded insert.
For thin-head rivet nuts, installation-tool compatibility and flange seating are particularly important.
Recommended installation checks include:
Correct mounting-hole dimensions
Panel thickness within the approved grip range
Correct mandrel and nosepiece
Tool alignment
Setting force or stroke
Thin flange seating
Backside deformation
Internal thread condition
Axial retention
Spin-out resistance
Under-setting may produce insufficient retention.
Over-setting may damage the insert, distort the parent panel, or affect the internal thread.
Installation parameters must be established using representative production materials.
Thin-Head Flange Seating and Panel Support
Thin-head geometry may influence the way the flange contacts the parent panel.
For automotive assembly design, engineers should evaluate:
Flange thickness
Flange diameter
Parent-panel hardness
Local bearing stress
Surface flatness
Hole-edge condition
Installation deformation
A thinner flange may reduce projection, but it does not automatically provide the same bearing behavior as a thicker flange.
The complete assembly should be evaluated for the intended loading conditions.
Mechanical Retention and Joint Reliability
The mechanical performance of a blind rivet nut depends on the complete installation.
For automotive OEM qualification, engineers should distinguish among:
Pull-out resistance
Push-out resistance
Spin-out torque
Thread stripping resistance
Parent-panel deformation
Joint stiffness
Vibration performance
Pull-out resistance concerns axial extraction of the installed insert.
Push-out resistance concerns displacement in the opposite axial direction.
Spin-out resistance concerns rotation of the installed insert within the mounting hole.
These characteristics are not interchangeable.
No numerical mechanical performance is claimed without product-specific testing.
Vibration and Repeated Assembly
Automotive assemblies may experience vibration, shock, temperature changes, and repeated maintenance operations.
The knurled body helps resist insert rotation within the mounting hole.
It does not independently prevent mating screw loosening.
The complete joint should be evaluated for:
Mating screw properties
Tightening torque
Clamp-load retention
Thread engagement
Joint stiffness
Service vibration
Thermal cycling
Repeated assembly and disassembly
Where required, an appropriate screw-locking strategy should be specified separately.
Automotive OEM Quality and Supplier Qualification
For automotive OEM and Tier 1 sourcing, qualification should address the complete technical specification.
Recommended review items include:
Approved product drawing
Part number identification
M6 thread specification
Thin-head flange dimensions
Knurled body geometry
Mounting-hole dimensions
Grip range
Steel material specification
Zinc-nickel coating specification
Installation parameters
Spin-out performance
Axial retention
Inspection and traceability requirements
Customer-specific automotive programs may require dimensional inspection records, material documentation, coating certificates, first article inspection, PPAP submissions, or additional quality records.
APQP, PPAP, IMDS, and IATF 16949-related requirements should be addressed according to the actual customer program.
No particular certification, PPAP approval, or automotive OEM qualification is implied without supporting evidence.
Automotive Procurement and Total Installed Cost
For purchasing managers, sourcing engineers, and supplier development teams, thin-head knurled rivet nuts should be evaluated using both product cost and assembly cost.
Important considerations include:
Thin-head dimensional consistency
Round-hole preparation
Installation-tool compatibility
Required spin-out resistance
Coating requirements
Inspection procedures
Rework risk
Packaging and traceability
Annual purchasing volume
Delivery planning
A thin-head design may reduce interference in selected assemblies, but it should be compared with alternative flange configurations using the complete assembly drawing.
The lowest unit price does not necessarily provide the lowest total installed cost.
Other Industrial Applications
Beyond automotive manufacturing, thin-head knurled body rivet nuts may be evaluated for suitable industrial applications, including:
Industrial machinery housings
Electrical equipment enclosures
Commercial vehicle equipment
Industrial automation systems
HVAC equipment panels
Fabricated sheet-metal brackets
Maintenance access panels
Equipment covers
Application suitability must be verified against the actual joint requirements.
Related Fastening Solutions
Steel Flat Head Open-End Knurled Body Blind Rivet Nuts
A related configuration with a different flange profile.
Steel High Flat Head Open-End Knurled Body Blind Rivet Nuts
An alternative for applications requiring a more pronounced flange geometry.
Steel Square Flange Knurled Body Blind Rivet Nuts
A custom configuration combining a square flange with a knurled round body.
Steel Flat Head Open-End Full Hexagonal Body Blind Rivet Nuts
An alternative for compatible hexagonal mounting-hole assemblies.
Steel High Flat Head Open-End Partial Hex Body Blind Rivet Nuts
An alternative body geometry for suitable anti-rotation requirements.
Each alternative must be evaluated against the approved drawing and application-specific requirements.
OEM RFQ and Engineering Information
For a technical review and quotation, please provide:
Part Number: JX-1358Q-S-M6-R-B12-20
Approved 2D drawing or 3D CAD model
Required M6 thread specification
Parent-panel material
Panel thickness
Mounting-hole dimensions
Thin-head flange diameter and thickness
Knurled body dimensions
Required grip range
Installation-tool information
Mating screw specifications
Required spin-out torque
Pull-out and push-out requirements
Zinc-nickel coating specification
Corrosion and environmental requirements
Inspection and traceability requirements
Prototype or production quantities
Estimated annual purchasing volume
Delivery destination
Why Source Thin-Head Twist-Resistant Rivet Nuts from JUXIN FASTENERS?
JUXIN FASTENERS supplies industrial fastening products for drawing-based OEM purchasing and engineering requirements.
For automotive customers, technical discussions can focus on thin-head flange geometry, knurled body engagement, mounting-hole compatibility, zinc-nickel coating requirements, installation conditions, and mechanical performance.
JX-1358Q-S-M6-R-B12-20 is identified as an M6 steel thin-head open-end knurled round-body blind rivet nut with zinc-nickel alloy plating and a 0.5–3.0 mm grip range.
Final dimensional details, installation requirements, and mechanical acceptance criteria must be confirmed before production approval.
Request an Automotive OEM Quotation
Looking for M6 open-end twist-resistant rivet nuts, thin-head knurled blind rivet nuts, or zinc-nickel plated automotive threaded inserts?
Send your drawings, technical specifications, and estimated purchasing quantities to JUXIN FASTENERS.
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Product Packaging
Product Packaging
JUXIN FASTENERS arranges packaging for custom M6 steel thin-head knurled body blind rivet nuts according to confirmed purchasing quantities, product dimensions, zinc-nickel coating requirements, and automotive OEM customer instructions.
Packaging Configuration
Inner Packaging: Protective bags or suitable containers, as agreed.
Outer Packaging: Cartons according to confirmed shipping requirements.
Pallet Packaging: Subject to order and logistics arrangements.
Custom OEM Packaging: According to approved customer specifications.
Quantity per Package: Confirmed during order processing.
Product Identification
Where required, packaging labels may include:
Product Name: M6 Thin Head Open-End Knurled Body Blind Rivet Nut
Part Number: JX-1358Q-S-M6-R-B12-20
Thread Size: M6
Material: Steel
Grip Range: 0.5–3.0 mm
Surface Treatment: Zinc-Nickel Alloy
Lot or Batch Number
Package Quantity
Customer Purchase Order Number
Product Protection
Packaging should protect the thin-head flange, knurled round body, internal threads, and zinc-nickel coating against unnecessary damage during handling, storage, and transportation.
Special attention should be given to protecting the thin flange geometry and coated surfaces, as these features are important for drawing-specific automotive assembly requirements.
Automotive OEM Packaging and Traceability
For automotive OEM and Tier 1 purchasing programs, packaging and identification requirements may be agreed according to customer-specific logistics procedures.
Where required, arrangements may include lot traceability, barcode labeling, batch segregation, coating identification, inspection documentation, and customer-specific packaging instructions.
Final packaging quantities, carton configurations, labeling formats, and shipment arrangements are confirmed before delivery.
Product Pictures
Tags
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY