Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809
Electric vehicle battery packs combine electrical, electronic, thermal, structural, and cable-routing systems within a tightly packaged assembly.
Plastic fasteners and engineered polymer hardware can play important roles throughout these systems,
including retaining low-voltage sensing harnesses, supporting BMS electronics, routing selected high-voltage cables,
locating tubing, protecting cable interfaces, spacing components, and securing lightweight covers or auxiliary hardware.
Product Specification
Electric vehicle battery packs combine electrical, electronic, thermal, structural, and cable-routing systems within a tightly packaged assembly.
Plastic fasteners and engineered polymer hardware can play important roles throughout these systems,
including retaining low-voltage sensing harnesses, supporting BMS electronics, routing selected high-voltage cables,
locating tubing, protecting cable interfaces, spacing components, and securing lightweight covers or auxiliary hardware.
The engineering challenge is that there is no single category called an “EV battery plastic fastener” with one universal material or performance requirement.
A plastic push rivet securing a lightweight protective panel, a fir tree clip locating a BMS harness, a P-clip retaining a large cable,
a PCB standoff supporting electronics, and a molded clip locating thermal-management tubing perform very different mechanical functions.
Their environments and failure modes are also different.
Correct selection should therefore begin with the functional zone and assembly requirement, not simply with the assumption that a component is made from nylon.
For EV engineering teams, important selection variables can include:
installation interface
retained component geometry
vibration and road loading
temperature and thermal cycling
moisture
chemical exposure
cable or hose movement
polymer creep and stress relaxation
dimensional stability
electrical-system architecture
flame-performance requirements where specified
assembly sequence
serviceability
automation requirements
vehicle-specific validation
For procurement and supplier-development teams, visually similar automotive plastic clips should not automatically be treated as interchangeable.
Differences in resin grade, locking geometry, panel interface, tolerances, conditioning, insertion behavior, and retention can materially affect assembly performance.
Juxin Fasteners supplies standard and custom plastic and nylon fastening components for industrial and automotive OEM supply chains and can review EV projects using existing manufacturer part numbers,
physical samples, 2D drawings, 3D CAD models, material specifications, assembly information, and estimated production requirements.
Rather than selecting plastic hardware by product family alone, engineers can divide the battery system into functional application zones.
Typical zones may include:
battery module and sensing-wire routing
BMS electronics and control hardware
low-voltage harness routing
selected high-voltage cable management
thermal-management tubing
battery enclosure auxiliary hardware
internal partitions and protective covers
power electronics and electrical distribution assemblies
Each zone creates a different combination of mechanical, thermal, electrical, and environmental requirements.
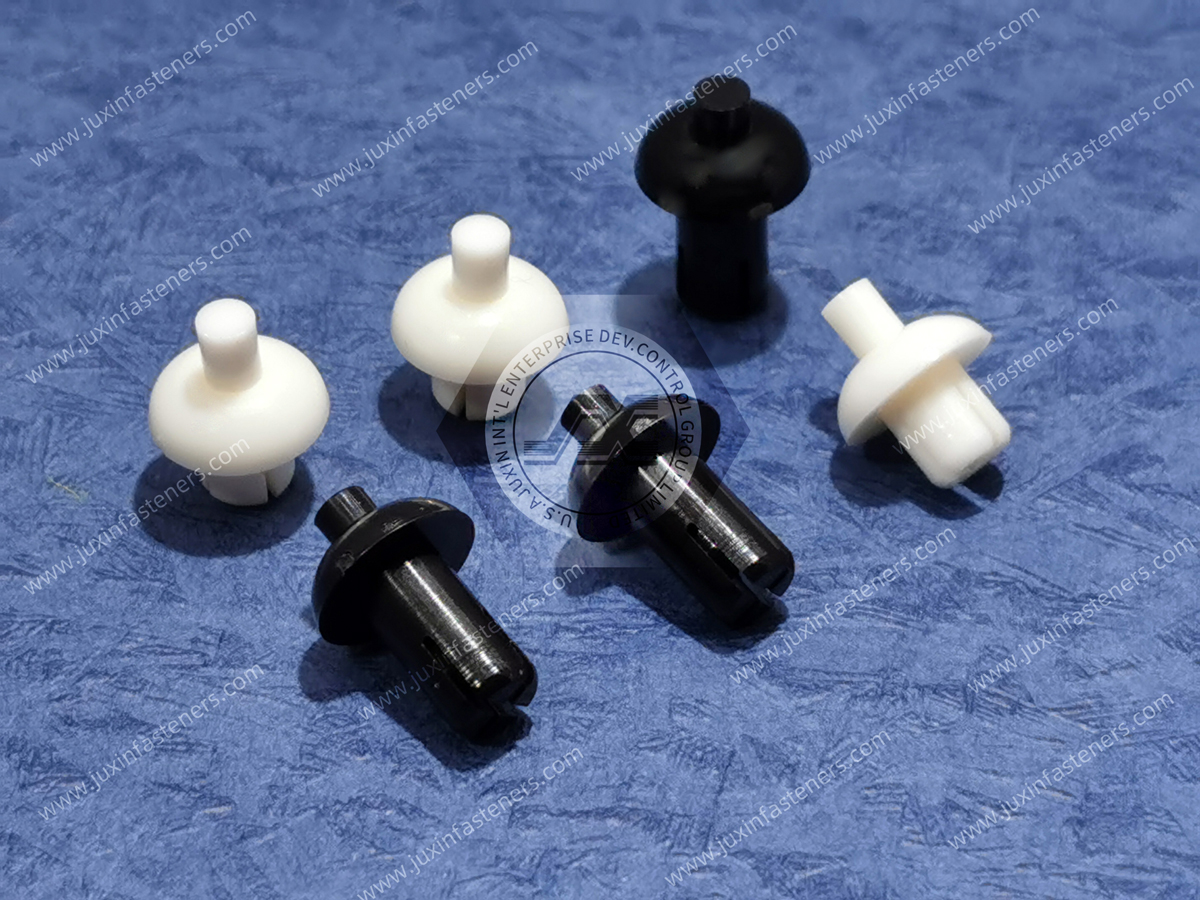
Battery modules can contain voltage-sensing wires, temperature-sensor leads, balancing circuits, communication wiring, and other low-voltage electrical connections.
Depending on the battery architecture, routing hardware may include:
nylon cable clips
small harness retainers
fir tree fasteners
push-in clips
cable tie mounts
low-profile molded retainers
application-specific plastic clips
The primary engineering objective is usually not maximum retention force.
The objective is controlled routing.
A suitable component should help maintain harness position without creating unacceptable compression, abrasion, sharp bending, or interference with neighboring components.
A useful failure path is:
Vehicle Vibration → Harness Movement → Relative Contact → Repeated Friction → Jacket Wear → Potential Electrical Reliability Risk
The clip therefore works as part of a complete routing system.
Engineers should consider:
clip spacing
harness weight
harness flexibility
connector locations
branch points
nearby edges
cable bend geometry
expected vibration
installation tolerance
A stronger clip cannot compensate for fundamentally poor harness routing.
Battery management systems contain electronics that may require controlled mechanical support inside an enclosure.
Depending on the design, plastic hardware may include:
PCB standoffs
snap-fit PCB supports
plastic spacers
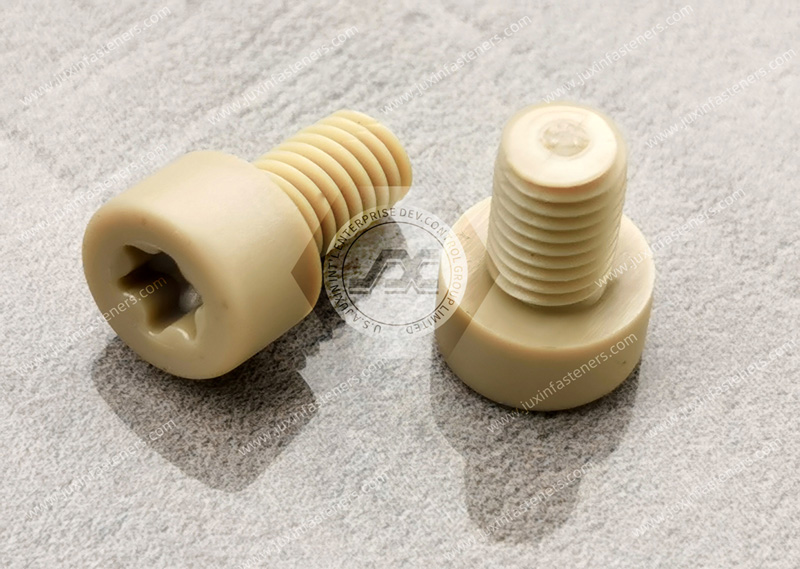
nylon machine screws
plastic washers
card supports
molded insulating components
These components can provide mechanical spacing and, where appropriate, a non-metallic interface between components.
However, mechanical spacing must not be confused with electrical creepage or clearance.
A plastic standoff height does not automatically establish a compliant electrical insulation distance.
System-level electrical requirements must be evaluated according to:
operating voltage
applicable equipment requirements
material properties
geometry
contamination conditions
surrounding conductive structures
complete insulation architecture
Plastic PCB hardware can contribute to the mechanical and electrical architecture, but it should not be presented as independently establishing high-voltage safety compliance.
High-voltage EV cables can introduce different mechanical requirements from small BMS wiring.
Depending on cable construction and system architecture, routing hardware may include:
plastic P-clips
cable clamps
heavy-duty harness retainers
fir tree mounting clips
cable tie mounts
custom molded cable supports
The correct clamp should be selected according to the actual cable and environment.
Important variables can include:
cable outside diameter
cable OD tolerance
cable stiffness
jacket material
jacket compressibility
cable mass
bend path
vibration
support spacing
mounting interface
temperature
surrounding clearance
A nominal cable diameter alone is not sufficient to qualify a cable clamp.
Large electrical cables may have relatively complex jacket and insulation constructions.
An undersized clamp can create excessive local compression.
An oversized clamp may permit relative motion.
Both conditions can create problems.
The engineering target is therefore not maximum clamping force. It is appropriate positional control without unacceptable cable damage.
Engineers should inspect:
contact area
internal edge geometry
molding flash
local pressure points
cable movement
surrounding metal edges
Cable jacket protection should be treated as a functional design requirement.
EV battery systems can use liquid cooling and other thermal-management architectures.
Plastic clips and retainers may be used to position selected:
flexible coolant hoses
small tubing
sensor lines
auxiliary thermal-management components
The component must be matched to the actual tube or hose construction.
Selection variables can include:
tube OD
tube tolerance
tube material
flexibility
allowable compression
thermal expansion
fluid environment
temperature
vibration
required movement
A retaining clip should not pinch a flexible fluid path or impose an unsuitable local bending condition.
Battery systems combine materials with different coefficients of thermal expansion, potentially including:
aluminum
steel
copper
engineering polymers
cable jackets
elastomers
composite materials
Thermal cycling can therefore create relative movement between components.
A plastic clip should not unintentionally over-constrain a cable or tube that requires limited movement during temperature change.
This is particularly important along longer routing paths and around fixed connection points.
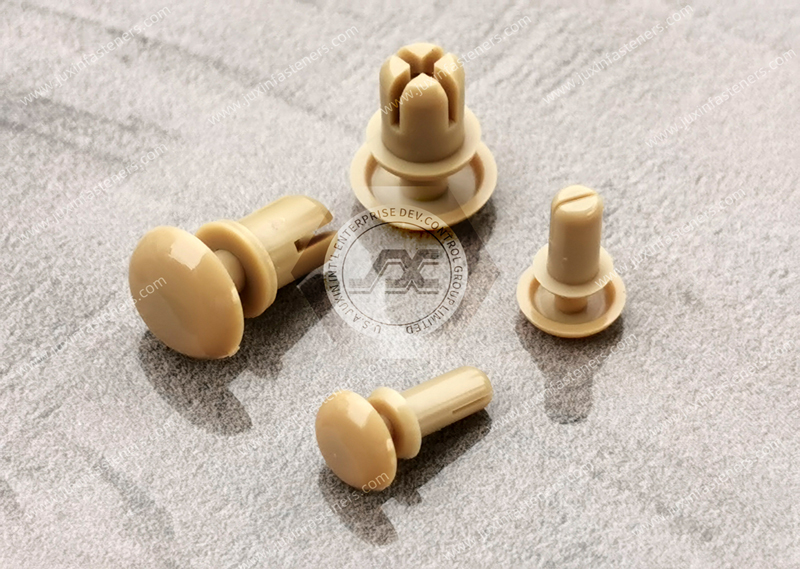
Plastic push rivets, snap fasteners, fir tree clips, and related retainers may be used for selected lightweight components such as:
covers
shields
routing features
insulation-related components
non-structural panels
auxiliary brackets or trim features where appropriate
These components should not be confused with structural battery-pack fasteners.
Primary load-bearing battery enclosure joints, crash-critical connections, structural module attachments,
and other safety-critical structural joints require fastening systems designed and validated for those specific loads.
Plastic fasteners should be selected only where their actual mechanical role is appropriate.
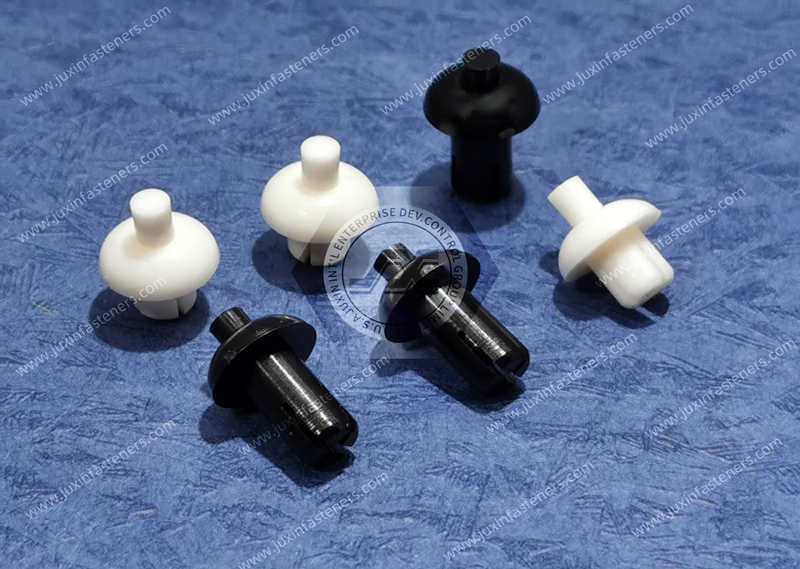
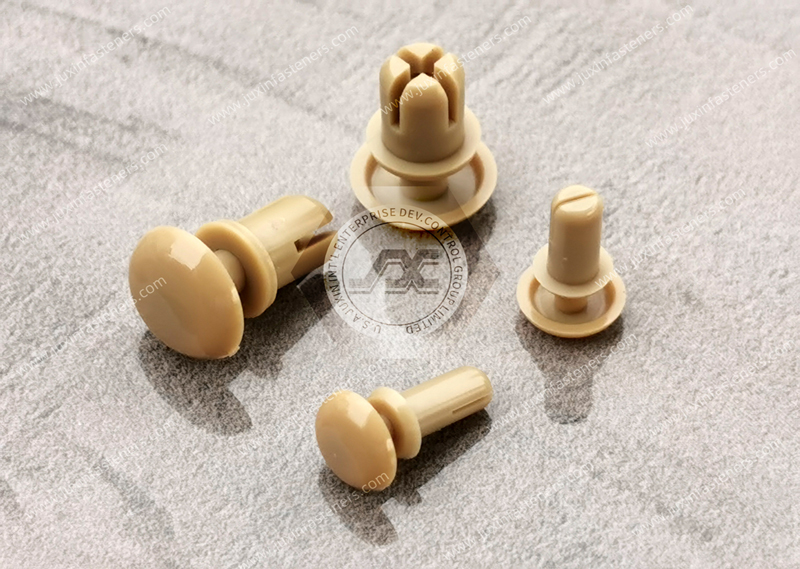
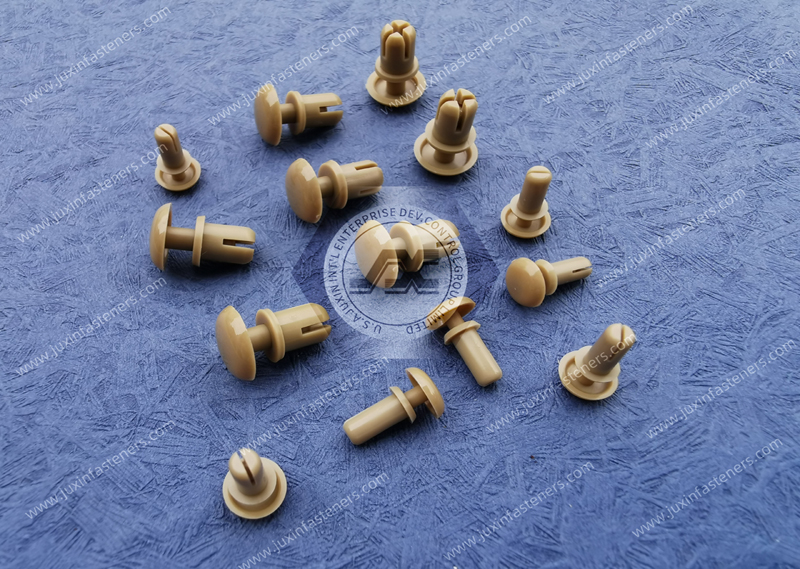
Push rivets can provide fast, tool-efficient attachment for selected lightweight components.
Selection should consider:
mounting-hole diameter
hole tolerance
total stack thickness
grip condition
substrate material
burr condition
insertion force
retention force
vibration
removal requirements
polymer grade
temperature
moisture
Two push rivets that look similar may have different expansion behavior and retention characteristics.
Visual similarity is not evidence of interchangeability.
Fir tree clips use flexible barbed features that engage a mounting hole.
They are commonly associated with automotive harness and trim attachment, but the correct component depends on the mating interface.
Engineers should evaluate:
hole diameter
hole tolerance
panel thickness
panel material
barb geometry
stem length
insertion force
extraction resistance
vibration
removal requirement
A clip developed for one sheet-metal hole condition may not perform identically in a different hole, plastic substrate, or composite panel.
P-clips and screw-mount cable clamps create a defined attachment point between a cable or harness and a supporting structure.
They may be useful where engineers require controlled routing and a mechanically secured mounting location.
Important selection variables include:
bundle diameter
bundle compressibility
cable jacket sensitivity
loop geometry
mounting-hole size
mounting screw
clamp-foot geometry
installation condition
vibration
polymer creep
thermal environment
For high-voltage cable applications, the complete electrical architecture must still be evaluated independently.
Cable tie mounts provide an attachment interface for a separate cable tie.
Depending on the design, mounts may use:
push-in panel attachment
screw mounting
molded snap features
other mechanical interfaces
The mount, cable tie, harness, and panel form a combined retention system.
Engineers should therefore avoid evaluating the mount independently of the tie and harness load.
There is no universal “EV-grade nylon.”
Material selection should follow the actual application.
Possible engineering polymers may include PA6, PA66, or other materials depending on the component and requirements.
Specialized resin formulations may include, where specified:
heat-stabilized grades
impact-modified grades
UV-stabilized grades
flame-retardant grades
reinforced materials
other application-specific engineered polymers
Not every product is available or appropriate in every polymer.
The exact resin grade should be selected according to the required mechanical, thermal, environmental, electrical, manufacturing, and documentation requirements.
Heat-stabilized PA6 or PA66 grades may be considered where elevated-temperature exposure justifies them.
Potential application areas can include components near:
power electronics
inverter systems
battery thermal zones
electrical distribution hardware
However, “heat stabilized” is not a universal temperature rating.
Actual suitability depends on:
resin grade
exposure temperature
duration
mechanical stress
moisture
component geometry
required service performance
Temperature capability should therefore be validated from the actual material specification and application.
Some clip applications can experience shock or high local deformation during assembly or service.
Impact-modified resin formulations may be considered where appropriate.
However, modifying one material property can affect others.
Material selection should consider the complete performance balance rather than optimizing a single characteristic.
Some battery, electrical, and power-electronics applications may specify flame-performance requirements.
Where a UL 94 classification such as V-0 or V-2 is required, the classification must be associated with the actual resin grade and relevant tested conditions.
A generic PA66 designation does not establish a UL 94 classification.
Similarly, using a resin with a documented UL 94 classification does not by itself establish compliance of the complete EV battery system with vehicle-level fire-safety requirements.
The component requirement and supporting material documentation should be defined according to the customer's specification.
PA6 and PA66 are hygroscopic polymers.
They absorb moisture from their environment.
Moisture conditioning can affect:
dimensions
stiffness
toughness
strength
insertion force
retention
snap-fit behavior
cable clamping behavior
creep
stress relaxation
This matters particularly for snap-fit automotive hardware because a component may be assembled under one conditioning state and operate under another.
Dry-as-molded properties should not automatically be used as the sole basis for long-term retention predictions.
The expected environmental condition should be considered where moisture sensitivity is relevant to the design.
A common design assumption is that a component inside a battery enclosure experiences no moisture because the pack is described as sealed.
Actual internal environmental conditions depend on the pack architecture, sealing strategy, assembly conditions,
service environment, pressure equalization, condensation risk, and other system factors.
Therefore, polymer conditioning requirements should be based on the actual battery-system environment rather than the word “sealed” alone.
Plastic fasteners and cable retainers can remain under sustained deformation for long periods.
Engineering polymers exhibit time-dependent mechanical behavior.
Depending on material and conditions, this may include:
creep
stress relaxation
dimensional change
reduction in contact pressure
The significance depends on:
resin grade
temperature
moisture
geometry
initial deformation
retained component
vibration
service duration
This is particularly relevant for:
P-clips
cable clamps
snap-fit retainers
PCB supports
tubing clips
continuously loaded fasteners
Initial retention should therefore not automatically be treated as long-term retention.
EV battery assemblies can experience vibration and mechanical shock originating from:
road inputs
suspension and body motion
drivetrain systems
cooling equipment
structural response
component-specific excitation
The actual vibration environment depends on the vehicle and component location.
A generic statement that an EV fastener is “vibration resistant” is therefore insufficient.
Engineers should evaluate the relevant failure mode.
For example:
Push Rivet: Does it loosen or disengage from the mounting hole?
Fir Tree Clip: Do the barbs maintain engagement with the substrate?
P-Clip: Does the cable move inside the loop?
Cable Clip: Does repeated deflection fatigue the latch or hinge?
PCB Support: Does board movement create excessive stress at support locations?
The correct test depends on the component function.
Thermal cycling affects the complete assembly.
Different materials expand and contract differently.
This means that thermal cycling can change:
clip preload
cable position
tube position
panel interface
snap engagement
contact pressure
dimensional fit
Engineers should therefore evaluate the fastener as part of the assembled system rather than testing only the free component.
Many engineering polymers are electrically insulating.
This can be useful when designers want a non-metallic interface around electrical wiring or between selected components.
However, a plastic clip does not automatically:
prevent all short circuits
establish required creepage distance
establish required clearance distance
provide a defined dielectric withstand rating
certify a high-voltage system
satisfy insulation coordination requirements
These are system-level electrical engineering requirements.
They depend on the actual polymer grade, geometry, voltage, contamination environment, surrounding structures, and applicable standards.
Plastic fasteners can contribute to the architecture but should not be treated as standalone high-voltage safety devices.
A non-metallic component can eliminate direct metal-to-metal contact at its own interface, which may be useful in assemblies containing dissimilar metals.
However, using a plastic clip does not automatically eliminate galvanic-corrosion risk throughout the complete assembly.
Moisture, conductive paths, adjacent metallic components, coatings, and overall joint architecture still matter.
Galvanic-corrosion control should therefore be evaluated at system level.
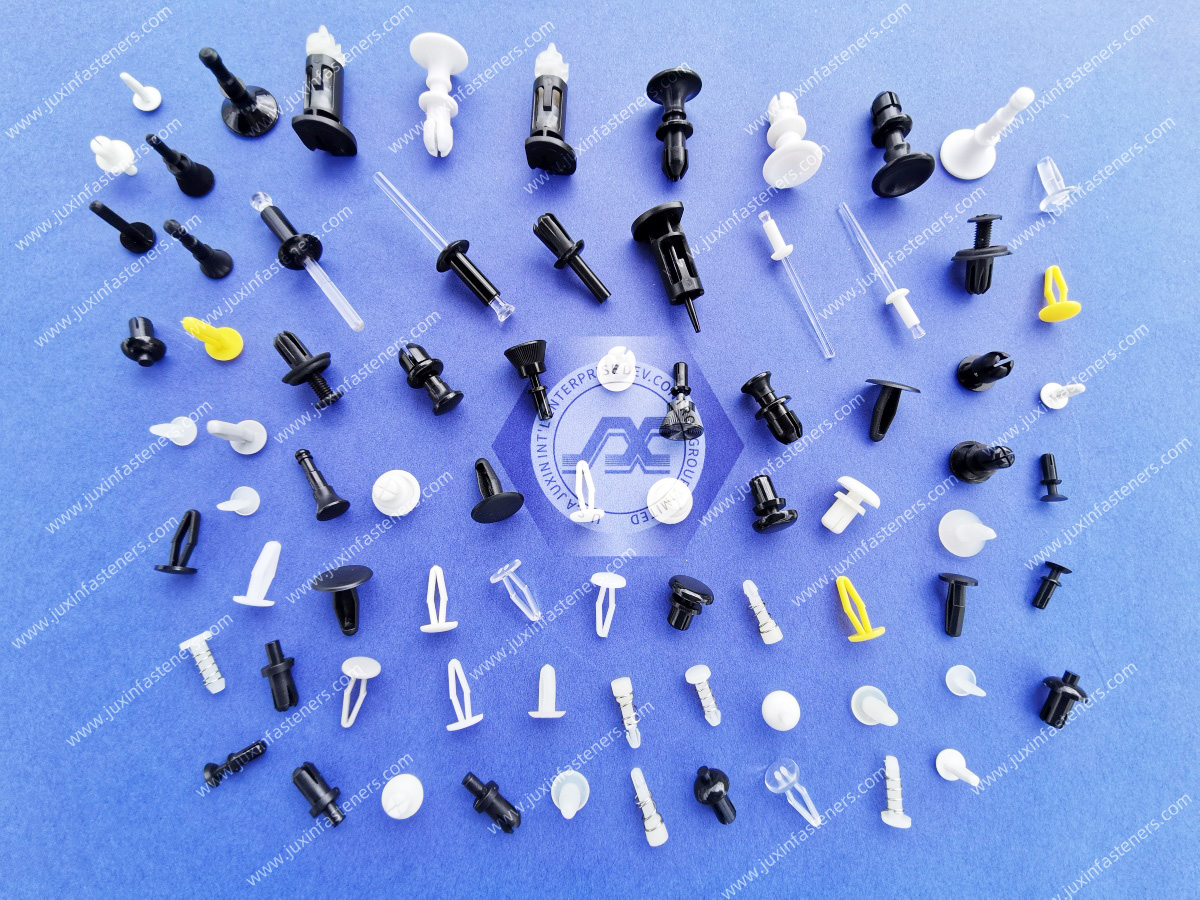
Automotive fasteners must work not only in the finished vehicle but also on the assembly line.
Important manufacturing considerations can include:
insertion direction
access
insertion force
operator ergonomics
tactile or visual confirmation
poka-yoke features
orientation
component feeding
robotic handling
installation speed
risk of incomplete engagement
A component with excellent retention but difficult installation can create manufacturing problems.
Conversely, very low insertion force may indicate insufficient engagement in some designs.
The objective is an appropriate insertion-to-retention balance for the actual assembly.
Where automated installation is planned, engineers may also need to consider:
part presentation
orientation stability
gripper access
end-effector geometry
dimensional consistency
installation force window
engagement detection
Automation compatibility is therefore a component-and-process requirement rather than an inherent property of “plastic fasteners.”
Not every EV plastic fastener should be designed as permanently non-removable.
Some assemblies require:
battery service
electronics replacement
harness repair
inspection
module access
Engineers should decide whether the component must be:
single-use
removable
reusable
replaceable during service
This decision can materially influence clip geometry and sourcing requirements.
A useful way to select a component is to begin with the failure that must be prevented.
Potential consequences can include:
harness movement
abrasion
connector loading
interference with nearby components
Potential consequences can include:
cable displacement
jacket wear
unintended bending
loss of routing control
Potential consequences can include:
tube movement
local compression
contact with surrounding structures
routing instability
Potential consequences can include:
board movement
PCB bow
connector stress
local mechanical loading
Potential consequences can include:
panel loosening
rattle
loss of auxiliary component retention
This failure-mode approach helps engineers identify what must actually be validated.
A practical first-pass selection logic can be summarized as follows:
| EV Application Zone | Possible Plastic Hardware | Key Engineering Questions |
|---|---|---|
| BMS sensing harness | Cable clips, fir tree clips, cable tie mounts | Harness OD, hole interface, vibration, chafing, serviceability |
| BMS electronics | PCB supports, standoffs, spacers, nylon screws | Board thickness, mounting interface, PCB bow, temperature, electrical architecture |
| HV cable routing | P-clips, cable clamps, custom retainers | Cable OD, jacket sensitivity, cable mass, vibration, mounting interface |
| Thermal-management tubing | Tube clips, custom retainers | Tube OD, allowable compression, temperature, expansion, fluid environment |
| Lightweight covers | Push rivets, snap fasteners | Hole size, stack thickness, retention, removal |
| Internal cable pass-through | Snap bushings, panel protectors | Panel hole, panel thickness, cable OD, edge protection |
| External cable entry where applicable | Strain relief hardware | Cable geometry, panel cutout, pull/push/twist requirements |
This table is a selection starting point, not a substitute for application-specific engineering validation.
Instead of asking:
“Which plastic fastener is suitable for an EV battery?”
use this sequence:
Functional Zone → Failure Mode → Environment → Mating Interface → Retained Component → Material → Fastener Geometry → Installation → Validation
Where is the component located?
What happens if retention is inadequate?
What temperature, moisture, vibration, chemicals, and other exposures exist?
Is the fastener engaging:
sheet metal
aluminum
molded plastic
PCB
bracket
another substrate?
Is it holding:
cable
harness
hose
PCB
cover
shield
auxiliary hardware?
Which resin properties are actually required?
What hole, thickness, grip, loop, latch, or mounting dimensions control installation?
Will the component be manually installed, tool-assisted, or automated?
What assembly-level testing is required by the OEM or Tier-1?
This approach creates a more reliable design and sourcing process than selecting by product name or material alone.
“PA66 clip” does not define geometry, resin grade, stabilization, conditioning, or performance.
Two clips that look identical may have different retention behavior.
Hole tolerance, panel thickness, substrate, and barb geometry also affect performance.
Two high-voltage cables with the same OD can have different stiffness and compressibility.
Actual environmental conditions must be evaluated.
Material flammability classification and complete vehicle-system compliance are different issues.
Electrical safety requires system-level design and validation.
Creep, stress relaxation, thermal cycling, and moisture can affect long-term behavior.
These distinctions are especially important during second-source qualification.
EV sourcing teams often inherit existing components from established vehicle or Tier-1 designs.
The commercial objective may be:
second sourcing
localization
cost evaluation
supply-chain risk reduction
capacity expansion
replacement of an obsolete component
new vehicle platform development
In each case, the technical baseline must be established before a candidate replacement can be qualified.
For an existing EV component, useful starting information includes:
existing manufacturer
manufacturer part number
OEM or Tier-1 internal part number
physical sample
2D drawing
3D CAD model
material specification
mating interface
retained component
application location
A candidate should be treated as a cross-reference candidate, not automatically as a fully interchangeable equivalent.
Automotive plastic clips often contain functional geometry that is difficult to communicate with only a few catalog dimensions.
Examples include:
barb profiles
flexible hinges
latch geometry
undercuts
lead-in angles
local wall thickness
retention shoulders
anti-rotation features
A physical sample combined with a drawing and application information can therefore significantly improve second-source evaluation.
A clip should ideally be evaluated with the actual or representative:
mounting hole
panel thickness
substrate material
cable
harness
tube
PCB
mating component
Testing only the loose plastic part cannot reproduce the actual fastening system.
Relevant evaluation may include, depending on the component:
insertion behavior
retention
extraction behavior
cable fit
tube compression
vibration
thermal cycling
environmental conditioning
assembly ergonomics
service removal
Test requirements should come from the actual customer or vehicle program rather than universal assumptions.
A structured pathway can follow:
Existing Part → Application Review → Dimensional Review → Material Review → Mating Interface Review
→ Candidate Cross-Reference → Sample → Assembly Validation → Supplier Qualification → Production RFQ
This sequence is especially useful for procurement and supplier-development teams because it separates finding a similar component from qualifying a production replacement.
Those are not the same task.
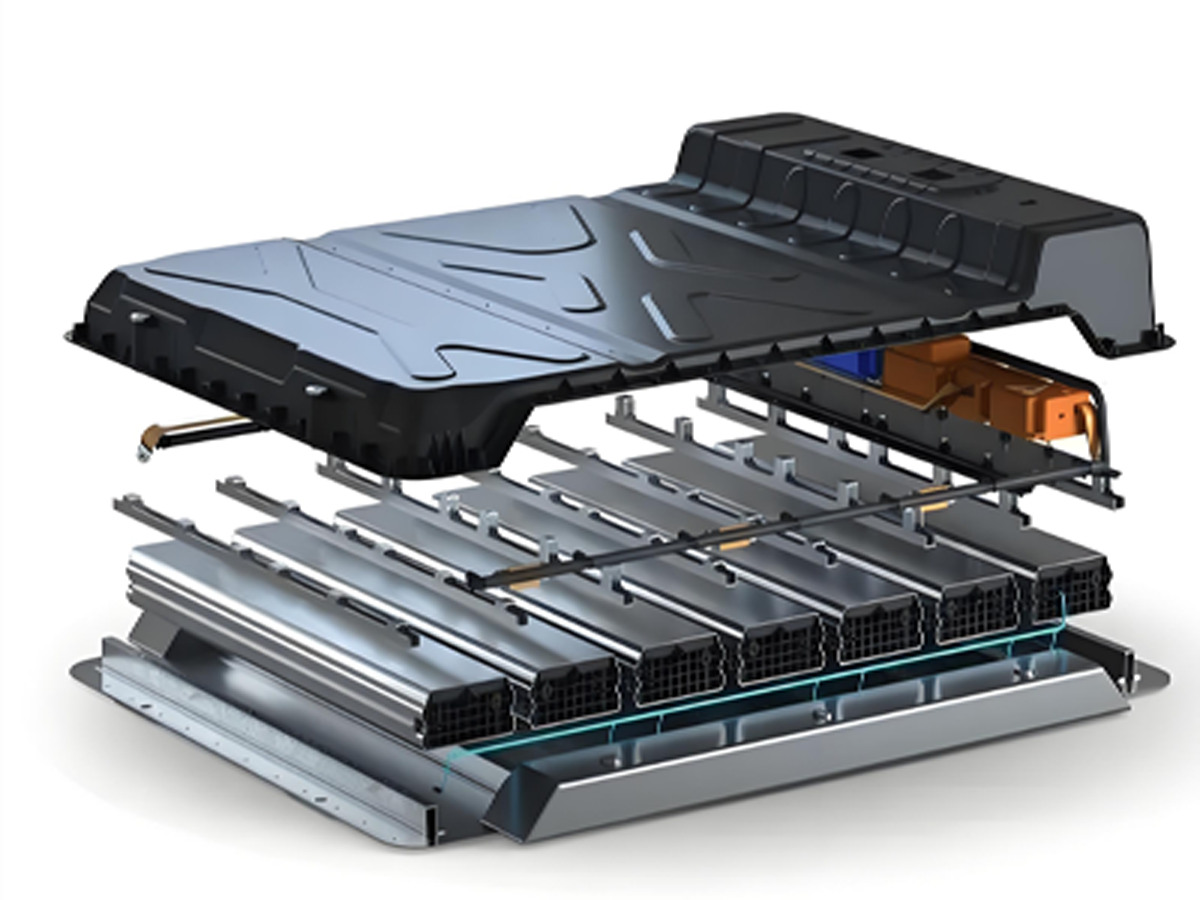
Standard catalog components may not fit every battery-pack architecture.
Custom molded components may be appropriate where a project requires:
unique mounting geometry
restricted packaging space
special cable or tube routing
multiple integrated retention features
special resin requirements
custom anti-rotation features
non-standard panel interfaces
application-specific installation geometry
Juxin Fasteners can review drawing-based plastic fastener projects using customer-provided:
2D drawings
3D CAD models
physical samples
material requirements
mating-component information
application conditions
expected purchasing volumes
A custom-development pathway can follow:
Application Requirement → Interface & Environment Review → Material & Geometry Review → Manufacturability Review
→ Sample / Prototype → Assembly Validation → Customer Qualification → Production
Automotive procurement and supplier-quality teams may require documentation beyond dimensional inspection.
Depending on the customer and project, requirements may include:
material identification
resin specification
dimensional inspection requirements
lot identification
traceability
environmental compliance declarations
customer-specific documentation
packaging requirements
automotive material reporting information
Where IMDS data, RoHS, REACH, material reports, flammability information, or other documentation is required, it should be explicitly stated during the RFQ and confirmed for the specific product.
These requirements should not be assumed to apply automatically to every component.
For efficient technical and commercial evaluation, provide as much of the following information as available:
existing manufacturer
existing part number
OEM or Tier-1 internal part number
physical sample
2D drawing
3D CAD model
application zone
component function
mating substrate
mounting-hole diameter
hole tolerance
panel thickness
stack thickness where relevant
cable or harness OD
cable construction where relevant
hose or tubing OD
PCB thickness where relevant
required grip or retention condition
material or resin grade
color
operating-temperature requirements
thermal-cycling requirements
moisture exposure
chemical exposure
vibration requirements
UV exposure where relevant
flame-performance requirement where applicable
electrical requirements where applicable
installation method
automated assembly requirement where applicable
removal or reuse requirement
required validation
required documentation
sample quantity
production quantity
estimated annual volume
packaging requirements
Providing both the component and its actual mating interface is particularly valuable for second-source projects.
For a new EV application:
Functional Requirement → Application Zone → Environment & Failure Mode → Interface Definition → Material & Geometry Selection
→ Candidate Component → Sample → Assembly Validation → Production RFQ
For an existing production component:
Existing Part / Physical Sample → Application & Interface Review → Dimensional & Material Review → Candidate Cross-Reference
→ Sample → Vehicle or Assembly Validation → Second-Source Qualification → Production RFQ
For a custom component:
2D/3D Drawing + Application Requirements → Engineering Review → Material & Manufacturability Review → Sample / Prototype → Customer Validation → Qualification → Production
This creates a direct technical-commercial path for EV OEMs, Tier-1 suppliers, battery manufacturers, supplier-development teams, and strategic sourcing organizations.
Juxin Fasteners supplies standard and custom plastic and nylon fastening components for industrial and automotive OEM applications,
including push rivets, fir tree fasteners, cable clips, P-clips, cable clamps, PCB hardware, spacers, standoffs, snap bushings, strain relief components, and custom molded plastic fasteners.
Engineering and sourcing teams can submit an existing manufacturer part number, competitor part number, physical sample, 2D drawing,
3D CAD model, mating-component information, material requirement, application conditions, and estimated production volume for evaluation.
For second-source EV projects, the objective is not simply to find a component that resembles the existing part.
The objective is to identify a technically appropriate candidate that can be evaluated against the actual interface, environment, installation process, and failure mode before customer qualification.
For new EV platforms, defining the functional zone, mating interface, retained component, environment, material requirements, assembly method,
and validation criteria early in the project creates a more efficient path from engineering review to sampling, qualification, and production sourcing.
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Product Packaging
Packaging Standard
At Juxin Fasteners, we apply standardized export packaging to ensure product protection, traceability, and compliance with international logistics requirements.
1. Standard Export Packaging
Unless otherwise specified, all products will be packed according to our factory standard export packaging, which includes:
Moisture-resistant inner protection
Poly bag or small box packing as required
Reinforced export cartons
Clear labeling with part number, specification, batch number, and quantity
Palletizing for sea or air shipment when necessary
Our standard packaging is designed to ensure safe transportation, efficient warehousing, and long-distance international shipping.
2. Customized Packaging Options
We also provide customized packaging solutions according to customer requirements, including but not limited to:
Private labeling
Customized barcodes
Specific carton dimensions
Retail packaging
Special pallet configuration
Customer-specific marking and identification
So that you know, customized packaging may involve additional costs and extended lead time depending on the complexity of the requirements.
3. Compliance & Quality Assurance
All packaging processes are controlled under our ISO 9001 quality management system to ensure consistency, traceability, and product integrity throughout the supply chain.
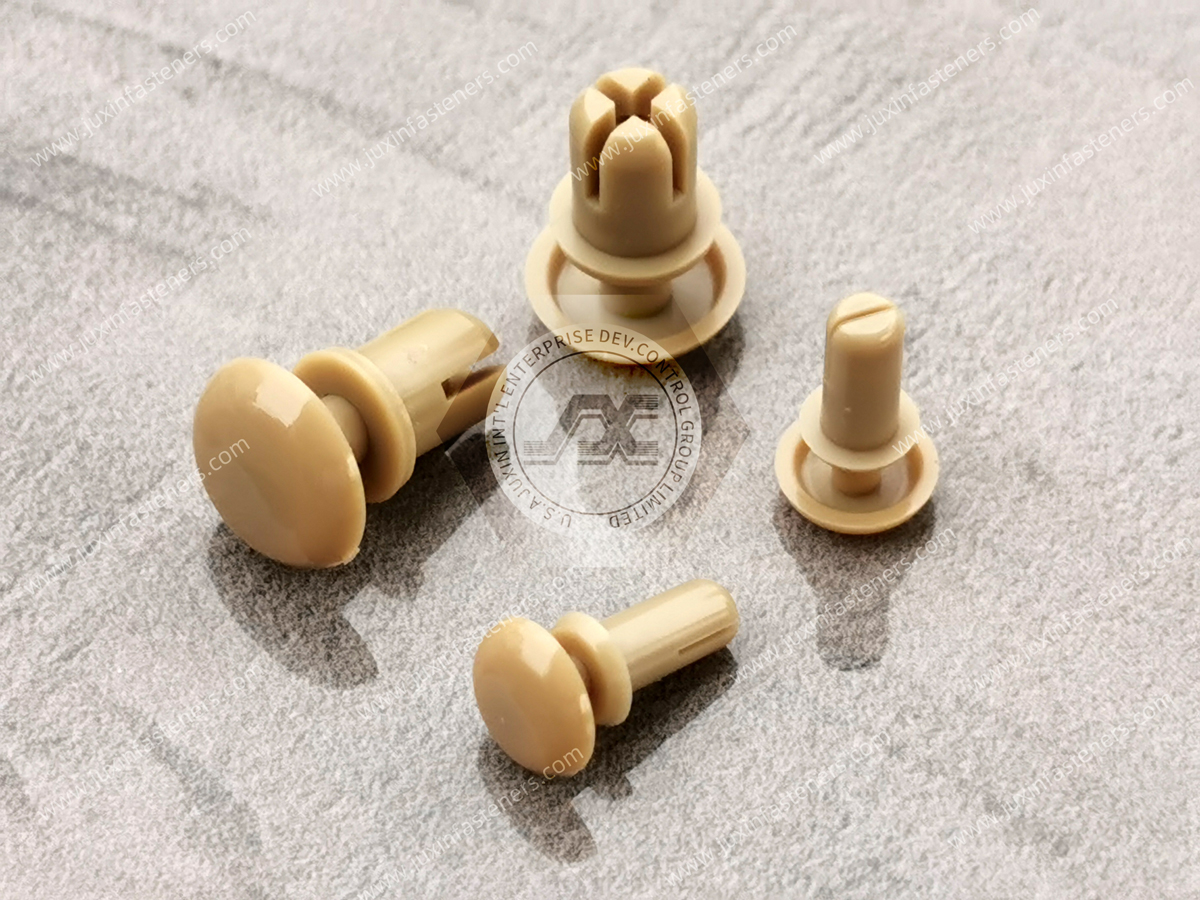
Product Pictures
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY