Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

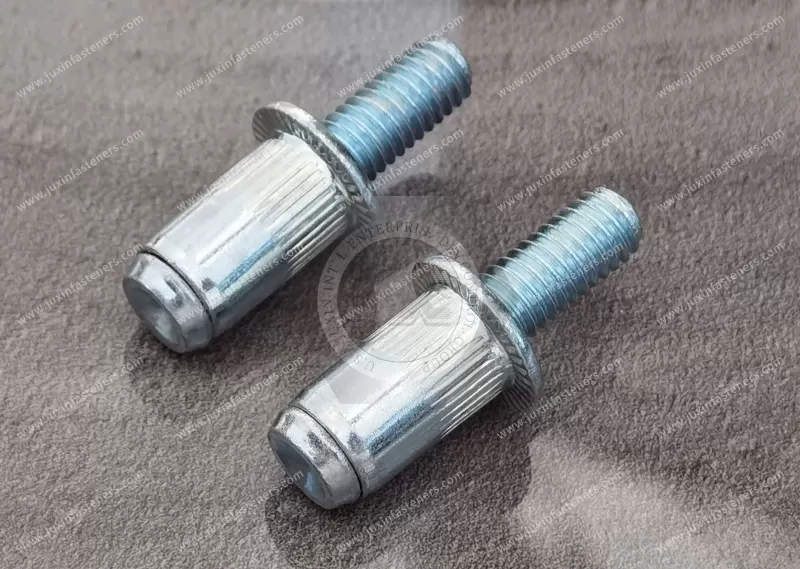
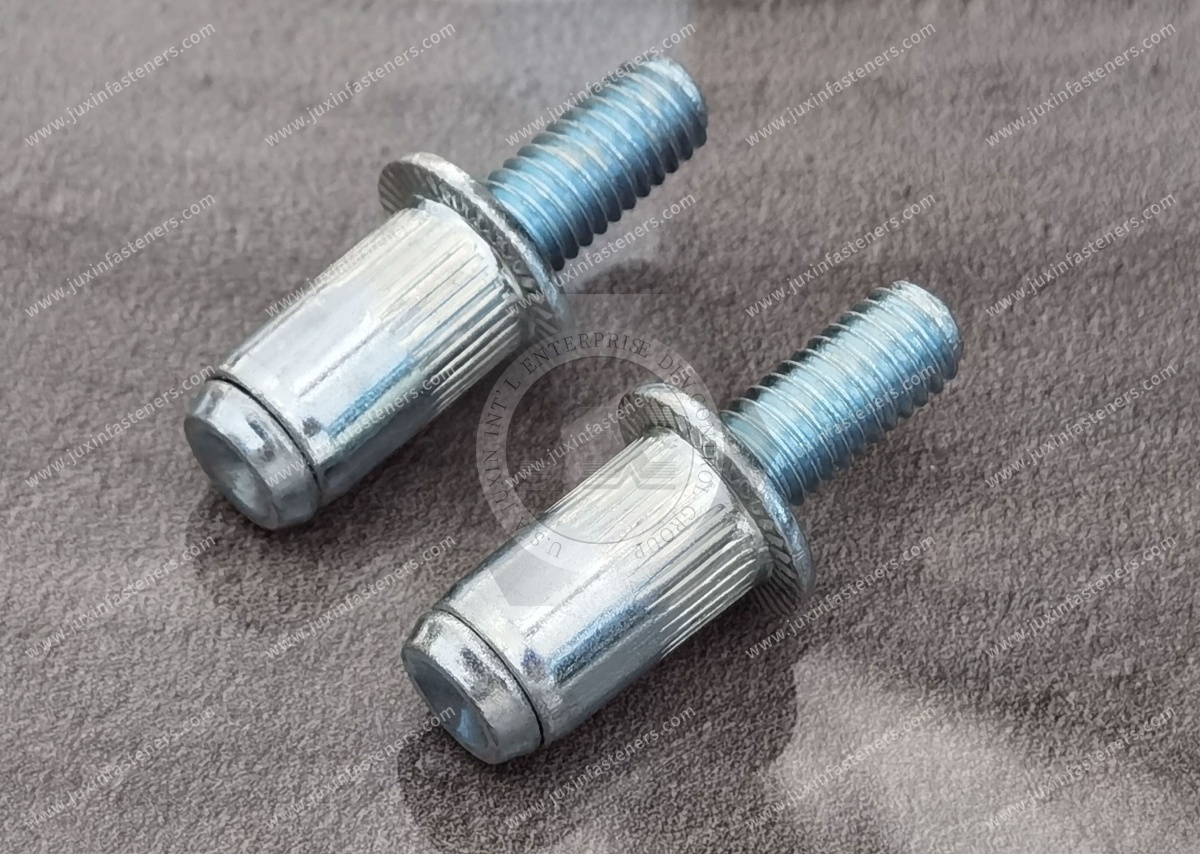
JUXIN FASTENERS supplies M5, M6 and M8 steel flat head knurled blind rivet studs for automotive and industrial sheet-metal assemblies.
These externally threaded fasteners use one-sided mechanical blind riveting, with a knurled body that helps resist rotation. Color zinc and RoHS blue zinc finishes are specified options.
Thread Sizes: M5, M6, M8
Material: Steel
Surface Treatments: Color Zinc / RoHS Blue Zinc
Grip Range: 0.5–5.5 mm (product family)
Head Type: Flat Head
Body Type: Knurled
Thread Configuration: External Metric Thread
Installation: Mechanical Blind Riveting
Product Specification
Product Specifications
Product Name: M5–M8 Flat Head Knurled Blind Rivet Studs
Product Type: Mechanically Installed External Threaded Rivet Studs
Alternative Names: Rivet-Type Studs; Knurled Blind Rivet Studs; Blind Threaded Studs; Flat Head Rivet Studs
Thread Sizes: M5, M6, M8
Material: Steel
Surface Treatment Options: Color Zinc or RoHS Blue Zinc
Head Design: Flat Head
Body Design: Knurled Riveting Body
Thread Configuration: External Metric Thread
Grip Range: 0.5–5.5 mm (approximately 0.020–0.217 in), product family
Installation: One-Sided Mechanical Blind Riveting
Stud Length: According to the approved drawing
Mounting-Hole Dimensions: According to the approved drawing
Mechanical Retention: Subject to product-specific testing
Primary Markets: Automotive OEM, Industrial Equipment, Sheet-Metal Fabrication and Electric Vehicle Equipment
Product Overview
JUXIN FASTENERS supplies M5, M6 and M8 steel flat head knurled blind rivet studs for automotive and industrial OEM assemblies requiring externally threaded mounting points.
These products are mechanically installed from one accessible side of the parent panel. A compatible setting tool deforms the designated rivet body section, creating retention without requiring access to the opposite side.
The knurled body helps resist rotation when a mating nut is tightened or removed.
This product family has a stated grip range of 0.5–5.5 mm and offers two specified surface-treatment options: Color Zinc and RoHS Blue Zinc.
The actual coating specification, stud length, mounting-hole dimensions and mechanical performance must be confirmed against the approved drawing and purchasing requirements.
The Engineering Value of a Blind Rivet Stud
A blind rivet stud creates an external threaded mounting point in a panel that may not provide sufficient thickness for a conventional tapped thread.
Unlike a blind rivet nut, which provides an internal threaded connection, a blind rivet stud leaves a threaded shaft projecting from the panel.
The mating component is typically secured using a compatible nut.
This configuration may be useful when:
A removable component requires an external threaded mounting point.
The panel is accessible from only one side.
The assembly contains a closed sheet-metal section.
The design requires mechanical riveting rather than thermal joining.
A mounting bracket or accessory must be positioned on a fixed stud.
The correct choice depends on the complete joint geometry and loading requirements.
Mechanical Blind Riveting: Installation Principle
These products are mechanically riveted studs.
They are not welded studs.
Installation involves controlled deformation of the designated rivet body section using compatible setting equipment.
A typical process includes:
Prepare the mounting hole according to the approved drawing.
Confirm the parent-panel thickness.
Insert the rivet stud into the hole.
Engage the stud with compatible installation tooling.
Apply the specified setting force or stroke.
Form the retaining section behind the parent panel.
Verify head seating, external thread condition and mechanical retention.
The actual setting process must match the approved product configuration.
A standard blind rivet nut tool should not automatically be assumed compatible with every blind rivet stud.
The assembly must provide sufficient clearance for the retaining feature formed during installation.
Why Knurled Body Geometry Matters
The knurled body is intended to provide mechanical engagement with the surrounding parent material after installation.
This helps resist rotation when the mating nut is tightened or removed.
Rotational retention is especially important in assemblies where the rear side of the panel cannot be accessed after installation.
If the installed stud rotates, tightening or servicing the mating nut may become difficult.
Actual performance depends on:
Knurl geometry
Rivet body diameter
Mounting-hole tolerance
Parent-material strength
Panel thickness
Installation deformation
Applied tightening torque
A knurled body does not guarantee a particular spin-out torque.
The required rotational resistance must be verified through testing with representative panels.
Knurling also does not independently prevent the mating nut from loosening under vibration.
Flat Head and Panel Seating
The flat head provides a contact surface on the accessible side of the parent panel.
Head dimensions influence local bearing pressure, installation alignment and available assembly clearance.
Engineers should verify:
Head diameter
Head thickness
Mounting-hole geometry
Panel flatness
Adjacent component clearance
Installed head seating
The flat head should not automatically be described as countersunk or flush-mounted.
Actual head projection must follow the approved drawing.
M5, M6 and M8 Thread Selection
The specified nominal metric thread sizes are M5, M6 and M8.
Common ISO metric coarse-thread references include:
M5 × 0.8
M6 × 1.0
M8 × 1.25
These are reference pitches only.
Actual thread pitch and tolerance must be confirmed from the approved product drawing.
Relevant thread references include ISO 261 and ISO 965.
For North American engineering and sourcing teams:
M5: 5.0 mm / approximately 0.1969 in
M6: 6.0 mm / approximately 0.2362 in
M8: 8.0 mm / approximately 0.3150 in
These are nominal diameter conversions, not interchangeable inch-thread specifications.
UNC and UNF threads defined under ASME B1.1 are not direct substitutes for ISO metric threads.
Any inch-thread variant requires separate product and supply confirmation.
Grip Range: 0.5–5.5 mm
The specified grip range for this product family is 0.5–5.5 mm, equivalent to approximately 0.020–0.217 in.
Grip range refers to the thickness of parent material that the riveted section is intended to retain.
It is different from external stud length and threaded engagement length.
The family grip range does not establish that every M5, M6 and M8 variant covers the full 0.5–5.5 mm range.
For engineering approval, confirm:
Actual panel thickness
Approved grip range for the selected variant
Required installation stroke
Backside deformation clearance
Head seating
Axial retention
Installing a stud outside its approved grip range may affect retention or damage the parent material.
Stud Projection and Assembly Stack-Up
The external threaded portion must provide sufficient length for the mating component and nut.
Stud projection should be selected according to:
Mounted component thickness
Washer thickness, if used
Mating nut height
Required thread engagement
Installation clearance
Joint loading
Service requirements
An excessively short stud may provide insufficient thread engagement.
An excessively long stud may interfere with nearby components.
The external stud length and grip range must therefore be specified independently.
Color Zinc vs. RoHS Blue Zinc: Coating Selection
This product family offers two specified finish options:
Color Zinc
RoHS Blue Zinc
These are commercial finish descriptions, not complete coating specifications.
Color Zinc is commonly used to describe zinc-plated components with a colored passivation appearance.
Blue Zinc generally refers to a zinc-plated surface with a blue or clear appearance.
However, visible color does not establish coating thickness, corrosion performance, passivation chemistry or regulatory compliance.
For OEM purchasing, each finish should be controlled through an approved coating specification.
Important requirements include:
Zinc coating system
Coating thickness
Passivation chemistry
Appearance requirements
Sealant or topcoat, if applicable
Corrosion-test criteria
Restricted-substance requirements
Thread fit after coating
Coating inspection and documentation
ISO 4042 is a relevant reference for electroplated fastener coating systems.
Where required, ISO 9227 or ASTM B117 may be used for specified salt-spray testing.
No specific coating thickness or corrosion-test duration is claimed without supporting documentation.
RoHS Blue Zinc and Compliance Documentation
The designation "RoHS Blue Zinc" is retained as a specified product finish.
However, a blue zinc appearance does not independently demonstrate compliance with restricted-substance requirements.
For relevant electrical and electronic equipment applications, RoHS-related documentation should be assessed according to the applicable regulatory scope and customer requirements.
Supporting documents may include:
Coating supplier declarations
Material declarations
Restricted-substance test reports
Customer-specific compliance records
The actual passivation chemistry should be verified.
Formal compliance claims must be supported by appropriate documentation.
Choosing Between the Two Finish Options
The correct coating should be selected according to the approved OEM specification rather than appearance alone.
For a purchasing comparison, confirm:
Whether the customer drawing specifies a particular finish.
Whether coating thickness is controlled.
Whether a particular passivation system is required.
Whether restricted-substance documentation is necessary.
Whether corrosion testing is specified.
Whether the coating affects thread fit or installation.
Whether the selected finish is approved for the intended environment.
Two studs with identical geometry but different zinc finishes should not automatically be treated as approved substitutes.
A finish change may require customer approval or additional validation.
Corrosion Protection in Automotive Assemblies
Automotive equipment may experience moisture, road spray, temperature changes and other environmental conditions.
For zinc-plated steel blind rivet studs, the complete assembly should be assessed for:
Coating durability
Parent-material compatibility
Contact with dissimilar metals
Installation damage
Mating nut material
Service environment
Long-term maintenance conditions
Where steel studs are installed in aluminum panels, galvanic corrosion should be considered.
A suitable coating or isolation strategy may be necessary according to the complete joint design.
Salt-spray test results should not be treated as direct predictions of service life.
Material Properties and Electroplating Risk
The confirmed base material is steel.
The actual steel grade, hardness and mechanical properties must follow the approved specification.
For electroplated steel fasteners, hydrogen embrittlement risk should be evaluated according to material strength, hardness and processing conditions.
ISO 4042 provides requirements and recommendations relevant to electroplated fastener systems and hydrogen embrittlement risk management.
No particular baking procedure or hydrogen embrittlement qualification is claimed without supporting process documentation.
Automotive and Electric Vehicle Applications
M5, M6 and M8 blind rivet studs may be evaluated for selected automotive equipment assemblies requiring external threaded mounting points.
Potential applications include:
Automotive electrical equipment brackets
Vehicle interior equipment mounting
Electric vehicle accessory supports
Power electronics equipment brackets
Thermal management equipment supports
Wiring and cable support brackets
Vehicle access panels
Commercial vehicle equipment housings
These are potential applications rather than confirmed approvals for every vehicle system.
Suitability depends on parent-panel material, installation geometry, mechanical loads and environmental exposure.
Safety-critical, structural and high-voltage battery applications require separate engineering qualification.
Other Industrial Applications
Beyond automotive manufacturing, these rivet studs may be evaluated for:
Industrial machinery
Electrical equipment enclosures
HVAC equipment panels
Industrial automation
Sheet-metal fabrication
Material handling equipment
Equipment mounting brackets
Removable access panels
The key engineering requirement is an externally threaded mounting point that can be installed from one accessible side.
Application suitability must be confirmed through the approved design.
Installation Quality and Process Validation
For production assembly, repeatable installation is essential.
Recommended process checks include:
Correct product identification
Mounting-hole diameter
Parent-panel thickness
Tool compatibility
Installation force or stroke
Head seating
Backside retaining-feature formation
External thread condition
Axial retention
Rotational retention
Under-setting may produce insufficient retention.
Over-setting may damage the stud, parent panel or external thread.
Production parameters should be established through representative installation trials.
Mechanical Retention and Joint Reliability
Relevant mechanical evaluations may include:
Pull-out resistance
Push-out resistance
Spin-out torque
External thread stripping
Parent-panel deformation
Repeated assembly behavior
Vibration performance
These characteristics must be evaluated separately.
A stud with acceptable axial retention may still require additional rotational testing.
A knurled body also does not independently prevent loosening of the mating nut.
Where vibration is significant, the complete joint should be evaluated for tightening torque, clamp-load retention, thread engagement and the appropriate nut-locking method.
No numerical mechanical ratings are claimed without product-specific testing.
OEM Replacement-Part and Alternative-Supplier Evaluation
When an automotive OEM or Tier 1 supplier evaluates an alternative rivet stud supplier, matching the thread diameter is not sufficient.
A replacement stud must be reviewed for:
Drawing revision
Thread pitch and tolerance
External stud length
Head geometry
Knurled body dimensions
Grip range
Mounting-hole compatibility
Installation-tool compatibility
Setting force or stroke
Axial retention
Spin-out torque
Coating specification
Traceability requirements
Two rivet studs may look similar but behave differently during installation.
Even a small change in body geometry can affect the formed retaining feature.
Likewise, a coating change may affect dimensional fit, corrosion requirements or customer approval status.
A replacement should therefore be qualified against the complete assembly requirements.
Automotive OEM and Tier 1 Quality Requirements
For automotive OEM and Tier 1 purchasing, the product should be controlled through an approved technical specification.
Customer-specific programs may require:
Approved engineering drawings
Dimensional inspection
Material documentation
Coating documentation
Installation validation
Mechanical testing
First article inspection
Lot traceability
PPAP submissions or other customer-defined approval records
APQP, PPAP, IMDS and IATF 16949-related requirements should be addressed according to the actual customer program.
No particular certification, OEM approval or PPAP status is implied without supporting evidence.
OEM Procurement and Total Installed Cost
For purchasing managers and supplier development teams, the complete installed fastening system should be considered.
Relevant commercial factors include:
Unit price
Mounting-hole preparation
Setting equipment
Assembly cycle time
Inspection
Installation defects
Rework risk
Coating requirements
Packaging
Inventory management
Delivery planning
A lower purchase price does not necessarily result in a lower total installed cost.
The correct rivet stud should satisfy the engineering requirements while supporting a repeatable production process.
Related Fastening Solutions and Internal Linking
Flat Head Knurled Blind Rivet Studs – M5, M6, M8, Color Zinc
A related product page focused on the specified color zinc finish and 0.5–5.5 mm family grip range.
Flat Head Knurled Blind Rivet Studs – M4 to M10
A related product family with a broader thread-size selection and a different stated family grip range.
RoHS Blue Zinc Knurled Blind Rivet Studs – M4 to M10
A related product family focused on blue zinc coating requirements.
Knurled Body Blind Rivet Nuts
An alternative for assemblies requiring an internal threaded connection rather than an external stud.
Full Hex Body Blind Rivet Nuts
A related blind-installed internally threaded fastener using geometric anti-rotation engagement.
Custom Double-Flange Rivet Nuts
A drawing-specific internally threaded fastening component for special mounting requirements.
Internal links should point to the corresponding verified JUXIN FASTENERS product pages using descriptive anchor text.
These product configurations should not be treated as directly interchangeable without engineering approval.
Frequently Asked Engineering and Purchasing Questions
What is the difference between a blind rivet stud and a blind rivet nut?
A blind rivet stud provides an external threaded mounting point. A blind rivet nut provides an internal threaded connection.
Does installation require welding?
No. These studs are installed by mechanical blind riveting using compatible setting equipment.
Can M5, M6 and M8 studs be installed from one side?
Yes. The products are intended for one-sided mechanical installation, subject to the approved mounting-hole geometry, grip range and tool requirements.
Does the knurled body prevent rotation?
The knurled body helps resist rotation. Actual spin-out torque must be verified through testing.
Do all three sizes cover 0.5–5.5 mm?
Not necessarily. The stated grip range applies to the product family. Each size and variant must be checked against its approved drawing.
Are Color Zinc and RoHS Blue Zinc interchangeable?
Not automatically. Coating chemistry, thickness, corrosion requirements and customer approvals must be reviewed before substitution.
Does a blue zinc appearance prove RoHS compliance?
No. Compliance requires appropriate material and coating documentation.
OEM RFQ Requirements
For technical review and quotation, please provide:
Approved 2D drawing or 3D CAD model
Required thread size: M5, M6 or M8
Thread pitch and tolerance
External stud length
Steel material grade
Parent-panel material
Panel thickness
Mounting-hole dimensions
Flat-head dimensions
Knurled body dimensions
Required grip range
Required finish: Color Zinc or RoHS Blue Zinc
Coating thickness and passivation requirements
Restricted-substance documentation requirements
Installation-tool information
Mating nut specifications
Required pull-out resistance
Required spin-out torque
Corrosion and environmental requirements
Inspection and traceability requirements
Prototype or production quantities
Estimated annual purchasing volume
Delivery destination
Why Source M5–M8 Blind Rivet Studs from JUXIN FASTENERS?
JUXIN FASTENERS supplies industrial fastening products for drawing-based OEM purchasing and engineering requirements.
For automotive customers, technical discussions can focus on external stud geometry, one-sided mechanical riveting, knurled body engagement, grip-range compatibility, coating selection and mechanical retention.
This product family includes M5, M6 and M8 steel flat-head knurled blind rivet studs with a stated 0.5–5.5 mm family grip range and Color Zinc or RoHS Blue Zinc finish options.
Final dimensions, coating documentation, installation parameters and mechanical acceptance criteria must be confirmed before production approval.
Request an OEM Quotation
Looking for M5, M6 or M8 blind rivet studs with specified zinc finishes for automotive sheet metal or industrial equipment?
Send your engineering drawings, coating requirements, technical specifications and estimated purchasing quantities to JUXIN FASTENERS.
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Product Packaging
Product Packaging
JUXIN FASTENERS arranges packaging for M5, M6 and M8 steel flat head knurled blind rivet studs according to confirmed order quantities, product dimensions, selected zinc finish and OEM customer instructions.
Packaging Configuration
Inner Packaging: Suitable protective bags, trays or containers, as agreed.
Outer Packaging: Cartons according to confirmed shipping requirements.
Pallet Packaging: Subject to order and logistics arrangements.
Custom OEM Packaging: According to approved customer specifications.
Quantity per Package: Confirmed during order processing.
Product Identification
Where required, packaging labels may include:
Product Name: Steel Flat Head Knurled Blind Rivet Stud
Thread Size: M5, M6 or M8
Material: Steel
Surface Treatment: Color Zinc or RoHS Blue Zinc, as ordered
Grip Range: According to the approved size-specific drawing
Customer or Supplier Part Number
Drawing Revision
Lot or Batch Number
Package Quantity
Customer Purchase Order Number
Product Protection
Packaging should protect the external threads, flat head, knurled body and zinc coating against unnecessary damage during handling, storage and transportation.
Different coating variants should be identified and segregated according to the approved order and traceability requirements.
Automotive OEM Packaging and Traceability
For automotive OEM and Tier 1 purchasing programs, packaging and identification requirements may be agreed according to customer-specific logistics procedures.
Where required, arrangements may include lot traceability, barcode labeling, coating identification, batch segregation and supporting inspection documentation.
Final packaging quantities, carton configurations, labeling formats and shipment arrangements are confirmed before delivery.
For OEM packaging requirements and quotations:
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Product Pictures
Tags
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY