Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

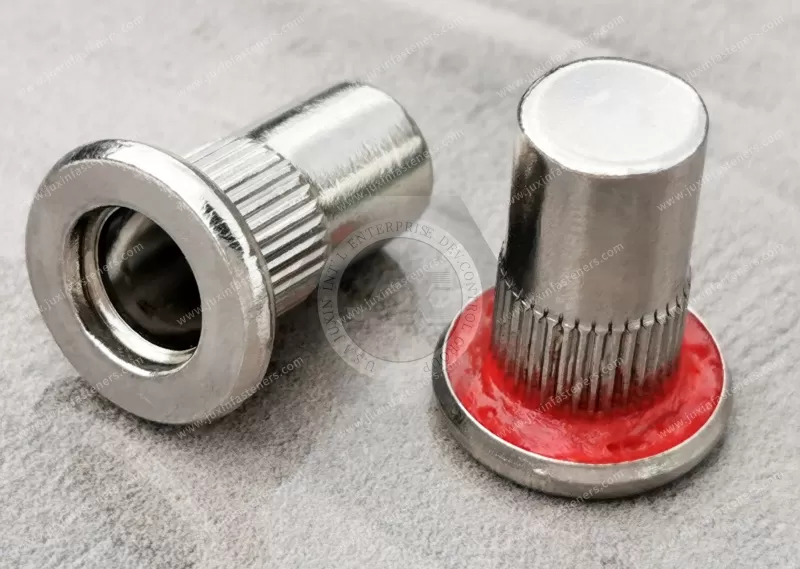
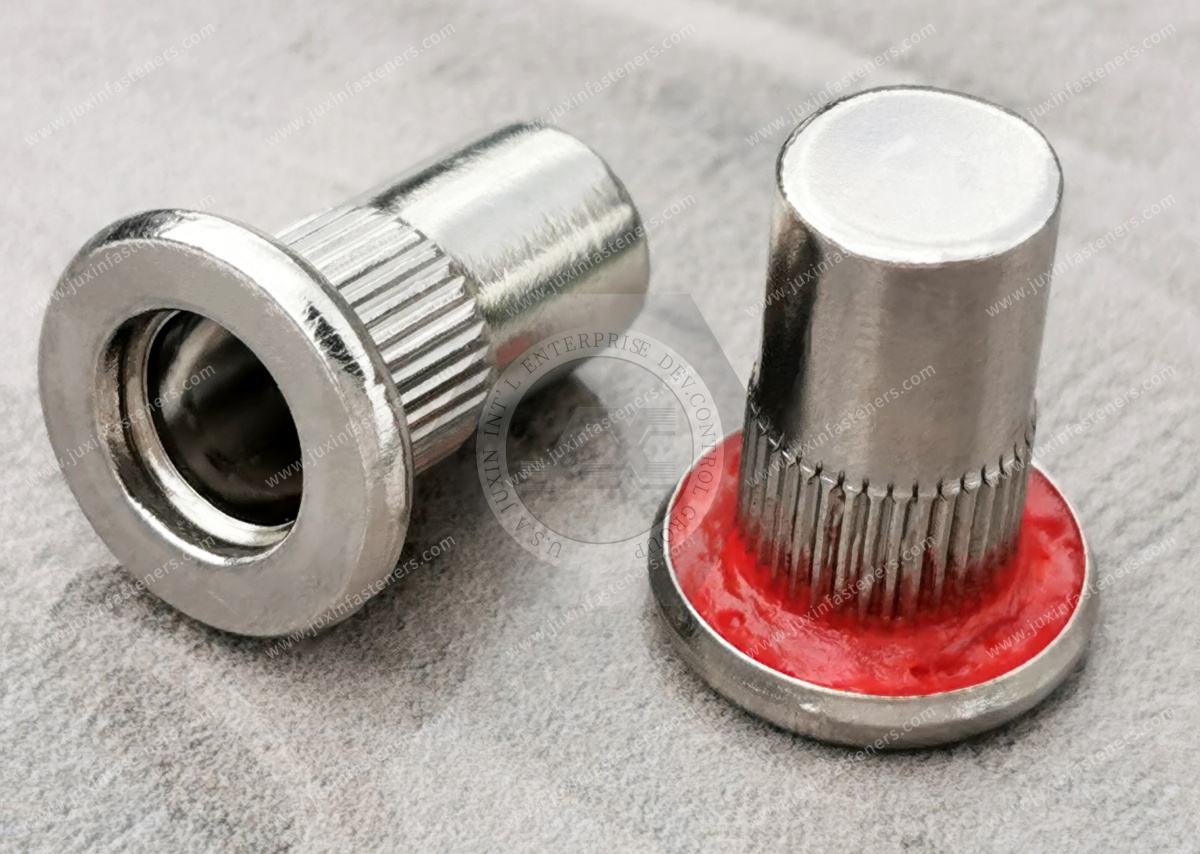
JUXIN FASTENERS supplies M6 stainless steel high flat head closed-end knurled blind rivet nuts with a red pre-applied anti-loosening compound for drawing-specific OEM assemblies.
This version combines a raised flange, knurled round body, closed-end barrel, and an additional red compound visible near the flange. The compound's precise function, application location, and performance requirements should be confirmed against the approved engineering specification.
Product Features
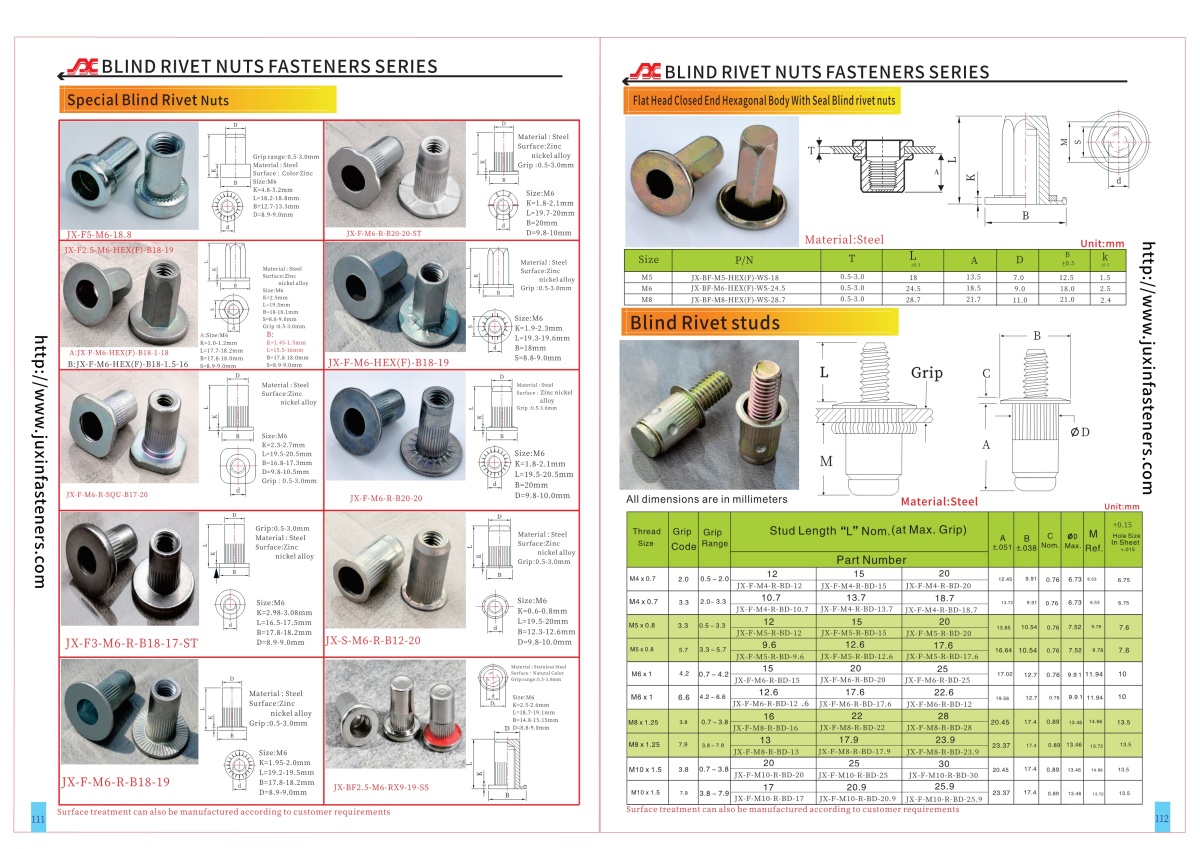
Part No.: JX-BF2.5-M6-RX9-19-SS
Thread: M6
Material: Stainless steel
Finish: Natural stainless steel
Grip range: 0.5–3.0 mm (approx. 0.020–0.118 in)
Head: High flat head / Raised flange
Body: Knurled round body
End: Closed end
Additional feature: Red pre-applied anti-loosening compound
Installation: One-sided blind installation
Mounting hole: Per approved drawing
Compound specification: Subject to confirmation
Applications include equipment enclosures, industrial machinery, electrical cabinets, automotive components, and OEM sheet-metal assemblies requiring controlled insert installation and specified adhesive functionality.
For technical review and quotations, contact info@juxinfasteners.com.
Product Specification
M6 Stainless Steel Closed-End Knurled Rivet Nut with Pre-Applied Adhesive – OEM Fastening Solutions
JUXIN FASTENERS supplies an M6 stainless steel high flat head closed-end knurled body blind rivet nut with a red pre-applied anti-loosening compound for drawing-specific OEM fastening applications.
Part number JX-BF2.5-M6-RX9-19-SS combines a raised flange, externally knurled round body, closed-end threaded barrel, and an additional pre-applied compound visible near the flange.
This configuration is intended for OEM assemblies requiring a reusable M6 internal thread, one-sided installation, and controlled retention of the installed threaded insert.
The exact adhesive chemistry, coating location, activation mechanism, and functional performance must be verified against the approved material and product specifications.
Product Specifications
Product type: High Flat Head Closed-End Knurled Body Blind Rivet Nut with Pre-Applied Compound
Part number: JX-BF2.5-M6-RX9-19-SS
Thread size: M6
Thread pitch and tolerance class: According to approved drawing
Material: Stainless steel
Surface finish: Natural stainless steel
Grip range: 0.5–3.0 mm
Approximate inch reference: 0.020–0.118 in
Head style: High flat head / Raised flange
Body style: Externally knurled round body
End configuration: Closed end
Additional feature: Red pre-applied anti-loosening compound
Compound location: Visible near the flange; exact application area subject to drawing confirmation
Mounting-hole geometry: Round hole, dimensions according to approved drawing
Installation: One-sided blind installation
Stainless steel grade: Subject to confirmation
Flange dimensions: According to approved drawing
Body dimensions: According to approved drawing
Internal screw depth: According to approved drawing
Adhesive performance: Subject to approved technical specification and validation
The product designation does not establish an adhesive brand, curing time, locking torque, sealing classification, or mechanical retention rating.
Engineering Features and Application Considerations
Why Use a Rivet Nut with Pre-Applied Adhesive?
Conventional knurled rivet nuts rely primarily on mechanical deformation and engagement with the parent material to establish retention.
An additional functional compound may be specified where the OEM requires enhanced retention, controlled assembly behavior, or another defined interface function.
For under-head adhesive systems, the intended purpose may be to increase resistance to rotation of the installed rivet nut.
Other under-flange materials may instead be designed for sealing or controlled interface contact.
The exact function depends on the compound chemistry and application design.
For this JUXIN product, the customer-specified anti-loosening function should be confirmed through the approved drawing and material documentation.
Under-Head Adhesive vs. Threadlocking Adhesive
These two fastening technologies should not be confused.
Under-head adhesive is applied at the interface between the rivet nut flange and the parent material.
Depending on its formulation, it may bond the installed insert to the panel and increase resistance to insert rotation.
Threadlocking adhesive is applied to the internal or external thread interface.
Its purpose is to resist relative rotation between the mating screw and the threaded component.
A red compound near the rivet nut flange does not automatically mean that the mating screw has a threadlocking feature.
The distinction is important because an insert can remain firmly anchored in the panel while the mating screw still loosens under service conditions.
OEM engineers should define whether the required anti-loosening performance concerns:
Rivet nut rotation within the mounting hole
Mating screw loosening
Joint clamp-load retention
Sealing of the flange-to-panel interface
A combination of these functions
Each requirement may need a different validation method.
Knurled Body and Mechanical Anti-Rotation
The external knurling is intended to engage the surrounding parent material during installation.
This can help resist rotation when a mating screw is tightened or removed.
For an adhesive-equipped version, the mechanical contribution of the knurling and the additional contribution of the compound should be evaluated separately where performance is critical.
Relevant variables include:
Knurl geometry
Mounting-hole diameter
Parent-material strength
Grip thickness
Installation deformation
Flange contact
Adhesive coverage
Surface cleanliness
Adhesive curing or activation conditions
No specific spin-out torque should be assumed without supporting test data.
High Flat Head and Adhesive Contact Area
The high flat head provides a raised bearing surface against the accessible side of the panel.
Where the functional compound is applied beneath the flange, the available contact area may influence the effectiveness of the adhesive interface.
However, flange height and flange diameter are separate dimensions.
A taller flange does not automatically create a larger adhesive bonding area.
For drawing review, engineers should confirm:
Flange outside diameter
Flange thickness
Adhesive application location
Adhesive coverage area
Contact surface condition
Flange seating
Mating component clearance
The flange should seat according to the approved installation specification.
Parent-Material Surface Condition
Adhesive performance may be sensitive to the condition of the parent material.
Oil, grease, corrosion products, loose coatings, and other surface contaminants can affect adhesion.
Painted, powder-coated, plated, and untreated metal surfaces may produce different results.
For OEM applications, engineers should identify:
Parent-material grade
Surface finish
Coating type
Surface cleanliness
Adhesive compatibility
Installation sequence
Environmental exposure
An adhesive system validated on bare metal should not automatically be assumed to provide equivalent performance on a painted or powder-coated panel.
Adhesive Activation and Curing
Pre-applied functional compounds can operate through different mechanisms.
Some materials develop adhesion during installation.
Others may require a defined curing period, temperature condition, or additional process control.
The color of the compound does not identify its chemistry.
Red does not automatically mean high-strength anaerobic threadlocker, and the product should not be assigned a curing schedule based on appearance.
For this part, the following information should be confirmed:
Compound manufacturer and grade
Chemical type
Application location
Required coating amount
Activation mechanism
Initial handling requirements
Curing conditions, if applicable
Temperature limits
Shelf life
Storage conditions
Where adhesive performance is required for production acceptance, testing should reflect the approved installation and curing conditions.
Closed-End Barrel and Screw Penetration Control
The closed-end barrel prevents the mating screw from passing through the far end of the insert.
This can be useful where nearby wiring, electronic components, insulation, or other internal structures must be protected from screw penetration.
However, the closed end does not automatically make the complete installed joint waterproof.
Where environmental sealing is required, the flange-to-panel interface and any additional sealing features must be evaluated.
The presence of red adhesive does not establish an IP rating or leak-tightness specification.
Screw Bottoming and Joint Clamp Load
Closed-end rivet nuts have limited internal screw depth.
If the mating screw is too long, its tip may contact the closed barrel before the joint components are properly clamped.
This can create a false tightening condition.
The applied torque may increase without producing the intended clamping force.
For this M6 product, engineers should verify:
Internal screw depth
Mating screw length
Minimum assembled stack thickness
Washer and spacer tolerances
Required thread engagement
Screw tip clearance
Worst-case dimensional tolerances
The adhesive under the flange, if confirmed, does not eliminate the need to verify screw bottoming clearance.
Grip Range and Panel Thickness
The specified grip range for this product is 0.5–3.0 mm.
This range should be used when evaluating the intended parent-panel thickness.
The insert should not be installed outside its approved grip range without engineering review.
For thin sheet-metal applications, installation performance should be verified at the relevant minimum and maximum panel thicknesses.
Where the compound is intended to improve retention, the selected panel thickness and surface condition should be included in the validation process.
Round-Hole Installation
The knurled round-body configuration is intended for installation in a compatible round mounting hole.
The exact mounting-hole diameter and tolerance must be confirmed from the approved drawing.
An M6 internal thread does not establish the required hole diameter.
For reliable installation, verify:
Mounting-hole diameter
Hole tolerance
Burr condition
Panel thickness
Surface cleanliness
Flange seating
Installation tool compatibility
Hole preparation should avoid damage to the intended adhesive contact surface.
Installation Process and Adhesive Protection
The installation process must account for both the rivet nut geometry and the pre-applied compound.
Excessive handling, contamination, or incompatible cleaning processes may affect the compound before installation.
Production validation should consider:
Packaging condition
Coating appearance
Compound location
Hole preparation
Installation tool selection
Flange seating
Setting stroke or force
Installed backside geometry
Adhesive activation or curing
Required retention performance
The installation method should follow the approved product and compound specifications.
Stainless Steel and Material Compatibility
The product is specified as stainless steel with a natural finish.
The exact stainless steel grade has not been confirmed.
The required grade should be established during technical review.
For applications involving moisture, cleaning chemicals, chlorides, or dissimilar metals, corrosion compatibility should be evaluated.
The compound must also be compatible with the stainless steel surface and the parent material.
Where material traceability or adhesive batch identification is required, the purchasing specification should identify the necessary documentation.
Installed Spin-Out Resistance
Spin-out resistance describes the resistance of an installed rivet nut to rotation within its mounting hole.
For an adhesive-equipped knurled rivet nut, spin-out performance may depend on both mechanical engagement and the functional compound.
A valid comparison between coated and uncoated inserts should control:
Rivet nut geometry
Parent material
Panel thickness
Mounting-hole dimensions
Installation settings
Surface condition
Adhesive curing conditions
Test method
Testing only the adhesive-equipped version does not isolate the contribution of the compound.
For OEM qualification, the required spin-out acceptance value and test conditions should be agreed upon.
Repeated Screw Removal and Maintenance
The closed-end M6 internal thread may be used for serviceable assemblies.
However, repeated tightening and loosening can place rotational loads on the installed insert.
Where the compound contributes to spin-out resistance, the effect of repeated service cycles should be evaluated.
The permitted number of service cycles cannot be determined from the visible coating color.
Maintenance requirements should be established using the approved assembly specification and relevant test results.
Adhesive Shelf Life and Inventory Control
Pre-applied compounds may have storage and shelf-life requirements.
For OEM procurement teams, this creates an additional supplier qualification consideration compared with an uncoated mechanical insert.
Where applicable, purchasing documentation should identify:
Compound grade
Coating batch
Manufacturing or application date
Shelf-life requirements
Storage temperature
Storage humidity
Packaging protection
Inspection criteria
These requirements should be established according to the actual compound technical data.
Coated vs. Uncoated M6 Knurled Rivet Nuts
An uncoated M6 knurled rivet nut relies on its mechanical installation features for retention.
An adhesive-equipped version introduces an additional functional material at the specified interface.
The coated version may be considered where the OEM requires additional insert retention or another validated interface function.
However, the coated and uncoated versions should not automatically be treated as interchangeable.
The compound may affect installation, inspection, storage, surface compatibility, and rework procedures.
Where the same base part number is used for both versions, the purchasing specification should include an explicit coating designation or approved drawing revision.
Industrial Applications and OEM Fastening Solutions
Automotive and Commercial Vehicle Components
Potential applications include equipment brackets, fabricated panels, service covers, and selected vehicle housings.
The knurled body and specified functional compound may be relevant where resistance to insert rotation is an important assembly requirement.
Vibration, temperature, corrosion, and retention requirements must be validated.
Electrical Cabinets and Control Equipment
Potential applications include electrical cabinets, instrument enclosures, equipment mounting panels, and serviceable covers.
The closed-end construction prevents screw penetration beyond the insert.
Where environmental sealing or electrical clearances are required, the complete assembly must be evaluated.
Industrial Machinery and Equipment
Potential applications include machine guards, maintenance panels, fabricated brackets, and equipment housings.
For repeatedly serviced components, engineers should evaluate installed spin-out resistance and thread durability.
HVAC and Appliance Manufacturing
Potential applications include equipment cabinets, appliance housings, mounting brackets, and fabricated sheet-metal structures.
The installation process should account for panel thickness, flange seating, and compound compatibility.
Transportation Equipment
Potential applications include selected non-safety-critical equipment enclosures, serviceable mounting components, and fabricated structures.
Mechanical loading, vibration, environmental exposure, and documentation requirements should be reviewed before approval.
Telecommunications and Electronic Equipment
Potential applications include equipment housings, instrument panels, and removable covers.
The closed-end barrel may help prevent screw penetration toward internal components.
Internal screw depth and backside clearance should be verified.
Engineering Standards and Technical Verification
The approved product drawing should control dimensions, thread requirements, material specifications, and installation compatibility.
Applicable ISO metric thread standards may include ISO 261 and ISO 965 where relevant.
Relevant ISO, DIN, EN, ASTM, SAE, ASME, or other applicable international standards should be selected according to the actual product, material, inspection, and application requirements.
Adhesive performance should be evaluated using agreed test methods and acceptance criteria appropriate to the intended function.
No specific certification, locking torque, spin-out value, sealing rating, curing time, or standard conformity should be assumed without supporting documentation.
OEM Procurement and Supplier Qualification
For purchasing managers and supplier development teams, this product requires qualification of both the mechanical insert and the functional compound.
The base rivet nut geometry should be verified against the approved drawing.
The compound should be identified by its approved material specification, application location, and acceptance criteria.
Where the same base part number is used for coated and uncoated versions, the purchase order should clearly distinguish the two configurations.
This helps prevent substitution errors and supports consistent incoming inspection.
For recurring OEM programs, material requirements, coating specifications, inspection criteria, traceability, packaging, annual demand, and delivery expectations should be established during sourcing.
OEM RFQ Requirements
Please provide:
Part number: JX-BF2.5-M6-RX9-19-SS
2D drawing or 3D CAD model
Required stainless steel grade
Parent material and surface finish
Panel thickness
Mounting-hole diameter and tolerance
Flange dimensions
Body dimensions and knurl requirements
Internal screw depth
Mating screw length
Required grip range
Compound specification
Compound application location
Required anti-loosening or spin-out performance
Adhesive curing and storage requirements
Installation method and tooling requirements
Inspection and traceability requirements
Prototype or production quantities
Estimated annual demand
Delivery destination
JUXIN FASTENERS supports drawing-based technical reviews and OEM sourcing discussions for M6 stainless steel closed-end knurled rivet nuts with specified pre-applied functional compounds.
Final dimensions, compound availability, material compatibility, installation performance, and inspection requirements should be confirmed before production approval.
Related Fastening Solutions
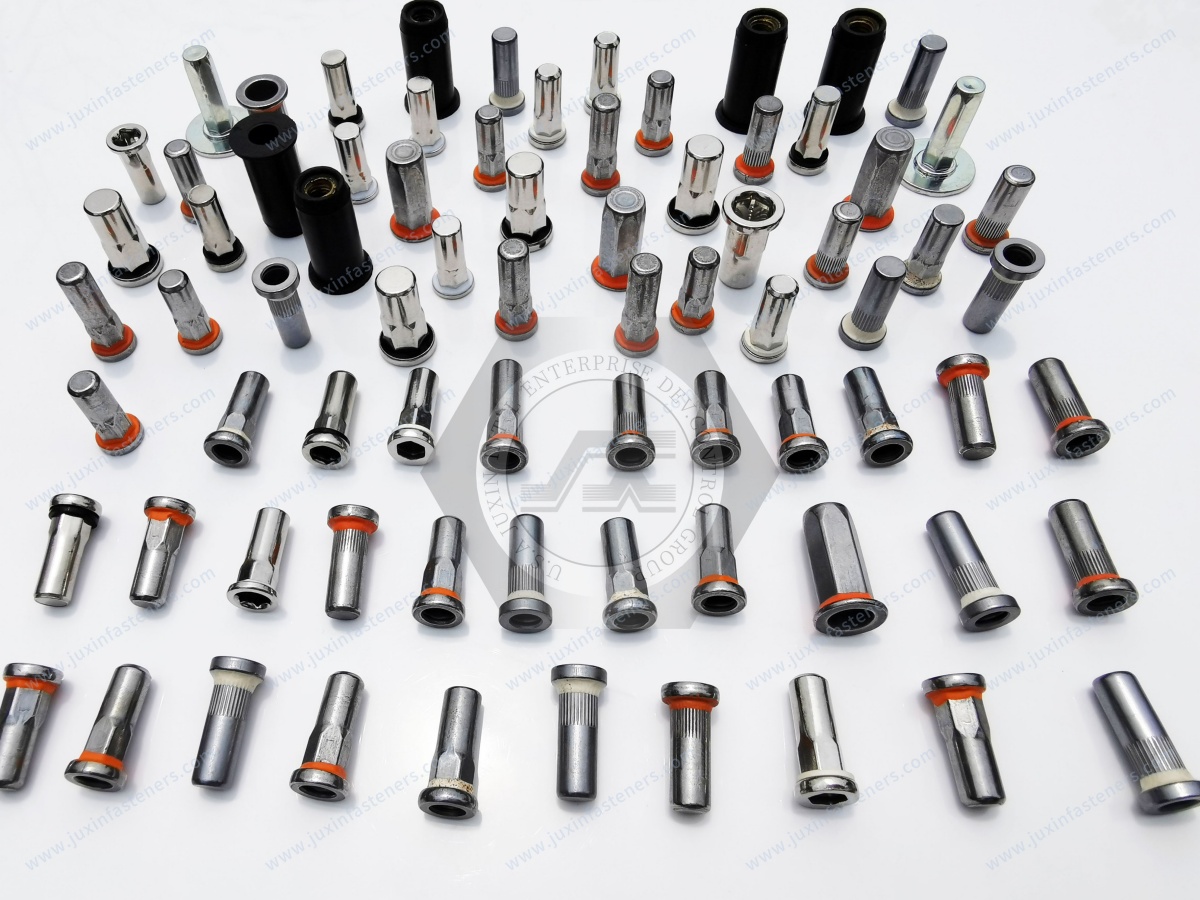
M6 Stainless Steel High Flat Head Closed-End Knurled Rivet Nuts
An uncoated configuration for applications relying on mechanical installation retention.
Stainless Steel High Flat Head Closed-End Partial Hex Body Blind Rivet Nuts
An alternative using partial hexagonal geometry for rotational engagement.
Stainless Steel Flat Head Closed-End Partial Hex Body Blind Rivet Nuts
An alternative combining a conventional flat flange with a closed-end partial hex body.
Stainless Steel Thin Head Closed-End Knurled Blind Rivet Nuts
A low-profile alternative where reduced flange projection is required.
Stainless Steel Rivet Nuts for Plastic and Composites
A slotted-body alternative for selected softer panels requiring a wider backside bearing structure.
Request an OEM Quotation
Looking for M6 stainless steel closed-end knurled rivet nuts with pre-applied adhesive or custom functional coatings?
Send JUXIN FASTENERS your engineering drawings, compound requirements, panel material, and estimated purchasing quantities.
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
JUXIN FASTENERS – Industrial Blind Rivet Nuts and Custom OEM Fastening Solutions.
Product Packaging
Packaging and Delivery – M6 Stainless Steel Rivet Nuts with Pre-Applied Adhesive
JUXIN FASTENERS reviews packaging arrangements according to product dimensions, compound requirements, order quantities, handling conditions, and OEM purchasing specifications.
Product Identification
Part number: JX-BF2.5-M6-RX9-19-SS
Thread size: M6
Material: Stainless steel, natural finish
Grip range: 0.5–3.0 mm
Additional feature: Red pre-applied anti-loosening compound
Compound identification: According to approved material specification
Packaging quantity: Subject to order confirmation
Inner packaging: According to approved packing instructions
Outer packaging: According to shipment requirements
Batch identification: According to agreed traceability requirements
Compound Protection
Packaging should protect the pre-applied compound from contamination, abrasion, and conditions that may affect its specified functionality.
Where the compound has defined storage temperature, humidity, or shelf-life requirements, these should be included in the approved packaging and handling instructions.
The flange, knurled body, internal threads, and closed-end barrel should also be protected from mechanical damage during storage and transportation.
OEM Supply and Documentation
For recurring OEM programs, compound identification, batch traceability, packaging quantities, labeling, inspection documentation, and delivery arrangements should be agreed upon before shipment.
Final packaging specifications are confirmed according to the approved purchase order.
For OEM packaging requirements and quotations, contact info@juxinfasteners.com.
Website: www.juxinfasteners.com
Product Pictures
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY