Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

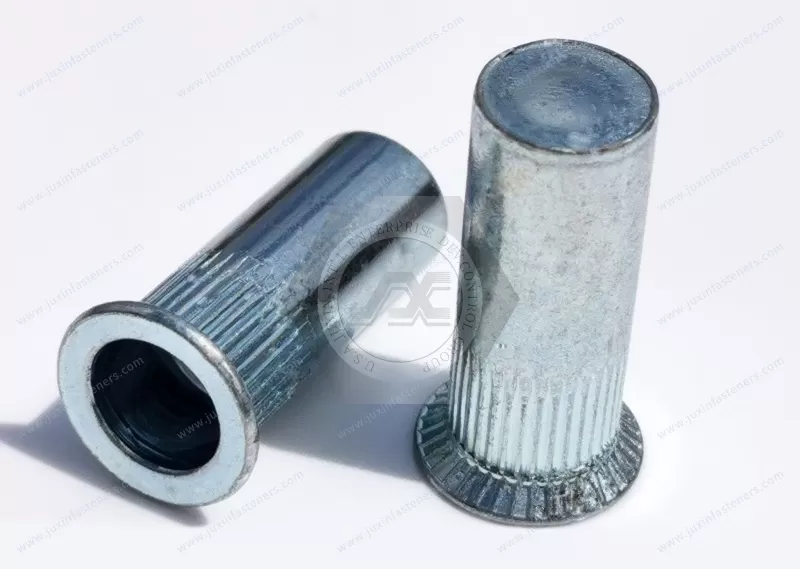
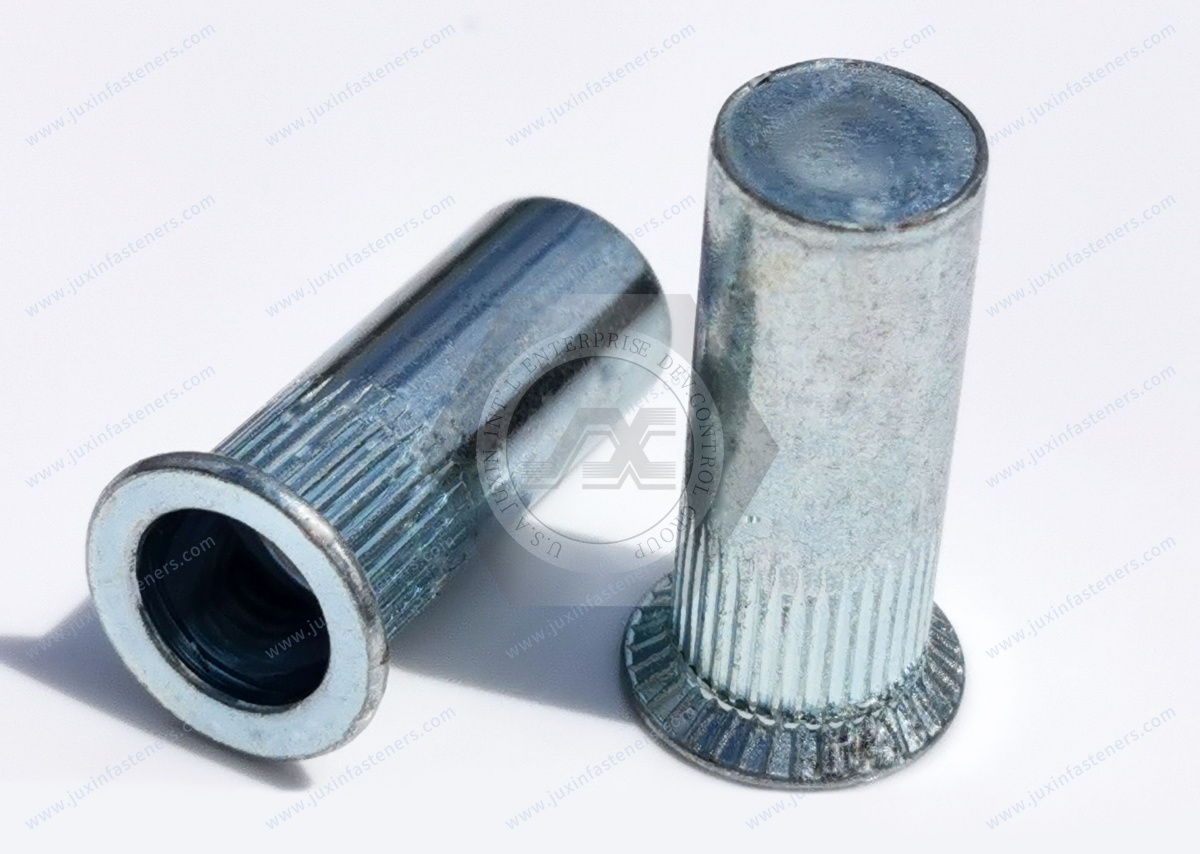
JUXIN FASTENERS manufactures blue zinc-plated steel blind rivet nuts with countersunk heads, closed-end barrels, and knurled round bodies for creating internal threads in thin sheet metal, hollow sections, and industrial assemblies requiring one-sided installation.
The countersunk head allows flush or near-flush mounting in a properly prepared hole, while the knurled body helps resist insert rotation. The closed-end barrel encloses the threaded cavity and prevents screws from passing through the insert end.
Product Features
Metric thread sizes: M3, M4, M5, M6, M8, M10
Inch-series threads: Custom OEM requirements subject to drawing review
Material: Steel
Surface finish: Blue zinc plating
Grip range: 0.5–4.5 mm (approx. 0.020–0.177 in) across the product family, depending on configuration
Head style: Full countersunk head
Body style: Knurled round body
End style: Closed end
Installation: One-sided blind installation
Typical applications include electrical enclosures, control cabinets, machinery housings, removable equipment covers, and OEM sheet-metal assemblies requiring reduced head projection and enclosed threaded inserts.
Product Specification
Technical Specifications — Closed-End Countersunk Knurled Steel Rivet Nuts
Metric Thread Specifications
| Thread Size | Pitch (mm) | Nominal Diameter (in) |
|---|---|---|
| M3 × 0.5 | 0.50 | 0.1181 |
| M4 × 0.7 | 0.70 | 0.1575 |
| M5 × 0.8 | 0.80 | 0.1969 |
| M6 × 1.0 | 1.00 | 0.2362 |
| M8 × 1.25 | 1.25 | 0.3150 |
| M10 × 1.5 | 1.50 | 0.3937 |
Applicable metric thread references include ISO 261, ISO 724, and ISO 965, according to the required thread geometry and tolerance class.
Unified Inch Thread Requirements
For North American OEM programs, Unified inch-thread configurations can be submitted for custom manufacturing feasibility review.
| Thread | Series | Status |
|---|---|---|
| #4-40 | UNC | Custom inquiry |
| #6-32 | UNC | Custom inquiry |
| #8-32 | UNC | Custom inquiry |
| #10-24 | UNC | Custom inquiry |
| #10-32 | UNF | Custom inquiry |
| 1/4-20 | UNC | Custom inquiry |
| 5/16-18 | UNC | Custom inquiry |
| 3/8-16 | UNC | Custom inquiry |
Unified thread requirements may reference ASME B1.1.
The inch-thread options above are not confirmed standard inventory items.
Availability, minimum order quantity, and tooling requirements must be reviewed individually.
Grip Range
Published series range:
0.5–4.5 mm (approximately 0.020–0.177 in)
Individual part numbers may have different usable grip ranges.
For countersunk configurations, effective panel thickness must account for the material removed during countersink preparation.
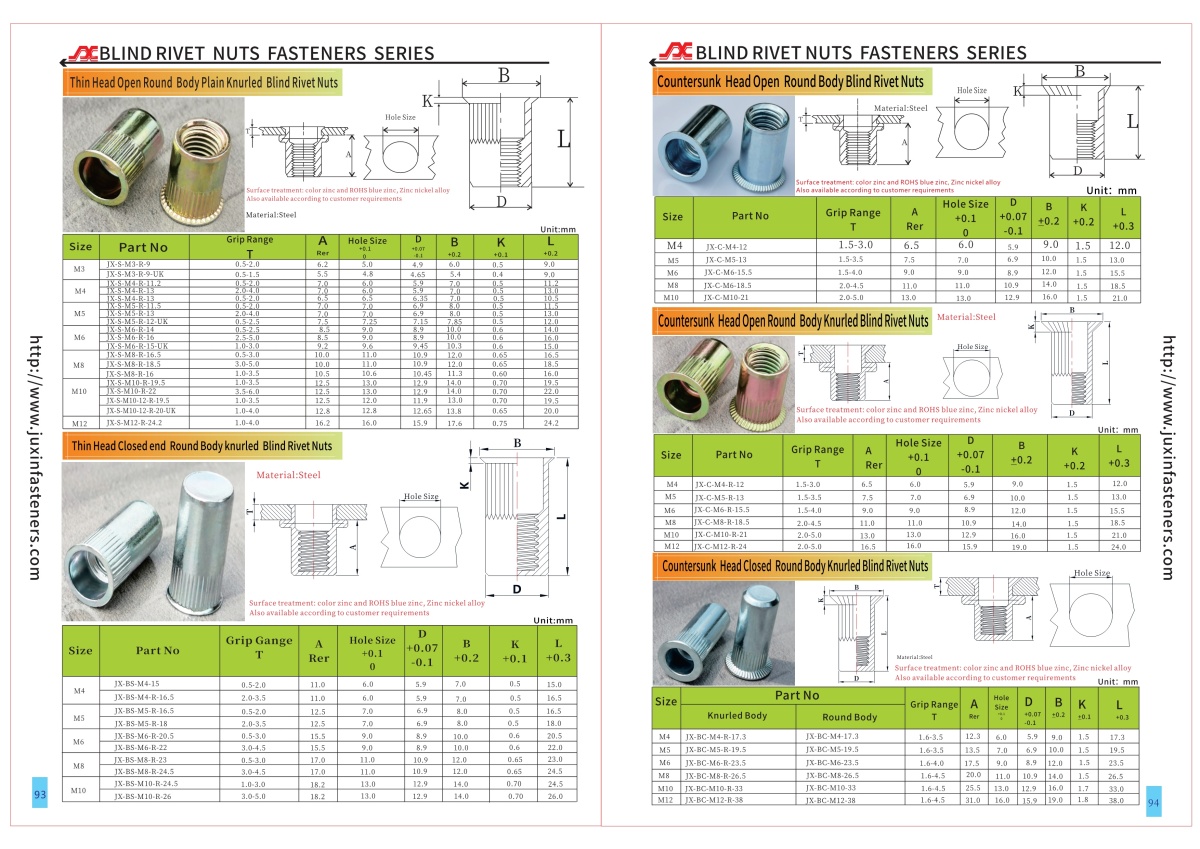
Original Catalog Dimension Reference
| Metric Thread | Reported Dimension (mm) |
|---|---|
| M4 × 0.7 | 11.5 |
| M5 × 0.8 | 13.0 |
| M6 × 1.0 | 17.0 |
| M8 × 1.25 | 19.0 |
| M10 × 1.5 | 21.0 |
The original information does not identify the dimensional feature represented by these values.
They must be verified against the technical drawing before use in hole preparation, installation tooling, or inspection.
Critical Closed-End Design Requirements
Internal Thread Depth
Closed-end rivet nuts have a finite internal cavity.
The mating screw must not bottom against the closed end before the joint reaches its intended clamp condition.
Engineers should verify:
Available internal thread depth
Minimum required thread engagement
Screw protrusion beyond the mating component
Installation deformation allowance
Screw length tolerance
Clearance to the closed end
Countersink Geometry
The approved drawing should specify the countersink angle, major diameter, and depth.
Do not assume that all metric countersunk rivet nuts use an identical head angle.
The mounting recess must match the actual supplied fastener geometry.
Installation Hole
Hole diameter and tolerance affect the engagement of the knurled body.
Excessive clearance may reduce resistance to rotation.
Insufficient clearance may damage the fastener or mounting panel.
Installation Stroke
The setting stroke must create sufficient backside deformation to retain the insert without damaging the threads or panel.
Installation parameters should be validated for each part size and grip condition.
Installation Procedure
Verify the rivet nut dimensions and thread size.
Confirm the panel thickness and effective grip range.
Prepare the installation hole according to the approved drawing.
Machine or form the specified countersink.
Remove unacceptable burrs and inspect the hole.
Select the correct rivet nut setting tool and mandrel.
Insert the rivet nut into the mounting hole.
Maintain proper tool alignment.
Apply the validated installation stroke.
Inspect flange seating and backside deformation.
Check internal thread integrity.
Verify installed retention performance as required.
Recommended OEM Qualification Tests
Depending on the application, engineering validation may include:
Spin-out torque
Axial pull-out strength
Push-out resistance
Thread engagement verification
Installation stroke consistency
Countersunk flange seating
Repeated assembly and disassembly
Coating thickness inspection
Corrosion resistance
Leakage or ingress testing where specified
Test methods and acceptance limits must be agreed upon for the specific application.
Technical Documentation
Please refer to the product PDF and CAD drawings for detailed dimensions.
Original catalog reference: Pages 93–94.
Customer-specific dimensions and technical requirements can be reviewed against submitted drawings.
RFQ Checklist
For an accurate engineering and commercial quotation, please provide:
Required thread size and pitch
Metric or Unified inch-thread designation
Part drawing or CAD file
Panel material and thickness
Mounting hole and countersink dimensions
Required grip range
Available backside clearance
Required internal thread engagement
Coating and corrosion specifications
Mechanical performance requirements
Estimated order quantity
Annual forecast
Packaging and delivery requirements
Engineering Advantages
1. Closed-End Design Protects the Threaded Cavity
Unlike open-end rivet nuts, closed-end inserts have an enclosed blind end.
This construction prevents direct entry of dirt, debris, and fluids through the bottom of the insert, helping protect the internal threads in enclosed equipment.
However, the closed end does not automatically seal the interface between the rivet nut flange and the mounting panel.
Applications requiring liquid-tight or airtight connections should specify appropriate sealing features and validate the completed assembly.
2. Flush-Mount Countersunk Head
The countersunk head is designed to sit within a matching recess in the host material.
When the countersink geometry and installation are correct, the flange can be positioned flush with the surrounding surface.
This is useful in:
Automotive interior panels
Industrial machine covers
Electrical equipment housings
Sheet metal enclosures
HVAC access panels
Railway interior equipment
Removable machinery components
A full countersunk head requires adequate panel thickness to maintain support around the installation hole.
For thin panels, reduced-head alternatives may be more appropriate.
3. Knurled Body for Improved Resistance to Rotation
The external knurled surface increases engagement between the rivet nut body and the host material.
This can improve spin-out resistance compared with smooth-body configurations, particularly when the hole dimensions and panel material are correctly matched.
The installed spin-out performance depends on:
Panel hardness and thickness
Installation hole tolerance
Knurl geometry
Setting stroke
Grip range
Backside deformation
Applied screw tightening torque
For production applications, spin-out torque should be verified using representative assemblies.
4. Single-Sided Installation
Closed-end knurled rivet nuts can be installed from the accessible side of a sheet or enclosed section.
A compatible installation tool engages the internal thread and applies axial force to collapse the deformable body section behind the panel.
This creates a mechanical retaining bulge without requiring welding or access to the opposite side.
5. Reusable Internal Threads
Once properly installed, the rivet nut provides a permanent internally threaded fastening point.
The mating screw can be removed and reinstalled for maintenance or equipment servicing, subject to thread condition and installation performance.
This is valuable for assemblies requiring periodic inspection or component replacement.
Closed-End Versus Open-End Rivet Nuts
| Feature | Closed-End | Open-End |
|---|---|---|
| Blind-End Cavity | Enclosed | Open |
| Screw Protrusion | Limited by Internal Depth | May Extend Through |
| Contaminant Entry Through Tail | Blocked by Intact Closed End | Possible |
| Overall Joint Waterproofing | Requires Validation | Requires Separate Sealing |
| Backside Clearance | Must Accommodate Closed Body | Depends on Body and Screw |
| Typical Selection | Protected Thread Cavity | Greater Screw-Length Flexibility |
When Should Engineers Choose Closed-End Rivet Nuts?
Closed-end inserts are worth evaluating when the assembly requires protection against contamination entering through the insert tail,
controlled screw engagement depth, or an enclosed threaded attachment point.
They should not be selected solely on the assumption that the complete joint will be waterproof.
For applications involving fluid pressure, outdoor exposure, or enclosure ingress protection, the full assembly must be assessed.
Industrial Applications
Automotive and Commercial Vehicle Equipment
Suitable for selected non-structural interior brackets, access panels, equipment housings, and removable assemblies.
The closed-end design helps protect internal threads from contamination entering through the blind end.
Electrical Enclosures and Control Cabinets
These inserts provide reusable threaded mounting points in enclosed sheet metal structures.
Where an enclosure requires an ingress protection rating, the complete fastening interface must be evaluated separately.
Industrial Machinery
Used for machine guards, fabricated covers, removable panels, and equipment housings requiring one-sided installation.
Railway Interior Equipment
May be considered for non-structural interior mounting brackets, access panels, and equipment covers where project-specific mechanical requirements are satisfied.
HVAC and Refrigeration Equipment
Suitable for selected equipment housings, access covers, and fabricated sheet metal assemblies.
Industrial Furniture and Equipment Fixtures
Countersunk closed-end rivet nuts provide concealed or flush threaded attachment points in compatible metal components.
Blue Zinc Plating and Corrosion Protection
The steel rivet nuts are specified with a blue zinc-plated finish.
Zinc plating provides sacrificial corrosion protection for the steel substrate.
For OEM projects, coating requirements should define the plating thickness, passivation system, corrosion resistance, and applicable restricted-substance requirements.
Relevant coating specifications may include ASTM B633 and ISO 2081.
The appearance of a blue zinc finish alone does not establish RoHS compliance. The actual plating chemistry and compliance documentation must be confirmed.
OEM Engineering and Custom Manufacturing
JUXIN FASTENERS supports customer-specific rivet nut requirements, including dimensional modifications, thread configurations,
and surface treatment specifications, subject to technical and manufacturing review.
For OEM engineers, important design considerations include mounting hole dimensions, countersink geometry, panel thickness, grip range,
installation stroke, thread engagement depth, and mechanical retention.
For procurement and supplier development teams, the purchasing specification should address material requirements, coating performance,
inspection criteria, packaging, order quantities, and production schedules.
Request a Quotation
JUXIN FASTENERS welcomes technical inquiries for standard metric closed-end countersunk rivet nuts and custom drawing-based fastening components.
Please provide your engineering drawing, panel material, grip thickness, required thread, coating specification, annual forecast, and estimated order quantity.
JUXIN FASTENERS
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Contact: https://www.juxinfasteners.com/contact-us/
Product Packaging
Export Packaging and OEM Supply
Standard Packaging
JUXIN FASTENERS provides protective export packaging for closed-end countersunk knurled steel blind rivet nuts.
The standard packaging arrangement includes plastic inner bags, outer cartons, and palletized shipping where required.
Packaging quantities and arrangements are determined according to product dimensions, order volume, and transportation requirements.
Reference Packaging Dimensions
| Packaging Type | Dimensions |
|---|---|
| Carton Option 1 | 29 × 19 × 19.5 cm |
| Carton Option 2 | 23.5 × 17.5 × 8 cm |
| Reference Pallet | 215 × 100 × 90 cm |
Final shipping dimensions and packing quantities are confirmed for each order.
Customized OEM Packaging
Customer-specific packaging requirements can be reviewed, including:
Customized bag and carton quantities
Customer part-number labels
Barcode identification
Batch and lot identification
Moisture-resistant protection
Special carton dimensions
Customer-specific pallet arrangements
Shipping marks and handling instructions
Special packaging may require additional preparation time and cost.
Bulk Purchasing and Supply Planning
For OEM and industrial purchasing programs, JUXIN FASTENERS can review annual demand forecasts, order schedules, technical documentation, packaging specifications, and delivery requirements.
For quotations and custom packaging inquiries:
JUXIN FASTENERS
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Contact: https://www.juxinfasteners.com/contact-us/
Product Pictures
Tags
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY