Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809
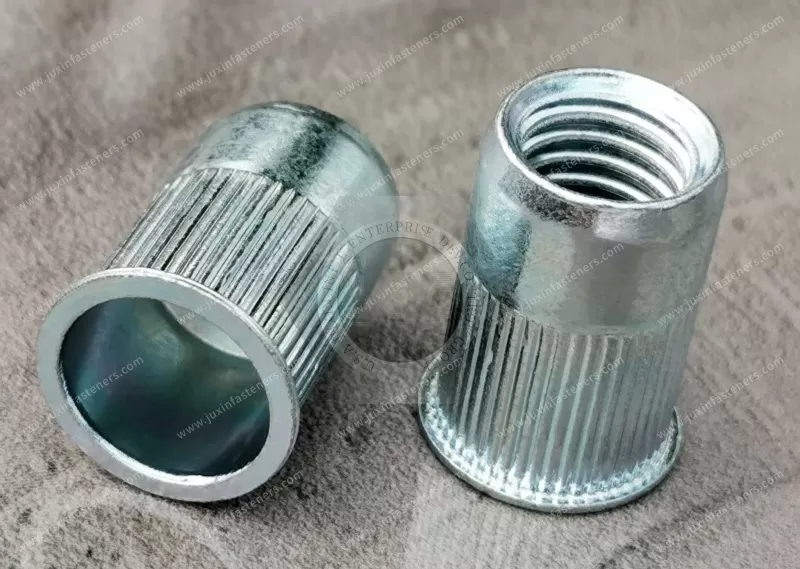
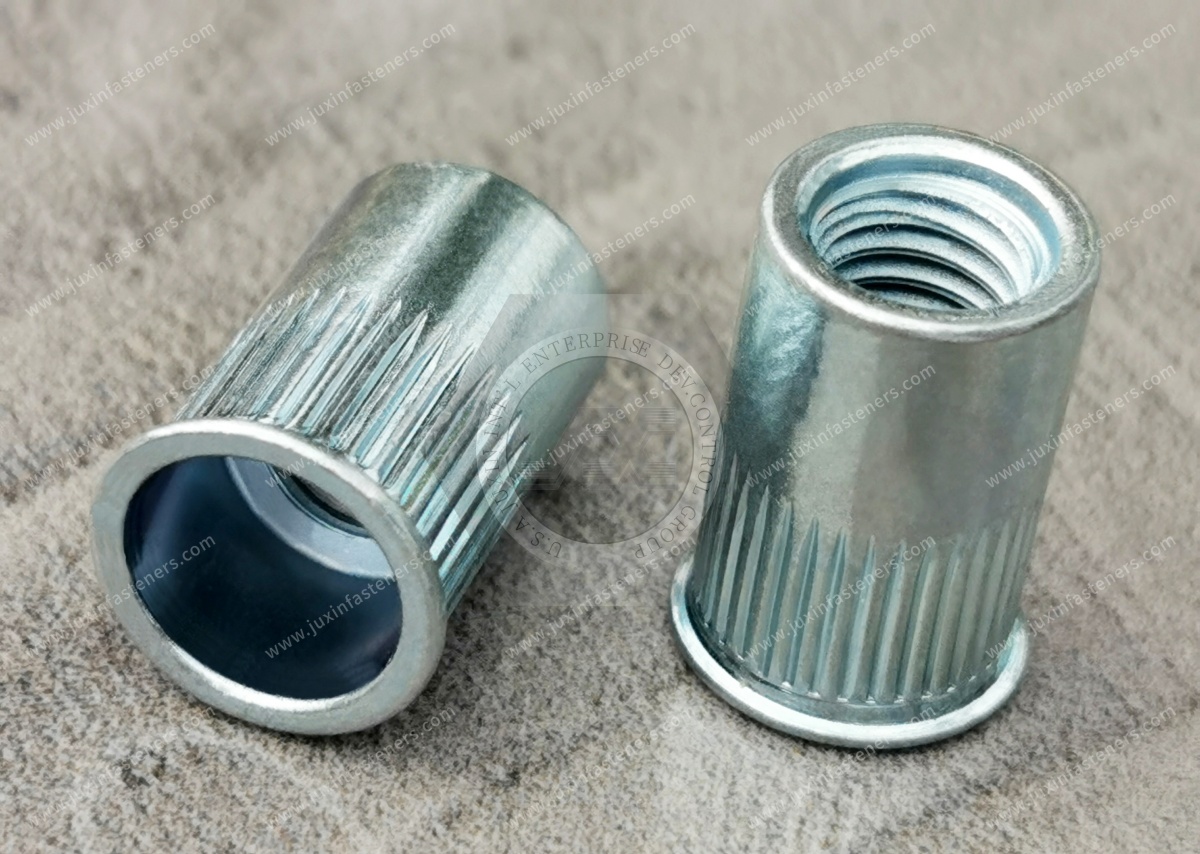
JUXIN FASTENERS manufactures low-profile head, open-end knurled round body steel blind rivet nuts for creating reusable internal threads in thin sheet metal, hollow sections, and OEM assemblies requiring one-sided installation.
The reduced-height flange minimizes surface protrusion, while the external knurling or ribs help resist insert rotation. The open-end design allows screw extension where sufficient backside clearance is available.
Product Features
Metric threads: M4, M5, M6, M8, M10, M12
UNC threads: #6-32, #8-32, #10-24, 1/4"-20, 5/16"-18, 3/8"-16, 1/2"-13
UNF threads: #10-32
Material: Steel
Finish: Blue-white zinc plating
Grip range: 0.5–7.9 mm (approx. 0.020–0.311 in), depending on size
Head: Thin head / Low-profile flange
Body: Knurled / Ribbed round body
End: Open end
Installation: One-sided blind installation
Applications include electrical enclosures, communication cabinets, electronic housings, machinery panels, and OEM sheet-metal assemblies requiring reduced head projection and reusable threaded connections.
Product Specification
Technical Specifications — Low-Profile Open-End Knurled Round Body Blind Rivet Nuts
1. Product Identification
Product Name: Low-Profile Head Open-End Knurled Round Body Blind Rivet Nuts
Common Alternative Names:
Thin Head Blind Rivet Nuts
Low-Profile Rivet Nuts
Knurled Round Body Rivet Nuts
Ribbed Body Rivet Nuts
Open-End Threaded Rivet Inserts
Low-Profile Threaded Inserts for Sheet Metal
Product Category: Steel Blind Rivet Nuts
Head Style: Low-Profile / Thin Head
Body Style: Knurled or Ribbed Round Body
End Style: Open End
Standard Material: Steel
Surface Treatment: Blue-White Zinc Plating
Stated Product-Family Grip Range: 0.5–7.9 mm
Installation Method: One-sided blind installation.
2. Thread Size Availability
Metric Thread Sizes
| Thread Size | Thread System |
|---|---|
| M4 | ISO Metric |
| M5 | ISO Metric |
| M6 | ISO Metric |
| M8 | ISO Metric |
| M10 | ISO Metric |
| M12 | ISO Metric |
Unified Inch Thread Sizes
| Thread Size | Thread Series |
|---|---|
| #6-32 | UNC |
| #8-32 | UNC |
| #10-24 | UNC |
| #10-32 | UNF |
| 1/4-20 | UNC |
| 5/16-18 | UNC |
| 3/8-16 | UNC |
| 1/2-13 | UNC |
Thread Selection Note: #10-32 is a Unified Fine thread designation (UNF), while #10-24 is a Unified Coarse thread designation (UNC). The specified rivet nut thread must match the mating screw or bolt.
The supplied product introduction lists metric sizes M4–M12. A separate general specification mentions M3–M12; M3 availability for this particular low-profile knurled body model requires confirmation before publication.
Custom thread configurations may be reviewed against customer drawings and manufacturing feasibility.
3. Material and Surface Finish
| Item | Product Specification |
|---|---|
| Base Material | Steel |
| Standard Finish | Blue-White Zinc Plating |
| Head Geometry | Low-Profile / Thin Head |
| Body Geometry | Round, Externally Knurled or Ribbed |
| Threaded End | Open End |
| Thread Systems | Metric and Unified Inch |
| Grip Range | 0.5–7.9 mm across the stated product family |
| Installation Access | One-Sided |
| Custom Options | Subject to drawing review |
The original specification describes the finish as "ROHS Blue White Zinc." For technical clarity, this page identifies the finish as blue-white zinc plating.
RoHS conformity is a material and substance-compliance matter, not a separate zinc-plating color. Where required, supporting declarations should be requested for the specific product and plating process.
Stainless steel and other material variants may be evaluated as separate products or custom manufacturing requirements; they are not presented as the standard material for this steel model.
4. Grip Range and Panel Thickness
Stated Product-Family Grip Range: 0.5–7.9 mm
The grip range represents the permitted total thickness of the material or material stack that an individual rivet nut can retain when correctly installed.
It is not the same as the overall body length.
For correct selection, engineers must verify:
Total panel or assembly thickness.
Specific rivet nut body length.
Deformable section geometry.
Parent-material strength.
Available blind-side installation space.
Installation equipment and setting parameters.
Not every thread size is necessarily available across the full 0.5–7.9 mm family range.
Thin-Sheet Installation Considerations
General product-family literature sometimes describes blind rivet nut installation in material thicknesses as low as 0.25 mm (0.010 in).
However, the supplied specification for this particular product states a minimum family grip of 0.5 mm.
Therefore, 0.25 mm should not be treated as the validated minimum installation thickness for this model without a corresponding drawing and installation test.
For extremely thin or fragile panels, engineers should evaluate local deformation, flange support, pull-out resistance and installation-induced damage.
5. Low-Profile Head Design
The low-profile head is intended to reduce projection above the accessible panel surface.
This feature is useful where mating parts must sit close to the panel or where conventional flange height would interfere with the assembly.
Key Design Considerations
Head Height: Determines the nominal projection above the mounting surface.
Flange Diameter: Influences the bearing area and local panel contact pressure.
Panel Flatness: Affects head seating and assembled clearance.
Installation Hole: Must be prepared to the required diameter and tolerance.
Mating Component Clearance: Must account for both the rivet nut head and the mating bolt or screw.
A thin head generally provides less flange thickness than a conventional flat-head configuration. The final selection should consider whether the available bearing area and panel support are adequate for the application.
A low-profile head is not necessarily flush with the panel. Flush installation requires a specifically designed fastening geometry and suitable panel preparation.
6. Knurled Body Geometry and Anti-Rotation Function
The external longitudinal knurling or ribs are designed to engage the surrounding parent material when the rivet nut is installed.
This geometry can increase mechanical resistance to insert rotation compared with an otherwise comparable smooth round body under suitable conditions.
Factors Affecting Torque-to-Turn
Knurl or rib geometry.
Body outside diameter.
Mounting-hole diameter and tolerance.
Panel material and hardness.
Grip thickness.
Installation stroke and setting force.
Panel coating and surface condition.
Testing method.
Torque-to-turn is the torque required to initiate rotation of the installed insert relative to the parent material under defined test conditions.
The supplied general technical text mentions an improvement of up to 50% compared with plain-body inserts. Because no corresponding JUXIN test report, specimen geometry or test conditions were provided, this figure is not stated as a guaranteed performance specification.
Where rotational resistance is critical, the OEM drawing or purchase specification should define a measurable acceptance criterion.
7. Pull-Out Resistance and Structural Loading
Pull-out resistance describes the axial load required to remove an installed insert from the parent material under specified test conditions.
It depends on the installed body deformation, panel thickness, parent-material properties, hole quality and rivet nut geometry.
For a complete threaded joint, engineers should separately consider:
Insert Pull-Out: Extraction of the rivet nut from the panel.
Insert Rotation: Loss of anti-rotation retention during tightening or servicing.
Internal Thread Stripping: Failure of the female thread under excessive loading.
Mating Bolt Failure: Tensile or shear failure of the screw or bolt.
Parent-Material Deformation: Local yielding, cracking or distortion around the installation hole.
Fatigue or Vibration Effects: Joint deterioration under repeated or fluctuating service loads.
These are different failure mechanisms and should not be represented by a single universal strength value.
For critical applications, testing should use the actual parent material, thickness, hole geometry and installation conditions.
8. Mounting Hole and Dimensional Requirements
A correctly prepared mounting hole is essential for reliable installation.
The product-specific drawing should identify:
| Dimensional Parameter | Engineering Purpose |
|---|---|
| Thread Diameter and Pitch | Mating fastener compatibility |
| Body Outside Diameter | Hole fit and body engagement |
| Recommended Hole Diameter | Installation compatibility |
| Hole Tolerance | Retention and insertion consistency |
| Head Diameter | Flange bearing area |
| Head Height | Installed projection and clearance |
| Body Length | Installation envelope |
| Grip Range | Permitted panel thickness |
| Blind-Side Clearance | Space for deformation during setting |
| Thread Engagement Length | Bolt and joint design |
These values are size-dependent and should not be invented or generalized across all available thread sizes.
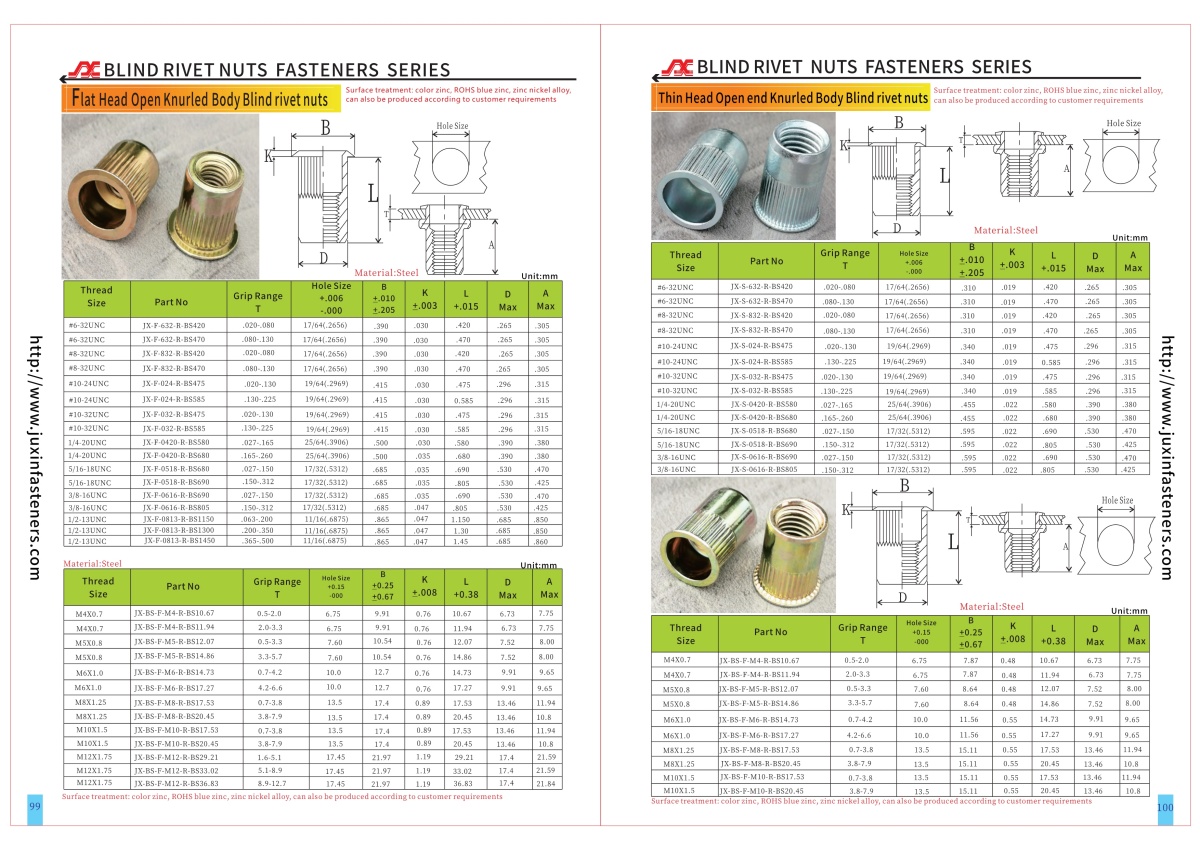
The supplied source refers to PDF pages 99–100 for detailed dimensional specifications and CAD information. Those pages should be checked against the selected model before publishing any numerical dimension table.
Round Hole vs. Hexagonal Hole
This product has a knurled round body and is intended for a corresponding round-hole installation design.
Full-hex and half-hex rivet nuts are different body configurations and may require specially shaped mounting holes.
A round-body product should not be described as a full-hex anti-rotation insert.
9. Installation Methods
Compatible setting methods may include:
Hand-operated rivet nut tools.
Pneumatic or hydro-pneumatic installation equipment.
Suitable automated production-line setting systems.
Tool selection depends on thread size, body material, geometry, grip range and the installation process.
Typical Installation Procedure
Confirm the rivet nut part number and specified grip range.
Prepare the mounting hole to the approved dimensions.
Remove unacceptable burrs and inspect the panel.
Select the correct installation mandrel and nosepiece.
Insert the rivet nut until the low-profile head seats against the panel.
Apply the specified setting stroke or installation force.
Form the retaining section behind the panel.
Release the setting tool without damaging the internal thread.
Inspect the installed head, panel condition and thread.
Perform required retention or torque checks according to the OEM inspection plan.
Incorrect setting may cause loose retention, insert rotation, thread damage or excessive panel deformation.
Installation settings should be established for the actual product and parent material rather than copied from another rivet nut model.
10. Open-End Thread Design
An open-end rivet nut has a threaded bore that is not closed at the blind end.
This allows the mating bolt to pass through the insert where sufficient assembly clearance exists.
Advantages may include flexibility in bolt length selection and straightforward thread engagement.
However, the open end does not prevent direct passage of water, dust or other contaminants through the threaded cavity.
Where environmental sealing is required, a closed-end or specially sealed fastening arrangement should be evaluated.
The complete joint must be assessed for the required environmental performance.
11. Installation in Painted or Coated Panels
Low-profile knurled rivet nuts may be installed in coated or painted assemblies when the hole dimensions, coating thickness and installation parameters are suitable.
Recommended engineering checks include:
Hole quality and burr control.
Coating buildup around the hole.
Head seating against the coated surface.
Risk of scratching or cracking during installation.
Local panel deformation.
Corrosion protection at exposed hole edges.
Damage-free installation cannot be assumed for all coatings or setting conditions.
Electrical Continuity
External knurling may influence metal-to-metal contact in some assemblies.
However, electrical bonding and grounding performance depend on the complete joint, including coating type, contact resistance, panel material and assembly conditions.
If electrical continuity is a design requirement, the OEM should specify an appropriate verification method and acceptance limit.
12. Relevant International Engineering References
The following standards may be relevant to thread definition, surface finishing and technical evaluation.
They are included as engineering references only; they do not imply that every JUXIN rivet nut is certified to each standard.
| Standard | Relevant Subject |
|---|---|
| ISO 261 | ISO metric screw thread series |
| ISO 965 | Metric screw thread tolerances |
| ASME B1.1 | Unified inch screw threads |
| ISO 4042 | Electroplated coating systems for fasteners, where applicable |
| ASTM B117 | Salt-spray testing when required by the specification |
| Customer-Approved Drawing | Product geometry, tolerances and acceptance criteria |
For OEM production, the customer drawing and agreed purchase specification should establish the actual requirements, including the applicable standard editions.
13. Industrial Application Engineering
Automotive and Transportation
Suitable for evaluation in compact sheet-metal brackets, covers and equipment components requiring a retained internal thread.
Important requirements include vibration resistance, tightening torque, service cycles, corrosion exposure and installation consistency.
Electrical Engineering and Control Cabinets
Useful for mounting plates, enclosure brackets and removable panels where reduced head projection is desirable.
Electrical continuity and coating compatibility must be validated where required.
Electronic Equipment and Metal Housings
Provides a compact fastening point for suitable sheet-metal housings, support structures and equipment enclosures.
Blind-side clearance and installation-induced deformation are important considerations.
Industrial Machinery
Applicable to fabricated frames, access panels, guards and equipment brackets.
Engineers should evaluate repeated servicing, torque-to-turn performance and joint loading.
Domestic Appliances and HVAC
Can be considered for thin-sheet housings, mounting components and serviceable assemblies.
Selection depends on panel thickness, available clearance and required joint retention.
General Light Fabrication
Supports one-sided threaded fastening in cabinets, brackets and fabricated sheet-metal structures.
For repetitive production, hole preparation and setting quality should be controlled.
14. OEM Manufacturing and Custom Product Review
JUXIN FASTENERS manufactures industrial fasteners and drawing-specific components using appropriate manufacturing processes.
Our broader manufacturing capabilities include cold heading, cold forming, CNC machining, secondary turning, metal stamping, plastic injection molding and combined production processes.
For custom rivet nut inquiries, JUXIN can evaluate:
Nonstandard thread requirements.
Modified low-profile head dimensions.
Special body lengths and grip ranges.
Alternative knurl or rib designs.
Material and plating requirements.
Customer-specific installation conditions.
Production volume and tooling considerations.
Packaging and identification requirements.
The actual manufacturing route and achievable tolerances must be determined from the customer drawing and technical review.
15. Technical Documentation and RFQ Checklist
For efficient product selection and quotation, please provide:
2D technical drawing or 3D CAD model.
Required thread size and thread series.
Panel material and thickness.
Mounting-hole dimensions and tolerances.
Maximum allowable installed head height.
Required grip range.
Available blind-side clearance.
Bolt tightening torque.
Torque-to-turn or pull-out acceptance criteria, if applicable.
Required plating and corrosion performance.
Expected order quantity and annual demand.
Inspection, traceability and packaging requirements.
Engineering Advantages
1. Reduced Head Projection for Space-Constrained Assemblies
A low-profile rivet nut is selected when the designer wants to minimize the height of the insert head above the accessible panel surface.
Compared with a conventional large-flange rivet nut, the reduced head height may help accommodate close-fitting covers, overlapping components and compact mechanical assemblies.
Typical design considerations include:
Clearance between the mounting panel and mating component.
Interference with covers, brackets or sliding parts.
Required flange bearing area.
Panel strength and local deformation.
Bolt head clearance and assembly accessibility.
A low-profile head is not automatically flush with the panel. If a truly flush installation is essential,
engineers should evaluate a suitable countersunk design or another validated fastening arrangement.
2. Knurled Body for Anti-Rotation Performance
The ribbed or knurled exterior creates a mechanical interface with the surrounding panel material.
When properly installed in a compatible hole, this geometry can help resist insert rotation during bolt tightening and subsequent servicing.
The achievable torque-to-turn resistance depends on the specific rivet nut design, panel material, hole dimensions, installation force and grip thickness.
A knurled round body may be attractive where the manufacturing process favors round holes rather than hexagonal holes.
However, it should not be assumed to provide the same anti-rotation performance as a full-hex rivet nut in every application.
For high-torque or safety-relevant joints, representative assembly testing is recommended.
3. Reusable Female Threads in Thin Sheet Materials
Thin metal panels may not provide sufficient thread engagement when tapped directly.
A blind rivet nut provides a mechanically retained internal thread for repeated bolt installation and removal, subject to the design's load and service requirements.
Applications may include removable panels, service covers, equipment brackets, electrical cabinets and machinery housings.
The insert can also help simplify assembly by eliminating the need to hold a separate nut on the inaccessible side of the workpiece.
4. One-Sided Installation for Enclosed Structures
The rivet nut can be installed from the accessible face of the panel without reaching behind it.
This makes it useful for box sections, tubular fabrications, enclosed frames, finished cabinets and other assemblies with restricted rear access.
Installation requires sufficient blind-side clearance for body deformation and compatible setting equipment.
5. Open-End Design for Flexible Bolt Engagement
The open-ended configuration permits the mating bolt to extend through the internal thread where the surrounding assembly allows.
This can be useful where bolt length and thread engagement requirements vary between applications.
Designers must still verify that the bolt does not interfere with adjacent components, electrical equipment or moving mechanisms.
For applications requiring a closed threaded cavity or protection against direct passage through the insert, a closed-end rivet nut may be more suitable.
6. Steel Body with Blue-White Zinc Finish
Steel provides a practical material choice for many industrial fastening applications, combining mechanical strength, formability and production efficiency.
The specified blue-white zinc-plated finish provides a protective surface coating for suitable operating environments.
Corrosion resistance depends on the coating specification, thickness, passivation, handling and service exposure.
A particular salt-spray result or corrosion classification must be supported by the applicable finish specification and test evidence.
Where the customer requires RoHS compliance, the applicable substance restrictions and supporting material or plating declarations should be confirmed for the supplied product.
Industrial Applications and Engineering Solutions
Automotive and Vehicle Component Assemblies
Low-profile knurled rivet nuts can be evaluated for sheet-metal brackets, equipment housings, interior hardware and other assemblies where a compact fastening point is required.
Design engineers should assess vibration, bolt tightening torque, repeated maintenance, parent-material thickness and corrosion exposure.
The reduced head height may help where adjacent components have limited clearance.
Electrical Enclosures and Control Cabinets
These threaded inserts can be used to attach mounting brackets, removable panels, support plates and internal cabinet hardware.
The low-profile head can be advantageous where a raised flange would interfere with a cover or adjoining component.
For painted enclosures, hole quality and installation settings should be controlled to minimize coating damage.
Where grounding or bonding is required, electrical continuity must be verified through the complete joint rather than assumed from the external knurling.
Industrial Machinery and Fabricated Equipment
Suitable applications include machine guards, access covers, equipment frames and fabricated housings.
A permanently retained internal thread simplifies maintenance when the rear of the mounting surface is inaccessible.
Designers should consider whether repeated bolt removal could cause insert rotation and whether the panel provides adequate support around the hole.
Electronics and Equipment Housings
Low-profile rivet nuts may be useful for compact metal housings, control units, support brackets and equipment panels.
Important design considerations include installation-tool access, clearance for the blind-side deformation, available panel thickness and the risk of distortion near sensitive components.
HVAC Equipment and Domestic Appliances
Thin sheet-metal housings, access panels and mounting brackets can benefit from one-sided threaded fastening.
A low-profile head can reduce interference between assembled panels, while the knurled body provides mechanical engagement with the parent material.
Installation parameters should be established for the actual sheet material and thickness.
General Sheet Metal Fabrication
These rivet nuts can support production of fabricated cabinets, brackets, light industrial structures and serviceable assemblies.
For high-volume production, repeatable hole preparation, controlled setting parameters and appropriate inspection criteria are essential.
Engineering Selection: Low-Profile vs. Flat Head Rivet Nuts
A low-profile knurled round body rivet nut and a conventional flat-head knurled round body rivet nut may share similar installation principles, but their head geometries serve different design priorities.
Low-Profile Head: Prioritizes reduced head projection and compact assembly geometry.
Flat Head / Large Flange: May provide greater bearing area and distribute contact pressure over a wider surface, depending on the actual flange dimensions.
Knurled Round Body: Offers mechanical engagement with the surrounding material while using a round mounting hole.
Smooth Round Body: May be appropriate where enhanced body-to-panel engagement is not a primary requirement.
Full-Hex Body: Provides geometric anti-rotation engagement when installed in a correctly prepared hexagonal hole.
Closed-End Configuration: Provides a closed threaded cavity but does not, by itself, guarantee sealing at the flange-to-panel interface.
The correct choice depends on the panel design, required installation geometry, torque and pull-out requirements, available clearance and assembly conditions.
Manufacturing Capabilities and OEM Customization
JUXIN FASTENERS is an industrial fastener and custom component manufacturer with production workshops and more than 20 years of industry experience.
Our manufacturing capabilities include cold heading, cold forming, secondary CNC turning and machining,
metal stamping, plastic injection molding and multi-process manufacturing, as appropriate to different product designs.
For suitable metal fasteners, production may combine cold forming with secondary machining to achieve particular geometries or dimensional requirements.
We select manufacturing processes according to the actual component design, material, tolerance requirements and production volume.
For OEM customers, we can review drawing-specific rivet nut requirements such as:
Special thread sizes or thread series.
Modified head height or flange diameter.
Custom body length and grip range.
Knurling or rib geometry.
Steel grade and alternative material requirements.
Surface-treatment specifications.
Installation-hole compatibility.
Production quantity and packaging requirements.
Our approach is to adapt manufacturing solutions to customer requirements wherever technically and commercially feasible.
OEM Sourcing and RFQ Support
For purchasing managers, supplier development teams and design engineers, a complete rivet nut inquiry should include:
Required metric or Unified thread size.
Panel material and thickness.
Installation-hole diameter and tolerance.
Maximum permitted head projection.
Available blind-side clearance.
Required tightening torque or retention performance.
Surface finish and corrosion-resistance requirements.
Drawing or 3D model, where available.
Sample quantity, production quantity and estimated annual usage.
Packaging, identification and delivery requirements.
For projects where the head height is critical, please provide the maximum acceptable installed head projection rather than relying on the general term "low profile."
Request a Technical Review or OEM Quotation
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
JUXIN FASTENERS — Flexible Manufacturing for Standard and Custom Industrial Fasteners.
Product Packaging
Product Packaging — Low-Profile Knurled Round Body Blind Rivet Nuts
Standard Industrial Packaging
JUXIN FASTENERS supplies low-profile head open-end knurled round body blind rivet nuts with packaging suitable for industrial customers, OEM assembly operations and international distribution.
The standard packaging arrangement includes inner plastic bags, outer cartons and palletized shipment packaging when required.
Packaging configurations can be adjusted according to product size, order quantity, customer handling requirements and shipment arrangements.
Packaging Specifications
| Packaging Item | Specification |
|---|---|
| Inner Packaging | Plastic Bags |
| Outer Packaging | Cartons |
| Carton Size Option 1 | 29 × 19 × 19.5 cm |
| Carton Size Option 2 | 23.5 × 17.5 × 8 cm |
| Pallet Dimensions | 215 × 100 × 90 cm |
| Custom Packaging | Available for Review Based on Customer Requirements |
The carton and pallet dimensions above are the packaging references supplied for this product family.
The number of rivet nuts per bag, quantity per carton, net weight, gross weight and pallet loading configuration are determined according to the selected product size and confirmed order requirements.
Packaging for OEM Production
JUXIN FASTENERS understands that industrial purchasing teams and assembly plants may require specific packaging arrangements for receiving, inventory management and production-line handling.
Customer-specific packaging options may include:
Defined quantities per inner bag.
Specified quantities per carton.
Product separation by thread size or part number.
Customer part-number labeling.
Lot or batch identification.
Carton identification and shipping labels.
Packaging suitable for warehouse and assembly-line handling.
Customized packing instructions.
Palletized shipping arrangements.
Any specific traceability, labeling or documentation requirements should be identified during RFQ review and order confirmation.
Surface Finish Protection
These steel rivet nuts are supplied with a blue-white zinc-plated surface finish.
Packaging and storage conditions should help minimize unnecessary handling damage, moisture exposure and contamination.
Customers should store the products in suitable dry conditions and avoid prolonged exposure to condensation or corrosive environments.
For long-distance shipments or special storage requirements, protective packaging measures can be reviewed as part of the order specification.
Custom Packaging and International Orders
For OEM manufacturing programs, distributors and procurement teams, JUXIN can review packaging requirements based on:
Thread size and product dimensions.
Order quantity and shipment frequency.
Customer warehouse requirements.
Assembly-line handling arrangements.
Product identification and labeling.
Transportation and palletization needs.
Please provide the required product size, purchase quantity, packaging instructions and shipping destination when requesting a quotation.
JUXIN FASTENERS
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Flexible Manufacturing. Practical Packaging. Customer-Focused OEM Support.
Product Pictures
Tags
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY