Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

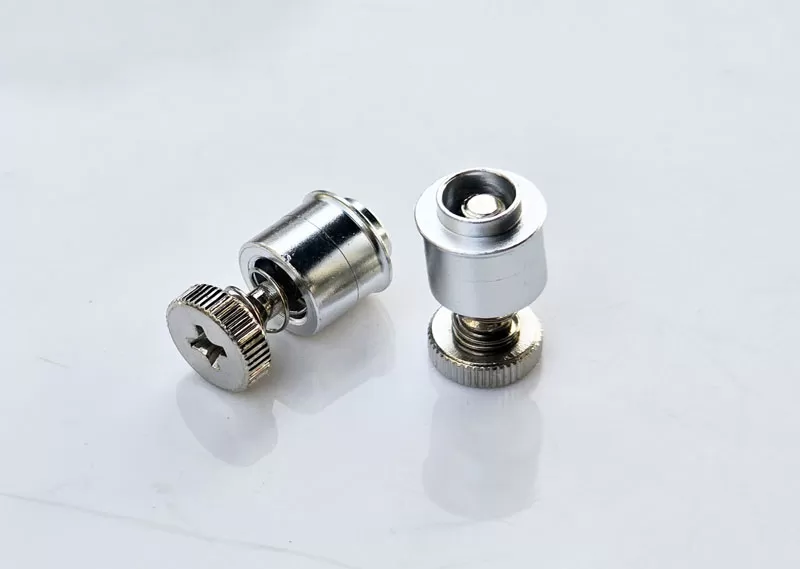
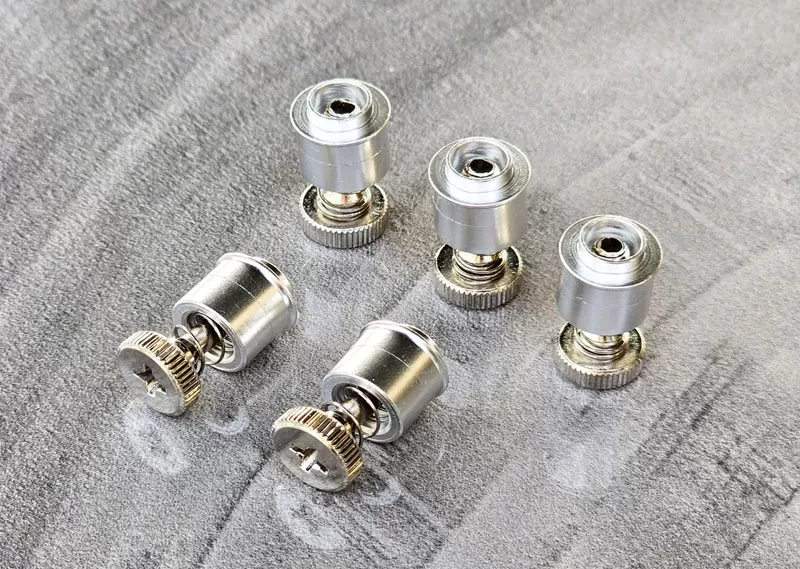
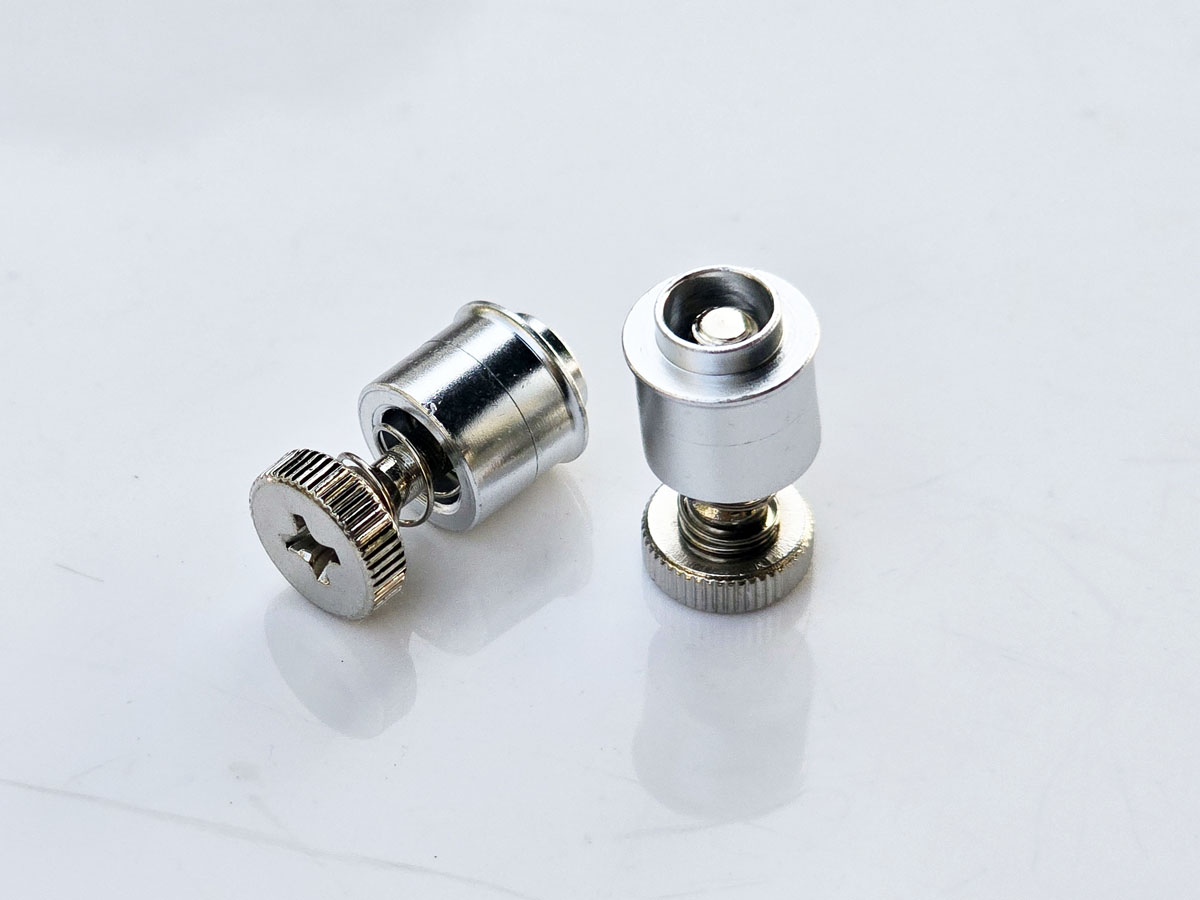
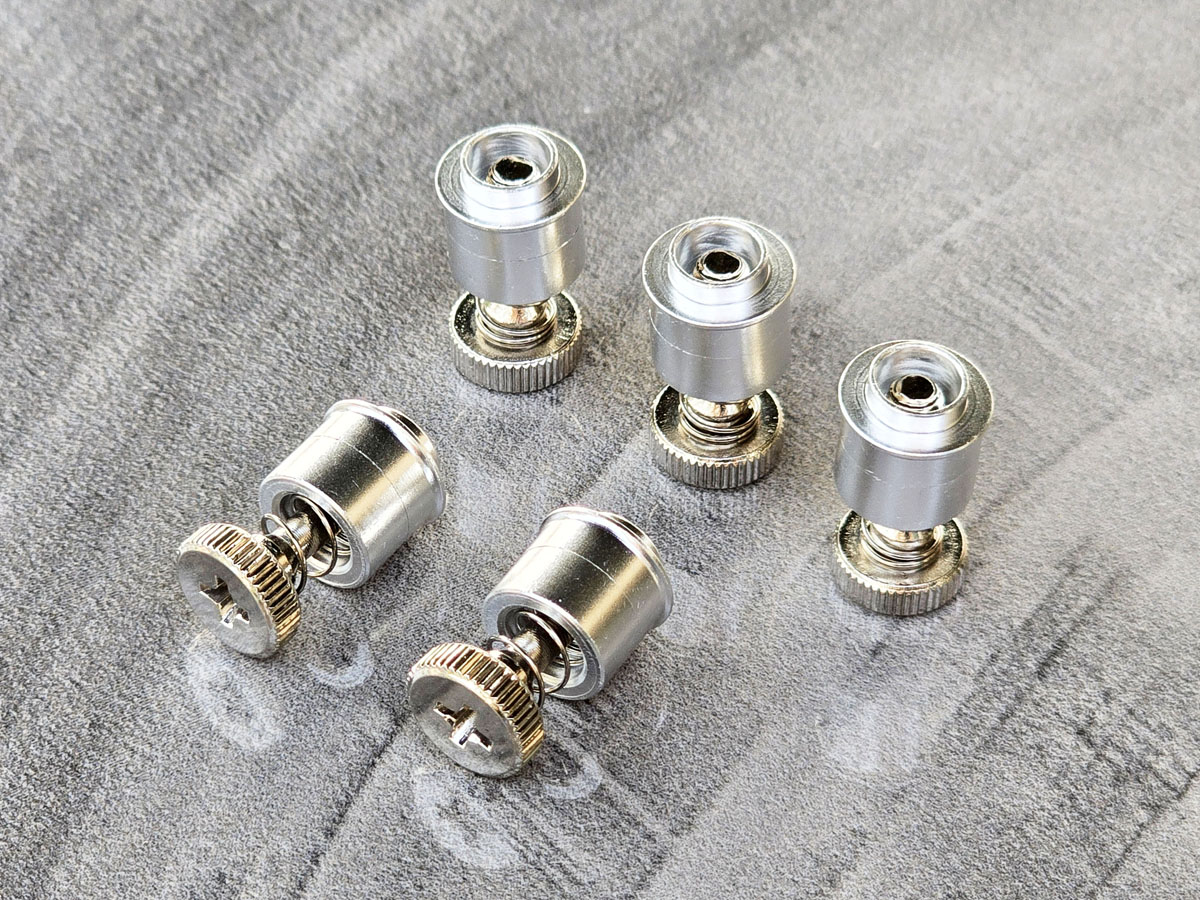
Spring-Loaded Flare-Mount Captive Panel Screw – Unified Type JX-PF7MF
JX-PF7MF is a spring-loaded captive panel screw designed for removable access panels, equipment covers, and industrial assemblies requiring retained fastening hardware.
Materials: Carbon steel or stainless steel, subject to the approved product configuration.
The flare-mount retention design is suitable for applications with limited centerline-to-edge distance and where conventional self-clinching installation may not be appropriate.
The mounting method does not require high installation force compared with some alternative press-in fastening arrangements.
Its flare-mounted construction can accommodate a broad range of panel hardness levels when the panel geometry and forming characteristics are compatible.
The retainer is designed to install flush with the backside of the panel, helping maintain clearance in compact assemblies.
The spring-loaded screw remains associated with the panel when disengaged, reducing loose hardware during maintenance and repeated access.
Typical applications include electronic enclosures, industrial control cabinets, telecommunications equipment, machinery access covers, instrumentation housings, and OEM sheet metal assemblies.
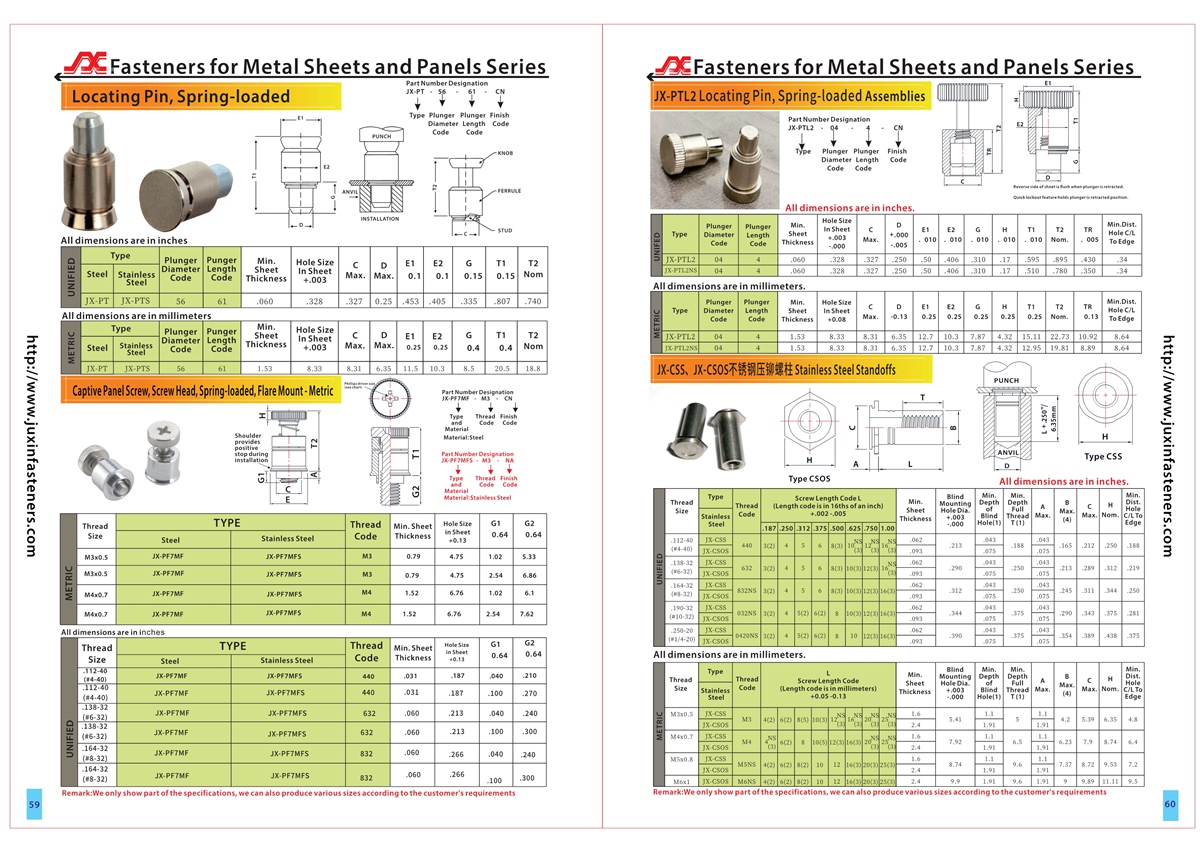
Unified inch-thread configurations and custom requirements are subject to the applicable JX-PF7MF technical drawing.
Product Specification
JX-PF7MF Spring-Loaded Flare-Mount Captive Panel Screws – Engineering and OEM Fastening Solutions
JX-PF7MF spring-loaded captive panel screws are designed for applications where removable panels must remain equipped with their fastening hardware during installation, inspection, and maintenance.
The product combines a retained screw, spring-loaded operating mechanism, and flare-mount panel attachment.
Its primary engineering advantages are compatibility with close-edge mounting arrangements, relatively low installation force, and a flush backside mounting condition.
These characteristics make JX-PF7MF a candidate for compact industrial enclosures and equipment assemblies where conventional self-clinching fasteners may be unsuitable.
Product Construction and Operating Principle
A captive panel screw consists of a screw retained within a panel-mounted assembly.
The retention feature prevents the screw from becoming a separate loose component when disengaged from the mating thread.
A spring-loaded arrangement helps control the position of the screw during operation.
This can make it easier to align the cover and mating component during assembly or servicing.
The JX-PF7MF mounting design uses a flared retention feature to secure the assembly to a compatible panel.
The screw thread, travel, retention geometry, and spring characteristics must be verified using the approved product drawing.
Flare-Mount Installation Technology
Flare mounting secures a fastener by mechanically deforming a designated mounting feature against the panel.
The formed feature creates a retaining geometry that captures the panel.
This method differs from conventional self-clinching, which depends on controlled displacement of a ductile sheet material into the fastener's retention features.
A flare-mount fastener may therefore be suitable for certain panel materials or hardness conditions that would not support conventional self-clinching.
However, the panel must still be compatible with the required forming operation.
The installation tooling, hole preparation, and flare geometry must follow the approved JX-PF7MF specification.
Close Centerline-to-Edge Applications
Some sheet metal assemblies provide very little material between the mounting hole and the panel edge.
Conventional fastening methods may require greater edge distance to avoid panel deformation or loss of retention.
The JX-PF7MF flare-mount configuration is intended for applications where the mounting hole is positioned relatively close to the panel edge.
This can be useful in narrow enclosure flanges, compact access covers, and densely arranged fastening locations.
The permissible edge distance must be determined from the product drawing and verified for the selected panel material.
The design should not assume that a close-edge feature eliminates the need for edge-distance validation.
Low Installation Force
The JX-PF7MF design is intended to avoid the high installation forces associated with certain alternative fastening technologies.
Lower installation force can be advantageous when the panel is thin, relatively rigid, or sensitive to deformation.
However, the force required for a successful flare depends on the fastener geometry, panel thickness, material properties, and installation tooling.
Insufficient forming force may produce inadequate retention.
Excessive forming force may distort the panel or damage the fastener.
Production installation settings should therefore be established through sample trials and approved assembly procedures.
Flush Backside Mounting
The flare-mounted retainer is designed to provide a flush condition on the backside of the panel.
This is useful where the mounting surface must remain clear of protruding fastener features.
Potential applications include compact enclosure assemblies, sliding cover arrangements, and panels installed near internal structural components.
The flush mounting feature can help engineers manage the available space behind a cover.
Nevertheless, the complete installed geometry must be checked.
The fastener head, screw travel, mounting flange, and adjacent components may still require additional clearance.
Spring-Loaded Captive Screw Function
The spring-loaded screw is retained within the panel-mounted assembly.
When the screw is disengaged, the spring mechanism helps control its position.
This reduces the need to handle loose screws during routine maintenance.
For frequently serviced equipment, retained screws may improve assembly consistency and reduce the risk of hardware being misplaced.
The actual spring travel and retraction characteristics depend on the selected product configuration.
Spring loading does not automatically mean that the screw provides a positive locking mechanism.
The final joint must still be secured using the intended mating thread and tightening procedure.
Unified Inch-Thread Configuration
The supplied product designation identifies JX-PF7MF as a Unified version.
Unified screw threads are commonly specified according to ASME B1.1.
The applicable thread diameter, pitch, class of fit, and screw length must be confirmed from the JX-PF7MF drawing.
A Unified thread should not be substituted with an ISO metric thread based only on similar nominal diameters.
For example, nominal diameter similarity does not establish thread compatibility.
OEM procurement documents should identify the complete thread designation and matching receiving hardware.
Material Selection
The supplied material options include carbon steel and stainless steel.
Carbon steel candidates may include C45, C46, C20, and free-machining steel grades, depending on the manufacturing requirements.
Stainless steel candidates may include austenitic or martensitic grades, subject to engineering review.
These grades are not automatically interchangeable.
The required material must support the forming, machining, corrosion resistance, and mechanical performance of the completed captive screw assembly.
Different components within the assembly may require different material properties.
Material selection should be defined by the approved drawing and purchase specification.
Where appropriate, recognized ASTM, SAE, ISO, or EN material standards may be used.
Corrosion Protection and Surface Finishes
The required finish depends on the equipment operating environment.
Carbon steel components may be evaluated for protective metallic coatings.
Stainless steel may be considered where corrosion resistance is a priority.
Applicable ISO or ASTM coating specifications can be used where appropriate.
Coating thickness and surface treatment must not interfere with screw movement, spring operation, or thread engagement.
For outdoor or chemically exposed equipment, corrosion resistance should be verified against the actual operating conditions.
No specific corrosion rating should be assumed without supporting qualification data.
Industrial Application Solutions
Electronic Equipment Enclosures
Captive panel screws can secure removable covers on electronic equipment.
The retained screw arrangement helps prevent loose metal hardware from entering the enclosure during servicing.
Industrial Control Cabinets
Control cabinet covers may require repeated access for inspection, adjustment, or maintenance.
Flare-mount captive screws can provide a fastening option where panel material or edge geometry makes conventional self-clinching less suitable.
Telecommunications Equipment
Telecommunications enclosures frequently use compact access panels and serviceable covers.
Close-edge fastening capability can be useful where available flange width is restricted.
Industrial Machinery
Machine covers and removable inspection panels may benefit from captive screws that remain attached during servicing.
The fastening system must be evaluated for vibration, operating loads, and the intended maintenance procedure.
Instrumentation Housings
Precision instrumentation often requires controlled packaging dimensions.
A flush backside retainer may help reduce interference within compact housings.
Automotive and Transportation Equipment
Selected service covers, electrical housings, and non-safety-critical access panels may use captive fastening systems.
Suitability must be assessed against vibration, temperature, corrosion exposure, and applicable equipment requirements.
Medical and Laboratory Equipment
Removable equipment covers may require repeatable assembly and controlled hardware handling.
Material compatibility, cleaning exposure, and applicable regulatory requirements must be reviewed for the specific application.
Engineering Comparison: Flare Mount Versus Self-Clinching
Flare mounting and self-clinching are different mechanical attachment technologies.
Self-clinching relies on the controlled flow of a sufficiently ductile sheet material around the fastener's retention geometry.
Flare mounting relies on deformation of the fastener's designated mounting feature to create mechanical retention.
A flare-mounted product may be advantageous where panel hardness, edge distance, or installation force makes conventional self-clinching unsuitable.
However, flare mounting requires suitable access and tooling to form the retaining feature.
The selection should consider substrate material, panel thickness, mounting-hole geometry, production sequence, and required retention strength.
Engineering Comparison: Captive Screws Versus Loose Screws
Loose screws may have a lower initial component cost.
However, they must be handled separately during assembly and maintenance.
Captive screws can reduce the risk of lost hardware and may simplify repeated cover removal.
The economic benefit depends on service frequency, production volume, installation operations, and equipment design.
For OEM sourcing, the total installed cost should be evaluated rather than comparing only the individual screw price.
Panel Hole Design and Installation Control
The mounting-hole geometry is essential to flare-mount retention.
The hole must be prepared according to the approved fastener drawing.
Panel thickness, hole diameter, surface condition, and local flatness can influence installation results.
The installation tooling must support the panel and form the retainer consistently.
Incorrect tooling may produce an incomplete flare or damage the surrounding sheet.
The engineering team should verify the formed retainer geometry and inspect the panel for distortion or cracking.
Any required countersink, chamfer, or special hole preparation must be taken directly from the approved drawing.
No universal hole preparation should be assumed for every flare-mount captive screw.
Fastener Retention and Mechanical Reliability
The flare-mounted assembly must remain securely attached to the panel during normal use.
Relevant performance considerations include resistance to axial displacement, rotation, and damage from repeated screw operation.
The completed fastening joint must also withstand the intended service loads.
The retention performance of the mounting feature and the strength of the threaded joint are separate engineering considerations.
An adequately retained panel screw may still fail to secure the assembly if the mating thread or tightening procedure is incorrect.
Mechanical testing should reflect the actual panel material, thickness, and equipment operating conditions.
Vibration and Repeated Maintenance
Frequently opened panels can expose captive fasteners to repeated handling and screw engagement.
The screw should operate smoothly without excessive binding or looseness.
The mating thread must provide suitable engagement for the required tightening conditions.
Vibration may require additional joint-design measures depending on the equipment.
The presence of a captive screw does not by itself provide vibration-resistant thread locking.
For demanding environments, the OEM should evaluate the complete joint and any necessary locking features.
Common Engineering Failure Modes
Incomplete Flaring
Insufficient forming or incorrect tooling can reduce mounting retention.
Panel Distortion
Excessive installation force or inadequate support can deform the mounting sheet.
Insufficient Edge Clearance
An unsuitable hole position can weaken the local panel structure.
Thread Damage
Misalignment or excessive tightening torque can damage the mating threads.
Restricted Screw Travel
Contamination, incorrect dimensions, or unsuitable coatings may interfere with the spring-loaded mechanism.
Corrosion and Wear
Environmental exposure and repeated operation may affect component performance.
These risks should be addressed through correct product selection, approved tooling, installation validation, and appropriate inspection.
Technical Specifications
Product name: Spring-Loaded Flare-Mount Captive Panel Screw.
Model: JX-PF7MF.
Thread system: Unified inch thread, subject to drawing verification.
Fastener function: Retained screw for removable panel fastening.
Operating mechanism: Spring-loaded captive screw.
Mounting method: Flare mounting.
Mounting characteristics: Close-edge suitability and relatively low installation force.
Backside condition: Flush mounting design.
Material options: Carbon steel or stainless steel, according to approved specifications.
Panel compatibility: Dependent on panel geometry, thickness, material properties, and validated flare installation.
Thread sizes: According to the applicable JX-PF7MF technical drawing.
Screw lengths: According to the selected specification.
Mounting-hole dimensions: According to the approved product drawing.
Installation force: To be established through approved tooling and application testing.
Surface treatment: According to customer requirements and manufacturing feasibility.
Custom dimensions: Subject to engineering review.
Technical documentation: Refer to the corresponding PDF and CAD drawings, pages 59–60, after confirming that they match the JX-PF7MF Unified configuration.
Design Standards and Engineering Documentation
Unified screw thread requirements may be specified using ASME B1.1.
Dimensional tolerances and engineering drawings may reference applicable ASME or ISO standards.
Material and surface-treatment requirements may be established using appropriate ASTM, SAE, EN, or ISO specifications.
The JX-PF7MF product should not be represented as certified to a specific standard unless that compliance has been verified.
For OEM projects, the approved product drawing remains the controlling technical document.
OEM Design and Qualification Checklist
Before selecting a flare-mount captive panel screw, engineers should identify the panel material and thickness.
The mounting-hole geometry and available edge distance must be confirmed.
The required backside clearance should be defined.
The selected screw thread must match the mating component.
The available installation access and forming-tool arrangement must be checked.
The assembly should be evaluated for service frequency, vibration, corrosion exposure, and operating loads.
Prototype installation should confirm adequate retention without unacceptable panel distortion.
The final assembly should be tested using the actual production panel and mating hardware.
Frequently Asked Questions
What is a flare-mount captive panel screw?
A flare-mount captive panel screw is a retained screw assembly secured to a panel by mechanically forming a mounting feature against the panel.
What is the main advantage of JX-PF7MF?
Its principal features are spring-loaded captive operation, suitability for close-edge mounting, relatively low installation force, and a flush backside design.
Can JX-PF7MF be installed in hard panels?
The flare-mount design can accommodate a broad range of panel hardness levels, but installation suitability must be verified for the actual panel material and geometry.
Is JX-PF7MF a self-clinching fastener?
No. Its specified attachment method is flare mounting, which differs from conventional self-clinching.
Does the spring automatically lock the panel?
No. The spring assists screw positioning. The threaded connection must still be engaged and tightened according to the assembly requirements.
Can Unified and metric captive screws be substituted?
No. The complete thread designation and mating hardware must match.
Can custom versions be supplied?
Custom dimensions, materials, and finishes can be reviewed according to customer drawings and manufacturing feasibility.
Related Products and Internal Linking
For alternative panel attachment methods, explore JX-PFC2 / JX-PFS2 Spring-Loaded Captive Panel Screws.
For compact spring-loaded fastening systems, review JX-PFC2P Tool-Only Captive Panel Screws.
For flush mounting solutions, see JX-PR10 Self-Clinching Flush-Mounted Retainers.
For other panel screw configurations, explore JX-PFHV Captive Panel Screws.
For additional engineering options, visit the Captive Panel Fasteners and Specialty Fastening Solutions product categories.
These references should link to the corresponding verified pages on www.juxinfasteners.com.
OEM Procurement and Supply Chain Considerations
Purchasing teams should confirm that the quotation covers the correct flare-mount configuration rather than a visually similar self-clinching assembly.
The approved specification should identify the screw thread, screw length, retainer dimensions, material, surface finish, and mounting-hole requirements.
For production sourcing, the supplier evaluation should consider dimensional consistency, installation compatibility, sample approval, and inspection requirements.
Customer-specific documentation, traceability, and packaging requirements should be established during quotation.
Annual demand, order quantities, and expected delivery schedules should be included in the RFQ.
Request an OEM Quotation
Juxin Fasteners supports OEM sourcing inquiries for JX-PF7MF spring-loaded flare-mount captive panel screws and related industrial fastening solutions.
Please provide your required model, drawing, Unified thread specification, panel material, panel thickness, mounting-hole details, finish requirements, estimated order quantity, and annual demand.
Our team can review the technical requirements and provide a quotation based on the confirmed specification.
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Juxin Fasteners – Captive Panel Fasteners and Industrial OEM Assembly Solutions.
Product Packaging
Packaging and Export Protection
Juxin Fasteners provides protective export packaging for JX-PF7MF spring-loaded flare-mount captive panel screws.
Inner protection may include poly foam, protective bags, or small boxes, followed by reinforced export cartons and palletizing when required.
Available carton dimensions include 29 × 19 × 19.5 cm and 23.5 × 17.5 × 8 cm, subject to product size and packing quantity.
The supplied pallet dimension is 215 × 100 × 90 cm, subject to the final shipment arrangement.
Packaging is designed to help protect the screw threads, spring-loaded mechanism, and flare-mount features during handling, storage, and transportation.
Carton labels can identify the product model, specification, material, batch number, and quantity according to agreed customer requirements.
Customized packaging options include private labeling, barcodes, specified packing quantities, protective separators, custom carton dimensions, and customer-defined pallet configurations.
Final packaging arrangements, quantities, and any additional packaging costs are confirmed according to the purchase order and shipment requirements.
Product Pictures
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY