Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809
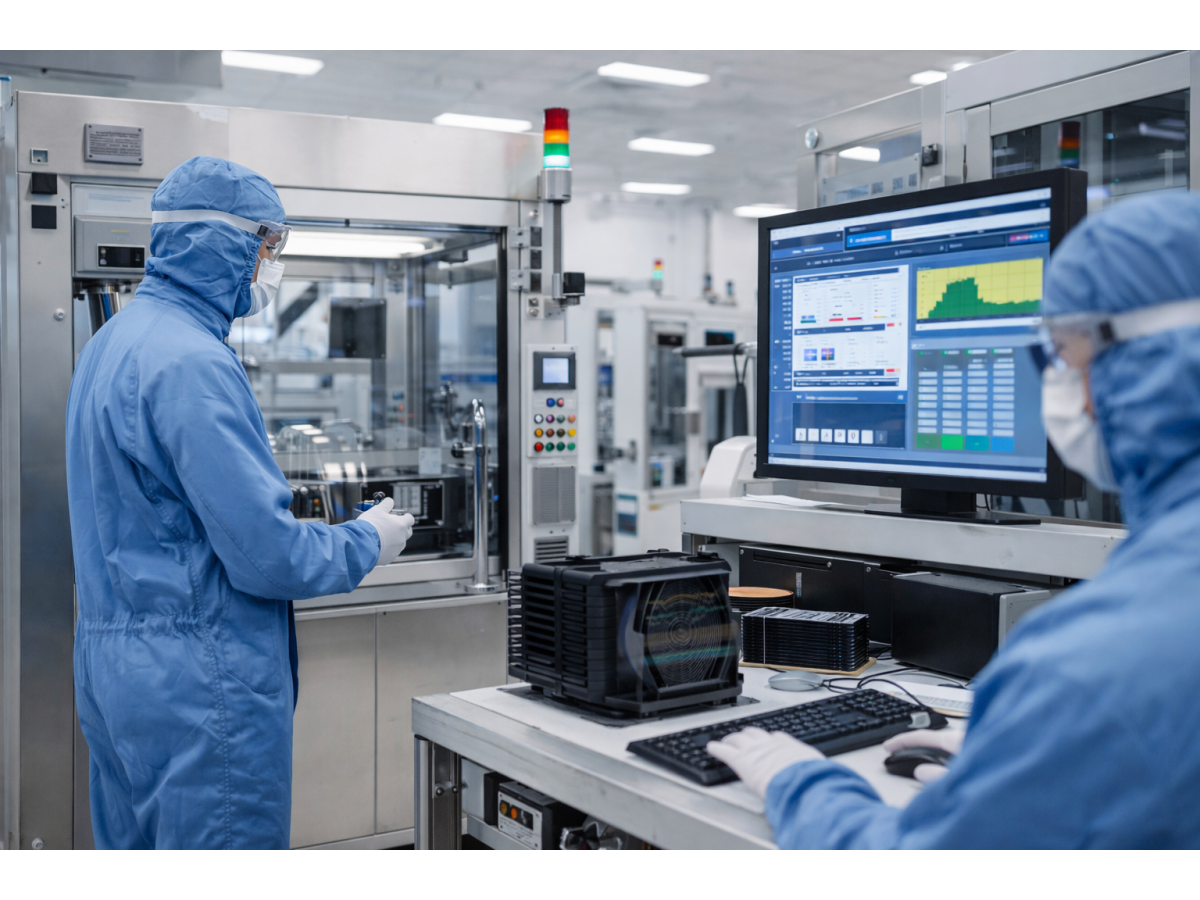
Semiconductor manufacturing equipment presents one of the most demanding environments for polymer fastening hardware.
Wafer fabrication tools, wet process equipment, cleanroom automation systems, inspection equipment, electronic control modules, vacuum systems,
and chemical-delivery assemblies may require combinations of chemical resistance, electrical isolation, low metallic contamination risk, dimensional stability,
controlled particle generation, thermal performance, and vacuum compatibility.
Product Specification
Semiconductor manufacturing equipment presents one of the most demanding environments for polymer fastening hardware.
Wafer fabrication tools, wet process equipment, cleanroom automation systems, inspection equipment, electronic control modules, vacuum systems,
and chemical-delivery assemblies may require combinations of chemical resistance, electrical isolation, low metallic contamination risk, dimensional stability,
controlled particle generation, thermal performance, and vacuum compatibility.
For these applications, selecting a plastic fastener is not simply a question of replacing a stainless steel screw with a polymer screw.
The correct engineering sequence is:
Process Environment → Contamination Requirement → Chemical Exposure → Temperature → Vacuum Level → Mechanical Load → Material → Fastener Geometry → Validation
Depending on the equipment zone, engineering polymers such as PA66, POM, PVDF, and PEEK may be considered for screws, nuts, washers, spacers, standoffs, bushings,
cable-management components, PCB supports, and drawing-specific molded components.
However, the suitability of a polymer family does not automatically establish that a finished fastener is cleanroom-qualified, vacuum-qualified,
semiconductor-grade, low-outgassing, plasma-resistant, or suitable for direct exposure to a specific process chemical.
Those requirements must be evaluated at the resin-grade, finished-component, cleaning, packaging, and application level.
Juxin Fasteners supports standard and custom plastic fasteners for industrial equipment applications,
including selected semiconductor manufacturing equipment and cleanroom automation projects.
Engineering review can begin from an existing OEM part number, 2D drawing, 3D CAD model, physical sample, material specification, or application requirement.
Plastic fastening and insulating hardware may be considered in multiple equipment zones, including:
wet process equipment;
chemical-delivery assemblies;
wafer handling equipment;
cleanroom automation;
electrical control cabinets;
sensor assemblies;
PCB mounting systems;
equipment enclosures;
cable and wire routing;
inspection and metrology equipment;
vacuum-supporting assemblies;
laboratory and process-development equipment.
The critical point is that these environments are not interchangeable.
A nylon standoff inside a protected electrical control cabinet faces completely different requirements from a
PEEK screw located near a vacuum process module or a PVDF component exposed to process chemicals.
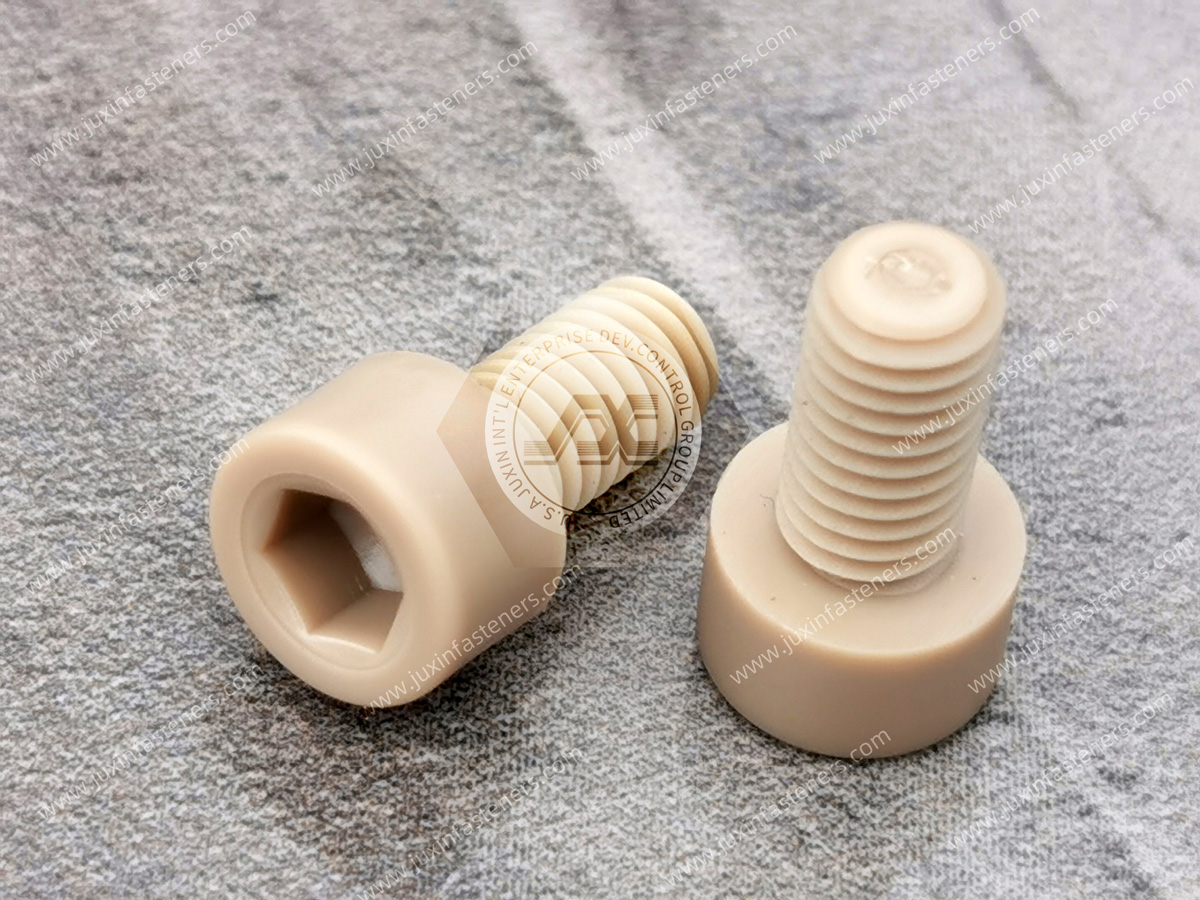
The phrase “semiconductor equipment plastic fastener” describes an application market—not a material specification.
Consider four examples:
The fastener may primarily require:
electrical isolation;
flame-performance consideration;
mechanical retention;
vibration resistance.
The component may require:
specific chemical compatibility;
low metallic contamination risk;
controlled extractables;
suitable temperature performance.
The main requirements may include:
wear resistance;
dimensional stability;
controlled particle generation;
repeated mechanical cycling.
The design may prioritize:
outgassing behavior;
temperature;
dimensional stability;
vacuum exposure;
contamination control.
Therefore:
Industry Name ≠ Application Environment ≠ Material Requirement
The exact equipment zone must be identified before material selection.
Wet process systems may contain aggressive acids, bases, solvents, oxidizers, ultrapure water, and other process chemistries.
Polymer fasteners can be considered for:
equipment covers;
support structures;
chemical-resistant mounting assemblies;
piping supports;
sensor mounting;
selected fluid-system hardware.
Potential materials may include PVDF, PEEK, and other application-specific engineering polymers.
Chemical compatibility must be evaluated against the actual process conditions, including:
chemical identity;
concentration;
temperature;
exposure duration;
mechanical stress;
cleaning process.
A polymer described generically as “chemical resistant” should not be assumed compatible with every semiconductor process chemistry.
A more useful semiconductor fastener specification includes:
| Parameter | Required Information |
|---|---|
| Chemical | Exact chemical or mixture |
| Concentration | Operating concentration |
| Temperature | Normal and maximum |
| Exposure | Continuous, intermittent, splash or vapor |
| Duration | Expected service life |
| Mechanical Load | Tension, compression, shear or preload |
| Cleaning | Cleaning chemistry and process |
| Purity | Contamination / extractables requirements |
For example, evaluating a PVDF or PEEK fastener for a wet-process assembly should begin with the actual chemistry and service conditions—not simply the material name.
Vacuum applications introduce another set of requirements.
Under reduced pressure, volatile constituents within polymer materials can be released from the component.
Depending on the vacuum level and process sensitivity, engineers may need to consider:
total outgassing behavior;
condensable volatile materials;
absorbed moisture;
resin additives;
pigments;
fillers;
processing aids;
cleaning residues;
packaging contamination.
This means that:
PEEK Material ≠ Automatically Low-Outgassing Finished Fastener
Even where the base polymer has favorable vacuum characteristics, the exact resin grade, additives, manufacturing process, post-processing,
cleaning, handling, and packaging can influence finished-component performance.
For critical vacuum applications, the customer should specify the required outgassing test method and acceptance criteria.
Where applicable, standardized vacuum-material screening methods such as ASTM E595 may be referenced by the equipment designer,
but applicability and acceptance limits should be defined by the project specification.
Vacuum engineers commonly distinguish between several material behaviors rather than treating “outgassing” as a single property.
Depending on the qualification method, evaluation may include parameters such as:
Total Mass Loss (TML);
Collected Volatile Condensable Materials (CVCM);
moisture-related mass loss;
application-specific vacuum testing.
The important sourcing principle is:
Do not qualify a semiconductor vacuum fastener from generic resin literature alone when the finished component requires documented vacuum performance.
The validation level should match the actual process risk.
A plastic component does not become “cleanroom compatible” simply because it is manufactured from PEEK, PVDF, POM, or nylon.
Particle generation can result from:
thread engagement;
repeated insertion;
sliding contact;
abrasion;
trimming;
molding flash;
surface damage;
packaging;
transportation;
installation.
For threaded polymer components, engineers should pay particular attention to mating-thread behavior.
Repeated tightening and loosening can generate polymer wear particles even when the base material itself is suitable for the surrounding environment.
Therefore cleanroom component qualification may need to consider:
Material + Surface Condition + Geometry + Assembly Method + Cleaning + Packaging + Installation
ISO 14644 is widely used for cleanroom classification and controlled-environment management.
However, an important distinction is:
An ISO-classified cleanroom does not automatically certify every component used inside it.
Likewise:
A component manufactured in a clean environment is not automatically qualified for every semiconductor process environment.
Equipment OEMs should define component-specific requirements for:
particulate cleanliness;
ionic contamination;
organic contamination;
metallic contamination;
cleaning;
packaging;
handling.
These requirements may vary substantially between equipment platforms and process nodes.
PEEK is a high-performance engineering thermoplastic that may be considered for demanding semiconductor-equipment applications because of its combination of:
mechanical strength;
elevated-temperature capability;
dimensional stability;
chemical resistance;
electrical insulation;
relatively favorable vacuum behavior for selected grades and applications.
Potential components include:
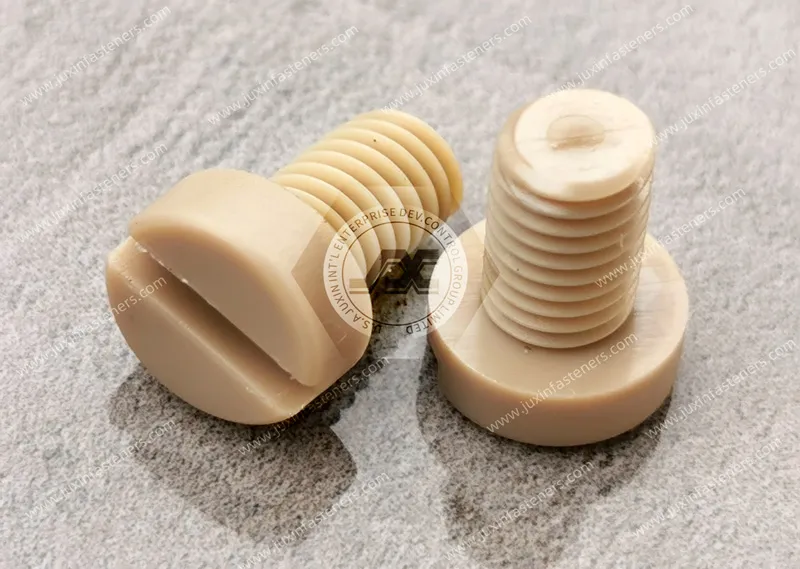
PEEK screws;
PEEK nuts;
PEEK washers;
PEEK spacers;
PEEK standoffs;
custom PEEK components.
Applications may include selected:
process equipment;
vacuum-support assemblies;
analytical equipment;
high-temperature equipment;
chemical-handling equipment.
However, suitability must be confirmed against the actual process specification.
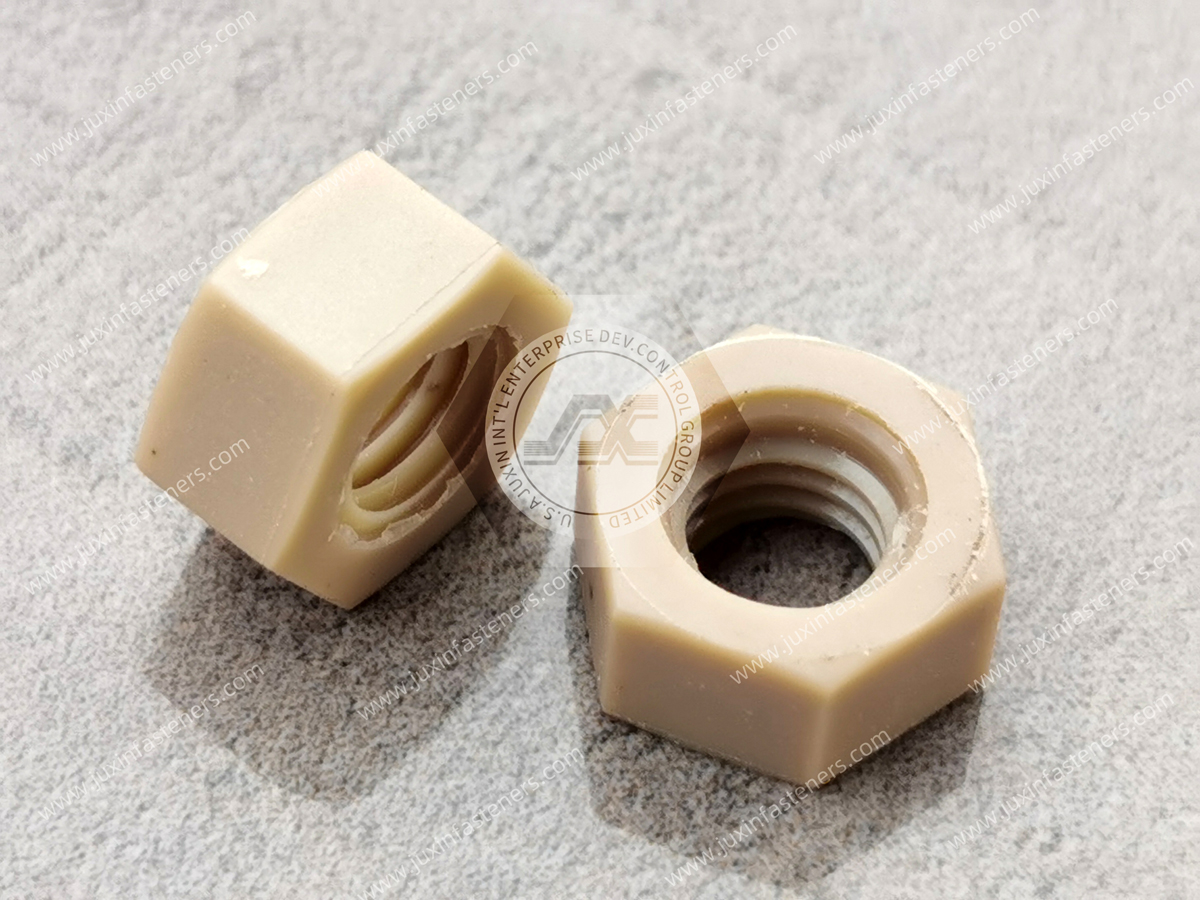
PVDF can be considered where chemical resistance and electrical insulation are major design requirements.
Potential semiconductor-equipment applications include selected:
wet process equipment;
chemical-handling systems;
fluid equipment;
sensor mounting;
corrosive-environment assemblies.
Chemical resistance depends on the specific chemical, concentration, temperature, stress state, and exposure duration.
POM may be useful in cleanroom automation and precision mechanical systems where engineers prioritize:
dimensional stability;
low moisture absorption;
low friction;
wear resistance;
mechanical repeatability.
Potential applications can include:
guides;
supports;
positioning components;
selected fasteners;
automation mechanisms.
POM should not automatically be selected for aggressive chemical or vacuum applications without application-specific evaluation.
PA66 remains useful for many protected semiconductor-equipment zones, particularly:
control cabinets;
PCB assemblies;
cable management;
electrical isolation;
equipment enclosures.
Potential components include:
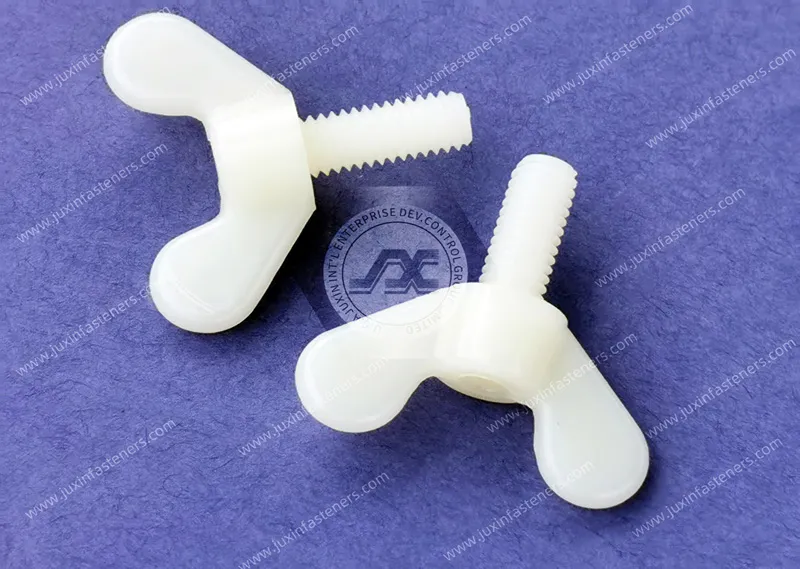
Nylon Machine Screws;
nylon nuts;
nylon washers;
Insulating Shoulder Washers;
Plastic Spacers and Standoffs;
PCB supports;
cable clamps;
snap bushings.
Because PA66 absorbs moisture, engineers should consider dimensional change and property variation where precision tolerances or controlled environments are involved.
For semiconductor equipment sourcing:
PEEK ≠ One Material
PVDF ≠ One Material
PA66 ≠ One Material
Different resin grades can contain different:
fillers;
pigments;
additives;
processing aids;
reinforcement systems.
These differences can affect:
mechanical performance;
chemical resistance;
electrical properties;
particle generation;
contamination;
outgassing.
Therefore the material specification should identify the required grade where the application is sensitive.
One reason engineers consider polymer fasteners in semiconductor equipment is the possibility of reducing metallic contact or metallic contamination sources in selected assemblies.
Plastic fasteners can also provide electrical isolation between:
metal panels;
sensors;
electronic modules;
PCB assemblies;
equipment structures.
However:
Polymer Fastener ≠ Zero Contamination Risk
Contamination can originate from:
raw materials;
pigments;
fillers;
manufacturing equipment;
handling;
cleaning;
packaging.
Where trace-metal limits are critical, the equipment manufacturer should define the required analytical method and acceptance criteria.
Gemini's original assumption that a polymer can simply be described as “plasma resistant” is too broad for semiconductor equipment design.
Polymer behavior can vary according to:
plasma chemistry;
ion energy;
temperature;
exposure time;
pressure;
location within the process chamber.
Possible degradation mechanisms include:
erosion;
surface roughening;
embrittlement;
mass loss;
particle generation.
Therefore a plastic fastener intended for direct plasma exposure requires application-specific material evaluation.
Do not infer plasma compatibility solely from general chemical-resistance data.
Polymer fasteners typically have different coefficients of thermal expansion from:
stainless steel;
aluminum;
ceramics;
quartz;
glass;
silicon-related components.
During thermal cycling, differential expansion can change:
clamp load;
alignment;
joint clearance;
bearing pressure;
thread engagement.
This is particularly important in:
metrology equipment;
inspection systems;
optical systems;
wafer positioning equipment;
precision sensor assemblies.
Where alignment is critical, the entire joint stack should be analyzed rather than considering the fastener independently.
Plastic fasteners exhibit viscoelastic behavior.
Under sustained preload, polymer screws, washers, or clamped plastic components can experience:
creep;
stress relaxation;
loss of clamp load.
Temperature can accelerate these effects.
Therefore a polymer fastener should not automatically replace a metal fastener in a high-preload structural joint.
Engineers should evaluate:
required clamp load;
service temperature;
bearing area;
thread engagement;
maintenance requirements;
joint stiffness.
For critical assemblies, long-term joint validation is more meaningful than short-term room-temperature tensile data alone.
Plastic fastening hardware can provide useful electrical isolation in semiconductor equipment.
Potential components include:
For selected low-load electrically isolated threaded joints.
For radial and axial isolation where a metal screw passes through a conductive panel.
For maintaining controlled distance between electronic modules, PCBs, and chassis structures.
For tool-free mounting of selected electronic assemblies.
For wire routing and protection within equipment enclosures.
The appropriate solution depends on voltage, temperature, mechanical load, creepage, clearance, and applicable equipment safety requirements.
Potential causes:
polymer creep;
stress relaxation;
differential thermal expansion;
inadequate bearing area.
Potential causes:
incompatible chemical;
excessive temperature;
environmental stress cracking;
incorrect resin grade.
Potential causes:
repeated assembly;
excessive torque;
poor mating-thread finish;
abrasive filler;
cross-threading.
Potential causes:
moisture absorption;
chemical swelling;
temperature;
residual molding stress.
Potential causes:
incorrect resin grade;
additives;
absorbed moisture;
cleaning residue;
surface contamination;
packaging contamination.
These examples illustrate why semiconductor fastener qualification must evaluate the complete component rather than relying on the polymer name alone.
| Application | Primary Concern | Potential Polymer Direction |
|---|---|---|
| Electrical Cabinet | Isolation / Mechanical Retention | PA66 / application-specific polymer |
| PCB Mounting | Isolation / Spacing | PA66 / POM / application-specific polymer |
| Wet Process Equipment | Chemical Compatibility | PVDF / PEEK / application-specific polymer |
| Cleanroom Automation | Wear / Particle Control | POM / PEEK / application-specific polymer |
| Vacuum Equipment | Outgassing / Temperature | PEEK / qualified material |
| Precision Equipment | Dimensional Stability | POM / PEEK / application-specific polymer |
| Cable Management | Isolation / Routing | PA66 / application-specific polymer |
This matrix is an initial screening tool—not a substitute for application validation.
A second-source fastener should not be approved from dimensions alone.
A robust comparison should evaluate:
Part geometry
Critical dimensions and tolerances
Thread specification
Polymer family
Exact resin grade where required
Filler and additive requirements
Operating temperature
Chemical exposure
Vacuum environment
Cleanliness requirements
Particle-generation requirements
Metallic contamination limits
Cleaning process
Packaging requirements
Documentation and traceability
A dimensionally interchangeable fastener can still fail semiconductor-equipment qualification if its material, cleanliness, or environmental behavior differs from the approved component.
Provide:
OEM part number;
existing supplier part number;
2D drawing;
3D CAD model;
physical sample.
Specify whether the component is located in:
wet process equipment;
vacuum equipment;
cleanroom automation;
electrical cabinet;
PCB assembly;
chemical-handling equipment;
inspection equipment;
another process zone.
Specify:
PA66;
POM;
PVDF;
PEEK;
other polymer;
exact resin grade where required;
filler;
color;
purity requirements.
Provide:
chemical;
concentration;
temperature;
exposure duration;
continuous or intermittent exposure.
Where applicable, provide:
operating pressure;
temperature;
outgassing specification;
test method;
acceptance criteria.
Specify:
cleanroom environment;
particle requirement;
metallic contamination limits;
ionic contamination limits where applicable;
cleaning requirements;
packaging requirements.
Provide:
installation torque;
clamp load;
tensile load;
shear load;
vibration;
assembly cycles.
Evaluate:
dimensions;
thread fit;
assembly behavior;
mating-component compatibility;
surface quality.
Where required, validate:
chemical exposure;
vacuum behavior;
thermal cycling;
particle generation;
mechanical performance;
contamination requirements.
Following engineering approval, procurement can define:
production quantity;
annual demand;
lot traceability;
packaging;
documentation;
delivery requirements.
For semiconductor equipment OEMs, procurement should distinguish between three sourcing levels.
Used in protected equipment zones where standard material and dimensional requirements are sufficient.
Used where dimensions, polymer grade, tolerance, or geometry are controlled by the equipment OEM.
Used where the project additionally requires documented:
chemical compatibility;
vacuum performance;
cleanliness;
contamination limits;
specialized cleaning;
controlled packaging.
The supplier qualification process should match the risk level of the component.
This prevents both under-specification and unnecessary qualification cost.
Semiconductor equipment manufacturers may require components that cannot be sourced from standard catalogs.
Potential custom components include:
PEEK screws;
PVDF screws;
specialized polymer nuts;
insulating washers;
precision spacers;
custom standoffs;
sensor supports;
cable-management hardware;
enclosure clips;
drawing-specific molded plastic components.
Juxin Fasteners can support drawing-based sourcing through:
2D drawing review;
3D CAD review;
physical sample comparison;
dimensional review;
material discussion;
DFM review;
sample evaluation;
production sourcing.
Material availability, grade, documentation, cleanliness requirements, and validation requirements should be confirmed for each project.
For efficient engineering and sourcing review, provide:
OEM part number;
current supplier part number;
2D drawing;
3D CAD;
physical sample;
photographs.
polymer family;
exact resin grade where required;
filler;
reinforcement;
color;
purity requirements.
thread size;
length;
critical dimensions;
tolerances;
mating-component dimensions.
wet process;
vacuum;
cleanroom automation;
electrical enclosure;
PCB assembly;
chemical handling;
other.
chemical identity;
concentration;
temperature;
exposure duration.
operating pressure;
temperature;
required outgassing test;
acceptance limits.
particle limits;
metallic contamination limits;
ionic contamination requirements;
cleaning requirements;
packaging requirements.
installation torque;
clamp load;
tensile / shear load;
vibration;
assembly cycles.
material documentation;
lot traceability;
RoHS;
REACH;
customer-specific documentation.
sample quantity;
prototype quantity;
production quantity;
estimated annual usage;
delivery schedule.
Related Juxin Fasteners engineering solutions include:
PEEK Screws and Fasteners for selected high-performance applications;
Nylon Machine Screws for protected electrically isolated assemblies;
Insulating Shoulder Washers for screw-shank and under-head isolation;
Plastic Spacers and Standoffs for electronic module spacing;
Snap-Fit Circuit Board Supports for PCB mounting;
Nylon Cable Clamps for internal wire routing;
Nylon Snap Bushings for cable protection through metal panels;
Custom Molded Plastic Fasteners for proprietary semiconductor equipment components.
These components should be selected according to the equipment zone and process environment rather than from catalog dimensions alone.
Juxin Fasteners supports equipment manufacturers, engineering teams, procurement organizations, supplier-development teams,
contract manufacturers, and industrial sourcing organizations requiring standard or drawing-specific plastic fastening components for semiconductor manufacturing equipment,
cleanroom automation, precision instrumentation, electronics manufacturing equipment, laboratory systems, and related industrial applications.
For semiconductor-equipment projects, the recommended sourcing path is:
Existing Part / Drawing / Sample → Equipment Zone Review → Material & Environmental Review → Chemical / Vacuum / Cleanliness Requirements
→ Candidate Component → Sample Evaluation → Application Validation → Documentation Review → Second-Source Qualification → Production RFQ
This workflow can support:
new equipment development;
metal-to-polymer conversion;
electrical-isolation projects;
corrosion reduction;
second-source qualification;
supplier consolidation;
obsolete-component replacement;
custom component development.
For applications involving semiconductor process chemicals, high vacuum, plasma exposure, trace-metal contamination limits, ultra-clean requirements,
or controlled particle-generation specifications, provide the exact engineering and validation requirements during RFQ review.
Do not rely on a generic polymer designation alone for process-critical qualification.
Send us your existing part number, 2D drawing, 3D CAD model, physical sample, resin requirement, chemical environment, temperature,
vacuum level, cleanliness specification, mechanical requirements, documentation requirements, sample quantity, production quantity, and estimated annual usage for technical review.
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Product Packaging
Packaging Standard
At Juxin Fasteners, we apply standardized export packaging to ensure product protection, traceability, and compliance with international logistics requirements.
1. Standard Export Packaging
Unless otherwise specified, all products will be packed according to our factory standard export packaging, which includes:
Moisture-resistant inner protection
Poly bag or small box packing as required
Reinforced export cartons
Clear labeling with part number, specification, batch number, and quantity
Palletizing for sea or air shipment when necessary
Our standard packaging is designed to ensure safe transportation, efficient warehousing, and long-distance international shipping.
2. Customized Packaging Options
We also provide customized packaging solutions according to customer requirements, including but not limited to:
Private labeling
Customized barcodes
Specific carton dimensions
Retail packaging
Special pallet configuration
Customer-specific marking and identification
So that you know, customized packaging may involve additional costs and extended lead time depending on the complexity of the requirements.
3. Compliance & Quality Assurance
All packaging processes are controlled under our ISO 9001 quality management system to ensure consistency, traceability, and product integrity throughout the supply chain.
Product Pictures
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY