Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

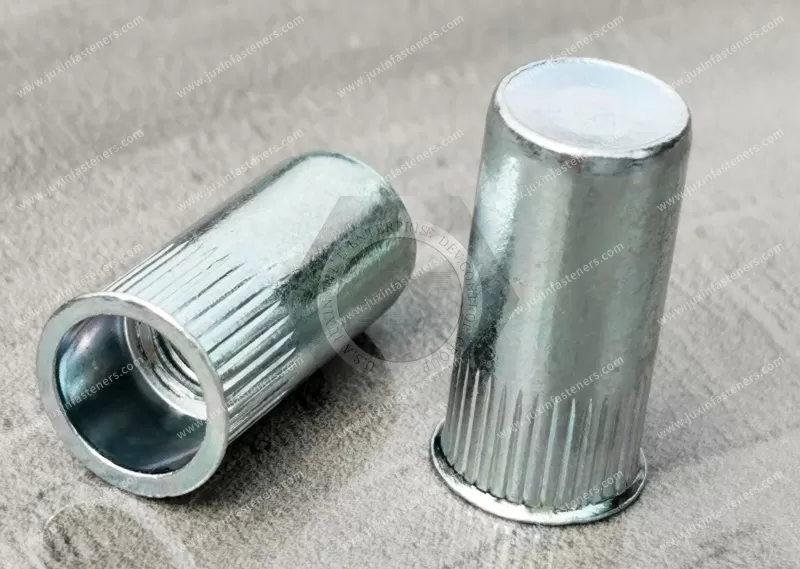
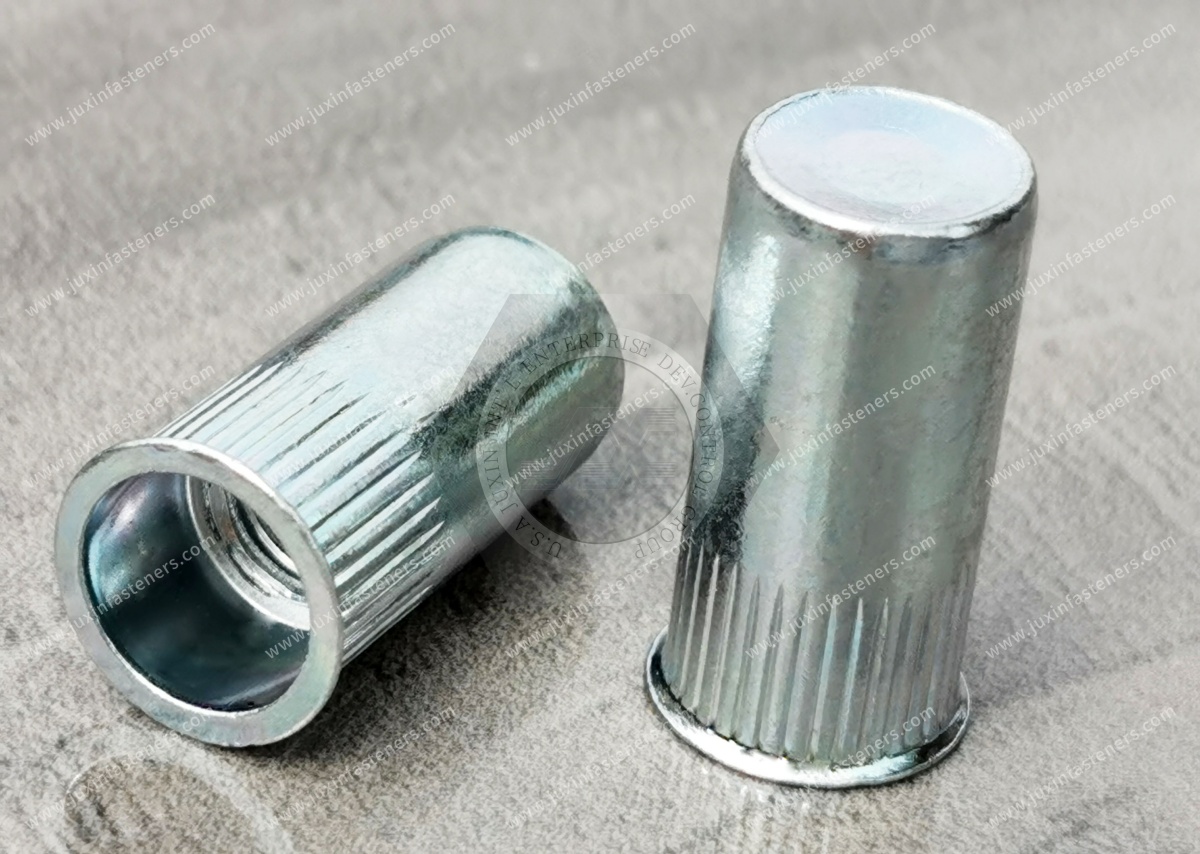
JUXIN FASTENERS manufactures blue zinc-plated carbon steel blind rivet nuts with thin heads, closed-end barrels, and knurled round bodies for low-profile threaded fastening in sheet metal, hollow sections, and industrial assemblies requiring one-sided installation.
The thin flange reduces head projection, while the knurled body helps resist insert rotation. The closed-end barrel prevents screws from passing through the insert end and eliminates the direct rear opening.
Product Features
Metric thread sizes: M3, M4, M5, M6, M8, M10, M12
UNC thread sizes: #6-32, #8-32, 1/4"-20, 5/16"-18, 3/8"-16, 1/2"-13
Material: Carbon steel
Surface finish: Blue zinc plating
Grip range: 0.5–5.0 mm (approx. 0.020–0.197 in) across the product family, depending on configuration
Head style: Thin head / Low-profile flange
Body style: Knurled round body
End style: Closed end
Installation: One-sided blind installation
Typical applications include electrical enclosures, control cabinets, machinery covers, compact equipment housings, tubular structures, and OEM sheet-metal assemblies requiring reduced flange projection and improved rotational resistance.
Product Specification
Technical Specifications — Low-Profile Closed-End Knurled Steel Rivet Nuts
Product Identification
| Parameter | Specification |
|---|---|
| Product Name | Low-Profile Closed-End Knurled Steel Blind Rivet Nuts |
| Alternative Names | Thin Head Closed-End Rivet Nuts, Small Flange Ribbed Nutserts |
| Material | Steel |
| Head Style | Thin Head / Low Profile |
| Body Style | Round Knurled Body |
| End Configuration | Closed End |
| Surface Treatment | Blue Zinc Plating |
| Metric Sizes | M3, M4, M5, M6, M8, M10, M12 |
| Published Series Grip Range | 0.5–5.0 mm |
| Approximate Inch Range | 0.020–0.197 in |
| Installation | One-Sided Blind Rivet Nut Setting |
| Hole Diameter | According to approved drawing |
| Flange Dimensions | According to approved drawing |
| Body Length | According to approved drawing |
| Closed-End Depth | According to approved drawing |
| Individual Grip Range | According to approved drawing |
| Custom Sizes | Subject to technical review |
Metric Thread Specifications
The following are ISO metric coarse thread designations.
| Thread Size | Pitch (mm) | Nominal Diameter (in) |
|---|---|---|
| M3 × 0.5 | 0.50 | 0.1181 |
| M4 × 0.7 | 0.70 | 0.1575 |
| M5 × 0.8 | 0.80 | 0.1969 |
| M6 × 1.0 | 1.00 | 0.2362 |
| M8 × 1.25 | 1.25 | 0.3150 |
| M10 × 1.5 | 1.50 | 0.3937 |
| M12 × 1.75 | 1.75 | 0.4724 |
Applicable thread references include ISO 261, ISO 724, and ISO 965.
Final thread tolerance and individual product dimensions must follow the approved technical drawing.
Unified Inch Thread Options for US OEM Inquiries
Unified inch threads may be reviewed for drawing-based custom sourcing requirements.
The following are commonly used Unified thread designations, not confirmed standard sizes for this particular product.
| Unified Thread | Series | Availability |
|---|---|---|
| #4-40 | UNC | Subject to confirmation |
| #6-32 | UNC | Subject to confirmation |
| #8-32 | UNC | Subject to confirmation |
| #10-24 | UNC | Subject to confirmation |
| #10-32 | UNF | Subject to confirmation |
| 1/4-20 | UNC | Subject to confirmation |
| 5/16-18 | UNC | Subject to confirmation |
| 3/8-16 | UNC | Subject to confirmation |
| 1/2-13 | UNC | Subject to confirmation |
Unified thread specifications should reference ASME B1.1.
Metric and Unified threads are not interchangeable.
Grip Range — Metric and Inch Reference
The published series grip range is 0.5–5.0 mm.
| Panel Thickness (mm) | Approximate Thickness (in) |
|---|---|
| 0.5 | 0.0197 |
| 1.0 | 0.0394 |
| 1.5 | 0.0591 |
| 2.0 | 0.0787 |
| 2.5 | 0.0984 |
| 3.0 | 0.1181 |
| 4.0 | 0.1575 |
| 5.0 | 0.1969 |
These values are conversion references only.
The appropriate grip interval for each individual rivet nut must be confirmed from the technical drawing.
Engineering Selection Guide
1. Closed-End Versus Open-End Rivet Nuts
Closed-end rivet nuts provide an enclosed threaded cavity, while open-end rivet nuts allow the mating screw to pass through the insert.
Closed-end configurations may be preferred when limiting direct backside contamination is important.
Open-end configurations may be more suitable where additional screw penetration is required.
For closed-end products, screw length and available internal thread depth must be verified to prevent bottoming out.
2. Closed-End Does Not Automatically Mean Watertight
The closed barrel blocks a direct passage through the insert body, but it does not automatically seal the interface between the flange and the mounting panel.
If water or air sealing is required, engineers should specify:
Maximum allowable leakage
Environmental exposure
Mounting hole tolerance
Flange sealing requirements
Optional sealing washer or gasket
Assembly test conditions
Sealing performance must be validated on the completed joint.
3. Low-Profile Versus Large-Flange Designs
A thin head reduces protrusion above the panel.
A large flange provides a wider load-bearing surface and may improve resistance to pull-through in suitable applications.
The choice depends on assembly clearance, panel strength, installation force, and mechanical load requirements.
4. Knurled Body and Spin-Out Resistance
Knurling is designed to improve mechanical engagement between the rivet nut and mounting material.
However, excessive hole clearance, insufficient setting force, or unsuitable panel properties can reduce spin-out performance.
For OEM applications, spin-out torque should be verified using representative mounting materials and installation conditions.
5. Panel Thickness and Grip Range
The specified grip range must correspond to the actual thickness of the mounting material.
For multi-layer assemblies, the combined thickness and compression behavior of the layers should be considered.
An incorrect grip range can result in inadequate backside deformation, poor retention, or panel damage.
6. Closed-End Screw Length Selection
Closed-end rivet nuts have a finite internal cavity.
A mating screw that is too long may bottom out before the joint reaches the required clamping condition.
Engineers should confirm:
Available internal thread depth
Screw engagement length
Screw tip clearance
Joint stack thickness
Required assembly torque
Thread fit and tolerance
This is particularly important when converting an existing assembly from open-end to closed-end rivet nuts.
7. Corrosion Protection and Surface Treatment
Blue zinc plating is a protective coating for steel components.
For international OEM sourcing, relevant coating references may include ASTM B633 and applicable ISO zinc electroplating specifications.
The coating specification should define the required deposit, passivation, coating thickness, corrosion performance, and acceptance criteria.
RoHS and REACH compliance should be supported by appropriate supplier documentation rather than assumed from coating color.
8. Installation Procedure
Verify the selected thread size and approved product drawing.
Confirm panel thickness and required grip range.
Prepare the mounting hole to the specified diameter.
Remove excessive burrs and inspect hole geometry.
Select a compatible rivet nut installation tool and mandrel.
Thread the closed-end rivet nut onto the mandrel without forcing it against the internal end.
Insert the rivet nut into the prepared hole.
Seat the flange against the mounting surface.
Maintain the tool perpendicular to the panel.
Apply the approved installation stroke or setting force.
Release the tool carefully.
Inspect flange seating, backside deformation, and thread condition.
Verify the installed fastener against the required mechanical acceptance criteria.
Manual, pneumatic, hydraulic, or automated tools may be used where compatible with the selected rivet nut configuration.
OEM Mechanical and Functional Validation
Recommended application-specific verification may include:
Mounting hole diameter and tolerance
Installation stroke and force
Flange seating
Backside deformation
Spin-out torque
Axial pull-out resistance
Push-out resistance where applicable
Thread integrity
Screw engagement depth
Screw bottoming clearance
Repeated assembly performance
Vibration testing where required
Corrosion testing
Leakage testing where sealing is specified
Acceptance values must be established from the OEM drawing, application requirements, or approved validation plan.
Technical Drawing and CAD Documentation
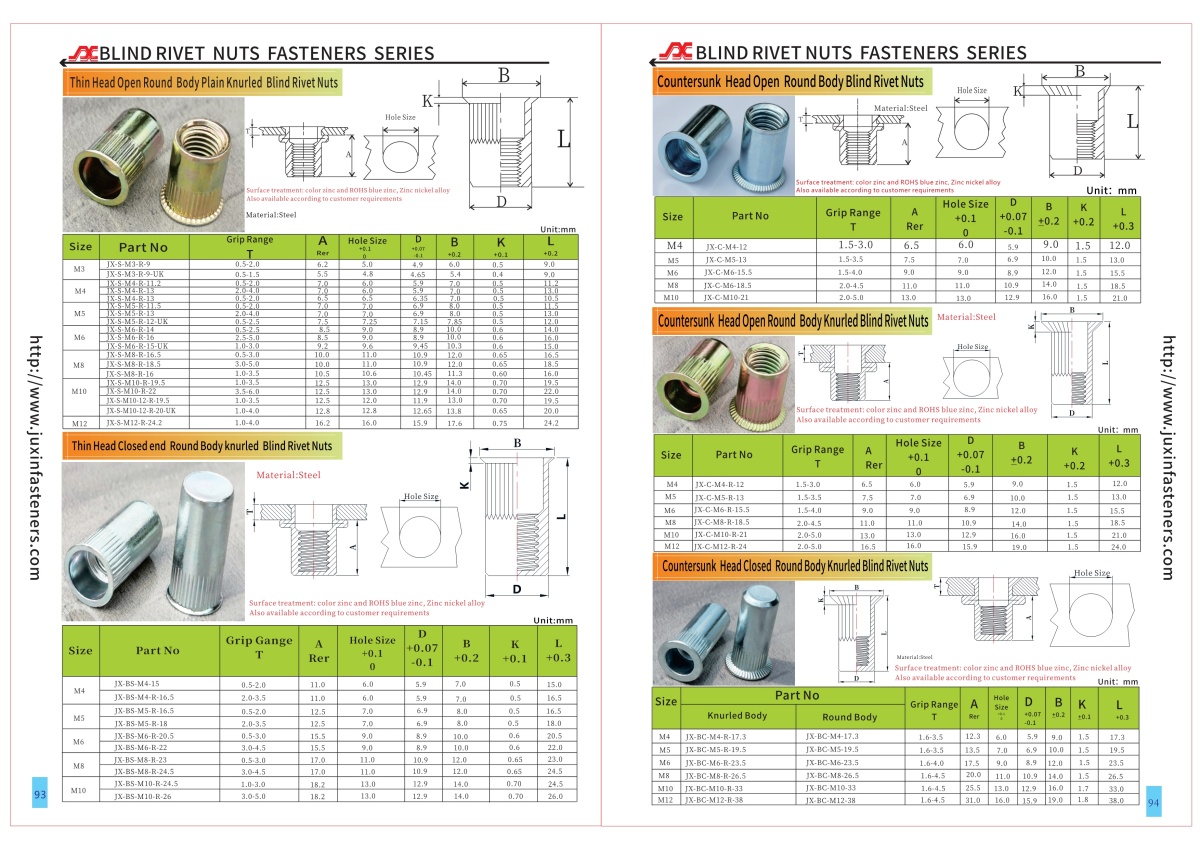
The existing product documentation references specification PDF pages 93–94 and related CAD information.
Customers should consult the applicable drawing revision for exact dimensions, including:
Flange diameter
Flange thickness
Body diameter
Knurl geometry
Overall length
Internal thread depth
Closed-end geometry
Mounting hole requirements
Individual grip intervals
Custom configurations can be reviewed according to customer drawings.
OEM RFQ Checklist
For technical evaluation and quotation, please provide:
Metric or Unified inch thread requirement
Approved 2D drawing or 3D CAD model
Mounting panel material
Panel thickness
Mounting hole diameter and tolerance
Required grip range
Maximum flange height
Available backside clearance
Required internal thread depth
Mating screw dimensions
Installation method
Pull-out and spin-out requirements
Surface finish specification
Corrosion resistance requirements
Sealing requirements, if applicable
Sample quantity
Initial order quantity
Annual forecast
Inspection and documentation requirements
Packaging and delivery requirements
Why Choose a Closed-End Blind Rivet Nut?
The closed-end design is the principal functional difference between this product and an open-end rivet nut.
An open-end insert allows the mating screw to pass through the threaded barrel, whereas a closed-end insert terminates the thread cavity inside an enclosed barrel.
This helps protect the threaded area against direct contamination from the blind side.
Closed-end rivet nuts may be considered for:
Industrial electrical enclosures
HVAC equipment housings
Instrument cabinets
Fabricated equipment covers
Automotive interior assemblies
Transportation equipment panels
Machinery guards
Selected container and compartment assemblies
A closed-end barrel alone does not guarantee a watertight or airtight installation. Leakage may still occur around the mounting hole, beneath the flange, or through other joint interfaces.
Applications requiring verified sealing performance should specify suitable sealing features and validated leakage-test criteria.
Low-Profile Head for Compact Assemblies
The thin head, also called a low-profile or reduced flange head, is designed to minimize protrusion above the mounting surface.
Compared with conventional large-flange rivet nuts, this configuration may improve clearance where a mating component sits close to the mounting panel.
However, the smaller flange provides less bearing area than a large-flange design.
Engineers should consider panel strength, installation force, pull-through resistance, and flange seating before selecting the head style.
A low-profile head should not be confused with a fully countersunk head.
Knurled Round Body for Improved Mechanical Engagement
The external knurling is designed to engage the surrounding panel material during installation.
When the rivet nut is properly set, the knurled body can help resist rotation during mating screw installation and removal.
Actual spin-out torque depends on mounting hole diameter, panel thickness, material properties, knurl geometry, and installation conditions.
The knurled body improves insert retention characteristics but does not independently provide screw-thread locking.
Where vibration resistance is required, the complete bolted joint should be evaluated.
Blue Zinc-Plated Steel Construction
This product uses steel construction with a blue zinc-plated surface finish.
Zinc plating provides sacrificial corrosion protection to the underlying steel within the limitations of the coating system.
Corrosion performance depends on zinc thickness, passivation, environmental exposure, and installation damage.
For OEM projects, JUXIN FASTENERS can review customer-defined coating requirements, including applicable ASTM or ISO references,
restricted-substance documentation, and corrosion testing specifications.
Industrial Applications
Automotive and Commercial Vehicles
Potential applications include interior brackets, access covers, fabricated panels, and non-critical equipment mounting points.
Electrical and Electronic Equipment
Closed-end rivet nuts can help protect threaded cavities from direct backside contamination in cabinets, instrument enclosures, and electrical equipment housings.
Electrical safety and enclosure protection ratings must be validated at assembly level.
HVAC and Refrigeration Systems
Suitable candidate applications include equipment housings, ventilation assemblies, service panels, and fabricated brackets.
Industrial Machinery
These fasteners may be used for machinery guards, removable equipment panels, and enclosed fabricated structures.
Transportation and Rail Interiors
Closed-end knurled rivet nuts may be evaluated for selected non-structural interior mounting applications, subject to project-specific engineering and qualification requirements.
Metal Furniture and Fabricated Structures
They can provide reusable threaded mounting points in tubular metal furniture, fixtures, cabinets, and other thin-wall assemblies.
OEM Engineering and Sourcing Support
JUXIN FASTENERS supports drawing-based sourcing inquiries for low-profile closed-end knurled steel rivet nuts.
Engineering teams can submit mounting hole requirements, grip ranges, head dimensions, installation parameters, and retention performance requirements.
OEM procurement managers, strategic sourcing teams, and supplier development professionals can provide approved drawings,
initial order quantities, annual forecasts, inspection specifications, and packaging requirements.
Request a Quotation
For closed-end knurled steel blind rivet nuts, metric or custom thread requirements, and industrial bulk orders, contact:
JUXIN FASTENERS
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Contact: https://www.juxinfasteners.com/contact-us/
Please send your technical drawing, thread size, panel thickness, required grip range, surface finish specification, and estimated purchasing quantity.
Product Packaging
Industrial Export Packaging — Closed-End Knurled Steel Rivet Nuts
Standard Packaging
JUXIN FASTENERS provides industrial export packaging for low-profile closed-end knurled steel blind rivet nuts.
The standard packaging arrangement consists of plastic inner bags, outer cartons, and palletized shipment where required.
Packaging is selected according to the product size, order quantity, handling requirements, and transportation conditions.
Reference Packaging Dimensions
| Packaging Type | Dimensions (cm) | Approximate Dimensions (in) |
|---|---|---|
| Carton Option 1 | 29 × 19 × 19.5 | 11.42 × 7.48 × 7.68 |
| Carton Option 2 | 23.5 × 17.5 × 8 | 9.25 × 6.89 × 3.15 |
| Pallet Reference | 215 × 100 × 90 | 84.65 × 39.37 × 35.43 |
These are reference packaging dimensions. Actual carton quantities, packing arrangements, and pallet dimensions are confirmed according to the purchase order.
Product Protection and Identification
Packaging arrangements may include:
Protective plastic inner bags
Reinforced export cartons
Moisture-resistant protection where required
Product identification labels
Thread size and specification marking
Part number identification
Batch and quantity labels
Palletized packing for international shipment
Appropriate packaging helps minimize handling damage and unwanted moisture exposure during storage and transportation.
Customized OEM Packaging
Customer-specific packaging options can be reviewed, including:
Private labeling
Customer part-number labels
Barcode identification
Customized carton dimensions
Specified quantities per bag or carton
Special pallet configurations
Customer-specific traceability markings
Additional packaging requirements may affect cost and lead time.
Bulk Purchasing and Supply Chain Requirements
For industrial purchasing programs, JUXIN FASTENERS can review customer requirements covering:
Initial order quantities
Annual demand forecasts
Customer-specific packaging
Part-number identification
Inspection documentation
Batch traceability requirements
Shipping and delivery arrangements
Final packaging and supply terms are confirmed during quotation and purchase order review.
Contact JUXIN FASTENERS
For closed-end knurled blind rivet nuts, custom threaded inserts, and OEM bulk purchasing requirements:
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Contact: https://www.juxinfasteners.com/contact-us/
Product Pictures
Tags
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY