
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Aug. 25, 2026
Aluminum CNC Machining for EV Battery Pack Components
Precision CNC Machining for EV Battery Pack OEM Applications
Aluminum CNC machining provides a flexible manufacturing solution for electric vehicle battery pack manufacturers requiring lightweight, dimensionally accurate, and application-specific mechanical components.
In EV battery pack assemblies, precision-machined aluminum parts can support enclosure mounting, module positioning, mechanical fastening, cooling-system interfaces, and structural connections.
For automotive OEMs and battery system manufacturers, successful component production involves more than machining an individual part to drawing dimensions.
Material selection, dimensional stability, thread engagement, surface treatment, thermal expansion, assembly compatibility, and batch-to-batch consistency all influence manufacturing performance and long-term reliability.
JUXIN FASTENERS supplies custom CNC machined components and fastening hardware for drawing-based OEM requirements.
Depending on part geometry, tolerance requirements, and production quantities, suitable manufacturing methods may include CNC milling, CNC turning,
Swiss-type machining, drilling, tapping, profiling, pocketing, and turn-mill operations.
Customers can submit 2D engineering drawings, 3D CAD models, samples, material specifications, and inspection requirements for technical evaluation and quotation.
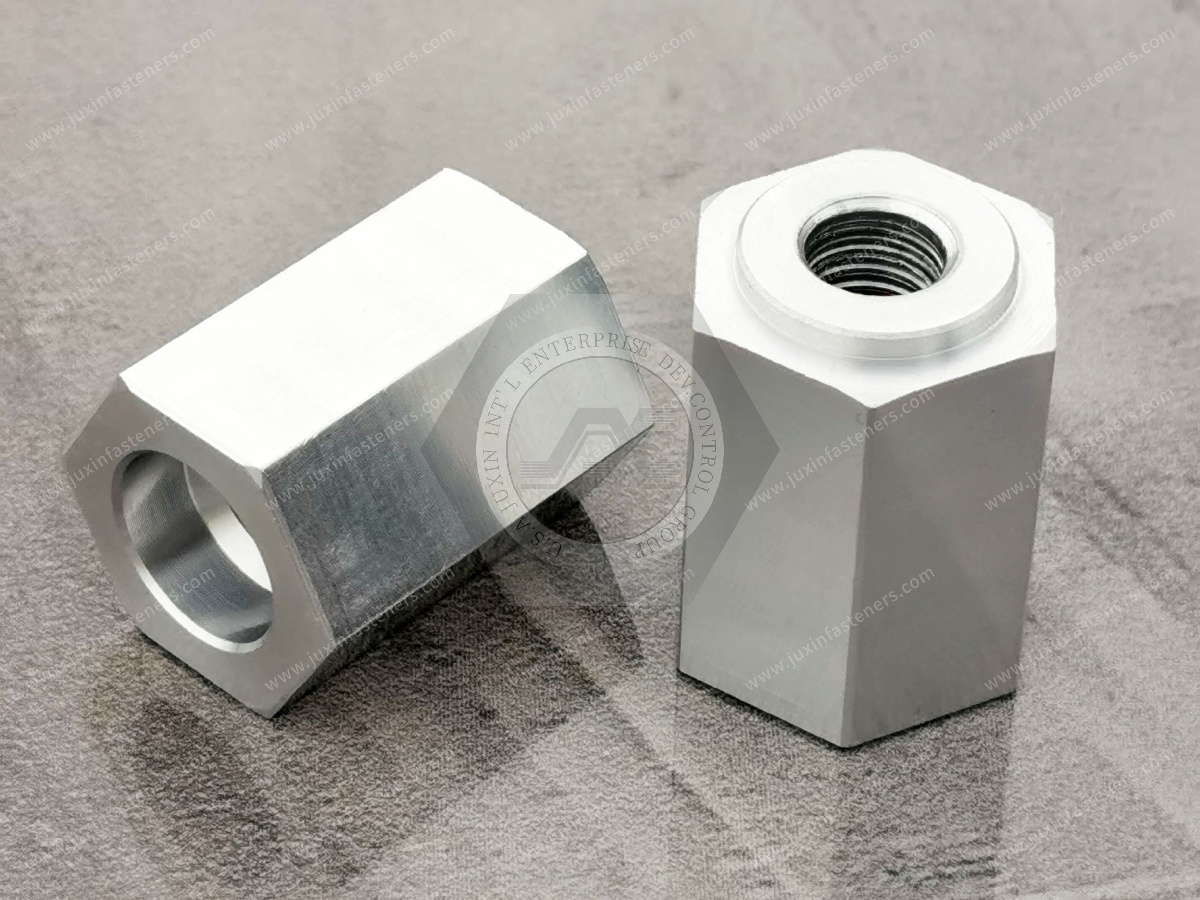
Why Aluminum Is Used in EV Battery Pack Components
Aluminum alloys are widely considered for EV battery pack mechanical components because they offer a useful combination of low density, machinability, corrosion resistance, and thermal conductivity.
Their suitability depends on the specific mechanical, electrical, thermal, and environmental requirements of each component.
Battery pack structures may combine aluminum enclosures, steel fasteners, copper conductors, polymer insulation, sealing systems, and other materials.
These combinations require careful consideration of contact conditions, thermal expansion, galvanic corrosion, and assembly loads.
For example, an aluminum spacer used to establish module positioning has different engineering requirements from a threaded mounting block supporting a mechanically loaded connection.
Similarly, a cooling interface must be evaluated for surface contact, flatness, and thermal performance rather than dimensional accuracy alone.
Common Aluminum Alloy Options
Commonly specified aluminum alloys for precision CNC machining include 6061, 6063, 6082, and 7075. These materials should not be treated as interchangeable without engineering review.
6061 Aluminum: Suitable for many general-purpose structural and machined components requiring a balance of strength, machinability, and corrosion resistance.
6063 Aluminum: Often considered where surface finish, extrusion compatibility, and moderate mechanical requirements are important.
6082 Aluminum: Used in suitable structural applications requiring strength and machining characteristics, particularly in European material specifications.
7075 Aluminum: Considered for higher-strength applications where corrosion exposure, surface treatment, and material condition require additional evaluation.
The final material specification should include the applicable alloy designation, temper, product form, and relevant material standard.
For example, an aluminum component specified as 6061-T6 should not automatically be substituted with another 6000-series alloy solely because the nominal alloy family appears similar.
Where aluminum components form part of a load-bearing battery pack structure, engineers should evaluate actual loading conditions, joint geometry, fatigue requirements,
and environmental exposure before approving material selection.
Typical CNC Machined Components for EV Battery Packs
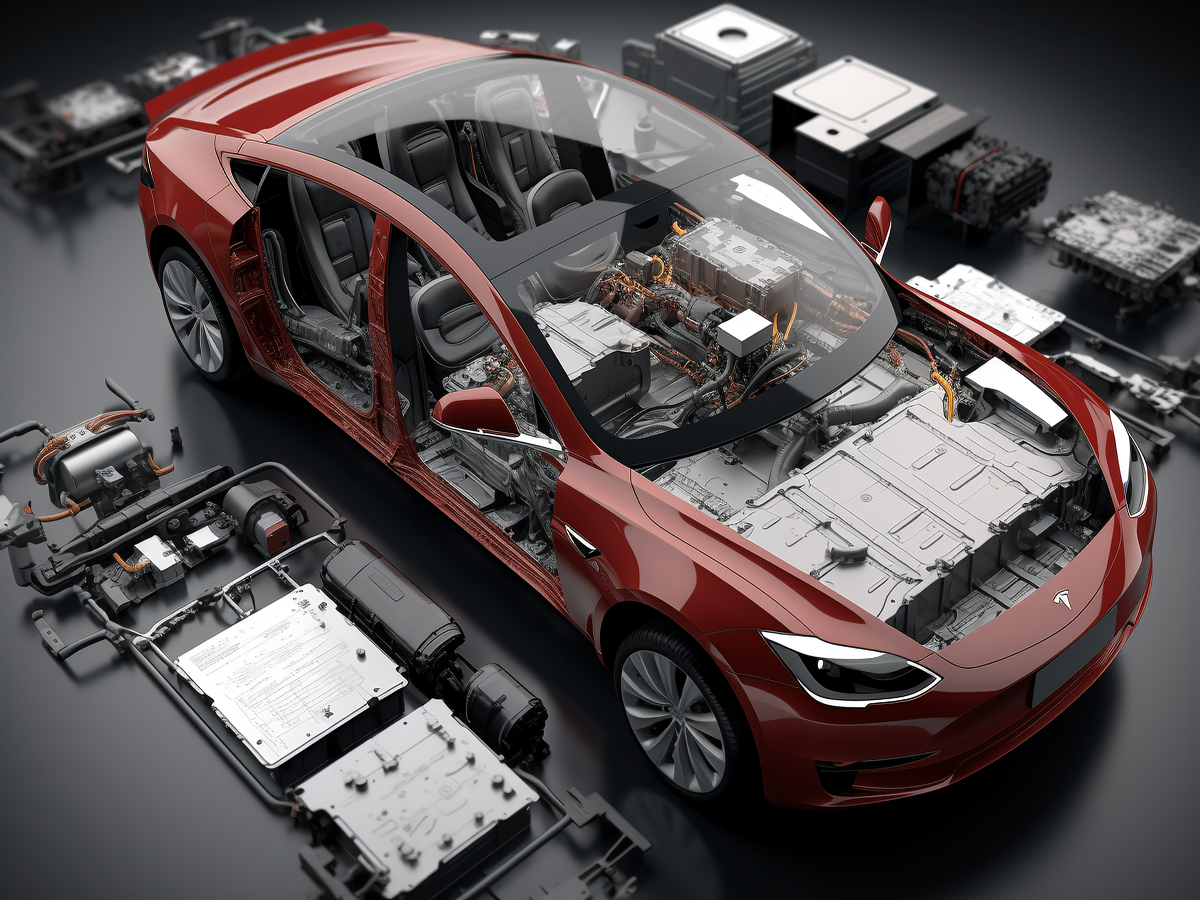
Custom CNC machined aluminum components can be used in several mechanical and assembly functions within EV battery systems.
Battery Enclosure Mounting Blocks
Machined mounting blocks provide defined fastening positions between battery enclosures, brackets, covers, and supporting structures.
Critical design considerations include threaded hole depth, mounting-face flatness, fastener access, and the ability of the joint to withstand specified assembly and service loads.
Precision Aluminum Spacers and Standoffs
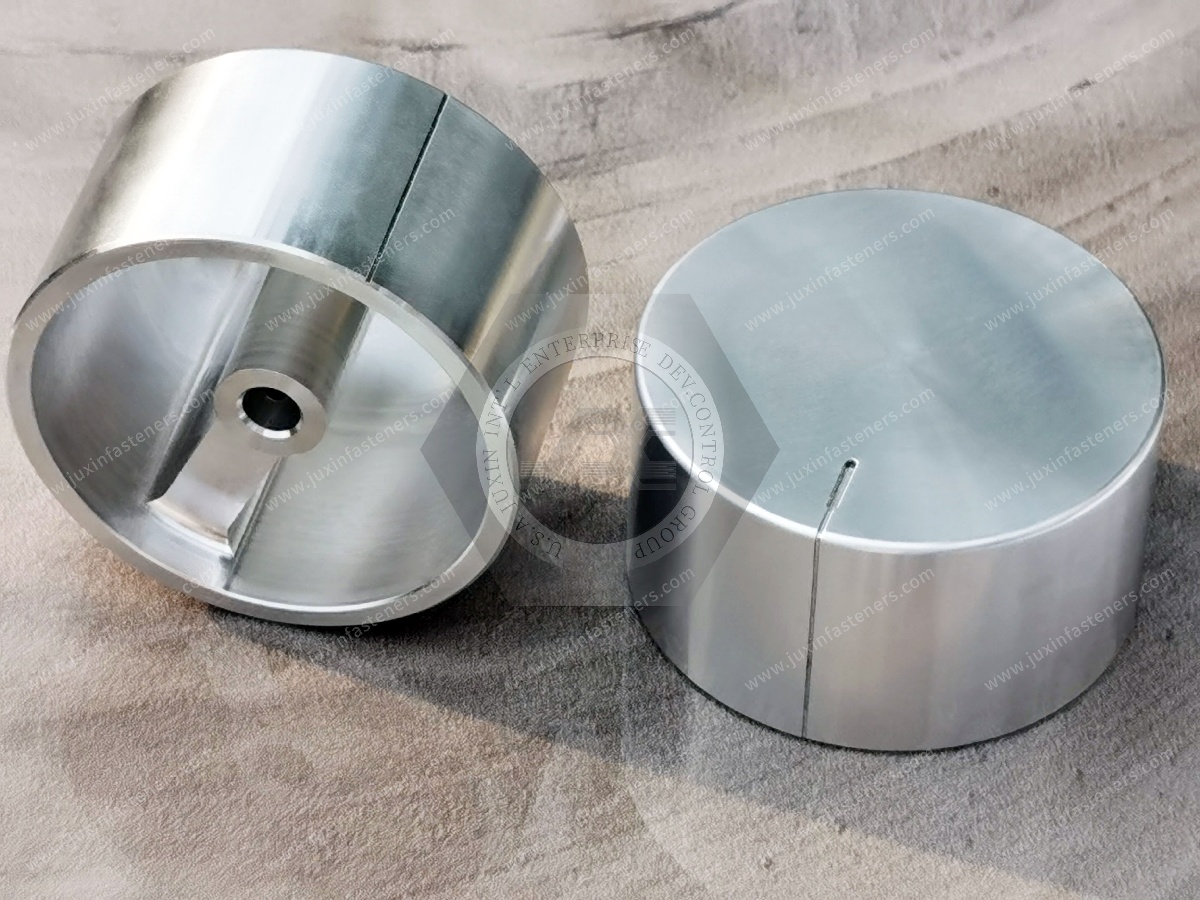
Aluminum spacers establish controlled distances between mechanical components, support assembly positioning, and help maintain designed clearances.
Important specifications include overall length, parallelism, internal diameter, external diameter, and contact-face quality.
For electrically sensitive locations, engineers must determine whether conductive aluminum spacers are permissible or whether insulating components are required.
Threaded Aluminum Components and Fastening Interfaces
Custom threaded blocks, inserts, and machined fastening components may provide attachment points for battery pack covers, module supports, and auxiliary brackets.
Thread design must account for aluminum alloy properties, thread engagement, expected clamp load, repeated assembly requirements, and possible thread stripping.
Where higher wear resistance or repeated maintenance is required, suitable threaded inserts or alternative fastening designs may be considered after engineering evaluation.
Battery Cooling-System Interfaces
Precision-machined aluminum parts may provide mechanical interfaces for cooling plates, thermal-management hardware, manifolds, and mounting systems.
Flatness, surface finish, sealing geometry, and dimensional compatibility can influence contact quality and assembly reliability.
Components exposed to coolant require separate evaluation of material compatibility and sealing performance.
Custom Pins, Bushings, and Positioning Components
Machined pins, bushings, sleeves, and locating components may support positioning and assembly alignment.
Their dimensions and material selection depend on contact loads, wear conditions, and the required locating function.
Custom Brackets and Mechanical Connectors
Machined brackets and connection components can support battery pack mounting and auxiliary equipment installation.
Their design should reflect actual load paths, available installation space, vibration exposure, and the selected fastening system.
CNC Machining Processes for Custom Aluminum Battery Components
Selecting the correct machining process affects component accuracy, manufacturing efficiency, material utilization, and overall OEM production cost.
JUXIN FASTENERS can evaluate appropriate machining methods according to customer drawings, component geometry, and production requirements.
CNC Milling for Complex Mounting and Interface Components
CNC milling is suitable for components requiring multiple mounting faces, pockets, slots, bolt-hole patterns, and complex external profiles.
Typical applications include battery enclosure mounting blocks, brackets, connector housings, and cooling-system mounting interfaces.
For parts requiring multiple machining setups, the selection of reference datums and workholding methods becomes particularly important.
Poor datum planning can introduce positional variation between features machined in separate operations.
CNC Turning and Swiss-Type Machining for Precision Cylindrical Parts
CNC turning is suitable for cylindrical spacers, sleeves, bushings, pins, and threaded components.
Swiss-type machining may be appropriate for certain small-diameter, slender, or geometrically complex components, depending on their design and production quantities.
Where parts require both turned features and milled details, turn-mill machining may reduce handling and improve positional relationships between features.
However, combining operations is not automatically the most economical solution. Production quantity, machine availability, setup time, and component complexity should all be considered.
Drilling, Tapping, Pocketing, and Secondary Operations
Battery pack mounting hardware frequently requires accurately positioned holes, internal threads, countersinks, counterbores, and machined contact surfaces.
Thread tapping and hole-making processes should be selected according to aluminum alloy, hole depth, thread size, and expected joint function.
Burr control is particularly important around threaded holes, mounting faces, and internal pockets.
Loose machining debris or sharp edges can interfere with assembly and may create unacceptable risks near sensitive electrical components.
Engineering Design Considerations for EV Battery Pack CNC Parts
Engineering teams should evaluate how each machined component interacts with the complete battery assembly rather than assessing its drawing dimensions in isolation.
Dimensional Tolerances and Functional Datums
Not every feature requires the same machining tolerance.
Mounting-hole positions, mating surfaces, locating diameters, and sealing interfaces may require tighter dimensional control than nonfunctional external surfaces.
A practical tolerance strategy distinguishes critical-to-function dimensions from general machining features.
Where appropriate, ISO 1101 geometric tolerancing or ASME Y14.5 geometric dimensioning and tolerancing principles can help define positional, flatness, perpendicularity, and profile requirements.
The drawing should establish the governing specification system clearly rather than combining potentially conflicting conventions.
Overly restrictive tolerances can increase machining time, inspection requirements, scrap risk, and manufacturing cost without improving actual assembly performance.
Thread Engagement and Joint Reliability
Threaded connections in aluminum components require attention to internal thread strength, engagement length, installation torque, and expected service loads.
Aluminum internal threads may be more vulnerable to stripping than comparable steel threads under certain loading conditions.
For repeated assembly or demanding mechanical applications, engineers may evaluate steel threaded inserts, alternative thread engagement designs, or different fastening configurations.
The appropriate engagement length cannot be established from nominal thread diameter alone. It depends on material strength, thread geometry, loading conditions, and the selected fastener.
Metric ISO threads and Unified UNC/UNF threads must be specified and manufactured according to their respective systems. Similar nominal diameters do not make them interchangeable.
Thermal Expansion and Assembly Compatibility
EV battery systems experience temperature changes during charging, discharging, operation, and environmental exposure.
Aluminum generally expands more with temperature than steel.
When aluminum components are mechanically constrained by steel fasteners or adjoining materials, differential thermal expansion can influence joint loading and dimensional relationships.
Design engineers should evaluate operating temperature ranges, component lengths, joint stiffness, and material combinations where thermal movement could affect assembly performance.
This is especially relevant for long mounting interfaces, closely controlled module positioning features, and mixed-material fastening systems.
Electrical Conductivity and Isolation Requirements
Aluminum is electrically conductive and should not be assumed to provide electrical isolation.
Where a machined spacer, bracket, or mounting block is installed near busbars, terminals, or other energized components, the assembly must satisfy applicable electrical clearance, creepage, insulation, and system safety requirements.
Anodizing or another surface treatment should not be assumed to provide a qualified electrical insulation barrier without appropriate design verification and testing.
Electrical safety decisions must be established at the battery system design level.
Surface Treatments and Corrosion Protection for Aluminum CNC Components
Surface finishing should be selected according to the intended operating environment, mechanical function, appearance requirements, and assembly interfaces.
Potential finishing options for suitable aluminum alloys include conventional anodizing, hard anodizing, conversion coatings, and other customer-specified treatments.
Anodizing can improve selected surface characteristics, but coating thickness, dimensional effects, electrical contact requirements, and corrosion conditions must be considered.
For precision-fit components, surface treatment may alter final dimensions or the effective fit between mating parts. Critical interfaces should therefore be evaluated using the required finished-condition dimensions.
Galvanic corrosion is another consideration when aluminum contacts dissimilar metals in the presence of an electrolyte.
Suitable design measures may include material pairing review, protective coatings, isolation methods, drainage provisions, and environmental validation.
Surface treatment specifications should reference appropriate requirements, such as ISO 7599 for applicable decorative and protective anodic oxidation coatings or other relevant customer-approved specifications.
These standards should only be applied when they match the actual finishing process.
Precision, Repeatability, and Production Stability
For OEM battery pack production, a CNC machining process must consistently reproduce acceptable components across multiple manufacturing batches.
Producing one accurate prototype does not automatically demonstrate stable serial-production capability.
Production consistency depends on several interconnected factors, including machine condition, tooling wear, fixture repeatability, raw material variation, machining sequence, thermal conditions, and inspection methods.
A stable production strategy should identify the features most likely to influence assembly performance.
For example, a battery mounting block may require simultaneous control of mounting-face flatness, threaded-hole position, and overall height.
Measuring only the overall dimensions may not adequately verify the component's intended function.
Manufacturing engineers can reduce unnecessary process complexity by selecting logical machining datums, minimizing avoidable setups, and establishing practical inspection access for critical features.
Production managers should also consider cycle time, tool replacement intervals, fixture changeover, and the effect of machining variations on downstream assembly.
Quality Control for Custom CNC Machined Battery Components
Inspection planning should begin with the engineering drawing and the intended function of the component.
Depending on customer specifications, quality verification may include:
Dimensional and geometric measurement
Thread size and functional gauge inspection
Hole diameter and positional verification
Surface roughness and flatness measurement
Material identification and documentation review
Hardness verification when specified
Visual inspection for burrs, damage, and surface defects
Functional fit or assembly verification where applicable
Critical characteristics should be identified before production rather than relying exclusively on final inspection.
For automotive OEM programs, customers may also require project-specific documentation, inspection records, traceability, or approval procedures.
Any requirements for first-article inspection, PPAP-related documentation, capability studies, or additional validation should be agreed upon during technical and commercial review. Such documentation should not be assumed to be included unless confirmed.
From Prototype Development to Repeat OEM Production
CNC machining supports product development because engineering changes can often be introduced through revised programming, tooling, or process arrangements without the need for dedicated forming dies.
A typical drawing-based manufacturing workflow includes:
Engineering drawing and CAD review
Material and process selection
CNC programming and process preparation
Prototype or first-article machining
Dimensional and functional inspection
Process optimization
Repeat production and final inspection
During prototype development, engineers may identify opportunities to simplify geometry, improve machining access, modify noncritical tolerances, or standardize fastening interfaces.
Before moving to volume production, these decisions should be reviewed against the final assembly requirements.
For larger production quantities, the economic evaluation should include raw material utilization, machining cycle time, fixture requirements, inspection effort, finishing operations, and total landed component cost.
Alternative manufacturing processes may become more economical at sufficiently high volumes.
However, any change from machining to casting, forging, extrusion-based production, or another process requires evaluation of material properties,
dimensional capability, tooling investment, and part qualification requirements.
Reducing CNC Machining Costs Without Compromising Battery Pack Reliability
OEM procurement teams often compare component prices without fully accounting for manufacturing complexity or assembly consequences.
A lower unit price does not necessarily provide the lowest total cost if dimensional inconsistency causes rework, line stoppages, or installation difficulties.
Several design and procurement decisions can influence total component cost.
Tolerance Allocation: Apply tight tolerances to functional features rather than the entire component. This can reduce unnecessary machining and inspection requirements.
Material Selection: Specify the alloy and temper required by the application. Selecting a higher-strength or more expensive alloy without a functional justification may increase cost unnecessarily.
Machining Accessibility: Deep pockets, difficult-to-reach internal features, and complex multi-angle machining may increase setup and tool costs.
Standardized Fastening Interfaces: Where the design permits, common thread sizes and fastening arrangements can simplify purchasing, assembly tooling, and maintenance.
Production Volume Planning: Accurate annual demand estimates and realistic delivery schedules help determine suitable manufacturing and purchasing arrangements.
Drawing Revision Control: Clearly identifying the approved drawing revision reduces the risk of producing obsolete components and helps maintain repeat-order consistency.
These considerations are particularly relevant when sourcing multiple custom spacers, mounting blocks, threaded components, and brackets for the same battery pack platform.
OEM Supplier Evaluation and RFQ Requirements
For procurement development, purchasing managers, and supply chain teams, supplier evaluation should address both technical capability and commercial suitability.
A complete RFQ package allows the manufacturer to evaluate the component and prepare a more relevant quotation.
Recommended RFQ information includes the 2D drawing or 3D CAD model, material grade and temper, critical tolerances, surface treatment,
inspection requirements, prototype quantity, expected production volume, and delivery destination.
For ongoing OEM programs, customers should also identify anticipated annual usage, release schedules, packaging requirements, and any required production or quality documentation.
MOQ, lead time, and production arrangements depend on the actual component geometry, material availability, order quantity, finishing requirements, and manufacturing process.
JUXIN FASTENERS can review drawing-based requirements and discuss suitable custom machining and fastening solutions according to the project's technical and commercial needs.
Custom CNC Machining and Fastening Solutions for Global OEMs
JUXIN FASTENERS supplies custom CNC machined parts and industrial fastening components for international OEM applications.
In EV battery pack manufacturing, precision aluminum components frequently operate together with bolts, screws, nuts, threaded inserts, spacers, bushings, and other mechanical connection hardware.
Evaluating these components as part of a complete assembly can help identify compatibility concerns before production.
For example, an aluminum mounting block should be evaluated alongside its mating fastener, specified installation method, expected clamp load, and supporting structure.
This assembly-oriented approach is relevant not only to electric vehicle battery systems but also to industrial energy storage equipment,
automotive assemblies, electrical enclosures, machinery, robotics, HVAC equipment, and other engineered products requiring precision mechanical components.
Requirements for safety-critical, aerospace, medical, or other regulated applications must be reviewed individually, including any applicable qualifications and customer approval conditions.
Request an OEM Aluminum CNC Machining Quote
If your company is sourcing custom aluminum CNC machined components, EV battery pack mounting hardware, precision spacers, threaded blocks, or drawing-based OEM parts,
contact JUXIN FASTENERS for a technical and commercial review.
Please send your 2D engineering drawing, 3D CAD file, sample information, material requirements, surface treatment specifications, expected order quantity, and inspection requirements.
Our team can evaluate the manufacturing requirements and discuss suitable machining processes, component specifications, and quotation details.
JUXIN FASTENERS
Website: https://www.juxinfasteners.com/
Email: info@juxinfasteners.com
OEM CNC Machining | Custom Aluminum Components | Precision Fastening Hardware | Drawing-Based RFQ Support
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY



