Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809
Oct. 13, 2026
Modern packaging machinery depends on precise mechanical connections to support repetitive motion, accurate product handling, reliable equipment alignment and efficient production changeovers.
Automated bottling lines, cartoning machines, case packers, labeling systems, shrink-wrapping equipment and packaging conveyors use threaded fasteners throughout their frames,
guide assemblies, drive systems, protective guards and adjustment mechanisms.
The fastening requirements vary across these assemblies.
A socket head screw securing a positioning bracket has different functional requirements from a prevailing-torque lock nut used in a vibration-exposed support
joint or a captive screw installed in a frequently opened maintenance panel.
For design and mechanical engineers, fastener selection involves joint loading, material strength, alignment, thread engagement, fatigue risk and installation geometry.
Manufacturing engineers and production managers must also consider assembly repeatability, line changeover time, maintenance access, installation tooling and overall equipment effectiveness (OEE).
Procurement and supplier development teams need to evaluate standard and custom fastener availability, drawing conformity, alternative sourcing, inspection requirements,
minimum order quantities, delivery planning and long-term supply consistency.
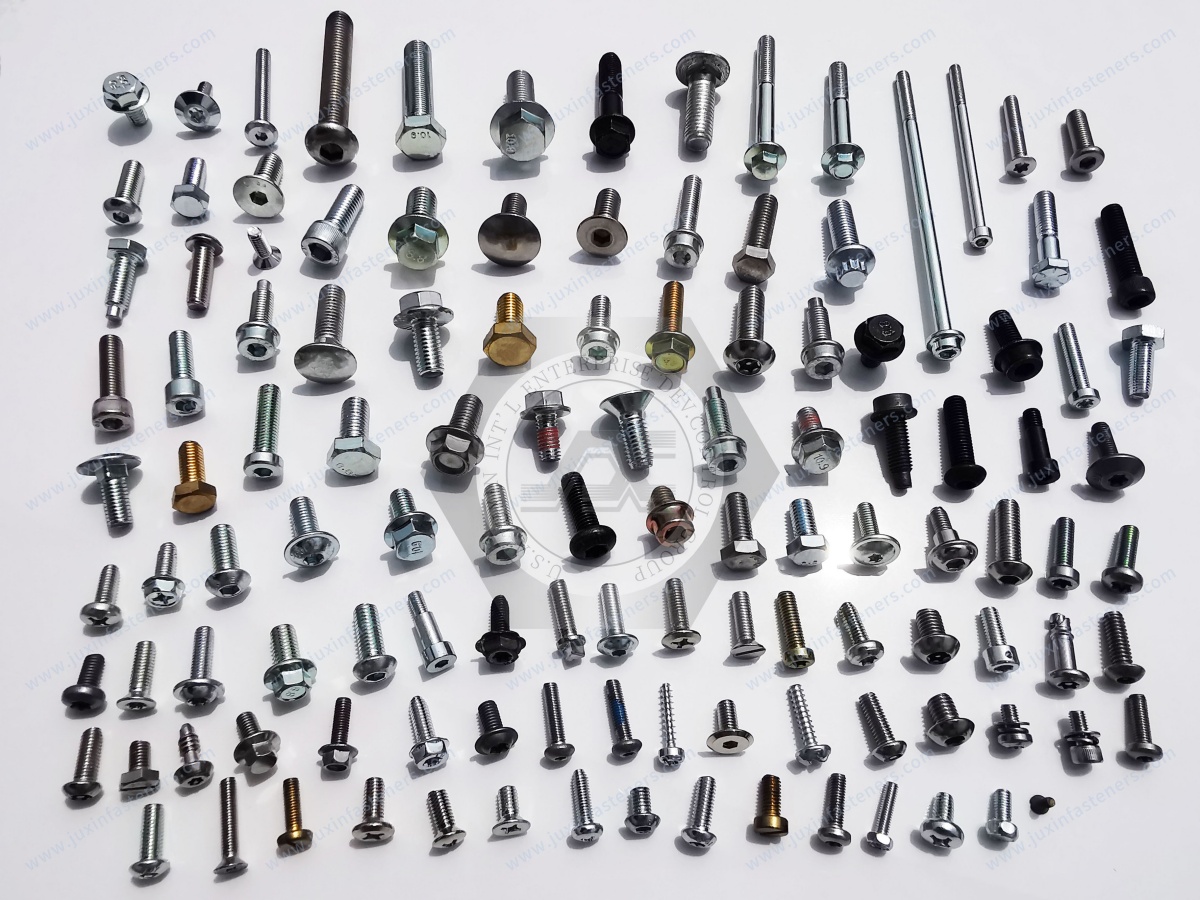
JUXIN FASTENERS supplies industrial machine screws, socket head screws, bolts, nuts, washers, prevailing-torque lock nuts, self-clinching fasteners,
captive hardware and drawing-based custom metal components for suitable packaging and bottling machinery applications.
This guide explains fastening selection for packaging equipment OEMs, with particular attention to high-cycle machinery, repeated adjustment,
quick-change assemblies, corrosion exposure and production efficiency.
Packaging machinery includes different mechanical and structural zones, each with its own fastening requirements.
| Equipment Application | Potential Fastener Solution | Main Engineering Consideration |
|---|---|---|
| Cartoning machine guide rails | Socket head screws and mounting bolts | Alignment and repeated adjustment |
| Bottling line support frames | Hexagon bolts, nuts and washers | Structural attachment and corrosion exposure |
| Case packing equipment | Machine screws and locking hardware | Repeated motion and joint stability |
| Labeling machine brackets | Precision screws and custom mounting studs | Positioning accuracy and serviceability |
| Packaging conveyor assemblies | Bolts and prevailing-torque lock nuts | Vibration and maintenance |
| Changeover adjustment mechanisms | Shoulder screws and custom threaded components | Repeatable positioning and thread wear |
| Safety guards and access panels | Captive panel screws | Fast access and reduced loose-part handling |
| Electrical control cabinets | Self-clinching nuts and threaded standoffs | Thin sheet metal assembly |
| Sealing and cutting equipment supports | Specified bolts and custom hardware | Temperature, loading and alignment |
| Custom packaging automation modules | Drawing-based pins, spacers and special fasteners | Dimensional compatibility and OEM integration |
The appropriate fastener must be selected according to the actual joint function.
A screw suitable for a lightweight protective cover should not automatically be used for a heavily loaded reciprocating mechanism.
Packaging equipment may operate with repeated acceleration, deceleration, indexing and continuous motion.
However, not every fastener experiences the same dynamic load.
A stationary frame connection may experience relatively modest vibration, while a fastener in a moving linkage may be exposed to repeated forces and changing load directions.
Important design factors include:
Joint loading and load direction
Bolt preload
Joint stiffness
Grip length
Thread engagement
Component alignment
Installation conditions
Fatigue-sensitive geometry
Repeated loading can contribute to fatigue damage if the fastener or joint is inadequately designed.
Potential problems include fatigue cracking, joint separation, fretting, bracket deformation and loss of alignment.
Engineering insight: The operating cycle rate alone does not determine whether a fastener will fail.
The stress range experienced by the fastener, joint configuration and installation condition are more important than a general description such as “high-speed machinery.”
A properly designed preloaded joint can reduce relative movement between clamped components.
However, excessive tightening may damage threads or deform lightweight mounting structures.
The OEM should define an installation method appropriate for the complete joint.
Socket head cap screws are frequently considered for machinery assemblies where installation space is limited.
ISO 4762 is a relevant dimensional standard for hexagon socket head cap screws.
Potential applications include:
Guide rail brackets
Sensor mounting structures
Positioning mechanisms
Machine frame accessories
Packaging automation modules
Adjustment assemblies
Important selection factors include head geometry, socket accessibility, screw length, material, mechanical property class and thread engagement.
Packaging machines may contain closely spaced guides, brackets and moving components.
The selected screw head and installation tool must fit within the available space.
When screws engage blind tapped holes, the designer must consider available thread depth and bottoming-out risk.
Screws used in adjustment mechanisms may be removed or loosened more frequently than permanent structural fasteners.
Engineering insight: A screw that is adequate for a permanent joint may not be the best choice for a mechanism requiring frequent removal, adjustment and reinstallation.
Thread durability, tool access and maintenance procedure should be evaluated together.
Packaging lines may process different carton sizes, bottle formats, labels and package configurations.
Changing product formats can require adjustment or replacement of guide rails, positioning brackets, tooling plates and other machine components.
Fastener selection can influence the time required for these operations.
Captive screws remain retained in a panel or component when disengaged from the mating thread.
They can reduce loose-part handling during equipment servicing or changeovers.
However, their suitability depends on the retention design, panel geometry and loading conditions.
Shoulder screws may be used where a controlled shoulder diameter or length supports positioning, spacing or a moving interface.
Their function depends on the actual joint geometry.
Drawing-based studs and spacers may help maintain consistent assembly geometry across interchangeable tooling modules.
Engineering insight: Reducing the number of loose fasteners and tool changes during a format changeover can be more valuable than reducing the unit price of each screw.
The equipment designer should evaluate changeover time, operator access, part retention and repeatability.
Repeated tightening and loosening can create additional requirements for threaded connections.
Potential concerns include:
Thread wear
Cross-threading
Galling
Stripped internal threads
Tool recess damage
Inconsistent installation force
Aluminum mounting structures may be used in packaging machinery because of their weight and machinability.
The internal thread strength of the aluminum component may limit the connection before the steel screw reaches its mechanical capacity.
Adequate thread engagement depends on the mating material, thread size, loading and joint design.
Where frequent maintenance is expected, a suitable threaded insert or other approved thread reinforcement may be considered.
The correct insert type and installation method depend on the base material.
Engineering insight: Upgrading from a lower-strength steel screw to a higher-strength screw does not automatically prevent thread stripping in a softer aluminum component.
The limiting feature may be the internal thread rather than the screw.
Some packaging machine assemblies experience vibration from motors, conveyors, indexing mechanisms and repeated mechanical motion.
Where rotational loosening is a concern, suitable locking arrangements may be considered.
Potential options include:
All-metal prevailing-torque lock nuts
Nylon-insert lock nuts where appropriate
Properly designed preloaded joints
Application-specific locking methods
All-metal prevailing-torque lock nuts use a mechanical feature to resist rotation.
Depending on the product design, ISO 7042 and related specifications may apply.
They may be considered for selected drive supports, conveyor brackets and vibration-exposed equipment connections.
Nylon-insert lock nuts may be suitable for certain packaging equipment applications.
Operating temperature, chemical exposure and maintenance requirements should be considered before selection.
Prevailing torque is the resistance generated by a locking feature during thread engagement.
Clamp load is the force holding the joint together.
These are different characteristics.
Engineering insight: A locking nut may resist rotational loosening, but it cannot independently prevent preload loss caused by joint settlement, component deformation or inappropriate installation.
For critical machinery joints, the complete fastening arrangement must be evaluated.
Packaging machinery may contain heat-sealing assemblies, cutting mechanisms and other process tooling.
These components can have additional requirements related to temperature, positioning and repeated motion.
Fasteners near heated tooling may experience temperature changes.
Material properties, differential thermal expansion and installation conditions should be considered.
Standard nylon-insert locking hardware may be unsuitable where temperatures exceed the relevant insert limitations.
Fasteners used in cutting equipment supports may influence alignment and positional stability.
The appropriate joint design depends on loading and tooling geometry.
A screw or pin used as part of a moving interface may require controlled geometry and wear considerations.
Engineering insight: A standard threaded fastener should not automatically be used as a precision bearing or pivot surface.
Where a moving interface is required, the OEM should evaluate shoulder geometry, clearance, surface condition and suitable bearing arrangements.
Bottling and beverage packaging lines may be exposed to moisture, cleaning chemicals and repeated washdown procedures.
Stainless steel fasteners may be suitable for selected applications.
304-type stainless steel may be suitable for certain indoor and moderately corrosive environments.
Its suitability depends on the actual exposure conditions.
316-type stainless steel generally offers improved resistance to certain chloride-related corrosion mechanisms compared with common 304-type compositions.
However, 316 stainless steel is not immune to pitting, crevice corrosion or chemical attack.
Applicable parts of ISO 3506 define mechanical properties for relevant stainless steel fasteners.
A2 and A4 are commonly associated with different austenitic stainless steel composition groups.
The material grade and mechanical property class should be specified according to the application.
Engineering insight: Selecting A4 stainless steel does not automatically establish suitability for every cleaning chemical or sanitary application.
Actual chemical exposure, temperature and equipment design must be considered.
Packaging equipment may include areas with different cleanliness requirements.
A fastener installed on an external support frame may have different requirements from one located near an exposed product zone.
Fasteners located near exposed food or beverage products may require additional attention to surface condition, cleanability and contamination risk.
Fasteners installed on external machine frames may be selected primarily for mechanical loading and environmental corrosion resistance.
Fasteners used in electrical cabinets may require serviceability and appropriate environmental protection.
Engineering insight: The same packaging machine may require several fastener material and finish specifications because the exposure conditions differ by equipment zone.
A single material upgrade across every location may increase cost without improving the critical connections.
Depending on the application, potential material and finish options include:
Zinc-plated carbon steel
Zinc-nickel-coated steel where specified
Zinc-flake coating systems
Stainless steel
Customer-specified protective finishes
Coating selection must consider environmental exposure, mechanical properties, thread fit and installation friction.
ASTM A967/A967M is a relevant specification for chemical passivation treatments for stainless steel parts.
Passivation may be specified to address certain surface contamination concerns.
However, it does not guarantee compatibility with all cleaning chemicals or operating environments.
ASTM B117 defines a laboratory salt spray test method.
Results depend on the tested coating system and test conditions.
Salt spray hours should not be treated as a direct prediction of actual packaging machinery service life.
For susceptible high-strength steel fasteners, coating and manufacturing processes should consider hydrogen embrittlement risk.
Engineering insight: Coating selection should be reviewed together with thread tolerances and tightening requirements.
A change in surface finish may affect installation friction even when the nominal fastener dimensions remain unchanged.
Packaging machinery frequently includes sheet metal guards, control cabinets and sensor mounting panels.
Self-clinching fasteners can provide reusable threaded attachment points in suitable sheet metal.
Self-clinching nuts may be used in:
Electrical control cabinets
Machine guards
Sensor panels
Automation enclosures
Their installation depends on panel thickness, hardness, hole dimensions and fastener design.
Self-clinching studs may provide fixed mounting points for brackets or internal components.
Threaded standoffs may be used for circuit board mounting, electrical modules and controlled spacing.
Engineering insight: Self-clinching fasteners should not be selected solely by thread size.
Panel thickness, hardness and required retention performance must also be considered.
Standard catalog fasteners may not satisfy every packaging equipment design.
Drawing-based custom hardware may be required for:
Special screw lengths
Modified head profiles
Precision shoulder screws
Custom threaded studs
Special nuts
Drawing-specific washers
Custom mounting pins
Precision spacers
Tooling and adjustment components
JUXIN FASTENERS supports drawing-based inquiry review for industrial fastening components.
Manufacturing feasibility depends on material, geometry, tolerances and production quantity.
Cold forming may be appropriate for selected fastener geometries and production volumes.
CNC machining may be appropriate for complex geometries, controlled shoulders and drawing-specific features.
Some components may require a combination of forming and secondary machining.
Engineering insight: Custom fastener drawings should identify dimensions that control alignment, installation and mechanical function.
Unnecessarily restrictive tolerances on noncritical features can increase manufacturing cost without improving equipment performance.
Production managers and manufacturing engineers must balance fastening reliability with assembly speed, changeover efficiency and maintenance requirements.
Fastener head geometry and tool clearance should be considered during equipment design.
Thread quality, surface condition and dimensional consistency can influence installation results.
Captive hardware and accessible mounting arrangements may simplify format changes.
Packaging equipment may require frequent inspection, adjustment and servicing.
The OEM should define when fasteners may be reused and when replacement is necessary.
Fastener unit price is only one part of total equipment cost.
Installation labor, maintenance time, rework, spare-part management and supply continuity should also be considered.
Engineering insight: A more expensive fastener may be commercially justified if it reduces recurring maintenance labor or equipment downtime.
However, the benefit should be evaluated against the actual operating and maintenance process rather than assumed.
Applicable standards depend on the specific fastener and equipment application.
| Product or Requirement | Potentially Relevant Standard |
|---|---|
| Hexagon socket head cap screws | ISO 4762 |
| Hexagon head bolts | ISO 4014 / ISO 4017 |
| Hexagon nuts | ISO 4032 |
| Carbon steel and alloy steel bolt mechanical properties | ISO 898-1 |
| Carbon steel nut mechanical properties | ISO 898-2 |
| Stainless steel fastener mechanical properties | Applicable parts of ISO 3506 |
| All-metal prevailing-torque nuts | ISO 7042 where applicable |
| Metric thread specifications | Applicable ISO metric thread standards |
| Inch-series threaded fasteners | Applicable ASME/ANSI standards |
| Stainless steel passivation | ASTM A967/A967M where specified |
| Salt spray testing | ASTM B117 |
| Material inspection documents | EN 10204 where contractually specified |
Custom shoulder screws, mounting pins and specialized packaging equipment hardware may require drawing-specific dimensions and functional validation.
Metric, UNC, UNF and other thread systems must be treated as separate specifications.
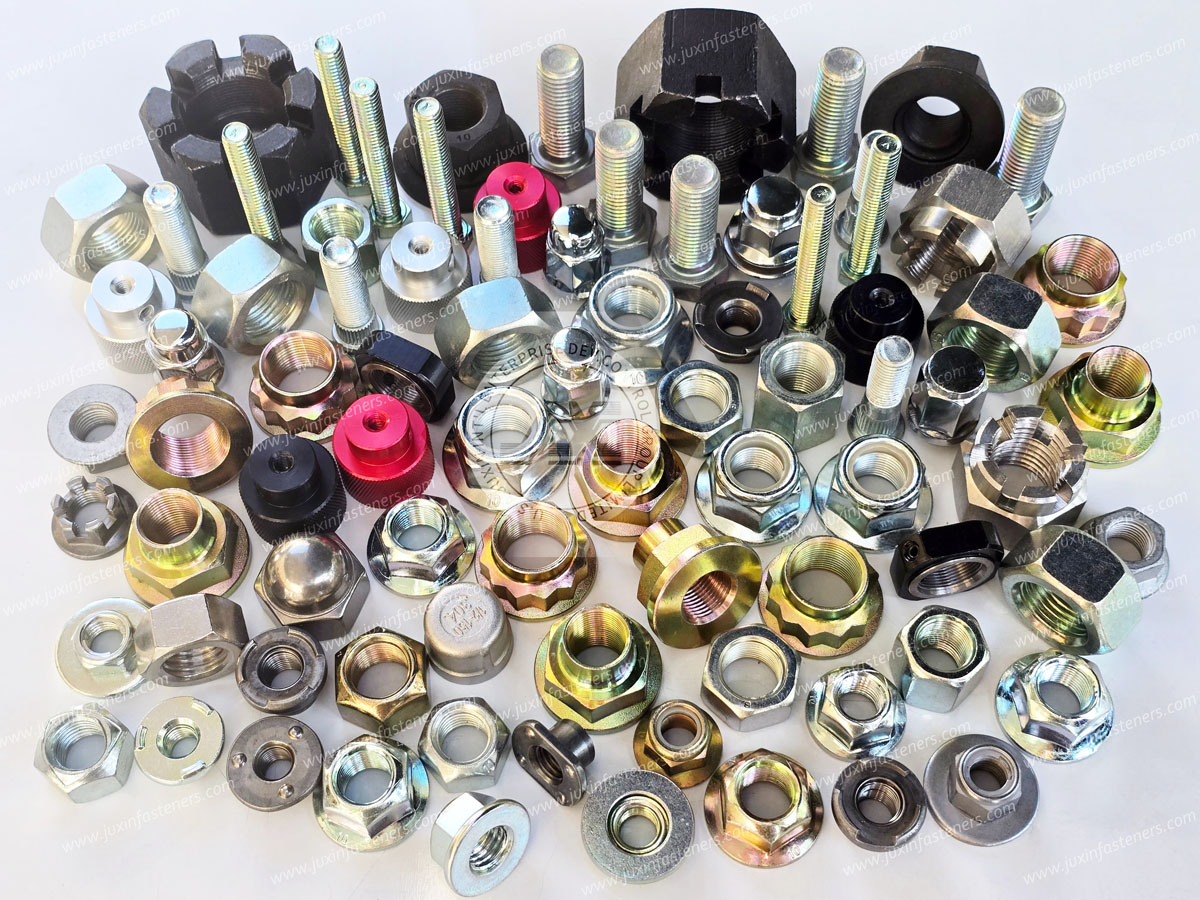
Packaging equipment manufacturers may seek alternative suppliers for screws, bolts, nuts, washers, locking hardware and custom fasteners.
Supplier qualification should consider both technical conformity and commercial supply requirements.
| Evaluation Area | Key Questions |
|---|---|
| Drawing conformity | Are dimensions, threads and tolerances correct? |
| Material specification | Is the required material grade identified? |
| Mechanical properties | Does the fastener meet the required property class? |
| Joint compatibility | Is the fastener suitable for the intended loading and installation method? |
| Surface treatment | Does the finish meet the agreed environmental requirements? |
| Functional performance | Are locking, wear or retention requirements defined? |
| Inspection | Which dimensions and characteristics require verification? |
| Documentation | Which material and inspection records are required? |
| Commercial supply | What are the MOQ, annual demand and delivery expectations? |
Some packaging machinery projects require material inspection documentation under EN 10204.
The specific document type should be identified during procurement.
An EN 10204 3.1 inspection certificate should not be assumed for every standard industrial fastener.
Where required, documentation availability and traceability requirements must be confirmed before order acceptance.
Two fasteners with the same nominal dimensions may differ in:
Material grade
Mechanical properties
Head geometry
Shoulder dimensions
Thread position
Coating thickness
Installation friction
Locking characteristics
For precision packaging machinery, dimensional similarity alone does not establish functional equivalence.
The OEM should define the required validation and approval procedures.
JUXIN FASTENERS supports OEM sourcing and drawing-based technical review for industrial fasteners used in suitable packaging and bottling equipment applications.
For cartoning machines, bottling lines, case packers, labeling systems, packaging conveyors and automated packaging equipment, please provide:
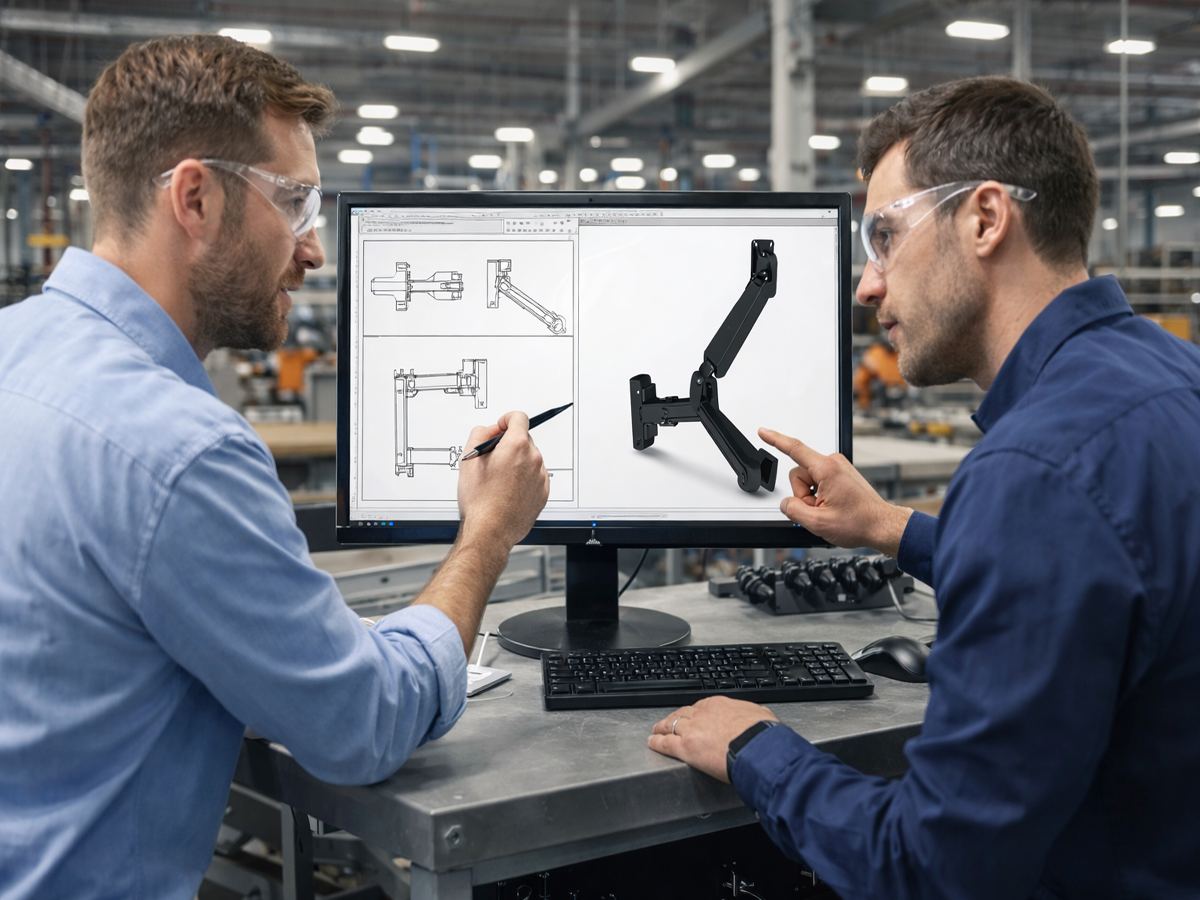
2D drawings and available 3D models
Fastener type and thread specification
Material and mechanical property requirements
Joint loading and installation conditions
Required surface treatment
Changeover or maintenance requirements
Inspection and testing requirements
Prototype quantity and annual forecast
Packaging and delivery requirements
For food-contact, washdown-intensive or high-cycle mechanisms, please also identify the applicable equipment specifications and qualification requirements.
Our team can review the supplied information to discuss suitable standard and custom fastening options and quotation feasibility.
Website: www.juxinfasteners.com
OEM Technical Review & RFQ: info@juxinfasteners.com
Send your drawings and purchasing requirements to discuss fastening solutions for your next packaging machinery project.
Stainless Steel Fasteners for Food Processing & Packaging Machinery — washdown exposure and stainless steel equipment fastening.
Industrial Automation & Robotics Fasteners: Precision Mounting and OEM Hardware Solutions — precision mounting for automated machinery.
All-Metal Prevailing-Torque Lock Nuts for High-Vibration Industrial Assemblies — vibration-resistant mechanical fastening.
Custom Cold-Headed Fasteners & Special Formed Parts for Industrial OEMs — drawing-based custom fastener sourcing.
These related topics provide additional guidance on corrosion-resistant hardware, automated equipment fastening, maintenance efficiency and OEM supplier qualification.
 MORE NEWS
Oct. 13, 2026
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY