
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Mar. 30, 2026
Threaded Inserts for EV Battery Modules: Plastic Housing Design, Retention and OEM Assembly
Electric vehicle battery systems combine lightweight structures, electronic controls, thermal management components and demanding automotive reliability requirements.
Many of these assemblies incorporate engineering plastics, aluminum components, composite structures and thin-wall housings.
These materials help manufacturers reduce weight and integrate complex component geometries.
However, fastening directly into lightweight materials can create challenges involving thread wear, limited engagement strength, material deformation and repeated assembly.
Threaded inserts for EV battery modules provide durable internal metal threads in appropriately designed host components.
They can support removable screw connections for selected battery-related housings, mounting brackets, electronic assemblies and serviceable covers.
For OEM engineers, the critical question is not simply whether an insert fits the component.
It is whether the complete insert–host material–screw joint can withstand its specified mechanical, thermal and environmental conditions.
For manufacturing engineers and production managers, insert installation must also be compatible with production cycle time, process monitoring and repeatable quality.
For procurement and supplier development teams, material consistency, dimensional compliance, approved drawings, inspection requirements and stable supply influence the final sourcing decision.
Juxin Fasteners welcomes inquiries for automotive threaded inserts and custom fastening components for EV-related applications.
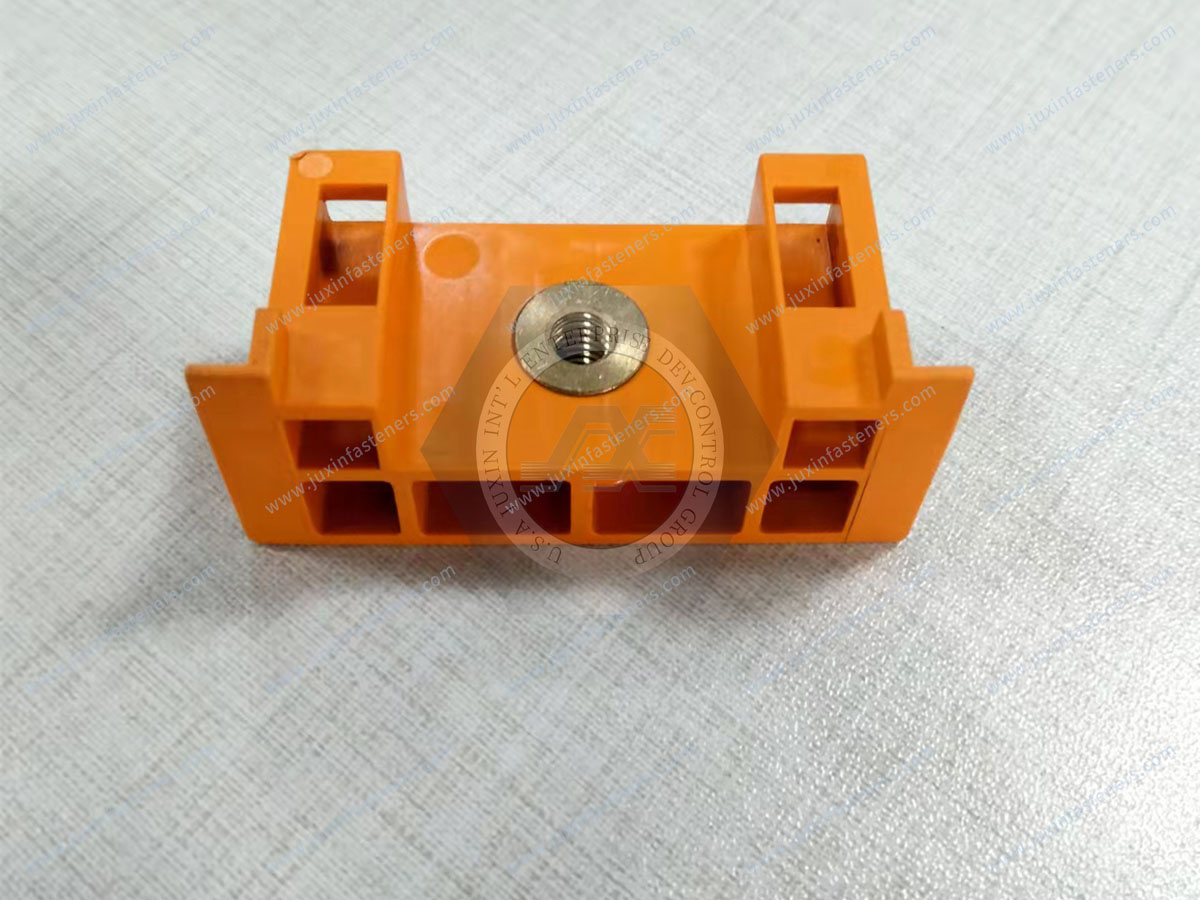
Why Are Threaded Inserts Used in EV Battery Components?
Electric vehicle battery-related components may experience:
Vehicle vibration and mechanical shock
Thermal expansion and contraction
Repeated temperature cycling
Humidity and environmental exposure
Assembly and maintenance operations
Long-term loading of plastic structures
Directly formed threads in certain plastics may not provide adequate durability when a screw is repeatedly installed and removed.
A threaded insert introduces a separate metal female thread into the host component.
Potential Benefits
Improved resistance to thread wear
Reusable threaded connections
Reduced damage to the host material during screw replacement
Consistent mating thread geometry
Greater flexibility in selecting screw materials
Improved suitability for controlled assembly processes
Actual performance depends on insert geometry, host material, installation quality and joint design.
Important Engineering Distinction
A threaded insert does not automatically provide vibration resistance, electrical isolation or environmental sealing.
Those functions must be addressed through the complete assembly design.
Where Are Threaded Inserts Used in EV Battery Systems?
Threaded inserts may be relevant to several different EV battery-related assemblies.
Plastic Battery Module Housings
Engineering plastic housings may require threaded attachment points for:
Protective covers
Internal mounting brackets
Electronic component supports
Cable management components
Selected serviceable attachments
The insert must be selected according to the plastic material, boss geometry and expected service loads.
Battery Monitoring and Electronics Housings
Battery management system components and related electronics may use threaded inserts in plastic enclosures.
Potential applications include:
Electronic control housings
Sensor mounting structures
Connector support brackets
Protective covers
Electronic module fixtures
Design priorities include dimensional stability, controlled screw tightening and suitable electrical clearance.
Thermal Management Assemblies
EV battery thermal management systems may incorporate plastic brackets, covers and electronic support components.
Threaded inserts can provide fastening points for:
Cooling system support brackets
Temperature sensor housings
Thermal management control components
Protective panels
Auxiliary mounting structures
The joint must be evaluated for temperature exposure, differential thermal expansion and vibration.
Battery Covers and Serviceable Components
Threaded inserts can support removable fasteners in selected housing covers.
However, a threaded insert alone does not establish a sealed enclosure.
Where moisture protection is required, the complete joint must include an appropriately designed sealing system.
Important Application Boundary
Primary battery structural connections, crash-load paths, electrical busbar connections and safety-critical joints require dedicated engineering validation.
A plastic threaded insert should not be treated as a universal replacement for structural bolts, weld nuts or other engineered fastening systems.
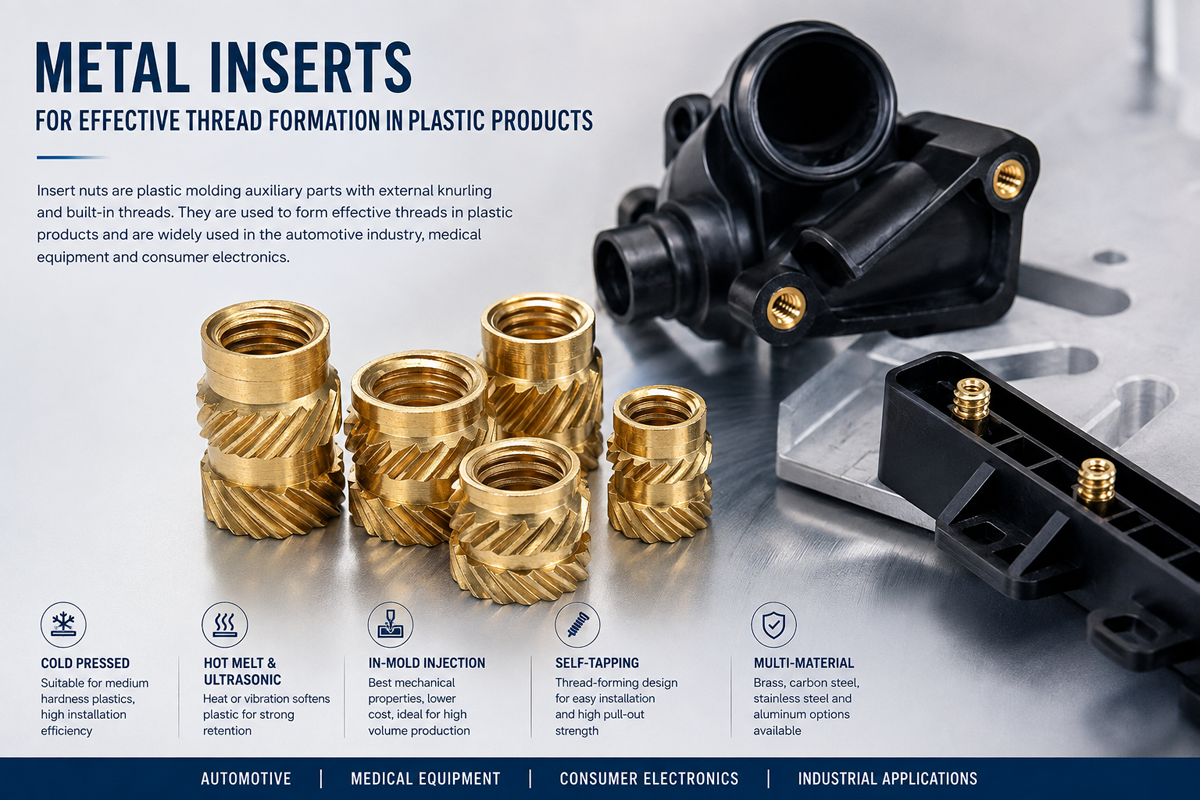
Threaded Insert Materials for EV Battery Applications
Material selection influences mechanical behavior, corrosion resistance, electrical conductivity, weight and manufacturing cost.
The appropriate choice depends on the host material and operating environment.
Brass Threaded Inserts
Brass is widely used for threaded inserts in thermoplastic components.
Potential advantages include:
Good machinability
Suitable internal thread durability
Compatibility with many established heat-insertion designs
Corrosion resistance in appropriate environments
Good thermal conductivity for heat-assisted installation
Potential EV Applications
Plastic electronics housings
Sensor enclosures
Battery-related protective covers
Engineering plastic brackets
Serviceable plastic components
Engineering Considerations
Brass is electrically conductive.
Where an insert is located near energized components, the design must maintain the required electrical clearances and insulation barriers.
Brass also has different thermal expansion characteristics from many engineering plastics.
Retention performance must therefore be evaluated across the specified operating temperature range.
Stainless Steel Threaded Inserts
Stainless steel inserts may be considered when higher mechanical properties or particular corrosion-resistance requirements are important.
Potential applications include:
Moisture-exposed equipment
Selected battery enclosure components
Automotive electronics
Industrial EV charging-related equipment
Specialized lightweight assemblies
Engineering Considerations
Stainless steel grade
Mechanical properties
Corrosion exposure
Installation method
Thread galling risk
Host material compatibility
Cost
A2 and A4 stainless steel designations may be relevant to certain fastener specifications, but the exact material grade and properties must be defined.
Stainless steel is not automatically appropriate for every plastic insert design or installation process.
Aluminum Threaded Inserts
Aluminum inserts may be evaluated for selected weight-sensitive applications.
Potential advantages include:
Low density
Reduced component mass
Compatibility with certain lightweight assembly concepts
However, aluminum also introduces considerations involving:
Internal thread wear
Material strength
Surface treatment
Galvanic corrosion
Repeated assembly durability
Engineering Recommendation
Use aluminum inserts only where the selected alloy, geometry and thread performance have been validated for the intended application.
Material Comparison
| Selection factor | Brass | Stainless steel | Aluminum |
|---|---|---|---|
| Relative density | Higher | Higher | Lower |
| Corrosion performance | Environment-dependent | Grade-dependent | Alloy and finish-dependent |
| Electrical conductivity | Conductive | Conductive | Conductive |
| Thread durability | Geometry-dependent | Grade-dependent | Alloy-dependent |
| Heat insertion | Common in suitable designs | Requires process evaluation | Requires process evaluation |
| Main consideration | Retention and plastic compatibility | Strength, corrosion and installation | Weight and thread durability |
Important Electrical Design Consideration
All three material groups are electrically conductive.
None should be assumed to provide electrical insulation simply because it is embedded in plastic.
Threaded Insert Types for EV Battery Components
Different host materials and production processes require different installation methods.
Heat-Set Threaded Inserts
Heat-set inserts are commonly installed into suitable thermoplastics after molding.
A controlled heating process softens the surrounding plastic and allows the insert's retention features to become embedded.
Potential Advantages
Suitable for many thermoplastic components
Compatible with post-molding installation
Established installation methods
Reusable internal metal threads
Engineering Limitations
Requires appropriate thermoplastic behavior
Installation temperature must be controlled
Hole geometry affects retention
Excessive heat may damage the boss
Incomplete insertion can cause dimensional problems
Potential EV Applications
Battery electronics housings
Plastic module covers
Sensor housings
Auxiliary mounting components
Molded-In Threaded Inserts
Molded-in inserts are positioned in the mold before the plastic component is formed.
Plastic flows around the insert during molding.
Potential Advantages
Integrated insert placement during molding
No separate post-molding insertion operation
Suitable for certain high-volume production processes
Potential for effective mechanical retention
Engineering Limitations
Insert positioning must be controlled
Mold loading may influence cycle time
Plastic flow and knit lines require consideration
Insert displacement can create defects
Tooling design may become more complex
Important Clarification
Molded-in inserts do not automatically provide the highest pull-out or torque-out strength.
Performance depends on geometry, plastic material, molding conditions and the complete component design.
Self-Tapping Threaded Inserts
Self-tapping inserts create or form engagement features in a compatible host material during installation.
Depending on the specific design, they may be used in certain plastics and other materials.
Potential Advantages
Post-molding installation
No separate heat-insertion step for suitable designs
Mechanical engagement with the host material
Flexibility in selected production processes
Engineering Limitations
Installation torque must be controlled
Hole size is critical
Brittle plastics may crack
Material displacement can damage thin bosses
Insert alignment affects final thread position
Important Clarification
Self-tapping inserts are not universally suitable for every plastic material.
The insert design must be compatible with the host material and specified installation process.
How to Select the Correct Insert Type
| Engineering condition | Potential insert approach | Main validation requirement |
|---|---|---|
| Thermoplastic housing with post-molding assembly | Heat-set insert | Thermal process and retention |
| Injection-molded component with integrated insert placement | Molded-in insert | Mold positioning and plastic flow |
| Compatible material requiring mechanical insertion | Self-tapping insert | Installation torque and boss integrity |
| Repeated service access | Suitable metal threaded insert | Thread wear and retention |
| High-temperature exposure | Application-specific design | Thermal aging and creep |
| High structural loading | Engineered fastening system | Complete joint strength and safety |
The final selection should be based on the actual host material, geometry, loading and production requirements.
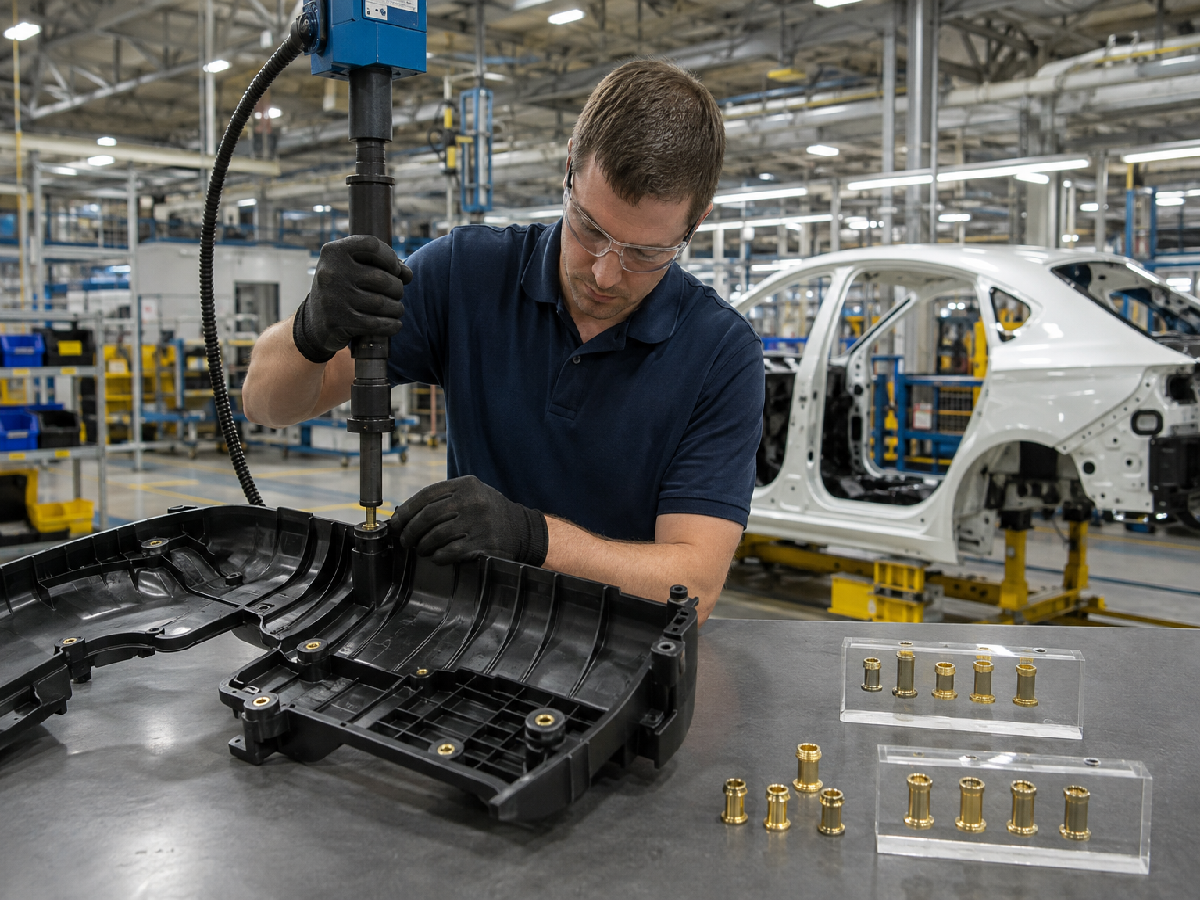
Plastic Boss Design for EV Threaded Inserts
The plastic boss is often the controlling element in an insert joint.
A strong metal insert cannot compensate for an inadequately designed surrounding plastic structure.
Pilot Hole Diameter
The pilot hole must match the insert geometry and installation method.
An oversized hole may reduce mechanical engagement.
An undersized hole may cause excessive insertion stress, plastic cracking or distortion.
Boss Outside Diameter
The boss must provide enough surrounding material to resist expansion forces and service loads.
Insufficient wall thickness can lead to cracking or splitting.
Boss Height
Boss height affects available insert engagement and load distribution.
The selected insert length must be compatible with the available component depth.
Hole Depth
Blind holes must provide sufficient clearance for the insert and any displaced material.
The mating screw must not bottom out before the intended clamp load is developed.
Edge Distance
Inserts placed too close to an unsupported edge may create localized stress concentrations.
Ribs and Reinforcement
Appropriate ribs may improve component stiffness, but poorly positioned ribs can introduce molding defects or local stress.
Engineering Recommendation
Confirm the following dimensions before tooling release:
Insert outside diameter
Insert length
Pilot hole diameter
Pilot hole depth
Boss outside diameter
Boss height
Distance to nearby walls
Screw engagement length
Clearance beneath the screw
The required dimensions must be established for the specific insert and host material.
EV Plastic Material Compatibility
Different engineering plastics respond differently to insertion forces, temperature and long-term loading.
ABS
ABS may be suitable for selected electronics housings, depending on temperature and environmental requirements.
Polycarbonate (PC)
PC offers useful engineering properties but requires attention to molding stress, chemical exposure and boss cracking.
Polyamide (PA / Nylon)
Polyamide properties are influenced by moisture absorption and temperature.
Glass-fiber reinforcement can also affect installation behavior and local stress.
PBT and Other Engineering Thermoplastics
Certain automotive electronics components use engineering thermoplastics selected for dimensional stability, electrical characteristics and thermal performance.
Insert installation must be validated for the specific material grade.
Composite and Thermoset Materials
These materials may not be suitable for conventional heat-set installation.
Mechanical inserts or other application-specific fastening methods may be necessary.
Engineering Recommendation
Specify the exact polymer grade, reinforcement level and relevant conditioning state during validation.
Generic material names are not sufficient for final production approval.
Pull-Out Resistance and Torque-Out Resistance
Two important performance characteristics of threaded inserts are pull-out resistance and torque-out resistance.
Pull-Out Resistance
Pull-out testing evaluates resistance to axial extraction from the host material.
Results depend on:
Insert geometry
Installation method
Host material
Boss dimensions
Test temperature
Loading direction
Conditioning and aging
Torque-Out Resistance
Torque-out testing evaluates resistance to insert rotation within the host material.
This is different from the torque required to tighten the mating screw.
Why Both Matter
An insert may resist axial extraction but rotate under tightening torque.
Alternatively, an insert may resist rotation while the surrounding plastic fails under axial load.
Both failure modes must be considered.
Important Engineering Recommendation
Do not use a single published retention value as proof of suitability for every EV battery component.
Validate the actual insert and molded part under representative conditions.
Screw Tightening and Joint Preload
The internal metal thread of an insert allows a machine screw to engage a durable threaded surface.
However, the surrounding plastic still influences the complete joint.
Relevant Factors
Screw material and thread
Insert thread strength
Plastic stiffness
Joint compression
Under-head bearing area
Friction
Temperature
Long-term creep
Potential Failure Modes
Insert rotation
Insert pull-out
Plastic boss cracking
Screw thread stripping
Excessive plastic compression
Loss of clamp load
Engineering Recommendation
Establish screw tightening torque through application-specific testing.
The torque used to install an insert into plastic is not necessarily the same as the torque used to tighten the mating screw.
Vibration Resistance in EV Battery Assemblies
Vehicle vibration can affect threaded connections over time.
Metal threaded inserts may provide durable internal threads, but they do not automatically prevent the mating screw from loosening.
Potential Causes of Joint Loosening
Inadequate initial preload
Joint settlement
Transverse vibration
Thermal expansion
Plastic creep
Insufficient joint stiffness
Where necessary, the assembly may require an appropriate locking feature or another validated retention method.
Engineering Recommendation
Evaluate insert retention and screw loosening as separate requirements.
Thermal Cycling and Plastic Creep
EV battery-related assemblies can experience temperature changes during operation and environmental exposure.
Metals and polymers generally have different thermal expansion characteristics.
This difference may influence the stresses around an insert.
Potential Effects
Reduced insert retention
Local plastic deformation
Boss cracking
Joint relaxation
Changes in screw preload
Plastic Creep
Under sustained load, certain polymers may deform over time.
This can affect joint compression and insert retention.
Engineering Recommendation
Where relevant, validate the complete joint after thermal cycling, temperature aging and sustained loading.
Electrical Isolation and Battery Safety
Battery systems introduce electrical design requirements that may not be present in ordinary mechanical assemblies.
Metal threaded inserts are electrically conductive.
Potential concerns include:
Unintended conductive paths
Reduced electrical clearance
Insulation damage
Contact with energized components
Galvanic interactions between dissimilar metals
Engineering Recommendation
The insert position, mating screw length, surrounding plastic geometry and electrical insulation system must be reviewed together.
An embedded metal insert should not be assumed to provide electrical isolation.
Battery Enclosure Sealing and Moisture Protection
Threaded inserts may be used in serviceable battery-related covers and enclosure components.
However, the insert itself does not establish an environmental sealing rating.
Where the complete enclosure requires protection against water or dust, the joint may also need:
Gaskets
Sealing surfaces
Suitable compression control
Sealed openings
Environmental validation
IEC 60529 defines the IP code classification system for enclosure protection.
Important Clarification
An IP rating applies to the tested enclosure configuration, not automatically to an individual threaded insert.
Installation Process Control for OEM Production
Production managers must consider whether the selected insert can be installed consistently at the required manufacturing volume.
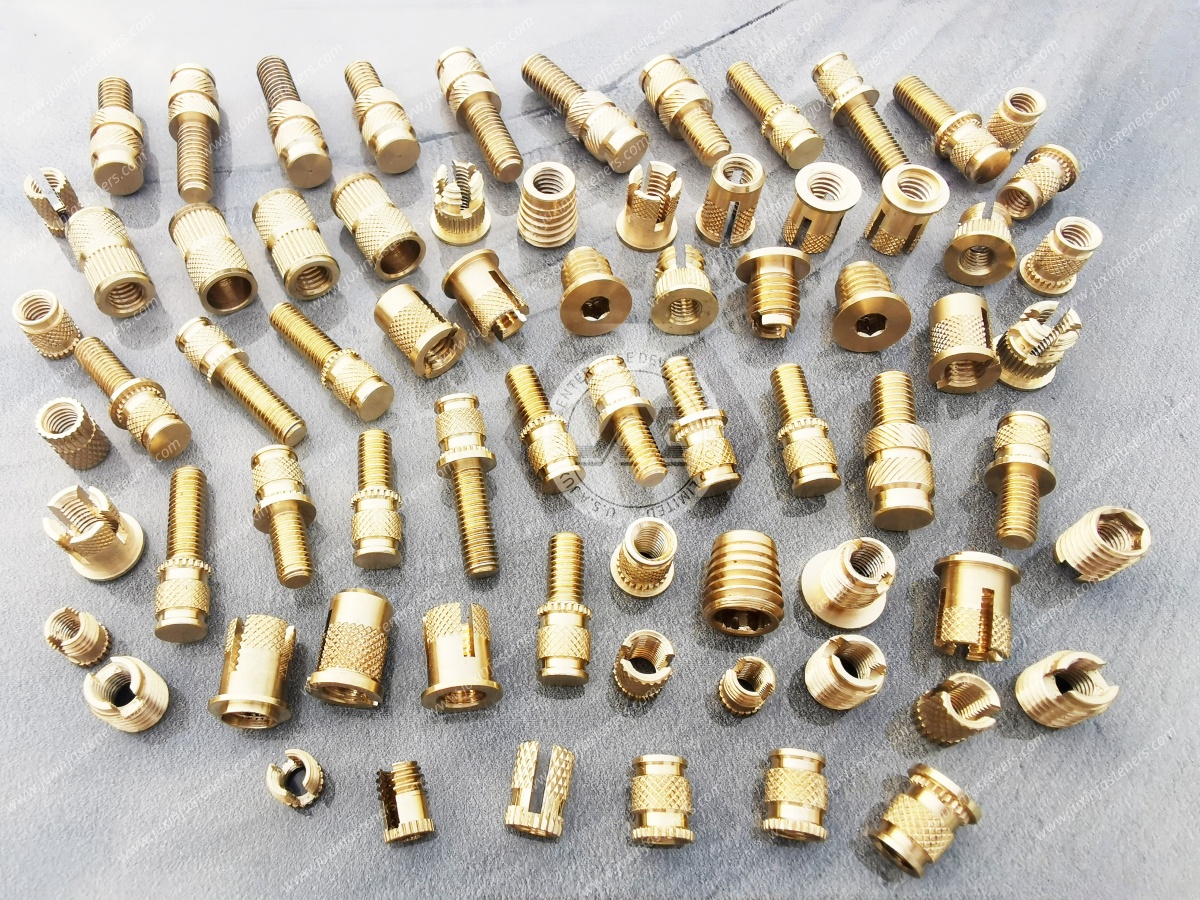
Heat-Set Installation Control
Relevant variables include:
Insert temperature
Heating method
Insertion force
Insertion speed
Insertion depth
Cooling conditions
Host material temperature
Molded-In Insert Control
Relevant variables include:
Insert positioning
Mold loading
Insert retention during injection
Plastic flow
Mold temperature
Part removal
Self-Tapping Insert Control
Relevant variables include:
Pilot hole diameter
Installation torque
Alignment
Insertion depth
Host material condition
Tool condition
Production Quality Indicators
Useful production measurements may include:
Insert seating depth
Installation force or torque
Position accuracy
Reject rate
Rework rate
Cycle time
Tool wear
Information Gain: Installation Consistency Can Matter More Than Nominal Insert Strength
An insert design may achieve satisfactory laboratory retention results but still perform poorly in production if installation conditions vary.
For example, inconsistent heating or hole dimensions may produce different retention levels across otherwise similar molded parts.
Engineering Recommendation
Validate both the insert design and the repeatability of the intended manufacturing process.
Quality Control and Validation for EV Threaded Inserts
OEM quality planning should reflect the actual component function and customer requirements.
Incoming Insert Inspection
Potential inspection characteristics include:
Material identification
Internal thread dimensions
Outside diameter
Insert length
Knurl or retention geometry
Surface condition
Visual defects
Installed Insert Inspection
Potential checks include:
Position
Seating depth
Perpendicularity
Boss damage
Insert movement
Thread condition
Mechanical Testing
Depending on the application, testing may include:
Pull-out resistance
Torque-out resistance
Screw tightening performance
Repeated assembly cycles
Joint load testing
Environmental Validation
Where relevant:
Thermal cycling
Temperature aging
Humidity exposure
Corrosion evaluation
Vibration testing
Relevant Thread Standards
For metric internal threads, ISO 261 and the ISO 965 series may be relevant to thread dimensions and tolerances.
For Unified inch threads, ASME B1.1 may be relevant.
Metric, UNC, UNF and other thread systems must be specified separately.
They are not directly interchangeable.
Metric and Inch Size References
| Metric nominal size | Approximate inch diameter |
|---|---|
| M3 | 0.118 in |
| M4 | 0.157 in |
| M5 | 0.197 in |
| M6 | 0.236 in |
| M8 | 0.315 in |
These values are dimensional references only and do not establish equivalent thread specifications or product availability.
Common Failure Modes and Engineering Prevention
| Failure mode | Potential cause | Recommended evaluation |
|---|---|---|
| Insert pulls out | Insufficient retention or weak boss | Review geometry and axial loading |
| Insert rotates | Inadequate anti-rotation engagement | Review insert profile and torque-out |
| Plastic boss cracks | Excessive insertion stress | Review hole size and installation |
| Screw thread strips | Excessive torque or incompatible thread | Review thread and tightening |
| Insert sits proud | Incorrect depth or installation control | Verify seating process |
| Clamp load decreases | Plastic creep or joint settlement | Evaluate long-term joint behavior |
| Retention changes after heating | Differential expansion or aging | Conduct thermal validation |
| Corrosion develops | Unsuitable material pairing or exposure | Review materials and environment |
| Electrical clearance is compromised | Insert or screw positioning | Review insulation geometry |
| Production rejects increase | Variable installation conditions | Improve process control |
Total Installed Cost and Production Planning
For production managers and purchasing teams, insert unit price is only one part of the total cost.
Relevant cost elements include:
Insert purchase cost
Mold or tooling allocation
Installation equipment
Assembly labor
Inspection
Scrap and rework
Maintenance
Replacement components
Installed Cost per Accepted Assembly
A useful comparison is:
Total production, installation, tooling allocation, inspection and rework costs ÷ accepted assembly output
The calculation should use a consistent production period and avoid double-counting cost elements.
Engineering Recommendation
Compare heat-set, molded-in and self-tapping inserts using the actual production process, annual volume and quality requirements.
The lowest insert unit price does not necessarily result in the lowest total assembly cost.
Custom Threaded Inserts for EV Battery OEM Projects
Different EV battery-related components may require application-specific insert dimensions and materials.
Potential custom requirements include:
Internal thread diameter
Thread pitch
Insert length
Outside diameter
Knurl pattern
Retention geometry
Material grade
Surface finish
Installation method
Packaging requirements
Engineering Recommendation
Provide a complete drawing and identify the host material and installation process.
A drawing without the surrounding component information may not be sufficient to evaluate retention performance.
OEM Supplier Qualification and Procurement Requirements
Purchasing and supplier development teams should evaluate technical and commercial requirements together.
Technical Requirements
Drawing compliance
Material specification
Thread accuracy
Retention geometry
Surface condition
Installation compatibility
Inspection criteria
Production Requirements
Dimensional consistency
Process control
Traceability where required
Packaging
Engineering change management
Production planning
Commercial Requirements
Prototype quantities
MOQ
Annual purchasing volume
Lead time
Unit price
Supply continuity
Delivery requirements
Specific commercial conditions must be confirmed for each RFQ.
OEM RFQ Checklist
| RFQ item | Information to provide |
|---|---|
| Product drawing | Part number and revision |
| Insert type | Heat-set, molded-in, self-tapping or specified design |
| Thread | Metric or specified inch thread |
| Insert dimensions | OD, length and tolerances |
| Material | Brass, stainless steel, aluminum or specified grade |
| Host material | Exact polymer or substrate grade |
| Boss geometry | Hole diameter, depth and wall thickness |
| Installation | Process and equipment |
| Loading | Axial, torsional and service loads |
| Temperature | Operating and validation range |
| Environment | Humidity, corrosion and chemical exposure |
| Electrical requirements | Clearance and insulation requirements |
| Validation | Pull-out, torque-out and other required tests |
| Samples | Prototype quantity |
| Annual demand | Volume forecast |
| MOQ | Commercial confirmation |
| Lead time | Required schedule |
| Packaging | Bulk or production-compatible |
Frequently Asked Questions
What are threaded inserts used for in EV battery modules?
They provide reusable metal threads in selected plastic and lightweight components such as electronics housings, covers and mounting structures.
Are brass threaded inserts suitable for EV battery plastic housings?
They may be suitable for compatible engineering plastics, subject to retention, temperature, electrical and application requirements.
Which insert is strongest: heat-set, molded-in or self-tapping?
There is no universally strongest method. Performance depends on insert geometry, host material, boss design, installation and loading.
Do threaded inserts prevent screws from loosening under vibration?
Not automatically. Insert retention and screw loosening are separate engineering considerations.
Can threaded inserts be used in aluminum battery enclosures?
Certain insert designs may be suitable for metal components, but inserts intended for plastic should not automatically be used in aluminum.
The host material and installation method must match the selected insert.
Are threaded inserts electrically insulating?
Metal inserts are conductive. Electrical isolation must be provided by the overall component design where required.
Can threaded inserts be used for IP-rated battery covers?
They can be part of a sealed assembly, but the complete enclosure and sealing system must be validated.
Can EV battery inserts be supplied with UNC or UNF threads?
Such thread requirements can be reviewed against the specific product drawing.
Availability must be confirmed, and Unified inch threads are not interchangeable with metric threads.
What tests should an OEM request?
Depending on the application, relevant evaluations may include pull-out, torque-out, repeated assembly, thermal cycling, vibration and installed joint performance.
What information is needed for a custom insert quotation?
Provide the insert drawing, material, host component design, installation method, required performance, annual volume and delivery requirements.
Juxin Fasteners: EV Battery Threaded Insert and OEM Fastening Solutions
Juxin Fasteners welcomes inquiries for threaded inserts and custom fastening components used in automotive and industrial applications.
Relevant product categories include:
Brass threaded inserts
Stainless steel threaded inserts
Aluminum threaded inserts
Heat-set threaded inserts
Molded-in threaded inserts
Self-tapping threaded inserts
Custom threaded inserts for plastic components
Drawing-specific OEM fastening components
Specific material grades, dimensions, production requirements, testing, MOQ and delivery schedules require confirmation.
Request an EV Battery Threaded Insert Quotation
Are you developing an EV battery electronics housing, lightweight plastic component, thermal management bracket,
protective cover or other automotive assembly requiring durable threaded connections?
Juxin Fasteners welcomes technical and commercial inquiries from:
Automotive design engineers
Mechanical and structural engineers
Manufacturing engineers
Production managers
Purchasing specialists
Procurement managers
Supplier development teams
Supply chain managers
For an efficient technical review, please send:
Insert drawing + thread specification + material grade + host polymer or substrate + boss geometry + installation method
+ loading requirements + operating temperature + environmental requirements + electrical considerations
+ validation criteria + prototype quantity + annual volume + packaging + delivery schedule.
Our team can review the requirements and confirm suitable product options, technical feasibility and quotation conditions.
Company: Juxin Fasteners
Website: https://www.juxinfasteners.com/
Email: info@juxinfasteners.com
Send your EV battery threaded insert drawings and OEM RFQ to Juxin Fasteners for technical confirmation and quotation.
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY



