
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Apr. 21, 2026
Three-Projection Weld Studs for Telecom Enclosures, RF Equipment and Communication Cabinets
Telecommunications equipment manufacturers require reliable fastening solutions for sheet metal cabinets, RF equipment housings,
antenna support structures, power distribution enclosures and electronic control assemblies.
These products frequently combine fabricated metal panels with internal brackets, mechanical supports, electronic components and serviceable equipment modules.
A common engineering challenge is creating a permanent male-threaded attachment point on a metallic panel without introducing an unnecessary through-hole in the parent sheet.
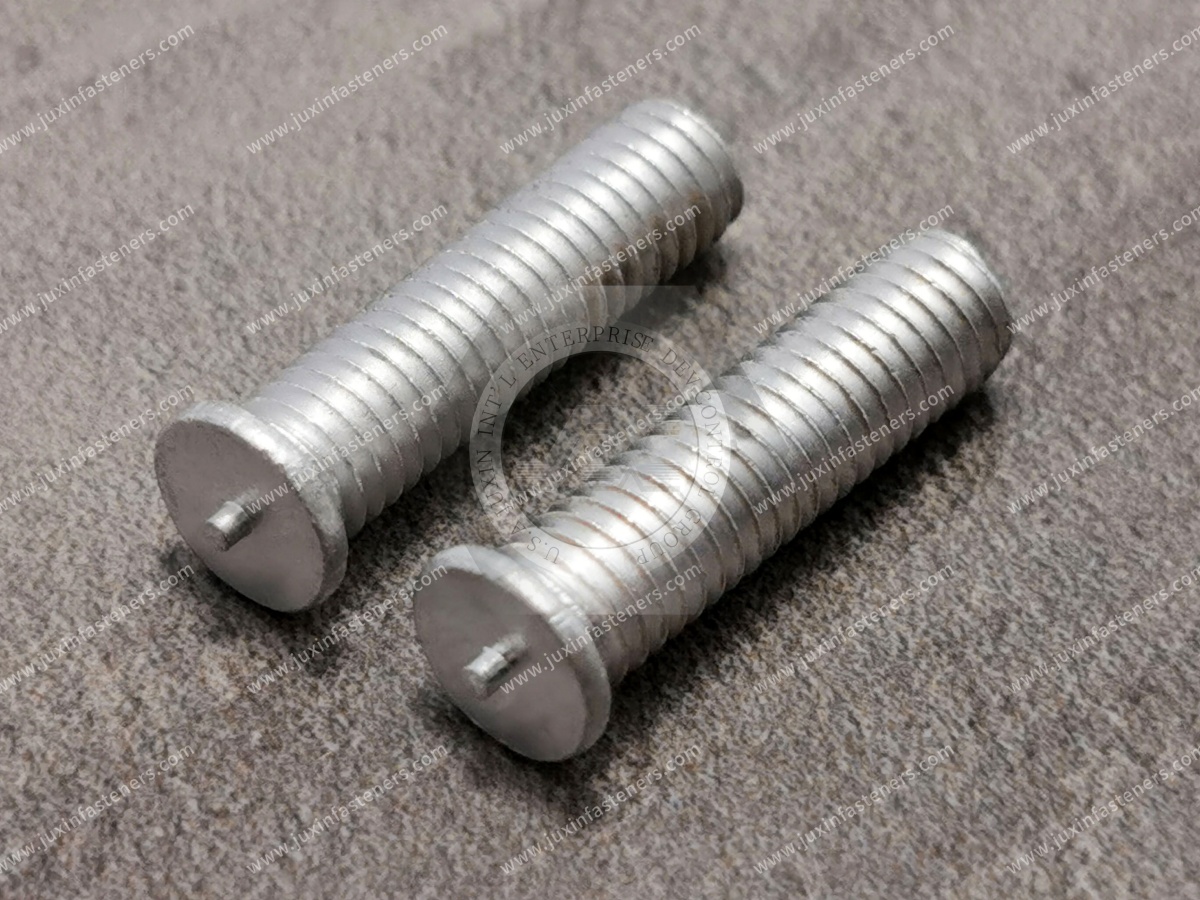
One fastening solution is the Weld Stud with 3 Projections on Top of Head, also described as a top-of-head projection weld stud,
three-projection weld screw or, for applicable configurations, an IFI-148 Type T3 projection weld stud.
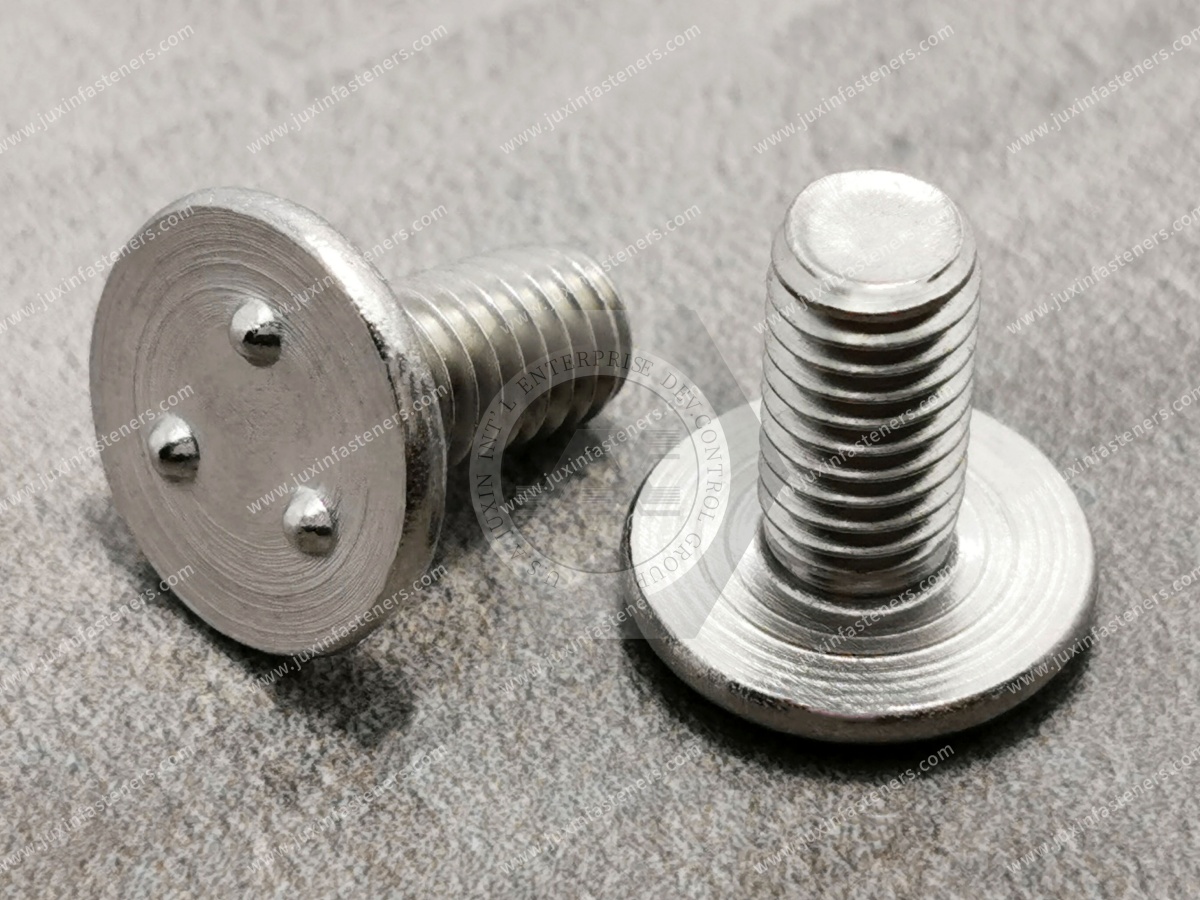
This fastener incorporates three formed welding projections on the top face of its head.
During resistance projection welding, these projections establish localized contact regions between the stud and a compatible metallic workpiece.
The threaded shank extends away from the welded interface, providing a permanent externally threaded mounting point for suitable brackets, support structures and mechanical accessories.
Unlike certain through-hole fastening arrangements, the top-of-head configuration does not inherently require a clearance hole for the threaded shank in the parent panel.
However, selecting the correct weld stud requires more than matching thread diameter and length.
Substrate material, sheet thickness, projection geometry, welding equipment, mechanical loading, corrosion protection and production repeatability all influence the finished assembly.
For design engineers, manufacturing engineers, production managers and international procurement teams, successful selection requires evaluation of the complete fastener, workpiece, welding process and finished joint.
JUXIN FASTENERS supplies industrial projection weld studs and related fastening components for suitable standard and drawing-based OEM applications.
Understanding Three-Projection Top-of-Head Weld Studs
A three-projection top-of-head weld stud combines an externally threaded shank with a formed head incorporating three localized welding projections.
The projections are positioned on the head face intended to contact the parent metal.
During resistance projection welding, electrical current and electrode force produce localized heating and controlled projection deformation as the joint develops.
The resulting attachment provides a male-threaded mounting point for compatible nuts, brackets and other mechanical components.
Main Structural Features
| Component | Engineering Function |
|---|---|
| External threaded shank | Provides the male-threaded mounting interface |
| Formed stud head | Transfers mechanical loads toward the welded joint |
| Three welding projections | Establish localized contact regions for resistance welding |
| Head-to-shank transition | Influences geometry and mechanical load transfer |
| Material and surface condition | Affect mechanical properties and welding behavior |
The fastener's actual dimensions, tolerances, material, thread specification and projection geometry must be established by the applicable product drawing.
Why Projection Position Matters
The position of the welding projections determines how the fastener contacts the parent sheet during installation.
For the top-of-head configuration, the projections are located on the head face rather than on a conventional weld end at the tip of the threaded shank.
This arrangement allows the threaded shank to remain accessible after the head has been welded to a suitable metal surface.
A clearance hole through the parent panel for the shank is not inherently required.
This distinction is important when comparing top-of-head projection weld studs with through-hole projection weld studs, capacitor discharge studs and other welded threaded fasteners.
These products should not be treated as interchangeable without checking their installation methods and engineering drawings.
Why Telecommunications Manufacturers Use Projection Weld Studs
Communication equipment manufacturers frequently work with fabricated sheet metal panels, brackets, internal frames and equipment mounting plates.
These assemblies may require permanent threaded attachment points while maintaining controlled panel geometry and efficient downstream assembly.
Top-of-head projection weld studs may offer several advantages when the application and welding process are suitable.
Permanent Threaded Mounting
A welded stud provides an externally threaded mounting point that remains attached to the parent metal during subsequent mechanical assembly.
This can be useful for brackets, equipment supports and mechanical accessories.
No Required Stud-Shank Mounting Hole
The top-of-head configuration may eliminate the need for a through-hole at the mounting location.
This can be useful where a continuous outer panel surface is desired.
However, eliminating the mounting hole does not automatically guarantee sealing performance, structural strength or cosmetic quality.
Potential Assembly Simplification
A welded threaded attachment may reduce the need for certain loose fastening components or through-bolting arrangements.
The actual benefit depends on the assembly design and manufacturing process.
Compatibility with Repetitive Manufacturing
Resistance projection welding may be incorporated into suitable repetitive sheet metal production operations.
Fastener positioning, electrode access, fixture design and process control must be evaluated before automated production is approved.
Telecommunications Cabinets and Outdoor Equipment Enclosures
Telecommunications cabinets contain internal mounting brackets, electronic equipment supports, cable management hardware,
power distribution components and mechanical accessories.
A three-projection weld stud may provide a permanent threaded mounting point on a suitable steel panel, mounting plate or bracket.
Potential Applications
Internal equipment mounting brackets
Cable management support plates
Mechanical accessory supports
Equipment mounting frames
Internal reinforcement brackets
Selected electrical enclosure components
Engineering Selection Considerations
The design engineer should evaluate the sheet material and thickness, bracket load, thread size, stud position,
available welding access, tightening torque and required corrosion protection.
The mounting location must also be checked against adjacent components, maintenance access and installation clearances.
Outdoor Equipment Requirements
Outdoor telecommunications equipment may experience moisture, condensation, temperature cycling, vibration and corrosive environmental conditions.
A welded stud does not independently establish the enclosure's weather resistance.
The complete assembly, including weld regions, coatings, mating components and any sealing arrangements, should be evaluated against the applicable environmental requirements.
Antenna Equipment and RF Mounting Structures
Antenna systems and RF equipment may incorporate metallic brackets, support plates, covers and internal mechanical structures.
Three-projection weld studs may be considered for suitable mechanical attachment points within these assemblies.
Examples include antenna equipment brackets, RF module support plates, cable-routing brackets and internal mounting structures.
Mechanical Loading Requirements
Depending on the equipment design, the welded connection may experience static tension, transverse shear, vibration, assembly torque, fatigue or environmental loading.
Outdoor antenna structures may also experience wind-induced loads and thermal cycling.
The required weld performance should be based on the actual loading conditions.
A fastener's nominal mechanical strength does not automatically establish the mechanical capacity of the welded interface.
RF Performance Considerations
A mechanically acceptable attachment does not necessarily satisfy RF performance requirements.
Where a welded stud is located within a sensitive RF structure or forms part of an intended conductive path,
its position, geometry and electrical contact conditions may influence the equipment design.
RF performance should be evaluated at the appropriate subsystem or assembly level.
EMI/RFI Shielding Enclosures and Electrical Bonding
Communication electronics frequently use conductive housings, covers and gaskets to control electromagnetic interference.
A three-projection weld stud may provide a mechanical attachment point for shielding covers, brackets or related components.
However, the presence of a welded stud does not automatically improve shielding effectiveness.
Factors Affecting Shielding Performance
Panel material and electrical conductivity
Seam and joint geometry
Aperture dimensions
Shielding gasket design
Fastener spacing
Contact pressure
Surface coatings
Electrical continuity
Shielding performance depends on the complete enclosure rather than the fastener alone.
Mechanical Attachment Versus Electrical Bonding
Mechanical strength and electrical continuity are separate engineering requirements.
A welded stud may provide sufficient mechanical attachment while failing to meet a specified electrical bonding resistance.
Where grounding or bonding is required, engineers should define the intended conductive path, acceptable electrical resistance and verification method.
Coatings, corrosion, contact geometry and mating hardware may influence electrical performance.
A mechanical weld test cannot substitute for electrical bonding validation.
PCB Mounting and Electronic Equipment Chassis
Printed circuit board assemblies frequently require spacers, standoffs, support brackets and other mechanical mounting hardware.
A three-projection weld stud may be considered where a suitable metallic chassis or support bracket requires a permanent threaded mounting point.
Projection welding is not normally performed directly onto a populated PCB.
Manufacturing Sequence
For suitable applications, welding may be performed during the metal fabrication stage before sensitive electronic components are installed.
A typical engineering sequence may include metal fabrication, weld stud installation, weld inspection, surface finishing,
dimensional verification, mechanical assembly and electronic component installation.
The actual sequence depends on the equipment design and production requirements.
When Self-Clinching Standoffs May Be More Appropriate
A self-clinching standoff may be preferable when the assembly requires a defined spacing function or when welding is unsuitable.
Selection depends on sheet thickness, material hardness, hole geometry, installation access and required retention performance.
The correct fastener should be selected according to the mechanical function rather than simply because the equipment contains electronic components.
Cable Management and Harness Support Brackets
Telecommunications equipment contains wiring harnesses, cable-routing structures, connectors and serviceable electrical assemblies.
Three-projection weld studs may provide permanent threaded mounting points for compatible metallic support brackets.
Engineering considerations include cable loads, vibration, thread engagement, tightening torque, corrosion protection and maintenance access.
Stud locations should avoid interference with cables, connectors, ventilation paths and service operations.
Resistance Projection Welding: Process and Engineering Principles
Resistance projection welding uses intentionally formed projections to localize initial electrical contact between the fastener and parent metal.
Electrical resistance produces heat at the intended interface while electrode force controls contact and deformation.
As the projections heat and collapse, the welded joint develops.
General Welding Sequence
Position the projection-bearing head against the parent metal.
Establish suitable electrode contact and workpiece support.
Apply the specified electrode force.
Pass welding current through the intended contact regions.
Allow localized heating and controlled projection collapse.
Maintain appropriate force during weld formation and the required hold period.
Inspect the resulting joint against the applicable acceptance criteria.
The welding cycle must be developed for the actual fastener, substrate and equipment combination.
Resistance Projection Welding Versus Capacitor Discharge Stud Welding
A three-projection top-of-head weld stud is intended for resistance projection welding.
Conventional capacitor discharge stud welding uses a different joining arrangement and weld-end configuration.
Although some resistance welding systems use capacitor-based energy storage, this does not make the two fastening methods interchangeable.
Equipment selection must follow the actual joining process and joint design.
Why Universal Welding Parameters Are Unreliable
Welding current, welding time and electrode force cannot be established from stud diameter alone.
Relevant variables include material composition, projection geometry, sheet thickness, surface coatings, contact resistance,
electrode arrangement, welding power source and mechanical follow-up.
A welding schedule developed for one fastener and substrate combination should not be transferred directly to another without appropriate validation.
Projection Geometry and Its Effect on Weld Formation
The three formed projections are central to the fastener's welding behavior.
Their dimensions and relative positions influence initial contact, current distribution and deformation during welding.
Projection Height
Projection height affects which contact regions first touch the parent sheet.
If one projection is higher than the others, it may establish contact first and alter the initial distribution of force and current.
Projection-height tolerances should be established by the applicable engineering drawing.
Projection Shape
Projection shape influences contact area and resistance to premature deformation.
A projection must remain sufficiently stable during initial electrode loading while allowing appropriate deformation during the welding cycle.
Projection Position
The position and spacing of the three projections influence the distribution of contact regions across the head.
Incorrect spacing or location may contribute to uneven welding behavior.
Projection Volume
Projection volume affects the amount of material involved in heating and deformation.
Two projections with similar nominal heights may behave differently if their contact geometry or material volume differs.
Why Equal Projection Dimensions Do Not Guarantee Equal Weld Quality
Even geometrically consistent projections may develop differently because of sheet flatness, electrode alignment,
surface contamination, coating variation, fixture movement or unequal electrical contact.
Therefore, projection geometry inspection and finished weld validation serve different purposes.
Dimensional conformity alone is not proof of acceptable weld performance.
Electrode Force, Alignment and Mechanical Follow-Up
Resistance projection welding requires coordinated control of current, force and mechanical movement.
Excessive Initial Force
Excessive electrode force or impact may deform the projections before sufficient welding heat develops.
This may reduce the intended localization of heating.
Insufficient Force
Insufficient force may contribute to unstable contact, excessive expulsion or inconsistent weld formation.
Mechanical Follow-Up
As the projections collapse, the welding head must accommodate changes in joint thickness.
Inadequate follow-up can affect contact pressure and welding consistency.
Electrode Alignment
Misalignment may create uneven pressure across the projections.
This can contribute to unequal collapse, stud tilt or inconsistent welding results.
Equipment Rigidity
Machine deflection, fixture movement and inconsistent positioning may influence the process.
For high-volume production, welding equipment characteristics can be as important as the stud's dimensional conformity.
Thin Sheet Metal Welding and Distortion Control
Communication equipment enclosures frequently use relatively thin fabricated metal panels.
Projection welding on thin sheet metal requires careful control of heat generation, electrode force and workpiece support.
Potential Manufacturing Risks
Local indentation
Exterior surface marking
Sheet distortion
Excessive weld expulsion
Incomplete weld formation
Burn-through
Stud misalignment
Insufficient joint strength
Why Reducing Welding Current Is Not Always the Solution
Lower current may reduce certain overheating risks, but insufficient current may also prevent adequate weld formation.
The correct welding schedule must balance heat generation, projection collapse, electrode force and required joint performance.
No Universal Minimum Sheet Thickness
The minimum suitable sheet thickness cannot be determined from the thread diameter alone.
Stud-head geometry, projection dimensions, material properties, welding equipment and mechanical requirements must be evaluated together.
Exterior Appearance and Mechanical Strength
A welded stud may satisfy a mechanical test while leaving unacceptable surface marks.
Conversely, an acceptable exterior appearance does not prove adequate weld strength.
Where both structural and cosmetic requirements apply, each must be evaluated separately.
Material Selection for Telecommunications Weld Studs
Material selection should consider both mechanical performance and weldability.
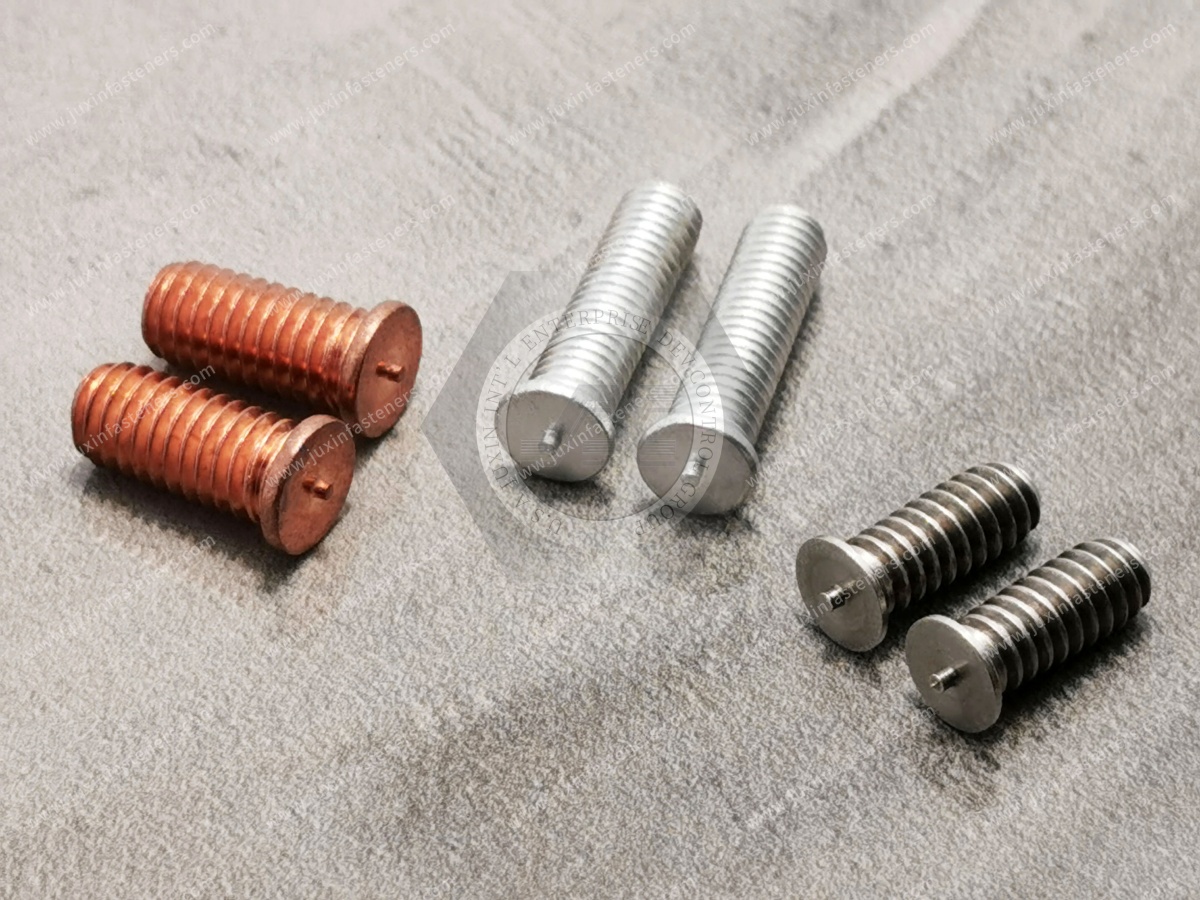
Carbon Steel
Suitable welding-quality carbon steel may be used for resistance projection welding applications.
Relevant requirements include chemical composition, mechanical properties, surface condition, heat-treatment condition and corrosion protection.
Low-carbon steel configurations may be suitable for certain applications, subject to the actual product and substrate requirements.
Stainless Steel
Stainless steel may be considered where corrosion resistance is important.
However, different stainless steel grades have different electrical resistivity, thermal behavior and mechanical properties.
The welding procedure must be appropriate for the selected grade and parent metal.
Aluminum Equipment Enclosures
Aluminum is commonly used in electronic and telecommunications equipment housings.
A conventional carbon steel projection weld stud should not be assumed suitable for direct welding to an aluminum panel.
Dissimilar-metal joining requires specific engineering evaluation.
Where welding is unsuitable, alternative mechanical fastening methods may be more appropriate.
Higher-Strength Steel Fasteners
A higher mechanical property class does not automatically provide better weldability.
Material composition, heat treatment and heat-affected-zone behavior may influence the welded joint.
For example, specifying a higher-strength fastener without reviewing weldability can introduce risks that are not evident from nominal tensile properties alone.
The fastener material and welding process must be considered together.
Surface Finishes and Corrosion Protection
Telecommunications equipment may operate in indoor, outdoor or environmentally demanding conditions.
The surface finish should be selected for the complete assembly rather than the fastener alone.
Plain Steel
Plain or appropriately prepared steel may be suitable where welding occurs before final coating.
The surface condition should support repeatable electrical contact and weld formation.
Zinc-Coated Steel
Zinc coatings may affect contact resistance, welding behavior, expulsion and electrode wear.
The coating specification must be compatible with the intended welding process.
Stainless Steel
Stainless steel may provide corrosion resistance, but the selected grade and service environment remain important.
Post-Weld Coating
Where appropriate, corrosion protection may be applied after welding.
The finishing process should not interfere with critical threads, electrical interfaces or dimensional requirements.
Outdoor Corrosion Performance
The weld region, adjacent sheet metal, coating system and mating components should be evaluated together.
A corrosion-resistant fastener material does not automatically guarantee corrosion resistance of the complete welded assembly.
IFI-148 Type T3 and Thread Specifications
IFI-148 is a relevant dimensional reference for certain threaded projection weld studs.
For applicable configurations, Type T3 identifies a particular three-projection arrangement.
The actual product must be checked against the applicable standard edition and engineering drawing before conformity is claimed.
What the Product Designation Does Not Automatically Define
A Type T3 designation alone does not establish material grade, surface finish, welding parameters, mechanical weld strength,
suitable sheet thickness, corrosion resistance, automated feeding compatibility or stock availability.
These requirements must be specified separately.
Metric and Unified Inch Threads
Relevant thread references include:
ISO 261 for general-purpose metric screw thread series
ISO 965 for metric thread tolerances
ASME B1.1 for Unified inch screw threads
Metric, UNC and UNF threads are different systems.
BSW and BSF are also distinct thread systems.
Similar nominal diameters do not establish interchangeability.
Thread selection should follow the mating component drawing, tolerance requirements and actual assembly design.
Welding Standards and Process Qualification
The applicable welding standards and qualification requirements must match the actual resistance projection welding process.
Standards developed for other stud-welding processes should not automatically be treated as governing requirements for top-of-head resistance projection weld studs.
The customer should establish applicable welding procedures, inspection methods and acceptance criteria based on the actual joint design.
Common Weld Stud Problems and Engineering Troubleshooting
Reliable troubleshooting begins with identifying the observed condition rather than immediately changing welding current or replacing the fastener.
| Observed Problem | Possible Causes | Engineering Response |
|---|---|---|
| Weak welded attachment | Insufficient heat, poor contact, material mismatch | Review welding schedule and joint testing |
| Uneven projection collapse | Geometry variation, electrode misalignment | Inspect projections and electrode contact |
| Excessive expulsion | Current, force or surface-condition problems | Review process settings and mechanical follow-up |
| Exterior panel marking | Heat input, electrode contact, thin sheet | Review panel design and electrode arrangement |
| Stud tilt | Uneven collapse, fixture movement | Check positioning and workpiece support |
| Thread damage | Handling, tooling interference, deformation | Inspect threads and tooling |
| Corrosion near weld | Coating damage, unsuitable protection | Review finishing and corrosion requirements |
| Variable production results | Material, coating or equipment variation | Compare lots and process records |
Separate Fastener Problems from Welding Process Problems
A dimensional problem with the fastener should not automatically be treated as a welding-machine problem.
Likewise, a weak weld should not automatically be attributed to the fastener.
A useful root-cause investigation separates the following variables.
Fastener Characteristics
Thread dimensions, head geometry, projection height, projection position, material and surface condition.
Parent-Material Characteristics
Sheet material, thickness, flatness, coating and contamination.
Equipment Characteristics
Electrode alignment, force delivery, current control, mechanical follow-up, fixture rigidity and positioning.
Finished-Joint Characteristics
Mechanical strength, dimensional condition, appearance and any required electrical performance.
This separation helps identify the actual source of variation before corrective action is selected.
Weld Joint Validation and Mechanical Testing
The completed weld must satisfy the requirements of the actual equipment assembly.
Potential evaluation methods include:
Visual examination
Dimensional inspection
Torque-related testing
Axial pull-off testing
Shear testing
Destructive weld examination
Fatigue testing where required
Corrosion testing where required
The test methods, sampling plan and acceptance limits should be defined by the customer or applicable engineering requirements.
Torque Resistance and Axial Strength
Torque resistance and axial tensile capacity are different mechanical characteristics.
Passing one test does not automatically establish acceptable performance under another loading condition.
Testing should reflect the intended application.
Electrical Bonding
Where the stud forms part of an electrical bonding or grounding path, electrical continuity or resistance may require separate testing.
RF Shielding
Where the fastener supports a shielding component, electromagnetic performance must be assessed at the enclosure or equipment level.
Quality Control for Repeat OEM Manufacturing
Consistent production requires control of both supplied fastener characteristics and the welding process.
For the fastener itself, important quality characteristics may include material specification, thread dimensions,
head geometry, projection dimensions, surface condition, dimensional tolerances and lot identification.
Projection Geometry Inspection
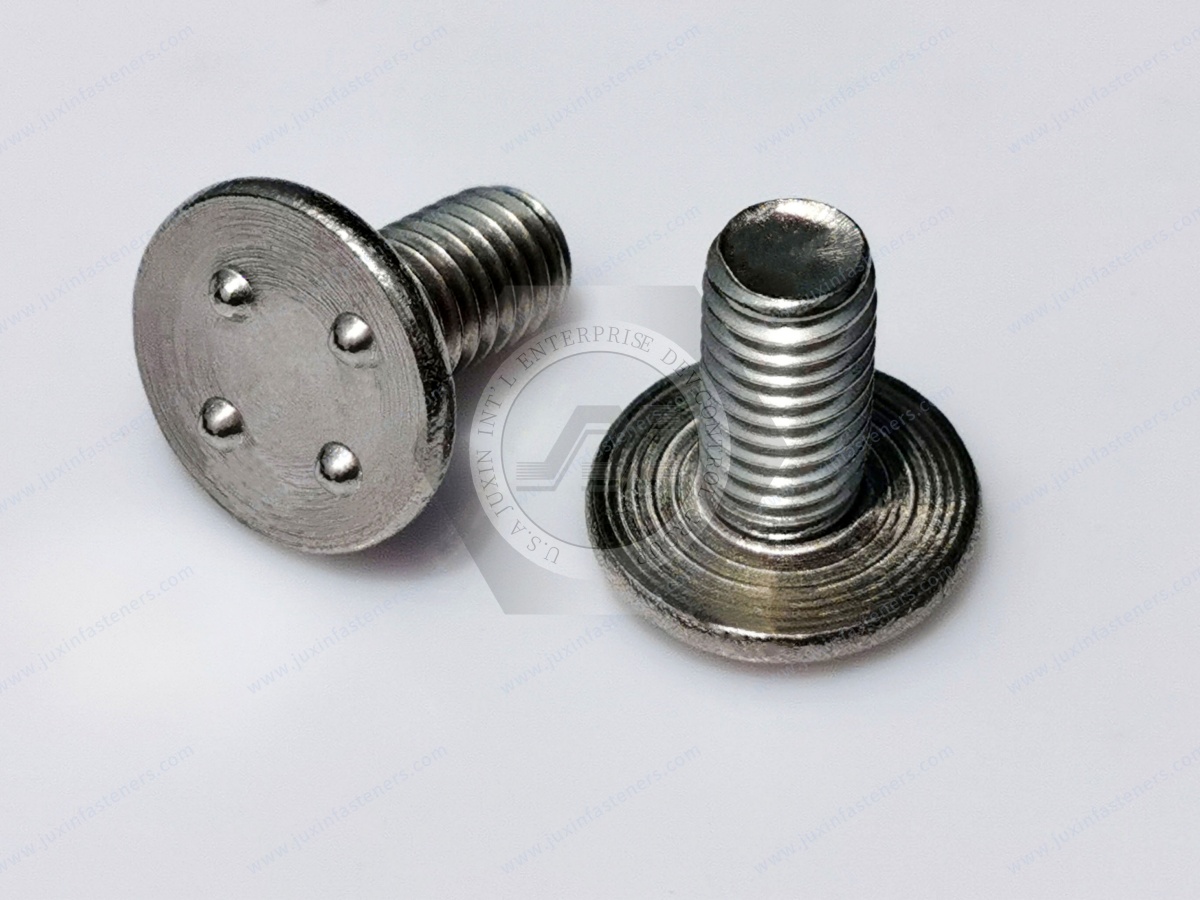
Projection height, shape and position may be critical characteristics.
The appropriate inspection method depends on the geometry and tolerances established by the engineering drawing.
Thread Inspection
Thread dimensions and tolerance classes should conform to the specified requirements.
Appropriate thread gauges or dimensional measurement methods may be used according to the inspection plan.
Material Verification
Material requirements must support the intended mechanical and welding functions.
Material documentation or additional verification should be agreed where required.
Packaging and Handling
Packaging should protect threads, formed projections and critical surfaces from damage.
Different thread sizes, materials and projection configurations should be properly identified to reduce the risk of mixing.
Inspection Scope
Sampling inspection, additional sorting or other inspection arrangements may be appropriate depending on the customer's requirements.
Inspection scope should be agreed rather than assumed.
A statement of 100% inspection does not independently establish zero defects or guarantee weld performance.
Automated Feeding and High-Volume Welding Production
Telecommunications equipment manufacturers may use automated handling, positioning and resistance welding equipment.
For production managers, the objective is not only to achieve an acceptable individual weld but also to maintain consistent manufacturing performance.
Fastener Geometry and Feeding Behavior
Feeding compatibility may be influenced by:
Overall stud length
Head diameter
Head-to-shank geometry
Projection position
Dimensional variation
Surface condition
Part orientation
Packaging and handling condition
A dimensionally acceptable stud is not automatically compatible with a particular feeding system.
Automated Equipment Validation
Vibratory feeders, escapements, transfer devices and robotic handling equipment may have different requirements.
Compatibility should be evaluated using the actual fastener configuration and production equipment.
Welding Process Monitoring
Depending on the welding equipment, production records may include current, welding time, electrode force, equipment identification, timestamps and process alarms.
These records can support process monitoring and troubleshooting.
However, a recorded welding cycle does not automatically prove that the finished joint meets mechanical requirements.
Supplier Traceability and Equipment Traceability
Fastener lot identification and welding equipment records represent different forms of traceability.
Their integration depends on the customer's production and quality systems.
Fastener supply should not be assumed to include MES integration, robotic programming or welding-machine commissioning unless those services are separately agreed.
Choosing Between Projection Weld Studs and Alternative Fasteners
The correct fastening technology depends on the substrate, installation access, mechanical requirements and manufacturing process.
| Fastener Type | Installation Method | Selection Consideration |
|---|---|---|
| Top-of-head projection weld stud | Resistance projection welding | Permanent male thread without a required shank mounting hole |
| Through-hole projection weld stud | Resistance projection welding | Hole-assisted positioning or specified joint configuration |
| CD weld stud | Capacitor discharge stud welding | Compatible CD equipment and weld-end design |
| Self-clinching stud | Mechanical clinching | Sheet hardness, thickness and prepared hole |
| Self-clinching standoff | Mechanical clinching | Defined spacing for PCB or chassis mounting |
| Blind rivet nut | Mechanical deformation | One-sided installation access |
| Projection weld nut | Resistance projection welding | Permanent female-threaded attachment |
When a Projection Weld Stud May Be Preferred
A top-of-head projection weld stud may be suitable when a permanent externally threaded mounting point is required on a weldable metal surface,
welding access is available and a shank mounting hole is undesirable.
When Self-Clinching Hardware May Be Preferred
Self-clinching studs or standoffs may be more appropriate where the sheet material, hardness and thickness permit mechanical installation and welding is undesirable.
When Blind Rivet Nuts May Be Preferred
Blind rivet nuts may be suitable where only one side of the workpiece is accessible or where the parent material is unsuitable for the proposed welding method.
When Weld Nuts May Be Preferred
Projection weld nuts may be appropriate where the assembly requires a permanent internal thread rather than an external stud.
No fastening method is universally superior.
The final selection should follow the engineering requirements and verified manufacturing capability.
Total Installed Cost and Production Efficiency
The fastener purchase price is only one part of the total manufacturing cost.
For telecommunications OEM production, cost evaluation may include:
Fastener unit price
Welding equipment and tooling
Electrode maintenance
Installation cycle time
Inspection requirements
Rework and scrap
Packaging
Production interruptions
Delivery planning
Why the Lowest Unit Price May Not Produce the Lowest Installed Cost
A lower-priced fastener may increase manufacturing cost if it introduces verified feeding problems, welding variation or additional inspection requirements.
Conversely, a higher-priced fastener does not automatically provide superior weld performance.
The correct decision should be supported by actual manufacturing data.
Production Manager Priorities
Production managers may focus on positioning repeatability, welding process stability, inspection requirements,
electrode maintenance, changeover time, scrap exposure and production throughput.
These requirements should be considered during supplier selection rather than after mass production begins.
OEM Supplier Development and Procurement Requirements
For procurement managers, supplier-development engineers and supply chain teams, sourcing a projection weld stud requires more than comparing thread size and price.
A complete purchasing specification helps reduce ambiguity and supports consistent repeat orders.
Important Supplier Evaluation Factors
Engineering drawing and revision
Applicable product standard
Material specification
Thread system and tolerance
Head and projection geometry
Surface finish
Mechanical requirements
Inspection requirements
Packaging
Prototype quantity
Minimum order quantity
Estimated annual demand
Lead time
Engineering change control
Drawing-Based Customization
Some telecommunications equipment designs require nonstandard dimensions or fastening configurations.
Potential customization requirements include stud length, thread diameter, pitch, head dimensions,
projection geometry, material, surface finish, dimensional tolerances and packaging.
Technical feasibility and commercial conditions depend on the actual drawing and project requirements.
Engineering Change Control
Changes to projection geometry, material or surface condition may influence welding behavior even when the nominal thread specification remains unchanged.
For repeat OEM production, changes affecting critical characteristics should be reviewed through the customer's applicable engineering and supplier quality procedures.
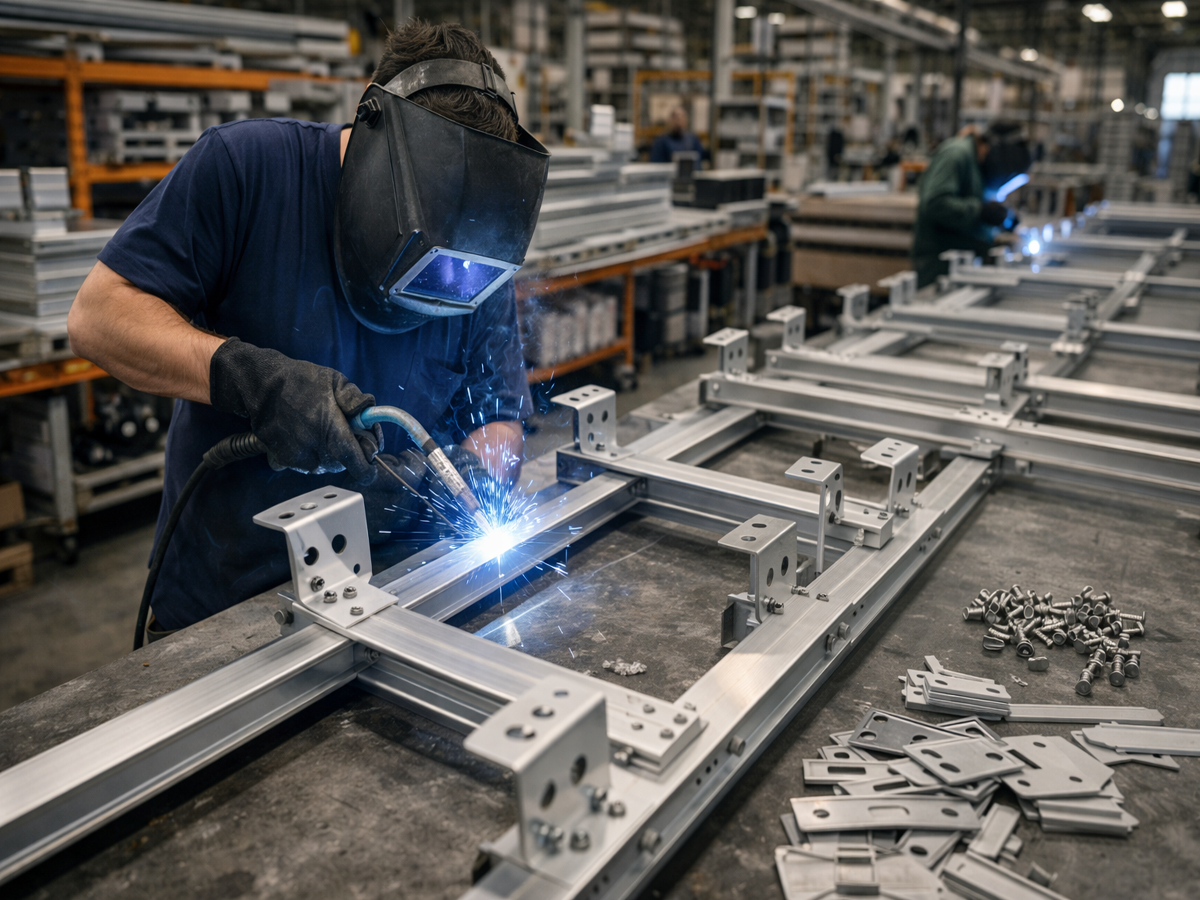
JUXIN FASTENERS — Industrial Weld Studs and OEM Fastening Solutions
JUXIN FASTENERS supplies industrial weld studs and related fastening components for international OEM manufacturing and drawing-based applications.
Relevant product families include:
Three-projection top-of-head weld studs
IFI-148 Type T3-style projection weld studs
Carbon steel projection weld studs
Stainless steel projection weld studs
Other projection weld stud configurations
Weld nuts
Self-clinching studs and standoffs
Blind rivet nuts
Drawing-based custom fastening components
For telecommunications equipment manufacturers, product selection should begin with the engineering drawing and intended installation conditions.
Specific dimensions, materials, surface finishes, inspection arrangements, availability and delivery terms require project-level confirmation.
Related JUXIN FASTENERS Products and Engineering Resources
Projection Weld Stud with 3 Formed Projections
Fastener Automated Feeding and Robotics: OEM Automation Integration Guide
Weld Fasteners Manufacturer — Industrial Weld Studs and Weld Nuts
Frequently Asked Questions
What is a three-projection top-of-head weld stud?
It is an externally threaded fastener with three formed welding projections on the top face of its head,
intended for resistance projection welding to a suitable metallic workpiece.
Does a top-of-head projection weld stud require a mounting hole?
The configuration does not inherently require a clearance hole for the threaded shank in the parent sheet.
Can these studs be used in telecommunications cabinets?
They may be suitable for selected metallic cabinets, brackets and equipment housings when the substrate, welding process and mechanical requirements are compatible.
Are three-projection weld studs suitable for thin sheet metal?
Suitability depends on sheet material, thickness, stud geometry, electrode arrangement and required joint performance.
There is no universal minimum thickness based only on thread diameter.
Can carbon steel projection weld studs be welded directly to aluminum enclosures?
A conventional carbon steel projection weld stud should not be assumed suitable for direct welding to aluminum.
The joining method requires specific engineering evaluation.
Are projection weld studs suitable for PCB mounting?
They may be used on suitable metallic chassis or support brackets.
Dedicated standoffs or self-clinching hardware may be more appropriate where a defined PCB spacing function is required.
Does a welded stud guarantee electrical grounding?
No. Electrical bonding and continuity requirements must be specified and validated separately.
Can projection weld studs improve EMI shielding?
They may provide mechanical attachment points for shielding components, but shielding effectiveness depends on the complete enclosure design.
Can welding current be calculated from stud diameter alone?
No. Welding parameters depend on the complete fastener, substrate, electrode and equipment combination.
Is IFI-148 Type T3 applicable to all three-projection weld studs?
No. The Type T3 designation should be used only when the product satisfies the applicable specification and drawing requirements.
Are metric and UNC threads interchangeable?
No. Metric, UNC and UNF threads are distinct systems and should not be interchanged based on nominal diameter similarity.
Can three-projection weld studs be automatically fed?
Potentially, but compatibility depends on fastener geometry and the actual feeding and positioning equipment.
Does passing a torque test prove adequate weld strength?
Not necessarily. Torque resistance, axial strength and shear performance are different characteristics and may require separate evaluation.
Can JUXIN FASTENERS review custom OEM drawings?
Drawing-based requirements may be submitted for technical and commercial review, including dimensions, material,
thread specification, projection geometry, inspection requirements and purchasing volume.
OEM RFQ — Three-Projection Weld Studs for Telecommunications Equipment
JUXIN FASTENERS welcomes inquiries from telecommunications equipment manufacturers, RF equipment OEMs,
antenna equipment manufacturers, electrical enclosure producers, design engineers, manufacturing engineers,
production managers and international procurement teams.
For technical evaluation and quotation, please provide the following information where applicable.
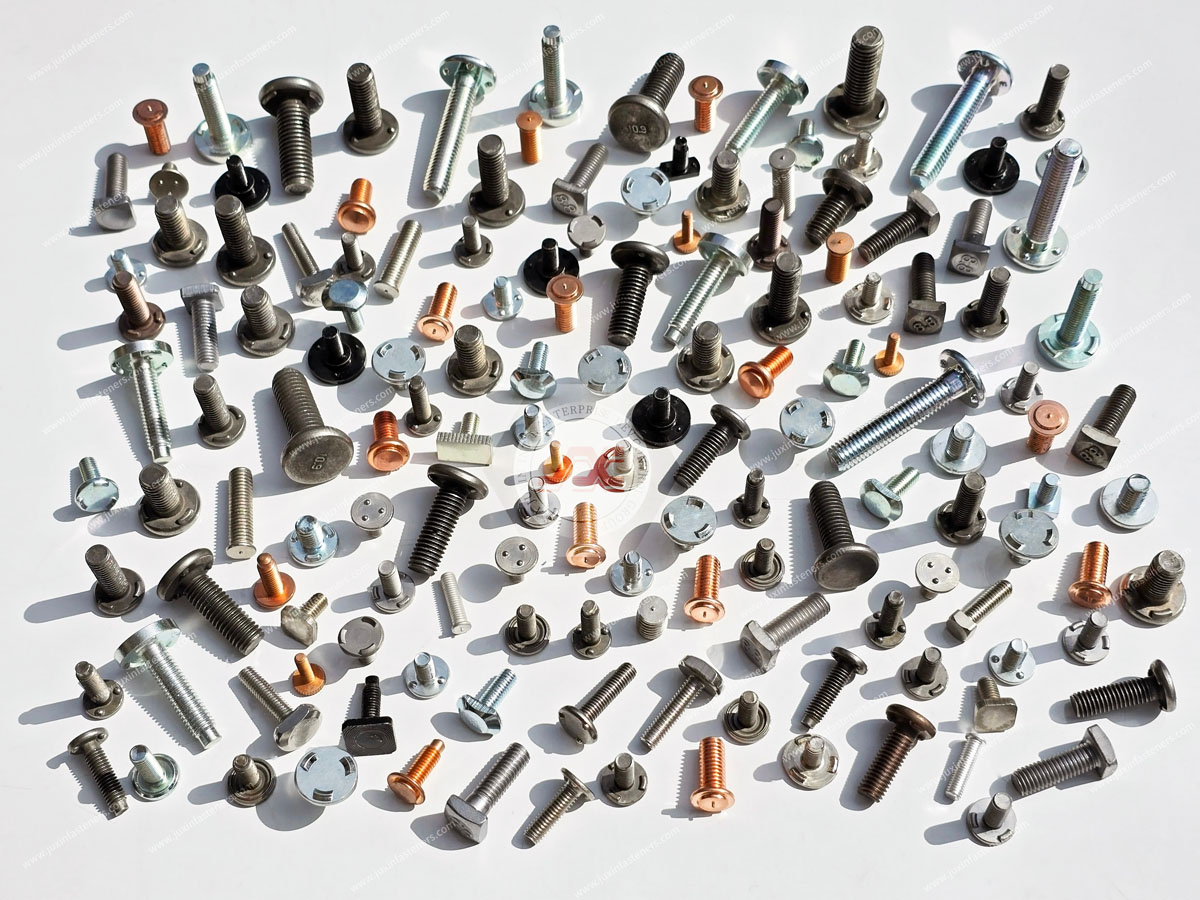
Engineering Drawings and Product Specifications
2D engineering drawing with revision
3D CAD model where available
Applicable IFI-148 type designation
Thread diameter, pitch and tolerance class
Stud length
Head dimensions
Three-projection geometry
Material specification
Mechanical property requirements
Surface finish
Application and Welding Requirements
Parent-sheet material and thickness
Intended resistance welding equipment
Electrode and fixture constraints
Mechanical loading requirements
Assembly torque requirements
Cosmetic surface requirements
Electrical bonding requirements, if applicable
EMI/RFI requirements, if applicable
Environmental and corrosion requirements
Quality and Commercial Requirements
Inspection and testing requirements
Acceptance criteria
Packaging specification
Lot identification requirements
Prototype or sample quantity
Estimated annual purchasing volume
Required delivery schedule
Applicable supplier documentation requirements
Complete technical information helps reduce clarification cycles and supports more accurate product evaluation and quotation.
Company: JUXIN FASTENERS
Website: https://www.juxinfasteners.com/
Email: info@juxinfasteners.com
For three-projection top-of-head weld studs, applicable IFI-148 Type T3 configurations and drawing-based threaded fastening solutions for telecommunications equipment,
contact JUXIN FASTENERS with your engineering drawings and project requirements.
Our team can review the supplied specifications and discuss suitable product options, technical feasibility and commercial requirements for your OEM project.
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY



