Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

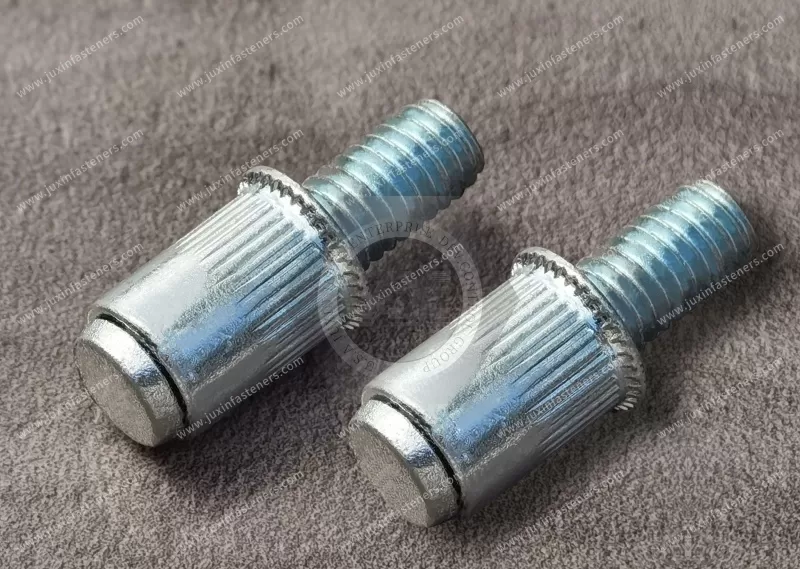
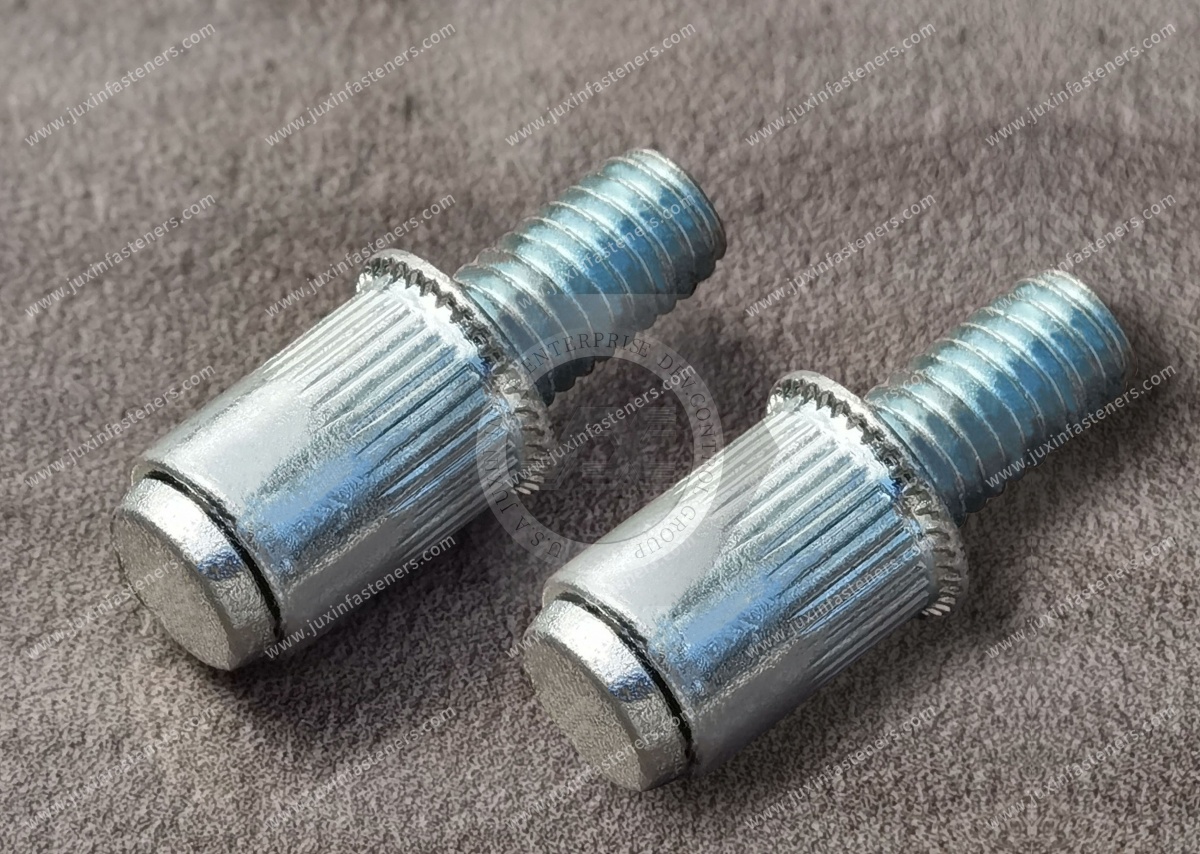
JUXIN FASTENERS supplies steel thin head open-end knurled blind rivet studs for creating external threaded mounting points in thin sheet-metal assemblies with access from one side. The thin head design helps minimize head protrusion compared with thicker-head configurations, subject to drawing dimensions. The knurled body supports rotational resistance after mechanical riveting. Available in M4, M5, M6 and M8, these studs can be evaluated for industrial enclosures, fabricated brackets, equipment housings and OEM sheet-metal components.
Thread Sizes: M4, M5, M6, M8
Material: Steel (grade subject to confirmation)
Surface Finish: Color Zinc or RoHS-Related Blue Zinc Finish (compliance subject to verification)
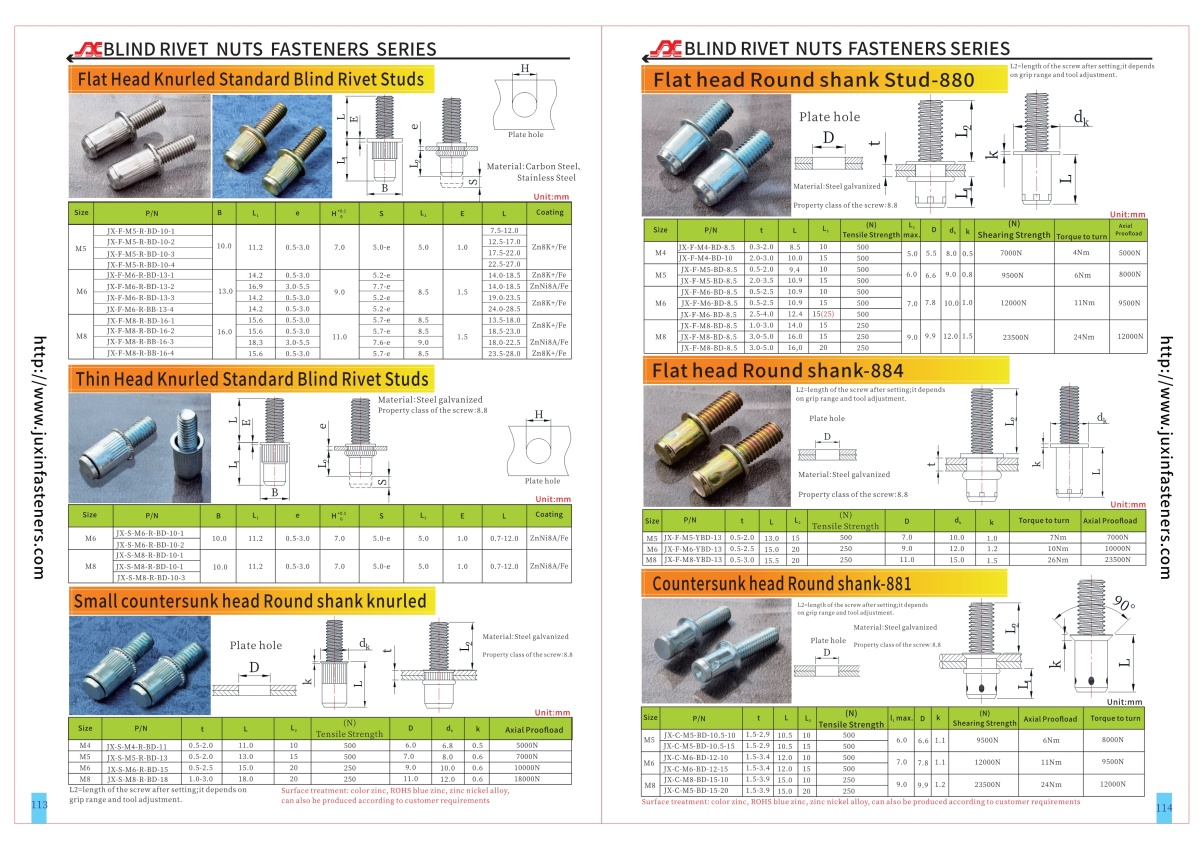
Grip Range: 0.5–3.0 mm (product family; verify by part number)
Head Type: Thin Head / Low-Profile Head
Body Type: Open-End, Knurled
Thread Type: External Male Metric Thread
Installation: One-Sided Mechanical Blind Riveting
Product Specification
Product Specifications — Steel Thin Head Open-End Knurled Blind Rivet Studs
JUXIN FASTENERS supplies steel thin head open-end knurled blind rivet studs for industrial sheet-metal assemblies requiring an externally threaded mounting point, one-sided installation and reduced head protrusion.
These mechanically installed rivet-type studs feature a thin head, open-end rivet body and knurled exterior. During installation, the deformable body section is upset behind the parent material, securing the stud while leaving the external male thread available for attaching components with compatible nuts.
The thin head configuration is particularly relevant to engineering designs where the available mounting height is limited or a conventional thicker-head fastener would interfere with adjacent components.
Technical Specifications
Product Type: Thin Head Open-End Knurled Blind Rivet Stud
Material: Steel
Material Grade: According to the approved specification
Thread Sizes: M4, M5, M6, M8
Thread Configuration: External Male Metric Thread
Head Configuration: Thin Head / Low-Profile Head
Body Configuration: Open-End, Knurled
Surface Finish Options: Color Zinc or Blue Zinc Finish
Grip Range: 0.5–3.0 mm (product-family information)
Installation: One-Sided Mechanical Blind Riveting
Thread Pitch and Tolerance: According to the approved drawing
Mounting-Hole Dimensions: According to the selected part drawing
Stud Projection: According to the selected part drawing
Custom Dimensions: Subject to drawing review and feasibility confirmation
The supplied 0.5–3.0 mm grip range describes the product family. The approved grip range for each individual M4, M5, M6 or M8 variant must be confirmed before selection.
1. Product Overview — Low-Profile External Threaded Mounting for Thin Sheet Metal
Thin head blind rivet studs are designed to provide fixed external male-thread mounting points in sheet-metal assemblies where access is available from one side.
The product combines two separate functions:
Mechanical retention of the rivet body in the parent material
External threaded attachment of the mating component
This distinction is important because the installed rivet connection and the subsequent nut-to-stud connection have different mechanical requirements.
The thin head design provides an additional geometric consideration compared with conventional flat head blind rivet studs.
Where an assembly includes closely fitted brackets, covers or mounting components, the head thickness may affect the available clearance and final component position.
A low-profile head may help reduce this interference, provided that the actual head dimensions meet the assembly requirements.
These products may be considered for industrial equipment, fabricated sheet-metal housings, electrical cabinets, HVAC components and selected automotive equipment assemblies.
2. Thin Head vs. Standard Flat Head Blind Rivet Studs
The primary engineering distinction of this product is its thin head configuration.
A conventional flat head rivet stud may create an installed head projection that must be accommodated by the mating component.
A thin head design is intended to reduce this projection.
However, the exact reduction depends on the dimensional comparison between the two specific products.
| Design Factor | Thin Head Design | Conventional Flat Head Design |
|---|---|---|
| Head Profile | Reduced-profile configuration | Standard head configuration |
| External Thread | Male thread | Male thread |
| One-Sided Installation | Available | Available |
| Panel Seating | Drawing-dependent | Drawing-dependent |
| Mating Component Clearance | May benefit from reduced projection | Must accommodate specified head height |
| Mechanical Retention | Requires validation | Requires validation |
| Interchangeability | Not automatic | Not automatic |
A Thin Head Is Not Necessarily a Flush Head
The terms thin head, low-profile head, reduced head and flush head should not be used interchangeably without dimensional confirmation.
A thin head generally describes a reduced head thickness relative to a thicker design.
A flush installation means the installed fastener does not protrude above the intended reference surface, within the applicable tolerance.
The supplied product information confirms a thin head configuration but does not establish a flush installation.
For applications requiring a truly flush mounting surface, the engineer should review the actual head thickness, mounting geometry and mating component clearance.
3. Engineering Information Gain — Why Head Height Matters Beyond Appearance
The head height of a blind rivet stud can influence more than the visual profile of the installed component.
Consider a thin sheet-metal panel supporting a removable equipment bracket.
If the bracket rests on the protruding head rather than the intended panel surface, the resulting assembly may experience:
Localized contact around the fastener head
Reduced contact between the bracket and panel
Changes in the intended clamping arrangement
Unintended component spacing
Possible bending of thin mating components
Difficulty maintaining consistent assembly geometry
A thinner head may reduce these issues when properly integrated into the joint design.
However, reducing head thickness may also change the bearing geometry and local installation behavior.
The head must still provide the required seating and retention characteristics.
Therefore, a thinner head should not automatically be interpreted as an improvement in mechanical strength.
4. One-Sided Mechanical Installation
Thin head blind rivet studs are installed using a compatible mechanical blind riveting process.
A typical installation procedure includes:
Prepare the mounting hole according to the approved drawing.
Confirm that the parent material thickness is within the selected stud's specified grip range.
Check the mounting-hole condition, including burrs and local flatness.
Engage the stud with the appropriate installation tool.
Insert the rivet body through the mounting hole from the accessible side.
Apply the specified setting action to deform the rivet body behind the panel.
Release the installation equipment.
Inspect head seating, stud alignment and installed body deformation.
Assemble the mating component using the specified nut and tightening procedure.
The required setting force, stroke, mandrel engagement and acceptance criteria depend on the actual product geometry and installation equipment.
They must not be inferred from the nominal thread size alone.
Installation Tool Compatibility
Certain threaded-mandrel blind fastening tools may support rivet-type studs.
However, equipment designed for blind rivet nuts is not automatically compatible with every externally threaded blind rivet stud.
The installation mandrel, engagement method, tool stroke and fastener geometry must be verified before production use.
5. Open-End Knurled Body Construction
The product incorporates an open-end rivet-body configuration and a knurled exterior.
The open-end designation describes the body construction.
It does not mean that the product provides an internal female thread.
The functional threaded interface remains the external male stud.
During installation, the rivet body deforms to establish mechanical retention behind the parent panel.
The knurled surface contributes to rotational resistance through engagement with the surrounding mounting-hole material.
The effectiveness of this engagement depends on the knurl geometry, mounting-hole dimensions, panel material and setting conditions.
6. Knurled Anti-Rotation vs. Nut Locking
Knurled blind rivet studs are sometimes described as vibration-resistant fasteners.
This description requires careful interpretation.
The knurled body helps resist rotation of the stud within the parent panel.
It does not independently prevent the mating nut from loosening under vibration.
These are different engineering functions.
Stud-to-Panel Interface
The knurled body and deformed rivet section help retain the fastener in the mounting panel.
Nut-to-Stud Interface
The mating nut, thread engagement, tightening conditions and any specified locking feature determine the behavior of the threaded connection.
For vibration-sensitive assemblies, both interfaces must be evaluated.
Where necessary, engineers should consider an appropriate locking nut or other approved joint-retention strategy.
No universal spin-out torque or vibration-resistance rating is claimed for this product.
7. Grip Range — Thin Sheet-Metal Installation from 0.5 to 3.0 mm
The supplied product-family grip range is 0.5–3.0 mm, approximately 0.020–0.118 in.
This range is especially relevant to applications involving thin fabricated panels.
However, the actual permitted grip thickness must be confirmed for each specific part number.
Grip range describes the material thickness captured by the installed rivet body.
It does not describe the external stud length.
Why Thin Panels Require Careful Installation Validation
Thin sheet-metal materials may be susceptible to local deformation during the riveting process.
Potential concerns include:
Enlargement of the mounting hole
Local panel distortion
Inconsistent head seating
Reduced knurl engagement
Uneven rivet-body deformation
Insufficient installed retention
Changes in stud perpendicularity
These effects depend on the actual panel material, thickness, hole geometry and installation conditions.
For thin panels, selecting the correct grip range is particularly important.
Example: Selecting a Blind Rivet Stud for a 1.0 mm Panel
Consider a fabricated metal enclosure using a nominal 1.0 mm sheet.
Before selecting an M5 thin head blind rivet stud, the engineer should verify:
The selected M5 variant is approved for the actual panel thickness.
The mounting-hole diameter is compatible with the stud body.
The panel material can support the required installation deformation.
The head thickness is acceptable for the mating component.
The external stud projection provides sufficient nut engagement.
The blind-side retaining feature has adequate clearance.
The installed stud meets the required axial and rotational performance.
The fact that 1.0 mm falls within the stated product-family range does not prove that every M5 variant is suitable.
8. Metric Thread Sizes and Inch Reference Dimensions
The confirmed metric thread sizes are M4, M5, M6 and M8.
| Metric Thread | Approximate Nominal Diameter |
|---|---|
| M4 | 0.157 in |
| M5 | 0.197 in |
| M6 | 0.236 in |
| M8 | 0.315 in |
These inch values are approximate diameter conversions for engineering reference.
They do not represent interchangeable Unified inch-thread sizes.
Metric threads are not directly interchangeable with UNC, UNF or BSW threads.
ISO 261 and ISO 965 may be used as applicable references for ISO metric thread combinations and tolerances.
The actual thread pitch and tolerance must be confirmed from the approved product drawing.
9. Steel Material Selection and Installation Formability
The confirmed base material is steel.
The specific steel grade, hardness and mechanical condition have not been supplied.
For mechanically installed blind rivet studs, material selection must account for both service requirements and the deformation needed during installation.
Important considerations include:
Steel grade
Material condition
Formability
Required thread properties
Rivet-body deformation characteristics
Parent-material compatibility
Corrosion protection
Operating temperature
Customer-specific material restrictions
A change in steel grade or hardness may affect the setting process even when the nominal dimensions remain unchanged.
For drawing-based OEM sourcing, material substitution should therefore be reviewed before approval.
10. Zinc Surface Finishes — Color Zinc and Blue Zinc
The specified finish options are color zinc and blue zinc.
These are commercial finish descriptions and should be translated into a complete coating specification before production qualification.
Depending on the agreed process, the final coating system may include a zinc deposit, conversion coating and other specified supplemental treatments.
The appearance alone does not establish coating thickness, corrosion resistance or regulatory compliance.
Color Zinc Finish
Color zinc is commonly used as a commercial description for a zinc-plated finish with a colored conversion coating.
The exact coating construction and appearance requirements should be confirmed against the approved purchasing specification.
Blue Zinc Finish
Blue zinc is commonly used to describe a zinc-plated finish with a blue or clear-blue appearance.
The final appearance and coating system must be established by the approved specification.
RoHS-Related Blue Zinc Requirements
The term RoHS blue zinc should not be treated as independent evidence of regulatory compliance.
Where RoHS compliance is required, the purchaser should request the applicable declaration or supporting documentation for the supplied coating system.
A blue appearance does not by itself establish whether the coating is free of restricted substances.
11. ISO 4042 and Electroplated Fastener Requirements
ISO 4042 provides a relevant international reference for electroplated coating systems on steel fasteners.
Where specified by the customer, the coating requirements may address:
Coating system designation
Coating thickness
Conversion coating
Supplemental sealers or topcoats
Thread dimensional compatibility
Corrosion testing requirements
Process control
Hydrogen embrittlement risk management
The applicable coating system must be agreed upon before manufacturing and qualification.
The use of ISO 4042 as a technical reference does not establish that this particular product has been certified or tested to the standard.
12. Hydrogen Embrittlement — A Material and Coating Qualification Consideration
Electroplating processes can introduce hydrogen into steel components.
For susceptible steel materials, hydrogen may contribute to delayed cracking under certain conditions.
The relevance of hydrogen embrittlement depends on factors such as:
Steel hardness and strength
Material condition
Manufacturing processes
Electroplating process
Residual or applied tensile stress
Applicable process controls
Because the steel grade and hardness have not been confirmed, no product-specific hydrogen embrittlement risk classification is claimed.
For applications where the material condition creates a relevant risk, engineering and supplier quality teams should review the coating process and applicable mitigation requirements.
13. Why Zinc Coating Changes Can Affect Rivet Stud Qualification
A coating change is not always a purely cosmetic modification.
For a knurled blind rivet stud, the coating system may influence:
External thread dimensions
Surface condition of the knurled body
Contact behavior in the mounting hole
Installation-tool engagement
Surface friction
Corrosion performance
Appearance and customer acceptance
For example, replacing one zinc coating system with another may change the final surface condition even when the underlying steel part remains dimensionally unchanged.
If the stud has already been qualified for an OEM assembly, the coating change should be reviewed against the approved drawing and validation requirements.
This is particularly important when the assembly depends on controlled knurl engagement or specified thread tolerances.
14. Mechanical Performance and Joint Reliability
The mechanical performance of an installed thin head blind rivet stud depends on the fastener, parent panel, installation process and mating threaded connection.
Axial Retention
The deformed rivet body must resist the required axial loading without pulling out of the parent material.
Rotational Resistance
The knurled body must provide sufficient resistance against rotation for the intended assembly process.
Head Seating
The thin head should seat consistently against the accessible panel surface.
Thread Integrity
The external thread must remain suitable for the specified mating nut after installation.
Panel Stability
The parent material must withstand the installation process without unacceptable deformation.
Repeated Assembly
Where maintenance requires repeated removal of the mating nut, the installed stud should remain suitable for the intended service procedure.
Vibration and Cyclic Loading
Applications involving repeated dynamic loading require assessment of the complete joint.
No specific pull-out force, spin-out torque, installation force, tightening torque or fatigue performance is claimed without product-specific test data.
15. Industrial Applications — Thin Head Blind Rivet Studs
Automotive Sheet-Metal Components
Potential applications include selected non-safety-critical brackets, fabricated mounting panels, accessory housings and equipment supports.
The thin head configuration may be useful where adjacent component clearance is limited.
Automotive applications require project-specific engineering and quality approval.
Electric Vehicle Equipment
Possible applications include fabricated equipment housings, removable mounting brackets and selected enclosure components.
Electrical insulation, grounding, environmental sealing and structural requirements must be evaluated separately.
Electrical Enclosures and Control Cabinets
Thin head blind rivet studs may be considered for mounting brackets, accessory supports and sheet-metal components where rear-side access is restricted.
The low-profile configuration can be relevant when mating components are positioned close to the mounting panel.
Industrial Machinery
Applications may include fabricated equipment covers, sheet-metal guards, mounting brackets and accessory attachment points.
Mechanical loading and maintenance requirements must be evaluated.
HVAC and Ventilation Equipment
Potential uses include thin sheet-metal housings, mounting brackets and selected removable equipment components.
Vibration, corrosion exposure and local panel deformation should be considered.
Commercial Vehicle Equipment
Thin head rivet studs may be evaluated for selected non-critical mounting points and fabricated metal components where assembly access is limited.
Dynamic loading and environmental conditions require application-specific validation.
Metal Furniture and Industrial Cabinets
Potential applications include fabricated metal panels, support brackets and serviceable mounting components.
The installed head projection and appearance may be relevant to product design.
16. Engineering Information Gain — Five Common Selection Mistakes
Mistake 1: Assuming Thin Head Means Flush Mounting
A reduced head thickness does not automatically create a flush surface.
The actual installed projection must be checked.
Mistake 2: Selecting Only by Thread Size
An M6 stud may have the correct external thread but an unsuitable grip range, head dimension or body diameter.
Mistake 3: Ignoring Parent-Panel Strength
A stud qualified in steel sheet may not provide equivalent installed performance in aluminum sheet of the same thickness.
Mistake 4: Treating Blue Zinc as a Complete Coating Specification
A color description does not define coating thickness, conversion treatment, corrosion requirements or RoHS compliance.
Mistake 5: Assuming Knurling Prevents Nut Loosening
Knurling helps resist rotation of the installed stud, while nut locking must be addressed separately.
Avoiding these mistakes can reduce incorrect fastener selection, installation problems and supplier substitution risks.
17. OEM and Tier 1 Engineering Qualification
For OEM production, qualification should consider the installed fastener rather than the loose component alone.
Depending on project requirements, the validation process may include:
Approved engineering drawing
Steel material identification
Dimensional inspection
Thread inspection
Coating specification verification
Surface appearance requirements
Installation-hole compatibility
Grip-range verification
Installation process validation
Installed axial retention
Installed rotational resistance
Head seating and alignment
Corrosion testing where specified
Packaging and identification requirements
Drawing revision control
Lot traceability
Automotive projects may require additional customer-specific documentation, inspection plans or production approval activities.
Such requirements must be agreed upon for the individual project.
No automotive approval, PPAP status or certified mechanical performance is implied by this product description.
18. Procurement and Supplier Development — Evaluating Alternative Sources
Purchasing engineers and strategic sourcing teams should evaluate thin head blind rivet stud suppliers using more than price and nominal thread size.
A practical supplier comparison should include:
Product Geometry
Confirm head thickness, head diameter, rivet-body diameter, knurl profile and external stud projection.
Material
Confirm the specified steel grade and relevant material condition.
Surface Finish
Define the exact zinc coating system rather than relying only on a color description.
Installation Compatibility
Verify the selected product against the intended panel material, thickness and installation equipment.
Installed Performance
Determine whether axial retention, rotational resistance or additional testing is required.
Quality Requirements
Review dimensional inspection, material documentation, coating requirements and traceability.
Commercial Requirements
Confirm quotation quantity, estimated annual demand, delivery expectations and packaging instructions.
Change Management
Define how changes in geometry, material or coating will be reviewed before implementation.
A lower purchase price does not necessarily represent a lower total assembly cost if the alternative fastener requires different tooling, additional inspection or redesign of the mounting interface.
19. Custom Thin Head Blind Rivet Stud Requirements
OEM projects may require specific dimensions or material and coating conditions.
Potential drawing-based requirements include:
Specified thin head dimensions
Customer-defined external stud projection
Particular body geometry
Specified knurl dimensions
Application-specific grip requirements
Defined steel material grade
Controlled dimensional tolerances
Customer-specified zinc coating system
Packaging and identification requirements
All custom configurations are subject to engineering review and manufacturing feasibility confirmation.
Providing a complete drawing and installation requirements helps determine whether a standard part or a custom design is appropriate.
20. Frequently Asked Questions
What is a thin head blind rivet stud?
It is a mechanically installed fastener that provides an external male thread in a parent panel accessible from one side. Its thin head configuration is intended to reduce head protrusion compared with a thicker-head design.
Is a thin head blind rivet stud flush mounted?
Not necessarily. Flush mounting depends on the actual head thickness and panel geometry.
What thread sizes are available?
The confirmed sizes are M4, M5, M6 and M8.
What is the grip range?
The supplied product-family range is 0.5–3.0 mm. Individual part-number grip ranges require confirmation.
What materials are available for this product?
The confirmed material is steel. The exact grade must be established from the approved specification.
What surface finishes are specified?
The supplied options are color zinc and blue zinc. Detailed coating requirements must be confirmed before qualification.
Does blue zinc mean RoHS compliant?
No. RoHS compliance requires appropriate verification and supporting documentation.
Can the stud be installed in aluminum sheet?
It may be considered where the panel material, hole geometry and installed performance are compatible. Application-specific validation is required.
Can a thin head stud replace a standard flat head stud?
Not automatically. Head geometry, body dimensions, grip range, installation tooling and installed performance must be compared.
Does the knurled body prevent the nut from loosening?
No. The knurled body contributes to stud rotational resistance in the panel. Nut locking is a separate joint-design consideration.
21. Related Industrial Fastening Solutions
Engineers evaluating thin head blind rivet studs may also compare other fastening technologies within the JUXIN FASTENERS product range.
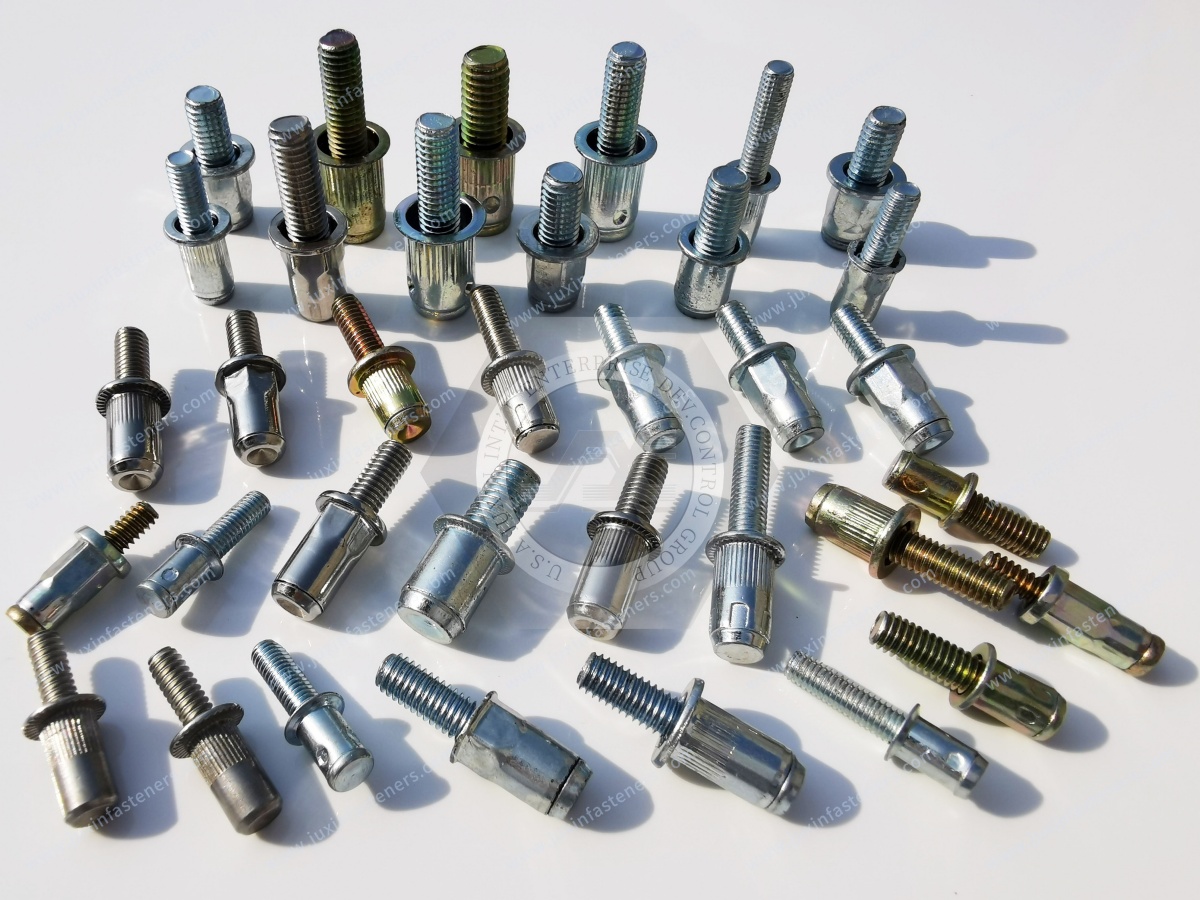
Relevant product categories include:
Flat Head Blind Rivet Studs — for comparison with conventional head configurations
Closed-End Blind Rivet Studs — for alternative rivet-body geometry
Blind Rivet Nuts — for one-sided installation requiring internal female threads
Self-Clinching Studs — for suitable press-installed sheet-metal applications
Weld Studs — for designs using an approved welding process
Steel Nuts and Locking Nuts — for compatible mating threaded connections
Custom Industrial Fasteners — for drawing-based fastening requirements
Selection should be based on the intended assembly geometry, installation access, parent material and required mechanical performance.
22. OEM RFQ Requirements
For accurate technical evaluation and quotation, please provide the following information where available:
Required thread size: M4, M5, M6 or M8
Product drawing or CAD file
External thread pitch and tolerance
Required steel grade
Head diameter and thickness
Stud projection and overall dimensions
Rivet-body and knurl dimensions
Parent-panel material
Panel thickness and required grip range
Mounting-hole diameter and tolerance
Installation equipment and setting requirements
Required zinc coating system
Corrosion or regulatory documentation requirements
Installed mechanical performance requirements
Inspection and quality documentation
Product labeling and packaging requirements
Initial order quantity
Estimated annual demand
Project schedule and delivery destination
A complete drawing and application description will help establish dimensional compatibility and quotation requirements.
23. JUXIN FASTENERS — OEM Thin Head Blind Rivet Stud Supply
JUXIN FASTENERS supplies industrial fastening products for international OEM engineering, purchasing and supplier development requirements.
Our steel thin head open-end knurled blind rivet studs are intended for applications where externally threaded mounting points, limited installation access and reduced head projection must be considered together.
For M4, M5, M6 and M8 requirements, customers are invited to submit drawings, material specifications, coating requirements and purchasing quantities for technical review.
Request a Technical Quotation
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Please include your engineering drawing, required quantity, panel thickness, material specification and installation requirements.
JUXIN FASTENERS — Industrial Fastening Solutions for OEM Engineering and Global Procurement.
Product Packaging
Product Packaging — Steel Thin Head Blind Rivet Studs
Packaging for M4, M5, M6 and M8 steel thin head open-end knurled blind rivet studs can be reviewed according to confirmed order specifications and OEM supply-chain requirements.
Inner Packaging: Protective inner packaging may be specified to help minimize thread damage, surface contact and contamination during handling.
Outer Cartons: Suitable export cartons may be arranged according to product quantity, shipment weight and agreed packaging requirements.
Pallet Packaging: Palletized arrangements may be considered for bulk industrial orders, subject to confirmed shipment specifications.
Thread and Coating Protection: Packaging should consider protection of external threads, thin head seating surfaces and zinc-plated finishes during transportation and storage.
Product Identification: Labels may include product description, thread size, material, finish, part number, quantity and drawing revision as agreed.
Lot Traceability: Batch identification and traceability requirements should be established in the approved quality and purchasing documentation.
OEM Custom Packaging: Customer-specific packaging quantities, labeling, component segregation and automotive supply-chain instructions are subject to review and confirmation.
Final packaging quantities, carton arrangements and shipping details will be confirmed against the approved order.
For OEM packaging specifications and quotation inquiries:
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Product Pictures
Tags
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY