Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

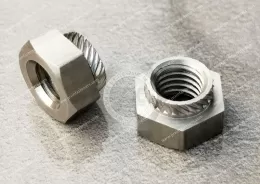
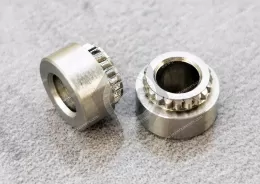
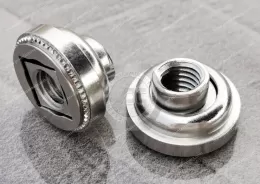
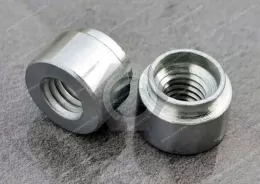
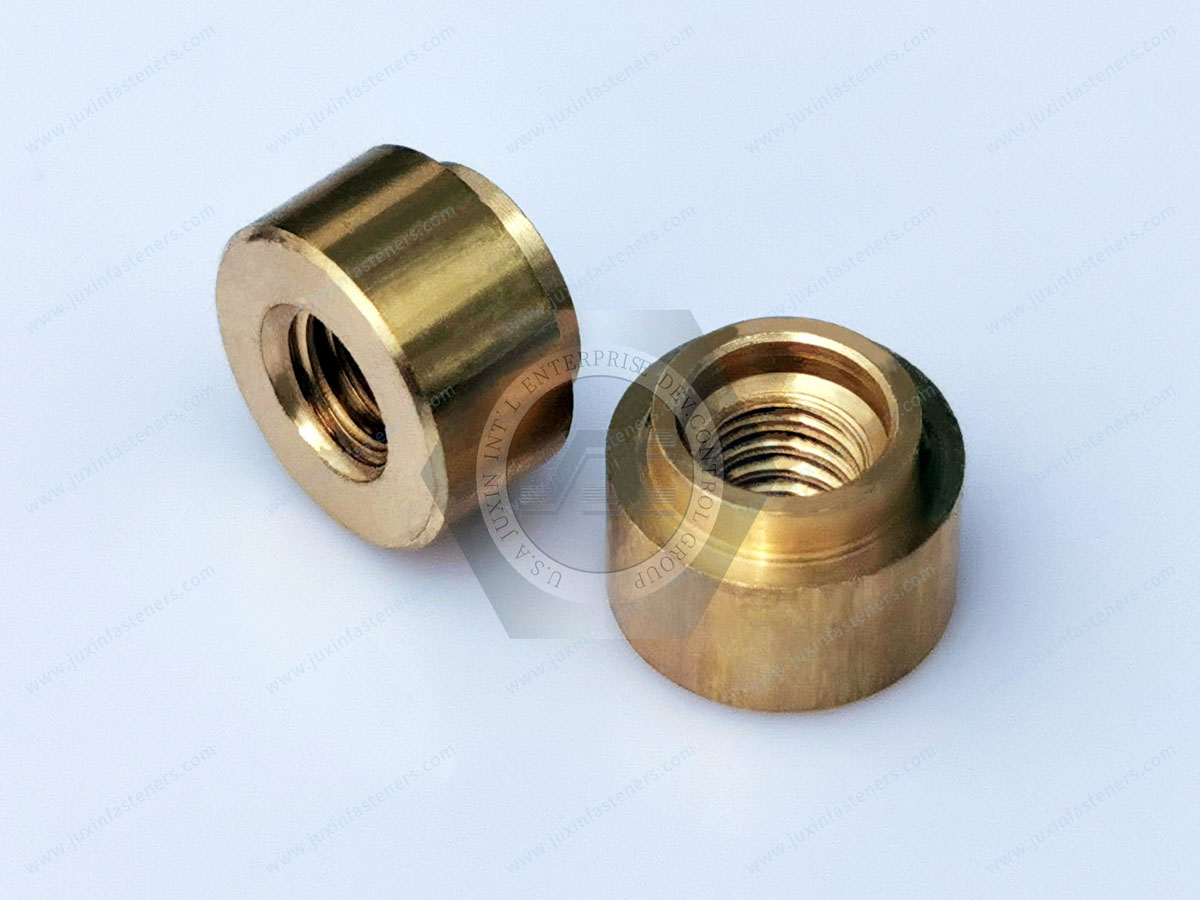
JUXIN FASTENERS supplies brass round flare-in nuts for sheet-metal panels, electrical enclosures, industrial control cabinets and precision equipment housings. These cylindrical threaded inserts are installed in prepared panel holes and mechanically secured by flaring a designated portion of the nut.
Brass offers a material alternative to steel for applications where machinability, corrosion behavior or electrical characteristics influence fastener selection. Actual performance depends on the selected alloy, panel material and installation design.
Product Type: Round Flare-In Nut
Material: Brass or Brass Alloy
Alloy Selection: According to Approved Drawing
Body Geometry: Cylindrical
Installation: Mechanical Flaring or Swaging
Thread Sizes: According to Confirmed Product Specifications
Surface Finish: As Specified for the Application
Custom dimensions and OEM configurations are subject to technical review.
Product Specification
Brass Round Flare-In Nuts – Engineering Selection and OEM Sheet-Metal Fastening Solutions
Brass round flare-in nuts are mechanically installed threaded inserts designed to provide retained internal threads in suitable metal panels.
They are used where a manufacturer needs a threaded attachment point without welding or relying solely on threads cut directly into the parent sheet.
The cylindrical insert is positioned in a prepared mounting hole. A designated section is then mechanically expanded or flared using suitable tooling, creating a retained connection with the panel.
For OEM engineers, selecting a brass flare-in nut involves more than choosing a nominal thread size. The brass alloy, mounting-hole dimensions, panel thickness, forming method, corrosion environment and required mechanical retention must all be considered.
JUXIN FASTENERS supplies brass round flare-in nuts for industrial sheet-metal fastening applications and reviews customer-specific configurations against approved engineering drawings.
Product Configuration
Product name: Brass Round Flare-In Nut
Alternative terminology: Brass Flare-In Threaded Insert, Round Brass Swage Nut, Brass Sheet-Metal Flare-In Nut
Body shape: Round or cylindrical
Thread configuration: Internal thread
Material family: Brass and brass alloys
Installation principle: Mechanical flaring or swaging
Panel compatibility: According to approved drawing and installation validation
Available dimensions: According to confirmed product specifications
Surface condition: According to the specified brass alloy and finishing requirements
The supplied material information references several brass alloy designations. The final alloy and its applicable international material designation must be confirmed for the specific product.
How Brass Round Flare-In Nuts Work
A prepared hole is produced in the sheet-metal component.
The brass insert is positioned in the mounting hole.
An appropriate installation tool supports the fastener and forms the designated deformable section.
The resulting flare creates mechanical retention between the nut and the panel.
Once correctly installed, the insert provides an internal thread for the mating screw.
The exact forming direction, tool arrangement and final retaining geometry depend on the selected fastener design.
A round flare-in nut should not be assumed to use the same installation tooling as a conventional self-clinching nut or blind rivet nut.
Brass Material Selection
Brass is a copper-based alloy family, typically containing zinc and potentially other alloying elements.
Different brass alloys can have significantly different mechanical and manufacturing characteristics.
The supplied product information identifies H63, H65, H68, H70 and H90 as examples of brass grades.
These designations should be translated into the appropriate verified international material specification before being used in an OEM drawing or purchase order.
They should not be presented as automatically equivalent to a particular ASTM, EN or other international grade without confirming the chemical composition and material condition.
Brass alloys may offer useful machinability, electrical conductivity and corrosion behavior.
However, these characteristics vary with alloy composition, processing condition and service environment.
The appropriate grade should be selected according to the installation deformation requirements and the finished joint's mechanical performance.
Engineering Information Gain – Brass Formability and Thread Strength Must Be Balanced
A flare-in nut has two important functional regions.
One region provides the internal thread.
Another region must undergo controlled deformation during installation.
These regions impose different requirements on the material.
The threaded portion must resist the intended assembly loads and repeated screw engagement.
The deformable portion must form without unacceptable cracking or loss of retention.
A brass alloy selected primarily for ease of machining may not necessarily provide the best combination of forming behavior and installed thread performance.
Material condition is therefore as important as alloy designation.
For custom brass flare-in nuts, the engineering review should consider the selected alloy, manufacturing process, deformation geometry and required mechanical performance together.
Brass vs. Steel Round Flare-In Nuts
Brass and steel flare-in nuts can use similar general attachment principles, but they should not be treated as mechanically interchangeable.
Steel may be preferred where the specified design requires mechanical properties that are more readily achieved with an appropriate steel grade.
Brass may be considered where its machinability, corrosion behavior or electrical properties provide a functional advantage.
The choice depends on the complete joint design.
A brass insert should not be assumed to provide the same allowable thread load, torque resistance or pull-out performance as a steel insert of similar dimensions.
Substitution requires engineering verification.
Engineering Information Gain – The Lowest-Cost Material Is Not Always the Lowest-Cost Joint
A steel insert may have a lower material cost than a comparable brass component.
However, total assembly cost may also depend on surface treatment, installation process, corrosion requirements and long-term maintenance.
In some applications, brass may reduce the need for a particular finishing operation or offer other material-specific advantages.
In other applications, steel may be more economical or mechanically appropriate.
OEM purchasing teams should compare the complete installed fastening solution rather than only the individual nut price.
Brass vs. Stainless Steel Flare-In Nuts
Brass and stainless steel offer different combinations of mechanical strength, corrosion behavior, conductivity and manufacturing characteristics.
A suitable stainless steel grade may be preferred for particular corrosive environments or strength requirements.
Brass may be selected where its electrical characteristics or forming and machining behavior are relevant.
Neither material is universally superior.
The choice should consider the actual environment, panel material, required load and installation method.
A stainless steel component should not automatically be replaced with brass based only on dimensional similarity.
Round vs. Hexagonal Flare-In Nuts
Round flare-in nuts use cylindrical bodies and are intended for compatible round mounting holes.
Hexagonal flare-in nuts use polygonal body geometry and may provide additional geometric resistance to rotation when installed in appropriately matched holes.
Round holes can be convenient for many sheet-metal manufacturing processes.
However, circular geometry does not provide the same positive polygonal engagement as a hexagonal interface.
For a round brass flare-in nut, rotational resistance depends on the formed attachment and the specific retention features of the design.
Engineers should verify torque resistance rather than assuming the same performance as a hexagonal insert.
Mounting-Hole Engineering
Mounting-hole accuracy is essential for reliable flare-in installation.
The hole must be compatible with the selected insert geometry.
An oversized hole can reduce the effectiveness of the formed connection.
An undersized hole may interfere with insertion or cause undesirable panel deformation.
Hole roundness, burr condition and local panel flatness can also affect installation quality.
The required diameter and tolerance must be obtained from the approved dimensional drawing.
Hole dimensions from a steel flare-in nut or another manufacturer's insert should not automatically be applied to the brass version.
Sheet Thickness and Forming Geometry
The thickness of the parent sheet influences the mechanical attachment.
The insert must have sufficient suitable material to form the intended retaining feature.
The panel must also provide adequate support around the mounting hole.
If the sheet thickness changes, the resulting forming geometry and retention performance may change.
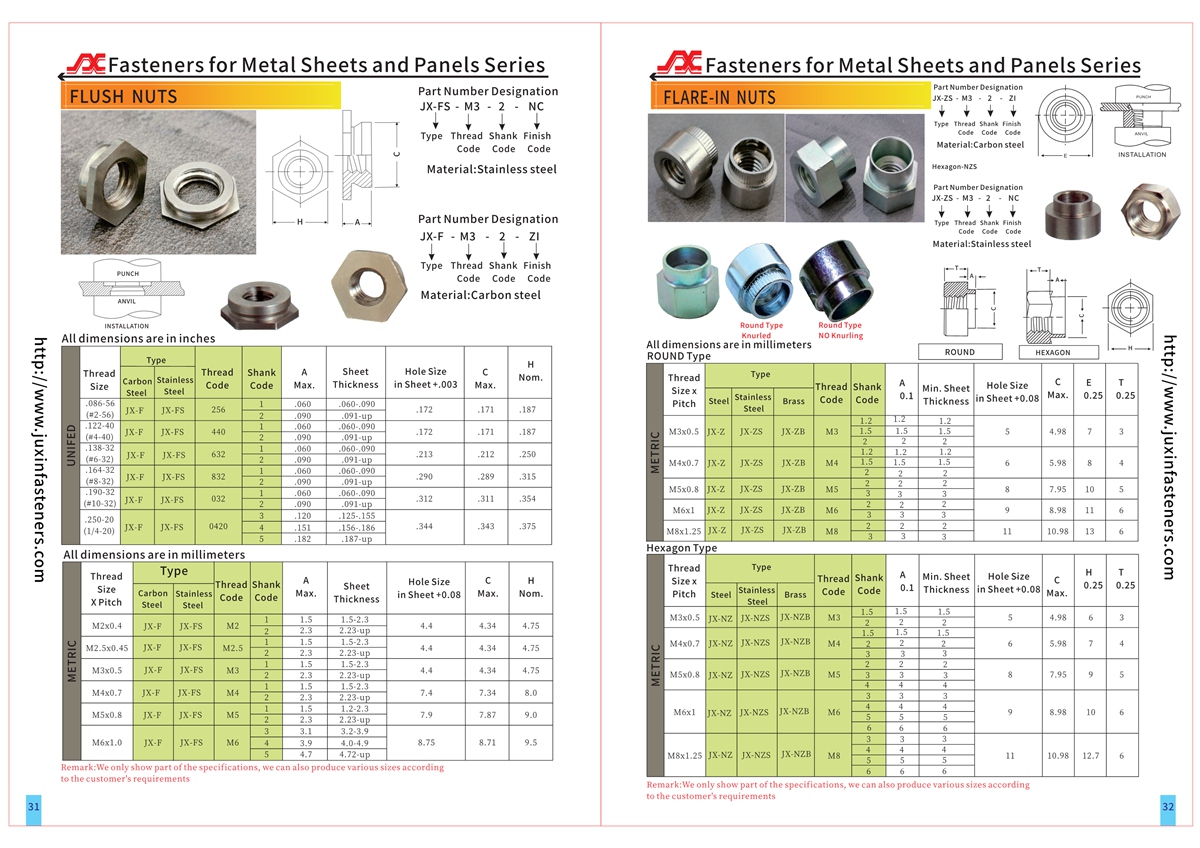
The supplied information does not establish one verified minimum sheet thickness or universal grip range for all brass round flare-in nuts.
These values must be confirmed for the selected size and design.
Where an OEM uses multiple sheet thicknesses, the engineering team should verify whether one insert configuration can accommodate the full range.
Engineering Information Gain – Why Sheet Thickness Cannot Be Selected from Thread Size Alone
Two flare-in nuts may share the same internal thread but have different body lengths, forming sections and mounting-hole requirements.
Consequently, nominal thread size alone is not sufficient to select the correct insert.
A successful design requires compatibility between the fastener's forming geometry and the sheet thickness.
The engineer should therefore specify the mounting panel and installation conditions together with the thread.
This reduces the risk of selecting a part that fits the screw but cannot be installed correctly in the panel.
Installation Process
Brass round flare-in nuts are installed through a controlled mechanical forming operation.
The insert is positioned in the prepared hole.
Suitable tooling supports the assembly and deforms the intended portion of the fastener.
The process must create the specified retaining geometry without unacceptable cracking, thread damage or distortion of the parent sheet.
Installation force, tool geometry and forming stroke depend on the product design.
A general forming-force value should not be applied across all brass alloys and dimensions.
Production tooling should be qualified using representative parts and panels.
Installation Access and Manufacturing Sequence
The forming operation may require access to the surfaces needed for tooling and support.
This should be reviewed before the panel is bent, enclosed or assembled with other components.
Installing the nut before subsequent sheet-metal forming may be practical in some designs.
However, later bending operations can introduce additional deformation or interfere with installed hardware.
The manufacturing sequence should be established according to the complete enclosure design.
The product should not be described as a universal one-sided blind fastener unless that capability is verified for the selected configuration.
Axial Retention and Pull-Out Resistance
Axial retention describes the installed fastener's ability to resist forces that tend to separate it from the panel.
The result depends on the formed geometry, panel material, sheet thickness and installation quality.
The selected brass alloy can also influence the performance of the finished attachment.
No universal pull-out load should be assigned without verified testing or approved engineering data.
Where axial retention is critical, the OEM should establish a suitable acceptance requirement.
Testing should use representative panel materials, hole conditions and installation parameters.
Torque Resistance
A retained threaded insert must resist rotation when the mating screw is tightened or removed.
For a round brass flare-in nut, torque resistance is developed by the installed mechanical connection and any additional design-specific retention features.
The actual value depends on the fastener geometry and the surrounding panel.
It should not be inferred from the nominal thread size.
The permissible tightening torque of the mating screw is a separate engineering consideration.
A fastener may have sufficient thread strength but inadequate resistance to rotation within the panel.
Both requirements should be evaluated where relevant.
Engineering Information Gain – Separate Three Different Failure Modes
A threaded insert can fail in several ways.
The internal thread may strip.
The insert may rotate in the mounting hole.
The insert may pull out of the panel.
These are different failure mechanisms.
A successful test for one condition does not automatically demonstrate acceptable performance for the others.
For OEM qualification, the engineer should identify the relevant failure modes and specify suitable validation requirements.
This is particularly important when changing from steel to brass or from a hexagonal body to a round body.
Thread Selection and Compatibility
The brass round flare-in nut family uses internal threads defined by the selected product drawing.
The exact available thread sizes must be verified against the dimensional table.
ISO 261 and ISO 965 are relevant references for ISO metric thread designation and tolerances.
ASME B1.1 is relevant where Unified inch threads are specified.
Metric and Unified inch thread forms are not directly interchangeable.
A quotation request should identify the complete thread designation, including nominal size, pitch or threads per inch, and required tolerance class.
Mating screw material and surface finish should also be considered.
Electrical Conductivity and Bonding Applications
Brass is electrically conductive.
This characteristic may be relevant in electrical equipment and industrial enclosures.
However, the presence of a brass fastener does not automatically establish a reliable or approved electrical bonding connection.
Electrical continuity depends on the complete contact arrangement, panel finish, contact pressure and service conditions.
Painted or insulated surfaces may affect electrical contact.
Where the joint forms part of a protective bonding system, the finished assembly must be evaluated against the applicable equipment requirements.
A brass flare-in nut should not be advertised as an approved grounding component without appropriate verification.
Engineering Information Gain – Conductive Material Does Not Guarantee Conductive Assembly
An electrical connection is influenced by more than the bulk conductivity of the fastener material.
Oxide films, coatings, surface contamination and contact geometry can affect the interface between the insert and the panel.
A mechanically secure flare-in nut may still require separate evaluation for electrical continuity.
For equipment designers, mechanical retention and electrical performance should therefore be treated as distinct requirements.
Galvanic Corrosion and Dissimilar Metals
Brass may be installed in contact with other metals, including steel, stainless steel or aluminum.
When dissimilar metals are electrically connected in the presence of a suitable electrolyte, galvanic corrosion may become a concern.
The severity depends on the specific materials, exposed surface areas and service environment.
This is particularly relevant for outdoor equipment, humid environments and assemblies subject to condensation.
The engineer should consider the panel material, protective coatings and moisture exposure when selecting the insert.
Suitable corrosion-control measures should be evaluated for the complete assembly.
Brass should not automatically be described as corrosion-proof.
Surface Finish and Appearance
Brass flare-in nuts may be supplied with a surface condition specified by the approved drawing.
The required finish depends on the application and customer requirements.
A coating or surface treatment should not be assumed merely from the appearance of a product photograph.
Where a plated finish is requested, its compatibility with the brass substrate and installation deformation must be reviewed.
The forming operation may place strain on the treated surface.
For corrosion-sensitive applications, the condition of the installed fastener may be more relevant than its appearance before assembly.
Any regulatory or material compliance declaration must be supported by appropriate documentation.
Electrical Cabinets and Power Distribution Equipment
Brass round flare-in nuts may be considered for threaded mounting points in suitable electrical cabinets and power distribution enclosures.
Potential applications include internal brackets, removable covers and equipment mounting panels.
The design should account for panel thickness, installation access, mechanical loading and environmental exposure.
If electrical bonding is part of the intended function, it must be separately validated.
Industrial Control Panels
Industrial control cabinets frequently contain threaded mounting points for brackets, instrument supports and removable components.
Brass flare-in nuts may provide an alternative to welded nuts or directly tapped holes where the mechanical forming process is compatible with the panel.
For equipment requiring repeated service access, thread durability and resistance to rotation should be evaluated.
Telecommunications Equipment
Telecommunications housings often require compact mounting points within sheet-metal structures.
Brass flare-in nuts may be considered for compatible equipment brackets, panels and enclosure components.
The engineering team should review assembly clearances, installation sequence and the corrosion environment.
Where electronic assemblies are nearby, the fastener must be positioned and installed without damaging sensitive components.
Precision Instruments and Electronic Enclosures
Instrument housings and electronic enclosures may require retained internal threads in thin metal components.
Brass inserts can be considered where their material properties are compatible with the application.
The correct fastener should be selected based on mechanical retention, thread size, available space and installation access.
The use of a conductive metal insert does not eliminate the need for electrical clearance or insulation design.
Industrial Machinery and Service Panels
Removable machinery covers and service panels may use retained threaded inserts to simplify maintenance.
A brass flare-in nut may be suitable where its mechanical performance meets the required service conditions.
For vibrating equipment, the complete screw joint should be evaluated for loosening and fatigue.
The installed nut's resistance to rotation is not the same as the mating screw's resistance to loosening.
Additional screw-retention measures may be required depending on the application.
Brass Flare-In Nuts vs. Self-Clinching Nuts
These products use different installation mechanisms.
A conventional self-clinching nut generally relies on displacement of the parent-sheet material into the fastener's retaining features.
A flare-in nut is mechanically formed to establish retention.
This distinction affects tooling, panel compatibility and quality inspection.
The two products should not be treated as direct substitutes without engineering review.
Brass Flare-In Nuts vs. Blind Rivet Nuts
Blind rivet nuts are commonly used where installation must be performed from one accessible side of a panel.
Round flare-in nuts use a mechanical forming process that must be evaluated for its actual tooling access requirements.
The correct choice depends on the panel design and manufacturing sequence.
A flare-in nut should not be described as a blind rivet nut solely because both products provide retained internal threads.
Brass Flare-In Nuts vs. Weld Nuts
Weld nuts require a welding attachment process.
Flare-in nuts use mechanical forming.
Mechanical installation may be considered where welding is undesirable or incompatible with the manufacturing process.
However, the overall cost and performance depend on the panel, equipment, production volume and required inspection.
The fastening technology should be selected using the complete manufacturing and service requirements.
OEM Procurement and Supplier Evaluation
Purchasing managers and supplier-development teams should confirm the actual brass alloy and fastener geometry before comparing quotations.
The approved drawing should define the internal thread, overall dimensions, forming features and required surface condition.
The RFQ should also identify the parent-sheet material, sheet thickness and mounting-hole dimensions.
If mechanical performance is critical, required retention and torque criteria should be stated.
For recurring production programs, dimensional consistency and controlled engineering revisions are important.
Supplier comparisons should use equivalent technical requirements rather than only matching product names.
Frequently Asked Questions
What is a brass round flare-in nut?
It is a cylindrical brass threaded insert that is mechanically secured in a prepared panel hole by flaring or expanding a designated portion of the fastener.
How is a brass flare-in nut installed?
It is positioned in the mounting hole and mechanically formed using suitable installation tooling.
Can brass flare-in nuts replace steel flare-in nuts?
Only after the material properties, installation behavior and required mechanical performance have been reviewed.
Are brass flare-in nuts suitable for aluminum panels?
Suitability depends on the specific insert design, panel properties, mounting-hole geometry and corrosion environment.
Do brass flare-in nuts provide electrical conductivity?
Brass is conductive, but the electrical performance of the installed connection depends on the complete assembly.
Are round flare-in nuts resistant to rotation?
They develop rotational resistance through the installed mechanical connection. The actual performance must be verified for the selected design.
Can brass flare-in nuts be used outdoors?
Outdoor suitability depends on the brass alloy, surrounding metals, moisture exposure and overall corrosion-control design.
Are custom brass flare-in nuts available?
Customer-specific configurations may be reviewed against approved engineering drawings and manufacturing requirements.
What information is needed for an OEM quotation?
Provide the product drawing, brass alloy requirement, thread designation, panel material, sheet thickness, mounting-hole dimensions, finish, expected performance and purchasing quantity.
Relevant International Engineering References
ISO 261 – ISO metric screw thread general plan.
ISO 965 – ISO metric screw thread tolerances.
ASME B1.1 – Unified inch screw threads, where applicable.
EN 12164 – Copper and copper alloys, rod for free machining purposes, where applicable to the selected material form.
EN 12165 – Copper and copper alloys, wrought and unwrought forging stock, where applicable.
ASTM B16/B16M – Free-cutting brass rod, bar and shapes for use in screw machines, where applicable to the selected material.
ISO 6508-1 and ASTM E18 – Rockwell hardness testing.
ISO 9227 and ASTM B117 – Salt-spray test methods where specified.
The applicable material and testing standards must be selected according to the actual product specification. Listing a reference does not establish certification or compliance for every supplied configuration.
Related JUXIN FASTENERS Product Categories
Steel Round Flare-In Nuts – for mechanically retained steel threaded inserts in suitable sheet-metal panels.
Hexagonal Flare-In Nuts – for configurations using compatible polygonal mounting holes.
Steel Self-Clinching Nuts – for conventional sheet-metal clinching applications.
Stainless Steel Self-Clinching Nuts – for applications requiring an appropriate stainless steel fastener.
Self-Clinching Flush Nuts – for applications requiring threaded attachments without intended protrusion from either sheet surface.
Blind Rivet Nuts – for applications requiring a suitable one-sided installation system.
Self-Clinching Standoffs – for threaded mounting points that also provide spacing between components.
Internal links should point to the corresponding verified JUXIN FASTENERS product pages.
Request an OEM Brass Flare-In Nut Quotation
JUXIN FASTENERS supplies brass round flare-in nuts and related industrial sheet-metal threaded inserts.
For a technical review and quotation, please send your 2D drawing or 3D CAD model together with the required thread designation, brass alloy, panel material, sheet thickness and mounting-hole dimensions.
Please include any surface-finish requirements, mechanical performance criteria, estimated annual demand and initial order quantity.
Our team can review the proposed configuration and prepare a quotation based on confirmed technical and commercial requirements.
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
JUXIN FASTENERS – Brass Round Flare-In Nuts and OEM Sheet-Metal Fastening Solutions.
Product Packaging
Product Packaging
Brass round flare-in nuts are packed according to the confirmed product dimensions, order quantity and shipment requirements.
Protective inner packaging and suitable outer cartons may be selected to help reduce handling damage during transportation.
Where appropriate, cartons may be arranged on pallets for industrial shipment.
Different thread sizes, brass alloy specifications and product configurations should be clearly identified to support inventory control and OEM assembly operations.
Packaging quantities, carton dimensions, gross weights, pallet arrangements and customer-specific labeling requirements are confirmed during order processing.
Please include any special packaging or identification requirements in your RFQ.
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Product Pictures
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY