Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

How can industrial manufacturers optimize fastener inventory and reduce the risk of production shortages?
Industrial fastener inventory management is not simply a matter of keeping more boxes of screws, weld nuts, weld studs, or other components in the warehouse.
Product Specification
How can industrial manufacturers optimize fastener inventory and reduce the risk of production shortages?
Industrial fastener inventory management is not simply a matter of keeping more boxes of screws, weld nuts, weld studs, or other components in the warehouse.
For OEM manufacturers, effective inventory management requires coordination between:
Actual production consumption
Demand forecasts
Supplier lead time
Transportation time
Order frequency
Minimum order quantities
Safety stock
Reorder points
Supplier capacity
Packaging quantities
Warehouse capacity
Line-side consumption
Production schedules
Quality-hold risk
Geographic supply-chain exposure
Vendor Managed Inventory (VMI), Kanban replenishment, two-bin systems, scheduled releases, and supplier buffer-stock programs can be useful tools for managing these variables.
However, no single inventory model is appropriate for every fastener.
A low-cost, low-volume maintenance fastener may be managed very differently from a production-critical weld nut used thousands of times per day in an automated assembly line.
For high-volume weld fasteners such as weld nuts and weld studs,
a shortage can interrupt a production process even when the fastener itself represents only a small percentage of the finished product cost.
This creates an important procurement principle:
Fastener inventory should be optimized according to production risk, not simply unit price.
A useful supply-chain model is:
Production Consumption
          |
          v
     Consumption Data
          |
          v
 Forecast + Lead Time + Variability
          |
          v
 Reorder Point / Safety Stock
          |
          v
 Supplier Replenishment
          |
          v
 Transportation / Local Buffer
          |
          v
 Warehouse / Line-Side Stock
          |
          v
 Production Line
The objective is to maintain sufficient availability for production while avoiding unnecessary working capital, excess inventory, obsolete stock, and uncontrolled emergency purchasing.
For OEM customers, JUXIN FASTENERS can discuss replenishment requirements as part of a broader sourcing program, using customer-provided consumption, forecast,
lead-time, packaging, and logistics information to determine an appropriate supply model.
Fasteners often have relatively low unit costs but extremely high usage volumes.
A production plant may consume large quantities of:
Weld nuts
Weld studs
Self-clinching fasteners
Rivet nuts
Screws
Bolts
Washers
Custom fasteners
The relatively low unit cost can make inventory appear unimportant.
That can be misleading.
If a production line requires a specific weld nut to complete an assembly operation,
the economic consequence of a shortage may be much greater than the value of the missing fasteners themselves.
Potential consequences include:
Production interruption
Operator idle time
Emergency freight
Expedited supplier production
Schedule disruption
Line-side labor
Rescheduling
Customer delivery risk
Additional quality inspection
Purchasing intervention
Therefore, inventory management should evaluate total shortage cost, not only component price.
The two-bin Kanban system is a simple replenishment method commonly used for repetitive consumption.
The basic concept is:
             Point of Use
                  |
        +---------+---------+
        |                   |
     BIN A                 BIN B
     In Use               Reserve
        |
        v
     Empty
        |
        v
 Replenishment Signal
When the active bin is consumed, the empty-bin signal triggers replenishment while the second bin provides available stock.
This creates a simple visual replenishment loop.
However, two-bin Kanban should not be described as a universal solution.
Its suitability depends on:
Consumption stability
Replenishment lead time
Container quantity
Available storage space
Production criticality
Supplier delivery frequency
Demand variability
Number of fastener SKUs
Line-side handling requirements
If demand changes significantly or supplier lead time is long and variable, a simple two-bin system may require additional safety stock or a different replenishment method.
The quantity in each Kanban container should be connected to actual consumption and replenishment characteristics.
A practical conceptual relationship is:
Kanban Quantity ≈ Expected Consumption During Replenishment Cycle + Required Buffer
The actual quantity should account for:
Average consumption
Demand variability
Replenishment frequency
Supplier lead time
Transportation time
Container quantity
Desired service level
Production criticality
This means that simply selecting a convenient carton quantity does not necessarily create an effective Kanban system.
Packaging should support the inventory model, not dictate it.
Safety stock exists to absorb uncertainty.
Sources of uncertainty may include:
Demand fluctuations
Forecast error
Supplier production variation
Transportation delays
Customs delays
Quality holds
Weather-related logistics disruption
Customer production changes
Unexpected production increases
A common conceptual model is:
Required Inventory = Expected Demand During Lead Time + Appropriate Safety Buffer
The actual safety-stock calculation should be based on the customer's demand history, lead-time behavior, target service level, and supply-chain risk.
There is no universal safety-stock quantity that can be applied to every weld nut or weld stud.
For example, a fastener consumed consistently every production day may require a different inventory strategy from a custom fastener with irregular demand and a long production lead time.
A reorder point defines when replenishment should begin.
Conceptually:
Reorder Point = Expected Demand During Replenishment Lead Time + Safety Buffer
This is different from simply asking:
“How many pieces are currently in the warehouse?”
Inventory managers should instead ask:
How quickly are these parts being consumed?
How long does replenishment normally take?
How variable is the demand?
How variable is the supplier lead time?
How much inventory is already in transit?
How much stock is available at the plant?
How much is available at the line side?
Is any inventory on quality hold?
What production schedule is expected?
This provides a more accurate view of available supply.
Fastener demand can be derived from production plans rather than purchased independently.
For example:
Fastener Demand ≈ Planned Production Quantity × Fasteners per Assembly
The calculation then needs to consider:
Scrap
Process losses
Engineering changes
Production mix
Safety stock
Forecast accuracy
Customer schedule changes
For OEM programs, procurement and suppliers should distinguish between:
Forecast
A planning signal that may change.
Firm Order
A commercially committed requirement according to the agreed purchasing arrangement.
Production Release
A requirement that the supplier is expected to manufacture or prepare according to the customer's release process.
This distinction is important because suppliers should not automatically treat every long-range forecast as a firm order.
Lead time is one of the most important inputs in inventory planning.
For an imported industrial fastener, total replenishment time may include:
Order Release
     |
     v
Supplier Production
     |
     v
Inspection
     |
     v
Packaging
     |
     v
Export Preparation
     |
     v
International Transportation
     |
     v
Customs / Import Process
     |
     v
Domestic Transportation
     |
     v
Customer Warehouse
The actual supply chain varies by customer, destination, shipment mode, and commercial arrangement.
This is why procurement teams should distinguish between:
Manufacturing lead time
Transit time
Total replenishment lead time
A supplier with a short manufacturing lead time may still create a long replenishment cycle if transportation or customs adds significant variability.
Vendor Managed Inventory is a supply-chain arrangement in which the supplier participates in managing replenishment based on agreed information and inventory rules.
Depending on the program, the supplier may receive information such as:
Consumption data
Current inventory
Forecast
Production schedule
Replenishment signals
Minimum stock level
Maximum stock level
Shipment requirements
The supplier then uses the agreed rules to plan replenishment.
A VMI program therefore depends on data visibility and clearly defined responsibilities.
It is not simply a supplier promise to “keep stock available.”
A conceptual VMI process may look like:
Customer Consumption
        |
        v
Inventory / Consumption Data
        |
        v
Agreed Replenishment Rules
        |
        v
Supplier Planning
        |
        v
Production / Allocated Stock
        |
        v
Shipment
        |
        v
Customer Inventory
        |
        +-------> Consumption Data
                    |
                    +----> Replenishment Loop
The exact operating model depends on the commercial agreement.
Before starting a VMI program, procurement and supply-chain teams should define:
Stock ownership
Inventory location
Minimum inventory
Maximum inventory
Replenishment trigger
Forecast horizon
Order-release process
Supplier lead time
Transportation responsibility
Emergency order procedure
Obsolete inventory responsibility
Engineering change handling
Quality-hold procedure
Inventory reporting
Physical inventory verification
Without clearly defined responsibilities, VMI can simply move inventory-management problems from one organization to another.
For international OEM sourcing, local or regional buffer stock can reduce exposure to transportation variability.
A supplier may potentially support different inventory models depending on the customer's commercial and logistics structure, such as:
Factory-direct supply
Scheduled shipments
Regional inventory
Customer-managed buffer stock
Supplier-managed inventory
Consignment-style arrangements where commercially agreed
Hybrid replenishment programs
Not every model is suitable for every customer.
The correct approach depends on:
Annual consumption
SKU count
Shipment frequency
Destination
Lead time
Inventory ownership
Working-capital strategy
Customer warehouse capacity
Not all fastener SKUs deserve the same inventory policy.
A practical classification may consider:
These are components where a shortage could significantly interrupt production.
Examples may include:
High-consumption weld nuts
Production-critical weld studs
Custom fasteners with long replenishment cycles
These parts may justify closer monitoring and stronger replenishment controls.
These have meaningful but manageable consumption.
They can often be managed through scheduled replenishment and standard inventory controls.
These may have lower demand or less production-critical usage.
For these items, excessive safety stock may create unnecessary inventory carrying cost.
The classification should be based on the customer's actual business impact rather than simply the unit price.
The objective of inventory optimization is to balance two opposing risks.
Too little inventory:
Stockout risk
Emergency freight
Production interruption
Purchasing escalation
Customer delivery risk
Too much inventory:
Working capital
Warehouse space
Obsolescence
Packaging degradation
Inventory counting burden
Engineering-change exposure
The optimal point is therefore not “maximum inventory.”
It is the inventory level that provides an appropriate service level at an economically justified cost.
For custom weld fasteners, this becomes especially important because an engineering change may make existing stock difficult or impossible to use.
Custom fasteners require additional inventory planning because their demand may be tied to a specific product design.
Potential risks include:
Product redesign
Engineering change
Customer model change
Program cancellation
Material substitution
Surface-treatment change
Thread or geometry revision
Therefore, purchasing teams should discuss:
Forecast commitment
Production batch size
Minimum order quantity
Finished-goods inventory
Raw-material inventory
Tooling ownership
Engineering change procedures
before building large inventories of custom components.
This is one reason why inventory strategy should be connected to the product-development and procurement process.
Article 25 discussed fastener packaging and feeder compatibility.
Inventory planning should connect directly to packaging strategy.
For example, if a production line consumes a fastener in standardized containers, the Kanban quantity may be based partly on that practical container unit.
The supply chain then becomes:
Supplier Pack Quantity → Warehouse Unit → Line-Side Container → Feeder/Hopper → Production Consumption
If the packaging quantity is poorly matched to consumption, the factory may experience:
Excessive replenishment
Partial-container handling
More packaging waste
Increased counting effort
More line-side storage
Poor inventory visibility
Therefore, packaging and inventory management should be designed together.
Automated assembly creates another supply-chain consideration.
When weld fasteners are fed automatically, production may depend on:
Correct fastener geometry
Correct packaging
Feeder availability
Line-side replenishment
Correct part identification
Reliable supply
A fastener shortage is therefore not the only risk.
Incorrect parts or packaging can also stop the production process.
Inventory management should therefore protect against:
Stockout
Wrong part
Mixed lot
Packaging error
Quality hold
Damaged fasteners
Engineering revision mismatch
For automated production, inventory accuracy becomes part of production reliability.
Modern OEM supply chains increasingly rely on digital inventory information.
Useful data points can include:
Part number
Lot number
Quantity
Location
Consumption rate
Forecast
Open purchase orders
In-transit inventory
Reorder point
Safety stock
Supplier lead time
The objective is to provide a reliable picture of available-to-production inventory.
This is particularly important when several plants, warehouses, or suppliers are involved.
A central procurement team may need to know not only how much inventory exists globally, but also:
Where is it, and can it reach the production line when needed?
Large OEM customers may purchase the same or related fasteners for multiple manufacturing locations.
In this situation, inventory management can become more complex.
Potential models include:
Plant-level inventory
Regional distribution
Centralized inventory
Supplier-held buffer
Multi-location scheduled replenishment
Procurement teams should evaluate:
Demand by plant
Transportation distance
Local production schedules
Regional customs requirements
Warehouse capacity
Emergency supply routes
SKU standardization
Where the same fastener can be standardized across multiple plants, procurement may also be able to improve forecasting and purchasing efficiency.
However, standardization should never override engineering requirements.
A robust fastener supply strategy should identify potential failure points before a shortage occurs.
Important risk questions include:
Is there more than one approved manufacturing source?
Is the supplier's production capacity adequate?
Are critical raw materials available?
Is tooling capacity sufficient?
How long is the normal transit time?
How variable is transportation?
Are there alternative shipping methods?
Is regional stock available where justified?
What happens if a production lot is placed on quality hold?
Is replacement stock available?
Can the supplier respond to a quality issue quickly?
How accurate are forecasts?
How frequently do production schedules change?
Are seasonal demand changes expected?
Are engineering changes controlled?
Could an existing inventory become obsolete?
Is the latest drawing revision clearly identified?
This risk-based approach is more effective than simply increasing safety stock indefinitely.
Emergency purchasing is often expensive.
Possible additional costs include:
Expedited production
Air freight
Premium transportation
Overtime
Manual intervention
Special inspection
Additional packaging
Purchasing escalation
A well-designed replenishment system should therefore aim to reduce the frequency of emergency orders.
However, emergency supply requirements can still occur because of:
Unexpected demand
Production disruption
Forecast error
Supplier quality issues
Transportation disruption
The objective is not to claim that emergencies can always be eliminated.
The objective is to establish a supply system that reduces their frequency and limits their impact.
Supply-chain teams should measure the performance of the inventory system.
Useful metrics may include:
Stockout frequency
Inventory turnover
Days of inventory
Emergency shipment frequency
Forecast accuracy
Supplier on-time delivery
Replenishment cycle time
Inventory accuracy
Excess inventory
Obsolete inventory
Line-side shortage incidents
These metrics help determine whether a VMI or Kanban system is actually improving the supply chain.
A program should not be considered successful merely because more inventory is available.
The goal is reliable production with controlled inventory investment.
Before establishing a VMI or Kanban program, procurement teams should confirm:
Part number
Drawing revision
Material
Surface treatment
Packaging specification
Critical dimensions
Annual consumption
Monthly consumption
Peak consumption
Production schedule
Forecast accuracy
Manufacturing lead time
Transit time
Replenishment frequency
Supplier capacity
Emergency supply procedure
Minimum stock
Maximum stock
Safety stock
Reorder point
Inventory ownership
Warehouse location
Line-side storage
Container quantity
Pallet configuration
Transportation method
Lot traceability
Inspection requirements
Quality-hold process
Nonconforming material procedure
MOQ
Pricing structure
Forecast commitment
Inventory carrying responsibility
Obsolete-stock responsibility
A VMI program should ideally be introduced in stages.
Review:
Historical consumption
Current inventory
Supplier lead time
Purchase frequency
Stockout history
Emergency shipment history
Identify:
Production-critical parts
High-consumption parts
Low-consumption parts
Long-lead custom parts
Determine whether each SKU is best suited to:
Scheduled ordering
Kanban
Two-bin replenishment
Min/max inventory
Supplier-managed replenishment
Hybrid supply
Start with a limited group of production-critical or high-consumption fasteners.
Monitor:
Consumption
Replenishment
Inventory accuracy
Shortages
Excess inventory
After the model is validated, additional fastener SKUs or production locations can be incorporated.
This staged approach reduces the risk of implementing a complicated inventory system before the underlying data and responsibilities are clear.
Procurement teams can ask suppliers:
What is the normal manufacturing lead time?
How does lead time vary with order quantity?
What information is required for production planning?
Can the supplier support forecast-based planning?
Can inventory be allocated for a specific customer program?
What packaging quantities are available?
Can packaging be matched to Kanban requirements?
How are engineering changes controlled?
How are quality holds handled?
What emergency-supply options exist?
Can multiple production plants be supported?
How are lot numbers and shipment quantities controlled?
These questions help procurement teams evaluate supply capability beyond the quoted unit price.
Inventory strategy should not be discussed only after the purchase order is issued.
During the RFQ stage, procurement should already provide:
Annual demand
Expected order frequency
Production ramp-up
Forecast information
Destination
Packaging requirements
Automated feeding requirements where applicable
Required delivery schedule
Customer inventory strategy
This allows the supplier to understand the actual supply-chain requirement.
Article 22 established the importance of a complete weld fastener RFQ.
Article 25 established the connection between packaging and automated feeding.
Article 26 extends that logic:
RFQ → Manufacturing → Quality → Packaging → Logistics → Inventory → Production
This creates a more complete OEM sourcing model.
A low-value fastener can still be production-critical.
Safety stock should be based on demand and supply variability rather than an arbitrary number.
Long-range forecasts may change and should be distinguished from firm releases.
Manufacturing lead time is only one part of total replenishment time.
Inventory that cannot be released for production should not be treated as available stock.
Packaging can influence practical Kanban and replenishment quantities.
More inventory does not automatically mean lower supply-chain risk.
Production-critical custom weld fasteners and low-consumption standard components may require very different inventory policies.
A practical decision framework is:
                FASTENER SKU
                     |
          +----------+----------+
          |                     |
      Demand Level        Production Criticality
          |                     |
          +----------+----------+
                     |
              Lead-Time Risk
                     |
          +----------+----------+
          |                     |
     Stable Supply        Variable Supply
          |                     |
          +----------+----------+
                     |
          Select Inventory Model
                     |
       +-------------+-------------+
       |             |             |
    Kanban         Min/Max        VMI
       |             |             |
       +-------------+-------------+
                     |
             Measure Performance
The final inventory policy should reflect the actual production and supply-chain environment.
For OEM customers purchasing industrial weld fasteners, supply-chain performance is closely connected to engineering, manufacturing, packaging, and logistics.
JUXIN FASTENERS can review customer requirements involving:
Weld nuts
Weld studs
Custom weld fasteners
Annual consumption
Production schedules
Packaging requirements
Automated feeding considerations
Delivery requirements
Sourcing locations
Inventory planning requirements
The appropriate supply model should be established based on the customer's actual data and commercial requirements.
This may involve conventional scheduled purchasing, forecast-based production planning, packaging standardization, buffer-stock discussions, or other replenishment structures depending on the program.
The objective is not to promise that every customer requires VMI.
The objective is to determine whether VMI, Kanban, scheduled replenishment, or another supply model provides the best balance between production continuity,
inventory investment, logistics reliability, and procurement control.
This article should connect with the broader JUXIN FASTENERS engineering and procurement architecture:
Weld Fasteners Solutions
Fastener Procurement & RFQ Best Practices
Fastener Supplier Quality Audits & Certifications
Fastener Packaging & Feeder Compatibility
Custom Weld Fasteners
Fastener Surface Finishes & Coatings
Automotive BIW Weld Fasteners
EV Battery Enclosure Weld Fasteners
The recommended information path is:
Product Selection → RFQ → Supplier Qualification → Quality → Packaging → Inventory → Automated Production → Long-Term OEM Supply
Vendor Managed Inventory is a supply arrangement in which the supplier participates in monitoring and replenishing agreed inventory according to defined rules and customer information.
The exact responsibilities, inventory ownership, stock levels, and replenishment process should be established contractually.
It can be suitable for high-consumption or production-critical weld fasteners, particularly where demand and replenishment requirements can be monitored reliably.
However, VMI is not automatically the best solution for every SKU.
No.
A two-bin system can provide a simple replenishment signal and a buffer between consumption and replenishment,
but it cannot eliminate risks caused by unexpected demand, supplier delays, transportation disruption, quality holds, or incorrect inventory settings.
Safety stock should reflect demand variability, lead-time variability, desired service level, and production criticality.
There is no universal safety-stock quantity applicable to all industrial fasteners.
Not necessarily.
Inventory policy should reflect consumption, production criticality, replenishment lead time, supply risk, and the economic consequences of shortage and excess inventory.
It can be one of the practical inputs, particularly when the production line consumes standardized containers.
However, the container quantity should still be evaluated against consumption rate, replenishment lead time, storage capacity, and required service level.
VMI requirements can be discussed as part of an OEM supply-chain program.
The actual model depends on customer demand, locations, logistics arrangements, inventory responsibilities, and agreed replenishment rules.
Useful information includes annual consumption, monthly demand, production schedules, plant locations,
current inventory, required delivery frequency, packaging requirements, supplier lead-time expectations, and any automated assembly requirements.
If your company is purchasing production-critical weld nuts, weld studs,
or custom industrial fasteners, include inventory and replenishment requirements in the sourcing discussion from the beginning.
Send JUXIN FASTENERS:
Part drawings or specifications
Annual consumption
Monthly or seasonal demand information
Production locations
Required delivery frequency
Current or target inventory model
Packaging requirements
Automated feeding requirements, where applicable
Forecast information
Required lead-time targets
Quality and traceability requirements
Email: info@juxinfasteners.com
JUXIN FASTENERS — Precision Fastening Solutions Since 2003.
Effective fastener inventory management is not about holding the largest possible stock.
It is about building a controlled supply loop in which demand, manufacturing, quality, packaging, logistics, replenishment, and production consumption are connected.
For OEM manufacturers, the right inventory strategy is therefore part of the fastening solution itself.
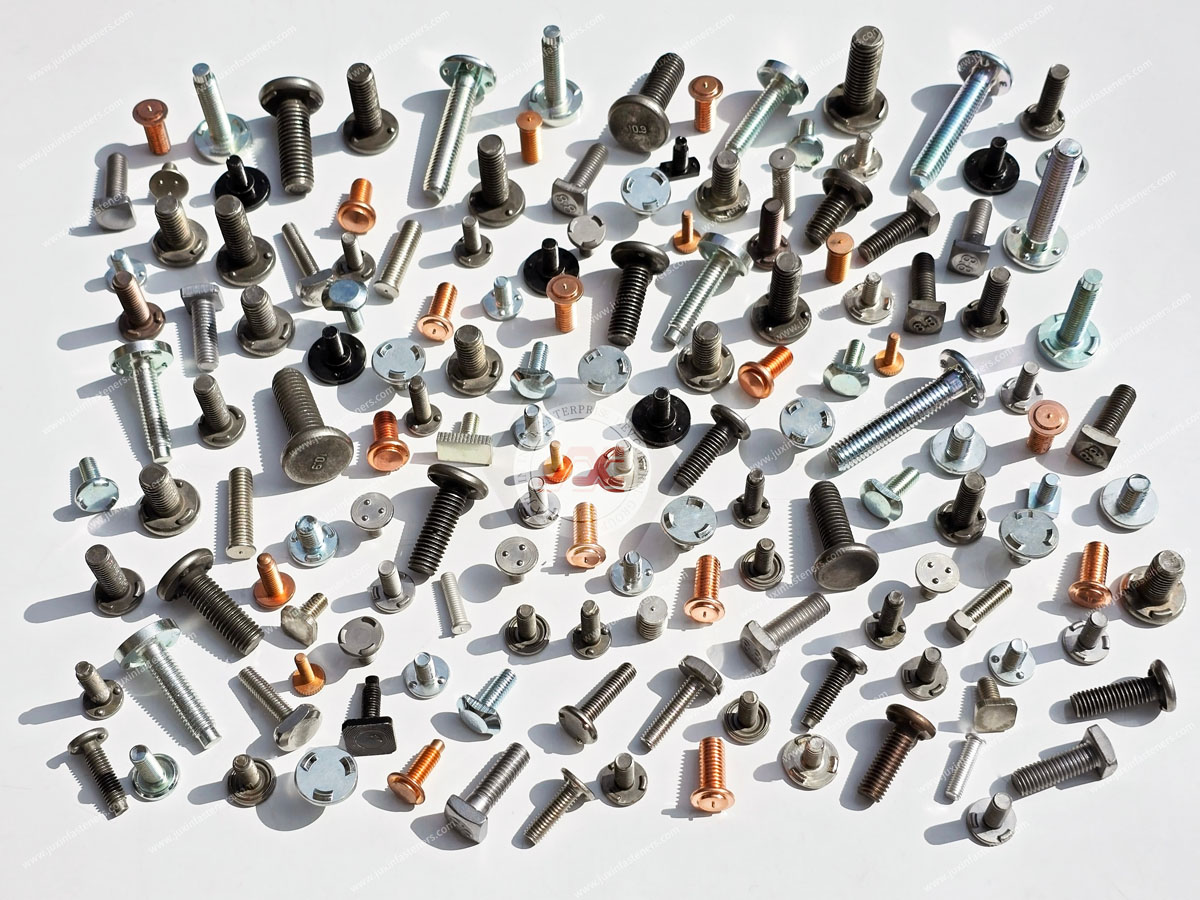
Product Packaging
Packaging Standard
At Juxin Fasteners, we apply standardized export packaging to ensure product protection, traceability, and compliance with international logistics requirements.
1. Standard Export Packaging
Unless otherwise specified, all products will be packed according to our factory standard export packaging, which includes:
Moisture-resistant inner protection
Poly bag or small box packing as required
Reinforced export cartons
Clear labeling with part number, specification, batch number, and quantity
Palletizing for sea or air shipment when necessary
Our standard packaging is designed to ensure safe transportation, efficient warehousing, and long-distance international shipping.
2. Customized Packaging Options
We also provide customized packaging solutions according to customer requirements, including but not limited to:
Private labeling
Customized barcodes
Specific carton dimensions
Retail packaging
Special pallet configuration
Customer-specific marking and identification
So that you know, customized packaging may involve additional costs and extended lead time depending on the complexity of the requirements.
3. Compliance & Quality Assurance
All packaging processes are controlled under our ISO 9001 quality management system to ensure consistency, traceability, and product integrity throughout the supply chain.
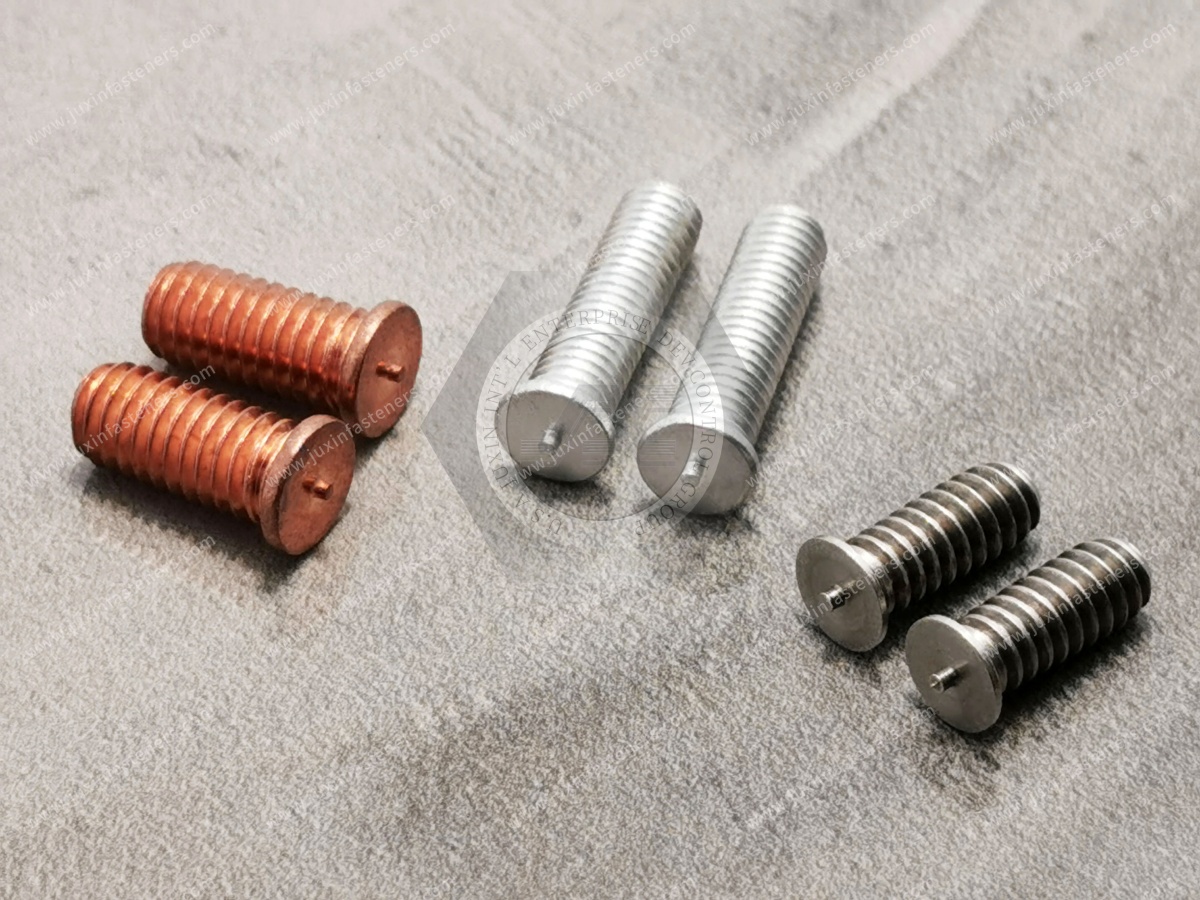
Product Pictures
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY