
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Aug. 11, 2026
How can engineers determine whether a critical bolt still has the required preload after months or years in service?
This question matters in wind-energy equipment, industrial machinery, transportation systems, pressure-containing equipment,
structural assemblies and other bolted joints where loss of clamp force can affect reliability.
But there is an important distinction:
Bolt monitoring is not the same as bolt design.
Sensors and inspection technologies can help detect changes in a joint. They cannot compensate for an incorrectly designed fastener, unsuitable material,
poor tightening process, uncontrolled friction or inadequate initial preload.
The engineering sequence should therefore be:
Joint Design → Fastener Selection → Installation → Baseline Verification → In-Service Monitoring → Diagnosis → Corrective Action
The original article presented ultrasonic measurement, vibration monitoring and fiber-optic sensing as three major monitoring approaches.
Those technologies remain useful topics, but a stronger OEM engineering question is:
What parameter actually needs to be monitored, how accurately must it be known, and what maintenance decision will be made from the result?
This guide explains how design engineers, maintenance engineers, reliability teams, procurement managers and supplier-development professionals can build
a practical bolt preload monitoring strategy without confusing measurement technology with joint qualification.
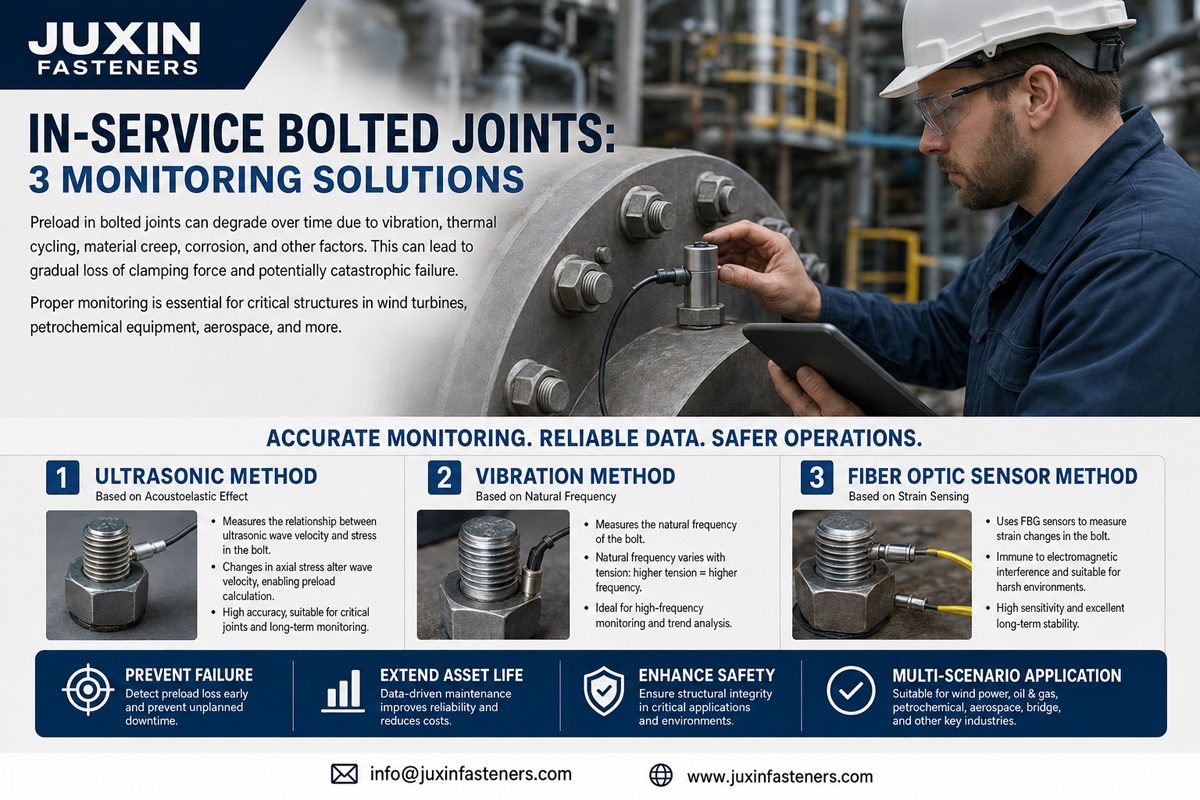
Several methods can be used depending on the joint and required information.
Measures changes in ultrasonic transit behavior through the bolt and, with appropriate calibration and compensation, can be used to estimate bolt elongation, stress or tension.
Best suited when engineers need quantitative information about an individual accessible fastener.
Looks for changes in the dynamic behavior of the assembly that may indicate reduced joint stiffness, looseness or other structural changes.
Best suited as a structural condition-monitoring or screening approach rather than assuming it directly measures individual bolt preload.
Measures strain or related structural response using sensors such as electrical strain devices or fiber-optic sensing technologies.
Potentially useful for continuous monitoring and multi-point structural health systems.
But no method should be selected before defining:
What is being measured
Required accuracy
Baseline condition
Temperature effects
Accessibility
Number of bolts
Monitoring frequency
Environment
Maintenance decision threshold
The statement:
"Bolt preload decreases over time."
is too broad when presented as an inevitable condition for every bolted joint.
A properly designed and installed joint may retain adequate clamp load for its intended service.
Preload can change, however, because of mechanisms such as:
Embedment
Joint settlement
Creep
Stress relaxation
Gasket relaxation
Thermal effects
Plastic deformation
Joint slip
Coating compression
Material changes
Fastener or joint damage
The original article attributed in-service preload reduction broadly to vibration, thermal cycling, creep and corrosion.
A better diagnostic approach is to identify the mechanism rather than assume that all service exposure causes the same preload decay.
This distinction is fundamental.
Clamp force decreases.
The bolt or nut may not rotate.
Possible causes include:
Embedment
Creep
Gasket relaxation
Thermal mismatch
Plastic deformation
The bolt or nut rotates relative to the mating thread.
This can occur under dynamic conditions, particularly when sufficient relative movement develops across the joint interfaces.
Therefore:
Preload loss ≠ rotational self-loosening.
A monitoring system intended to detect one should not automatically be assumed to detect the other.
Maintenance teams frequently inspect bolts using a torque wrench and then interpret the result as bolt preload.
That can be misleading.
The core principle is:
Torque ≠ Preload.
Tightening torque is strongly influenced by friction.
Preload is the axial clamp-producing force created by bolt elongation.
Residual breakaway or checking torque measured later is affected by additional factors and should not automatically be converted into remaining preload.
Therefore:
Residual torque ≠ direct preload measurement.
For joints where actual bolt tension matters, a method that measures or estimates bolt elongation or strain may provide more useful information than torque checking alone.
An in-service measurement becomes much more valuable when engineers know the original condition.
A useful baseline may include:
Bolt identification
Material
Mechanical property class
Heat treatment
Geometry
Effective length
Surface treatment
Lubrication condition
Tightening method
Installation torque
Target preload
Measured initial preload where applicable
Temperature
Sensor calibration data
Measurement position
Without baseline data, engineers may be able to detect an abnormal condition but have difficulty determining how much the joint has changed.
The monitoring strategy should therefore begin during manufacturing or installation—not after a field problem appears.
Ultrasonic measurement is one of the best-known methods for evaluating tension in installed bolts where the fastener geometry and measurement conditions are suitable.
The basic concept is to transmit an ultrasonic signal through the bolt and evaluate changes in propagation behavior associated with bolt elongation and stress.
The original article correctly identified time-of-flight change and calibration as key elements of ultrasonic measurement.
However, ultrasonic measurement should not be described as a universally direct force measurement independent of calibration.
A better description is:
Measured Ultrasonic Response + Bolt Geometry + Material Calibration + Temperature Compensation → Estimated Bolt Elongation / Stress / Tension
Potential advantages include:
Non-destructive measurement
Ability to evaluate individual bolts
Quantitative trend monitoring
Measurements before and after tightening
Repeat inspection during maintenance
Potential correlation with bolt elongation and preload
This can be valuable when torque alone does not provide enough information about clamp load.
Two bolts with the same nominal dimensions do not automatically produce identical ultrasonic behavior.
Important variables can include:
Material
Heat treatment
Microstructure
Geometry
Bolt length
End condition
Stress state
Temperature
Therefore, calibration should reflect the actual fastener and measurement method.
Same bolt size ≠ same ultrasonic calibration.
For OEM projects, changing fastener material or heat treatment may require reviewing the measurement correlation.
Temperature can change:
Bolt length
Acoustic velocity
Joint dimensions
Material response
A change in ultrasonic transit time can therefore result from both:
Mechanical stress
Temperature
Without appropriate compensation, the measurement may incorrectly interpret thermal change as preload change.
For systems operating across large temperature ranges:
Temperature compensation is part of the measurement system—not an optional refinement.
Ultrasonic measurement normally requires suitable signal transmission and reflection.
Measurement quality can be influenced by:
Bolt-end surface condition
End parallelism
Geometry
Surface roughness
Coating
Couplant
Transducer positioning
Accessible measurement surface
If ultrasonic inspection will be used throughout the product life, the bolt itself may need to be designed with measurement accessibility in mind.
This creates an important engineering concept:
Monitoring requirements can become fastener design requirements.
The original article stated that ultrasonic monitoring had limited applicability below approximately M20 or 200 mm bolt length.
That should not be treated as a universal engineering limit.
Practical feasibility depends on:
Instrument
Transducer
Bolt geometry
Length
Diameter
Signal quality
Required accuracy
Calibration method
A specific monitoring supplier or instrument may have operating limits, but these should not be generalized to all ultrasonic preload measurement.
The old article also quoted approximately 1.5% full-scale measurement performance.
That may be achievable for a particular instrument and controlled setup, but it should not be presented as a universal accuracy for ultrasonic bolt preload monitoring.
Measurement uncertainty depends on:
Calibration
Temperature
Material consistency
Geometry
Instrument
Transducer placement
Operator
Signal processing
Repeatability
For critical joints, specify the required measurement uncertainty and validate the complete measurement process.
Instrument specification ≠ application measurement uncertainty.
Ultrasonic measurement may be considered for selected:
Large structural bolts
Wind turbine fasteners
Flange bolts
Anchor bolts
Heavy industrial machinery
Critical equipment joints
Large custom bolts
Selected transportation applications
But suitability must be established for the specific fastener and access condition.
Vibration analysis takes a different approach.
Instead of measuring individual bolt tension directly, it evaluates changes in the dynamic behavior of the structure.
A bolted joint contributes to overall:
Stiffness
Damping
Contact behavior
Load transfer
If joint conditions change, the structural dynamic response may also change.
Possible monitored features include:
Natural frequencies
Frequency response
Mode shapes
Damping behavior
Signal features derived from vibration data
The original article described reduced preload as causing joint stiffness changes that may become visible in structural vibration response.
That is a useful concept, but the relationship is not universally one-to-one.
A structural vibration response can change because of many variables:
Boundary conditions
Temperature
Operating speed
Added mass
Bearing condition
Structural damage
Joint condition
Sensor position
Environmental noise
Therefore:
Changed vibration signature ≠ confirmed bolt preload loss.
Vibration analysis is often more useful for:
Screening
Trend monitoring
Detecting structural change
Identifying areas requiring further inspection
rather than directly assigning a preload value to a specific bolt.
Imagine a large flange containing many bolts.
Measuring every bolt continuously may be expensive or impractical.
Structural monitoring can potentially provide a higher-level warning that the assembly behavior has changed.
The maintenance workflow may then become:
Structural Screening → Identify Abnormal Zone → Targeted Bolt Inspection → Root-Cause Diagnosis
This can be more economical than installing an individual sensor on every fastener.
Bolt tension produces elastic strain.
That means strain measurement can potentially be correlated with bolt load.
Possible technologies include:
Bonded electrical strain gauges
Instrumented bolts
Load-sensing washers
Integrated sensor fasteners
Fiber-optic strain sensors
Each approach has different implications for:
Calibration
Wiring
Environmental protection
Installation
Maintenance
Cost
The sensor should therefore be selected according to the required maintenance decision rather than technological novelty.
Fiber Bragg Grating, or FBG, sensors detect changes in reflected wavelength associated with strain and temperature.
The original article highlighted their ability to support multiple sensing points and distributed structural monitoring architectures.
Potential advantages include:
Multiple sensing locations
Lightweight sensing networks
Long-distance optical signal transmission
Electromagnetic immunity
Potential continuous monitoring
These characteristics can make fiber-optic sensing attractive for large structural health monitoring systems.
FBG sensors respond to both:
Strain
Temperature
This creates cross-sensitivity.
A wavelength shift alone should therefore not automatically be interpreted as bolt preload change.
The system may require:
Reference temperature measurement
Compensation strategy
Sensor packaging design
Calibration
Again:
Sensor output ≠ preload until the measurement relationship is established.
A sensor attached to a bolt does not automatically experience exactly the same strain as the bolt.
Load transfer can depend on:
Adhesive
Sensor location
Packaging
Surface preparation
Bond length
Protective layer
Geometry
Poor strain transfer can create measurement error.
For long-term industrial monitoring, sensor protection must also address:
Moisture
Chemicals
Mechanical damage
Temperature
Cable routing
Maintenance access
This is why laboratory sensing performance and field performance should be treated separately.
In addition to external sensing systems, some applications use fasteners or washers incorporating load-indicating features.
Depending on the technology, these may use:
Mechanical indicators
Direct-tension indicators
Embedded strain sensing
Electronic sensing
RFID or wireless communication
Load-sensing washers
These technologies can reduce the separation between fastener and monitoring system.
But:
Smart fastener ≠ automatically accurate preload measurement.
The same engineering questions still apply:
What is measured?
How is it calibrated?
What is the uncertainty?
What is the temperature effect?
What happens after repeated loading?
How is the sensor protected?
What is the maintenance strategy?
| Method | What It Primarily Observes | Individual Bolt Capability | Continuous Monitoring Potential | Major Engineering Challenge |
|---|---|---|---|---|
| Ultrasonic measurement | Acoustic response correlated with elongation/stress | High | Possible with suitable architecture | Calibration, temperature, access |
| Vibration analysis | Structural dynamic response | Usually indirect | High | Separating bolt condition from other structural changes |
| Electrical strain sensing | Local strain | High | High | Sensor bonding, wiring, drift, environment |
| FBG sensing | Optical wavelength response to strain/temperature | High / multi-point | High | Packaging and temperature compensation |
| Load-sensing washer / instrumented fastener | Force/strain-related response | High | Technology-dependent | Calibration and integration |
| Torque audit | Rotational resistance | Individual fastener | Usually periodic | Does not directly equal preload |
No method is universally superior.
Monitoring only creates value when it supports a maintenance decision.
Before installing sensors, define actions such as:
Continue operation
Schedule inspection
Retighten according to approved procedure
Replace fastener
Investigate joint settlement
Inspect for fatigue
Inspect corrosion
Shut down equipment
Escalate engineering review
Without decision thresholds, a monitoring system can produce large amounts of data without reducing risk.
A practical architecture is:
Measurement → Threshold → Diagnosis → Maintenance Action
not simply:
Sensor → Dashboard → More Data
Continuous bolt monitoring may be appropriate when:
Failure consequences are high
Inspection access is difficult
Joint condition changes cannot be tolerated
Downtime is expensive
Condition data materially improves maintenance planning
The monitoring system itself can be maintained
But continuous monitoring may be unnecessary for many conventional industrial joints.
Periodic inspection may be more appropriate when:
Joint risk is moderate
Access is easy
Fasteners are inexpensive
Failure is detectable before becoming hazardous
Replacement intervals are well established
More monitoring ≠ automatically better reliability.
The monitoring strategy should match the risk.
A useful decision process can be divided into five levels.
Ask:
What happens if preload is lost?
Is the failure safety-related?
Can it cause leakage?
Can it stop production?
Is there redundancy?
Determine whether the primary risk is:
Settlement
Creep
Self-loosening
Fatigue
Corrosion
Overload
Thermal effects
Decide whether the most useful parameter is:
Bolt strain
Bolt elongation
Structural vibration
Joint displacement
Temperature
Leakage
Another system response
Select the method that can reliably measure the required parameter.
Define the decision threshold and corrective action.
This prevents expensive sensors from being installed without a clear reliability objective.
A monitoring system cannot rescue an uncontrolled installation process.
Before the equipment enters service, engineers should control:
Fastener material
Mechanical property class
Thread condition
Surface treatment
Lubrication
Mating surfaces
Tightening method
Target preload
Tightening sequence
Tool calibration
If initial preload varies widely, later monitoring becomes much harder to interpret.
Poor installation + sophisticated monitoring ≠ reliable joint.
Fastener coatings can influence friction during tightening.
Examples include:
Zinc plating
Zinc-nickel
PTFE-based coatings
Other customer-specified finishes
Remember:
Same torque + different friction ≠ same preload.
If a monitored joint changes from one fastener coating to another during second-source qualification, the original tightening process may require review.
The sensor may accurately detect a different bolt tension, but the root cause may be the coating/friction change rather than service degradation.
Bolt monitoring should not be separated from fastener metallurgy.
Changes in:
Material grade
Mechanical property class
Heat treatment
Hardness
can affect:
Elastic response
Ultrasonic calibration
Fatigue performance
Hydrogen embrittlement susceptibility
Failure mode
For this reason:
Same dimensions ≠ monitoring equivalence.
A second-source bolt that fits the assembly may still require new calibration or validation.
For high-strength bolts, engineers should consider both joint performance and fastener integrity.
Potential risks may include:
Excessive preload
Fatigue
Hydrogen embrittlement
Stress corrosion where material/environment combinations are susceptible
Thread damage
Surface-treatment effects
A monitoring system that reports reduced preload does not automatically identify the root cause.
The correct response may require metallurgical and failure analysis.
Corrosion can affect bolted joints through several mechanisms.
Depending on the assembly, it may cause:
Cross-section loss
Surface damage
Thread damage
Increased disassembly torque
Seizure
Joint-interface changes
But corrosion does not simply translate into one predictable preload-loss curve.
Therefore:
Corrosion detection ≠ preload measurement.
And:
Preload change ≠ proof of corrosion.
Both conditions may need separate inspection methods.
Wind turbines contain large bolted connections in areas such as:
Tower flanges
Equipment mounting structures
Large structural interfaces
These joints may experience:
Cyclic loading
Environmental exposure
Temperature variation
Difficult maintenance access
Depending on the joint criticality, engineers may consider:
Controlled installation
Periodic ultrasonic inspection
Structural vibration monitoring
Instrumented fasteners
Continuous strain monitoring
But each bolted interface requires its own maintenance and qualification strategy.
Industrial machinery may contain hundreds or thousands of bolted joints.
Continuous sensing of every bolt is rarely economically justified.
A practical strategy may divide joints into:
Critical Joints → Quantitative Monitoring
Important Joints → Periodic Inspection
General Joints → Standard Preventive Maintenance
This risk-based approach can provide better lifecycle economics than treating every fastener identically.
Automotive production generally emphasizes:
Controlled tightening
Process monitoring
Traceability
Torque-angle strategies where appropriate
End-of-line quality control
rather than installing permanent sensors on every production bolt.
For selected research, structural testing or highly specialized applications, direct load measurement may be valuable.
But:
Bolt sensor ≠ automotive joint qualification.
And in EV applications:
Mechanical preload monitoring ≠ battery-system safety qualification.
Railway vehicles and infrastructure contain many different classes of bolted connections.
Monitoring strategies should distinguish:
Interior equipment
Secondary equipment
Structural assemblies
Safety-critical systems
For non-critical equipment, conventional inspection may be sufficient.
Primary structural, running gear, braking and other safety-critical joints require applicable OEM, project and regulatory maintenance procedures.
Monitoring technology ≠ railway safety approval.
Loss of joint clamp load can contribute to sealing problems in selected flange and gasketed connections.
But leakage can also result from:
Gasket damage
Surface condition
Thermal cycling
Flange distortion
Incorrect assembly sequence
Material compatibility
Therefore:
Leakage ≠ proof that one bolt has lost preload.
Diagnosis should evaluate the complete flange system.
| Observed Condition | Possible Cause | Useful Engineering Response |
|---|---|---|
| Ultrasonic reading changes | Preload, temperature, calibration or measurement condition changed | Verify compensation and repeatability before diagnosis |
| Structural vibration signature changes | Joint condition or another structural/operating variable changed | Perform targeted inspection |
| Bolt preload decreases without rotation | Settlement, creep, thermal effects or deformation | Investigate joint interfaces |
| Nut/bolt rotates | Self-loosening mechanism | Review transverse movement and locking strategy |
| Preload differs between new supplier bolts | Material, coating, friction or calibration difference | Review second-source qualification |
| Preload falls repeatedly after retightening | Joint design or material relaxation problem | Investigate root cause instead of repeated tightening |
| Bolt fractures | Fatigue, overload, hydrogen-related failure or other mechanism | Perform formal failure analysis |
| Joint leaks | Clamp-load issue or sealing-system problem | Inspect complete joint |
| Sensor drifts over time | Temperature, packaging, electronics or calibration issue | Validate measurement system |
If monitoring identifies reduced preload, the automatic response should not always be:
"Tighten the bolt again."
Repeated tightening without understanding the cause can be inappropriate if the joint is experiencing:
Plastic deformation
Thread damage
Gasket degradation
Fastener yielding
Material creep
Fatigue cracking
The maintenance procedure should define when a fastener can be retightened and when it must be replaced or the joint inspected.
Detected preload loss → root-cause evaluation → approved maintenance action.
For high-value critical joints, traceability may include:
Fastener ID
Location
Drawing revision
Lot
Material
Surface treatment
Installation date
Installation tool
Initial tightening result
Baseline sensor result
Inspection history
Maintenance action
This allows reliability teams to distinguish individual anomalies from broader process trends.
Monitoring creates an additional qualification dimension.
Suppose an OEM approves a second-source bolt with:
Same dimensions
Same thread
Same mechanical property class
That does not automatically mean the existing monitoring calibration remains valid.
Compare:
Drawing + Revision + Material + Mechanical Properties + Heat Treatment + Hardness + Thread + Geometry + Surface Treatment + Friction
+ Installation Behavior + Elastic Response + Monitoring Interface + Calibration + Functional Testing + Documentation + Change Control
For ultrasonic systems, material and geometry changes may affect acoustic calibration.
For bonded sensors, surface treatment changes may affect sensor attachment.
For instrumented bolts, manufacturing changes may affect the sensing system.
Therefore:
Same dimensions ≠ functional equivalence.
And:
Same fastener specification ≠ automatically identical sensor calibration.
Procurement and supplier-development teams should ask:
Is the bolt standard or drawing-based?
What material is required?
What mechanical property class applies?
What heat treatment applies?
Is hardness controlled?
What surface treatment applies?
Is friction controlled?
What installation method is used?
Is a target preload specified?
Will ultrasonic measurement be used?
Are bolt-end geometry or surface requirements needed for sensing?
Will a strain sensor be attached?
Are traceability requirements defined?
Is individual identification required?
What inspection documentation is required?
Are production changes subject to customer approval?
These questions help ensure that monitoring requirements are considered during sourcing rather than added after production.
Condition monitoring should be evaluated economically as well as technically.
A useful model is:
Lifecycle Joint Cost = Fastener Cost + Installation + Monitoring + Inspection + Maintenance + Downtime + Rework + Replacement + Warranty Risk + Failure Risk
For a low-risk machine cover, continuous bolt monitoring may have no economic justification.
For a difficult-to-access critical structural connection, monitoring may reduce inspection cost or unplanned downtime.
The objective is not maximum sensor coverage.
It is:
Appropriate monitoring for the consequence and probability of failure.
Even sophisticated monitoring cannot eliminate the importance of fastener quality.
The overall system may still fail because of:
Wrong material
Incorrect heat treatment
Thread defects
Coating problems
Dimensional errors
Poor tightening
Inadequate joint design
This is why monitoring and fastener supplier qualification should be connected.
Measurement technology cannot compensate for an unsuitable fastener.
JUXIN FASTENERS focuses on the fastening components and drawing-based engineering requirements that form the mechanical foundation of monitored bolted joints.
Relevant product capabilities include:
Carbon steel bolts and screws
Stainless steel bolts and screws
High-strength fasteners
Nuts
Nylon insert lock nuts
All-metal lock nuts
All-metal flange lock nuts
Flat washers
Precision washers
Weld nuts
Weld studs
Self-clinching fasteners
Custom cold-formed fasteners
CNC secondary-machined components
Drawing-based OEM fasteners
Second-source fastener development
For applications using ultrasonic, strain-based or other bolt monitoring technologies, fastener requirements can be evaluated for:
Material
Mechanical properties
Heat treatment
Geometry
Bolt-end condition
Surface treatment
Friction
Thread
Installation requirements
Traceability
Drawing control
JUXIN FASTENERS does not treat the sensor system itself as a substitute for the OEM's structural-health-monitoring, inspection or safety qualification process.
There is no universal best method. Ultrasonic measurement can be useful for quantitative individual-bolt evaluation,
while strain sensing and structural monitoring may be better for other architectures.
Torque can be used as part of an installation strategy, but torque does not directly equal preload because friction strongly influences the relationship.
Not reliably as a universal rule. Breakaway or residual torque is affected by friction and other interface conditions and should not automatically be converted into remaining clamp load.
It measures changes in ultrasonic propagation through the bolt and uses calibrated relationships involving material, geometry,
stress and temperature to estimate elongation or tension.
Yes. Material, heat treatment, geometry, temperature and measurement setup can influence the relationship between ultrasonic response and bolt tension.
Potentially, depending on the instrument, transducer, geometry, length, signal quality and required accuracy.
There is no universal M20 minimum applicable to every system.
Generally, it evaluates structural dynamic behavior. Changes may indicate joint-condition changes,
but they do not automatically provide individual bolt preload.
FBG sensors can measure strain-related optical wavelength changes that may be correlated with bolt load when the sensor system is properly designed,
calibrated and temperature-compensated.
Not necessarily. Monitoring strategy should be based on failure consequence, accessibility, inspection cost, failure mechanism and maintenance value.
Not automatically. Determine why preload was lost and follow an approved maintenance procedure.
It may. Bolt length, material, end geometry, surface condition and accessibility can affect measurement quality.
Monitoring requirements should preferably be identified before production.
Do not assume so. Material, heat treatment, geometry and other manufacturing differences may affect the measurement relationship.
Provide the drawing, revision, material, mechanical property class, heat treatment, surface treatment, tightening requirements,
target preload where applicable, monitoring method and any sensor-interface requirements.
JUXIN FASTENERS' role is the fastening component and drawing-based fastener requirement.
Monitoring equipment and structural-health-monitoring systems should be specified and qualified through the appropriate sensing or monitoring-system provider.
Because monitoring detects conditions; it does not eliminate failures caused by unsuitable material, heat treatment, geometry, coating, thread quality or installation behavior.
For accurate engineering and commercial evaluation, provide:
2D drawing
3D model if available
Part number
Drawing revision
Application
Fastener type
Thread size and pitch
Fastener length
Grip length
Base material
Material grade
Mechanical property class
Heat treatment
Hardness requirement
Surface treatment
Coating thickness where applicable
Friction requirement where applicable
Lubrication condition
Mating nut or internal thread
Washer requirements
Joint materials
Tightening method
Installation torque
Torque-angle requirement where applicable
Target preload where applicable
Initial preload verification method
Monitoring method
Ultrasonic measurement requirements where applicable
Bolt-end geometry requirements
Sensor attachment requirements where applicable
Operating temperature
Temperature cycling
Vibration environment
Corrosion environment
External loading
Fatigue requirements
Traceability requirements
Individual fastener identification if required
Inspection documentation
Functional testing
PPAP or customer-specific documentation where applicable
Annual volume
Existing approved sample for second-source development where available
For an existing monitored joint, also provide the current measurement method and calibration requirements so that second-source compatibility can be evaluated.
This page should connect internally with existing JUXIN FASTENERS resources covering:
Bolt tightening and over-torque
Torque, friction and preload
Spring lock washers and flat washers
Bolt and nut strength class matching
Hydrogen embrittlement in high-strength fasteners
Fastener surface finish selection
Zinc plating and zinc-nickel coatings
Nylon insert lock nuts
All-metal lock nuts
Automotive fastening solutions
Railway fastening solutions
Wind-energy fastening applications
Custom high-strength fasteners
Second-source fastener qualification
Use the existing indexed JUXIN FASTENERS URL when implementing each internal link.
The intended content path is:
Bolted Joint Design → Installation & Preload → Baseline Measurement → In-Service Monitoring → Failure Diagnosis → Maintenance → Fastener Supplier Qualification → RFQ
The most useful bolt monitoring strategy begins before a sensor is selected.
Start with:
What can fail?
Then ask:
Which physical parameter changes before that failure?
Then:
Can we measure it reliably enough to make a maintenance decision?
The complete reliability path is:
Joint Design → Fastener Specification → Controlled Installation → Baseline → Measurement → Trend → Diagnosis → Maintenance Action
Ultrasonic measurement can provide valuable quantitative information for suitable individual bolts.
Vibration monitoring can help identify structural changes across larger assemblies.
Strain and fiber-optic sensing can support continuous or distributed monitoring where the application justifies the complexity.
But none of these technologies changes the fundamental requirements of a reliable bolted joint.
Monitoring ≠ Joint Design.
Torque ≠ Preload.
Sensor Output ≠ Root Cause.
Standard Compliance ≠ Application Qualification.
For design engineers, this framework connects sensing technology with actual joint mechanics.
For maintenance teams, it converts measurements into actionable reliability decisions.
For procurement and supplier-development teams, it shows why monitored fasteners require tighter control of material,
heat treatment, geometry, coating, installation behavior and change management—not merely dimensional interchangeability.
JUXIN FASTENERS supports OEM, Tier-1, Tier-2 and industrial manufacturers with high-strength fasteners, bolts, nuts, lock nuts,
precision washers, weld fasteners, self-clinching fasteners, custom cold-formed components, CNC secondary-machined parts and drawing-based second-source development.
For a monitored bolted joint, critical fastener project, second-source qualification or preload-related failure investigation,
send your drawing, revision, material and mechanical requirements, surface treatment, installation method, target preload,
monitoring interface requirements, service environment and annual volume for technical review.
JUXIN FASTENERS
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY



