
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Oct. 29, 2023
A drawing that says only "black finish" does not fully specify a fastener surface treatment.
Black fasteners can be produced using several fundamentally different coating technologies, including black zinc,
black zinc-nickel, black zinc-flake, phosphate-based finishes, black oxide and organic coating systems.
They may look similar.
They do not necessarily provide the same:
Corrosion performance
Coating thickness
Friction
Tightening behavior
Thread fit
Wear behavior
Process compatibility
Hydrogen embrittlement considerations
Cost
For OEM engineers, procurement managers and supplier-development teams, this creates an important sourcing principle:
Black Color ≠ Coating Specification.
JUXIN FASTENERS supplies selected black zinc-nickel coated bolts, screws, nuts, rivet nuts and drawing-based industrial fasteners according to customer drawings and project requirements.
This guide explains when black Zn-Ni should be considered, how it differs from other black finishes, and what should be controlled when qualifying a production or second-source supplier.
Black zinc-nickel fasteners use a zinc-nickel alloy electroplating system combined with a black finishing system that can include passivation and,
depending on the specification, a sealer, topcoat or lubricant.
A simplified coating architecture can be represented as:
Steel Fastener → Surface Preparation → Zinc-Nickel Alloy Deposit → Black Passivation → Optional Sealer / Topcoat / Lubricant
This is important because the visible black surface represents only one part of the finished coating system.
The engineering performance depends on the complete system.
Therefore:
Black Zn-Ni appearance ≠ complete Zn-Ni specification.
Black zinc-nickel may be considered when a project requires a combination of:
Black appearance
Higher corrosion requirements than a conventional finish can provide
Thin engineered coating suitable for threaded components
Controlled friction where required
OEM-defined surface-treatment requirements
Compatibility with high-volume assembly
Production repeatability
Potential applications can include selected:
Automotive components
EV equipment
Industrial machinery
Automation equipment
Electrical enclosures
Power electronics
Outdoor industrial equipment
Appearance-sensitive mechanical assemblies
However, black Zn-Ni should not be specified simply because the component must be black.
If the engineering requirement is primarily appearance and the environment is mild, another finish may be more economical.
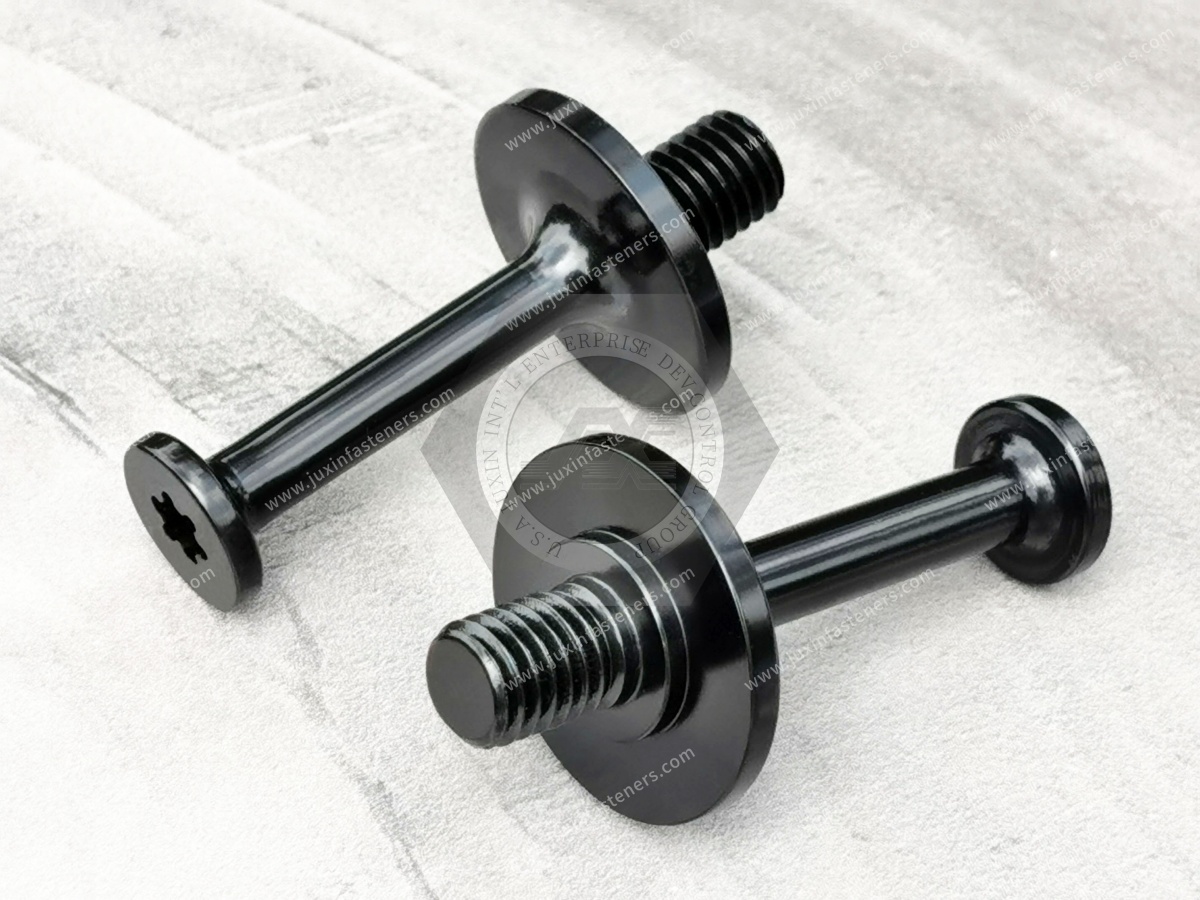
A useful first-stage comparison is:
| Black Finish | Process Family | Typical Reason to Evaluate | Important Engineering Questions |
|---|---|---|---|
| Black zinc | Electroplating | General corrosion protection + black appearance | Corrosion requirement, thickness, friction |
| Black zinc-nickel | Alloy electroplating | Higher corrosion requirement + black appearance | Zn-Ni system, passivation, topcoat, friction |
| Black zinc-flake | Non-electrolytic coating system | Demanding corrosion protection, selected high-strength fasteners | Basecoat/topcoat, friction, thickness |
| Black phosphate | Conversion coating | Lubricant retention, process function, dark appearance | Oil/lubricant, corrosion requirement |
| Black oxide | Conversion finish | Dark appearance and selected functional uses | Post-treatment, environment, corrosion expectation |
| Black e-coat | Organic coating | Appearance and protective film | Film thickness, curing, thread fit |
This table is a selection framework rather than a universal performance ranking.
The correct finish depends on the actual joint.
Black zinc and black zinc-nickel can look similar enough that visual inspection alone may not distinguish their engineering performance.
But the deposited metallic layers are different.
Black zinc typically uses a zinc electroplated layer followed by a black finishing system.
It may be suitable for selected general industrial applications where:
Conventional corrosion protection is sufficient
Black appearance is required
Cost sensitivity is important
The applicable specification permits the system
Black Zn-Ni uses a zinc-nickel alloy deposit.
It may be considered where:
Corrosion requirements are more demanding
An OEM specification calls for Zn-Ni
Friction must be controlled
The application requires a specific engineered coating system
The correct decision is not:
Black Zn-Ni is always better than black zinc.
It is:
Use the least complex coating system that reliably satisfies the application requirements.
Black Zn-Ni and black zinc-flake can both be used for demanding industrial applications, but their process technologies are fundamentally different.
| Engineering Factor | Black Zinc-Nickel | Black Zinc-Flake |
|---|---|---|
| Process type | Electroplating | Non-electrolytic coating |
| Metallic system | Zinc-nickel alloy | Zinc/aluminum flake-based system |
| Black appearance | Through specified finishing system | Through specified coating/topcoat system |
| Corrosion capability | System-dependent | System-dependent |
| Friction | Must be specified where important | Must be specified where important |
| Thread fit | Coating thickness must be controlled | Coating thickness must be controlled |
| High-strength steel | Electroplating process requires hydrogen-risk review | Avoids electrolytic deposition, but complete process still requires review |
| OEM substitution | Requires engineering review | Requires engineering review |
Neither coating should be substituted for the other solely because both are black.
Same Color ≠ Same Coating Technology.
Black phosphate has a very different engineering role from black Zn-Ni.
Phosphate conversion coatings can support functions such as:
Lubricant retention
Oil retention
Paint preparation
Selected wear behavior
Dark appearance
The finished corrosion performance depends strongly on the complete system, including oil or other post-treatment where used.
Black phosphate should therefore not automatically be treated as equivalent to black Zn-Ni for demanding corrosion requirements.
If an old drawing says only:
"Black finish"
the engineering team should determine whether the original requirement was driven by:
Appearance
Corrosion
Lubricity
Assembly
Light reflection
Identification
Another functional reason
Only then should a replacement coating be selected.
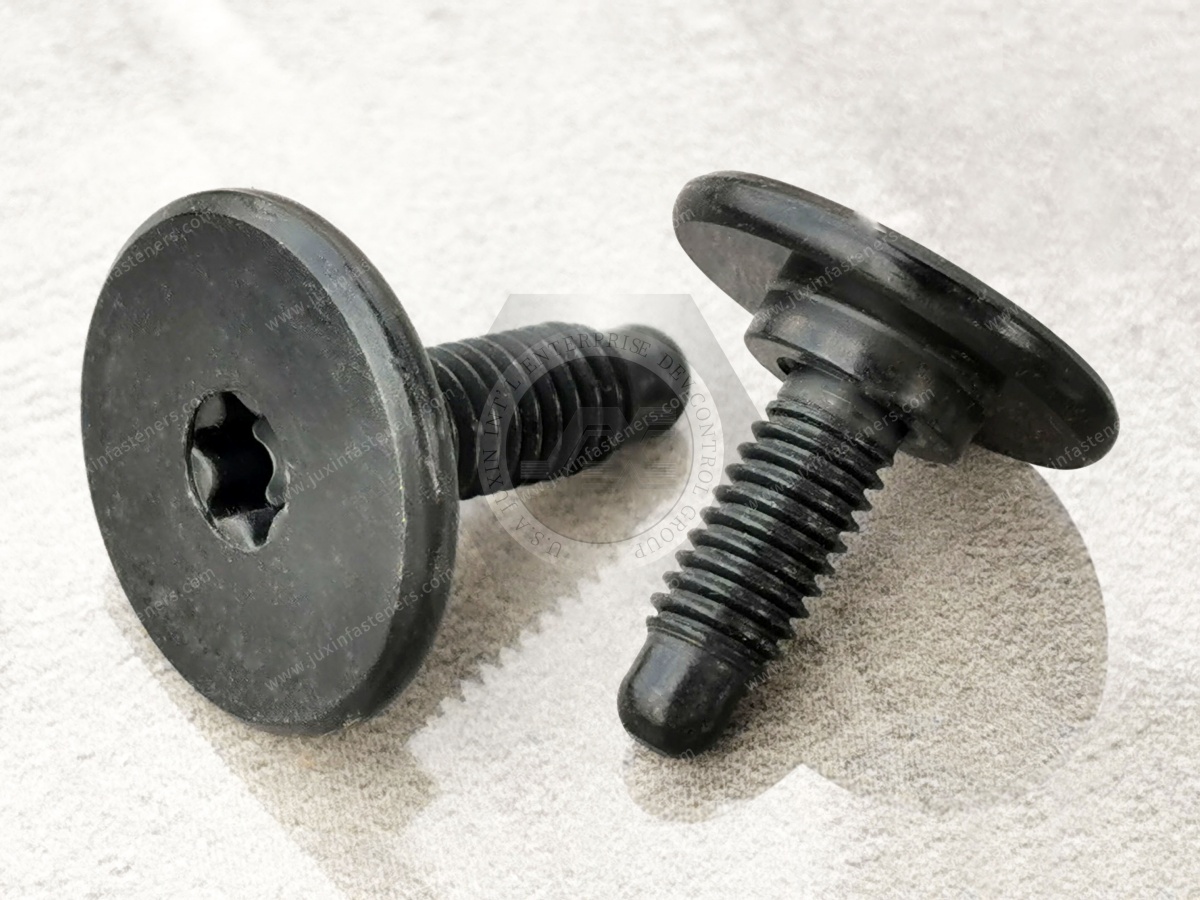
Black oxide can produce an attractive dark finish with minimal dimensional buildup.
That can be useful for selected components.
But:
Black oxide ≠ black zinc-nickel.
The two systems use different protection mechanisms and should not be considered direct substitutes simply because both create a black appearance.
Where corrosion protection is important, the complete environmental requirement must be evaluated before approving a black oxide finish.
Electrophoretic coating can also create a uniform black appearance.
However, e-coating is an organic film system rather than Zn-Ni electroplating.
For threaded components, film thickness can become important because it may influence:
Thread engagement
Gauging
Assembly torque
Mating compatibility
A black e-coated bracket bolt and a black Zn-Ni bolt may therefore look similar while behaving differently during assembly.
Even the description:
"Black Zinc-Nickel"
may not be complete enough for an engineered OEM fastener.
Additional requirements may include:
Base material
Mechanical property class
Heat-treatment condition
Zn-Ni coating specification
Alloy composition requirement
Coating thickness
Black passivation
Sealer
Topcoat
Lubricant
Friction requirement
Corrosion test
Acceptance criteria
Final thread condition
Appearance criteria
Hydrogen embrittlement controls where applicable
This is why drawing control matters.
A common sourcing assumption is that one black finish is "better" because it looks darker, smoother or more uniform.
Appearance does not establish corrosion performance.
Actual performance can depend on:
Coating chemistry
Thickness
Passivation
Sealer
Topcoat
Substrate
Surface preparation
Process control
Handling
Installation damage
Environment
Therefore:
Darker Black ≠ Better Corrosion Resistance.
Cosmetic acceptance and corrosion acceptance should be treated as separate requirements.
Black Zn-Ni coatings may be specified against salt-spray requirements.
But a number such as:
720 hours
or
1,000+ hours
is incomplete without additional information.
The specification should identify, where applicable:
Test method
Test duration
Coating system
Substrate
Coating thickness
Passivation
Topcoat
White corrosion criterion
Red corrosion criterion
Acceptance criteria
Therefore:
Salt Spray Hours ≠ Complete Coating Specification.
Laboratory corrosion testing provides controlled comparative information.
It does not directly predict years of service in an automotive, machinery, coastal or outdoor application.
Field exposure can involve:
Wet/dry cycling
Chlorides
Chemicals
Temperature variation
Abrasion
Stone impact
Joint crevices
Coating damage
Galvanic interaction
Therefore:
Salt Spray Hours ≠ Field Service Life.
Procurement teams should avoid comparing coatings solely by the largest advertised laboratory-hour number.
Zn-Ni coating adds material to the fastener surface.
On threaded components, this means coating thickness must remain compatible with:
Thread tolerance
Mating component
Final gauging
Assembly
Functional engagement
Internal threads can require particular attention because coating buildup reduces available clearance.
Therefore:
More Coating Thickness ≠ Automatically Better Fastener Performance.
A coating that provides corrosion protection but prevents correct assembly has not met the overall fastener requirement.
For threaded joints, one of the most important but frequently overlooked coating characteristics is friction.
The surface system can influence friction at:
Threads
Bearing surface
Washer interface
Mating component
This affects the relationship between applied tightening torque and resulting fastener tension.
Therefore:
Torque ≠ Preload.
And:
Same Torque + Different Friction ≠ Same Preload.
This is why two black fasteners with the same dimensions can behave differently on the same assembly line.
A topcoat is not always just an additional corrosion layer.
Depending on the coating system, it may also influence:
Friction
Lubricity
Tightening consistency
Appearance
Handling
Corrosion performance
Therefore, replacing one black Zn-Ni topcoat with another can potentially change assembly behavior.
For torque-controlled OEM applications, the approved topcoat should be included in change-control decisions where it affects functional performance.
A useful drawing may need to define both:
Appearance Requirement: Black
and
Functional Requirement: Controlled Friction Range
These should not be assumed to mean the same thing.
A coating supplier may be able to produce the required black appearance using multiple finishing systems, but they may not provide identical tightening behavior.
Engineering should therefore specify both when both matter.
High-strength steel fasteners require additional attention because Zn-Ni is an electroplating process.
Potential hydrogen introduction can occur during manufacturing stages such as:
Cleaning
Pickling
Surface activation
Electroplating
Susceptibility depends on:
Material
Strength
Hardness
Residual stress
Applied stress
Manufacturing route
Pretreatment
Plating process
Therefore:
Black Zn-Ni ≠ Hydrogen-Embrittlement-Free Process.
Where high-strength fasteners are involved, the applicable material, OEM and international requirements should govern process selection.
Hydrogen embrittlement cannot meaningfully be reduced to statements such as:
"Black Zn-Ni has a 1.5% hydrogen embrittlement risk."
Risk is component- and process-dependent.
For susceptible components, engineering should instead control:
Base material
Hardness
Pretreatment
Acid exposure
Plating process
Post-plating treatment
Timing of post-treatment
Verification requirements
Where required, relevant ISO, ASTM or OEM requirements should be followed.
Post-plating baking may form part of a hydrogen embrittlement risk-control process for susceptible components where required.
However:
Baking ≠ Guaranteed Elimination of Hydrogen Embrittlement.
Process control must begin with appropriate material and manufacturing decisions before the part reaches the baking stage.
Black Zn-Ni coated bolts may be evaluated where a project requires black appearance together with an engineered corrosion-protection system.
The RFQ should identify:
Bolt material
Property class
Thread
Coating specification
Black finish requirement
Coating thickness
Topcoat
Friction requirement
Mating component
Tightening method
Corrosion test
Environment
For high-strength bolts, hydrogen embrittlement controls may also be relevant.
For screws, the coating must remain compatible with the installation process.
Relevant variables include:
Screw material
Thread form
Drive geometry
Mating material
Installation torque
Friction
Coating damage during driving
Appearance requirement
For thread-forming or self-tapping applications, installation can place significant local stress on the coating.
Testing the installed component may therefore provide more useful information than evaluating the unused screw alone.
Internally threaded black Zn-Ni nuts require control of coating buildup.
Engineering should consider:
Nut material
Mechanical property requirement
Internal thread tolerance
Coating thickness
Mating bolt
Final gauging
Friction
Corrosion requirement
A visually acceptable nut that no longer assembles correctly is not an acceptable finished component.
Lock nuts introduce an additional torque characteristic:
Prevailing Torque.
Prevailing torque is generated by the locking feature and is different from joint preload.
Therefore:
Prevailing Torque ≠ Preload.
Surface treatment can influence torque behavior, especially where metal-to-metal friction contributes to the locking mechanism.
For second-source lock nuts, engineering should therefore compare both:
Locking behavior
Finished surface system
not merely dimensions and color.
Rivet nuts are mechanically deformed during installation, so coating selection must consider installed behavior.
Important variables include:
Rivet nut material
Coating system
Coating thickness
Grip range
Body geometry
Parent sheet
Hole geometry
Setting process
Pull-out
Spin-out
The coating should remain compatible with the required deformation and installation process.
Remember:
Pull-Out ≠ Spin-Out.
And:
More Setting Force ≠ Better Installation.
The rivet nut, coating, parent sheet and installation tool form one fastening system.
This requires process review.
Weld nuts depend on controlled electrical and thermal behavior at the welding interface.
Surface condition can influence that process.
Important variables include:
Nut material
Projection geometry
Parent sheet
Coating
Welding current
Welding time
Electrode force
Electrical contact
Thread protection
Therefore:
Coating Substitution Can Be a Welding-Process Change.
A black Zn-Ni finish should not simply be added to a weld nut drawing without confirming welding compatibility.
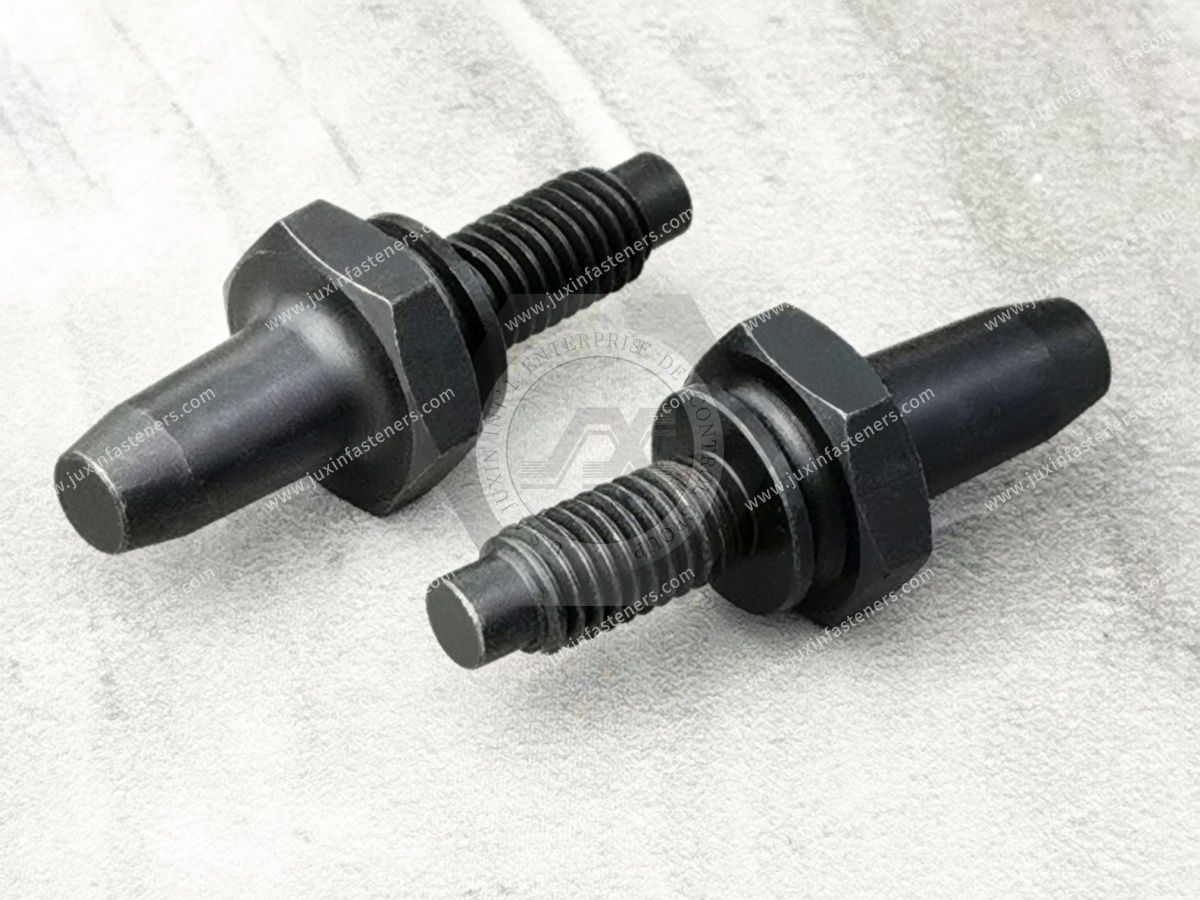
Automotive projects are a major commercial application area for black Zn-Ni fasteners.
Potential JUXIN FASTENERS products can include selected:
Bolts
Screws
Nuts
Lock nuts
Rivet nuts
Custom drawing-based components
Possible application areas include selected:
Body equipment
Brackets
Electrical equipment
EV-related equipment
Interior or exterior hardware
Underbody-related components where the applicable specification permits the coating
However, automotive requirements vary significantly by vehicle location.
A black Zn-Ni fastener should be qualified against the applicable drawing and OEM requirements.
Automotive application ≠ automatic safety-critical qualification.
EV platforms and power-electronic equipment often combine:
Steel
Aluminum
Copper alloys
Plastics
Coated sheet
Electronic components
This makes material compatibility important.
Black Zn-Ni fasteners may be considered for selected:
Electrical enclosures
Power modules
Brackets
Battery-related equipment
Cooling equipment
Serviceable covers
Cable-management hardware
Engineering should evaluate:
Corrosion
Galvanic compatibility
Friction
Thermal cycling
Electrical contact strategy
Serviceability
A metallic coating does not automatically establish grounding or electrical performance.
Black fasteners are frequently specified on machinery because they integrate visually with equipment frames, enclosures and mechanisms.
But industrial applications can also require corrosion and assembly performance.
Black Zn-Ni may be considered for selected:
Automation equipment
Robotics
Manufacturing machinery
Industrial enclosures
Material-handling equipment
Outdoor machinery
The actual requirement should distinguish between:
Cosmetic Black
and
Functional Black Coating.
This distinction can prevent unnecessary coating cost.
AI data centers, telecom systems, electrical cabinets and power equipment use large numbers of threaded and sheet-metal fastening components.
Black finishes may be specified for:
Equipment racks
Enclosures
Cooling equipment
Power modules
Control systems
Internal mounting hardware
Potential products can include:
Black coated screws
Black nuts
Black rivet nuts
Black lock nuts
Custom black fasteners
Where the fastener is part of a grounding path or electrical interface:
Conductive Metallic Coating ≠ Qualified Electrical Connection.
Electrical performance must be defined and validated separately.
Black coated fasteners may be used in selected railway:
Interior equipment
Enclosures
Electrical cabinets
Secondary equipment
Non-primary attachment applications
Selection should consider corrosion, vibration, maintenance and the project specification.
Primary structural, running gear, braking, crash-related and other safety-critical railway applications require formal project-specific qualification.
A black Zn-Ni finish alone does not establish railway suitability.
Applying a high-performance coating to a steel fastener does not eliminate the need to evaluate the mating materials.
Mixed-material assemblies can contain:
Carbon steel
Stainless steel
Aluminum
Copper alloys
In the presence of an electrolyte, galvanic interaction may become relevant.
Risk depends on:
Material combination
Coating
Exposed area
Electrical contact
Environment
Coating damage
Joint geometry
Therefore:
Corrosion-Resistant Fastener ≠ Corrosion-Resistant Assembly.
Black Zn-Ni may be unnecessary when:
The environment is mild
Conventional zinc satisfies the corrosion requirement
Black appearance is the only requirement
A non-electrolytic system is preferred for the specific high-strength component
The customer drawing specifies another coating
The coating is incompatible with the manufacturing process
The additional cost creates no functional value
A good supplier should not automatically recommend the most expensive coating.
The objective is to select the appropriate surface system for the application.
Instead of writing:
Finish: Black
consider whether the drawing needs to define:
Base Material + Mechanical Requirement + Coating Technology + Thickness + Passivation + Topcoat + Friction + Corrosion Test + Appearance + Final Thread Requirement
The exact level of detail depends on the application.
For a cosmetic cover screw, fewer controls may be sufficient.
For a torque-controlled OEM joint, much more may need to be defined.
Black Zn-Ni is particularly vulnerable to incorrect visual substitution.
A second-source component can look nearly identical while using a different surface system.
Therefore:
Same Dimensions + Same Black Color ≠ Functional Equivalence.
A second-source review may need to compare:
Drawing revision
Base material
Mechanical properties
Heat treatment
Thread
Zn-Ni system
Alloy requirement
Coating thickness
Black passivation
Sealer
Topcoat
Friction
Corrosion requirement
Hydrogen embrittlement controls
Installation behavior
Appearance
Final assembly performance
For rivet nuts, installed performance may need to be compared.
For weld fasteners, welding behavior may need to be compared.
For torque-controlled bolts, friction may be critical.
Before comparing quotations, procurement and supplier-development teams should answer:
| Question | Why It Matters |
|---|---|
| Is black appearance cosmetic or functional? | Determines whether Zn-Ni is necessary |
| What exact coating technology is required? | Prevents black-finish substitution |
| What is the base fastener material? | Affects coating and process selection |
| What is the strength/hardness? | Relevant to hydrogen embrittlement risk |
| What coating thickness is required? | Affects corrosion and thread fit |
| What black passivation is specified? | Part of the complete finish |
| Is a topcoat required? | Can affect corrosion and friction |
| Is friction controlled? | Important for torque-controlled assembly |
| What corrosion test applies? | Allows meaningful comparison |
| What are the acceptance criteria? | Test hours alone are incomplete |
| Must the finished thread pass a defined requirement? | Coating buildup can affect fit |
| Is the fastener welded or deformed during installation? | Coating must be process-compatible |
| Is this a second source? | Functional equivalence must be demonstrated |
This transforms a visual finish request into an engineering sourcing specification.
A coating should not be selected only by the cost added to each fastener.
For OEM production:
Total Installed Cost = Fastener Price + Coating + Installation + Inspection + Rework + Scrap + Downtime + Logistics + Supply Risk
A cheaper black finish may create higher total cost if it causes:
Corrosion failure
Thread interference
Tightening variation
Coating damage
Appearance rejection
Rework
Additional inspection
Production interruption
Conversely, specifying high-performance black Zn-Ni where only cosmetic black is required may also increase cost unnecessarily.
The best commercial solution is the one that satisfies the actual functional requirement.
For a technically meaningful quotation, provide:
2D drawing
3D model where relevant
Part number
Drawing revision
Fastener type
Base material
Property class or mechanical requirement
Heat treatment
Thread
Black Zn-Ni specification
Coating thickness
Passivation
Sealer / topcoat
Friction requirement where applicable
Corrosion test
Acceptance criteria
Appearance requirement
Mating material
Installation method
Operating environment
Annual volume
Sample quantity
Validation requirements
Applicable ISO, DIN, EN, ASTM, SAE or OEM specification
If the drawing currently says only "black," provide the functional requirements so the coating can be reviewed correctly.
A practical OEM development path can be:
Application Requirement → Black Finish Requirement → Coating Technology Selection → Drawing Review → Friction / Thread-Fit Review
→ Quotation → Sample → Coating Inspection → Functional / Corrosion Testing → Assembly Validation → Approval → Production
This prevents a cosmetic decision from becoming an uncontrolled engineering variable.
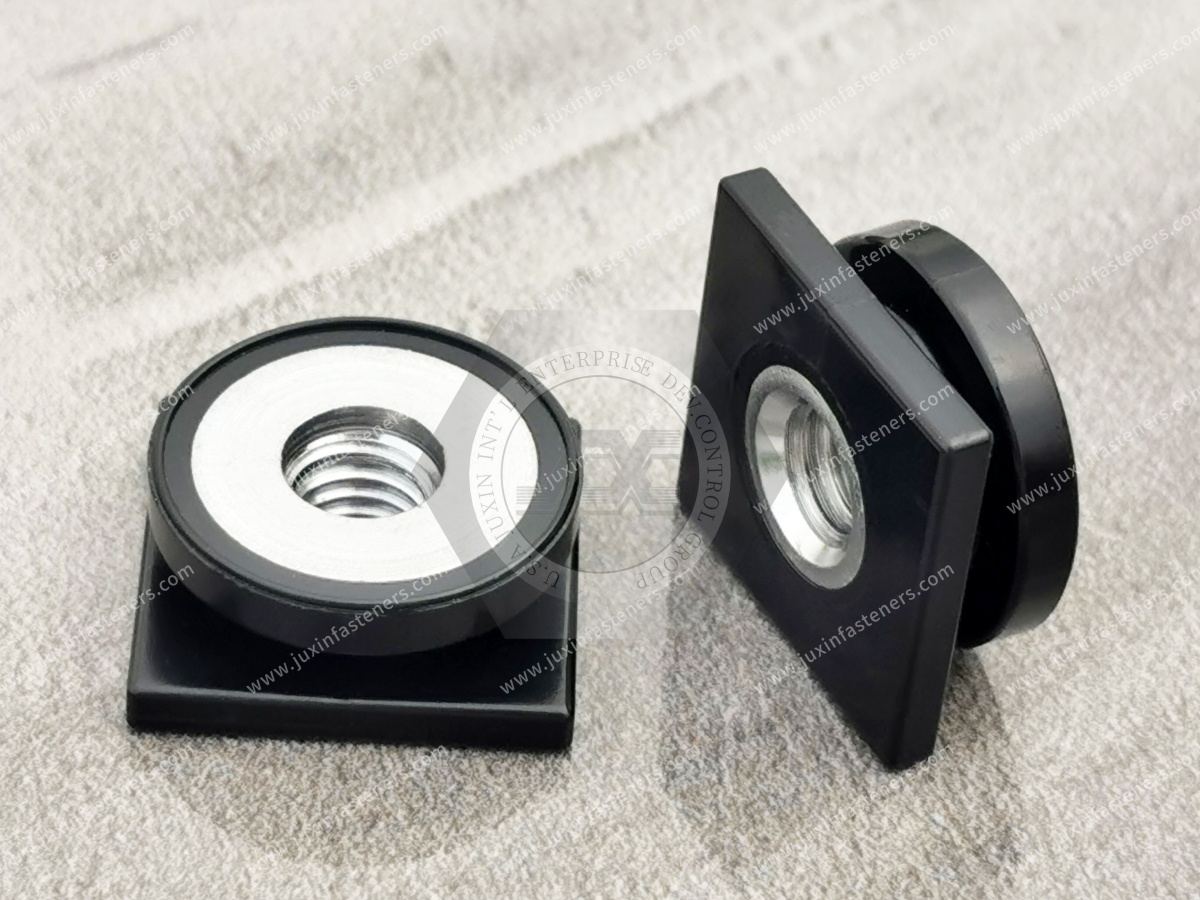
This page should operate as the Black Zinc-Nickel / Black Fastener Finish cluster page rather than duplicate the general Zn-Ni page.
Recommended internal links include:
Fastener Surface Treatment & Coating Selection → overall coating-selection hub
Zinc-Nickel Coated Fasteners → complete Zn-Ni engineering and sourcing guide
Zinc-Plated Fasteners → conventional zinc coating resources
Zinc-Flake Coated Fasteners → non-electrolytic corrosion-protection resources
High-Strength Fasteners → strength, preload and hydrogen embrittlement considerations
Automotive Sheet Metal Fastening → automotive coating and joint engineering
Rivet Nuts → coating and installed-performance considerations
Weld Nuts → coating and welding-process compatibility
Lock Nuts → friction and prevailing-torque engineering
Custom Fastener Manufacturing → material, heat treatment, coating and DFM
Fastener Failure Modes → corrosion, loosening and coating-related failures
Use the existing indexed JUXIN FASTENERS URL when implementing these internal links.
No. Black zinc normally uses a zinc deposit, while black Zn-Ni uses a zinc-nickel alloy deposit.
Their corrosion capability, process controls and cost can differ.
No. Zn-Ni is an electroplated alloy system, while zinc-flake is a non-electrolytic coating technology.
They should not be substituted solely because both can have a black appearance.
Zn-Ni systems can be selected for higher corrosion requirements, but actual performance depends on coating thickness, passivation,
topcoat and test conditions. The complete specification must be compared.
No. Color intensity is not a reliable measure of corrosion performance.
For a purely cosmetic, low-risk application it may sometimes be sufficient to define appearance through the applicable purchasing specification.
For an engineered fastener, the coating technology and functional requirements should normally be defined more clearly.
It can. Passivation, topcoat and lubricant can influence friction. Since torque is not preload, a friction change can change the resulting clamp load.
It may be used on selected high-strength fasteners when the electroplating process and hydrogen embrittlement controls are appropriate for the material and governing specification.
It should not be approved based only on the coating name.
It can be used on selected rivet nuts when the coating remains compatible with thread fit and installation deformation.
The installed component should be evaluated where functional performance is important.
Potentially, but welding compatibility must be reviewed. Surface condition can affect electrical contact and the welding process.
Compare the base fastener, Zn-Ni system, coating thickness, passivation, topcoat, friction, corrosion test, thread fit, process controls and relevant functional performance—not just appearance and price.
For an industrial OEM, a black fastener should be treated as an engineered system:
Fastener Geometry + Material + Mechanical Properties + Heat Treatment + Thread + Black Coating System + Friction + Installation + Environment
The word "black" defines appearance.
It does not automatically define engineering performance.
JUXIN FASTENERS supports selected black zinc-nickel bolts, screws, nuts, lock nuts, rivet nuts and drawing-based fasteners for OEM and industrial sourcing projects.
If you are developing a new black fastener, replacing black zinc with black Zn-Ni, evaluating black zinc-flake, or qualifying a second source, send the available technical package for review.
For an effective RFQ, provide:
2D Drawing + 3D Model + Part / Revision + Fastener Material + Mechanical Requirement + Thread + Required Black Finish + Mating Component + Installation Method + Environment + Annual Volume
Where applicable, also provide:
Coating Technology + Thickness + Passivation + Topcoat + Friction Requirement + Corrosion Test + Acceptance Criteria + Hydrogen Embrittlement Requirements + OEM Specification
This allows engineering and procurement teams to compare the finished fastener by function rather than approving a coating simply because it looks black.
JUXIN FASTENERS
Black Zinc-Nickel Fasteners | Black Zn-Ni Bolts | Black Screws | Black Nuts | Custom Coated Fasteners
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY



