Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809
Industrial automation control panels, electrical switchgear, power distribution cabinets, machinery control enclosures, robotics systems,
and electrical equipment require organized wire routing, reliable component mounting, protected cable interfaces, and efficient assembly.
Product Specification
Industrial automation control panels, electrical switchgear, power distribution cabinets, machinery control enclosures, robotics systems,
and electrical equipment require organized wire routing, reliable component mounting, protected cable interfaces, and efficient assembly.
As control systems become increasingly compact and functionally dense, a single enclosure may integrate programmable logic controllers (PLCs),
variable frequency drives (VFDs), safety relays, power supplies, terminal blocks, communication modules, sensors, control PCBs, power electronics,
cooling components, and extensive combinations of power and signal wiring.
This creates multiple mechanical interfaces where molded plastic hardware can provide practical assembly and routing functions.
Plastic and nylon components may be used to:
route control wiring and cable bundles;
protect conductors passing through sheet metal;
secure harnesses to enclosure walls and sub-panels;
support PCBs and electronic modules;
provide controlled component spacing;
retain lightweight panels and internal components;
close unused enclosure openings;
separate selected components from conductive metal surfaces;
support efficient assembly and maintenance.
However, these components should not be selected simply because they are described as “nylon electrical hardware.”
Control panel plastic hardware should be selected according to its actual mechanical function, mounting interface,
cable or PCB geometry, temperature, vibration, material requirements, serviceability, and applicable electrical equipment design requirements.
Juxin Fasteners supplies standard and custom plastic fastening and cable-management components for industrial automation equipment, control panels,
switchgear, power distribution systems, machinery, robotics, and electrical enclosures.
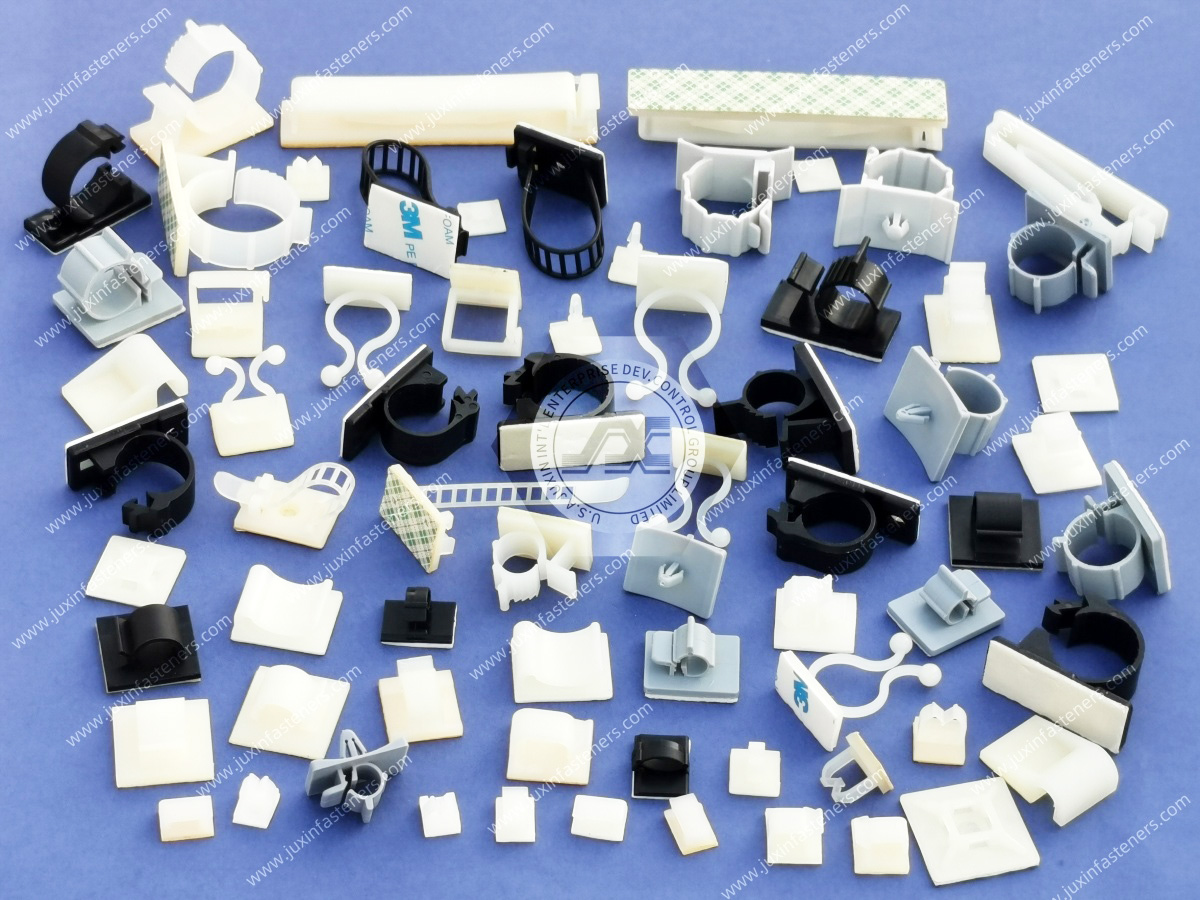
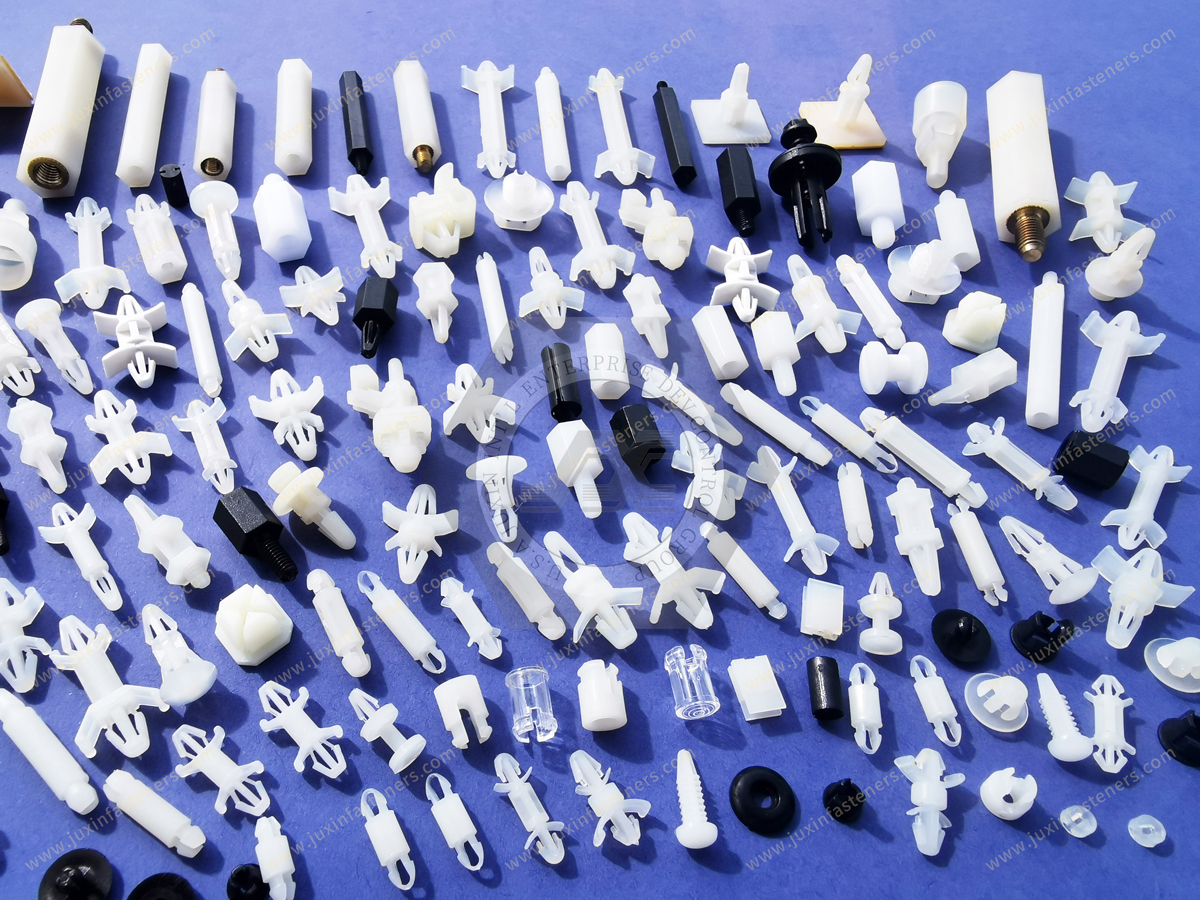
Product families include nylon cable clips, P-clips, adjustable cable clamps, cable tie mounts, nylon snap bushings, strain relief bushings,
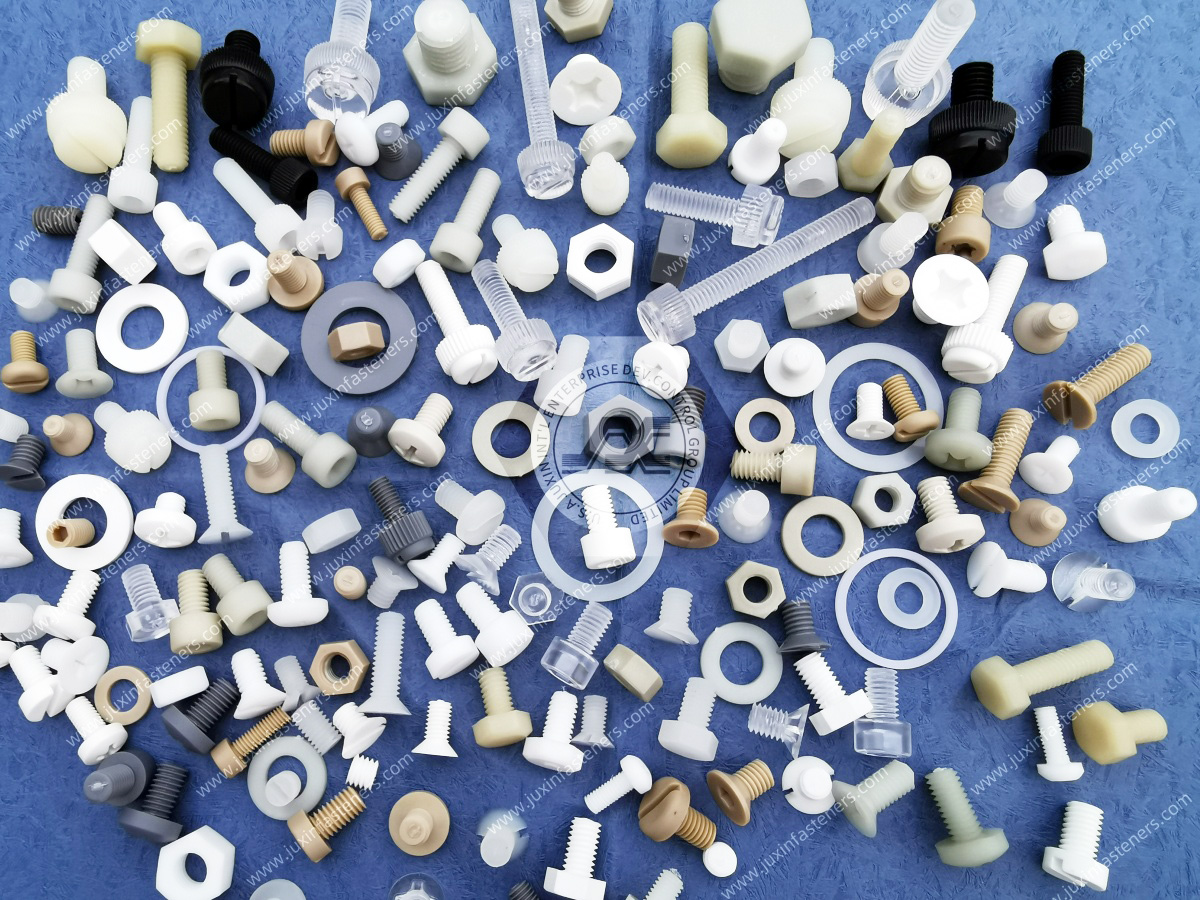
PCB supports, plastic spacers and standoffs, nylon push rivets, panel fasteners, panel hole plugs, nylon screws and nuts, and drawing-based custom molded plastic components.
For OEM sourcing and second-source qualification, technical evaluation can begin from an existing supplier part number, OEM part number,
physical sample, 2D engineering drawing, 3D CAD model, or application specification.
There is no single universal “control panel plastic accessory.”
A cable clip on a swinging cabinet door performs a different function from a snap bushing in a sheet metal cutout, a PCB standoff, or a panel hole plug.
The correct component should therefore be selected according to the application zone and required function.
Control cabinet doors frequently contain:
operator interfaces;
push buttons;
indicator lights;
switches;
displays;
safety devices;
communication equipment.
Wiring between the main enclosure and door-mounted equipment must remain controlled as the door opens and closes.
Depending on the design, cable-management hardware may include:
nylon cable clips;
P-clips;
adjustable cable clamps;
cable tie mounts;
snap-in harness retainers;
custom molded routing components.
The objective is not simply to make the wiring look organized.
Routing should help prevent:
excessive cable sag;
interference with hinges;
mechanical pinch points;
uncontrolled movement;
abrasion against enclosure surfaces;
unnecessary connector loading.
A cable bundle attached to a fixed sub-panel and a cable bundle crossing a moving cabinet-door interface do not experience the same mechanical conditions.
For moving harnesses, engineers should consider:
bend location;
movement envelope;
cable flexibility;
harness mass;
clamp spacing;
attachment points;
repeated movement;
minimum permitted bend radius where applicable.
Maximum clamping force ≠ maximum moving-harness reliability.
A clamp should control the harness without creating an unnecessary stress concentration at the point where the cable repeatedly bends.
Control panels and electrical cabinets frequently use punched, drilled, stamped, or laser-cut openings for wiring.
Where cables pass through sheet metal, engineers may evaluate:
Nylon Snap Bushings for panel-edge protection;
Strain Relief Bushings where cable pull or movement must also be managed;
Closed Grommets for suitable unused openings;
Panel Hole Plugs for redundant panel cutouts.
These products should not be treated as interchangeable.
Edge protection ≠ strain relief ≠ environmental sealing.
A snap bushing can isolate a cable jacket from a sharp metal edge, but that does not automatically mean it provides cable strain relief or a specified enclosure ingress rating.
Industrial cabinets may contain substantial quantities of:
control wiring;
sensor wiring;
communication cables;
power conductors;
fan wiring;
auxiliary harnesses.
Plastic cable-management hardware can provide defined attachment points between wire bundles and the enclosure structure.
Depending on the application, engineers may use:
P-clips;
adjustable cable clamps;
cable tie mounts;
snap-in cable clips;
custom molded harness retainers.
Selection should consider more than nominal bundle diameter.
Important factors include:
cable quantity;
bundle mass;
conductor stiffness;
cable jacket;
vibration;
mounting orientation;
local temperature;
required service access.
Bundle diameter ≠ harness mechanical load.
Two harnesses with the same outside diameter can impose very different loads on a retaining component.
Modern automation equipment increasingly integrates electronic control and communication assemblies.
Plastic PCB supports and standoffs may be used for:
control boards;
communication boards;
monitoring electronics;
interface PCBs;
auxiliary electronic modules.
Potential functions include:
controlled PCB-to-chassis spacing;
local board support;
positioning;
separation from conductive surfaces;
snap-fit assembly in appropriate designs.
Selection should consider:
PCB thickness;
PCB mounting-hole diameter;
chassis hole geometry;
standoff height;
board mass;
connector insertion and extraction forces;
vibration;
service access;
surrounding component geometry.
Higher standoff height ≠ automatically better board support.
Increasing the support height can affect board flexure, vibration, connector alignment, packaging, and mechanical leverage.
Gemini's original concept of using plastic spacers and standoffs to elevate terminal blocks, relays,
and auxiliary mounting hardware can be valid in appropriately designed assemblies, but it should not be generalized.
Many industrial electrical components are designed around dedicated DIN rail or manufacturer-specific mounting systems.
Plastic spacers or standoffs may instead be appropriate where the equipment design specifically requires:
component spacing;
auxiliary support;
PCB mounting;
custom mounting plates;
non-standard internal assemblies.
A plastic standoff should not be used as an improvised replacement for a component's specified mounting system.
Where DIN rail equipment is specified, the manufacturer's intended DIN rail mounting architecture should remain the primary reference.
Cable tie mounts provide defined anchoring positions for wire bundles.
Common mounting concepts can include:
screw-mounted cable tie bases;
snap-in mounts;
adhesive-backed mounts;
application-specific molded anchors.
The mounting method should be selected according to the actual environment.
For example, an adhesive-backed mount may be convenient for some applications, but its long-term performance can depend on:
substrate;
surface preparation;
temperature;
contamination;
adhesive system;
sustained load;
vibration.
Adhesive installation convenience ≠ universal long-term retention.
Where retention is critical, the mounting method should be evaluated under representative conditions.
Nylon push rivets and panel fasteners may be suitable for retaining:
lightweight covers;
internal barriers;
fan guards;
airflow guides;
labels or auxiliary panels;
other low-load components.
Selection should consider:
mounting-hole diameter;
total panel stack thickness;
material thickness;
required retention;
removal requirements;
installation access.
A push rivet selected only by head diameter can easily be mismatched to the actual panel interface.
Standardized control cabinet designs may contain unused holes created for:
optional switches;
alternate cable entries;
accessories;
customer-specific configurations;
future expansion.
Panel hole plugs and closed grommets can provide a clean closure where appropriate.
However:
Closed opening ≠ automatically sealed enclosure.
If an enclosure must achieve a specific environmental ingress rating, the complete closure interface must satisfy the applicable equipment requirements.
Material selection should be based on the actual application rather than simply specifying “plastic” or “nylon.”
PA66 is commonly used in many molded fastening and cable-management components because suitable grades can provide a useful combination of:
mechanical strength;
stiffness;
toughness;
wear resistance;
snap-fit behavior;
molded feature definition.
Applications can include:
cable clips;
snap bushings;
PCB supports;
push rivets;
panel fasteners;
spacers;
cable tie mounts.
However:
PA66 is a material family, not a complete engineering specification.
Actual performance depends on factors such as:
resin grade;
conditioning;
additives;
geometry;
temperature;
mechanical load;
environmental exposure.
Different PA66 components should therefore not automatically be treated as mechanically equivalent.
Polyamides are hygroscopic and absorb moisture from the surrounding environment.
Moisture conditioning can influence:
stiffness;
toughness;
dimensions;
latch flexibility;
insertion behavior;
retention characteristics.
This is relevant for snap-fit cable clips, bushings, push rivets, and PCB supports.
Moisture absorption is not simply an advantage or disadvantage; it changes the mechanical condition of the polymer.
For tight-tolerance snap-fit interfaces, the expected operating environment should be considered during validation.
Control panels may contain heat-generating components such as:
VFDs;
power supplies;
transformers;
contactors;
power electronics;
cooling equipment.
The temperature experienced by a plastic fastener can differ significantly depending on its location within the enclosure.
Therefore:
Cabinet ambient temperature ≠ actual component temperature.
Heat-stabilized resin grades may be considered where appropriate, but there is no single universal service-temperature limit for every heat-stabilized PA66 component.
Suitability depends on the specific resin, load, geometry, exposure duration, moisture, and aging requirements.
Some electrical equipment applications may require defined flammability characteristics.
Where required, flame-retardant polymer grades can be evaluated.
However:
A UL 94 classification associated with a resin does not automatically mean every molded fastener manufactured from that material has an independent finished-component certification.
Flammability requirements should be specified according to the actual project.
The RFQ should identify, where applicable:
required flammability classification;
material grade;
relevant thickness;
color;
required documentation;
customer or equipment-level compliance requirements.
This distinction helps procurement teams avoid treating a resin data-sheet classification as a universal product certification.
Non-metallic fasteners, spacers, and supports can be useful where designers want to avoid a direct conductive mounting path at selected locations.
However:
Plastic hardware ≠ complete electrical insulation system.
Electrical safety and insulation coordination can depend on:
working voltage;
creepage distance;
clearance distance;
dielectric properties;
pollution degree;
material group;
geometry;
environmental conditions;
applicable equipment standards.
A nylon spacer should therefore not be described as automatically creating a compliant creepage or clearance distance.
The electrical design engineer must establish the required insulation architecture at assembly level.
Plastic hardware can then be selected as one component within that design.
Industrial control panels commonly contain circuits with different electrical and functional requirements.
Mechanical cable-management hardware can help maintain organized routing between:
power conductors;
control wiring;
communication cables;
sensor wiring.
However, plastic clips alone do not establish compliant circuit separation.
Required spacing, segregation, shielding, wiring practices, and routing should be determined according to the applicable equipment architecture and electrical design requirements.
Cable organization supports the electrical design; it does not replace it.
Control cabinets attached to machinery may experience vibration generated by:
motors;
pumps;
compressors;
conveyors;
transformers;
machine structures;
mobile or material-handling equipment.
Vibration can affect:
cable clip retention;
harness movement;
snap-fit interfaces;
PCB support;
push rivets;
panel hardware.
A component that remains secure in a stationary cabinet should not automatically be assumed suitable for a vibration-intensive machine.
Where vibration is significant, the actual mounting orientation, mass, geometry, and equipment requirements should be included in validation.
Plastic components subjected to sustained mechanical load can exhibit creep or stress relaxation.
This can be important for:
cable clamps;
continuously deflected snap features;
loaded PCB supports;
panel retainers;
components near elevated-temperature zones.
Therefore:
Initial assembly fit ≠ guaranteed long-term retention.
Long-term mechanical requirements should be considered where a component remains continuously loaded throughout equipment operation.
Control cabinets and machinery can be exposed to:
lubricants;
oils;
cleaning agents;
coolants;
process chemicals;
airborne industrial contaminants.
Polymer compatibility depends on:
specific resin;
chemical;
concentration;
temperature;
exposure duration;
mechanical stress.
Nylon ≠ universal chemical resistance.
Where chemical exposure is relevant, material compatibility should be evaluated against the actual operating environment.
Plastic hardware can also influence manufacturing efficiency.
Snap-in bushings, push rivets, PCB supports, and selected cable retainers can reduce assembly steps in suitable applications.
However, the fastest component to install is not always the best component for the complete product lifecycle.
Engineering teams should consider:
insertion force;
assembly direction;
tool access;
operator ergonomics;
removal;
maintenance;
reusability;
risk of incorrect installation.
Tool-free installation ≠ automatically tool-free removal or repeated reusability.
The intended service strategy should be defined before selecting the retention mechanism.
As panel density increases, plastic hardware should consume as little unnecessary space as possible while maintaining its mechanical function.
Engineers may need to consider:
clip profile;
harness clearance;
bend space;
adjacent terminal blocks;
wire ducts;
PCB spacing;
door clearance;
cooling airflow;
maintenance access.
This means the “smallest fastener” is not automatically the best choice.
A low-profile component that creates poor cable routing or difficult maintenance can increase total assembly complexity.
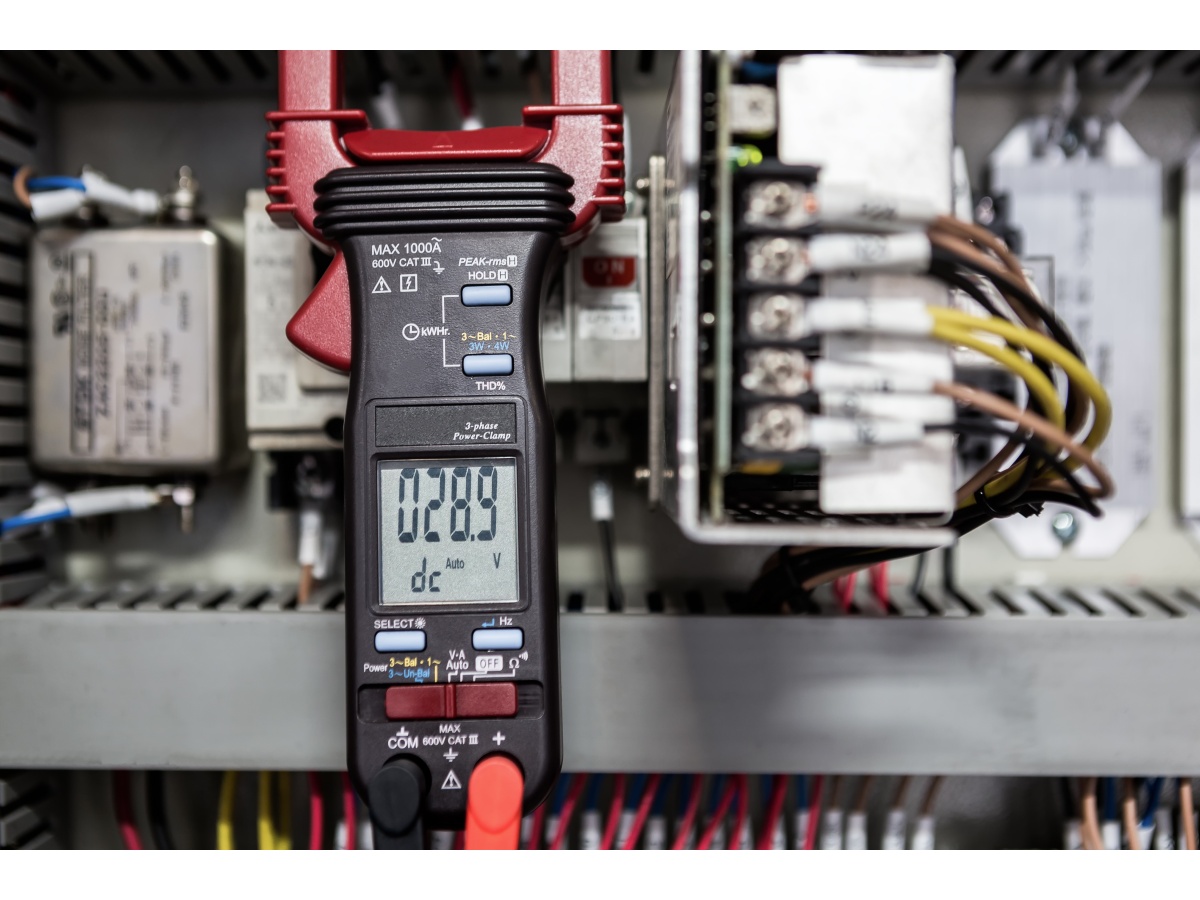
Understanding failure modes helps engineering and sourcing teams qualify components more effectively.
Possible causes include:
unprotected sheet metal edges;
incorrect snap bushing size;
cable movement;
excessive clamp pressure;
unsuitable routing.
Possible causes include:
incorrect cable range;
vibration;
mounting-interface mismatch;
creep;
stress relaxation;
excessive temperature.
Possible causes include:
incorrect bend location;
insufficient movement allowance;
excessive clamp rigidity;
poor anchor positioning;
repeated door movement.
Possible causes include:
oversized panel hole;
incompatible panel thickness;
incomplete snap engagement;
incorrect geometry.
Possible causes include:
incorrect PCB hole diameter;
incorrect chassis hole;
insufficient retention;
connector loads;
vibration;
unsuitable support geometry.
Possible causes include:
incorrect hole diameter;
incorrect panel stack thickness;
excessive insertion stress;
unsuitable material;
environmental aging.
Possible causes can include:
inadequate surface preparation;
unsuitable adhesive system;
contamination;
elevated temperature;
sustained load;
vibration.
Possible contributors include:
creep;
stress relaxation;
thermal aging;
unsuitable resin;
excessive continuous load.
Failure analysis should evaluate the complete component-interface-environment system rather than attributing every problem simply to “plastic quality.”
| Application Requirement | Plastic Hardware to Evaluate |
|---|---|
| Protect wire through sheet metal | Nylon Snap Bushing |
| Manage cable movement at panel entry | Strain Relief Bushing |
| Route fixed wire bundle | Nylon P-Clip / Cable Clip |
| Accommodate variable bundle size | Adjustable Cable Clamp |
| Create cable tie anchoring point | Cable Tie Mount |
| Support control PCB | Snap-Fit PCB Support |
| Provide controlled component spacing | Plastic Spacer / Standoff |
| Retain lightweight internal panel | Nylon Push Rivet / Panel Fastener |
| Close unused cabinet opening | Panel Hole Plug / Closed Grommet |
| Proprietary cabinet interface | Custom Molded Plastic Fastener |
This selection method helps engineering teams specify components according to actual function instead of treating all plastic enclosure hardware as interchangeable.
Typical plastic hardware applications can include:
control wiring retention;
communication cable routing;
PCB support;
cable-entry protection;
unused hole closure;
internal panel retention.
Component selection should reflect cable density, service access, vibration, and thermal conditions.
Plastic hardware may support:
control circuit routing;
auxiliary electronics;
monitoring systems;
cable pass-through protection;
selected internal mounting functions.
Electrical insulation and spacing requirements must be determined at the complete assembly level rather than assigned to the plastic fastener alone.
Robotic systems and automated machinery can create additional requirements for:
vibration resistance;
cable movement;
compact routing;
sensor harnesses;
control wiring;
serviceability.
Dynamic wiring should be distinguished from static cabinet wiring during component selection.
VFDs and power conversion systems can combine:
control electronics;
power circuitry;
cooling hardware;
internal harnesses;
communication wiring.
Local temperature and electrical architecture should be considered when selecting polymer hardware.
HVAC and building automation equipment may use plastic components for:
control PCB mounting;
sensor wiring;
fan wiring;
enclosure cable routing;
panel interfaces.
Temperature, vibration, condensation risk, and service requirements can vary significantly by equipment type.
Electrical cabinets used in conveyor, logistics, warehouse, and material-handling systems may experience continuous equipment vibration.
Cable clips, P-clips, snap bushings, and other retention hardware should therefore be evaluated according to the actual mechanical environment.
Control and power distribution equipment used in data centers can require:
PCB supports;
cable-management components;
enclosure bushings;
panel plugs;
lightweight internal fasteners.
These applications connect naturally with Juxin Fasteners' broader AI Data Center Plastic Fasteners & Cable Management solutions.
Many of the same plastic hardware families are used in:
BESS control cabinets;
inverters;
power conversion equipment;
solar electrical enclosures;
monitoring systems.
Outdoor and renewable-energy environments may introduce additional UV, moisture, thermal-cycling, and environmental requirements.
See our Plastic Fasteners for Solar, BESS & Renewable Energy Systems solution for applications requiring broader environmental evaluation.
Automation OEMs, electrical equipment manufacturers, and panel builders may need alternative sources for existing molded components.
An existing manufacturer part number is useful, but part-number matching alone does not prove interchangeability.
Visual similarity ≠ functional interchangeability.
Depending on the component, second-source comparison should evaluate:
mounting-hole dimensions;
panel thickness;
PCB thickness;
PCB hole diameter;
standoff height;
cable diameter or bundle range;
locking geometry;
retention mechanism;
material;
resin requirements;
flammability requirements;
local temperature;
vibration;
installation method;
removal requirements.
Provide one or more of the following:
existing supplier part number;
OEM part number;
2D engineering drawing;
3D CAD model;
physical sample;
clear photographs.
Depending on the product, confirm:
panel hole diameter;
panel thickness;
PCB thickness;
PCB hole diameter;
cable diameter;
bundle range;
mounting method;
mating component.
Identify whether the component provides:
cable routing;
edge protection;
strain management;
PCB support;
spacing;
panel retention;
hole closure;
another mechanical function.
Specify relevant conditions such as:
temperature;
vibration;
humidity;
chemical exposure;
indoor or outdoor installation;
service and maintenance requirements.
Specify where applicable:
polymer requirement;
flame-retardant requirement;
color;
RoHS documentation;
REACH documentation;
material documentation;
lot traceability;
customer-specific quality requirements.
Evaluate candidate samples in the actual assembly or a representative fixture.
Depending on the product, review:
insertion behavior;
retention;
cable fit;
board fit;
panel fit;
routing geometry;
vibration behavior;
removal and serviceability.
After technical validation, procurement teams can proceed with:
commercial quotation;
production quantities;
packaging;
inspection requirements;
quality documentation;
supply planning.
Standard plastic hardware covers many common control panel applications, but proprietary automation equipment may require dedicated geometries.
Custom molded components may be considered for:
unique enclosure interfaces;
integrated cable-routing features;
proprietary PCB supports;
specialized panel retention;
custom harness clips;
obsolete component replacement;
equipment-specific mounting requirements.
Juxin Fasteners can support drawing-based custom plastic component sourcing through:
2D drawing review;
3D CAD review;
dimensional and interface evaluation;
DFM discussion;
resin selection according to project requirements;
tooling evaluation;
prototype or sample validation;
production sourcing.
See our Custom Molded Plastic Fasteners solutions for non-standard industrial automation applications.
For efficient engineering review and quotation, provide the information relevant to the component.
supplier part number;
OEM part number;
2D drawing;
3D CAD;
physical sample;
product photographs.
cable type;
cable diameter;
bundle range;
cable jacket where relevant;
fixed or moving harness;
mounting method;
routing constraints;
vibration requirements.
panel hole diameter or cutout geometry;
panel thickness;
panel material;
coating or finish;
installation direction.
PCB thickness;
PCB hole diameter;
chassis mounting hole;
required standoff height;
board retention method;
significant connector loads where relevant.
required polymer;
temperature requirement;
humidity;
vibration;
chemical exposure;
flame-retardant requirement;
color;
other material requirements.
sample quantity;
estimated annual volume;
production schedule;
material documentation;
RoHS declaration;
REACH declaration;
lot traceability;
dimensional inspection requirements;
customer-specific documentation.
Providing these details allows the supplier to evaluate the actual mechanical interface and application instead of simply searching for a visually similar component.
A modern control cabinet normally uses several plastic hardware families rather than one universal component.
Related Juxin Fasteners solutions include:
Nylon Cable Clips for organized wire routing;
Nylon P-Clips for fixed harness retention;
Adjustable Cable Clamps for variable bundle sizes;
Cable Tie Mounts for structured harness anchoring;
Nylon Snap Bushings for sheet metal cable-edge protection;
Strain Relief Bushings for cable-entry retention;
Snap-Fit PCB Supports for electronic board mounting;
Plastic Spacers and Standoffs for controlled component spacing;
Nylon Push Rivets for lightweight panel retention;
Panel Hole Plugs and Closed Grommets for unused enclosure openings;
Custom Molded Plastic Fasteners for proprietary automation equipment interfaces.
These components should be selected according to their actual mechanical function, mating interface, material requirements,
and operating environment rather than simply because they are molded from plastic.
Juxin Fasteners supports industrial automation OEMs, electrical equipment manufacturers, control panel builders,
switchgear manufacturers, machinery manufacturers, robotics companies, contract manufacturers, engineering teams, procurement departments, and supplier-development programs requiring standard or custom plastic fastening components.
For industrial automation and control panel projects, the sourcing path can begin with:
Existing Part Number / Drawing / Sample → Application & Interface Review → Material & Environment Review
→ Candidate Component → Sample Validation → Second-Source Qualification → Production RFQ
This process can support:
new control panel development;
industrial automation equipment;
switchgear and power distribution equipment;
robotics and machinery;
power electronics;
HVAC control equipment;
data center power infrastructure;
second-source qualification;
obsolete component replacement;
supplier consolidation;
custom molded component sourcing.
Send us your existing supplier part number, OEM part number, drawing, CAD model, physical sample, cable or PCB information,
panel dimensions, material requirements, operating environment, documentation requirements, and expected annual volume for technical review.
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Product Packaging
Packaging Standard
At Juxin Fasteners, we apply standardized export packaging to ensure product protection, traceability, and compliance with international logistics requirements.
1. Standard Export Packaging
Unless otherwise specified, all products will be packed according to our factory standard export packaging, which includes:
Moisture-resistant inner protection
Poly bag or small box packing as required
Reinforced export cartons
Clear labeling with part number, specification, batch number, and quantity
Palletizing for sea or air shipment when necessary
Our standard packaging is designed to ensure safe transportation, efficient warehousing, and long-distance international shipping.
2. Customized Packaging Options
We also provide customized packaging solutions according to customer requirements, including but not limited to:
Private labeling
Customized barcodes
Specific carton dimensions
Retail packaging
Special pallet configuration
Customer-specific marking and identification
So that you know, customized packaging may involve additional costs and extended lead time depending on the complexity of the requirements.
3. Compliance & Quality Assurance
All packaging processes are controlled under our ISO 9001 quality management system to ensure consistency, traceability, and product integrity throughout the supply chain.
Product Pictures
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY