
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Oct. 16, 2023
External retaining rings for shafts, commonly called external circlips, shaft circlips, shaft retaining rings or external snap rings,
are compact mechanical fasteners used to axially retain components mounted on shafts.
They are installed into a machined groove around the outside diameter of a shaft. Once correctly seated,
the retaining ring creates a mechanical shoulder that helps prevent bearings, gears, bushings, pulleys, rollers, sleeves and other shaft-mounted components from moving beyond their intended axial position.
Standard external circlips are widely associated with DIN 471 dimensional architecture, while other international, customer-specific and drawing-based retaining ring designs are also used across industrial equipment.
Unlike the description sometimes applied to older retaining-ring literature, a conventional external shaft retaining ring does not work through "elastic claws" continuously gripping the shaft.
Its primary retaining function comes from engagement between the ring, the machined shaft groove and the retained component.
A useful engineering model is therefore:
Retained Component → External Retaining Ring → Shaft Groove → Shaft
Understanding this load path is essential for reliable selection.
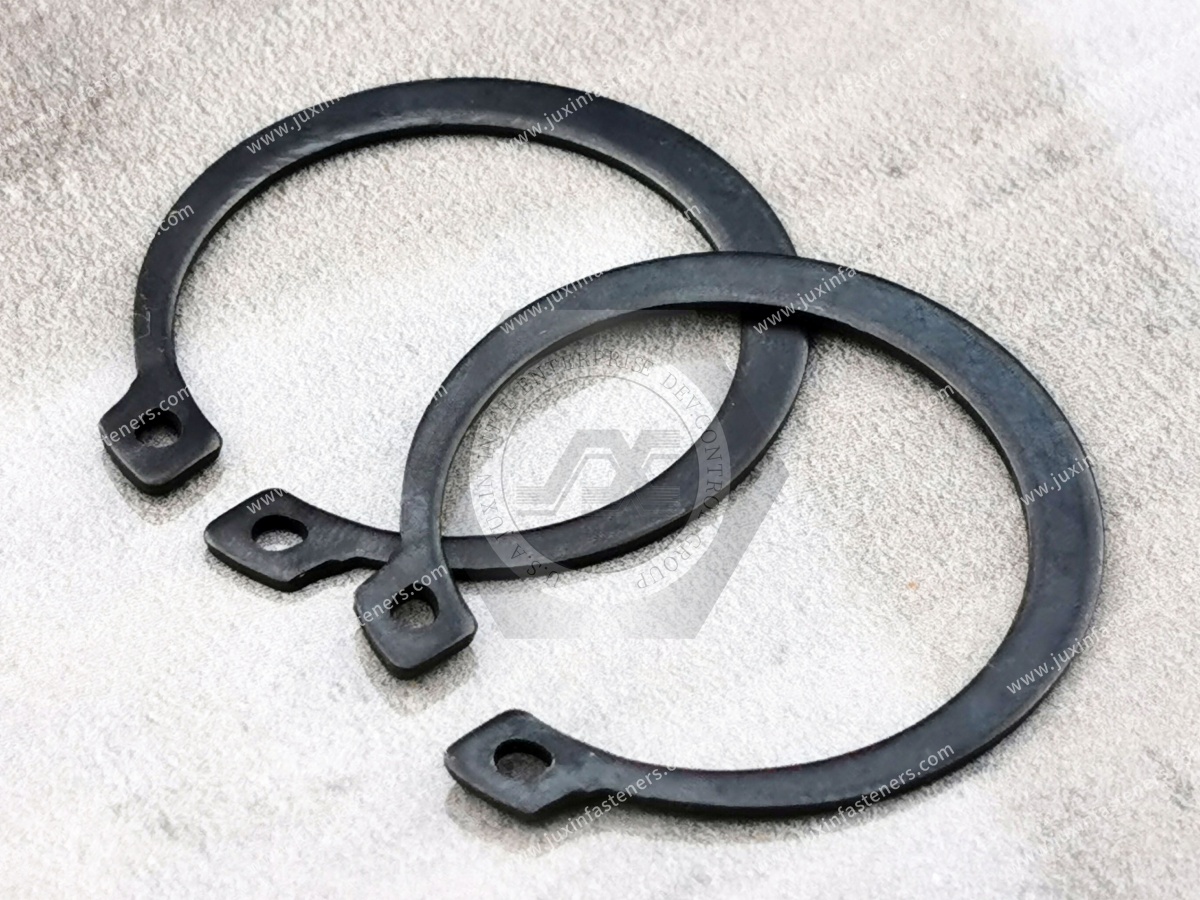
An external retaining ring is an elastic ring designed to fit into a circumferential groove machined around a shaft.
In its free state, the ring's internal geometry is smaller than the installation path required to pass over the shaft.
During installation, appropriate external circlip pliers or production tooling expand the ring sufficiently to pass over the shaft and reach the groove.
When the installation force is released, the ring contracts toward its free condition and seats in the groove.
The portion of the ring projecting beyond the groove then creates an axial stop for the adjacent component.
This provides a compact alternative to retention methods such as:
Threaded shaft ends
Lock nuts
End plates
Retaining screws
Cotter-pin arrangements
Machined shoulders combined with additional threaded hardware
The correct solution depends on load, shaft geometry, available space, assembly sequence and service requirements.
DIN 471 is widely associated with retaining rings for shafts.
A DIN 471-style external circlip is designed for installation into a corresponding shaft groove.
Standardized retaining rings can provide important advantages for OEM engineering and purchasing teams:
Established dimensional architecture
Standard nominal sizes
Defined groove relationships
Easier component identification
Easier sourcing
Reduced custom tooling requirements
Simplified maintenance replacement
Improved second-source opportunities
However, engineers and buyers should not assume that every shaft retaining ring is automatically DIN 471.
Existing equipment may contain:
Modified standard rings
Heavy-section retaining rings
Reduced-lug designs
Custom thicknesses
Special materials
Special coatings
Non-standard shaft grooves
Drawing-specific retaining rings
The applicable standard or approved drawing should therefore be confirmed before quotation or replacement.
External and internal retaining rings have similar axial-retention purposes but use opposite installation architectures.
An external retaining ring fits into a groove on the outside of a shaft.
It is normally expanded during installation.
Typical function:
Retain a component on a shaft.
An internal retaining ring fits into a groove inside a bore or housing.
It is normally compressed during installation.
Typical function:
Retain a component inside a housing.
DIN 471 is commonly associated with external shaft retaining rings, while DIN 472 is commonly associated with internal bore retaining rings.
For bore-mounted assemblies, see our engineering guide to Internal Retaining Rings for Bores and our dedicated DIN 472 Retaining Rings for Bores resource.
External circlips and E-clips can both provide axial retention on shafts, but their installation architecture is different.
A conventional external circlip generally requires access from the end of the shaft.
The ring is expanded over the shaft and then released into the groove.
An E-type retaining ring is typically installed radially from the side of the shaft.
This can be useful when:
Shaft-end access is restricted
Fast radial assembly is preferred
The assembly architecture is designed specifically for an E-clip
The two products should not automatically be treated as interchangeable.
Groove geometry, load capability, installation method and available space must be evaluated separately.
For radial-installation applications, see our E-Type Retaining Rings for Shafts guide.
A retaining ring is small, but the complete load path is structural.
When a shaft-mounted component applies axial force against the ring, the load is transferred approximately through:
Component Face → Retaining Ring → Groove Shoulder → Shaft
This means retention capability does not depend only on the strength of the ring.
The complete system can be influenced by:
Ring geometry
Ring material
Ring hardness
Groove diameter
Groove width
Groove depth
Groove edge geometry
Shaft material
Shaft hardness
Shaft diameter
Component contact geometry
Axial load
Shock loading
Cyclic loading
Installation condition
This leads to an important engineering principle:
The strongest retaining ring does not automatically create the strongest retaining system.
If the groove shoulder or shaft material becomes the limiting feature, simply increasing ring strength may not solve the problem.
The shaft groove is one of the most important parts of the retaining system.
Key groove parameters include:
Groove diameter
Groove width
Groove depth
Groove position
Groove tolerance
Edge condition
Surface condition
Distance from the shaft end
Incorrect groove geometry can create problems even when the retaining ring itself is manufactured correctly.
Possible consequences include:
Incomplete seating
Excessive axial movement
Difficult installation
Ring deformation
Groove-edge deformation
Reduced load capacity
Unexpected disengagement
Difficult service removal
For OEM sourcing, groove dimensions should therefore be included with the retaining-ring drawing whenever possible.
The groove must allow the retaining ring to seat correctly while maintaining sufficient engagement with the shaft.
If the groove geometry is incorrect, the ring may:
Sit too high
Sit too deeply
Fail to seat completely
Contact the retained component incorrectly
Experience unfavorable load distribution
Standard parts should use the corresponding groove dimensions defined by the applicable standard or approved engineering specification.
For custom rings, the ring and groove should be developed as a matched system.
Ring thickness and groove width are related but should not be treated as identical dimensions.
The groove must provide appropriate space for the retaining ring while allowing the completed assembly to meet its axial-clearance requirements.
The relationship can be affected by:
Ring thickness tolerance
Groove-width tolerance
Groove-position tolerance
Component-width tolerance
Surface coating
Manufacturing variation
This is particularly important when developing replacement retaining rings for existing equipment.
A replacement ring that appears dimensionally similar may still produce unacceptable axial clearance if the complete tolerance stack is not considered.
Installing a retaining ring does not automatically eliminate axial movement.
Final axial clearance may depend on:
Shaft Shoulder + Component Width + Groove Position + Groove Width + Ring Thickness + Spacer / Shim + Adjacent Components
This matters for assemblies containing:
Bearings
Gears
Rollers
Pulleys
Bushings
Mechanical cartridges
Precision positioning components
If preload or tightly controlled endplay is required, the retaining ring may need to work with additional components.
The groove shoulder transfers load from the retaining ring into the shaft.
Therefore, engineers should consider:
Shaft material
Shaft hardness
Groove geometry
Groove-to-end distance
Component load
Contact geometry
Shock conditions
Cyclic loading
A ring may remain intact while the groove shoulder deforms.
When this happens, the root cause is not necessarily insufficient retaining-ring strength.
This distinction is important when investigating field failures.
A groove positioned close to the end of a shaft may leave limited supporting material behind the groove.
Depending on the application, this can affect the strength of the retaining architecture.
Engineers should therefore evaluate the relationship between:
Groove location
Shaft-end distance
Shaft material
Groove geometry
Axial load
Component geometry
The applicable standard, validated engineering calculation or application-specific testing should govern critical designs.
Material selection should reflect both mechanical requirements and operating environment.
Spring steels are widely used for external retaining rings because they can provide:
High strength
Elastic recovery
Wear resistance
Fatigue performance
Manufacturing efficiency
Actual performance depends on the complete material and manufacturing route, including:
Steel grade
Forming
Heat treatment
Hardness
Surface condition
Final inspection
A generic material name alone should not be used to guarantee performance.
Stainless retaining rings may be selected for environments requiring improved corrosion resistance.
Potential applications include:
Food-service equipment
Medical equipment
Laboratory equipment
HVAC systems
Pumps
Outdoor equipment
Telecommunications equipment
Semiconductor equipment
Processing machinery
The specific stainless grade should be selected according to actual environmental exposure.
"Stainless steel" should not be interpreted as universally corrosion-proof.
Special materials may be required for:
Elevated temperatures
Aggressive chemicals
Special magnetic requirements
Special fatigue requirements
Customer-specific material specifications
These projects should normally be reviewed from the drawing and application conditions rather than treated as ordinary catalog substitutions.
External retaining rings made from carbon or alloy spring steel may use surface treatments such as:
Phosphate and oil
Black finishes
Zinc-based coatings
Zinc-nickel coatings
Zinc-flake coating systems
Other engineered finishes
The correct finish depends on:
Corrosion requirement
Base material
Hardness
Environmental exposure
Coating thickness
Dimensional tolerance
Installation behavior
Customer specifications
Restricted-substance requirements
For high-strength spring components, coating-process selection should also consider the relevant risk of hydrogen embrittlement.
Retaining rings operate in controlled groove geometry.
Changing from one coating system to another may alter finished dimensions and friction behavior.
Potential effects include:
Effective ring thickness
Groove clearance
Installation force
Seating behavior
Removal force
Corrosion performance
This becomes particularly important when an OEM is qualifying a second source for an existing assembly.
A supplier should not assume that changing the coating is purely cosmetic.
A structured engineering process helps avoid incorrect part selection.
Determine the nominal shaft size and whether the assembly follows a standardized retaining-ring architecture.
What is being retained?
Examples include:
Bearing
Gear
Pulley
Bushing
Roller
Sleeve
Sprocket
Mechanical cartridge
Linkage component
Consider:
Load magnitude
Load direction
Static loading
Cyclic loading
Reversing loads
Shock loads
Verify:
Groove diameter
Groove width
Groove depth
Groove location
Groove tolerance
Consider:
Material
Hardness
Shaft geometry
Groove-to-end distance
Evaluate the complete assembly tolerance stack.
Can the retaining ring be installed from the end of the shaft?
If not, an E-clip or another retaining architecture may be more suitable.
Evaluate:
Corrosion
Temperature
Humidity
Chemical exposure
Service environment
Customer requirements
Critical, high-load or high-cycle applications may require prototype assembly and functional validation.
External circlips are normally expanded during installation.
A typical procedure is:
Confirm the correct retaining-ring specification.
Inspect the ring for distortion or damage.
Inspect and clean the shaft groove.
Use suitable external circlip pliers or controlled installation tooling.
Expand the ring only enough to pass over the shaft.
Move the ring into alignment with the groove.
Release the ring carefully.
Confirm complete seating around the groove.
Inspect the final assembly.
High-volume production may use dedicated installation tooling rather than manual pliers.
One of the most important installation risks for external retaining rings is excessive expansion.
The ring must expand to pass over the shaft, but it should not be opened farther than necessary.
Excessive spreading can cause:
Permanent deformation
Increased free diameter
Reduced groove engagement
Distorted geometry
Uneven seating
Reduced retaining performance
This is particularly important in automated assembly.
Installation tooling should control ring expansion rather than relying on uncontrolled operator force.
External circlips generally need shaft-end access for installation.
This means retaining-ring selection should occur during assembly design rather than after the shaft geometry has been finalized.
Engineers should ask:
Can installation tooling reach the ring?
Can the ring pass over all preceding shaft features?
Is there enough space for circlip pliers?
Will the component sequence block installation?
Will maintenance personnel be able to remove the ring later?
A ring that fits dimensionally but cannot be assembled efficiently is not a successful design.
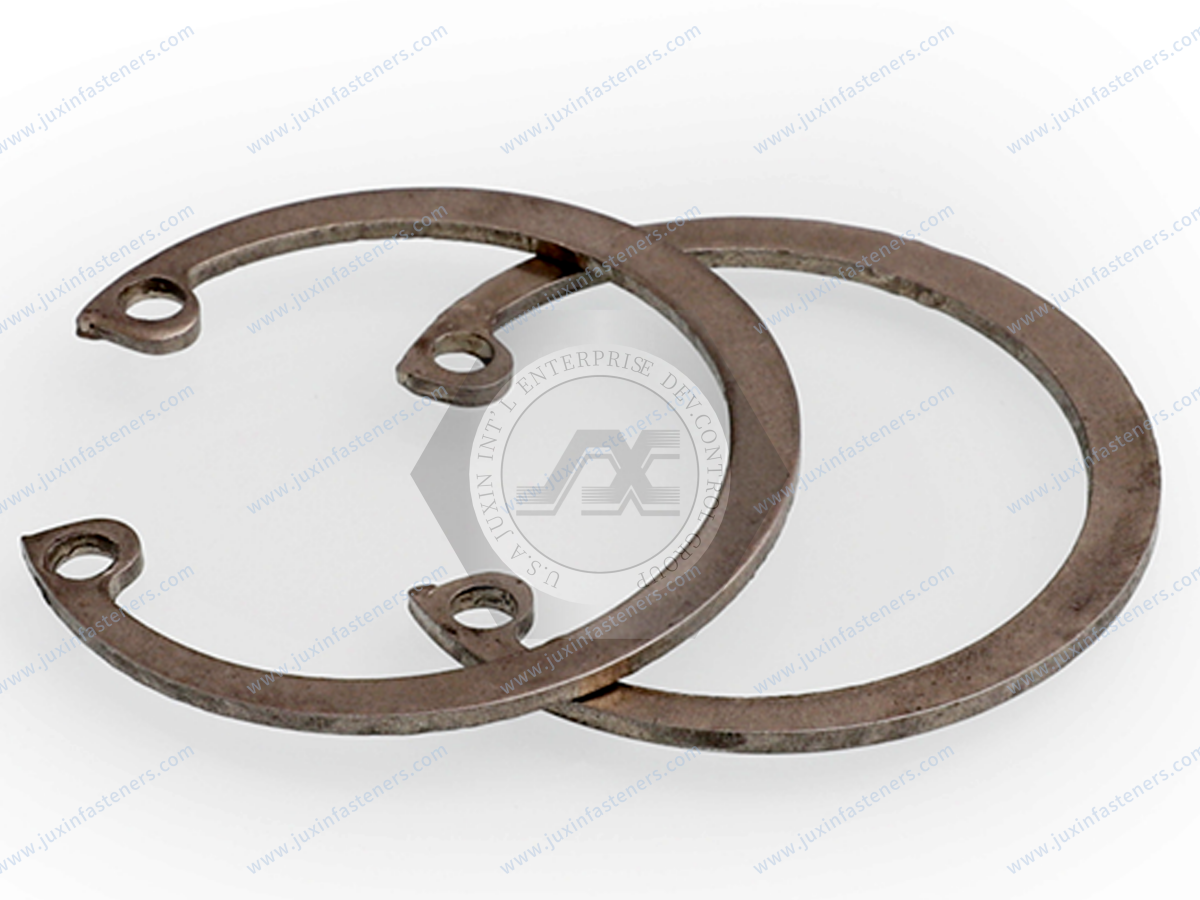
Stamped retaining rings can have edge characteristics resulting from the stamping process.
Depending on the ring design, load direction and application, orientation may affect how the ring contacts the groove and retained component.
Rather than applying one universal rule to every retaining ring, engineers should follow:
Applicable standard
Approved drawing
Supplier technical data
Validated assembly requirement
This is particularly important in high-load or safety-relevant applications.
Reuse should not be assumed automatically.
Removal and reinstallation can affect:
Free diameter
Ring geometry
Elastic recovery
Lug condition
Surface coating
Installation damage
For maintenance applications, the equipment specification should determine whether reuse is acceptable.
For critical production assemblies, replacing a removed retaining ring may be preferable when required by the engineering or maintenance specification.
A failed retaining system should be investigated as an assembly rather than blaming the ring immediately.
The ring may not match the shaft or groove architecture.
Improper groove width, depth or diameter can reduce engagement.
The ring may not be fully engaged around the circumference.
Excessive expansion can permanently deform the ring.
The shaft material or groove geometry may be insufficient for the applied load.
The operating load may exceed the capability of the complete ring-and-groove system.
Corrosion can damage the ring or groove interface.
Improper mechanical properties may reduce elastic recovery or durability.
Unexpected axial movement may originate from the complete assembly rather than the retaining ring itself.
Bearing retention is one of the most common applications for shaft circlips.
An external retaining ring can act as an axial stop for a bearing inner ring mounted on a shaft.
Typical applications include:
Electric motors
Pumps
Gearboxes
Rollers
Actuators
Power transmission equipment
Industrial machinery
However, the complete bearing arrangement should be reviewed.
Important factors include:
Bearing inner-ring geometry
Bearing chamfer
Shaft shoulder
Groove position
Ring contact
Axial clearance
Operating load
For a more focused discussion, review our Bearing Retaining Rings: Shaft & Bore Circlips for Axial Bearing Retention resource.
Shaft retaining rings may also be used to position gears, sprockets and related transmission components.
Potential applications include:
Gearboxes
Reduction drives
Conveyor systems
Automated equipment
Small transmission assemblies
Mechanical actuators
The retaining ring provides axial positioning; torque transmission should be provided by the appropriate shaft-to-component interface.
A retaining ring should not automatically be assumed to transmit drive torque.
External retaining rings may be used in suitable automotive and electrification-related assemblies including:
Electric motors
Pumps
Actuators
Transmission mechanisms
Seat mechanisms
Steering-related mechanisms
Thermal-management equipment
Auxiliary mechanical systems
Manufacturing equipment
The correct retaining ring depends on the actual assembly rather than the vehicle application name alone.
Engineering teams should evaluate load, shaft geometry, environment, material and customer-specific requirements.
External circlips are widely applicable to:
Gearboxes
Motors
Pumps
Reducers
Conveyors
Rollers
Machine tools
Packaging machinery
Processing equipment
Material-handling systems
Their compact axial footprint can help reduce component count and simplify assembly where a grooved-shaft design is appropriate.
Potential applications include:
Robotic joints
Gear mechanisms
Grippers
Actuators
Rollers
Positioning systems
Automated assembly equipment
Material-handling equipment
High-cycle applications may require additional evaluation of fatigue, wear, groove integrity and production consistency.
External retaining rings may be used in appropriate mechanical subassemblies within:
Door mechanisms
Actuators
Seat systems
Auxiliary equipment
Mechanical controls
Maintenance equipment
Rail projects may impose project-specific requirements for:
Material
Coating
Fatigue
Documentation
Traceability
Inspection
These requirements should be defined in the RFQ rather than assumed from the end-use industry.
Potential shaft-retention applications include:
Fans
Blowers
Motors
Pumps
Compressors
Valve actuators
Cooling equipment
Material and coating selection may be influenced by humidity, condensation, outdoor exposure and chemical environments.
Modern data centers depend increasingly on high-capacity cooling and liquid thermal-management systems.
External retaining rings may be used inside mechanical subassemblies such as:
Pumps
Motors
Fans
Blowers
Valve actuators
Cooling distribution equipment
Liquid-cooling systems
The data-center application itself does not define the retaining ring specification.
Selection should be based on the actual mechanical assembly.
External retaining rings can be used in mechanical systems within:
Electric motors
Generators
Cooling equipment
Actuators
Fans
Auxiliary drives
Electrical cabinet mechanisms
Where electrical equipment operates outdoors or in humid environments, corrosion protection should be considered during material and finish selection.
Potential applications include:
Cooling fans
Motors
Antenna adjustment mechanisms
Actuators
Outdoor communication equipment
Mechanical drive systems
Outdoor telecommunications equipment may require enhanced corrosion resistance depending on the actual exposure environment.
Precision machinery used in semiconductor production may contain external retaining rings in:
Motors
Pumps
Rollers
Actuators
Robotic mechanisms
Positioning systems
Automated handling equipment
If special cleanliness, vacuum compatibility or process restrictions apply, they should be specified separately.
A standard retaining ring should not automatically be represented as cleanroom- or semiconductor-qualified.
External retaining rings may be used in suitable mechanical assemblies such as:
Commercial mixers
Refrigeration equipment
Food-processing machinery
Conveyors
Pumps
Motors
Dispensing equipment
Material selection may need to account for:
Humidity
Cleaning chemicals
Washdown conditions
Corrosion exposure
Use in food-service equipment does not automatically mean that the component is approved for direct food contact.
Potential non-implant applications include:
Diagnostic equipment
Laboratory automation
Pumps
Motors
Actuators
Positioning equipment
Sample-handling systems
Medical or laboratory applications may require project-specific controls for material, cleanliness, traceability and documentation.
These should be clearly identified during sourcing.
External retaining rings can be used in suitable:
Hydraulic systems
Actuators
Pivot assemblies
Mechanical linkages
Construction machinery
Agricultural equipment
Heavy shock or high axial loading requires evaluation of the complete shaft, groove and ring system.
Compact shaft retaining rings may also be used in:
Small motors
Measuring equipment
Printers
Office equipment
Cooling fans
Electronic appliances
Mechanical indicators
Adjustment mechanisms
Miniature applications can be especially sensitive to dimensional variation because relatively small changes may affect groove engagement and installation behavior.
Standard retaining rings should generally be considered first when the assembly architecture allows them.
Advantages include:
Easier sourcing
Lower development complexity
Standard groove relationships
Easier maintenance replacement
Better second-source flexibility
Reduced tooling requirements
However, custom external retaining rings may be required for:
Non-standard shaft diameter
Existing legacy groove
Special thickness
Restricted installation envelope
Modified lug geometry
Special material
Special surface finish
Special axial-load requirement
Customer-specific drawing
A sourcing program should therefore distinguish among:
Standard DIN 471 Retaining Ring
Standard-Based Modified Ring
Drawing-Based Replacement Ring
Functional Equivalent
Fully Custom External Retaining Ring
OEM second-source projects sometimes begin with an existing sample rather than a complete drawing.
A practical development route is:
Sample → Dimensional Inspection → Shaft & Groove Review → Material / Finish Evaluation → Drawing Confirmation → Prototype → Assembly Validation → Pilot Production → Production
However, reverse engineering from a sample has limitations.
A sample alone may not reveal:
Original material specification
Heat-treatment requirement
Hardness requirement
Original coating specification
Design axial load
Fatigue requirement
Environmental requirement
Original dimensional standard
Whenever possible, provide application information together with the sample.
Design and mechanical engineers may search for:
External retaining ring
External circlip
Shaft retaining ring
Shaft circlip
External snap ring
DIN 471 retaining ring
Retaining ring for shaft
External circlip groove dimensions
Bearing shaft retaining ring
Circlip for gear shaft
How to retain a bearing on a shaft
External circlip vs E-clip
Their underlying question is usually:
How can I reliably prevent this component from moving axially on the shaft without adding unnecessary assembly complexity?
A useful engineering page should answer that question rather than simply listing dimensions.
Purchasing and supplier-development teams may search for:
External retaining ring manufacturer
Shaft circlip supplier
DIN 471 retaining ring supplier
Stainless steel circlip manufacturer
Spring steel retaining ring supplier
Custom external snap ring
OEM retaining ring manufacturer
Retaining ring second source
Custom circlip from drawing
Their underlying question is different:
Can this supplier consistently manufacture the required geometry, material, heat treatment, surface finish and production quantity for our assembly?
A strong B2B retaining-ring resource should therefore support both engineering selection and supplier qualification.
For faster technical review and quotation, provide as much of the following information as possible.
Applicable standard
Customer drawing
Existing part number
Physical sample
Nominal shaft diameter
Groove diameter
Groove width
Groove depth
Groove position
Dimensional tolerances
Shaft material
Hardness where relevant
Shaft diameter
Groove-to-end distance
Adjacent shaft geometry
Component type
Component dimensions
Contact geometry
Required axial position
Acceptable axial clearance
Axial load
Static or cyclic load
Shock
Vibration
Rotational speed where relevant
Required service life
Retaining-ring material
Hardness requirement
Surface treatment
Corrosion requirement
Restricted-substance requirements
Temperature
Humidity
Outdoor exposure
Chemical exposure
Cleaning agents
Other corrosive conditions
Prototype quantity
Pilot quantity
Production quantity
Estimated annual volume
Packaging
Traceability
Required delivery schedule
Providing this information converts a generic part inquiry into an engineering RFQ that can be evaluated much more effectively.
For OEM, Tier-1 and Tier-2 supply chains, supplier evaluation may include more than unit price.
Depending on the project, relevant manufacturing and quality controls can include:
Drawing interpretation
Material control
Forming-process control
Heat-treatment control
Hardness verification
Dimensional inspection
Surface-treatment control
Prototype development
Production consistency
Lot identification
Packaging control
Engineering-change management
Long-term supply continuity
For replacement and second-source projects, fit and functional validation against the actual shaft groove is especially important.
A practical decision sequence is:
What component must be retained?
→ Is the component mounted on a shaft or inside a bore?
→ What is the shaft diameter?
→ Can a standard DIN 471-type external retaining ring be used?
→ What axial load reaches the ring?
→ What shaft material supports the groove?
→ What groove geometry is available?
→ Is the groove sufficiently supported?
→ What axial clearance is acceptable?
→ Is shaft-end installation access available?
→ Would an E-clip or another retention method be more suitable?
→ What corrosion and temperature conditions exist?
→ What material and surface finish are required?
→ Will the ring require service removal?
→ Is a standard, modified or custom retaining ring required?
This decision process is more reliable than selecting a retaining ring from shaft diameter alone.
For an overview of retaining-ring families, selection logic and groove considerations, review Elastic Retaining Rings & Circlips: Types, Selection, Groove Design and Industrial Applications.
For comparison between shaft and bore retention, see Retaining Rings for Shafts and Bores.
For bore-mounted components, review Internal Retaining Rings for Bores: Selection, Groove Design & Industrial Applications.
For standardized internal circlips, see DIN 472 Retaining Rings for Bores.
For bearing-specific retention, review Bearing Retaining Rings: Shaft & Bore Circlips for Axial Bearing Retention.
For radial shaft installation, see E-Type Retaining Rings for Shafts.
For drawing-based components and non-standard dimensions, review Custom Retaining Rings & Spring Fasteners.
JUXIN FASTENERS supports external retaining rings, shaft circlips, DIN 471-type retaining rings, E-clips and custom spring-fastener sourcing for industrial OEMs,
engineering teams, purchasing organizations and supplier-development programs.
Projects can be evaluated from:
International standard
Customer drawing
Existing sample
Shaft dimensions
Groove dimensions
Retained component
Material specification
Surface finish
Application conditions
Production quantity
Depending on the application, the sourcing route may involve:
Standard External Circlip → DIN 471-Type Retaining Ring → Standard-Based Modified Ring → Drawing-Based Replacement → Custom Shaft Retaining Ring
A reliable retaining-ring sourcing process begins with the assembly rather than the product name:
Retained Component → Shaft → Groove → Axial Load → Shaft Material → Tolerance Stack → Retaining Ring → Material → Surface Finish → Installation → Validation → Production
This changes a generic purchasing inquiry such as:
"Please quote an external circlip."
into a useful engineering RFQ:
"Please evaluate an external retaining ring for this shaft diameter, groove geometry, retained component, axial load, material, environment and annual production requirement."
For external retaining rings, shaft circlips, external snap rings, DIN 471-type retaining rings, stainless steel circlips, spring steel retaining rings,
E-clips, drawing-based replacement rings, custom retaining rings or OEM second-source development, send your drawing, sample, shaft dimensions,
groove dimensions, material, surface finish, application requirements and quantity to:
JUXIN FASTENERS can review the available technical information and evaluate an appropriate standard, manufacturing, sampling and production path for your project.
 MORE NEWS

Sep. 27, 2026

Sep. 27, 2026

Sep. 27, 2026
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY