
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Jun. 13, 2024
Automotive Bolt Loosening Prevention: Vibration, Locking Nuts and Chassis Joint Design
Automotive chassis fasteners operate in mechanical assemblies exposed to repeated road loading, vibration, temperature changes and environmental corrosion.
Maintaining joint reliability requires more than specifying a high-strength bolt or increasing tightening torque.
A properly designed automotive bolted joint must maintain the intended mechanical connection throughout its specified service conditions.
One of the most important engineering distinctions is the difference between rotational self-loosening and loss of bolt preload without rotation.
These failure mechanisms can produce similar symptoms, but they may require different corrective actions.
A prevailing-torque nut may help resist fastener rotation, yet it cannot prevent every form of clamp-load loss caused by material settling or joint relaxation.
Similarly, a property class 10.9 flange bolt may provide the required mechanical strength but still loosen if the assembled joint permits sufficient transverse movement.
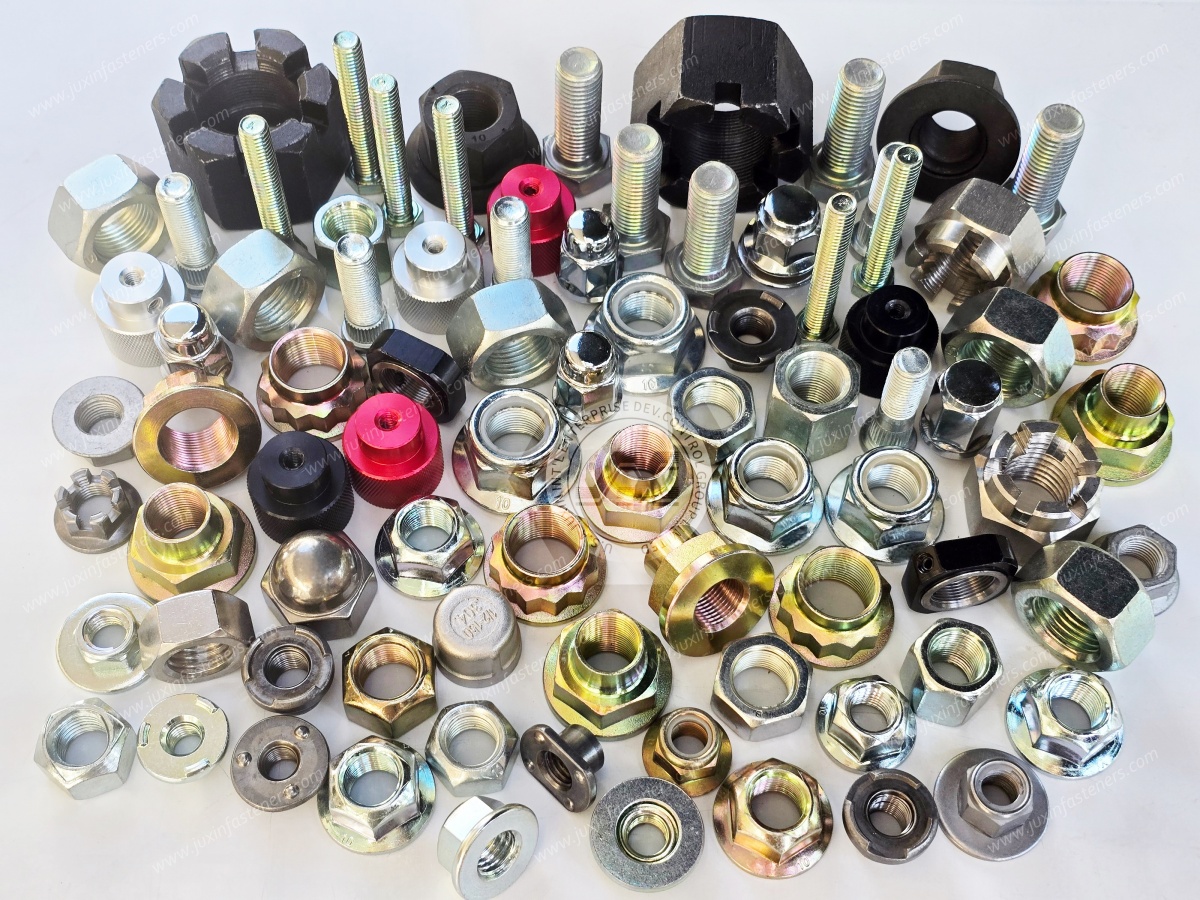
JUXIN FASTENERS supplies high-strength bolts, flange head fasteners, nylon-insert locknuts,
all-metal prevailing-torque nuts and drawing-based threaded components for industrial and automotive OEM applications.
This guide examines the engineering mechanisms behind automotive chassis fastener loosening and the practical selection of suitable retention methods.
Why Do Automotive Chassis Bolts Loosen?
Automotive chassis joints may experience combinations of axial loading, transverse movement, cyclic loading and thermal expansion.
Potential applications include:
Suspension mounting assemblies
Subframe connections
Structural brackets
Steering-related mechanical components
Selected EV battery mounting structures
Commercial vehicle mechanical assemblies
The fastener may be exposed to vibration, but vibration alone does not establish that loosening will occur.
The actual risk depends on the assembled joint.
Engineering Principle
The important question is not simply whether the vehicle vibrates.
It is whether the joint experiences conditions that allow relative movement, rotation or a reduction in clamping force.
Rotational Self-Loosening vs. Preload Loss
These two phenomena should be evaluated separately.
Rotational Self-Loosening
Rotational self-loosening occurs when a threaded fastener rotates in the loosening direction under suitable loading and joint conditions.
Transverse movement between clamped components can be an important contributing factor.
Preload Loss Without Rotation
Preload may decrease even when the fastener does not visibly rotate.
Potential causes include:
Surface embedment
Joint settling
Material creep
Gasket or coating compression
Thermal effects
Permanent deformation
Why This Distinction Matters
A locking nut may resist rotation but cannot automatically compensate for a joint that loses clamp load because a soft component continues to deform.
The corrective action must address the actual failure mechanism.
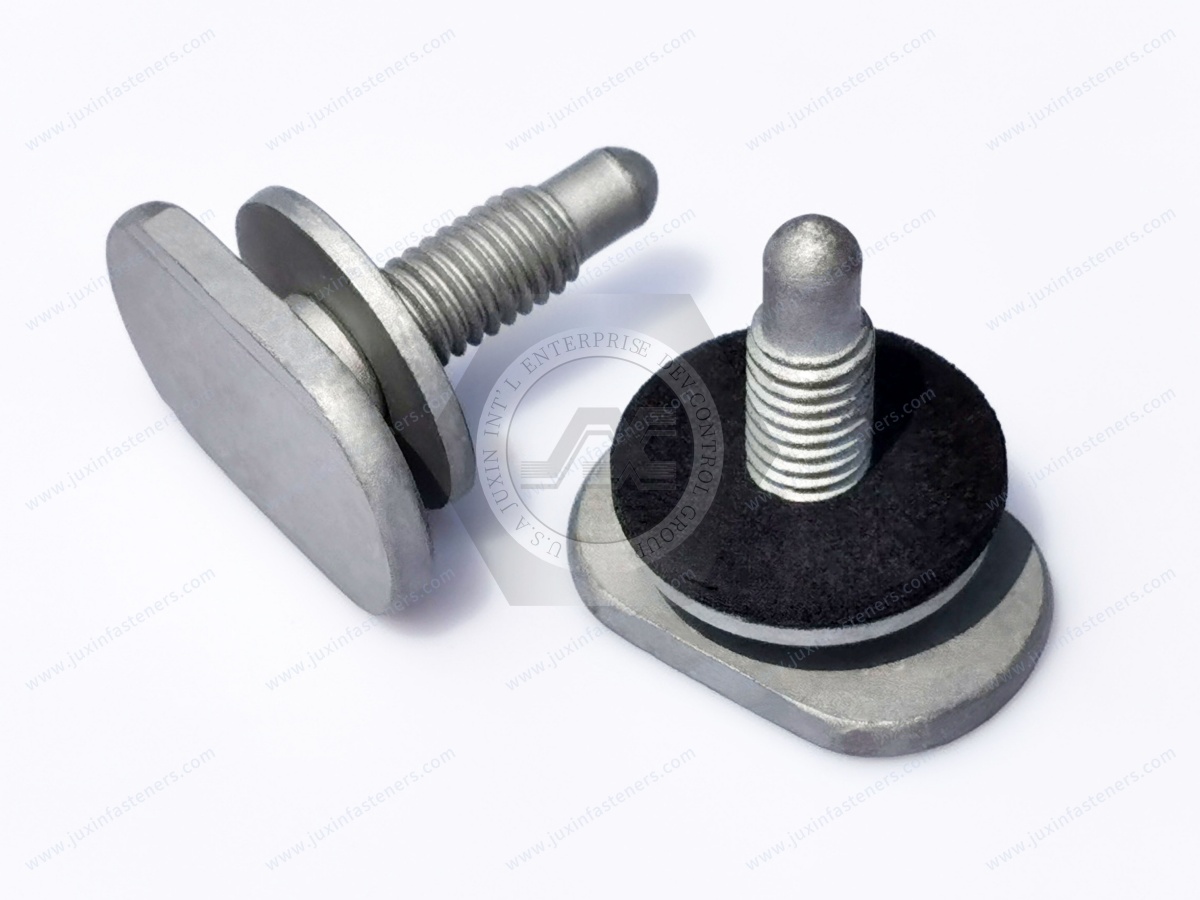
How Transverse Vibration Causes Bolt Self-Loosening
Transverse loading acts across the joint rather than directly along the bolt axis.
If the clamped interfaces experience sufficient relative movement, the conditions may permit rotational loosening.
Relevant variables include:
Initial preload
Joint stiffness
Interface friction
Transverse displacement
Bolt and nut geometry
Bearing surface behavior
Engineering Recommendation
Evaluate the joint's movement and load path before selecting a locking feature.
Why Higher Bolt Strength Does Not Guarantee Anti-Loosening Performance
High-strength fasteners are selected to meet specified mechanical requirements.
For applicable metric carbon steel and alloy steel bolts, ISO 898-1 defines mechanical property requirements.
Common property classes include 8.8, 10.9 and 12.9.
A property class 10.9 bolt has different mechanical property requirements from a property class 8.8 bolt.
However, higher tensile strength does not independently prevent rotational self-loosening.
Important Engineering Principle
Increasing bolt strength is not a substitute for controlling joint movement or selecting an appropriate retention method.
Preload and Clamp-Load Retention
Preload is the tensile force introduced into a bolt during tightening.
It creates a corresponding clamping action across the joint.
The intended preload depends on the fastener, joint geometry and approved assembly procedure.
Potential Consequences of Insufficient Preload
Increased joint movement
Reduced frictional resistance at the interface
Greater variation in load transfer
Increased loosening risk under susceptible conditions
Potential Consequences of Excessive Preload
Bolt overload
Thread damage
Mating component deformation
Excessive bearing pressure
Engineering Recommendation
Establish a suitable preload range through joint design and validation rather than applying the maximum possible tightening torque.
Tightening Torque Is Not the Same as Preload
Tightening torque is the rotational moment applied during installation.
Preload is the resulting tensile force.
The relationship between them depends on friction and the complete assembly.
Important friction locations include:
Thread interfaces
Bolt-head bearing surfaces
Nut bearing surfaces
Changes in lubrication, coating or surface condition may change the preload produced at the same torque.
Manufacturing Recommendation
Do not assume that two fasteners with identical dimensions and property classes will produce identical preload under the same torque if their surface conditions differ.
Why Friction Control Matters
Automotive fastener coatings may be specified for corrosion protection and particular assembly characteristics.
However, friction behavior depends on the complete coating and lubrication system.
Engineering Considerations
Thread friction
Bearing-surface friction
Coating thickness
Lubrication condition
Mating component material
Assembly speed
Important Limitation
A general coating description such as zinc-nickel or zinc-flake does not establish a universal friction coefficient.
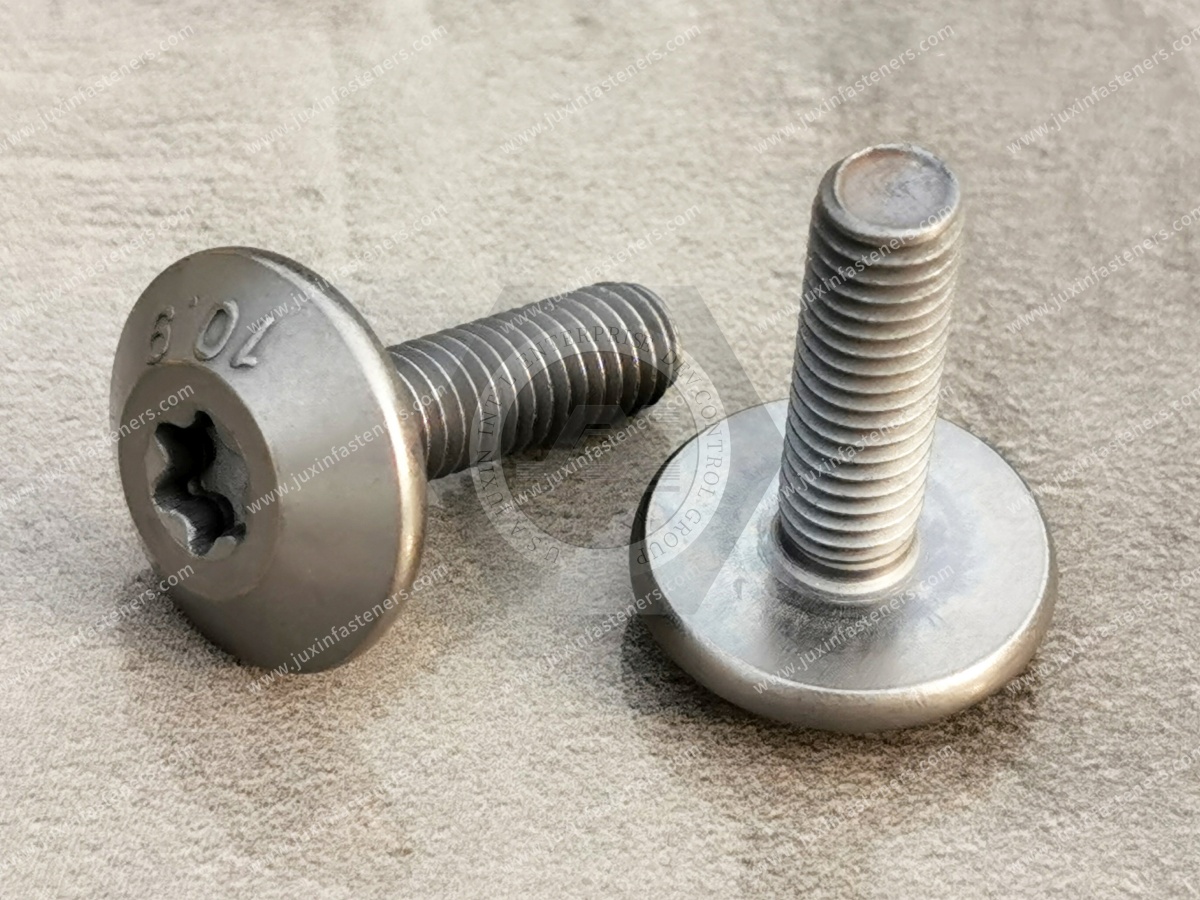
Property Class 10.9 Flange Bolts for Chassis Joints
Property class 10.9 flange bolts may be specified for selected automotive mechanical connections.
Potential applications include:
Suspension brackets
Subframe assemblies
Structural mounting points
Powertrain-related mechanical supports
Engineering Considerations
Required preload
Flange bearing area
Joint material
Fastener grip length
Coating
Tightening procedure
Important Limitation
The flange geometry does not automatically provide an anti-loosening function.
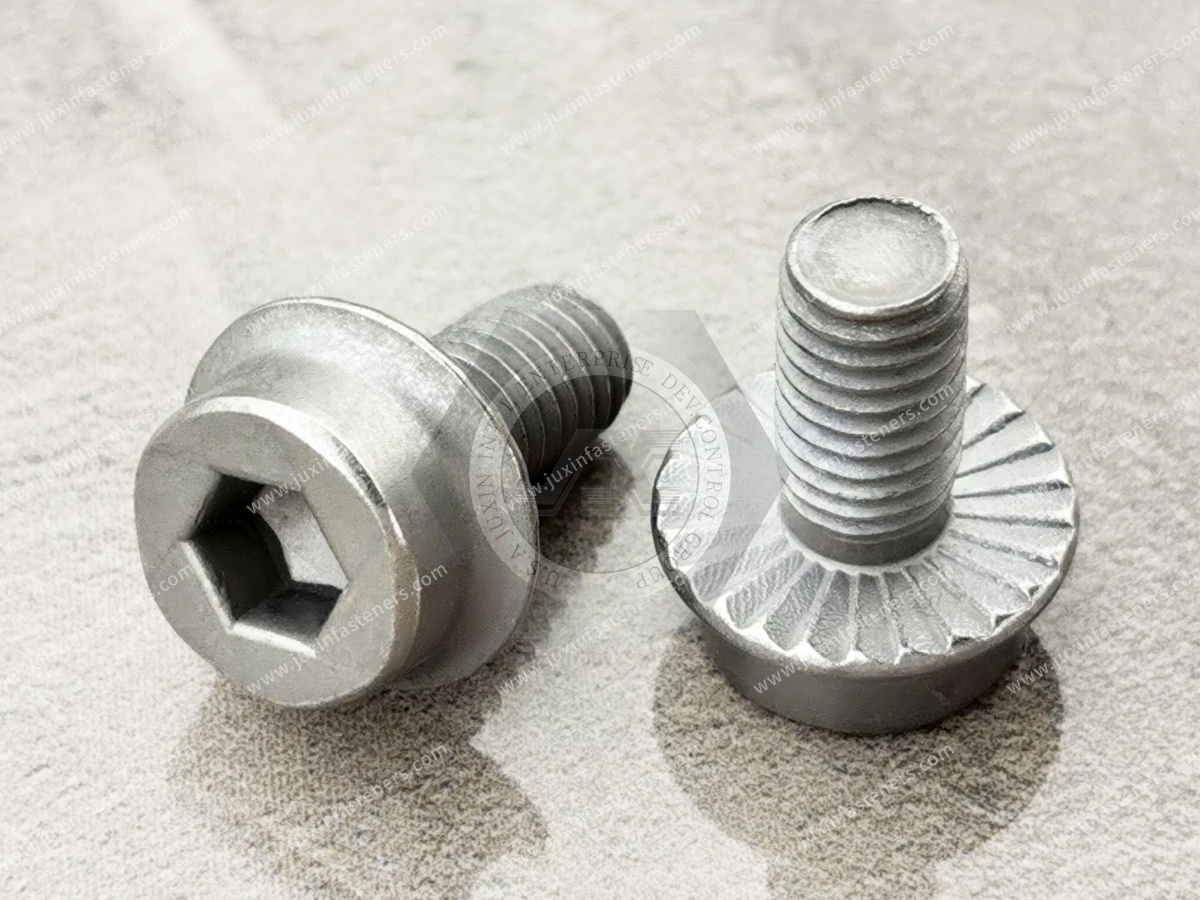
Serrated Flange Bolts: When Are They Appropriate?
Serrated flange bolts have teeth on the bearing surface.
Under suitable conditions, the serrations can influence resistance to rotation.
However, their performance depends on the actual joint.
Potential Engineering Considerations
Mating surface hardness
Surface coating
Bearing pressure
Joint preload
Installation method
Service loading
Important Limitation
Serrated flange bolts should not be described as universally vibration-proof.
Their teeth may damage paint, zinc coatings or softer mating materials.
Special Consideration for Aluminum Components
In aluminum structures, serrations may alter the bearing surface and local contact condition.
The complete joint must be evaluated for mechanical performance and corrosion compatibility.
Engineering Recommendation
Use serrated flange bolts only where the approved joint design permits their bearing-surface characteristics.
Prevailing-Torque Lock Nuts
Prevailing-torque nuts incorporate a feature that resists relative rotation between the nut and mating thread.
Common types include:
Nylon-insert locknuts
All-metal prevailing-torque nuts
Distorted-thread locknuts
Selected prevailing-torque flange nuts
Important Engineering Distinction
Prevailing torque is the torque associated with the locking feature.
It is not equivalent to the axial preload generated in the joint.
All-Metal Prevailing-Torque Nuts
All-metal locking nuts use a metallic locking feature rather than a polymer insert.
They may be considered where the application requires a locking arrangement compatible with the specified operating environment.
Engineering Considerations
Temperature
Thread compatibility
Installation torque
Locking feature geometry
Reuse requirements
Coating
Important Limitation
All-metal locking nuts do not automatically maintain the intended preload if the joint experiences significant relaxation.
Distorted-Thread Lock Nuts
Distorted-thread locknuts use controlled thread deformation or another metallic interference feature to generate prevailing torque.
Potential applications include selected vibration-exposed mechanical assemblies.
Engineering Considerations
Locking torque specification
Thread compatibility
Installation behavior
Repeated assembly
Coating and lubrication
Engineering Recommendation
Confirm the approved prevailing-torque requirements and installation procedure before substitution.
Nylon-Insert Locknuts
Nylon-insert locknuts use a polymer locking element to provide resistance to rotation.
DIN 985 is associated with a widely recognized prevailing-torque nut configuration, while the applicable current product specification and customer drawing should be confirmed for procurement.
Engineering Considerations
Operating temperature
Chemical exposure
Installation condition
Thread engagement
Reuse requirements
Important Limitation
A nylon-insert locknut should not automatically be specified for high-temperature or safety-critical chassis applications.
The approved product and joint requirements determine suitability.
Flange Lock Nuts
Flange locknuts combine a bearing flange with a locking feature in certain designs.
Potential benefits may include:
Integrated bearing surface
Reduced separate-component handling
Compatibility with controlled assembly
Important Engineering Distinction
A plain flange nut and a prevailing-torque flange locknut are not necessarily the same product.
The locking mechanism must be identified in the drawing and purchasing specification.
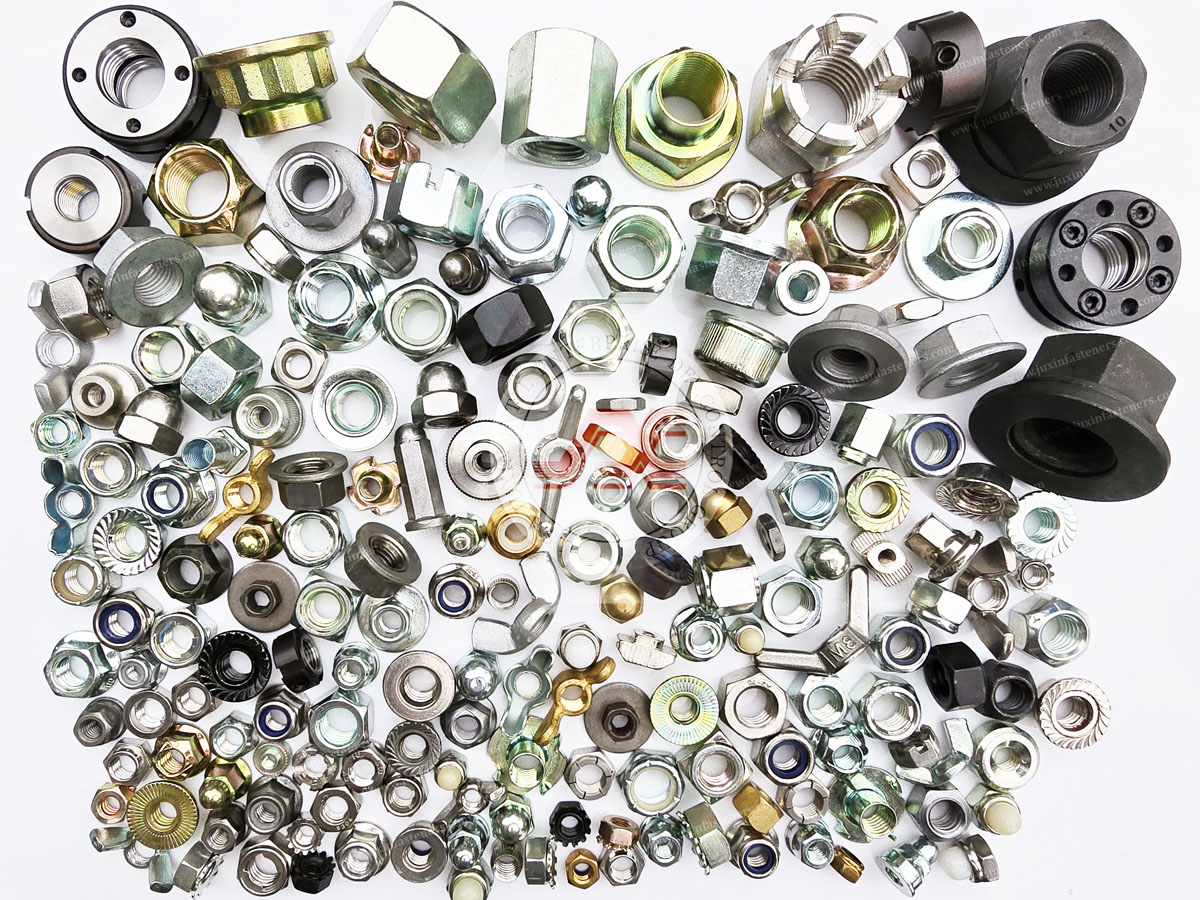
How to Select a Locking Nut
The appropriate choice depends on the actual operating conditions.
| Selection factor | Engineering question |
|---|---|
| Temperature | Is the locking feature compatible with the full operating range? |
| Vibration | What transverse movement and service loads are expected? |
| Preload | Does the joint require a defined clamp-load range? |
| Reuse | Is the nut intended for single or repeated installation? |
| Coating | Are friction and corrosion requirements specified? |
| Mating thread | Are the bolt and nut fully compatible? |
| Qualification | Has the complete joint been approved for the application? |
Important Recommendation
Do not select a locking nut based only on its nominal diameter and thread pitch.
Mechanical Locking Arrangements
Some automotive and industrial joints use mechanical retention arrangements such as:
Locking plates
Cotter pins with compatible fastener geometry
Safety wire arrangements
Other application-specific mechanical locking components
Engineering Considerations
Joint geometry
Available installation space
Service access
Inspection requirements
Approved assembly procedure
Important Limitation
A mechanical retention feature may prevent complete disengagement without necessarily maintaining the original clamp load.
Thread-Locking Adhesives
Thread-locking adhesives may be used in selected engineered assemblies.
Engineering Considerations
Thread size
Material compatibility
Surface cleanliness
Operating temperature
Cure conditions
Service disassembly requirements
Important Limitation
Adhesives are not automatically suitable for every coated fastener, temperature range or safety-critical automotive joint.
Locking Washer Systems
Certain locking washer systems are designed to influence resistance to rotation or joint loosening.
Engineering Considerations
Washer geometry
Mating surface
Bolt preload
Installation procedure
Coating
Joint stiffness
Important Limitation
A conventional split lock washer should not automatically be assumed to provide reliable protection against severe transverse-vibration loosening.
Thread Engagement and Loosening
Thread engagement must be sufficient for the mating material and mechanical loading.
However, increasing engagement length does not automatically prevent rotational self-loosening.
Engineering Distinction
Thread engagement primarily concerns the integrity of the threaded connection.
Self-loosening resistance also depends on preload, joint movement and the selected retention arrangement.
Engineering Recommendation
Evaluate thread strength and anti-loosening performance as related but separate design requirements.
Bearing Surface and Washer Selection
Bearing pressure influences the behavior of clamped components.
A larger bearing surface may be useful where the mating material requires additional support.
Engineering Considerations
Surface hardness
Local deformation
Washer hardness
Flange diameter
Coating
Contact pressure
Important Limitation
A larger washer does not automatically prevent loosening.
Joint Relaxation and Surface Embedment
Bolted joints may lose preload as contacting surfaces settle.
Potential contributors include:
Surface roughness
Coating compression
Local material deformation
Soft interlayers
Temperature-dependent creep
Engineering Recommendation
Evaluate the complete joint stack-up and material behavior.
Adding a locking nut alone may not correct preload loss caused by these mechanisms.
Thermal Expansion in Automotive Joints
Automotive assemblies may contain materials with different thermal expansion characteristics.
Potential combinations include:
Steel bolts and steel brackets
Steel bolts and aluminum structures
Mixed-metal assemblies
Joints containing polymer components
Temperature changes can influence joint loading and clamp-force retention.
Engineering Recommendation
Evaluate the full operating temperature range and material combination.
Steel Fasteners in Aluminum EV Chassis Structures
EV structures may combine high-strength steel bolts with aluminum components.
Engineering Considerations
Mating thread strength
Bearing pressure
Galvanic corrosion
Differential thermal expansion
Coating compatibility
Joint stiffness
Important Engineering Principle
A higher-strength steel bolt cannot compensate for an inadequately designed aluminum threaded connection.
Corrosion Protection and Loosening Reliability
Corrosion can change the condition of threads and bearing surfaces.
It may also affect maintenance and disassembly.
Engineering Considerations
Road salt
Moisture
Coating damage
Material pairing
Exposure duration
Important Limitation
Corrosion resistance and anti-loosening performance are separate requirements, even though both influence joint reliability.
Zinc-Nickel Coatings
Zinc-nickel coatings may be specified for selected automotive fasteners.
Engineering Considerations
Corrosion requirements
Coating thickness
Friction characteristics
Thread fit
Hydrogen embrittlement risk
Customer-specific compliance requirements
Important Limitation
A zinc-nickel coating does not automatically establish RoHS compliance or a specified friction coefficient.
Zinc-Flake Coatings
Zinc-flake systems may be selected for certain automotive fastener applications.
Engineering Considerations
Coating system
Friction-control topcoat
Corrosion specification
Mechanical property class
Installation process
Important Recommendation
Validate tightening behavior when changing coating systems.
Black Phosphate and Other Surface Treatments
Phosphate coatings may be used in selected fastening applications.
Their suitability depends on the complete surface treatment and environmental requirements.
Important Limitation
A phosphate finish alone should not be assumed to provide sufficient corrosion protection for exposed chassis applications.
Hydrogen Embrittlement in High-Strength Steel Fasteners
Certain high-strength steel fasteners may be susceptible to hydrogen embrittlement.
Relevant factors include:
Material strength
Hardness
Processing
Surface treatment
Hydrogen exposure
Applied stress
Important Engineering Recommendation
Review the relevant material and processing controls for susceptible high-strength fasteners.
A post-treatment operation should not be assumed to eliminate every hydrogen embrittlement risk.
Vibration Testing and Joint Validation
Laboratory testing may help engineers compare fastening arrangements under defined conditions.
ISO 16130 addresses transverse-displacement testing of fasteners for evaluation of loosening behavior.
Important Engineering Distinction
A laboratory test result applies to the tested configuration and conditions.
It does not automatically guarantee identical performance in every vehicle joint.
What Should Be Evaluated?
Depending on the test method and project requirements, engineers may consider:
Initial preload
Applied transverse displacement
Clamp-load change
Relative rotation
Test duration
Joint configuration
Important Recommendation
Specify the required test method, configuration and acceptance criteria before supplier qualification.
Failure Diagnosis: What Actually Caused the Bolt to Loosen?
Before replacing a fastener with a stronger bolt or a locking nut, identify the failure mechanism.
| Observed problem | Possible mechanism | Engineering investigation |
|---|---|---|
| Nut visibly rotates loose | Rotational self-loosening | Examine transverse movement and locking method |
| Clamp load decreases without rotation | Joint relaxation or embedment | Examine contact surfaces and joint stack-up |
| Bolt fractures | Overload, fatigue or other damage | Review load history, geometry and material |
| Threads strip | Inadequate mating thread strength | Review engagement and material compatibility |
| Joint moves under service load | Insufficient frictional resistance or unsuitable load path | Review preload and joint design |
| Coating damage | Excessive contact pressure or incompatible bearing surface | Review flange, washer and coating |
| Installation torque varies | Friction or process inconsistency | Review coating, lubrication and tooling |
Engineering Principle
The correct solution depends on the diagnosed cause, not simply the visible symptom.
Production-Line Controls for Anti-Loosening Fasteners
Manufacturing engineers and production managers should consider:
Fastener identification
Locking nut type
Correct thread specification
Coating condition
Approved tightening program
Tool calibration
Installation sequence
Inspection requirements
Important Production Principle
A locking feature does not replace a controlled assembly process.
Prevailing Torque and Assembly Tooling
Prevailing-torque nuts may require additional torque to turn during installation.
This resistance must be distinguished from torque associated with generating joint preload.
Engineering Recommendation
Use the approved tightening procedure and applicable inspection requirements for the selected locking nut.
Repeated Installation and Reuse
Some locking fasteners have reuse restrictions.
Repeated installation can alter the locking feature or assembly behavior.
Engineering Recommendation
Follow the component manufacturer's or automotive OEM's approved reuse policy.
EV Battery Mounting Applications
Battery enclosure and structural mounting joints may be exposed to vibration and environmental loading.
Engineering Considerations
Mechanical loading
Preload retention
Material compatibility
Corrosion
Service access
Approved sealing arrangements
Important Limitation
A vibration-resistant mechanical fastener does not independently establish electrical or battery safety compliance.
Suspension and Subframe Applications
Suspension and subframe joints may have different requirements depending on whether they are intended to remain rigidly clamped or accommodate controlled movement.
Engineering Considerations
Joint function
Load path
Bolt grip length
Bushing arrangement
Tightening condition
Service replacement requirements
Important Recommendation
Use the approved component-specific fastener and tightening specification.
Commercial Vehicle Applications
Trucks, buses and heavy-duty equipment may require fastening arrangements suited to their particular loads and maintenance conditions.
Engineering Considerations
Service loading
Vibration
Corrosion
Maintenance intervals
Approved retention method
Important Limitation
A passenger-vehicle fastening arrangement should not automatically be transferred to a commercial-vehicle application.
OEM Supplier Qualification for Anti-Loosening Fasteners
Automotive procurement and supplier-development teams should evaluate both product conformity and assembly compatibility.
Technical Requirements
Approved drawing
Thread designation
Mechanical property class
Locking feature
Prevailing-torque requirements
Surface treatment
Inspection criteria
Production Requirements
Installation compatibility
Part identification
Packaging
Batch controls
Change management
Customer-specific approval
Commercial Requirements
MOQ
Annual volume
Sample requirements
Lead time
Delivery schedule
Important Procurement Principle
A locking nut with the same thread size is not automatically an approved replacement.
Drawing-Based Automotive Anti-Loosening Fasteners
Custom applications may require:
Special flange geometry
Controlled locking feature
Defined thread length
Specific coating
Customer-specified friction characteristics
Special inspection requirements
JUXIN FASTENERS welcomes drawing-based inquiries for suitable high-strength bolts and locking nut products.
Feasibility, production requirements and qualification conditions should be confirmed during technical review.
Frequently Asked Questions
Why do automotive chassis bolts loosen under vibration?
Rotational self-loosening may occur when the joint experiences conditions that permit relative movement and fastener rotation. Other joints may lose preload without rotation.
Are property class 10.9 bolts vibration-proof?
No. Property class 10.9 defines mechanical properties, not guaranteed anti-loosening performance.
Do prevailing-torque nuts maintain bolt preload?
They resist rotation through a locking feature, but cannot prevent every form of preload loss.
Are serrated flange bolts suitable for aluminum chassis parts?
Only where the approved design accounts for bearing-surface effects, coating damage and material compatibility.
Can increasing thread engagement prevent bolt loosening?
Not automatically. Adequate thread engagement supports thread strength but does not independently prevent rotational self-loosening.
Are nylon-insert locknuts suitable for suspension applications?
Suitability depends on the approved joint design, operating temperature, locking requirements and OEM specifications.
Are all-metal locknuts better than nylon-insert locknuts?
Neither is universally better. The appropriate choice depends on the operating conditions and qualification requirements.
Does zinc-nickel plating improve anti-loosening performance?
Not automatically. Coating and friction behavior must be evaluated as part of the joint.
What is transverse-vibration testing?
It is a controlled method of evaluating loosening behavior under specified transverse displacement conditions.
What information is needed for an OEM anti-loosening fastener RFQ?
Provide drawings, thread designation, property class, locking feature, coating, installation requirements, quantities and applicable test criteria.
JUXIN FASTENERS: Automotive High-Strength Bolts and Locking Nut Solutions
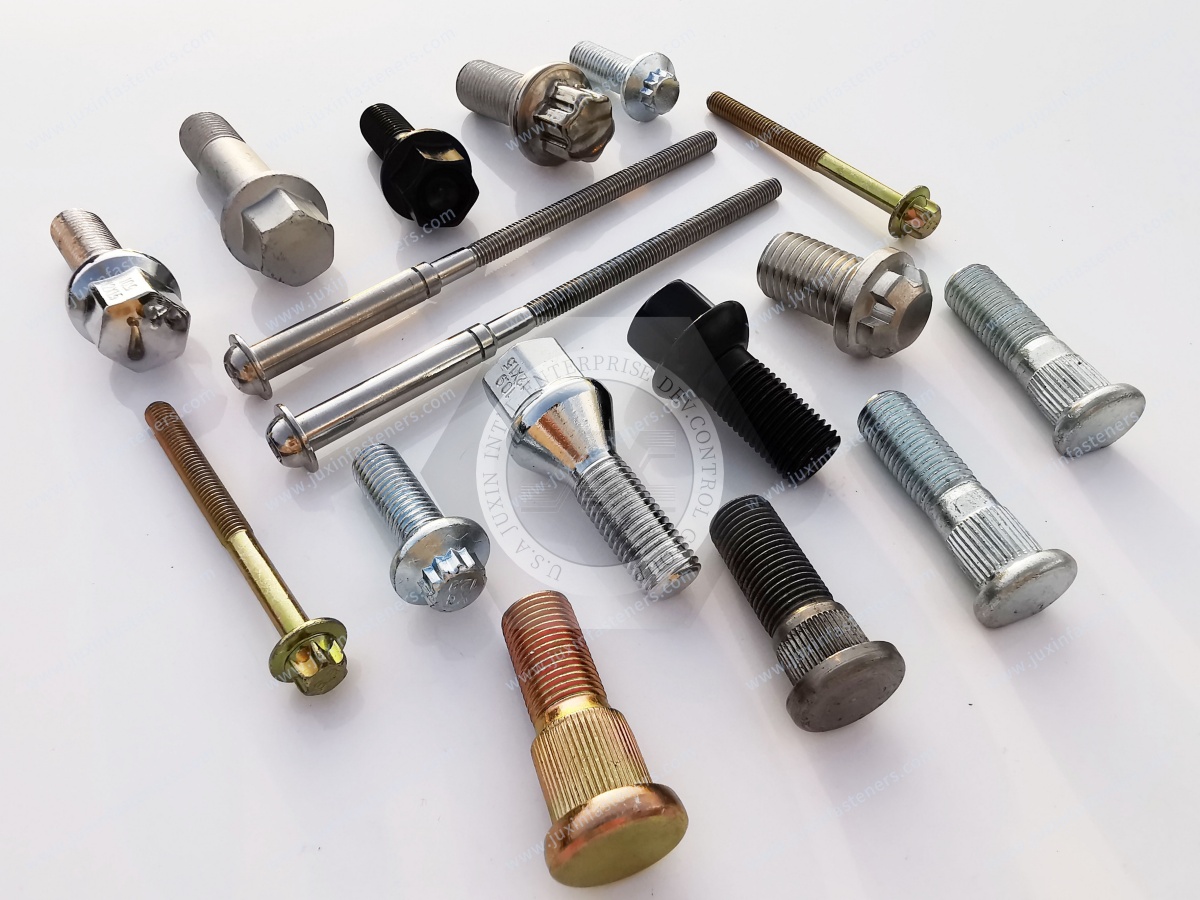
JUXIN FASTENERS supplies industrial threaded fasteners for automotive and mechanical equipment applications.
Relevant product families include:
Property class 8.8 bolts
Property class 10.9 bolts
Property class 12.9 screws
Hexagon flange bolts
Nylon-insert locknuts
All-metal prevailing-torque nuts
Distorted-thread locking nuts
Flange locking nuts
Drawing-based OEM threaded components
Specific locking performance, materials, coatings and customer qualification requirements should be reviewed against the approved drawings and purchasing specifications.
Request an Automotive Anti-Loosening Fastener RFQ
Are you sourcing vibration-resistant locking nuts, property class 10.9 flange bolts or drawing-based chassis fastening components?
JUXIN FASTENERS welcomes inquiries from automotive OEMs, Tier-1 and Tier-2 suppliers, design engineers, manufacturing engineers, production managers and global procurement teams.
For an efficient technical and commercial review, provide:
Approved drawing + application + thread specification + property class + locking feature + coating + installation requirements + inspection criteria + annual volume + delivery schedule
Where applicable, include the required prevailing-torque specification, transverse-vibration test requirements and customer qualification criteria.
Company: JUXIN FASTENERS
Website: https://www.juxinfasteners.com/
Email: info@juxinfasteners.com
Send your automotive locking fastener drawings and OEM RFQ requirements to JUXIN FASTENERS for technical review and quotation.
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY



