
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Sep. 21, 2023
When an engineer or buyer searches for an “ASME shaft retaining ring,” identifying the correct standard is only the beginning.
The next questions are:
Which ASME B18.27 retaining-ring type is required?
What inch shaft size and groove does it fit?
What axial load must the ring-and-groove system retain?
Is the requirement a current production design or a replacement for a legacy U.S. drawing?
These questions matter because ASME B18.27 does not describe only one external retaining ring.
The standard covers multiple tapered and reduced-cross-section retaining-ring configurations for inch-series shafts and housings.
For the conventional external shaft-retaining-ring configuration, an important designation is:
External Type NA1
JUXIN FASTENERS supports standard and drawing-based retaining rings for U.S. inch-series OEM, replacement and industrial sourcing requirements.
ASME B18.27 covers:
Tapered and Reduced Cross Section Retaining Rings — Inch Series
The current standard designation is:
ASME B18.27-1998 (S2022)
The standard provides general and dimensional data for multiple types of retaining rings used with nominal inch-series shafts and housings and corresponding recommended grooves.
This makes ASME B18.27 particularly relevant to:
U.S. machinery;
North American OEM equipment;
legacy inch-series drawings;
industrial replacement parts;
MRO sourcing;
equipment designed around inch shaft and bore dimensions.
Older product descriptions, supplier pages or internal records may use inconsistent terminology such as:
ASME B18.27.2 Type A
For current engineering and procurement work, the recognized ASME standard is:
ASME B18.27-1998 (S2022)
and the conventional external ring covered by the standard is identified as:
External Type NA1
Therefore, an RFQ should not rely on an ambiguous description when the exact standard and ring type can be identified.
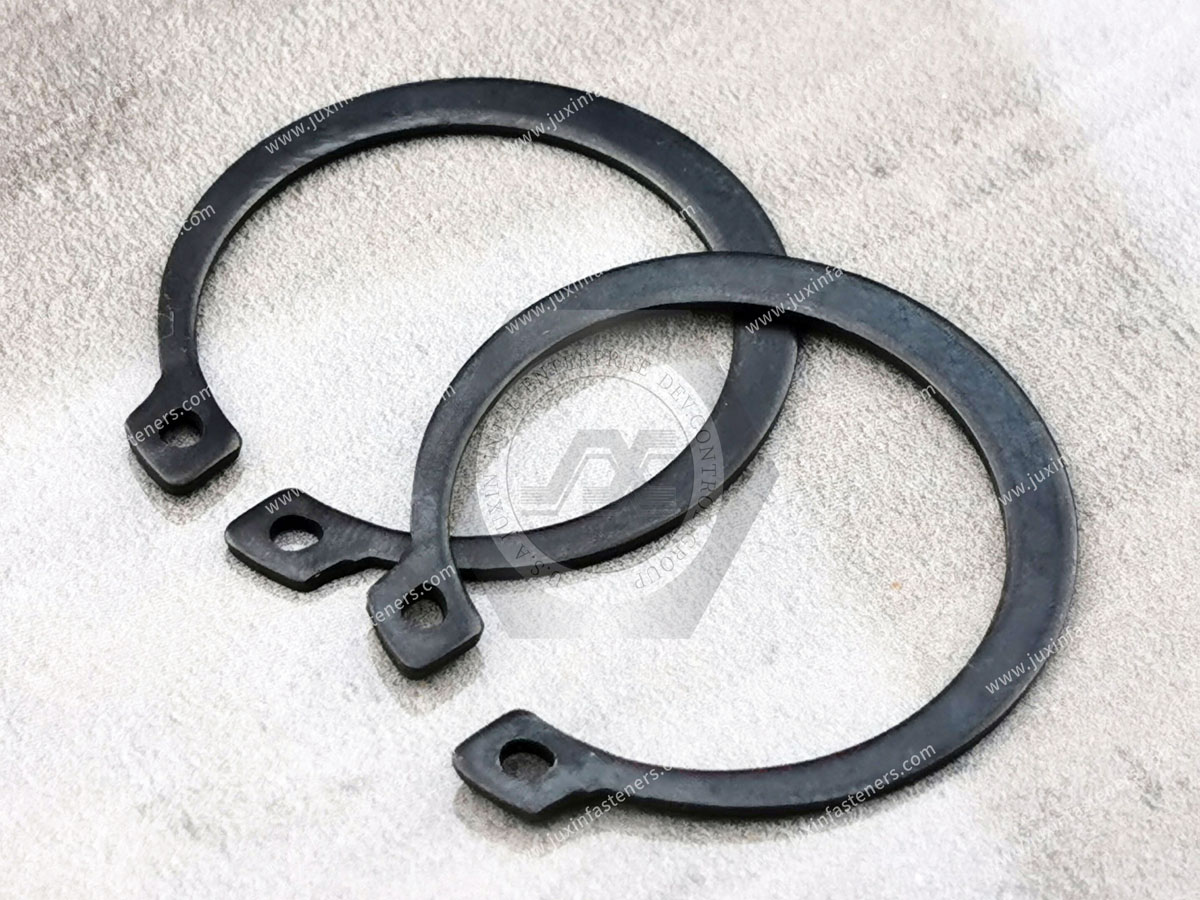
An External Type NA1 retaining ring is installed into a groove on the outside of a shaft.
The ring creates an axial retaining shoulder that restricts movement of a component along the shaft.
Typical retained components may include:
bearings;
gears;
spacers;
sleeves;
pulleys;
mechanical subassemblies.
The basic retention system is:
Retained Component → External Retaining Ring → Shaft Groove → Shaft
The shaft groove is therefore part of the functional retaining system.
A retaining ring should not be evaluated independently from the shaft.
When axial load acts on the retained component, force passes through the ring and into the groove.
Conceptually:
Component Axial Force → Ring → Groove Face → Shaft
The functional capacity can therefore depend on:
ring geometry;
groove geometry;
shaft material;
shaft strength;
axial load;
installation condition.
A ring that physically fits the groove is not automatically validated for the application.
Many conventional retaining rings are designed so that their radial cross section changes around the circumference.
This geometry helps the ring behave appropriately when expanded or compressed for installation and when seated in the groove.
The geometry should not be altered casually in a replacement part.
For OEM sourcing, the correct standard type or customer drawing should control the configuration.
ASME B18.27 also includes reduced-cross-section retaining-ring designs.
These represent additional geometries within the standard rather than one universal external circlip.
This is why an RFQ stating only:
“ASME retaining ring”
may not completely identify the required component.
The standard includes multiple retaining-ring configurations.
Among the listed types are:
External Type NA1;
Internal Type NA2;
E-Ring Type NA3;
Heavy Duty External Type NA4;
Reinforced E-Rings Type NA5;
C-Rings Type NA6;
Bowed External Rings Type NA7;
Bowed Internal Rings Type NA8;
Bowed External E-Rings Type NA9;
Inverted External Type NA10;
Inverted Internal Type NA11;
Beveled External Type NA12;
Beveled Internal Type NA13;
External Self-Locking Rings Type NA14;
External Interlocking Rings Type NA15;
External Bowed Locking Prongs Rings Type NA16.
This creates an important sourcing rule:
ASME B18.27 ≠ One Retaining Ring Geometry
The type designation matters.
NA1 is the conventional external retaining-ring category within ASME B18.27.
It is relevant where the assembly requires a ring installed in an external shaft groove.
The design question should be:
Is NA1 the required configuration for this shaft and load case?
rather than:
Does any external circlip fit?
NA2 applies to internal retaining-ring geometry for housing or bore applications.
Therefore:
NA1 → External / Shaft
NA2 → Internal / Housing or Bore
These should not be confused during procurement.
An E-ring uses a different geometry and installation concept from a conventional plier-installed external ring.
E-rings can be useful where assembly architecture favors radial installation.
However:
NA3 E-Ring ≠ NA1 External Ring
Even where both retain components on shafts, their groove and installation requirements differ.
ASME B18.27 also includes Heavy Duty External Type NA4.
The existence of a heavy-duty type does not mean it should automatically replace NA1.
The correct type depends on:
drawing;
shaft geometry;
groove;
axial load;
available space;
assembly method.
“Heavy duty” should be treated as a specific standard configuration, not as a marketing adjective.
For engineering selection, ask:
What load must be retained?
What shaft and groove geometry is available?
Which ASME B18.27 type is specified?
Is the application new design or legacy replacement?
Do not assume:
Higher Section Size = Automatically Better Design
Changing ring type can also require changing the groove and surrounding geometry.
This distinction is commercially important.
DIN 471 and ASME B18.27 can both relate to external shaft-retaining rings, but they belong to different dimensional systems and standards frameworks.
Primarily associated with metric external retaining rings for shafts.
Covers inch-series tapered and reduced-cross-section retaining rings, including multiple external, internal and specialized forms.
Therefore:
DIN 471 → Metric Shaft-Ring Search Intent
ASME B18.27 → U.S. Inch-Series Retaining-Ring Search Intent
They should not be treated as automatic dimensional equivalents.
A common sourcing mistake is to convert an inch nominal size to its approximate metric value and then select a metric circlip.
For example:
Inch Shaft → Approximate Millimeter Conversion → Metric Ring
does not establish equivalence.
The groove dimensions, ring geometry and tolerances may differ.
For replacement programs:
Identify Original Standard First → Verify Groove → Compare Candidate Replacement → Approve Substitution
Industrial equipment can remain in service for decades.
Maintenance teams may encounter drawings containing:
older ASME references;
ANSI references;
manufacturer part numbers;
obsolete supplier numbers;
inch shaft dimensions;
incomplete retaining-ring descriptions.
The correct replacement process should begin with technical identification rather than visual similarity.
If the original part number is unavailable, collect:
shaft diameter;
groove diameter;
groove width;
ring thickness;
ring geometry;
lug geometry;
free diameter;
material if known;
surface finish;
equipment model;
original drawing or sample.
A physical sample can be useful, but wear or permanent deformation should be considered.
A used retaining ring may have:
permanent expansion;
wear;
corrosion;
installation damage;
distorted lugs.
Therefore, reverse engineering should include the shaft groove wherever possible.
The groove often provides more reliable information about the intended ring than a damaged used sample alone.
The shaft groove controls the ring's engagement and axial position.
Important variables include:
groove diameter;
groove width;
groove location;
groove corner geometry;
shaft material;
nearby shoulders.
The applicable ASME dimensions or controlled drawing should govern the groove.
Groove diameter influences:
ring engagement;
remaining shaft section;
installed ring geometry.
A groove that is too shallow or too deep can affect retention.
Therefore:
Deeper Groove ≠ Automatically Stronger Groove
Groove width influences axial ring fit.
Incorrect width can create:
excessive clearance;
poor seating;
assembly interference;
uneven load transfer.
The groove's axial location determines the position of the retained component.
This can influence:
bearing position;
gear alignment;
spacer stack;
end play;
assembly tolerance.
Groove position may therefore be a functional dimension.
The shaft must support the axial load transferred through the groove.
Potential limiting conditions can include:
groove-edge deformation;
shaft yielding;
local shear;
ring deformation.
A higher-strength retaining ring cannot compensate for an inadequately designed groove.
External retaining rings are primarily axial-retention components.
Potential axial loads can come from:
bearing thrust;
gear reaction;
spring force;
actuator force;
assembly loads;
transient mechanical events.
The actual loading should be identified before selecting the retaining system.
The old description of a retaining ring as carrying both axial and radial loads can be misleading.
The primary retention task is normally axial.
Radial forces within the machine should be carried by the intended bearing, shaft or other structural components.
Therefore:
Retaining Ring ≠ Radial Bearing
Another common description is that retaining rings “absorb vibration.”
That is not their primary engineering function.
A conventional retaining ring is a mechanical axial-retention component.
Therefore:
Elastic Installation Behavior ≠ Vibration Damping
If vibration isolation is required, use an appropriate vibration-control strategy.
The ring may experience transient axial loading, but it should not automatically be marketed as a shock absorber.
Shock loading should instead be included in the mechanical load case.
Noise reduction depends on the complete mechanical system.
Installing a retaining ring does not inherently create a low-noise assembly.
The ring's function is retention.
A conventional external retaining ring is expanded during installation so that it can pass over the shaft.
A general sequence is:
Verify ring type and size.
Inspect the shaft and groove.
Engage the correct installation tool.
Expand the ring only as much as necessary.
Move the ring into the groove position.
Release it in a controlled manner.
Verify complete seating.
The exact procedure depends on the retaining-ring design.
The ring must deform elastically during installation.
However:
Necessary Expansion ≠ Unlimited Expansion
Over-expansion can cause:
permanent set;
lug damage;
distortion;
reduced spring recovery;
poor seating.
Installation tooling is therefore part of retaining-ring process control.
After installation, verify that the ring is fully engaged with the groove.
Partial seating can result from:
burrs;
contamination;
wrong ring;
incorrect groove;
ring deformation;
poor installation technique.
A partially seated ring can compromise axial retention.
Machining burrs can interfere with seating and damage the ring.
The shaft groove should therefore be inspected as part of the complete assembly.
Many conventional lugged external rings use appropriate retaining-ring pliers.
Tool selection should consider:
ring size;
lug-hole geometry;
required expansion;
production volume;
operator control.
Incorrect plier tips can damage the installation holes.
High-volume OEM production may use dedicated installation equipment.
Automation can improve:
repeatability;
cycle time;
process control.
However, automated installation should still control:
ring orientation where relevant;
expansion;
groove location;
seating verification.
Automation does not compensate for an incorrect ring or groove.
Reuse should not automatically be assumed.
Inspect for:
permanent deformation;
excessive expansion;
corrosion;
wear;
damaged lugs;
damaged installation holes;
loss of spring recovery.
Follow the equipment manufacturer's maintenance requirements for critical applications.
Retaining rings require material properties suitable for elastic installation and mechanical retention.
Potential material systems depend on:
standard requirement;
customer drawing;
corrosion environment;
operating temperature;
mechanical load.
Material should not be inferred only from the ring's appearance.
Spring steels are commonly associated with retaining-ring applications because they can provide the elastic behavior required during installation.
The actual material and heat treatment should match the product specification.
Spring steel does not automatically provide sufficient corrosion resistance for every environment.
Stainless steel may be selected for improved corrosion resistance in appropriate environments.
However:
Stainless Steel ≠ Corrosion-Proof
The application should still consider:
moisture;
chemicals;
temperature;
galvanic compatibility;
mechanical properties.
Surface treatment should be specified according to the actual environmental and customer requirements.
For hardened spring-steel components, processing should consider hydrogen-embrittlement risk where applicable.
Do not assign a universal corrosion-life claim based only on coating name.
External retaining rings can be installed on rotating shafts.
At higher rotational speeds, the designer should consider the specific retaining-ring geometry and complete rotating system.
ASME-related engineering literature notes that tapered-section rings with lugs can introduce imbalance considerations at higher rotational speeds.
Therefore:
Fits the Shaft ≠ Automatically Suitable for Unlimited RPM
Rotational requirements should be included in engineering evaluation.
A lugged retaining ring is not perfectly rotationally symmetric.
For many ordinary industrial applications this may not control the design.
For high-speed equipment, however, rotating mass distribution can become relevant.
Possible alternatives may include other retaining-ring architectures where the application requires them.
The correct choice depends on:
RPM;
shaft diameter;
ring mass;
surrounding geometry;
equipment balance requirements.
A ring subjected to constant axial load and a ring exposed to repeated axial load can experience different service conditions.
Evaluate:
load magnitude;
load direction;
cycle frequency;
impact;
service life requirement.
Do not convert a dimensional standard into an unsupported universal fatigue rating.
A retaining ring can leave or partially leave its groove if the retention system is unsuitable.
Possible contributors include:
incorrect groove;
excessive axial force;
incomplete seating;
ring deformation;
groove failure;
wrong ring type.
The cause should be diagnosed before simply installing a stronger ring.
If the shaft or groove cannot support the transferred load, the groove edge may deform.
Possible contributors include:
weak shaft material;
insufficient groove geometry;
excessive axial force;
impact loading.
The solution may require a shaft-design change rather than only a ring change.
This can result from:
over-expansion during installation;
incorrect tooling;
excessive rotational effects;
overload.
A permanently expanded ring may no longer seat correctly.
Installation lugs can be damaged by:
incorrect pliers;
excessive expansion;
repeated installation;
poor handling.
Damaged rings should be evaluated before reuse.
Corrosion can reduce section thickness or affect removal and serviceability.
Material and finish should be matched to the actual environment.
Both belong to ASME B18.27, but they represent different retaining-ring configurations.
A practical selection process is:
Check Drawing → Identify Type → Confirm Shaft and Groove → Determine Axial Load → Verify Material / Finish → Validate Assembly
Do not substitute NA4 for NA1 simply because “heavy duty” sounds stronger.
Both may be used on shafts, but installation architecture differs.
NA1 is a conventional external ring.
NA3 is an E-ring configuration.
The groove and installation method must match the selected ring.
For global OEM sourcing, this comparison is especially important.
| Requirement | ASME B18.27 External NA1 | DIN 471 |
|---|---|---|
| Primary dimensional system | Inch | Metric |
| Installation location | Shaft | Shaft |
| General category | External retaining ring | External retaining ring |
| Standard family | ASME | DIN |
| Groove requirement | ASME/inch geometry | DIN/metric geometry |
| Typical sourcing context | U.S./inch equipment | European/global metric equipment |
| Automatic interchangeability | No | No |
ASME also maintains B27.7, which covers general-purpose tapered and reduced-cross-section retaining rings in metric dimensions.
Therefore:
ASME B18.27 → Inch Series
ASME B27.7 → Metric Series
ASME currently lists B27.7-1977 (S2022) as remaining in effect under stabilized maintenance.
This distinction can be useful for U.S.-standard equipment using either inch or metric retaining-ring systems.
ASME also maintains B27.6, covering general-purpose uniform-cross-section spiral retaining rings.
A spiral retaining ring differs substantially from a conventional tapered-section lugged circlip.
Potential differences include:
cross-section geometry;
installation method;
rotational balance;
groove interaction.
Therefore:
Conventional Circlip ≠ Spiral Retaining Ring
The correct architecture depends on the application.
ASME inch-series retaining rings may appear in:
North American machinery;
automotive production equipment;
pumps;
motors;
actuators;
drive systems;
thermal-management equipment.
Safety-critical vehicle applications require the applicable customer specification and qualification.
ASME B18.27 retaining rings can be relevant to:
machine tools;
conveyor equipment;
packaging machinery;
material-handling systems;
industrial drives;
bearing housings;
rotating equipment.
They are particularly relevant where the machine architecture uses inch-series shafts.
Potential uses include axial retention of appropriate:
bearings;
sleeves;
spacers;
shaft-mounted components.
The retaining ring itself is not a fluid seal.
External retaining rings may locate shaft-mounted components in suitable motor designs.
Rotational speed and rotor dynamics should be considered separately from basic dimensional fit.
Potential retained components include:
bearings;
gears;
spacers;
sleeves.
The ring provides axial retention.
It should not automatically be treated as the primary torque-transmission feature.
Potential applications include:
fans;
blowers;
pumps;
motors;
compressors;
actuators.
The retaining ring provides mechanical retention rather than vibration isolation or sealing.
Mechanical equipment within AI data center and HPC infrastructure can include:
pumps;
fans;
blowers;
motors;
liquid-cooling equipment.
ASME inch-series retaining rings may be relevant where the underlying mechanical component uses an inch shaft-retention architecture.
The data-center application itself does not determine the ring specification.
Potential applications may include appropriate:
motors;
generators;
pumps;
auxiliary machinery.
The actual shaft, groove, speed and axial-load requirements should control selection.
North American mobile equipment may contain inch-series retaining components in:
transmissions;
hydraulic systems;
drive equipment;
bearings;
actuators.
Shock and cyclic loading should be evaluated where relevant.
Material and surface treatment should account for:
moisture;
salt exposure;
galvanic interaction;
maintenance environment.
Do not assume a standard spring-steel retaining ring is suitable for every marine environment.
A generic ASME B18.27 industrial retaining ring should not automatically be represented as aerospace-qualified hardware.
Aerospace programs may require dedicated:
aerospace standards;
approved materials;
traceability;
inspections;
supplier qualification.
Drawing-based tooling, ground-support and appropriate MRO requirements can be evaluated according to customer specifications.
| Requirement | Engineering Direction |
|---|---|
| External inch shaft groove | Evaluate NA1 or another applicable external B18.27 type |
| Internal inch housing groove | Evaluate NA2 or another applicable internal type |
| Radial-install E-ring architecture | Evaluate NA3 family where applicable |
| Heavy-duty external requirement | Evaluate NA4 |
| Metric DIN shaft | Evaluate DIN 471 |
| Metric ASME retaining-ring system | Review ASME B27.7 |
| Spiral ring architecture | Review ASME B27.6 |
| High rotational speed | Evaluate ring geometry and RPM requirements |
| High axial load | Check ring, groove and shaft |
| Corrosive environment | Select appropriate material / finish |
| Legacy U.S. equipment | Identify original standard and inch dimensions |
| Unknown used sample | Measure sample and groove before replacement |
Use the actual applicable ASME B18.27 designation and ring type rather than relying on ambiguous legacy terminology.
The standard covers multiple NA ring types.
The groove and axial load also matter.
Approximate diameter conversion does not establish equivalence.
The groove is part of the retention system.
Its primary function is axial retention.
The primary retaining function is axial.
Torque transmission normally requires the appropriate shaft-drive feature.
Rotating equipment may require additional ring-geometry evaluation.
Permanent deformation can compromise seating.
Service and installation can permanently change the ring.
The groove and complete assembly must match the selected type.
Engineers may search:
ASME B18.27 retaining ring;
ASME external retaining ring;
NA1 retaining ring;
inch retaining ring;
inch shaft circlip;
external snap ring inch;
retaining ring groove dimensions;
ASME circlip standard;
ASME B18.27 vs DIN 471;
NA1 vs NA4 retaining ring;
inch shaft retaining ring;
high speed retaining ring.
These searches often indicate an active engineering, replacement or troubleshooting task.
Procurement teams may search:
ASME B18.27 supplier;
NA1 retaining ring supplier;
inch retaining ring manufacturer;
external retaining ring supplier USA standard;
inch circlip manufacturer;
spring steel retaining ring supplier;
stainless retaining ring supplier;
OEM retaining ring manufacturer;
legacy retaining ring replacement;
custom inch retaining ring supplier.
These searches indicate stronger commercial sourcing intent.
For technical and commercial evaluation by JUXIN FASTENERS, provide where applicable:
ASME B18.27 designation;
ring type, such as NA1;
nominal inch shaft size;
customer part number;
original drawing;
shaft drawing;
groove diameter;
groove width;
groove location;
shaft material;
shaft hardness where relevant;
retained component;
expected axial load;
static or cyclic load condition;
shock or impact requirement;
rotational speed where relevant;
operating temperature;
corrosion environment;
ring material;
surface finish;
installation method;
removal and service requirement;
dimensional tolerances;
inspection requirements;
documentation requirements;
legacy sample where applicable;
sample quantity;
prototype quantity;
production quantity;
estimated annual demand;
packaging requirement;
labeling requirement;
customer-specific requirements.
ASME B18.27 covers tapered and reduced-cross-section retaining rings in inch-series dimensions.
The current listed standard is ASME B18.27-1998 (S2022).
NA1 is the external retaining-ring type listed in ASME B18.27 for shaft applications.
No. It includes external, internal, E-ring, heavy-duty, bowed, inverted, beveled and other retaining-ring configurations.
NA1 is an external ring for shaft applications. NA2 is an internal ring for housing or bore applications.
NA1 is the conventional external type, while NA4 is the heavy-duty external type within the ASME B18.27 family.
ASME B18.27 covers inch-series retaining rings and multiple configurations. DIN 471 covers metric retaining rings for shafts. They should not be treated as automatically interchangeable.
ASME B18.27 is the inch-series standard, while ASME B27.7 covers metric general-purpose tapered and reduced-cross-section retaining rings.
No. Their primary function is mechanical axial retention.
They should not be treated as radial bearings. Their primary retaining function is axial.
It should not automatically be used as the primary torque-transfer feature. Keys, splines, interference fits or other features may be required.
Not based on nominal diameter conversion alone. Ring geometry, groove dimensions, tolerances and the complete assembly should be checked.
They can be used in rotating systems, but rotational speed, ring geometry and equipment balance should be evaluated for the actual application.
JUXIN FASTENERS can evaluate standard, legacy and drawing-based retaining-ring requirements using the applicable ring type, shaft and groove dimensions, material, finish and production quantity.
A buyer may initially request:
“External retaining ring for 1-inch shaft, 50,000 pcs.”
That does not completely define the part.
The supplier may still need to know:
ASME B18.27 or Another Standard?
NA1 or Another Ring Type?
What Is the Actual Shaft Diameter?
What Is the Groove Diameter?
What Is the Groove Width?
What Component Is Being Retained?
What Axial Load Must Be Carried?
What RPM Applies?
What Material Is Required?
What Surface Finish Is Required?
Is This a New Design or Legacy Replacement?
The sourcing path becomes:
Drawing / Application → Inch Shaft → ASME B18.27 Type → Groove → Axial Load → RPM → Material / Finish → Sample Verification → Validation → Production RFQ
This is the difference between sourcing a ring that simply fits an inch shaft and sourcing the correct retaining system for the actual equipment.
JUXIN FASTENERS supports OEM and replacement sourcing for:
ASME B18.27 retaining rings;
External Type NA1 retaining rings;
inch-series external retaining rings;
inch shaft circlips;
external snap rings;
heavy-duty retaining rings where specified;
spring-steel retaining rings;
stainless steel retaining rings;
legacy replacement retaining rings;
drawing-based retaining components.
Potential application sectors include:
industrial machinery;
North American OEM equipment;
automotive and EV equipment;
electric motors;
gearboxes;
pumps and compressors;
industrial automation;
HVAC equipment;
AI data center and HPC cooling equipment;
power equipment;
construction machinery;
agricultural machinery;
material-handling systems;
marine equipment;
MRO and legacy machinery.
For metric external shaft-retaining systems, refer to the JUXIN FASTENERS DIN 471 External Retaining Rings: Shaft Groove, Axial Load & Selection Guide.
For internal bore-retaining systems, refer to the JUXIN FASTENERS DIN 472 Internal Retaining Rings: Bore Groove, Axial Load & Selection Guide.
For bearing preload rather than simple axial retention, refer to the JUXIN FASTENERS Bearing Preload Wave Washers: Load, Working Height, Tolerance Stack & Selection Guide.
For custom shaft and groove components, see Stainless Steel CNC Machining Parts.
For OEM ASME B18.27 retaining-ring RFQs, send the standard designation, ring type, drawing, inch shaft size, groove dimensions, shaft material, axial load,
rotational speed where relevant, material, finish, quantity and estimated annual demand to:
For ASME inch-series retaining rings, the correct sourcing question is not simply:
“What ring fits this shaft?”
It is:
“Which ASME B18.27 ring type, shaft groove and material combination matches the actual axial-retention requirement?”
 MORE NEWS

Sep. 27, 2026

Sep. 27, 2026

Sep. 27, 2026
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY