
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Aug. 26, 2023
Blind threaded studs provide an efficient way to create a permanent external threaded mounting point in sheet metal, hollow sections,
tubular structures and industrial assemblies where access is available from only one side.
Also known as blind rivet studs, externally threaded blind studs or blind-install threaded studs,
these fasteners combine the mounting function of an external threaded post with the installation advantages of blind fastening technology.
Unlike conventional welded studs, compatible blind threaded studs can be mechanically installed without introducing welding heat at the mounting location.
Unlike blind rivet nuts, which provide internal female threads, blind threaded studs present an external male thread that allows a bracket,
cover, spacer or other component to be positioned over the stud and secured with a mating nut.
This difference can influence the entire assembly architecture, including component positioning, production sequence, installation access, serviceability and fastening cost.
For OEM engineers, the most important consideration is not simply selecting a thread diameter.
Reliable performance depends on the complete installed joint, including the parent material, mounting hole, grip range, stud projection, installation method, loading conditions and mating hardware.
JUXIN FASTENERS supports drawing-based industrial fastening inquiries involving blind threaded studs, blind rivet studs and related custom fastening solutions.
This guide explains the engineering decisions that matter when selecting these products for production applications.
A blind threaded stud is a mechanically installed fastener that creates an external threaded post in a receiving panel or structure when the reverse side cannot be accessed during installation.
A typical design includes an externally threaded stud section, a deformable body or sleeve, a head or flange, and a blind-side forming zone.
During installation, the fastener is inserted into a prepared mounting hole.
A compatible installation tool then deforms the blind-side portion of the fastener to create mechanical retention against the rear surface of the parent material.
The external threaded section remains accessible for mounting the mating component.
The exact construction and deformation mechanism depend on the selected product design.
Blind threaded studs should therefore be specified by their actual geometry, installation method and performance requirements rather than by a generic product name alone.
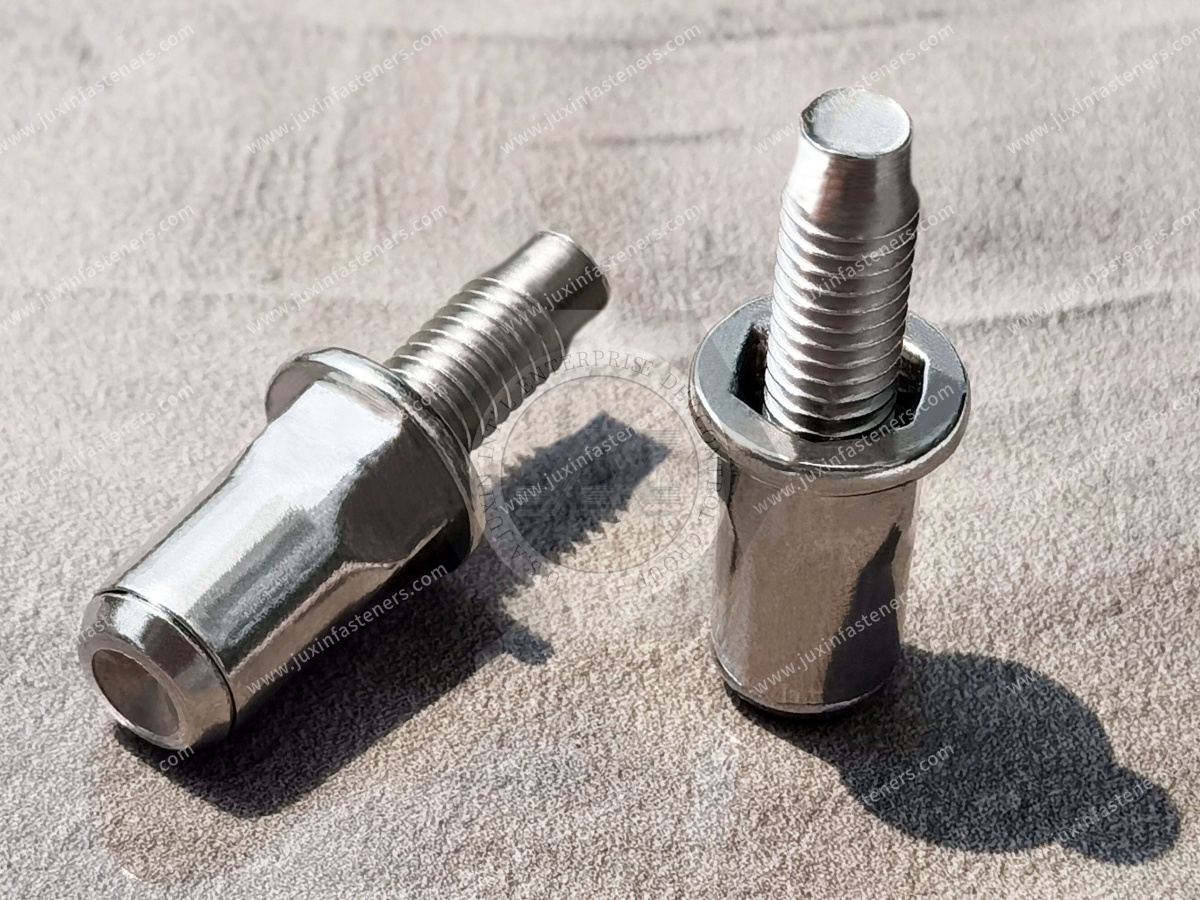
Both product families can be installed from one side, but they provide different threaded interfaces.
| Feature | Blind threaded stud | Blind rivet nut |
|---|---|---|
| Thread interface | External male thread | Internal female thread |
| Final mating hardware | Nut or compatible internally threaded component | Screw or bolt |
| Mounting architecture | Component positioned over exposed stud | Screw inserted into threaded hole |
| Installation access | One side | One side |
| Typical assembly advantage | Pre-positioned mounting post | Reusable internal threaded attachment |
| Primary design consideration | Stud projection, engagement and installed retention | Internal thread, grip and installed retention |
The choice affects more than the fastener itself.
An external stud may simplify positioning because a bracket can be placed over the existing threaded post before the mating nut is tightened.
An internal-threaded insert may be more suitable when a flush receiving surface or screw-in mounting arrangement is preferred.
The correct solution depends on the complete assembly design.
A fixed external mounting stud can change the sequence of an industrial assembly.
Consider a sheet-metal enclosure requiring several mounting brackets.
With a conventional bolt-and-nut arrangement, the assembly may require access to both sides or an operator to hold one component while the other is tightened.
With an appropriately designed blind threaded stud, the mounting post can be installed into the panel before the bracket is positioned.
The bracket is then placed over the exposed studs and secured using mating nuts.
This can provide several potential manufacturing advantages:
Easier component positioning during assembly
Reduced need for backside access
A defined external mounting interface
Potential simplification of assembly sequencing
Compatibility with selected pre-finished sheet-metal components
Reduced dependence on welding at the mounting location
Improved accessibility for certain maintenance operations
These benefits depend on the actual production layout and should not be treated as guaranteed cycle-time reductions.
For manufacturing engineers and production managers,
the practical question is whether the blind stud simplifies the complete assembly process while meeting mechanical and quality requirements.
Blind threaded studs rely on controlled mechanical deformation to establish retention in the parent structure.
The fastener is inserted through a correctly sized mounting hole.
A compatible installation system then forms or collapses the designated blind-side portion of the fastener.
This creates a mechanical interlock between the accessible-side head or flange, the parent material and the formed blind-side section.
After installation, the exposed external thread is available for final assembly.
Depending on the specific fastener design, installation may use a spin/pull mechanism or another dedicated mechanical setting method.
Not every blind threaded stud uses the same installation principle.
Tool compatibility must be confirmed against the actual fastener configuration.
A blind threaded stud should not be evaluated as an isolated metal component.
Its performance depends on the interaction of:
Stud geometry + mounting hole + parent material + installation process + mating hardware + applied load.
Changing any of these elements can change the behavior of the finished joint.
For example, a stud that performs well in a steel test panel may behave differently when installed into a thinner aluminum panel.
Similarly, a stud installed with an incorrect setting stroke may have insufficient retention even if its external thread dimensions are correct.
The mounting hole is a critical functional feature.
If the hole is undersized, the fastener may be difficult to insert or may damage the surrounding material.
If the hole is oversized, the intended mechanical engagement may be reduced.
Hole quality can also affect installation consistency.
Engineers should consider:
Nominal hole diameter
Hole tolerance
Hole roundness
Burrs and sharp edges
Local sheet distortion
Drilling or punching quality
Coating thickness
Hole location relative to adjacent features
The correct hole dimensions should come from the selected fastener specification or approved engineering drawing.
A generic hole-size recommendation should not be transferred between different blind stud designs without verification.
A blind stud installed near a panel edge, bend, cutout or adjacent hole may experience different local stiffness and deformation behavior from one installed in an uninterrupted flat panel.
Insufficient edge distance can increase the risk of local yielding, cracking or pull-through.
The required edge distance should therefore be established according to the actual panel geometry and expected loading.
For formed sheet-metal parts, the designer should also confirm that installation tooling can access the mounting location without interfering with nearby bends or structural features.
Grip range is one of the most important dimensions in blind stud selection.
It defines the receiving-material thickness condition for which the fastener is designed.
The selected grip range must accommodate the actual installation stack-up and relevant manufacturing tolerances.
A product intended for one sheet thickness may not form correctly in a significantly thinner or thicker material.
The installation condition may involve a single sheet or multiple layers.
Where multiple layers are present, the engineer must identify which layers are captured by the blind-side forming mechanism.
A bracket installed later over the exposed stud should not automatically be counted as part of the stud's installation grip.
The distinction between the receiving structure and the subsequently mounted component is important.
The grip specification should reflect the actual material captured during setting.
Surface coatings can affect the effective thickness and contact conditions.
For pre-painted or coated sheet metal, the installation process should be evaluated for possible coating damage, local indentation and dimensional variation.
Mechanical installation avoids welding heat, but it does not automatically eliminate surface damage.
The external thread is the functional mounting interface.
Its specification must match the mating nut and the complete joint requirements.
Important parameters include:
Thread system
Nominal diameter
Pitch or threads per inch
Thread tolerance
Usable threaded length
Mating nut specification
Required engagement
Corrosion protection and coating effects
For metric threaded products, ISO 261 and ISO 965 may be relevant to thread designation and tolerance requirements.
For Unified inch-series threads, ASME B1.1 may apply.
UNC and UNF threads must be specified correctly.
Metric threads are not directly interchangeable with UNC or UNF threads simply because their nominal diameters appear similar.
British Whitworth systems such as BSW and BSF also require their own correct specifications.
For replacement-part sourcing, the exact mating thread must be verified.
International OEM buyers may work with both metric and inch-based drawings.
For dimensional reference:
| Metric dimension | Approximate inch equivalent |
|---|---|
| 5 mm | 0.197 in |
| 6 mm | 0.236 in |
| 8 mm | 0.315 in |
| 10 mm | 0.394 in |
These values are dimensional conversions only.
They do not establish equivalent UNC, UNF, BSW or BSF thread specifications.
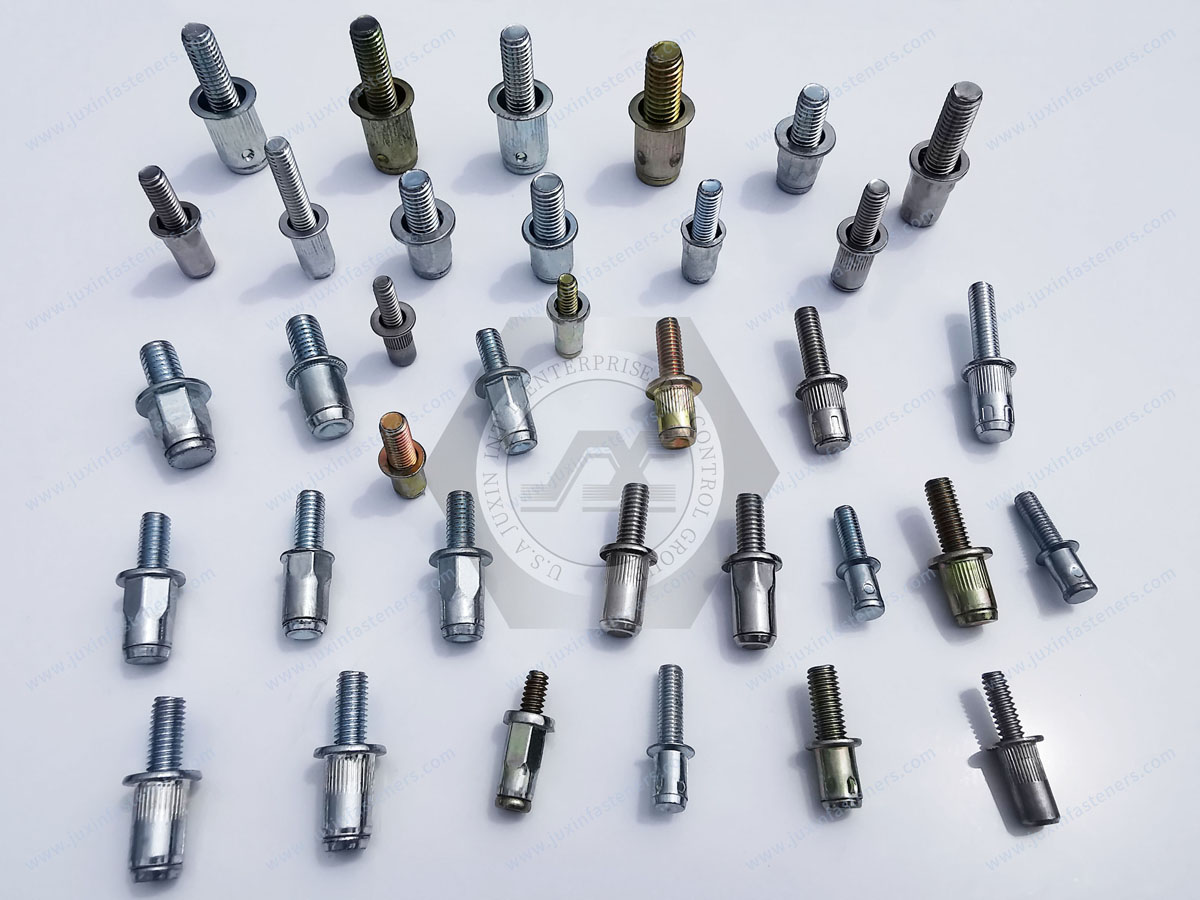
Stud length should be selected according to the complete assembly stack-up.
The required exposed length depends on the thickness of the mounted component, washer arrangement, mating nut, thread engagement and surrounding clearance.
A practical design review should distinguish between:
Overall stud length: The complete physical length of the fastener.
Threaded length: The portion carrying the external thread.
Exposed projection: The length available above the installed panel.
Usable engagement length: The portion available to engage the mating component after accounting for assembly geometry.
These dimensions are related but not interchangeable.
An unnecessarily long exposed stud can interfere with nearby components or complicate packaging.
It can also increase bending effects when the applied load is offset from the panel.
An excessively short stud may prevent the mating nut from achieving the required engagement.
The correct length is therefore determined by the joint design, not by selecting the longest available stud.
A major engineering mistake is to describe blind threaded stud performance using only one generic strength value.
The installed joint can experience several different failure mechanisms.
Axial pull-out describes loading that tends to remove the installed fastener from the parent material.
The result depends on the blind-side mechanical interlock, installation condition, parent-material properties and hole geometry.
Pull-through occurs when the fastener or its retaining geometry moves through the receiving material.
In thin or relatively soft panels, local material deformation may govern joint performance.
The metal stud may remain intact while the parent panel fails.
Shear acts laterally across the fastening interface.
The load path can involve the stud, mating component, parent panel and local bearing surfaces.
A blind stud suitable for axial mounting should not automatically be assumed suitable for a demanding lateral load.
Bending becomes important when the applied load is offset from the panel.
For a simplified cantilevered loading condition:
Bending moment = applied transverse force × effective lever arm
This relationship explains why stud projection and bracket geometry matter.
A longer unsupported projection can increase the moment applied to the fastener and its installation interface.
Actual stress and deflection depend on the complete geometry, material properties and boundary conditions.
A high-strength external thread does not automatically create a high-strength installed joint.
The governing failure mode may be:
Stud fracture
Thread stripping
Blind-side retention failure
Parent-panel yielding
Hole enlargement
Pull-through
Bending deformation
Fatigue under repeated loading
Engineering qualification should identify the relevant failure modes rather than assuming that the strongest individual component controls the assembly.
Welded studs and mechanically installed blind threaded studs can both create external mounting posts, but they use fundamentally different retention mechanisms.
A weld stud is attached through a welding process.
A blind threaded stud relies on mechanical deformation and engagement with the parent material.
| Engineering consideration | Blind threaded stud | Weld stud |
|---|---|---|
| Installation principle | Mechanical blind installation | Welding |
| Backside access | Generally not required for compatible designs | Depends on welding process and joint |
| Local welding heat | Not introduced by the stud-setting process | Introduced during welding |
| Pre-coated panel compatibility | Requires installation validation | May require coating removal or repair |
| Retention mechanism | Mechanical interlock | Welded connection |
| Load capacity | Depends on fastener and parent-panel system | Depends on stud, weld and parent material |
| Process equipment | Compatible setting tool | Appropriate welding equipment |
| Substitution | Requires joint validation | Requires joint validation |
A blind threaded stud can be an attractive alternative when welding access is restricted or a pre-finished surface should be preserved.
However, a mechanical blind stud should not be presented as a universal replacement for a welded stud.
The two solutions may have different fatigue behavior, load capacity, joint stiffness and production requirements.
Material selection affects installation behavior, thread performance, corrosion resistance and manufacturing compatibility.
Carbon steel is a common industrial fastener material.
Depending on the product design and material specification, it may provide a practical combination of strength, formability and cost.
Applications can include equipment brackets, industrial enclosures, machinery covers and sheet-metal assemblies.
The required surface treatment should be specified according to the actual environment.
Stainless steel may be considered where corrosion resistance or material compatibility is important.
However, the exact grade and product construction must be confirmed.
Stainless steel is not a single universal material specification.
Different grades have different mechanical and corrosion properties.
Because blind threaded studs require controlled deformation during installation, material substitutions can also affect setting behavior.
Where applicable, ISO 3506 may provide relevant stainless steel fastener material and mechanical classification requirements within its defined scope.
Its applicability should be checked against the exact finished product.
Aluminum alloys may be considered for weight-sensitive assemblies when the selected fastener design and application requirements permit.
However, aluminum should not be assumed mechanically equivalent to steel.
Relevant factors include thread durability, installation deformation, joint loading and galvanic compatibility.
Any material substitution should be validated using the actual parent structure and mating hardware.
The surface finish should be selected as part of the complete assembly.
Potential coating systems may include zinc-based finishes, zinc-nickel coatings or other customer-specified protective treatments, depending on material and manufacturing compatibility.
The appropriate specification depends on the intended service environment.
For example, an indoor electrical enclosure and an outdoor industrial equipment assembly may have different corrosion requirements.
Dissimilar metals can create galvanic corrosion risks when an electrolyte is present.
This may be relevant when combining steel, stainless steel or plated fasteners with aluminum panels.
The engineer should consider material pairing, coating continuity, moisture retention, drainage and the expected exposure environment.
ASTM B117 provides a laboratory salt-spray testing method.
However, a salt-spray exposure duration should not be interpreted by itself as a direct prediction of real-world service life.
Corrosion requirements should identify the relevant coating system, test method and acceptance criteria.
Blind threaded stud assemblies may experience repeated mechanical and environmental loading.
Automotive equipment, HVAC systems and industrial machinery can introduce vibration, temperature variation and cyclic loads.
Potential concerns include:
Mating nut loosening
Joint movement
Stud bending fatigue
Panel deformation
Loss of retention
Differential thermal expansion
Coating degradation
The appropriate locking strategy should be selected according to the mating hardware and application.
A prevailing-torque locknut or other retention method may be considered where compatible with the joint design.
However, using a locking nut does not compensate for inadequate blind-stud retention in the parent material.
For demanding applications, vibration and thermal-cycle validation should use representative assemblies.
Thin sheet-metal assemblies are among the most relevant applications for blind threaded studs.
When the sheet is too thin to provide sufficient tapped-thread engagement, an installed threaded fastener can create a dedicated mounting interface.
Potential applications include electrical cabinets, industrial enclosures, HVAC equipment, machinery covers, appliance panels and equipment brackets.
The design must account for panel thickness, material strength, local stiffness and hole quality.
A thin panel may fail through local deformation even when the stud itself has adequate strength.
Where necessary, engineers should evaluate reinforcement, alternative fastener geometry or a different mounting architecture.
Blind threaded studs can be considered for selected vehicle brackets, equipment covers, shields, compartment components and accessory mounting points.
Potential benefits include single-sided installation and external threaded positioning.
Automotive applications may require evaluation of vibration, corrosion, temperature cycling and manufacturing consistency.
Safety-critical or highly loaded vehicle applications require the appropriate engineering qualification.
Electrical enclosures and control cabinets often use sheet-metal structures with limited internal access.
Blind threaded studs can provide mounting points for brackets, cable-management components, covers and equipment supports.
Where environmental sealing is required, the complete enclosure must be evaluated.
A blind threaded stud is not automatically waterproof or IP-rated.
For ingress-protection requirements, IEC 60529 may be relevant to the complete enclosure.
HVAC systems use formed sheet-metal panels, brackets, housings and serviceable components.
External mounting studs may help simplify assembly in locations where rear-side access is restricted.
The material and finish should be selected according to condensation, moisture, temperature and other relevant service conditions.
Industrial equipment may use blind threaded studs for guards, covers, control cabinets, mounting plates and support brackets.
The assembly design should account for service loads, vibration, access requirements and maintenance procedures.
Appliance production often involves thin, formed and pre-finished sheet metal.
Mechanically installed studs may be considered where a fixed external mounting point is advantageous.
Production engineers should validate installation quality and any potential effects on visible or coated surfaces.
Hollow sections can restrict access to the reverse side of a mounting location.
A compatible blind threaded stud can establish an external threaded post without requiring conventional access to an internal nut.
However, internal clearance, wall thickness and local structural geometry must be confirmed.
Blind threaded studs may be considered for selected nonmetallic substrates, but the material behavior differs from steel.
Plastics and composites can experience local crushing, creep, stress relaxation, cracking or delamination.
The installation process and joint performance should be evaluated using the actual substrate construction.
The installation tool must be compatible with the selected blind stud.
Relevant variables can include tool alignment, forming force, stroke, stud geometry and receiving-material thickness.
Incorrect installation can affect both retention and external thread integrity.
If the blind-side section does not form correctly, the installed fastener may have inadequate mechanical engagement.
Possible symptoms include movement, rotation or inconsistent seating.
Excessive setting can damage the fastener or receiving material.
Potential consequences include panel deformation, thread damage, coating damage and local cracking.
For repetitive OEM assembly, manufacturing engineers should evaluate:
Installation cycle time
Tool compatibility and accessibility
Fastener feeding and handling
Hole-position consistency
Setting-process repeatability
Operator training
Inspection and rejection criteria
Rework procedures
Tool maintenance
Production traceability requirements
A fastener that is easy to install during prototyping may still require process development before high-volume production.
Qualification should evaluate the fastener as part of the complete joint.
Depending on the application, testing may include axial retention, pull-through, rotation resistance, shear, bending, vibration, fatigue and corrosion exposure.
Not every project requires every test.
The validation plan should reflect the actual service loads, environment and customer specifications.
Testing should use representative parent material, thickness, hole geometry and installation conditions.
A result obtained from one substrate should not be transferred automatically to another.
When a mating nut is tightened, the installed stud may experience torque.
Rotation resistance depends on the body geometry, hole and parent material.
It should be evaluated separately from axial pull-out performance.
The external thread should be inspected according to its specified thread system and tolerance.
Depending on the requirement, inspection may include thread gauges, dimensional measurements and functional mating checks.
Not every dimension has equal importance.
Typical critical characteristics can include:
External thread geometry
Stud projection
Overall length
Head or flange dimensions
Body diameter
Grip-related dimensions
Installation hole compatibility
Material and surface finish
The inspection plan should follow the approved drawing and agreed quality requirements.
Blind threaded studs do not have one universal standard that covers every design and installation method.
Applicable requirements should be selected according to the exact product.
Potentially relevant standards include:
ISO 261: General-purpose metric screw-thread designation.
ISO 965: Metric screw-thread tolerances.
ASME B1.1: Unified inch screw threads.
ISO 3506: Applicable corrosion-resistant stainless steel fastener material and mechanical property classifications, subject to product scope.
ASTM B117: Salt-spray testing method where specified.
These standards address different aspects of the specification.
A thread standard is not a finished-fastener performance standard.
A material standard is not automatically an installation qualification.
A corrosion test method is not proof of a particular service life.
For drawing-based OEM products, the approved customer specification should identify the applicable requirements.
Unrelated standards should not be assigned merely to make a product appear standardized.
A practical blind threaded stud selection process should follow the actual assembly requirements.
Define the mounting architecture. Confirm that an external threaded post is preferable to an internal threaded insert or through-bolt.
Identify the receiving structure. Record material, thickness, coating and local geometry.
Specify the mounting hole. Establish the required diameter, tolerance and hole-making process.
Select the grip range. Match the fastener to the actual receiving-material thickness and stack-up.
Define the external thread. Specify the exact thread system, size, pitch and tolerance.
Determine stud projection. Account for the mating component, washer, nut and required engagement.
Evaluate loads. Consider axial retention, pull-through, shear, bending and cyclic loading.
Review the environment. Identify moisture, corrosion, temperature and chemical exposure.
Confirm installation tooling. Validate the setting process using representative production parts.
Define procurement requirements. Establish drawing revision, material, finish, inspection, packaging and expected production volume.
This process helps convert a generic product search into a controlled engineering specification.
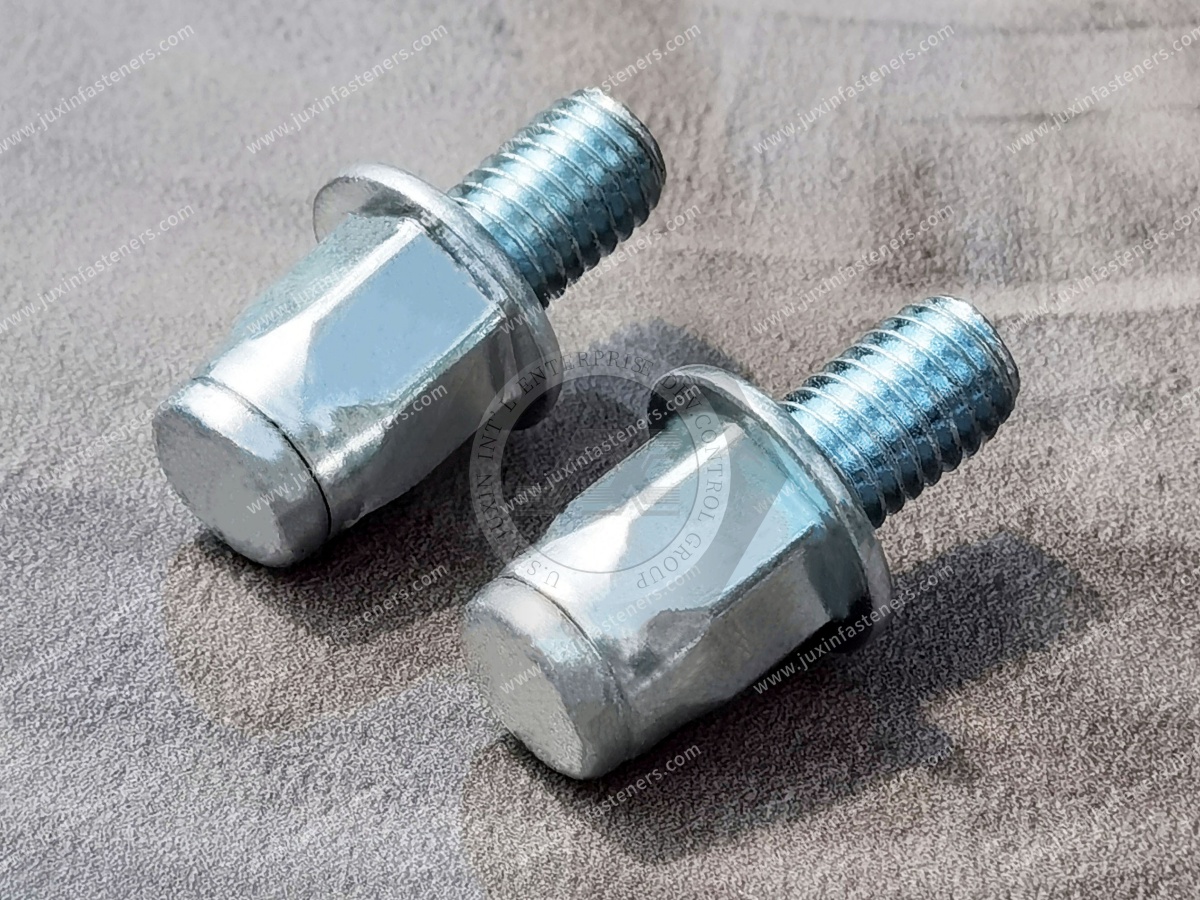
Standard catalog products may not match every OEM assembly.
A customer-specific blind threaded stud may require evaluation of:
External thread designation
Usable threaded length
Overall length
Head diameter and thickness
Body geometry
Grip range
Blind-side forming characteristics
Material
Surface treatment
Critical dimensional tolerances
Installation method
Custom geometry should be assessed for both manufacturing feasibility and installed performance.
For example, increasing stud projection may affect bending behavior.
Changing head geometry may alter the contact pressure on the panel.
Changing material may affect the forming process.
These design variables should be reviewed together rather than treated as independent substitutions.
For industrial purchasing teams, blind threaded studs should be sourced as engineering-controlled components.
Two products with the same nominal thread size may have different grip ranges, head geometries, installation requirements and mechanical behavior.
Comparing quotations only by thread diameter and unit price can therefore produce misleading results.
A more effective supplier evaluation considers:
| Evaluation area | Key procurement question |
|---|---|
| Drawing interpretation | Does the proposed product match the controlled drawing? |
| Thread compatibility | Is the exact thread system and tolerance correct? |
| Grip range | Is the product compatible with the production panel? |
| Installation | Can the specified product be installed using the approved process? |
| Material | Is the required material clearly defined? |
| Surface treatment | Does the finish meet the application specification? |
| Inspection | Are critical characteristics and acceptance criteria agreed? |
| Production planning | Are volume, MOQ and lead-time expectations confirmed? |
| Documentation | Are the required records and traceability arrangements defined? |
| Change control | Will critical product changes require customer approval? |
MOQ, lead time, manufacturing arrangements and documentation availability should be confirmed for each specific inquiry.
They should not be assumed from a generic product description.
The lowest unit price does not necessarily produce the lowest installed cost.
The purchasing decision may also be affected by tooling, installation labor, rework, scrap, inspection and assembly reliability.
A mechanically installed blind stud may reduce certain welding-related operations in a suitable application.
However, any claimed cost advantage should be evaluated against the actual production process.
A prototype should reproduce the intended production joint as closely as practical.
Important variables include the receiving material, thickness, hole specification, stud design, installation tool and mating hardware.
After approval, changes to these variables may affect the installed performance.
Engineering and procurement teams should agree on which characteristics require formal change control.
Depending on customer requirements, these may include material, geometry, surface finish, thread specification, grip range and installation method.
Packaging and part identification should also prevent thread damage, surface damage, mixed part numbers and lot confusion.
What is the difference between a blind threaded stud and a blind rivet nut?
A blind threaded stud provides an external male threaded post. A blind rivet nut provides an internal female threaded hole.
Both can support one-sided installation, but they use different mating hardware and assembly arrangements.
Can blind threaded studs replace welded studs?
They may be considered as an alternative in selected applications.
However, the retention mechanism, loading behavior and manufacturing process differ, so engineering validation is required.
Are blind threaded studs suitable for thin sheet metal?
Yes, compatible designs can provide mounting points in selected thin sheet-metal assemblies.
The actual panel thickness, hole, grip range and loading must be verified.
Can blind threaded studs be installed in hollow sections?
Certain designs are suitable for hollow sections where backside access is restricted.
Internal clearance and local wall geometry must be checked.
Are blind threaded studs waterproof?
Not automatically. Blind installation describes access, not sealing performance.
Any sealing requirement must be addressed by the specific fastener and complete assembly design.
What determines blind threaded stud pull-out resistance?
Pull-out resistance depends on fastener geometry, parent material, hole dimensions, grip condition and installation quality.
Why does exposed stud length matter?
Exposed length affects mating-component engagement, assembly clearance and bending behavior under offset loads.
Can metric blind threaded studs replace UNC or UNF versions?
Not directly. Metric and Unified inch-series threads have different specifications and require correct mating hardware.
What should an OEM buyer provide for a blind threaded stud quotation?
A controlled drawing, thread specification, dimensions, panel material, grip range, mounting-hole information,
finish requirements, application conditions and expected quantities are useful starting points.
Are you sourcing blind threaded studs, blind rivet studs, externally threaded blind fasteners or custom threaded mounting studs for an industrial OEM application?
JUXIN FASTENERS can review your drawings and technical requirements to help clarify the appropriate fastening configuration.
For an efficient engineering and procurement discussion, please provide:
2D drawing and 3D model, if available
External thread size, pitch and tolerance
Overall length and usable thread length
Head or flange dimensions
Parent material and thickness
Mounting-hole diameter and tolerance
Required grip range
Material and surface-treatment requirements
Mating component and loading conditions
Installation process requirements
Environmental and validation requirements
Prototype quantity or estimated annual demand
Required inspection, packaging and documentation
For replacement-part inquiries, an existing manufacturer part number or reference drawing may also be helpful.
Company: JUXIN FASTENERS
Website: https://www.juxinfasteners.com/
Email: info@juxinfasteners.com
Send your technical drawings and RFQ to JUXIN FASTENERS to discuss blind threaded stud selection, OEM customization and industrial sourcing requirements.
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY



