
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Sep. 27, 2023
DIN 9250 carbon steel safety washers are mechanical locking components used in bolted joints where vibration, shock, cyclic loading and demanding service conditions can increase the risk of rotational loosening.
Compared with stainless steel versions selected primarily where corrosion resistance is a major material requirement,
hardened carbon or alloy steel safety washers can be particularly relevant to heavy-duty industrial assemblies where mechanical strength,
hardness, surface interaction and compatibility with high-strength fasteners are important design considerations.
For engineering and procurement teams, however, selecting a DIN 9250 washer involves more than matching the nominal bolt diameter.
Washer material, hardness, coating, bolt preload, mating-surface hardness, tightening friction, vibration direction and environmental exposure all influence joint performance.
JUXIN FASTENERS supplies DIN 9250 carbon and alloy steel safety washers together with other vibration-resistant fastening components for industrial OEM, Tier-1 and engineered equipment applications.
For drawings, specifications, coating requirements and RFQs, contact info@juxinfasteners.com.
A DIN 9250 safety washer is a locking element installed beneath a bolt head or nut to increase resistance to unintended rotational loosening.
Depending on market terminology and application, buyers may search for these components as:
DIN 9250 safety washers
DIN 9250 lock washers
carbon steel lock washers
heavy-duty safety washers
toothed safety washers
anti-loosening washers
vibration-resistant washers
locking washers for bolts
zinc-flake coated lock washers
The washer incorporates formed locking features intended to interact mechanically with the adjacent fastener and mating surfaces after tightening.
This differentiates it from a conventional flat washer, whose principal function is generally load distribution rather than rotational locking.
DIN 9250 safety washers should also not be confused with wedge-lock washer pairs. Both technologies may be used in vibration-resistant bolted joints,
but their geometries and locking mechanisms differ. The required standard, drawing and validated joint performance should determine which technology is appropriate.
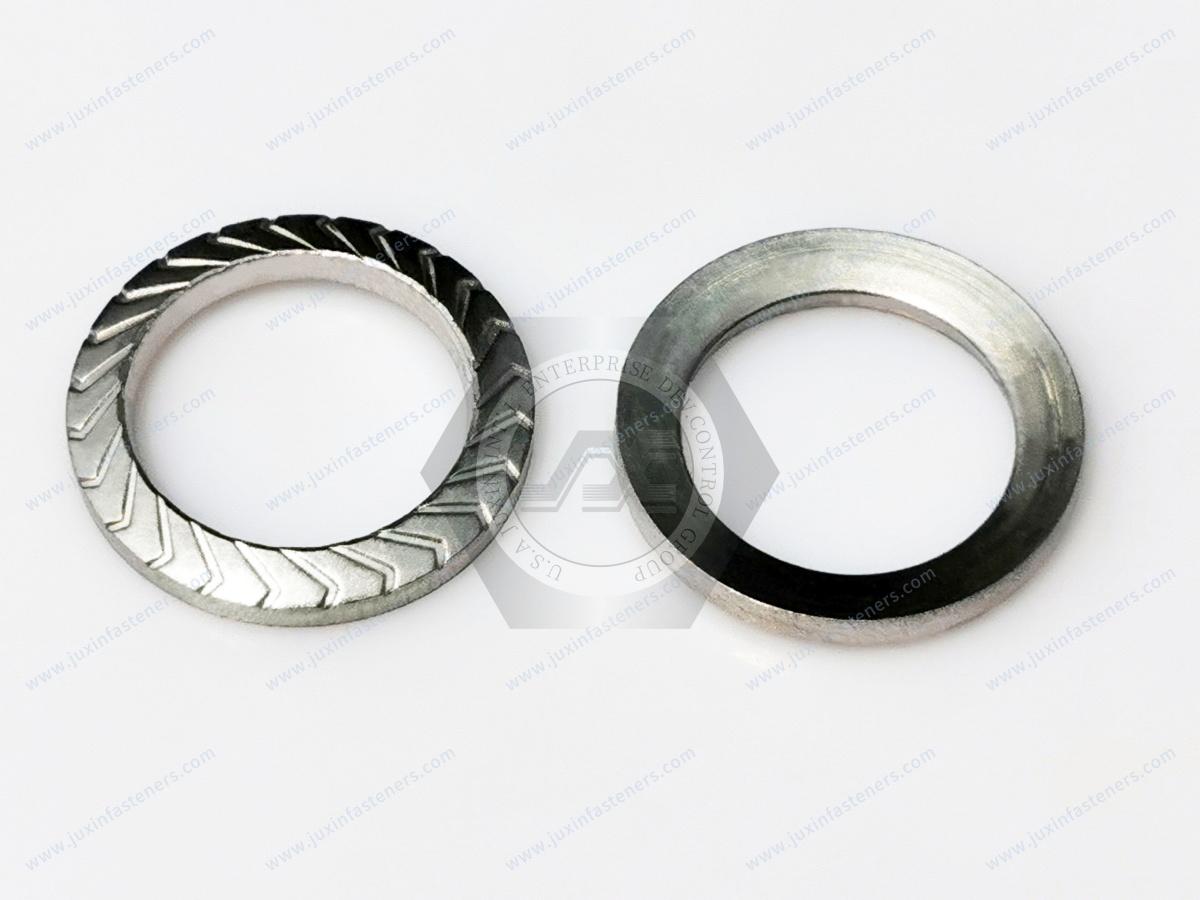
For demanding bolted connections, washer material selection affects hardness, elastic behavior, wear resistance, locking-interface performance and compatibility with the surrounding fasteners.
Carbon and alloy spring steels can provide a useful combination of:
high hardness after controlled heat treatment
resistance to permanent deformation
mechanical durability
stable locking geometry
compatibility with demanding industrial bolted joints
suitability for engineered corrosion-protection coatings
Material selection should nevertheless be based on the approved DIN requirement, customer drawing or application-specific specification.
Depending on the required design, materials may include suitable carbon or alloy spring steels such as 51CrV4-type material or other approved grades with the required heat-treatment response and mechanical characteristics.
Equivalent substitutions should not be made solely on the basis of nominal chemistry. Mechanical properties, heat treatment, hardness and finished washer performance should also be confirmed.
The decision between carbon/alloy steel and stainless steel should not be reduced to the assumption that one material is universally better.
They solve different sourcing and engineering priorities.
Often considered when the application prioritizes:
high hardness
demanding mechanical loading
heavy machinery
compatibility with high-strength bolted assemblies
engineered coated surfaces
cost-effective high-volume OEM production
Often considered when the application prioritizes:
corrosion resistance
humid environments
outdoor exposure
foodservice equipment
certain chemical environments
reduced dependence on an applied protective coating
The correct choice depends on the complete bolted joint.
A hardened carbon steel washer with a suitable zinc-flake coating may provide an effective solution in one outdoor industrial assembly,
while an A4 stainless steel washer may be more appropriate in another environment with persistent chloride exposure.
Material selection should therefore combine mechanical requirements and environmental requirements, rather than considering either factor independently.
When a bolted joint is tightened, bolt elongation generates preload and clamps the joint members together.
Vibration becomes especially problematic when external forces create relative movement across the joint interface.
DIN 9250 safety washers introduce additional mechanical resistance at the bearing interfaces beneath the nut or bolt head. Their formed locking geometry is designed to resist relative rotation after tightening.
However, the washer does not generate correct bolt preload by itself.
Effective joint performance still depends on:
correct bolt size
appropriate bolt property class
adequate preload
suitable tightening procedure
thread engagement
mating-surface condition
joint stiffness
washer hardness
vibration direction and amplitude
operating temperature
This is an important distinction for both engineers and purchasing teams: a locking washer is one component of a bolted-joint system, not a substitute for correct joint design.
A useful engineering distinction is the difference between fastener rotation and loss of clamp load.
A nut or bolt can lose preload because of:
embedding
settlement
gasket creep
polymer relaxation
local yielding
thermal expansion differences
thread deformation
without necessarily rotating significantly.
Conversely, transverse movement can promote self-loosening through fastener rotation.
A DIN 9250 safety washer is primarily relevant to resisting rotational loosening. It cannot automatically compensate for every mechanism that reduces clamp force.
If an assembly repeatedly loses preload even though the fastener remains rotationally locked, engineers should investigate the joint materials,
stiffness and settlement behavior rather than simply selecting a more aggressive locking washer.
The term "heavy-duty lock washer" is widely used commercially, but engineers should avoid defining heavy-duty performance solely by washer thickness.
A reliable high-load locking system depends on the relationship between:
washer material
washer hardness
locking geometry
bolt property class
bearing pressure
mating-surface hardness
joint preload
surface coating
cyclic loading
A thicker washer manufactured from an unsuitable material or installed against an incompatible surface does not automatically provide superior locking performance.
For OEM sourcing, the dimensional drawing and mechanical specification should therefore take priority over a generic "heavy-duty" description.
Unlike stainless steel, carbon and alloy steel washers generally require an appropriate surface treatment when corrosion protection is required.
Depending on the application and approved specification, options may include:
phosphate finishes
mechanical zinc coatings
zinc-flake coating systems
other customer-specified industrial coatings
The coating should be selected according to corrosion exposure, friction requirements, temperature, assembly conditions and environmental compliance.
Zinc-flake coating systems are widely used on industrial and automotive fasteners where high corrosion resistance is required without relying on conventional electrolytic zinc deposition.
Modern coating systems may use zinc and aluminum flakes in an inorganic or organic binder system and can be specified as Cr(VI)-free where required by the applicable customer and environmental requirements.
Commercial coating families may include systems commonly recognized in the market under Dacromet-, Delta- or Geomet-type technologies, but the trade name alone should never define the engineering requirement.
A procurement specification should instead identify characteristics such as:
required corrosion resistance
coating thickness
friction range where controlled
topcoat requirements
appearance
temperature exposure
environmental compliance
test method
This allows purchasing teams to source an equivalent approved coating system without relying only on a brand name.
No universal salt-spray value should be assigned to every zinc-flake coated washer.
Corrosion performance depends on:
coating system
coating thickness
number of layers
basecoat/topcoat combination
application process
part geometry
curing parameters
handling damage
acceptance criteria
Where corrosion performance is contractually important,
the required resistance should be specified and verified according to an applicable test method such as ISO 9227 neutral salt spray testing and the customer's product specification.
For example, if an OEM requires a particular corrosion exposure target, that requirement should be included in the RFQ and purchase specification rather than assumed from the phrase "zinc-flake coated."
This is particularly important for automotive, outdoor power equipment, energy storage and infrastructure supply chains.
For a precision locking washer, coating is not simply cosmetic protection.
Excessive or inconsistent coating build can potentially affect:
formed locking features
dimensional fit
surface interaction
friction
seating behavior
This means coating requirements should be considered together with washer geometry and function.
For OEM projects, coating thickness and functional areas may need to be included in the drawing or supplier quality specification.
One important reason zinc-flake and mechanically applied coatings are used on high-strength fasteners is the need to consider hydrogen embrittlement risk.
Certain acid-cleaning and electrolytic plating processes can introduce hydrogen into hardened steel components.
Under tensile stress, susceptible high-strength materials may experience delayed brittle failure.
The actual risk depends on factors including:
material strength and hardness
manufacturing process
surface preparation
plating method
component stress
geometry
post-treatment controls
This does not mean every hardened washer will experience hydrogen embrittlement. It means that surface-treatment selection for hardened fasteners should be treated as an engineering decision.
For high-strength assemblies, procurement teams should therefore communicate the fastener hardness, coating specification and applicable hydrogen-embrittlement controls during supplier qualification.
Phosphate finishes can provide a dark industrial surface and support certain lubrication or assembly requirements.
However, phosphate alone should not automatically be treated as equivalent to a high-performance zinc-flake corrosion-protection system.
Its suitability depends on the operating environment and customer specification.
Indoor machinery may have very different corrosion requirements from an EV battery enclosure, outdoor energy-storage cabinet or construction machine.
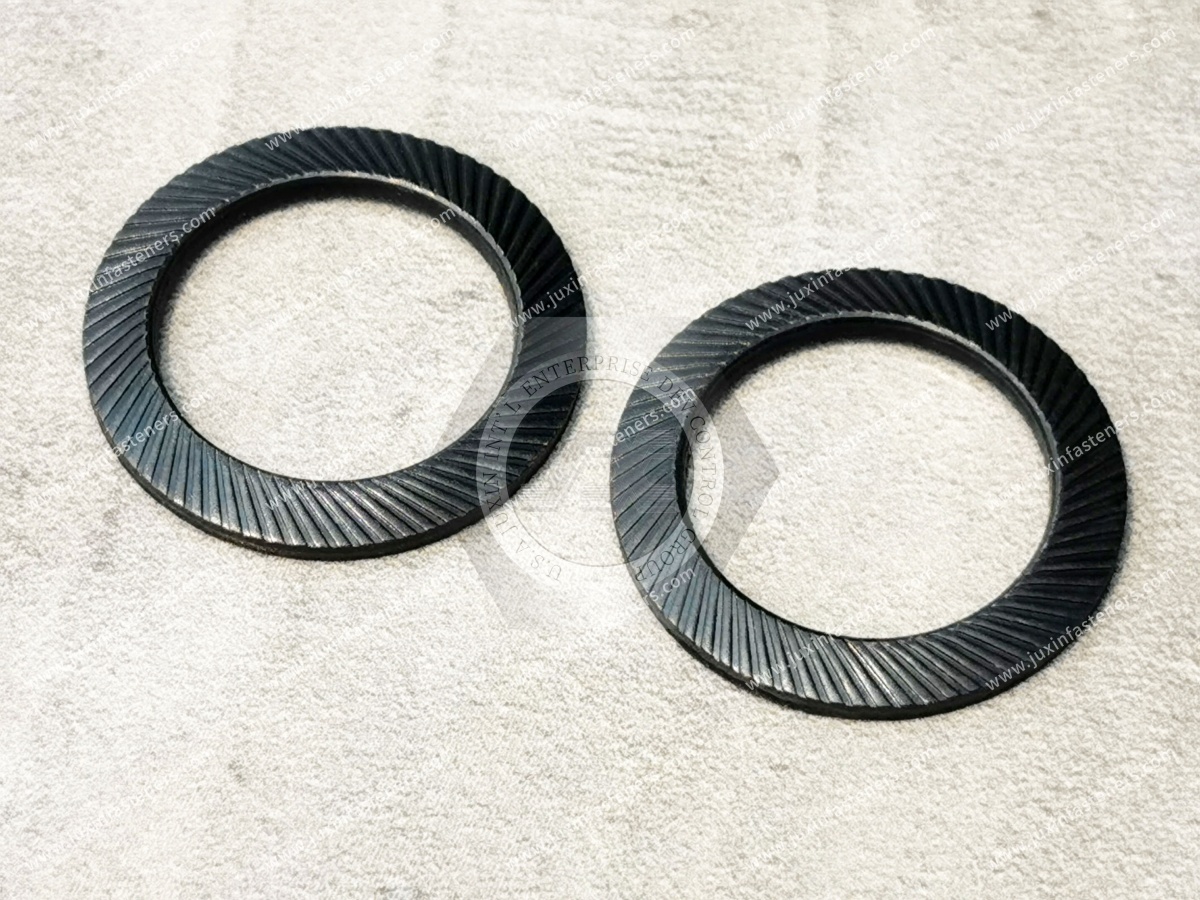
A locking washer must interact with the surface beneath the nut or bolt head.
If the mating surface is too soft, the washer may embed excessively into the material.
If the surface is protected by a thick or soft coating, tightening may damage the coating or change interface behavior.
Relevant mating materials can include:
hardened steel
structural steel
aluminum
painted steel
zinc-coated sheet
cast components
polymers
composite materials
Engineers should evaluate whether the locking interface is compatible with the actual joint material rather than testing the washer only against a generic steel plate.
DIN 9250 safety washers do not eliminate the need for controlled tightening.
The bolt still requires sufficient preload to maintain joint clamp force.
Torque-preload relationships can be affected by:
thread friction
under-head friction
washer coating
bolt coating
lubrication
prevailing torque
installation speed
surface condition
repeated installation
For critical bolted joints, tightening requirements should be validated using the actual combination of bolt, nut, washer, lubricant and surface treatment.
Changing only the washer coating can change friction conditions and therefore alter the preload achieved at the same installation torque.
This is especially relevant when OEM purchasing teams approve alternate coating suppliers.
Whether a locking washer can be reused should be determined by the approved product specification and application requirements.
Repeated tightening can affect:
locking geometry
coating integrity
interface condition
friction
mating-surface condition
For safety-critical, highly loaded or validated production joints, reuse should not be assumed without engineering approval.
A low-cost washer should never create uncertainty around a much more valuable assembly.
DIN 9250 carbon steel safety washers can be produced across a range of metric fastener sizes.
Typical requirements may include sizes such as:
M3
M3.5
M4
M5
M6
M8
M10
M12
M14
M16
M18
Availability should be confirmed against the required DIN designation, dimensional drawing, material and coating.
For OEM projects, non-standard dimensions or application-specific washer designs can also be reviewed against customer drawings.
Heavy machinery often contains bolted connections exposed to repetitive vibration, start-stop cycles and dynamic loads.
DIN 9250 carbon steel safety washers may be considered for appropriate joints in:
machine frames
motors
pumps
industrial gearboxes
production equipment
automation systems
material-handling equipment
The required locking method should be selected according to actual joint loading and maintenance requirements.
Excavators, loaders, agricultural machinery, lifting equipment and other off-highway systems operate under vibration, shock, contamination and outdoor exposure.
For these applications, engineers may require both mechanical locking performance and an engineered corrosion-resistant coating.
Zinc-flake coated carbon or alloy steel safety washers can be evaluated as part of the bolted-joint system where appropriate.
Automotive assemblies combine vibration, thermal cycling, corrosion exposure and high-volume automated assembly.
Potential applications for vibration-resistant washers can include appropriate bolted joints in:
chassis-related equipment
brackets
battery supporting systems
thermal-management equipment
production fixtures
auxiliary structures
manufacturing equipment
For automotive programs, washer material, hardness, coating, friction behavior and corrosion requirements should follow the approved OEM or Tier-1 specification.
EV battery packs and stationary energy-storage systems contain numerous structural, electrical and thermal-management subassemblies.
Potential joint challenges include:
transportation vibration
road shock
thermal cycling
outdoor exposure
long service intervals
dissimilar materials
Locking washers may form one part of the fastening strategy, but engineers must also consider galvanic corrosion, sealing, aluminum interfaces and clamp-load retention.
For aluminum battery enclosures in particular, mating-surface compatibility should be evaluated before specifying a hardened locking washer.
High-density computing infrastructure includes pumps, cooling distribution units, heat exchangers, power equipment, cabinets and structural frames.
Vibration-resistant fastening may be relevant in:
CDU assemblies
pumps
cooling manifolds
equipment frames
electrical cabinets
power-distribution equipment
HVAC and liquid-cooling systems
Carbon steel DIN 9250 safety washers may be appropriate for selected mechanical joints where high hardness and coated corrosion protection are required.
Railway and transportation systems experience persistent vibration, dynamic loads and long service cycles.
Potential applications include appropriate equipment mounting and mechanical assemblies where an approved locking method is required.
Railway applications should always follow the applicable engineering specification and customer validation requirements rather than relying solely on a generic DIN component designation.
Outdoor energy infrastructure requires fastening components capable of operating under changing temperature, humidity, vibration and long maintenance intervals.
Potential applications include:
inverter structures
control cabinets
tracking equipment
auxiliary frames
equipment housings
maintenance-access assemblies
For these applications, corrosion-protection requirements should be defined according to the actual exposure category and expected service life.
Power converters, UPS systems, electrical cabinets and industrial power equipment combine mechanical structures with thermally cycled electrical systems.
DIN 9250 washers may be considered for appropriate mechanical connections.
For electrical current-carrying joints, however, engineers must additionally evaluate electrical contact resistance, interface pressure and thermal behavior.
A mechanical locking washer should not automatically be specified for an electrical contact joint without system-level review.
One of the most important engineering decisions is recognizing when another fastening technology is more appropriate.
Depending on the joint, alternatives may include:
all-metal prevailing-torque lock nuts
nylon-insert lock nuts
wedge-lock washer systems
thread-locking adhesive
castellated nuts with mechanical retention
self-clinching fasteners
weld nuts
threaded inserts
redesigned bolted joints
For example, if joint preload is being lost because a polymer component is creeping, changing from one locking washer to another may not solve the root cause.
The assembly may instead require a compression limiter, metal insert or redesigned load path.
JUXIN FASTENERS supplies multiple locking and fastening technologies, allowing the joint requirement to determine the product rather than forcing every application into one washer category.
A practical selection process should consider the complete joint.
Is the problem rotational loosening, preload loss, corrosion, surface damage or a combination?
Confirm:
thread size
bolt property class
nut type
required preload
tightening method
Identify:
material
hardness
coating
surface finish
bearing area
Consider:
humidity
salt exposure
temperature
chemicals
outdoor service
maintenance interval
Do not simply request "Dacromet."
Specify the required:
coating system or approved equivalent
corrosion performance
coating thickness
friction requirement
environmental compliance
test method
Identify:
dimensional inspection
hardness testing
coating verification
corrosion testing
material documentation
traceability
packaging
This produces a much more reliable RFQ than purchasing by size and unit price alone.
Depending on the customer specification and application risk, quality control may include verification of:
inside diameter
outside diameter
thickness
formed locking geometry
material
hardness
heat-treatment condition
coating thickness
surface condition
corrosion performance
packaging and lot identification
For OEM and high-volume programs, the inspection plan can be established according to drawing characteristics and customer quality requirements.
Where salt spray testing is required, the test method and acceptance criteria should be specified in advance.
Strategic sourcing teams should avoid comparing DIN 9250 washer quotations only by nominal size.
Two washers described as "M10 DIN 9250 carbon steel" may differ in:
material
hardness
heat treatment
geometry
coating
coating thickness
friction behavior
corrosion resistance
inspection level
documentation
packaging
These differences can materially affect both joint performance and total sourcing risk.
Supplier comparison should therefore be based on the complete approved specification.
For an accurate quotation and engineering review, provide:
DIN 9250 designation or customer drawing
bolt/thread size
required dimensions
material requirement
hardness requirement
heat-treatment requirement
surface coating
required corrosion resistance
applicable corrosion test method
friction requirement if controlled
mating-surface material
bolt property class
operating temperature
application environment
annual usage
order quantity
inspection/documentation requirements
packaging requirements
delivery schedule
For application-specific components, a 2D drawing, 3D model or physical sample can support technical review.
JUXIN FASTENERS supports industrial OEM, Tier-1 and supply-chain customers requiring standard and custom fastening components for engineered assemblies.
Our product portfolio allows procurement and engineering teams to source DIN 9250 carbon steel safety washers together with related fastening technologies, including:
stainless steel safety washers
spring washers
disc spring washers
all-metal lock nuts
nylon-insert lock nuts
high-strength bolts and nuts
self-clinching fasteners
blind rivet nuts
weld nuts
threaded inserts
custom cold-formed components
CNC-machined fastening parts
This broader capability is useful when a project requires multiple fastening technologies and the customer wants coordinated technical review, quality requirements and supply-chain management.
It is a mechanical locking washer used beneath a bolt head or nut to increase resistance to unintended rotational loosening in suitable bolted joints.
Carbon and alloy steels can provide high hardness and mechanical performance after appropriate heat treatment.
Stainless steel may be preferred where corrosion resistance is the dominant material requirement. The correct choice depends on the complete joint.
No. Their geometries and locking principles differ. The approved standard, drawing and required joint performance should determine product selection.
Not automatically. Performance depends on the coating system, thickness, application process and acceptance criteria.
Required corrosion resistance should be specified and verified using the agreed test method, such as ISO 9227 where applicable.
They can provide high corrosion resistance and may help avoid some hydrogen-introduction risks associated with certain electrolytic plating processes.
The complete coating and pretreatment process still requires engineering control.
No. Correct preload remains fundamental to bolted-joint reliability.
Potentially, but the interface requires evaluation. A hardened washer can interact differently with softer aluminum surfaces, and coating damage, embedding and galvanic conditions should be considered.
Reuse should not be assumed. The approved product and application specification should define whether reuse is acceptable.
Provide the standard or drawing, size, material, hardness, coating, corrosion requirement, quantity, application, mating material, quality documentation and delivery requirements.
A heavy-duty anti-loosening washer should not be selected simply because it is harder, thicker or coated with a recognizable commercial finish.
Reliable bolted-joint performance comes from matching the washer material, hardness, locking geometry, coating, mating surface and installation preload to the actual operating environment.
For engineers, this means identifying the real joint failure mechanism before selecting the locking technology.
For procurement and supplier-development teams, it means defining measurable material, dimensional, coating and quality requirements before comparing suppliers.
JUXIN FASTENERS supplies DIN 9250 carbon steel safety washers, zinc-flake coated locking components,
high-strength fasteners, lock nuts, spring washers and custom fastening solutions for industrial OEM applications.
For quotation, drawing review, coating evaluation or fastening application support, send your specification, drawing and expected quantity to:
 MORE NEWS

Sep. 27, 2026

Sep. 27, 2026

Sep. 27, 2026
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY