
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Oct. 13, 2023
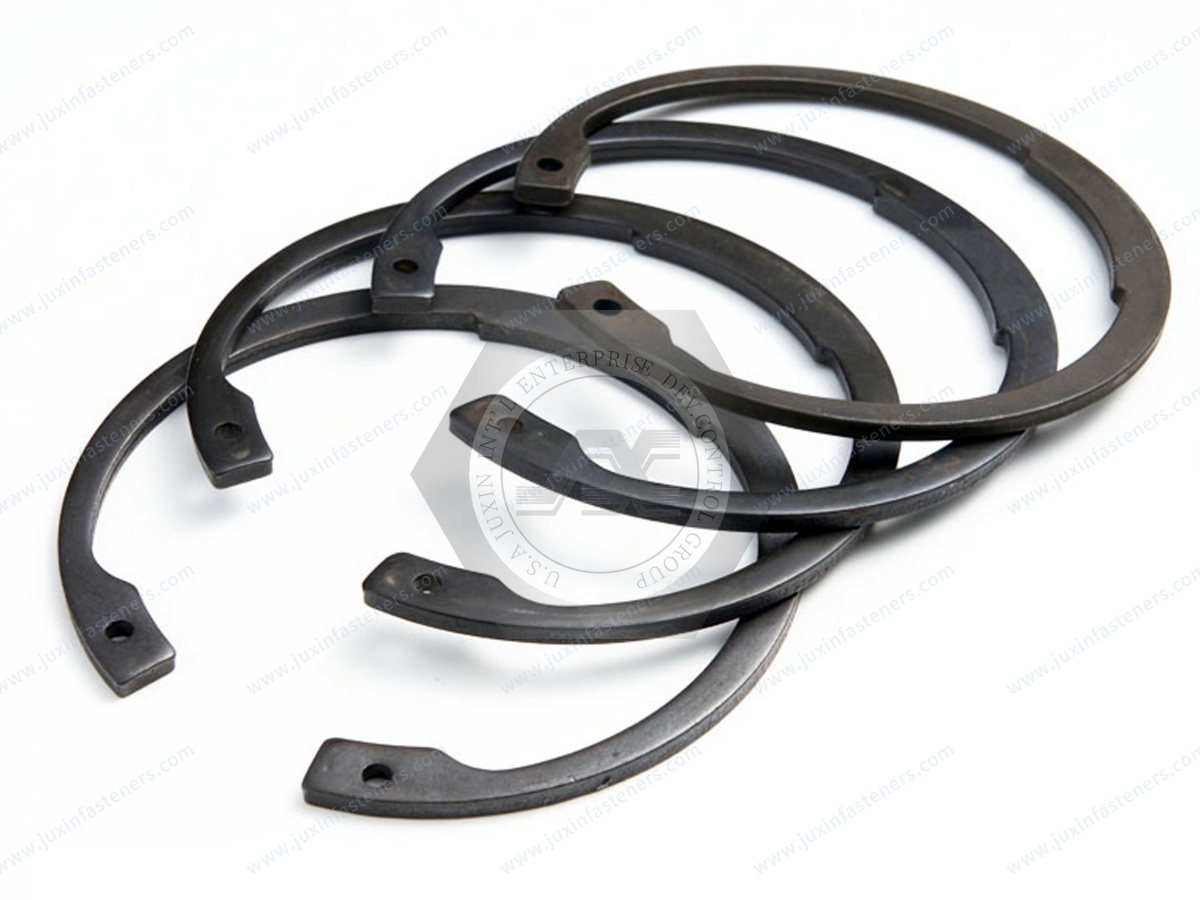
Internal retaining rings, also known as internal circlips, bore retaining rings or internal snap rings,
are spring retaining components installed into machined grooves inside bores or housings to provide axial retention for assembled components.
Typical retained components include bearings, bushings, pistons, seals, sleeves, gears and other mechanical elements positioned inside a housing.
Unlike E-clips or external retaining rings that engage grooves on shafts, an internal retaining ring works from the inside of a bore.
During installation, the ring is compressed to reduce its outside diameter, positioned inside the housing and then released into the internal groove.
Once correctly seated, the retaining ring creates a mechanical axial stop.
For design engineers, however, the load capacity of an internal retaining-ring assembly cannot be determined from the ring alone.
The complete retention system should be considered as:
Retained Component + Internal Retaining Ring + Bore Groove + Housing Material + Axial Load + Installation Method + Operating Environment
Understanding this system-level relationship is essential when specifying internal retaining rings for industrial machinery,
automotive and EV assemblies, rail equipment, robotics, HVAC systems, electrical equipment, telecommunications equipment,
semiconductor equipment, food-service equipment, medical equipment and precision mechanical assemblies.
An internal retaining ring is a spring component designed to fit into a circumferential groove machined inside a bore or housing.
The ring is manufactured with a free diameter larger than the installed diameter required by the groove.
During installation, it is compressed and inserted into the bore. When released at the groove position, the ring expands outward and engages the groove.
The ring then acts as an axial shoulder against which the retained component can react.
A simplified load path is:
Retained Component → Retaining Ring → Groove Face → Housing
This is the fundamental mechanical function of an internal retaining ring.
It should not be confused with a shaft clamping device, vibration isolator or general-purpose radial load-bearing component.
The difference begins with the location of the groove.
An internal retaining ring:
Installs inside a bore or housing
Engages an internal circumferential groove
Expands outward into the groove
Retains components positioned inside the housing
Typical retained components include bearings, bushings, pistons, sleeves and seals.
An external retaining ring:
Installs around a shaft
Engages an external shaft groove
Contracts into the groove after installation
Prevents shaft-mounted components from moving axially
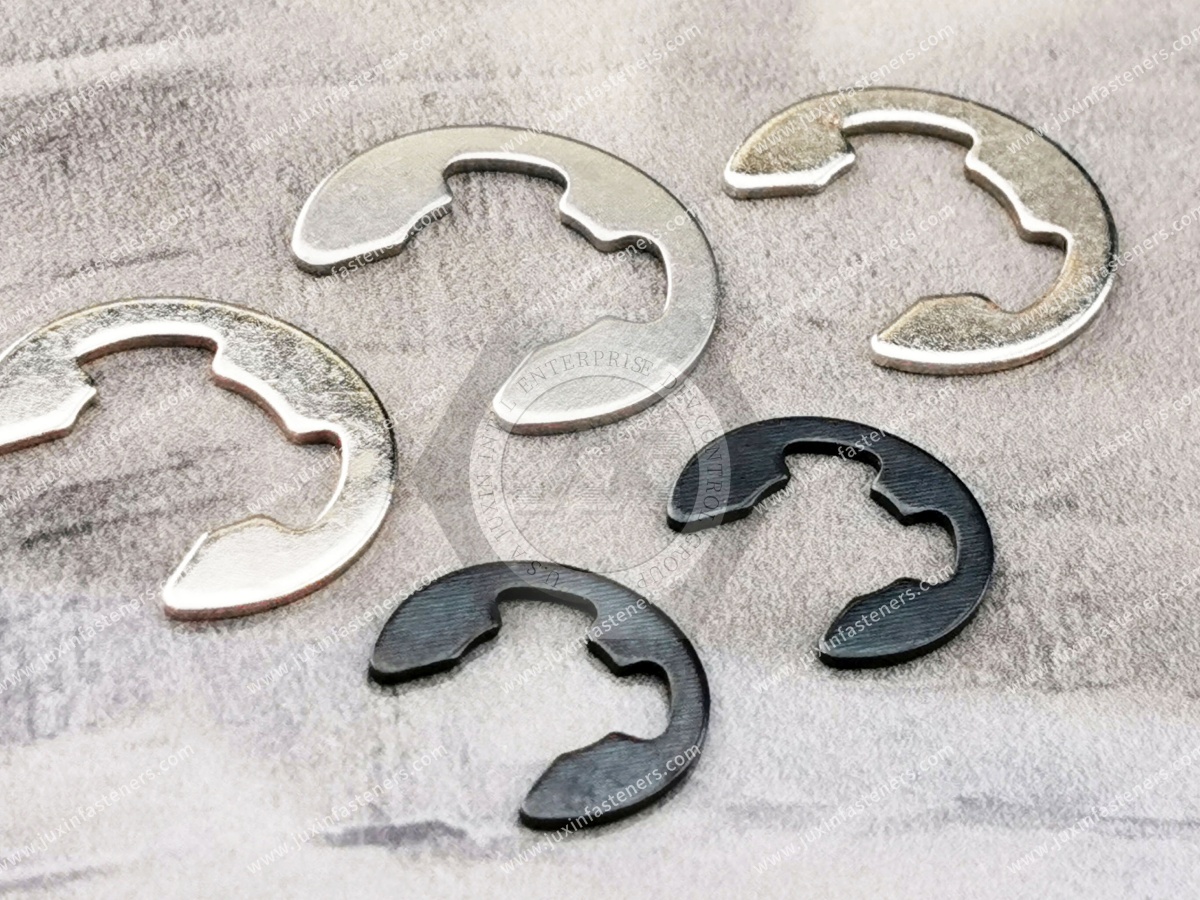
An E-clip is also normally associated with shaft retention, but its open geometry allows radial installation into a shaft groove.
Therefore:
Internal Ring → Bore Groove
External Ring → Shaft Groove
E-Clip → Shaft Groove + Radial Installation
This distinction is important for both engineering selection and procurement search.
When a bearing, bushing, piston or other retained component moves axially against the ring,
the load is transferred from the component into the retaining ring and then from the ring into the groove wall of the housing.
The load path can be represented as:
Axial Component Load → Ring Contact Area → Ring Cross-Section → Groove Face → Housing Material
This means the ring is only one part of the structural system.
Potential limiting conditions can include:
Ring deformation
Ring displacement
Groove-edge deformation
Groove shear or bearing failure
Housing deformation
Retained-component edge deformation
Excessive axial clearance
Installation damage
A catalog rating for the retaining ring should therefore not automatically be treated as the allowable load of every assembly using that ring.
One of the most important engineering distinctions in retaining-ring design is the difference between the capacity of the ring and the capacity of the groove.
A retaining ring may be mechanically capable of carrying a certain axial force while the housing groove becomes the weaker part of the assembly.
Conversely, a strong housing and correctly machined groove cannot compensate for an undersized or incorrectly selected ring.
The practical allowable load of the assembly is influenced by the weakest relevant part of the load path.
This is why engineers should evaluate:
Ring geometry
Ring material
Groove geometry
Housing material
Component contact geometry
Axial loading
Safety requirements
rather than selecting an internal retaining ring from bore diameter alone.
A common sourcing request is:
“We need an internal retaining ring for a 30 mm bore.”
The bore diameter is important, but it does not completely define the application.
Two assemblies with the same nominal bore diameter may require different retaining-ring solutions because of differences in:
Groove diameter
Groove width
Groove location
Housing material
Ring thickness
Retained component
Axial load
Operating temperature
Corrosion environment
Installation access
Required serviceability
Therefore:
Same Bore Diameter ≠ Same Retaining-Ring Application
For OEM sourcing and second-source qualification, the approved drawing or complete groove information should be reviewed whenever possible.
The groove is a functional part of the retaining system.
Important dimensions and conditions can include:
Nominal bore diameter
Groove diameter
Groove width
Groove depth
Groove location
Groove edge geometry
Distance from the housing end
Housing wall thickness
Surface condition
Manufacturing tolerance
Incorrect groove geometry can prevent the ring from seating correctly or reduce the available axial support.
The groove should therefore be designed according to the applicable retaining-ring standard, approved engineering drawing or validated customer specification.
Groove width must provide sufficient space for the retaining ring to seat while maintaining the required axial relationship with the retained component.
If the groove is too narrow, possible consequences include:
Incomplete seating
Installation difficulty
Ring distortion
Excessive interference
If the groove is too wide, possible consequences can include:
Increased axial play
Reduced positional accuracy
Uncontrolled movement of the retained component
The correct groove width depends on more than nominal ring thickness.
Manufacturing tolerance, ring geometry and required axial clearance should also be considered.
Groove depth determines how the ring engages the housing.
Insufficient groove engagement can reduce retention security.
Excessive or incorrect groove geometry can also affect how the ring seats and transfers axial load.
For this reason, groove diameter and depth should not be modified independently from the selected retaining ring.
The ring and groove should be treated as a matched mechanical interface.
The axial location of the groove determines the final position of the retained component.
The total axial stack may include:
Housing shoulder
Bearing or bushing width
Spacer
Washer
Seal
Retaining ring
Groove location
Assembly tolerances
For precision assemblies, tolerance stack-up should be evaluated across the complete system.
An internal retaining ring creates an axial stop, but it does not automatically eliminate all axial clearance.
The housing material directly affects the performance of the groove.
Potential housing materials may include:
Carbon steel
Alloy steel
Stainless steel
Aluminum alloys
Cast materials
Other engineered metals
A retaining-ring groove machined into a softer material may behave differently under axial loading from an equivalent groove in hardened steel.
Housing material, hardness and groove geometry should therefore be considered together when axial load is significant.
The component pushing against the ring is another part of the load path.
Relevant features can include:
Flat bearing face
Chamfer
Radius
Recess
Spacer interface
Bearing outer-ring geometry
Bushing geometry
A large chamfer or radius may alter the effective contact with the retaining ring.
For bearing-retention applications, engineers should review whether the ring contacts the intended structural surface rather than an unsuitable chamfer or edge.
One of the most common uses of internal retaining rings is axial retention of bearings inside housings.
A typical arrangement may include:
Housing Shoulder → Bearing Outer Ring → Internal Retaining Ring
In this configuration, the housing shoulder locates one side of the bearing while the retaining ring provides an axial stop on the opposite side.
Important design questions include:
Is the bearing intended to be axially fixed or allowed controlled movement?
What axial loads reach the bearing outer ring?
What clearance is required?
Does the bearing chamfer interfere with ring contact?
Can the ring be installed and removed after the bearing is positioned?
Is thermal expansion relevant to the bearing arrangement?
The correct answer depends on the bearing system and should not be determined from the retaining ring alone.
Internal retaining rings with suitable installation features are commonly compressed using appropriate internal retaining-ring pliers or dedicated assembly tooling.
A typical installation sequence is:
Inspect the bore and groove.
Confirm the correct retaining-ring size and orientation.
Compress the ring only as much as necessary for installation.
Insert the compressed ring into the bore.
Position it at the groove.
Release the installation force gradually.
Confirm that the ring has fully expanded into the groove.
Verify seating before the assembly enters service.
For high-volume production, dedicated fixtures or automated installation systems may be used depending on the ring design and assembly architecture.
Retaining rings are designed to deform elastically during installation, but they do not have unlimited installation travel.
Excessive compression can cause:
Permanent deformation
Reduced spring recovery
Distorted geometry
Difficult seating
Reduced groove engagement
Installation damage
Installation tooling should therefore be matched to the ring geometry and assembly process.
A ring that appears to be inside the housing is not necessarily fully seated.
Partial engagement can result from:
Incorrect groove dimensions
Burrs
Contamination
Wrong ring size
Installation-tool misalignment
Ring deformation
Surface coating interference
Depending on the assembly, seating can be verified through:
Visual inspection
Tactile confirmation
Dimensional checks
Fixture inspection
Automated vision systems
Functional assembly checks
For critical applications, seating verification should be part of the assembly-control plan.
Some retaining-ring designs may have manufacturing features or edge conditions that make installation orientation relevant to the application.
The correct orientation should follow:
Product drawing
Applicable standard
Supplier technical information
Validated assembly requirements
A universal orientation rule should not be applied to every retaining-ring design without reviewing the specific component.
If the assembly requires maintenance, engineers should consider removal access during the design stage.
Questions include:
Can the installation holes or removal features be reached?
Is enough tool clearance available?
Can the ring be removed without damaging the housing?
Will the retained component obstruct tool access?
Is ring replacement required after servicing?
Designing only for initial installation can create unnecessary maintenance problems later.
Internal retaining rings require materials capable of providing controlled elastic deformation and recovery.
Depending on the product design and application, material families may include:
Carbon spring steels
Alloy spring steels
Stainless steels
Other engineered spring materials
Material selection should consider:
Required elasticity
Strength
Heat-treatment response
Fatigue conditions
Operating temperature
Corrosion exposure
Installation deformation
Customer specification
The material should be confirmed against the actual drawing or performance requirement.
Spring steel is widely used because appropriate grades can provide the combination of strength, elasticity and manufacturing characteristics required for retaining rings.
Depending on the application, spring-steel rings may use suitable corrosion-protection finishes.
Material grade, heat treatment and hardness should be specified according to the relevant standard, customer drawing or validated product requirement.
Stainless steel retaining rings may be selected where corrosion resistance is required.
Potential applications include:
Food-service equipment
Medical and diagnostic equipment
HVAC systems
Outdoor machinery
Telecommunications equipment
Laboratory equipment
Selected semiconductor equipment
Electrical equipment
The specific stainless steel grade should be selected according to the environment.
Stainless Steel ≠ Universal Corrosion Resistance
Chlorides, cleaning chemicals, temperature and other environmental factors can affect material selection.
Depending on material and customer requirements, surface protection for spring-steel retaining rings may include appropriate:
Phosphate and oil systems
Zinc-based coatings
Zinc-nickel systems
Black finishes
Other engineered coating systems
Surface-treatment selection should consider:
Corrosion target
Ring material
Hardness
Hydrogen-embrittlement risk where applicable
Coating thickness
Installation deformation
Dimensional tolerance
Customer restricted-substance requirements
A coating should not be selected only by appearance.
Internal retaining rings operate within controlled bore and groove dimensions.
Surface coating can influence:
Ring thickness
Surface friction
Groove fit
Installation force
Elastic behavior
Seating
For precision or small-size retaining rings, even relatively small coating changes may affect assembly behavior.
A finish change should therefore be reviewed as an engineering change when dimensional or functional fit could be affected.
DIN 472 is a widely recognized standard associated with retaining rings for bores.
Where a project specifies DIN 472, engineers and sourcing teams should use the applicable standard dimensions and requirements for the specified ring size.
However, not every internal retaining ring used in industrial equipment should automatically be described as DIN 472.
OEM drawings may specify:
Standard retaining rings
Modified standard rings
Customer-specific geometry
Special materials
Special finishes
Custom retaining rings
The drawing remains the primary sourcing reference for a drawing-controlled component.
JUXIN FASTENERS can evaluate projects involving metric and inch retaining-ring requirements based on the applicable drawing, dimensions, sample or specified standard.
Metric and inch retaining rings should not be treated as simple dimensional conversions.
Differences may exist in:
Groove geometry
Ring thickness
Tolerances
Free dimensions
Installation features
Standard requirements
For replacement projects, confirm the actual specification before substituting one series for another.
Internal retaining rings can be used in suitable mechanical assemblies involving:
Bearings
Pumps
Motors
Actuators
Gear mechanisms
Steering-related mechanisms
Seat mechanisms
Auxiliary mechanical systems
Production equipment
In EV manufacturing, retaining rings may also appear in suitable motor, pump, thermal-management and production-equipment assemblies.
Selection should consider the actual:
Load
Vibration
Temperature
Corrosion exposure
Assembly method
Service requirement
Automotive application alone does not establish qualification for a specific program.
Potential retaining-ring applications in rail-related systems can include:
Actuators
Door mechanisms
Bearings
Auxiliary machinery
Pumps
Motors
Maintenance equipment
Production tooling
Rail-specific requirements for fatigue, vibration, documentation, fire behavior or safety remain dependent on the particular system and program.
Industrial machinery is one of the broadest application areas for internal retaining rings.
They may retain:
Bearings
Bushings
Pistons
Sleeves
Gears
Rollers
Seals
Mechanical subassemblies
Applications can include:
Pumps
Compressors
Gearboxes
Machine tools
Conveyors
Packaging machinery
Processing equipment
The ring should be selected from the actual load path and housing design rather than simply from machine type.
Robotics and automation systems can use internal retaining rings in:
Actuators
Gear mechanisms
Bearings
Rotary joints
Grippers
Positioning equipment
Conveyor systems
Automated tooling
High-cycle equipment may require additional evaluation of fatigue, groove condition and repeated dynamic loading.
Potential applications include:
Motors
Fans
Blowers
Pumps
Compressors
Actuators
Valve mechanisms
For HVAC and cooling equipment, humidity, condensation, outdoor exposure and operating temperature may influence material and coating selection.
As AI data centers increase the use of high-density thermal-management infrastructure, retaining rings may be used in supporting mechanical equipment rather than directly in computing electronics.
Potential mechanical applications include:
Pumps
Fans
Motors
Cooling distribution units
Actuators
Valve mechanisms
Liquid-cooling equipment
The retaining ring should be specified according to its actual mechanical function and service conditions.
Internal retaining rings can be used in mechanical and electromechanical components associated with:
Switch mechanisms
Actuators
Motors
Fans
Control equipment
Mechanical interlocks
Cabinet hardware
They should not be represented as electrical grounding components unless the specific assembly has been designed and validated for that function.
Potential applications include mechanical systems within:
Telecommunications equipment
Communication equipment
Antenna mechanisms
Base-station equipment
Cooling systems
Adjustment mechanisms
Outdoor equipment
For outdoor telecommunications equipment, corrosion protection may become a key sourcing parameter.
Semiconductor production and handling equipment may contain retaining rings in:
Motion-control assemblies
Robotics
Pumps
Actuators
Handling mechanisms
Automation equipment
Positioning systems
However, a standard industrial retaining ring should not automatically be described as cleanroom-, vacuum- or semiconductor-process-qualified.
Material, cleanliness, particle, lubricant and vacuum requirements should be specified separately where applicable.
Internal retaining rings can be used in suitable mechanical systems within:
Commercial mixers
Pumps
Motors
Dispensing mechanisms
Refrigeration equipment
Conveyors
Food-processing machinery
Where moisture, washdown or cleaning chemicals are present, material and finish selection should be reviewed accordingly.
A standard retaining ring should not automatically be described as food-contact compliant.
Potential non-implant applications include:
Diagnostic equipment
Laboratory automation
Sample-handling systems
Pumps
Motors
Actuators
Mechanical positioning systems
Medical-equipment projects may require customer-specific controls for:
Material
Surface finish
Cleanliness
Traceability
Documentation
Dimensional consistency
A standard retaining ring does not itself establish medical-device certification or biocompatibility.
Precision instruments and measurement equipment may use small internal retaining rings to locate:
Bearings
Bushings
Adjustment mechanisms
Rotating components
Sensor-related mechanical parts
In these applications, axial clearance and groove position can be particularly important.
Internal retaining rings may be used in suitable secondary mechanical systems within construction and heavy equipment, including:
Pumps
Actuators
Gear mechanisms
Control systems
Auxiliary machinery
For high axial loads or safety-critical retention, the complete structural load path should be evaluated rather than assuming a standard retaining ring is sufficient.
Suitable applications may include:
Ground-support equipment
Test equipment
Tooling
Laboratory systems
Automation
Non-flight-critical mechanical equipment
where project requirements permit.
Generic industrial retaining rings should not be represented as flight-qualified or aerospace-certified without supporting evidence.
Failure analysis should consider the complete assembly.
Possible causes include:
Incorrect ring size
Inadequate groove geometry
Excessive axial load
Housing-groove deformation
Incomplete seating
Installation damage
Incorrect component contact
Possible causes include:
Excessive installation compression
Incorrect installation tools
Wrong ring size
Material issue
Heat-treatment issue
Possible causes include:
Soft housing material
Insufficient groove support
Excessive axial load
Incorrect groove dimensions
Unfavorable component contact geometry
Possible causes include:
Groove location
Groove width
Ring thickness
Component tolerance
Housing tolerance
Spacer tolerance
Assembly stack-up
Possible causes include:
Unsuitable material
Incorrect coating
Chemical exposure
Moisture
Chlorides
Installation damage
The visible failed ring may therefore be the result of a system-level design or assembly issue rather than the original cause.
Standard internal retaining rings are often the most efficient choice when:
Standard groove geometry is available
Standard materials are suitable
Required load is within the validated application
Installation access is compatible
A custom retaining ring may be considered when the assembly requires:
Non-standard bore diameter
Special groove geometry
Restricted radial space
Modified thickness
Special installation features
Different material
Special corrosion protection
Drawing-specific geometry
Custom design should begin from the complete mechanical interface rather than simply scaling a standard ring.
Second-source projects should distinguish between different sourcing objectives.
Critical dimensions and interfaces follow the approved drawing.
Some non-critical characteristics may differ while the required assembly function is maintained after customer engineering review and validation.
The design is intentionally changed to address:
Material
Finish
Geometry
Installation
Manufacturing requirements
The ring is developed around the specific:
Bore + Groove + Retained Component + Load + Environment + Installation Process
requirements.
A visually similar ring should not automatically be treated as a drop-in replacement.
When the original drawing is unavailable, a physical retaining-ring sample can support second-source development.
A practical process can include:
Physical Sample → Dimensional Inspection → Application Review → Groove Review → Material / Finish Evaluation → Drawing Confirmation → Prototype → Assembly Validation → Production
A sample can help establish:
Ring geometry
Thickness
Free diameter
Installation features
Visible surface finish
However, a sample alone may not establish:
Exact material chemistry
Original hardness specification
Heat-treatment history
Coating specification
Required axial load
Fatigue requirement
Original standard
Application information should therefore accompany the sample whenever possible.
Design engineers and sourcing professionals often search for the same product from different perspectives.
Engineers may search for:
internal retaining ring groove design
internal circlip groove dimensions
retaining ring axial load
bearing retaining ring for bore
internal snap ring installation
DIN 472 retaining ring
internal vs external retaining ring
Their core question is:
Will the retaining ring and groove safely retain the component in the actual housing?
Procurement teams may search for:
internal retaining ring manufacturer
DIN 472 supplier
stainless steel circlip supplier
custom retaining ring manufacturer
retaining ring from drawing
retaining ring from sample
retaining ring second source
Their core question is:
Can the supplier consistently reproduce the required ring geometry, material, finish and functional interface at production volume?
A successful OEM sourcing project must connect both questions.
For an engineering review or quotation, provide as much of the following information as possible.
2D drawing
3D model where relevant
Standard designation
Customer part number
Existing sample
Bore diameter
Groove diameter
Groove width
Groove location
Housing material
Housing hardness where relevant
Housing wall thickness where relevant
Component type
Component dimensions
Contact geometry
Required axial clearance
Bearing or bushing information where applicable
Expected axial load
Static or dynamic loading
Shock conditions
Vibration
Operating speed where relevant
Required service life
Required ring material
Hardness requirement if specified
Surface finish
Corrosion requirement
Restricted-substance requirements
Temperature
Humidity
Chlorides
Cleaning chemicals
Outdoor exposure
Other relevant environmental conditions
Prototype quantity
Sample quantity
Pilot quantity
Production quantity
Estimated annual volume
Packaging
Traceability
Delivery schedule
Long-term sourcing requirements
For OEM and second-source retaining-ring programs, supplier qualification may consider capabilities relevant to the project, including:
Drawing review
Tooling control
Forming-process control
Material control
Heat-treatment control where applicable
Dimensional inspection
Surface-treatment control
Prototype development
Production consistency
Automatic optical sorting where applicable
Packaging
Lot identification
Change communication
Long-term supply support
Automatic sorting can help inspect compatible externally measurable characteristics in suitable high-volume programs.
It does not replace material verification, mechanical testing, fatigue validation or application testing when those controls are required.
JUXIN FASTENERS supports standard, drawing-based and custom industrial fastener projects for OEM manufacturers, engineering teams,
procurement organizations, strategic sourcing teams and supplier-development programs.
Internal retaining-ring projects can be evaluated from:
Engineering drawings
Physical samples
Standard references
Bore and groove dimensions
Material requirements
Surface-finish requirements
Application information
Production-volume requirements
For second-source development, the first step is determining whether the project requires:
Standard retaining ring
Exact replacement
Functional equivalent
Modified alternative
Custom retaining ring
Sample development and assembly evaluation can then be used before volume production to confirm the required:
Groove fit
Installation behavior
Ring seating
Axial retention
Component clearance
Removal access
Functional performance
A practical engineering decision path is:
What component must be retained inside the housing?
→ What axial force can reach the retained component?
→ What is the bore diameter?
→ What groove geometry is available?
→ What is the housing material?
→ What component surface will contact the ring?
→ What axial clearance is acceptable?
→ What installation access is available?
→ Does the assembly require future removal or maintenance?
→ What material and surface finish are required?
→ What corrosion, temperature, vibration or dynamic conditions apply?
→ Is a standard internal retaining ring suitable?
→ Does the project require DIN 472, another specified standard or a customer drawing?
→ Is the sourcing objective an exact replacement, functional equivalent or custom design?
→ How will samples be validated in the actual assembly?
→ What are the production quantity and annual demand?
This changes the sourcing question from:
“Do you have a retaining ring for this bore?”
to:
“What internal retaining ring, groove interface, material and manufacturing specification are required to retain this component reliably in the actual housing?”
That is the more useful question for mechanical engineers, design engineers, manufacturing engineers, procurement managers, supplier-development teams and strategic sourcing professionals.
For internal retaining rings, internal circlips, bore retaining rings,
DIN 472 retaining rings, stainless steel retaining rings, custom retaining rings, drawing-based parts, sample development or second-source programs,
send your available drawing, sample, bore and groove dimensions, material, finish, application requirements and quantity to:
JUXIN FASTENERS can review the available technical information and evaluate an appropriate sample-development and manufacturing path for your application.
 MORE NEWS

Sep. 27, 2026

Sep. 27, 2026

Sep. 27, 2026
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY