
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Apr. 21, 2026
Flanged CD Weld Studs for Medical Equipment Enclosures: Precision Welding, Design Validation and OEM Sourcing
Medical equipment manufacturers rely on precision sheet metal assemblies to protect electronic systems,
support mechanical components and provide reliable mounting interfaces throughout a product's service life.
Diagnostic instruments, laboratory analyzers, medical imaging equipment, hospital equipment cabinets and electronic control housings often
require permanent threaded attachment points on stainless steel or other metallic panels.
These assemblies may also impose demanding requirements for dimensional accuracy, corrosion resistance, cleaning compatibility,
cosmetic appearance, vibration resistance and repeatable manufacturing quality.
Flanged Capacitor Discharge Weld Studs (Inch / Metric) offer a fastening option for suitable metallic components
where a permanent externally threaded mounting point is needed without drilling a conventional clearance hole through the parent sheet.
The capacitor discharge (CD) welding process uses stored electrical energy to create a short-duration welding event.
When the fastener, substrate and equipment are compatible, this process can help limit localized thermal effects and support efficient sheet metal manufacturing.
However, a successful welded attachment requires more than selecting the correct thread diameter.
Flange geometry, ignition-tip condition, material selection, sheet thickness, welding energy, installation alignment and finished-joint testing all influence performance.
For medical equipment manufacturers, the requirements may extend further to include supplier qualification, material documentation, manufacturing traceability and change control.
A critical distinction must also be made between industrial fasteners used in medical equipment housings and components intended for direct or indirect patient contact.
JUXIN FASTENERS supplies flanged CD weld studs and related industrial fastening components for suitable standard and drawing-based OEM applications.
This guide focuses on practical engineering selection, manufacturing process validation,
production quality and procurement requirements for medical equipment and precision sheet metal assemblies.
What Are Flanged Capacitor Discharge Weld Studs?
A flanged CD weld stud is a fastener designed for attachment to a compatible metallic workpiece using capacitor discharge stud welding.
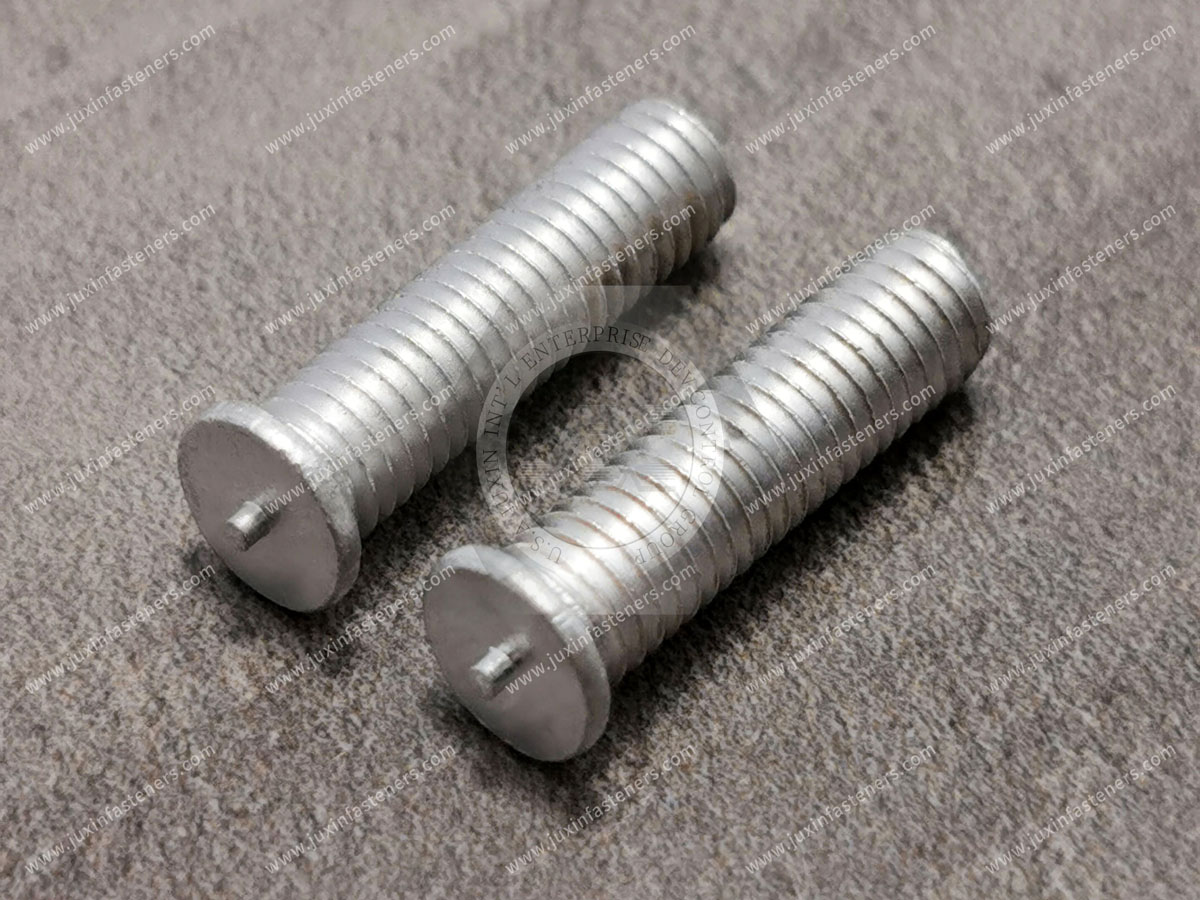
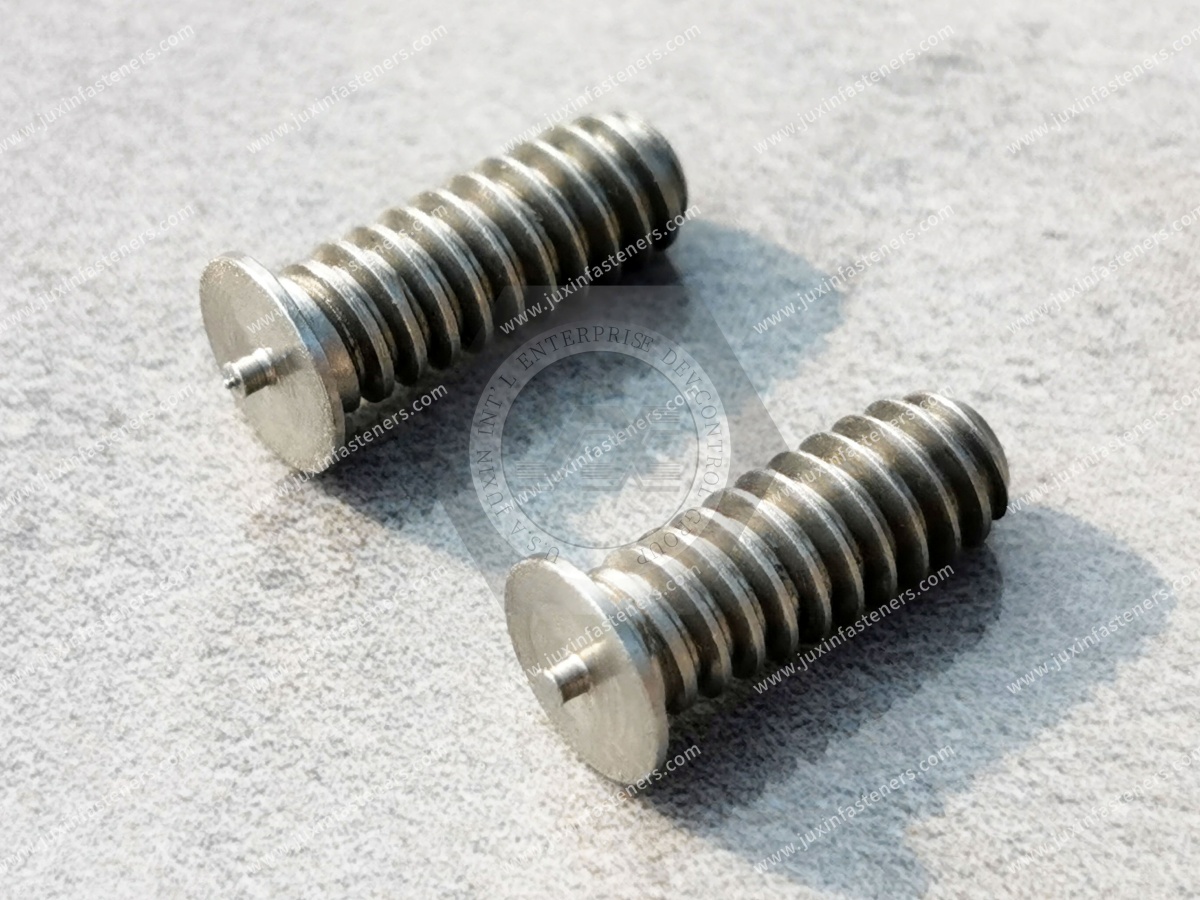
A typical externally threaded configuration incorporates a threaded shank, a wider flange at the welding end and an ignition tip designed for the intended CD welding process.
The flange provides a defined weld-base region, while the threaded shank remains accessible for subsequent mechanical assembly.
Depending on the product family, flanged CD weld studs may be specified with metric or Unified inch-series threads.
Main Product Features
External Threaded Shank
Provides a male-threaded mounting point for compatible nuts, brackets and other mechanical components.
Flanged Weld Base
Provides a defined joining interface and may increase the effective welded area compared with a comparable non-flanged design.
Ignition Tip
Supports initiation of the tip-ignition capacitor discharge welding process.
Stud Length
Determines available thread engagement and clearance for the mating assembly.
Material and Surface Condition
Influence weldability, corrosion resistance, mechanical properties and manufacturing consistency.
The actual thread dimensions, flange diameter, flange thickness, ignition-tip geometry and overall length must be established by the applicable product drawing.
Why the Flanged Design Matters
The flange is an important functional feature of the fastener.
Compared with a similar non-flanged configuration, a wider flange may provide a greater effective joining area between the stud and parent metal.
This can be useful where the assembly requires a permanent threaded attachment and sufficient space is available around the weld base.
However, flange size alone does not determine mechanical strength.
The completed joint must be evaluated according to its material, weld formation, substrate thickness and loading conditions.
Flange Diameter
The flange diameter influences the joining interface and the space occupied by the fastener.
A larger flange may be beneficial for certain mechanical requirements, but it can also interfere with nearby components.
Flange Thickness
Flange thickness influences the distance between the parent sheet and a mating component.
Where a nut or bracket must move very close to the sheet, the flange may create an interference condition.
Flange Geometry and Installation Tooling
Welding chucks, positioning devices and automated feeding systems may require specific flange dimensions.
A stud with the correct thread size is not necessarily compatible with an existing welding gun or feeder.
Standard Flanged Versus Automatic-Feed Configurations
Industrial CD stud product families may distinguish standard flanged studs from reduced-flange or automatic-feed configurations.
These differences can affect tooling, part orientation and installation behavior.
A replacement stud should therefore be evaluated using its complete geometry rather than nominal thread size alone.
How Capacitor Discharge Stud Welding Works
Capacitor discharge stud welding uses electrical energy stored in capacitors to produce a short-duration welding event.
In a suitable tip-ignition process, the ignition tip participates in initiating the arc between the stud and workpiece.
The welding equipment controls the discharge and movement of the stud to form the welded connection.
The process may use contact or gap operation depending on the equipment.
General CD Welding Sequence
The stud is positioned at the specified location on the parent metal.
The welding system establishes the required contact or gap arrangement.
Stored electrical energy is discharged through the welding circuit.
The ignition tip initiates the intended welding event.
The welding gun controls the stud movement as the joining surfaces develop the connection.
The completed weld is inspected against the specified acceptance criteria.
The actual sequence depends on the equipment and approved welding procedure.
Contact CD Welding
In contact operation, the stud begins in contact with the workpiece through the intended ignition arrangement.
The welding system initiates the discharge and controls the subsequent joining movement.
Gap CD Welding
In gap operation, the equipment establishes a defined movement sequence before the joining event.
The process characteristics and setup requirements differ from contact operation.
The appropriate method should be selected according to the stud, substrate and welding equipment.
Why CD Welding Is Considered for Precision Sheet Metal
The short-duration welding event can help limit thermal effects compared with some longer-duration welding processes.
For suitable applications, this may reduce the risk of panel distortion and reverse-side marking.
However, these benefits depend on the actual material, sheet thickness, stud geometry and welding procedure.
CD welding does not guarantee a completely mark-free surface.
CD Welding Versus Resistance Projection Welding
Tip-ignition capacitor discharge stud welding and resistance projection welding are different joining processes.
Resistance projection welding uses formed projections and electrode force to concentrate electrical resistance heating.
Tip-ignition CD welding uses a different weld-end arrangement and welding sequence.
The fasteners, equipment and welding parameters should not be treated as interchangeable.
Medical Equipment Applications for Flanged CD Weld Studs
Medical equipment manufacturers use sheet metal structures for a wide range of mechanical and electronic functions.
The suitability of a flanged CD stud depends on the intended component, loading conditions, manufacturing process and regulatory responsibilities.
Diagnostic Equipment Enclosures
Diagnostic equipment may incorporate metallic housings, electronic module supports, mounting brackets and internal structural panels.
Flanged CD studs may provide permanent threaded mounting points for suitable non-patient-contact mechanical attachments.
Potential applications include internal equipment brackets, auxiliary mounting plates and selected removable-cover supports.
Laboratory Analyzer Housings
Laboratory instruments frequently use fabricated metal enclosures with precise mounting locations.
CD studs may be considered for suitable internal support brackets, mechanical accessories and electronic equipment mounting structures.
The design should account for vibration, service access, cleaning exposure and dimensional accuracy.
Medical Imaging Equipment Cabinets
Medical imaging systems may contain extensive electronic, mechanical and thermal management assemblies.
Flanged CD studs may be considered for selected cabinet panels, cable-management brackets and auxiliary mounting structures.
Their use should not be assumed suitable for primary load-bearing, patient-supporting or safety-critical connections without application-specific qualification.
Hospital Equipment Enclosures
Hospital equipment may contain control panels, protective covers, mechanical accessories and support structures.
CD welded threaded attachments may be suitable where the substrate and assembly requirements are compatible.
Cleaning procedures and repeated maintenance should be considered during selection.
Medical Electronics and Power Supply Housings
Medical electronic equipment may use metallic enclosures to protect power supplies, circuit assemblies and control components.
Flanged CD studs may support selected mechanical brackets or internal hardware.
Electrical insulation, grounding, electromagnetic compatibility and thermal safety must be evaluated separately from weld strength.
Patient-Contact Versus Non-Patient-Contact Components
Not every fastener used in medical equipment requires the same biological safety evaluation.
A threaded stud used inside a diagnostic instrument enclosure may have no direct or indirect patient contact.
A component intended for contact with tissue, blood or patient-contacting fluid pathways presents different requirements.
Non-Patient-Contact Applications
Examples may include:
External instrument housings
Internal electronic equipment brackets
Protected control cabinets
Auxiliary mechanical mounting plates
Non-patient-contact equipment supports
For these applications, mechanical performance, corrosion resistance, cleanliness and supplier quality requirements may be the principal concerns.
Direct or Indirect Patient-Contact Applications
Where a component directly contacts the body or forms part of a relevant indirect-contact pathway, biological safety requirements may apply.
Material selection alone is insufficient to establish biocompatibility.
The complete device, including manufacturing processes, surface treatments, residues and intended exposure, must be evaluated by the medical device manufacturer.
Why Stainless Steel Does Not Automatically Mean Biocompatible
Stainless steel grades are selected for a range of mechanical and corrosion requirements.
A commercial stainless steel designation does not independently establish suitability for implantation or patient contact.
The relevant biological safety evaluation depends on the intended use and exposure conditions.
ISO 10993-1 and Biological Safety
ISO 10993-1:2025 addresses the biological safety evaluation of medical devices within a risk management process.
Its relevance depends on the device's intended contact conditions.
A non-patient-contact enclosure fastener should not automatically be described as an implantable or biocompatible component.
JUXIN FASTENERS does not claim that the industrial CD weld studs described here have been qualified for implantation or specific patient-contact applications.
Selecting Stainless Steel for Medical Equipment Enclosures
Stainless steel may be selected for medical equipment housings because of its corrosion resistance, appearance and compatibility with appropriate cleaning procedures.
However, the actual grade must be selected for the service environment and welding process.
304 Stainless Steel
304 stainless steel may be suitable for many general industrial and medical equipment enclosure applications.
The actual corrosion resistance depends on environmental exposure, surface condition and cleaning chemicals.
316 Stainless Steel
316 stainless steel may be considered where improved resistance to certain corrosive environments is required.
However, 316 stainless steel is not immune to pitting or crevice corrosion.
The selection should reflect the actual chemical exposure, temperature and cleaning procedure.
Grade Verification
The specified material grade should be established by the product drawing or purchasing specification.
Material documentation or additional verification may be required by the OEM.
Stainless Steel Weldability
Different stainless steel grades have different electrical, thermal and metallurgical characteristics.
A welding schedule developed for low-carbon steel should not automatically be applied to stainless steel.
The stud and substrate combination must be evaluated.
Carbon Steel CD Weld Studs
Suitable low-carbon steel CD studs may be appropriate for protected internal structures where corrosion requirements permit.
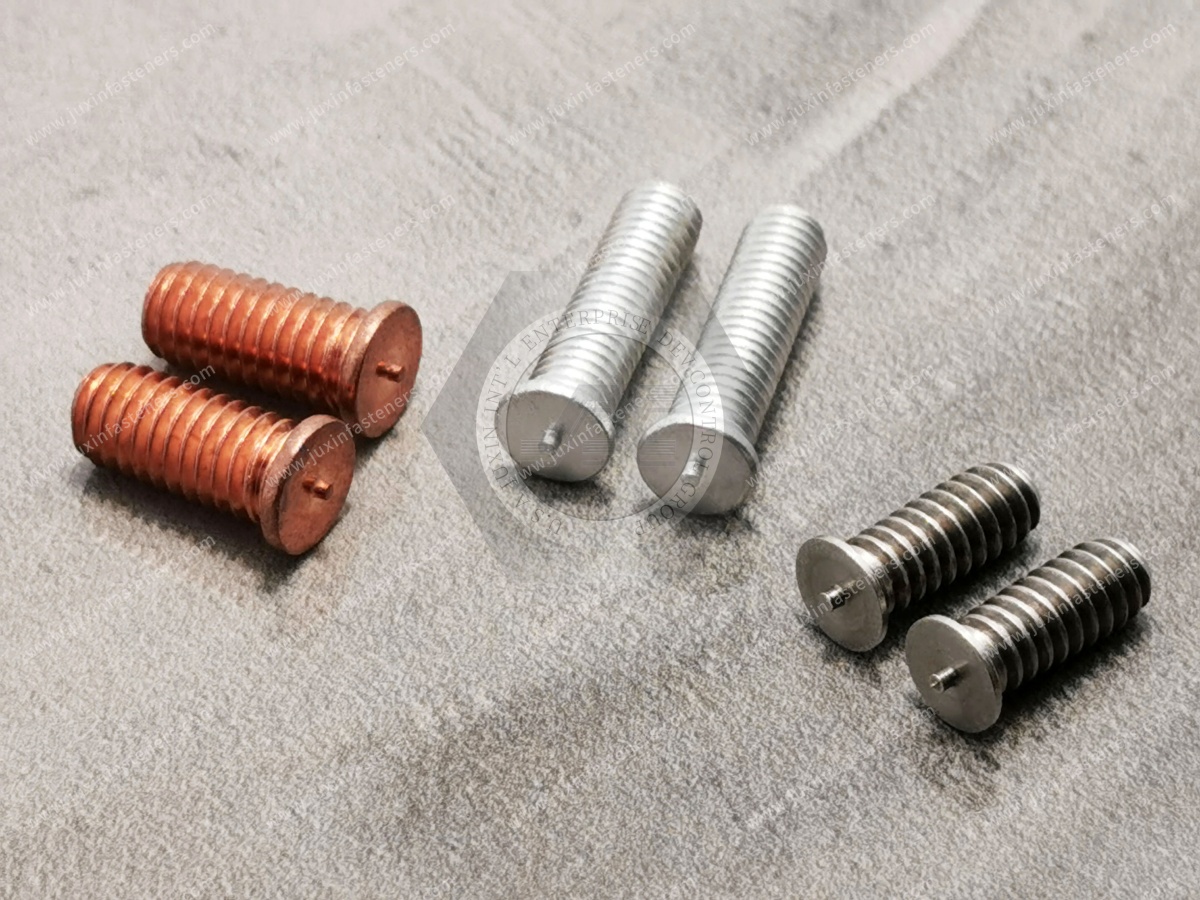
Copper-flashed carbon steel is used in certain commercial CD stud configurations.
However, carbon steel should not automatically replace stainless steel in equipment exposed to repeated cleaning, condensation or corrosive chemicals.
Aluminum CD Weld Studs
Aluminum CD weld studs may be considered for compatible aluminum assemblies.
The actual alloy and welding process must be evaluated.
A conventional steel or stainless steel CD stud should not be assumed suitable for direct welding to aluminum.
Brass and Other Material Options
Other material configurations may be considered where available and technically appropriate.
The actual combination of material, thread size, stud length and weld-end geometry requires supplier confirmation.
Cleaning Compatibility and Corrosion Resistance
Medical equipment may be exposed to cleaning agents, disinfectants, moisture and repeated maintenance procedures.
The selected fastener material and finished joint should be evaluated for the actual environment.
Disinfectant Exposure
Different cleaning and disinfecting chemicals can affect metallic surfaces in different ways.
The equipment manufacturer should specify the relevant chemical exposure and cleaning conditions.
Chloride-Containing Chemicals
Certain chloride-containing cleaning agents can increase the risk of localized corrosion in stainless steel.
Material selection and cleaning procedures should be evaluated together.
Crevice Corrosion
Gaps around mating components or flange transitions may retain moisture or cleaning residues.
The complete assembly geometry should be reviewed where cleanability is important.
Post-Weld Surface Condition
Welding may affect the local surface condition of stainless steel.
Where appropriate, cleaning, finishing or passivation procedures may be specified.
The selected procedure must be compatible with the material and equipment requirements.
Cleanroom Manufacturing Considerations
A flanged CD weld stud is not automatically a cleanroom-qualified component.
Cleanroom compatibility depends on the complete manufacturing process, contamination controls, packaging and handling requirements.
Potential Contamination Sources
Welding expulsion
Surface residues
Handling contamination
Packaging particles
Cleaning chemicals
Post-weld processing residues
Welding Before Sensitive Component Installation
Where possible, welding may be performed during the metallic fabrication stage before sensitive electronic or optical components are installed.
The manufacturing sequence should be established according to the equipment design.
Cleaning and Inspection
Cleaning requirements should be specified by the OEM.
A visually clean surface does not necessarily establish compliance with a defined particulate or chemical residue limit.
Why No Universal Surface Roughness Limit Applies
Surface roughness requirements depend on the component function and cleaning specification.
A single Ra limit should not be imposed on every medical equipment housing or welded stud location.
Where surface roughness is critical, the requirement should be established by the actual drawing and validated measurement method.
Thin Sheet Metal Welding and Reverse-Side Appearance
Medical equipment housings frequently use precision-fabricated metal panels.
These components may require both reliable mechanical attachments and controlled exterior appearance.
Potential Welding Effects
Reverse-side discoloration
Local surface marking
Panel distortion
Burn-through
Weld expulsion
Incomplete weld formation
Stud misalignment
Minimum Sheet Thickness
The minimum suitable sheet thickness depends on the material, stud diameter, flange geometry, welding energy and mechanical requirements.
There is no universal minimum thickness applicable to every flanged CD stud.
Why No-Mark Welding Cannot Be Guaranteed
The short-duration CD process may help limit thermal effects.
However, the opposite side of the panel may still show marking or distortion.
Where cosmetic appearance is critical, representative samples should be evaluated before production approval.
Mechanical Strength Versus Cosmetic Appearance
A weld may satisfy a mechanical test while failing the appearance requirement.
Conversely, a visually acceptable weld may not provide adequate mechanical strength.
These requirements should be specified and verified separately.
Welding Parameters and Process Validation
CD welding parameters must be developed for the actual stud, substrate and equipment combination.
A fixed current or welding-time formula based only on stud diameter is not a reliable basis for process development.
Important Process Variables
Capacitor charging voltage
Equipment capacitance
Stored electrical energy
Discharge circuit characteristics
Stud diameter
Flange geometry
Ignition-tip dimensions
Stud material
Parent-metal material
Sheet thickness
Surface condition
Contact or gap operation
Welding gun setup
Stud movement
Workpiece grounding
Required joint performance
Stored Electrical Energy
The electrical energy stored in a capacitor bank is described by:
E = ½ CV²
Where E represents stored energy, C represents capacitance and V represents capacitor charging voltage.
This relationship describes stored electrical energy.
It does not directly establish the energy delivered to the weld interface or guarantee an acceptable joint.
Surface Preparation
The intended welding surface should be prepared according to the approved process.
Oil, contamination, heavy oxide layers and incompatible coatings may interfere with weld formation.
The cleaning method should be appropriate for the substrate and manufacturing requirements.
Stud Alignment
The stud should be positioned according to the engineering drawing and equipment requirements.
Misalignment may affect weld formation and assembly accuracy.
No universal angular tolerance should be assumed for every stud and application.
Preheating
Preheating should not be introduced as a standard requirement for flanged CD stud welding.
Any special thermal procedure must be justified by the actual material and qualified joining process.
Shielding Gas
Conventional tip-ignition CD stud welding often operates without external shielding gas.
However, the process requirements depend on the welding equipment and application.
Shielding gas should not be prescribed solely because the equipment is used in the medical industry.
Common Welding Defects and Engineering Troubleshooting
Weak Weld Attachment
Possible contributing factors include unsuitable welding energy, surface contamination, incorrect equipment setup or material incompatibility.
The finished joint should be evaluated using appropriate testing.
Incomplete Fusion
Incomplete fusion may occur when the joining conditions are insufficient or unstable.
The engineering team should review the welding schedule, ignition-tip condition and surface preparation.
Excessive Expulsion
Excessive expulsion may be associated with inappropriate welding energy, equipment behavior or surface conditions.
The actual cause should be established before changing parameters.
Stud Tilt
Stud tilt may result from positioning errors, unsuitable tooling or inconsistent stud movement.
The installation equipment and fixture arrangement should be inspected.
Reverse-Side Marking
Visible marking may result from localized heating, substrate thickness or welding conditions.
The response should consider both mechanical and cosmetic acceptance criteria.
Thread Damage
Thread damage may occur during handling, welding or subsequent assembly.
The inspection plan should identify the required thread characteristics.
Variable Weld Quality
Variation may result from changes in fastener geometry, material, surface condition or equipment setup.
A systematic investigation should compare production lots and welding records.
Root-Cause Analysis for Medical Equipment Production
A practical investigation separates the process into four groups.
Fastener Variables
Material, thread dimensions, flange geometry, ignition-tip condition and dimensional consistency.
Substrate Variables
Material grade, thickness, flatness, coating and cleanliness.
Equipment Variables
Welding energy, gun setup, stud movement, positioning and workpiece grounding.
Finished-Joint Variables
Mechanical performance, appearance, dimensions and any required electrical properties.
This approach helps identify the actual source of variation before corrective action is selected.
Mechanical Loading and Joint Reliability
The finished welded attachment must meet the mechanical requirements of the assembly.
The nominal strength of the stud material does not automatically establish the strength of the weld.
Relevant Loading Conditions
Axial tension
Transverse shear
Bending
Assembly tightening torque
Vibration
Repeated maintenance loading
Fatigue where applicable
Potential Failure Modes
Weld interface failure
Parent-sheet tearing
Local panel deformation
Stud fracture
Thread damage
Fatigue-related failure
Why Flange Diameter Alone Does Not Determine Strength
A larger flange may provide a greater effective joining area.
However, the actual joint capacity depends on weld formation, substrate material and applied loading.
The required mechanical performance must be validated.
Assembly Torque
The tightening torque applied to the mating nut must be compatible with the stud, thread engagement and welded joint.
Excessive torque may damage the thread or welded attachment.
The applicable tightening requirements should be established by the assembly design.
Repeated Maintenance
Medical equipment may require periodic inspection, calibration and servicing.
Where threaded components are repeatedly removed and reinstalled, the welded attachment should be evaluated for the intended maintenance conditions.
International Standards and Medical Device Quality Requirements
Different standards address different aspects of the product and manufacturing process.
They should not be treated as interchangeable.
ISO 13918:2017
ISO 13918:2017 addresses specified studs and ceramic ferrules for arc stud welding.
The applicable stud type, dimensions, material requirements and standard edition must be checked against the actual product.
The 2017 edition was reviewed and confirmed in 2025.
ISO 14555:2025
ISO 14555:2025 addresses arc stud welding of metallic materials, including welding procedure, qualification and production testing requirements within its scope.
Its applicability must be assessed for the actual joining process.
ISO 13485:2016
ISO 13485:2016 establishes quality management system requirements for medical devices and related regulatory purposes.
Medical device OEMs may use these requirements when qualifying suppliers and managing purchased components.
A fastener supplier should not be described as ISO 13485 certified unless valid certification has been confirmed.
ISO 14971
ISO 14971 provides a framework for medical device risk management.
Its relevance concerns the medical device manufacturer's evaluation and control of product risks.
A fastener's dimensional conformity does not independently establish that the complete medical device meets its risk management requirements.
ISO 10993-1:2025
ISO 10993-1:2025 addresses biological safety evaluation within a risk management process.
Its applicability depends on the intended patient-contact conditions.
A general industrial weld stud should not be represented as biocompatible or implantable without appropriate evaluation and supporting evidence.
United States Medical Device Quality System Requirements
The FDA Quality Management System Regulation became effective on February 2, 2026, incorporating ISO 13485:2016 by reference into the updated requirements of 21 CFR Part 820.
The obligations applicable to a particular supplier depend on its role, activities and contractual responsibilities.
Supplying a fastener to a medical equipment OEM does not automatically establish that the fastener supplier holds medical device certification.
Thread Standards for Metric and Inch CD Weld Studs
Flanged CD weld studs may be specified with metric or Unified inch-series external threads.
Metric Thread References
ISO 261 provides general-purpose metric screw thread series.
ISO 965 addresses metric thread tolerances.
Unified Inch Thread Reference
ASME B1.1 covers Unified inch screw threads, including UNC and UNF series.
Common Metric Search Specifications
Industry examples include:
M3 × 0.5
M4 × 0.7
M5 × 0.8
M6 × 1.0
M8 × 1.25
Common Unified Inch Search Specifications
Industry examples include:
#4-40 UNC
#6-32 UNC
#8-32 UNC
#10-24 UNC
#10-32 UNF
1/4-20 UNC
These examples are not a guarantee that every size is available in every material, length or flange configuration.
Metric and Inch Threads Are Not Interchangeable
Metric, UNC and UNF threads are different systems.
BSW and BSF are also distinct thread systems.
Similar nominal diameters do not establish interchangeability.
For example, M6 × 1.0 and 1/4-20 UNC have different nominal diameters and pitches.
Thread selection must follow the actual mating component drawing.
Thread Engagement and Stud Length
The specified stud length should provide adequate thread engagement while avoiding interference with adjacent components.
The design should consider bracket thickness, nut height, available clearance, flange geometry and dimensional tolerances.
Quality Control for Medical Equipment OEM Supply
Medical equipment manufacturers may require additional documentation and supplier controls depending on the component's function and risk classification.
The quality plan should reflect the actual purchasing specification.
Dimensional Inspection
Critical dimensions may include:
Thread diameter and pitch
Thread tolerance class
Stud length
Flange diameter
Flange thickness
Ignition-tip geometry
Straightness
Material Verification
The material grade should be specified and verified according to the customer's requirements.
Material documentation or additional testing may be required.
Weld-End Inspection
The ignition tip is a functional feature of the fastener.
Damage or dimensional variation may influence welding behavior.
The inspection plan should address critical weld-end characteristics where applicable.
Weld Testing
Potential evaluation methods include visual examination, dimensional inspection, bend testing, torque-related testing, pull-off testing and other mechanical testing where appropriate.
The acceptance criteria should be defined by the application.
Cleaning and Contamination Requirements
Where specified, the supplier and OEM should agree on cleanliness requirements, packaging and handling controls.
A general statement of cleanliness is not a substitute for defined acceptance criteria.
Traceability
Depending on the project, traceability may include material lots, production batches, inspection records and relevant manufacturing documentation.
The required level of traceability should be established in the purchasing specification.
Inspection Scope
Sampling inspection or additional verification may be appropriate depending on the component risk and customer requirements.
A universal claim of 100% inspection should not be made without confirming the actual inspection plan.
Supplier Change Control
Changes to material, flange geometry, ignition-tip dimensions, surface condition or manufacturing process may affect welding behavior.
Critical changes should be reviewed according to the OEM's supplier quality requirements.
Automated CD Stud Welding and Production Integration
Automated stud welding may support repetitive manufacturing operations where the equipment and fastener geometry are compatible.
However, not every flanged CD stud is suitable for every automatic feeding system.
Fastener Characteristics Affecting Automation
Stud length
Thread diameter
Flange diameter
Flange thickness
Ignition-tip condition
Straightness
Surface condition
Dimensional variation
Packaging and orientation
Standard Flange Versus Automatic-Feed Flange
Some automated feeding systems are designed around specific flange geometries.
A standard flanged stud may require different tooling from a reduced-flange automatic-feed configuration.
The actual stud and equipment should be evaluated together.
Production Manager Considerations
Production managers may focus on positioning repeatability, welding cycle consistency, equipment maintenance,
inspection requirements, changeover time, rework and delivery planning.
These factors should be considered during process development.
Process Monitoring
Depending on the equipment, monitoring may record welding settings, cycle completion and process alarms.
These records can support troubleshooting.
However, a completed welding cycle does not automatically prove that the finished joint meets mechanical requirements.
Pilot Production Validation
Representative samples should be used to evaluate stud positioning, weld formation, mechanical performance, reverse-side appearance, tooling compatibility and assembly fit.
The validation plan should reflect the actual manufacturing requirements.
Choosing Between Flanged CD Studs and Alternative Fasteners
Different fastening methods may be appropriate depending on the substrate, installation access and assembly requirements.
Flanged CD Weld Stud
Provides a permanent externally threaded attachment using a compatible capacitor discharge welding process.
May be suitable where the flange fits the assembly and the welded joint meets the mechanical requirements.
Non-Flanged CD Weld Stud
May be preferred where a conventional flange interferes with a nut or mating bracket.
The reduced weld-base geometry requires appropriate mechanical evaluation.
CD Weld Pin
May be suitable where an unthreaded locating or stop feature is required.
It should not be treated as identical to an externally threaded stud.
CD Weld Standoff
May be appropriate where a defined spacing function or internal thread is required.
The actual configuration must be selected according to the assembly.
Self-Clinching Stud
Uses mechanical installation in a prepared hole.
May be suitable where the sheet thickness and hardness permit installation and welding is undesirable.
Self-Clinching Standoff
Provides a defined spacing function for compatible sheet metal assemblies.
Blind Rivet Nut
Provides an internal thread through mechanical deformation.
May be useful where one-sided installation access is required.
Arc Weld Stud
May be suitable for applications requiring a different stud welding process and joint design.
No fastening method is universally superior.
The correct choice depends on the mechanical, manufacturing, environmental and regulatory requirements of the assembly.
Total Installed Cost and Supplier Development
The unit price of a flanged CD stud is only one part of total installed cost.
A complete evaluation may include:
Fastener purchase price
Welding equipment and tooling
Feeding compatibility
Installation cycle time
Inspection requirements
Rework and scrap
Cleaning and packaging
Documentation requirements
Delivery planning
Why the Lowest Unit Price May Not Be the Best Choice
A lower-priced fastener may increase manufacturing cost if it introduces dimensional variation, feeding problems or additional inspection requirements.
Conversely, a higher-priced fastener does not automatically provide better welding performance.
The correct decision should be supported by actual manufacturing results.
Medical Equipment Supplier Qualification
Medical equipment OEMs may require suppliers to provide material documentation, inspection records, traceability information or other project-specific quality evidence.
These requirements should be agreed before production.
Drawing-Based Customization
Some projects require nonstandard stud lengths, flange dimensions, materials or other features.
Technical feasibility and commercial terms depend on the actual drawing and manufacturing requirements.
JUXIN FASTENERS — Flanged CD Weld Studs and OEM Fastening Solutions
JUXIN FASTENERS supplies industrial weld studs and related fastening components for international OEM manufacturing and drawing-based applications.
Relevant product families include:
Flanged CD Weld Studs
Stainless Steel Flanged CD Weld Studs
Carbon Steel CD Weld Studs
Aluminum CD Weld Studs
Metric CD Weld Studs
Unified Inch CD Weld Studs
Non-Flanged CD Weld Studs
CD Weld Pins
CD Weld Standoffs
Projection Weld Studs
Self-Clinching Fasteners
Drawing-Based Custom Fasteners
Specific dimensions, materials, surface finishes, inspection arrangements, availability and delivery terms require project-level confirmation.
Related JUXIN FASTENERS Products
Flanged CD Weld Studs — Inch / Metric
Stainless Steel Flanged CD Weld Studs
Stainless Steel Flanged CD Weld Pins
Frequently Asked Questions
What is a flanged CD weld stud?
A flanged CD weld stud is a fastener designed for capacitor discharge stud welding with a defined flange at the welding end.
Can flanged CD studs be used in medical equipment?
They may be suitable for selected medical equipment housings and non-patient-contact mechanical attachments when the material,
welded joint and assembly requirements are compatible.
Are these studs medical-grade or implantable?
Not automatically. Industrial CD weld studs should not be represented as implantable or biologically qualified without appropriate evidence.
Does stainless steel guarantee biocompatibility?
No. Biological safety depends on the intended contact conditions and the complete device evaluation.
Can CD studs be welded to thin stainless steel?
Potentially, but suitability depends on the stud geometry, sheet thickness, material and welding procedure.
Does CD welding guarantee no reverse-side marking?
No. The process may help limit thermal effects, but surface appearance must be verified.
Can flanged CD studs be used in cleanrooms?
Potentially, but cleanroom compatibility depends on the manufacturing process, contamination controls, cleaning and packaging requirements.
Are 304 and 316 stainless steel interchangeable?
Not automatically. Their corrosion behavior and suitability depend on the environment and cleaning conditions.
Does ISO 13485 certification automatically apply to industrial fastener suppliers?
No. Certification status and regulatory obligations depend on the supplier's actual quality management system, role and applicable requirements.
Does ISO 10993-1 apply to every fastener inside medical equipment?
No. Its applicability depends on the device's intended patient-contact conditions and biological safety evaluation.
Are metric and UNC threads interchangeable?
No. Metric, UNC and UNF threads are different systems.
Can flanged CD studs be automatically fed?
Certain configurations may be suitable for automated feeding, but compatibility depends on the actual stud and equipment.
Does passing a torque test prove adequate weld strength?
Not necessarily. Torque resistance, axial strength and shear performance are different characteristics.
Can JUXIN FASTENERS review custom OEM drawings?
Drawing-based requirements may be submitted for technical and commercial evaluation, including dimensions, material,
flange geometry, thread specification, inspection requirements and purchasing volume.
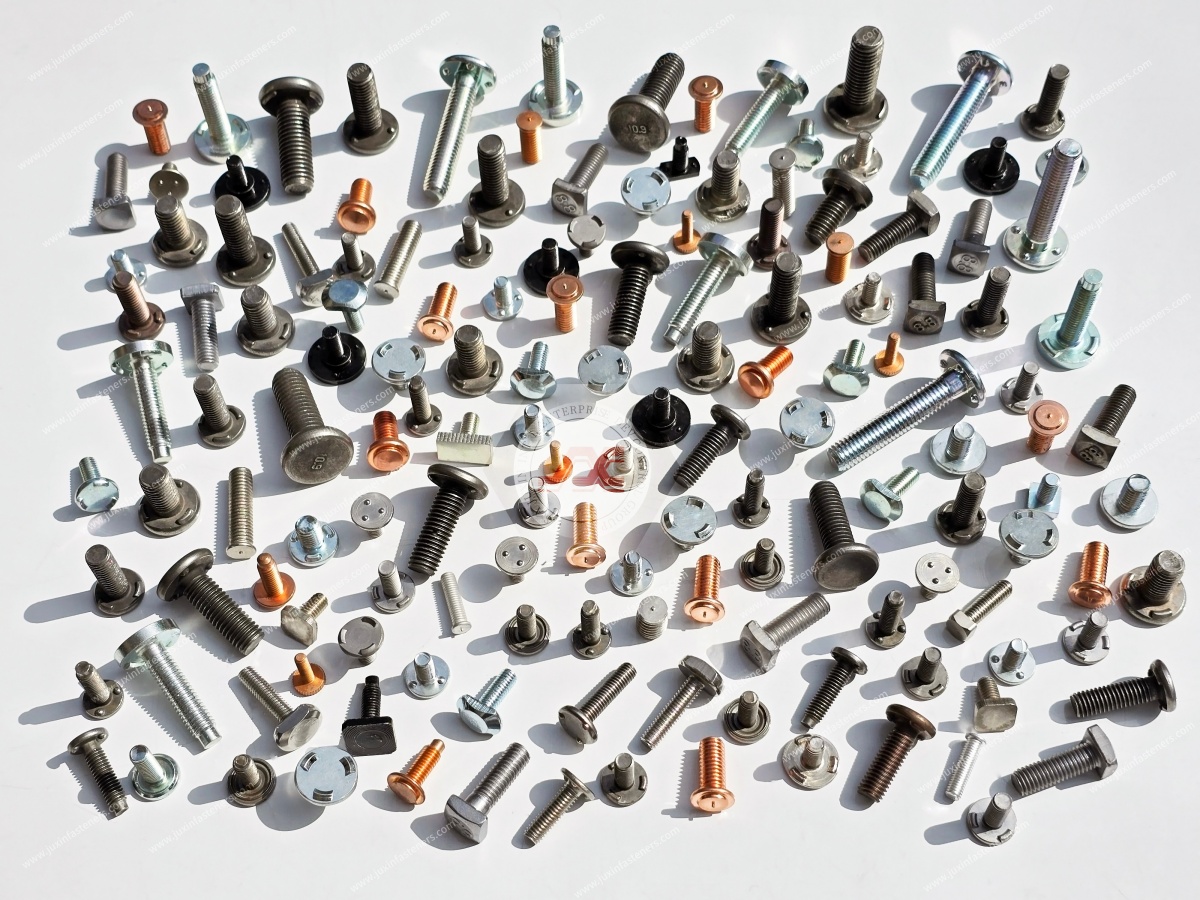
OEM RFQ — Flanged CD Weld Studs for Medical Equipment Manufacturing
JUXIN FASTENERS welcomes inquiries from diagnostic equipment manufacturers, laboratory instrument OEMs,
medical imaging equipment manufacturers, hospital equipment producers, precision sheet metal fabricators,
design engineers, manufacturing engineers, production managers and international procurement teams.
For technical evaluation and quotation, please provide the following information where applicable.
Engineering Drawings and Product Specifications
2D engineering drawing with revision
3D CAD model where available
Metric or Unified inch thread specification
Thread diameter, pitch and tolerance class
Stud length
Flange diameter and thickness
Ignition-tip geometry
Material grade
Surface finish
Critical dimensional tolerances
Application and Welding Requirements
Parent-sheet material and thickness
Capacitor discharge welding equipment
Contact or gap welding process
Mechanical loading requirements
Assembly tightening torque
Reverse-side appearance requirements
Cleaning and corrosion exposure
Cleanliness requirements
Patient-contact classification, where relevant
Inspection and testing requirements
Quality and Commercial Requirements
Prototype or sample quantity
Estimated annual purchasing volume
Minimum order quantity expectations
Material documentation requirements
Traceability requirements
Packaging specification
Required delivery schedule
Supplier quality requirements
Engineering change-control requirements
Complete engineering information helps reduce clarification cycles and supports accurate product evaluation and quotation.
Company: Juxin Fasteners
Website: https://www.juxinfasteners.com/
Email: info@juxinfasteners.com
For flanged capacitor discharge weld studs, stainless steel CD weld screws, inch and metric threaded studs and drawing-based fastening
components for medical equipment enclosures, contact JUXIN FASTENERS with your drawings and project requirements.
Our team can review the supplied specifications and discuss suitable product options,
manufacturing feasibility, inspection requirements and commercial arrangements for your OEM project.
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY



