
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Jul. 26, 2024
High Strength Screw Grades 8.8, 10.9 and 12.9: Engineering Selection and OEM Fastening Solutions
High strength screws are essential fastening components in industrial machinery, automotive systems, hydraulic equipment, construction machinery and precision mechanical assemblies.
They are selected for applications requiring defined mechanical strength, reliable clamp load and resistance to demanding service conditions.
However, selecting a high tensile screw is not simply a matter of choosing the highest available strength class.
A Class 12.9 screw is not automatically a better engineering solution than a Class 10.9 or Class 8.8 screw.
The correct selection depends on the joint design, service loads, mating materials, installation method, environmental exposure and required reliability.
For design and mechanical engineers, the main questions involve tensile strength, proof load, preload, thread engagement, fatigue behavior and joint stiffness.
For manufacturing engineers and production managers, the priorities include tightening consistency, friction variation, assembly cycle time, tooling, rework and production-line reliability.
For procurement and supplier development teams, the decision also involves material specifications, dimensional standards, surface treatments,
inspection requirements, manufacturing feasibility, MOQ, lead time and long-term supply consistency.
This guide explains how to select metric high strength screws in property classes 8.8, 10.9 and 12.9, with practical engineering considerations for OEM manufacturing and industrial assembly.
What Are High Strength Screws?
High strength screws are threaded fasteners manufactured to meet defined mechanical-property requirements.
In metric industrial fastening, common carbon steel and alloy steel property classes include:
Property Class 8.8
Property Class 10.9
Property Class 12.9
These designations are associated with the ISO 898-1 mechanical-property system for applicable bolts, screws and studs.
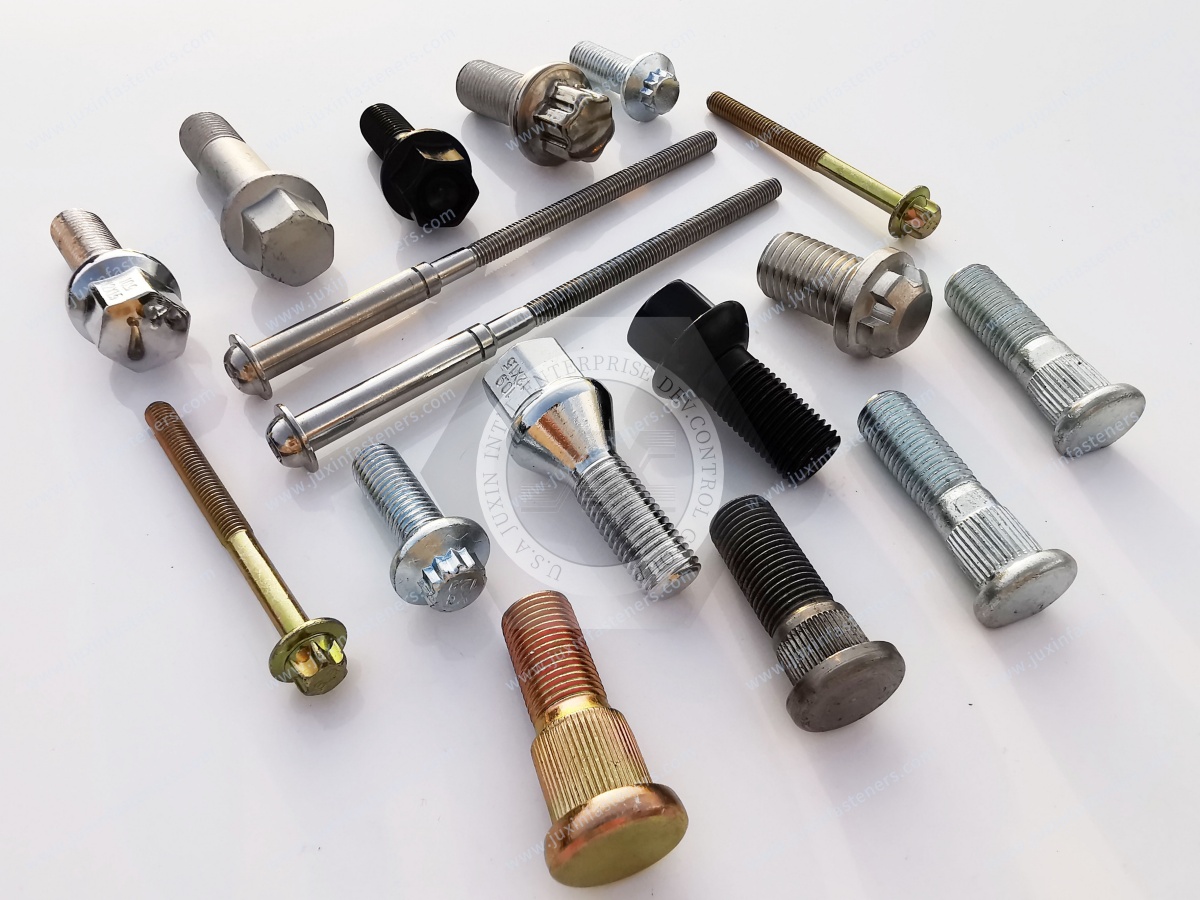
Important Engineering Distinction
The correct technical terminology is property class, rather than treating 8.8, 10.9 and 12.9 as interchangeable material grades.
A property class defines mechanical requirements, but does not by itself identify a single steel composition, heat-treatment route or surface coating.
Understanding ISO Metric Screw Property Classes
The ISO metric property-class designation provides an indication of specified strength characteristics.
For common property classes:
| Property class | Nominal tensile strength represented by designation | Nominal yield or proof-strength relationship indicated by designation |
|---|---|---|
| 8.8 | 800 MPa | 0.8 |
| 10.9 | 1,000 MPa | 0.9 |
| 12.9 | 1,200 MPa | 0.9 |
These values explain the designation system.
Important Limitation
Actual specified minimum tensile strength, proof stress, yield-related requirements and testing criteria must be taken from the applicable edition of ISO 898-1.
They may depend on nominal diameter and other conditions.
The nominal values above should not be used as substitutes for standard-based engineering calculations.
Property Class 8.8 Screws: Balanced Strength and Industrial Versatility
Class 8.8 screws are widely used in general industrial machinery and mechanical assemblies.
They are often selected where a balance of mechanical strength, manufacturing practicality and cost is required.
Typical Applications
General machinery
Industrial equipment
Automation systems
Agricultural machinery
Mechanical brackets
Equipment frames
Engineering Advantages
Suitable strength level for many industrial joints
Broad use in standard metric fastening systems
Potentially economical compared with higher property classes
Applicable to many conventional bolted-joint designs
Important Limitation
Class 8.8 does not automatically mean that a screw is suitable for every structural or safety-critical application.
Engineering Recommendation
Verify the required preload, proof load, joint geometry and service loads before specifying Class 8.8.
Property Class 10.9 Screws: Higher Strength for Demanding Assemblies
Class 10.9 screws are commonly selected where greater fastener strength is required.
They may allow higher specified preload than Class 8.8 screws of the same geometry, provided the joint and installation system are designed accordingly.
Potential Applications
Automotive powertrain-related equipment
Industrial machinery
Hydraulic assemblies
Heavy equipment
High-load brackets
Selected EV equipment structures
Engineering Advantages
Higher mechanical-strength capability
Potential for increased clamp load in a properly designed joint
Useful for selected high-load applications
Important Engineering Limitation
Higher tensile strength does not automatically improve fatigue life or vibration resistance.
The complete joint must be evaluated.
Engineering Recommendation
Select Class 10.9 when its strength capability is needed and the mating components can safely support the intended preload.
Property Class 12.9 Screws: Very High Strength With Additional Design Considerations
Class 12.9 screws are used in selected applications requiring high mechanical strength.
They are commonly associated with certain high-strength socket head cap screw designs and other specialized industrial fasteners.
Potential Applications
Precision machinery
High-load mechanical assemblies
Selected transmission-related equipment
Industrial tooling
Specialized equipment
Engineering Advantages
High tensile-strength capability
Potentially useful where space constraints limit fastener diameter
Suitable for selected demanding mechanical joints
Important Engineering Limitations
Class 12.9 fasteners require careful attention to:
Joint design
Installation preload
Material and heat treatment
Surface treatment
Hydrogen embrittlement susceptibility
Environmental exposure
Application-specific validation
Engineering Recommendation
Do not upgrade from Class 10.9 to Class 12.9 solely because the higher number appears stronger.
8.8 vs 10.9 vs 12.9: Which High Strength Screw Should You Choose?
| Selection factor | Class 8.8 | Class 10.9 | Class 12.9 |
|---|---|---|---|
| Relative tensile-strength class | High | Higher | Very high |
| Typical design priority | General industrial strength | Higher-load joints | Specialized high-strength joints |
| Preload capability | Application-dependent | Potentially higher | Potentially higher |
| Fatigue performance | Joint-dependent | Joint-dependent | Joint-dependent |
| Hydrogen embrittlement concern | Process and application dependent | Greater attention may be required | Particularly important |
| Surface treatment | Must be qualified | Must be qualified | Requires careful review |
| Relative cost | Often economical | Often higher | Often higher |
| Preferred selection basis | Required joint performance | Required joint performance | Required joint performance |
Information Gain: Stronger Screws Do Not Necessarily Create Stronger Joints
A high-strength screw may remain intact while the joint fails through:
Internal thread stripping
Bearing surface deformation
Joint separation
Fatigue cracking
Mating component failure
Excessive preload
Engineering Recommendation
Evaluate the fastener and the surrounding joint as one mechanical system.
Tensile Strength, Yield Strength and Proof Load
Three mechanical concepts are important when selecting high strength screws.
Tensile Strength
The stress associated with failure during a tensile test under defined conditions.
Yield Strength
The stress associated with the onset of specified plastic deformation behavior.
Proof Load
A specified load used to evaluate whether a fastener meets relevant proof-loading requirements.
Important Engineering Distinction
Proof load is not the same as ultimate tensile load.
Engineering Recommendation
Use the applicable standard values and the fastener's tensile stress area when performing design calculations.
Preload: The Foundation of Bolted-Joint Reliability
Preload is the tensile force developed in a screw or bolt during tightening.
The resulting clamp force holds the joint members together.
Why Preload Matters
Appropriate preload can help:
Maintain joint contact
Reduce separation under service loads
Improve load transfer
Reduce some fatigue-related risks
Support joint stability
Important Limitation
Excessive preload can damage the fastener, internal threads or clamped components.
Engineering Recommendation
Define an acceptable preload range based on the complete joint design.
Why Higher Strength Does Not Automatically Improve Fatigue Resistance
Bolted-joint fatigue depends on how external loads are transferred through the joint.
Important factors include:
Initial preload
Joint stiffness
Fastener stiffness
Load direction
Thread geometry
Surface condition
Stress concentration
Joint separation
Information Gain: Joint Stiffness Can Matter More Than Property-Class Upgrading
If a joint separates under service load, a higher-strength screw may not resolve the underlying fatigue problem.
Engineering Recommendation
Review preload retention, clamped-member stiffness and external load transfer before increasing the screw property class.
High Strength Hex Head Screws
Hex head screws are commonly used in industrial assemblies requiring wrench or socket installation.
Typical Applications
Machinery frames
Equipment mounting
Mechanical brackets
Industrial assemblies
Engineering Considerations
Head dimensions
Tool clearance
Bearing area
Thread length
Fastener strength class
Installation access
Important Limitation
A fully threaded hex head screw and a partially threaded hex bolt may not perform identically in a joint.
Engineering Recommendation
Confirm the grip length and whether the shear plane passes through the threaded or unthreaded portion.
High Strength Flange Head Screws
High strength flange screws combine an external hex head with an integrated flange.
The flange may increase the bearing area and simplify certain assemblies.
Potential Advantages
Integrated bearing surface
Reduced need for a separate washer in suitable designs
Potentially improved assembly efficiency
Simplified parts handling
More consistent component count
Important Engineering Limitation
A flange does not automatically provide vibration resistance or eliminate the need for joint validation.
Engineering Recommendation
Check the bearing surface, mating material, flange geometry and tightening behavior.
High Strength Socket Head Cap Screws
Socket head cap screws are often used where compact head geometry and internal-drive installation are beneficial.
Potential Applications
Precision machinery
Tooling
Automation equipment
Mechanical assemblies with restricted access
Engineering Considerations
Socket engagement
Tool accessibility
Head clearance
Material strength
Tightening method
Important Limitation
Not every socket head cap screw is Class 12.9.
Engineering Recommendation
Specify the applicable dimensional standard and mechanical-property class independently.
Thread Engagement and Internal Thread Strength
A high-strength screw requires a mating internal thread capable of supporting the intended load.
Potential Failure Modes
Internal thread stripping
Bolt thread stripping
Pull-out
Local deformation
Joint loosening
Information Gain: A Class 12.9 Screw Can Be Limited by a Lower-Strength Nut or Tapped Hole
The external screw property class alone does not establish the capacity of the threaded connection.
Engineering Recommendation
Evaluate the mating nut property class or tapped-hole material and effective thread engagement.
Coarse vs Fine Metric Threads
Metric coarse and fine threads have different pitches and geometric characteristics.
Coarse Threads
Often selected for general-purpose industrial assembly.
Fine Threads
May be useful where specific adjustment, engagement or geometric requirements apply.
Important Engineering Limitation
Fine threads are not inherently vibration-proof.
Their suitability depends on the complete joint design.
Engineering Recommendation
Select thread pitch according to the application, mating component and required installation behavior.
Vibration Loosening and High Strength Screws
Vibration-related loosening can occur even when high-strength screws are used.
Important Factors
Preload
Joint stiffness
Transverse displacement
Friction
Surface embedding
Thermal cycling
Joint geometry
Potential Locking Options
Prevailing torque nuts
All-metal lock nuts
Nylon insert lock nuts where temperature permits
Serrated flange fasteners where appropriate
Thread-locking systems
Mechanical locking devices
Important Limitation
A higher property class is not itself a locking mechanism.
Engineering Recommendation
Select and validate the locking strategy according to the service conditions.
Torque-Tension Relationship in High Strength Screw Assembly
Tightening torque is commonly used to develop fastener preload.
However, torque does not directly measure clamp load.
The relationship is influenced by friction.
Important Variables
Thread friction
Bearing surface friction
Lubrication
Coating
Washer condition
Installation speed
Fastener geometry
Information Gain: Two Screws With the Same Strength Class Can Produce Different Preloads at the Same Torque
Differences in coating or lubrication can change the torque-tension relationship.
Engineering Recommendation
Validate tightening parameters using the actual screw, nut, coating and mating components.
ISO 16047 and Torque-Clamp Force Testing
ISO 16047 addresses torque/clamp force testing for threaded fasteners under its applicable scope.
It can support evaluation of tightening behavior.
Important Limitation
A test performed on one fastener configuration does not automatically establish the tightening behavior of every coating, material or production batch.
Production Recommendation
Define the relevant friction and installation requirements during qualification.
Hydrogen Embrittlement in High Strength Steel Screws
Hydrogen embrittlement is an important consideration for susceptible high-strength steel fasteners.
Hydrogen may enter the material during certain manufacturing, surface-treatment or service processes.
Under unfavorable conditions, delayed cracking or fracture may occur.
Potential Risk Factors
High material strength or hardness
Hydrogen-generating processing
Certain electroplating operations
Aggressive service environments
Sustained tensile stress
Important Engineering Limitation
Not every high-strength screw will experience hydrogen embrittlement.
Risk depends on material, process and service conditions.
Information Gain: Surface Coating Selection Is Part of Mechanical Reliability
A coating process may improve corrosion resistance while introducing other risks if not properly controlled.
Engineering Recommendation
For susceptible high-strength fasteners, review the complete manufacturing and coating process, applicable requirements and validation strategy.
Zinc-Plated High Strength Screws
Zinc electroplating is used for corrosion protection in many industrial fastening applications.
Potential Applications
General machinery
Industrial equipment
Selected automotive components
Indoor equipment
Important Engineering Considerations
Coating thickness
Thread fit
Corrosion requirements
Friction behavior
Hydrogen embrittlement controls
Important Limitation
Zinc electroplating is not automatically appropriate for every Class 10.9 or Class 12.9 application.
Engineering Recommendation
Confirm coating-process suitability and required safeguards before approval.
Zinc-Nickel Coated High Strength Screws
Zinc-nickel coatings are used in selected automotive and industrial applications requiring defined corrosion performance.
Potential Advantages
Corrosion protection
Compatibility with selected automotive specifications
Application-specific surface performance
Important Engineering Limitation
Performance depends on coating composition, process, thickness, passivation, topcoat and test conditions.
Engineering Recommendation
Specify the required coating system and acceptance criteria rather than relying only on the term zinc-nickel.
Zinc-Flake Coated High Strength Screws
Zinc-flake coating systems may be used for selected high-strength fasteners.
They are often considered where corrosion performance and process-related hydrogen embrittlement risk are important.
Potential Applications
Automotive fasteners
Heavy equipment
Industrial machinery
Outdoor mechanical assemblies
Important Engineering Limitation
Not every zinc-flake system has identical corrosion or friction performance.
Engineering Recommendation
Confirm the coating specification, application process, thread fit and torque-tension requirements.
Black Oxide and Phosphate Finishes
Black oxide and phosphate finishes are used in selected industrial applications.
Potential Considerations
Appearance
Surface condition
Lubrication retention
Assembly behavior
Limited corrosion protection without suitable additional measures
Important Limitation
A black finish should not automatically be described as a high-performance corrosion-resistant coating.
Engineering Recommendation
Separate appearance requirements from corrosion-performance requirements.
Coating Selection Comparison
| Surface treatment | Main consideration | Important qualification requirement |
|---|---|---|
| Zinc electroplating | General corrosion protection | Hydrogen embrittlement and thread-fit controls |
| Zinc-nickel coating | Defined corrosion protection | Coating system and friction requirements |
| Zinc-flake coating | Selected industrial corrosion protection | Coating process, thickness and torque behavior |
| Black oxide | Appearance and surface condition | Corrosion limitations |
| Phosphate finish | Surface condition and lubrication compatibility | Additional protection where required |
Information Gain: Corrosion Protection and Tightening Performance Must Be Qualified Together
Changing a coating can alter the friction behavior of a high-strength screw.
Production Recommendation
Revalidate tightening parameters when coating systems or lubrication conditions change.
Automotive and EV High Strength Fastening
Automotive and EV systems contain many joints requiring defined mechanical strength and installation control.
Potential Applications
Powertrain-related assemblies
Motor housings
Equipment brackets
Selected chassis components
EV equipment structures
Battery-related mechanical assemblies
Engineering Considerations
Preload
Vibration
Fatigue
Corrosion exposure
Thermal cycling
Assembly traceability
Critical Limitation
Safety-critical automotive joints, suspension systems and battery structural connections require approved OEM specifications and application-specific validation.
Engineering Recommendation
Use the specified property class and coating only after joint-level qualification.
Industrial Machinery and Automation
High strength screws are widely used in machinery and automated equipment.
Potential Applications
CNC machinery
Industrial robots
Machine frames
Linear motion equipment
Mechanical brackets
Hydraulic systems
Engineering Considerations
Joint stiffness
Installation access
Service loads
Maintenance
Preload retention
Production Recommendation
Standardize approved screw specifications and tightening procedures.
Construction Machinery and Heavy Equipment
Heavy equipment may expose fasteners to demanding mechanical loads and environmental conditions.
Potential Applications
Excavators
Agricultural machinery
Mining equipment
Industrial lifting equipment
Heavy mechanical assemblies
Engineering Considerations
Fatigue
Shock loading
Vibration
Corrosion
Maintenance
Mechanical safety
Important Limitation
High strength fasteners for regulated structural or lifting applications must meet the applicable engineering and approval requirements.
Hydraulic Equipment and Power Systems
Hydraulic and power equipment may use high-strength screws in suitable mechanical joints.
Potential Applications
Hydraulic equipment housings
Pump assemblies
Motor mounts
Industrial power equipment
Mechanical support structures
Engineering Considerations
Cyclic loading
Preload
Joint separation
Sealing interfaces
Temperature
Engineering Recommendation
Evaluate fastener preload together with gasket, sealing and joint-stiffness requirements.
Electrical and Electronic Equipment
High strength screws may be used in selected electrical and electronic equipment structures.
Potential Applications
Equipment frames
Industrial cabinets
Power conversion equipment
Mechanical support assemblies
Communication equipment
Engineering Considerations
Joint loading
Electrical clearance
Thermal cycling
Corrosion
Assembly accessibility
Important Limitation
A high-strength screw does not automatically establish electrical bonding, conductivity or high-voltage safety compliance.
Railway and Transportation Equipment
Transportation-related mechanical assemblies may require controlled strength and fatigue performance.
Engineering Considerations
Dynamic loading
Vibration
Fatigue
Corrosion
Maintenance
Traceability
Important Limitation
Railway safety-critical fastening systems require applicable sector-specific approval and validation.
Manufacturing Engineering: Controlling High Strength Screw Installation
Reliable fastening in mass production requires consistent control of the screw, mating components and installation process.
Critical Production Variables
Fastener property class
Thread dimensions
Coating condition
Lubrication
Mating nut or tapped-hole specification
Tightening tool
Installation speed
Torque or angle control
Joint seating behavior
Potential Production Problems
Insufficient preload
Excessive preload
Thread stripping
Screw fracture
Damaged drive features
Joint separation
Rework
Information Gain: Assembly Process Capability Matters as Much as Fastener Strength
A high-strength screw that meets dimensional and mechanical requirements may still produce inconsistent clamp load if friction varies significantly.
Production Recommendation
Validate the fastening process using representative production components.
Torque-Controlled vs Torque-Angle Tightening
Different tightening strategies may be used depending on the joint.
Torque-Controlled Tightening
Uses a specified tightening torque.
Torque-Angle Tightening
Uses a defined torque and angular displacement strategy.
Important Engineering Limitation
Neither method is universally superior.
The appropriate strategy depends on joint behavior, friction variation and the required preload.
Engineering Recommendation
Select the tightening strategy through application-specific validation.
High Strength Screw Inspection and Quality Requirements
OEM fastener qualification should address both product conformity and assembly performance.
Dimensional Inspection
Diameter
Thread pitch
Thread tolerance
Length
Head geometry
Drive dimensions
Mechanical Verification
Applicable property class
Tensile requirements
Proof-load requirements
Hardness requirements
Other tests required by the standard or drawing
Surface Inspection
Coating specification
Coating thickness
Surface condition
Thread fit
Corrosion requirements
Assembly Verification
Torque-tension behavior
Installation process
Mating components
Joint performance
Important Limitation
Not every test applies to every fastener size, geometry or product category.
Engineering Recommendation
Define inspection and test requirements according to the applicable standard and approved drawing.
International Standards for High Strength Screws
Relevant standards depend on the product geometry and intended application.
ISO 898-1
Mechanical properties of applicable carbon steel and alloy steel bolts, screws and studs.
ISO 4017
Hexagon head screws.
ISO 4014
Hexagon head bolts.
ISO 4162
Hexagon flange bolts, small series.
ISO 4762
Hexagon socket head cap screws.
ISO 16047
Torque/clamp force testing for threaded fasteners.
SAE J429
Mechanical and material requirements for applicable inch-series externally threaded fasteners.
ASME B18.2.1
Dimensional requirements for applicable inch-series square and hex bolts and screws.
Important Standards Distinction
A dimensional standard does not automatically define every mechanical, coating or assembly requirement.
Engineering Recommendation
Specify the product geometry, property class, material requirements, surface treatment and inspection criteria separately.
Metric Property Classes vs SAE Grades
Metric property classes and SAE grades belong to different specification systems.
Metric Examples
Class 8.8
Class 10.9
Class 12.9
Inch-Series Examples
SAE Grade 5
SAE Grade 8
Important Engineering Limitation
SAE Grade 8 is not the same designation as ISO Property Class 8.8.
The systems have different requirements and should not be treated as directly interchangeable.
Metric, UNC, UNF and British Thread Systems
Metric threads, Unified inch threads and British thread systems must be identified separately.
Metric Examples
M6
M8
M10
M12
Unified Inch Examples
1/4-20 UNC
5/16-18 UNC
3/8-16 UNC
Important Limitation
Metric, UNC, UNF, BSW and BSF threads are not directly interchangeable.
Approximate inch conversions are dimensional references only.
Engineering Recommendation
Confirm the full thread designation and applicable standard before approving an alternative fastener.
OEM Supplier Qualification for High Strength Screws
Supplier development and procurement teams should evaluate both technical conformity and commercial suitability.
Product Definition
Approved drawing or standard
Part number and revision
Screw geometry
Thread designation
Property class
Material requirements
Surface treatment
Quality Requirements
Dimensional inspection
Mechanical-property verification
Coating requirements
Functional testing where specified
Documentation
Change control
Production Requirements
Prototype quantities
Batch quantities
Annual demand
Packaging
Traceability where required
Delivery schedule
Commercial Requirements
MOQ
Lead time
Pricing structure
Supply continuity
Approved substitutions
Information Gain: Fastener Supplier Qualification Should Include Assembly Performance
A supplier may provide a screw that meets ISO mechanical requirements,
but the final assembly can still fail if coating friction or mating-thread compatibility differs from the approved configuration.
Procurement Recommendation
Evaluate fastener conformity and joint-level performance separately.
Total Cost of Ownership for High Strength Fasteners
Fastener purchasing decisions should consider more than unit price.
Potential Cost Drivers
Material and heat treatment
Manufacturing process
Surface coating
Inspection
Packaging
Assembly cycle time
Rework
Maintenance
Supply reliability
Information Gain: The Lowest Unit Price May Not Produce the Lowest Assembly Cost
A fastener with inconsistent coating friction may increase assembly variation and rework.
Procurement Recommendation
Compare qualified suppliers using total installed cost and supply reliability.
Frequently Asked Questions
What is the difference between Class 8.8, 10.9 and 12.9 screws?
They are ISO metric mechanical-property classes with different specified strength requirements. Selection should be based on the complete joint design.
Is Class 12.9 always stronger than Class 10.9?
Class 12.9 has a higher nominal tensile-strength designation, but it is not automatically the better choice for every application.
Are Class 10.9 screws more vibration-resistant than Class 8.8?
Not inherently. Vibration resistance depends on preload, joint geometry, friction and locking strategy.
Can Class 12.9 screws be zinc plated?
Coating suitability requires careful evaluation of hydrogen embrittlement risk, applicable specifications and process controls.
What is the difference between SAE Grade 8 and ISO Class 8.8?
They belong to different mechanical-property systems and are not equivalent designations.
Are fine-thread high strength screws better for vibration?
Not automatically. Thread pitch alone does not guarantee resistance to loosening.
Do high strength flange bolts eliminate the need for washers?
They may eliminate separate washers in some approved joint designs, but not in every application.
How should installation torque be selected?
Torque should be validated using the actual fastener, coating, mating components and joint requirements.
Can high strength screws be used outdoors?
Yes, in suitable applications with appropriate corrosion protection and environmental qualification.
What should be included in an OEM high strength screw RFQ?
Provide the approved drawing, property class, dimensions, thread designation, coating requirements, assembly conditions and purchasing quantities.
Juxin Fasteners: High Strength Screws and OEM Industrial Fastening Solutions
Juxin Fasteners supplies industrial fastening components for OEM manufacturing and mechanical assemblies.
Relevant product categories include:
Class 8.8 high strength screws
Class 10.9 high tensile screws
Class 12.9 high strength screws
Metric hex head screws
Hexagon bolts
High strength flange screws
Socket head cap screws
Automotive fastening components
Custom OEM screws and bolts
Specific property classes, materials, dimensions, manufacturing methods, coatings, inspection requirements, samples,
MOQ and delivery schedules are subject to technical and commercial confirmation.
Request a High Strength Screw RFQ
Are you developing a new high-load mechanical assembly?
Do you need to compare Class 8.8, 10.9 and 12.9 fasteners, improve tightening consistency or qualify an alternative OEM screw supplier?
Juxin Fasteners welcomes drawing-based inquiries from design engineers, manufacturing teams, production managers, procurement specialists and supplier development teams.
For technical review and quotation, please provide:
Approved drawing or standard + part number and revision + screw geometry + nominal diameter and length + thread designation and tolerance
+ property class + material requirements + surface coating + mating components + installation method
+ preload or torque requirements + corrosion environment + inspection criteria + prototype quantity + annual demand + batch size + packaging + target delivery schedule.
Company: Juxin Fasteners
Website: https://www.juxinfasteners.com/
Email: info@juxinfasteners.com
Send your high strength screw drawings and OEM RFQ to Juxin Fasteners for technical review and quotation.
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY



