
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Nov. 16, 2024
ISO 16047 Torque–Clamp Force Testing: Fastener Friction Measurement, OEM Validation and Assembly Quality
A fastener's mechanical property class does not, by itself, determine the clamp force achieved during tightening.
In a bolted joint, the relationship between applied torque and generated axial load depends on thread geometry, friction at contacting surfaces, lubrication, coating condition and the mating components.
For automotive OEMs, electric vehicle manufacturers, industrial equipment producers and other high-volume assembly operations,
variation in these factors can create inconsistent clamp loads even when the same tightening torque is applied.
ISO 16047 — Fasteners — Torque/clamp force testing provides a standardized framework for measuring torque–clamp force behavior under defined test conditions.
The results help engineers understand tightening characteristics, compare specified surface conditions and evaluate whether a fastener system is suitable for further assembly validation.
At Juxin Fasteners, we supply standard and drawing-specific industrial fasteners, including bolts, screws, nuts and threaded fastening components.
Where an OEM project requires torque–clamp force testing, the applicable test configuration, acceptance criteria, documentation and supply feasibility should be confirmed during technical review.
This guide explains the test principles, important measured parameters, common interpretation errors and practical considerations for production engineers, quality teams and purchasing departments.
What Is ISO 16047 Torque–Clamp Force Testing?
ISO 16047 specifies a test method for evaluating the relationship between tightening torque and clamp force in threaded fasteners under controlled conditions.
The method supports the determination of tightening characteristics and, where the required measurements and test configuration are available, friction-related parameters.
The principal purpose is to generate comparable test data under clearly defined conditions.
It is not a universal certification of joint safety, nor does a successful test establish that a fastener will maintain the same clamp force throughout its service life.
What the Test Can Help Determine
Applied tightening torque
Generated clamp force
Torque–clamp force relationship
Thread and bearing friction characteristics where appropriately measured
Total friction characteristics under the specified method
Variation between tested samples
Influence of surface treatment and lubrication
The actual parameters reported depend on the test equipment, procedure and customer specification.
Why Tightening Torque Is Not the Same as Clamp Force
Tightening torque is a rotational moment applied to a fastener.
Clamp force is the compressive force acting across the joint, associated with the axial tension developed in the fastener.
During tightening, torque is consumed by several mechanisms, particularly friction at the threads and under the rotating bearing surface.
Therefore, identical tightening torque does not necessarily produce identical clamp force.
A change in lubricant, coating, washer or mating nut may alter the result even when the bolt itself remains unchanged.
The Main Parameters in an ISO 16047 Test
| Parameter | Meaning | Why it matters |
|---|---|---|
| Tightening torque | Rotational moment applied during tightening | Defines the applied tightening input |
| Clamp force | Axial load developed in the test assembly | Indicates achieved fastening load |
| Thread torque | Torque contribution associated with the threaded interface | Supports thread friction evaluation |
| Bearing torque | Torque contribution at the rotating bearing interface | Supports bearing friction evaluation |
| Thread friction coefficient | Friction behavior of mating threads | Influences torque needed to develop preload |
| Bearing friction coefficient | Friction behavior beneath the rotating head or nut | Influences torque consumption at the bearing surface |
| Total friction coefficient | Combined friction characteristic under the defined method | Useful for specified friction-performance comparisons |
Important Distinction
The test cannot independently determine every friction component unless the necessary measurements and assumptions are supported by the selected configuration.
How ISO 16047 Testing Works
A typical torque–clamp force test uses a suitable tightening arrangement with instrumentation for measuring applied torque and clamp force.
Depending on the required parameters, additional measurements may be used to distinguish torque contributions.
The fastener is tightened under the prescribed conditions while measurement equipment records the relevant values.
The resulting data may be presented as a torque–clamp force curve or as specified numerical results.
A Practical Test Sequence
Identify the fastener, mating components and surface conditions.
Prepare the test arrangement according to the selected procedure.
Verify the required measurement equipment and test conditions.
Tighten the fastener while recording the specified parameters.
Evaluate the results against the agreed acceptance criteria.
Document the configuration, results and relevant observations.
The detailed procedure must follow the applicable edition of ISO 16047 and the customer-approved test specification.
Why the Test Assembly Must Be Defined
The measured behavior belongs to the tested combination, not simply to an isolated bolt.
A bolt tested against one nut and washer combination may produce different results when used with another nut, bearing surface or lubricant.
This distinction is particularly important when comparing suppliers or validating a surface coating change.
Engineering Recommendation
Always identify the mating components and surface conditions in the test request and report.
Torque–Clamp Force Curves: How to Interpret the Results
A torque–clamp force curve illustrates how clamp force develops as tightening torque increases.
The curve can help engineers identify differences in tightening behavior between samples or surface conditions.
For example, if two otherwise comparable test assemblies develop different clamp forces at the same torque, their combined tightening characteristics differ.
However, the curve alone may not identify the root cause. Differences may arise from thread friction, bearing friction, seating behavior or other aspects of the test configuration.
What Engineers Should Review
Clamp force at the specified evaluation point
Torque required to reach a defined clamp force
Variation between samples
Unexpected changes in the curve
Test configuration and surface condition
Any visible thread or bearing damage
Important Limitation
A smooth torque–clamp force curve does not prove that the assembled joint will resist fatigue, vibration loosening, corrosion or long-term relaxation.
Thread Friction and Bearing Friction
The two principal friction interfaces should be considered separately.
Thread Friction
Thread friction occurs between the mating internal and external threads. It is affected by thread geometry, coating, lubricant, roughness and mating material.
Bearing Friction
Bearing friction occurs beneath the rotating bolt head or nut. It depends on the bearing diameter, contact pressure, surface finish, washer condition and lubrication.
A fastener coating may influence both interfaces, but not necessarily by the same amount.
Engineering Recommendation
Where an OEM specification requires individual friction coefficients, confirm that the proposed test configuration supports the necessary measurements.
Torque Coefficient or K-Factor
The simplified torque–preload relationship is commonly expressed as:
T = K × F × d
Where:
T = tightening torque
K = dimensionless torque coefficient or nut factor
F = axial preload
d = nominal thread diameter
This expression is useful for understanding the approximate relationship between torque and preload under defined conditions.
However, K is not the same as the thread friction coefficient or bearing friction coefficient.
It combines several influences and must not be assumed to remain constant across different coatings, mating surfaces or assembly conditions.
ISO 16047 Versus VDI 2230
These references serve different engineering purposes.
| Reference | Primary purpose | Practical use |
|---|---|---|
| ISO 16047 | Torque–clamp force testing | Measuring tightening behavior under specified test conditions |
| VDI 2230 | Systematic calculation of highly loaded bolted joints | Evaluating joint loading, preload requirements, stresses and related design considerations |
| Production tightening specification | Controlling the actual assembly process | Defining tool settings, monitoring limits and acceptance criteria |
Engineering Recommendation
Use ISO 16047 data as relevant input to the fastening-engineering process, not as a substitute for joint design calculations or production validation.
How Surface Coatings Influence Test Results
Fastener surface treatments affect corrosion resistance, appearance, friction and assembly behavior.
Common coating systems for suitable industrial fasteners include electroplated zinc, zinc-nickel and zinc-flake systems.
Other finishes and lubricated topcoats may be specified for particular applications.
The coating's friction behavior depends on the complete system, including supplementary sealers or lubricants.
A coating that provides suitable corrosion protection does not automatically provide the friction range required by an OEM tightening specification.
Electroplated Zinc Fasteners
Zinc-plated bolts may exhibit different friction characteristics depending on the plating, passivation, sealer and lubricant system.
Zinc-Nickel Fasteners
Zinc-nickel coatings may be selected for particular corrosion requirements,
but their tightening behavior must be evaluated with the actual supplementary treatment.
Zinc-Flake Coated Fasteners
Zinc-flake systems may incorporate topcoats that influence friction.
Test results should identify the coating system and relevant surface condition.
Stainless Steel Fasteners
Stainless steel threaded fasteners may require attention to galling, surface finish, lubrication and mating material.
Engineering Recommendation
Do not compare coating systems solely by their nominal corrosion rating.
Evaluate torque–clamp force behavior under the specified conditions.
Lubrication and Test Repeatability
Lubrication can change the torque needed to achieve a particular clamp force.
A lubricant applied inconsistently may increase variation between samples. Storage conditions, handling and repeated tightening can also affect surface behavior.
Engineering Recommendation
State whether the test specimens are dry, prelubricated or treated with an assembly lubricant, and define whether the specimens are new or previously tightened.
Tightening Speed and Test Conditions
Tightening speed and other procedural conditions can influence measured results.
The applicable test method and customer specification should establish the required conditions.
Important Limitation
Results obtained under one test procedure should not automatically be treated as equivalent to results obtained under another.
Why Fastener Testing Must Consider Mating Components
A production bolt may be assembled into a welded nut, threaded insert, self-clinching nut or blind rivet nut.
These threaded components may differ from the standardized mating hardware used in a laboratory test.
For example, a rivet nut can rotate in the panel or deform under load before the bolt reaches the intended tightening condition.
Similarly, a self-clinching nut may be limited by its retention in the sheet rather than by the strength of its internal thread.
Engineering Recommendation
Where the actual mating component is a threaded insert or sheet metal fastener,
validate the complete assembly in addition to any applicable standardized torque–clamp force test.
Automotive OEM Fastener Validation
Automotive manufacturers use torque-controlled fastening in body assemblies, chassis-related components, equipment brackets and other threaded joints.
ISO 16047 testing may help evaluate the tightening characteristics of specified bolts and nuts before production release.
For applications with high safety or durability requirements, additional joint-specific design and validation are necessary.
Important Distinction
ISO 16047 testing does not, by itself, qualify a fastener for a safety-critical automotive application.
EV Battery Pack and Electric Vehicle Assemblies
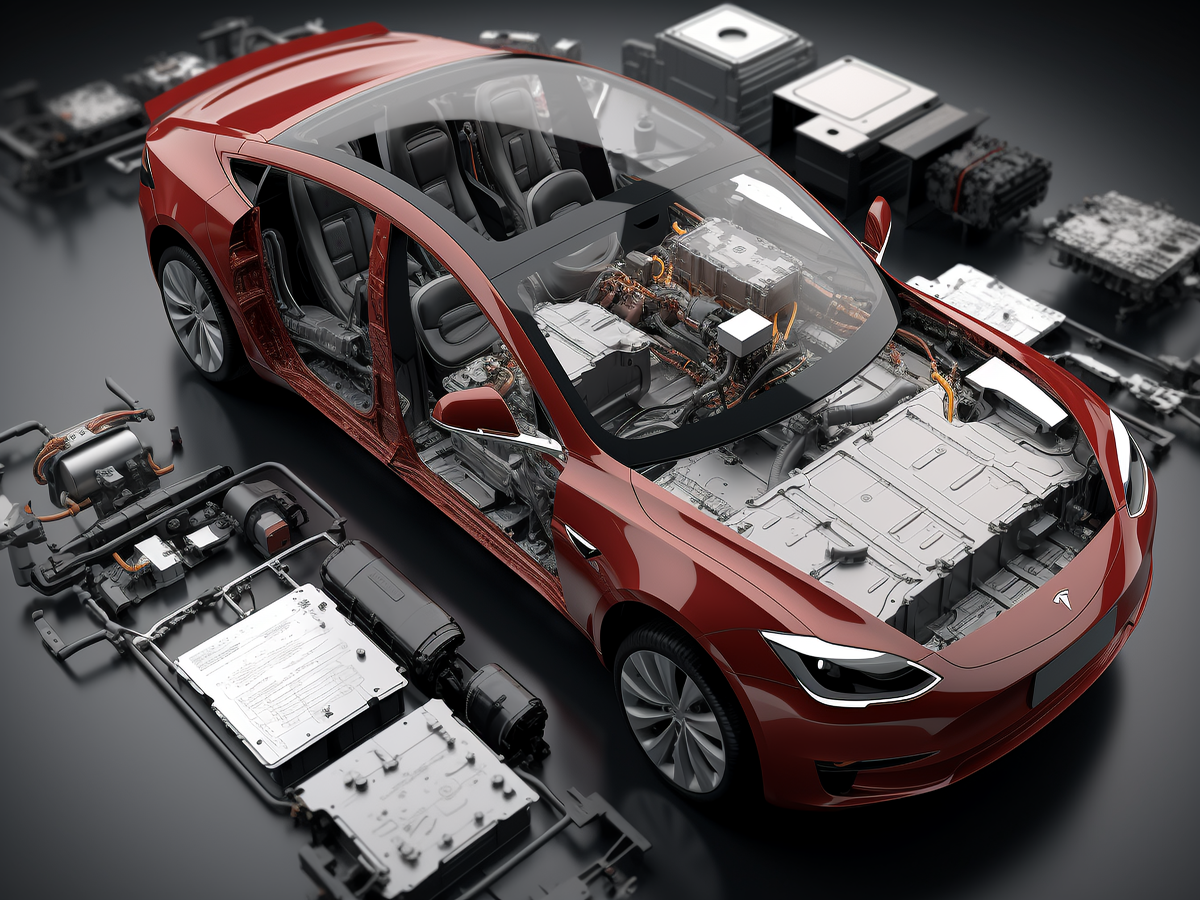
EV battery enclosures, electrical equipment housings and auxiliary mounting structures may require controlled bolt preload.
In a battery cover assembly, for example, insufficient preload may affect gasket compression, while excessive preload may damage thin flanges or threaded attachment points.
Torque–clamp force data can help engineers understand how the specified fastener and surface finish behave during tightening.
However, the complete battery enclosure must also be evaluated for sealing, vibration, thermal expansion and any applicable safety requirements.
Engineering Recommendation
For EV battery assemblies, validate the fastener together with the mating thread, enclosure material and sealing system.
Industrial Machinery and Automated Production
Industrial equipment manufacturers often rely on repeatable tightening operations for motor mounts, machinery frames, brackets and equipment housings.
ISO 16047 testing can support the selection of fasteners with appropriate tightening characteristics.
For production managers, the key question is whether the laboratory results translate into consistent assembly performance on the actual line.
Production Recommendation
Compare laboratory data with representative production tightening trials, including the intended tools, mating components and surface conditions.
Electrical Enclosures and Sheet Metal Fasteners
Electrical cabinets and sheet metal assemblies may use self-clinching nuts, rivet nuts, threaded inserts and other retained fastening components.
For these applications, a bolt's torque–clamp force behavior must be considered alongside the attachment strength of the installed nut or insert.
Additional Validation May Include
Insert pull-out resistance
Insert torque-out or spin-out resistance
Panel deformation
Thread stripping
Joint seating
Repeated service assembly
The required tests depend on the product and application.
Railway, Wind Energy and Structural Equipment
Railway vehicles, wind energy equipment and structural assemblies may contain highly loaded joints with specific design and inspection requirements.
Torque–clamp force testing can provide useful information about tightening behavior,
but it does not replace project-specific structural calculations, fatigue assessment or applicable assembly qualification.
Engineering Recommendation
Where the application uses a qualified bolt assembly or specialized tightening method, follow the governing project requirements before approving a coating or supplier substitution.
ISO 16047 Testing for Production Managers
Production managers need consistent assembly results, predictable cycle times and manageable quality risks.
Torque–clamp force testing can help identify whether fastener friction variation is a potential contributor to inconsistent tightening.
However, laboratory results must be connected to the production process.
A Practical Production Validation Approach
Begin with approved fastener samples and a defined test configuration. Review torque–clamp force results,
then perform representative assembly trials using the actual production components and tightening equipment.
Evaluate whether the tightening process achieves the required joint performance within acceptable variation.
Where appropriate, establish monitoring limits for torque, angle or other measurable process characteristics.
Important Limitation
Torque monitoring alone does not directly measure clamp force in every production joint.
Batch-to-Batch Variation
Fasteners produced or coated in different batches may show variation in tightening behavior.
Potential contributors include:
Coating thickness and distribution
Lubricant application
Surface roughness
Mating-part variation
Handling and storage
Thread condition
Quality Recommendation
Where friction performance is a critical characteristic, define an appropriate sampling and acceptance plan.
How to Review an ISO 16047 Test Report
A useful test report should allow the customer to understand exactly what was tested and under which conditions.
| Report item | Why the customer needs it |
|---|---|
| Fastener identification | Confirms part number, drawing and revision |
| Material and property class | Identifies the tested fastener |
| Thread designation | Confirms the applicable thread geometry |
| Coating and lubricant | Defines the tested surface condition |
| Mating hardware | Identifies the thread and bearing interfaces |
| Test procedure | Establishes the method used |
| Test conditions | Supports comparison and repeatability |
| Measured parameters | Shows what was actually recorded |
| Individual and summary results | Supports assessment of variation |
| Acceptance criteria | Establishes the basis for approval |
| Equipment identification and calibration status | Supports measurement traceability |
| Test date and sample identification | Supports record control |
Important Distinction
A report stating only that a product “passed ISO 16047” is insufficient unless the relevant acceptance criteria and test conditions are defined.
ISO 16047 specifies a testing method; it does not establish a universal pass/fail friction range for every fastener.
Common Problems Revealed During Torque–Clamp Force Evaluation
| Observation | Possible explanation | Recommended action |
|---|---|---|
| Lower clamp force at target torque | Increased friction | Review coating, lubricant and mating surfaces |
| Higher clamp force at target torque | Reduced friction | Review tightening specification and surface treatment |
| Wide result scatter | Variable interfaces or test conditions | Review sample preparation and procedure |
| Unexpected torque increase | Thread interference or galling | Inspect threads and surface condition |
| Irregular test curve | Seating, damage or measurement issue | Investigate the test assembly |
| Supplier results do not match | Different test configurations | Align test conditions before comparison |
These observations are diagnostic clues, not definitive root-cause conclusions.
Supplier Qualification and Alternative Fastener Approval
For procurement specialists, purchasing managers and supplier development teams, a new supplier's bolt should not be approved solely
because it has the same dimensions and mechanical property class as the current product.
Differences in coatings, lubricants or mating-surface interactions may change the clamp force developed at the same torque.
Supplier Review Checklist
Approved drawing and revision
Applicable fastener standard
Material and mechanical property class
Coating specification
Lubrication requirements
ISO 16047 test configuration
Required acceptance criteria
Sample approval
Production consistency requirements
Inspection documentation
Packaging and storage conditions
Change notification requirements
Annual demand, MOQ and delivery schedule
Engineering Recommendation
Where tightening behavior is critical, evaluate the proposed alternative fastener in the actual joint before approving a supplier change.
ISO 16047 and OEM Custom Fasteners
Juxin Fasteners welcomes inquiries for standard and drawing-specific threaded fasteners with defined mechanical, dimensional and surface treatment requirements.
Relevant product categories include:
High-strength bolts and screws
Automotive bolts and nuts
Custom threaded fasteners
Weld nuts and weld studs
Self-clinching fasteners
Blind rivet nuts
Threaded inserts
Industrial fastening components
ISO 16047 testing is particularly relevant to suitable threaded fastener combinations.
For welded, clinched or riveted threaded attachments, additional assembly-specific testing may be needed to evaluate the attachment to the parent material.
The availability of specific testing services, reports, inspection plans or customer documentation must be confirmed during quotation.
Frequently Asked Questions
What does ISO 16047 measure?
It specifies methods for evaluating the relationship between tightening torque and clamp force, together with applicable friction-related characteristics under defined test conditions.
Does ISO 16047 specify one acceptable friction coefficient for all bolts?
No. Acceptance criteria depend on the customer's fastener and assembly requirements.
Can ISO 16047 testing determine the correct tightening torque for my assembly?
It provides useful test data, but the correct tightening specification also depends on the joint design, required preload and production conditions.
Does a successful ISO 16047 test guarantee vibration resistance?
No. Resistance to vibration loosening and fatigue requires additional joint-specific evaluation.
Can zinc-plated and zinc-flake coated bolts have different torque–clamp force results?
Yes. Their coating and lubricant systems may produce different friction behavior.
Can the same bolt produce different results with different nuts or washers?
Yes. The mating threads and bearing surfaces influence the measured relationship.
Is ISO 16047 testing suitable for rivet nuts and self-clinching nuts?
The torque–clamp force behavior of a mating threaded fastener may be evaluated under an appropriate configuration, but the installed insert or clinch attachment also requires its own functional validation.
What should a purchasing manager request from a supplier?
The approved drawing, coating specification, test configuration, measured results, acceptance criteria and relevant inspection documentation.
Can Juxin Fasteners support OEM projects with ISO 16047 testing requirements?
Juxin Fasteners welcomes inquiries involving defined torque–clamp force testing requirements.
The specific test arrangement, documentation and supply scope are subject to confirmation.
Juxin Fasteners: OEM Fastener Supply and Testing Requirements
Juxin Fasteners supplies industrial fastening components for OEM and manufacturing applications.
Our product range includes bolts, screws, nuts, threaded inserts, self-clinching fasteners, rivet nuts and drawing-specific fastening components.
For projects involving torque–clamp force performance, customers can submit their fastener drawings, coating specifications,
test requirements and expected order quantities for technical and commercial review.
Exact product availability, testing scope, documentation, MOQ and delivery schedules are confirmed during quotation.
Request a Quote for OEM Fasteners with Torque–Clamp Force Requirements
Are you sourcing automotive bolts, high-strength industrial fasteners, custom screws and nuts or threaded components with specified ISO 16047 torque–clamp force testing requirements?
Juxin Fasteners welcomes inquiries from design engineers, mechanical engineers, manufacturing engineers, production managers, purchasing managers and supplier development teams.
For technical review and quotation, please provide:
Fastener drawing and revision + thread designation + material and property class + coating and lubricant specification + mating nut and bearing surface details
+ required torque–clamp force test method + friction or preload acceptance criteria + production tightening conditions + inspection documentation
+ sample quantity + annual demand + packaging + target delivery schedule.
Company: Juxin Fasteners
Website: https://www.juxinfasteners.com/
Email: info@juxinfasteners.com
Send your OEM fastener drawings, torque–clamp force requirements and RFQ to Juxin Fasteners for technical review and quotation.
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY



