
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Aug. 16, 2023
Stainless steel extra-long dog point set screws are specialized headless fasteners used where a projecting cylindrical tip must reach and engage a prepared locating feature within a mechanical assembly.
They are particularly relevant to recessed shaft collars, thick gear hubs, couplings, machine fixtures, automation mechanisms and precision positioning equipment.
Unlike flat point set screws that typically apply contact force against a shaft surface, a dog point set screw uses an extended tip to engage a corresponding hole, slot or recess.
This geometric engagement can provide more repeatable positioning and reduce reliance on friction alone.
For deep recessed assemblies, a custom extended dog point can reach a locating feature that a conventional short projection cannot access.
However, increasing the projection length also introduces engineering considerations. Tip bending, hole alignment, unsupported length, thread engagement and installation accessibility must all be evaluated.
A longer dog point is not automatically a stronger fastening solution.
For OEM applications, the correct design depends on the complete mechanical interface: threaded host, extended tip, mating hole, material selection, assembly tolerances and actual service loads.
This guide explains how to select stainless steel extra-long dog point set screws for precision machinery while connecting engineering design, production assembly,
quality control and international procurement requirements.
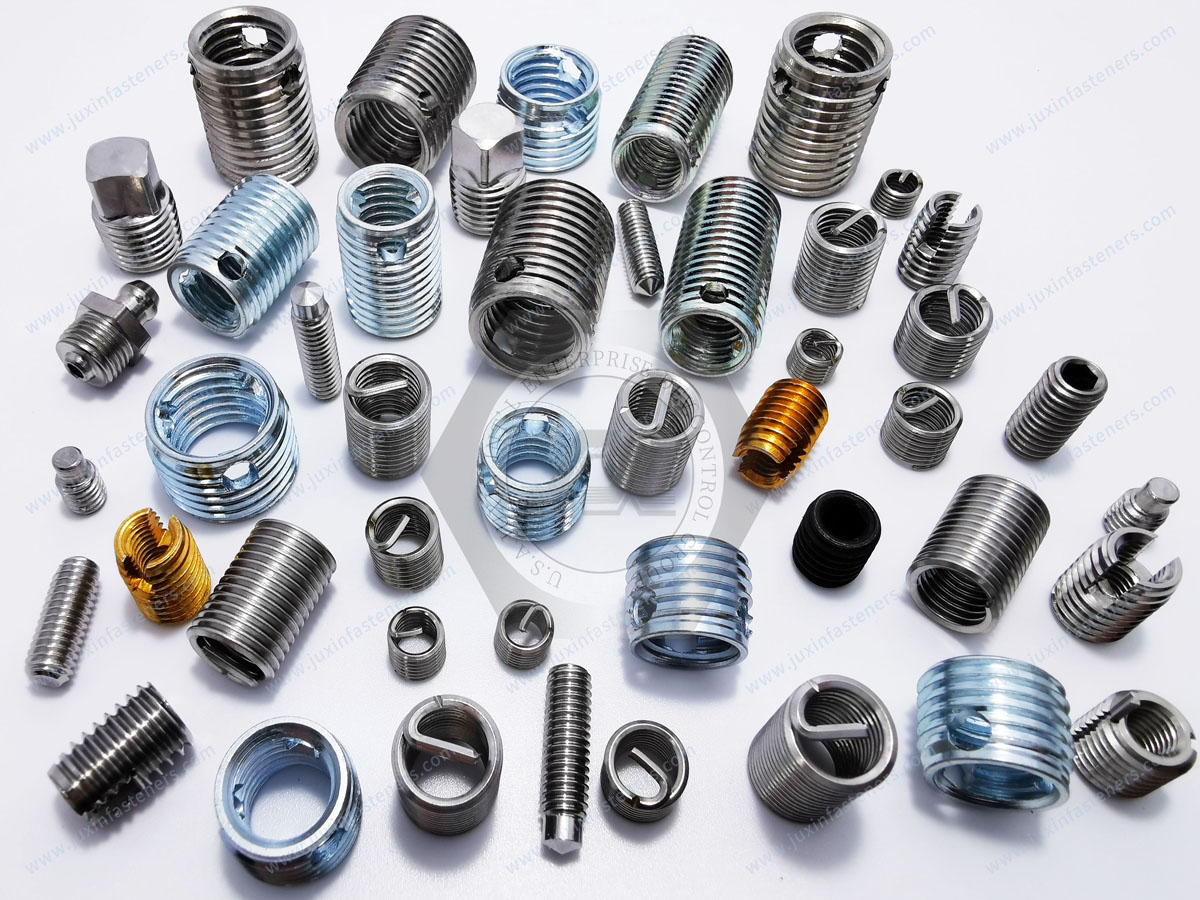
A dog point set screw is a headless threaded fastener with a projecting cylindrical working end.
The projection is normally smaller in diameter than the threaded body and is designed to enter a mating hole, slot or other prepared locating feature.
The threaded portion provides the installation interface, while the dog point establishes the intended geometric engagement.
An extra-long dog point set screw has a projection designed to reach farther than a conventional configuration.
Depending on the drawing, the extension may be intended to engage a deeply recessed hole, pass through a clearance region or position a component within a multi-level assembly.
Typical functions include:
Shaft and hub positioning
Rotational indexing
Axial component location
Repeatable fixture positioning
Engagement with recessed locating holes
Alignment of removable machine components
Positioning in automation mechanisms
Custom OEM mechanical retention
The actual function must be defined by the assembly design.
A dog point should not automatically be treated as a structural dowel pin or a high-capacity torque-transmission component.
The main difference between a standard dog point and a custom extra-long dog point is the projecting working-end geometry.
A conventional dog point provides a cylindrical extension suitable for its intended standard configuration.
A custom extra-long version may require a longer projection, special diameter, modified end geometry or non-standard relationship between the threaded body and the locating tip.
Standard configurations are suitable where the prepared mating feature is accessible within the intended product geometry.
For metric hexagon socket dog point set screws, ISO 4028 and the commonly associated DIN 915 designation are relevant references.
Extra-long versions may be appropriate when the mating hole is recessed beyond the reach of a conventional dog point.
The extended projection must be dimensioned according to the actual assembly.
A non-standard projection should not be described as fully compliant with every dimensional requirement of ISO 4028 or DIN 915 merely because its general tip geometry resembles a standard dog point.
The customer drawing should define the deviations from the standard configuration.
| Configuration | Typical Function | Main Design Consideration |
|---|---|---|
| Standard dog point | Engagement with a prepared locating feature | Standard geometry and mating-hole fit |
| Extra-long dog point | Engagement with a recessed locating feature | Projection length and bending exposure |
| Flat point | Surface contact and adjustable retention | Contact pressure and shaft marking |
| Cup point | Surface gripping and retention | Local indentation and wear |
| Dedicated dowel pin | Precision locating in a designed joint | Fit, load capacity and assembly method |
The selection should begin with the required mechanical function rather than the fastener's appearance.
Dog point, flat point and cup point set screws create different contact conditions.
A dog point is designed to enter a prepared locating feature.
The resulting engagement may resist relative movement through contact between the projecting tip and the walls of the mating feature.
This can provide a more defined locating function than a screw acting only through surface friction.
A flat point presses against a mating surface.
It may be suitable for adjustable shaft retention, particularly where surface marking should be minimized.
However, the actual holding performance depends on contact conditions and the complete assembly.
A cup point uses an annular edge that can grip or indent the mating surface.
It may provide useful retention in applications where localized surface deformation is acceptable.
| Design Requirement | Potential Fastening Approach |
|---|---|
| Repeatable location in a prepared hole | Dog point |
| Engagement with a deeply recessed feature | Custom extra-long dog point |
| Adjustable contact against a shaft flat | Flat point |
| Surface gripping where marking is acceptable | Cup point |
| Precision location with substantial shear loading | Engineered locating pin or alternative connection |
| High torque transmission | Evaluate keyed, splined, clamped or other dedicated connections |
The correct fastener should be selected according to the load path, positioning requirements and service conditions.
Deep recessed assemblies may place the mating locating feature below a surrounding surface or behind another mechanical element.
A conventional dog point may not reach the required location without changing the threaded host geometry.
An extended projection can help solve this problem.
Potential applications include:
Thick shaft collars
Deep gear hubs
Recessed coupling mechanisms
Machine-tool fixtures
Positioning housings
Multi-level mechanical assemblies
Industrial automation mechanisms
Removable locating components
The extension must be long enough to reach the intended feature while avoiding unnecessary unsupported length.
The dog point projection and the threaded body perform different functions.
The threaded body engages the internal thread of the host component.
The dog point enters the locating feature.
These dimensions should be controlled separately.
Increasing the dog point length does not automatically increase thread engagement or thread strength.
Likewise, increasing the overall screw length does not necessarily increase the effective engagement depth of the dog point.
For custom OEM designs, the drawing should identify both dimensions independently.
One of the most important engineering principles is that the dog point and mating hole must be designed together.
The dog point provides the projecting locating geometry.
The mating hole provides the receiving interface.
Neither component can be evaluated independently when accurate positioning is required.
Important characteristics include:
Projection diameter
Projection length
End geometry
Concentricity relative to the threaded body
Surface condition
Material properties
Dimensional tolerances
The mating component should define:
Hole diameter
Hole depth
Hole position
Hole orientation
Entry chamfer or edge condition
Material and hardness
Relevant geometric tolerances
Relationship to the shaft or assembly datum
The dog point must enter the mating hole without unacceptable interference.
Insufficient clearance can cause difficult assembly, edge contact or unintended loading.
Excessive clearance can allow positional movement before the tip contacts the hole wall.
The correct clearance depends on the intended locating accuracy, manufacturing variation, thermal conditions and assembly method.
No universal clearance value should be applied without considering the actual geometry.
The mating hole must provide sufficient space for the required projection.
If the dog point bottoms out before the intended threaded installation condition is reached, the assembly may develop an unintended axial load path.
This can cause misleading installation torque, local damage or incomplete engagement of the intended contact surfaces.
The design should therefore distinguish between locating engagement and end-face bottoming.
Bottoming should occur only when it is an intentional, engineered feature.
A longer dog point can reach a deeper locating feature, but it can also become more sensitive to lateral loading.
The unsupported projection behaves differently from the threaded body.
If side force is applied near the end of a long projection, bending stress can develop.
The magnitude depends on the actual geometry, material and load conditions.
An insufficient projection may fail to reach the mating hole or provide the intended engagement.
An unnecessarily long projection may bottom out, interfere with surrounding components or increase bending exposure.
A tip that is too large may interfere with the mating hole.
A tip that is too small may allow excessive positional movement or create unsuitable contact conditions.
Angular or positional misalignment can cause the tip to contact the hole edge during installation.
This may damage the dog point or mating component.
The engineering objective is not maximum projection length.
It is sufficient engagement with controlled alignment and an appropriate load path.
Extended dog point set screws require particular attention to side loading.
When the screw axis is not properly aligned with the mating hole, the projecting tip may experience lateral contact during installation or operation.
Potential causes include:
Incorrect hole position
Angular misalignment
Assembly tolerance stack-up
Shaft deflection
Component deformation
Incorrect installation sequence
Excessive clearance
Unexpected service loads
An extended tip may be exposed to a bending moment when lateral force acts away from its supported section.
The resulting stress depends on projection geometry and the actual contact location.
A longer projection is not automatically suitable for greater shear loading.
A sharp or poorly controlled hole edge can create localized contact and wear.
The entry geometry should be compatible with the intended installation method.
Several individually acceptable dimensions can combine to create poor alignment in the finished assembly.
For example, variation in the threaded hole position, shaft location and mating-hole position may cause the dog point to approach the hole off-center.
For precision OEM equipment, the complete tolerance chain should be reviewed.
A dog point can provide geometric positioning without automatically becoming a structural locating pin.
This distinction is particularly important in rotating machinery.
Consider a hub mounted on a shaft.
A dog point engaging a radial hole may help define the relative position of the hub and shaft.
However, if the assembly transmits substantial torque, the tip and hole may experience significant contact loading.
The actual load capacity depends on:
Dog point diameter
Engagement depth
Hole diameter
Shaft and hub materials
Edge distance
Contact geometry
Applied torque
Cyclic loading
Local deformation
Fatigue considerations
A larger or longer dog point does not automatically make the connection stronger.
For demanding torque-transfer applications, a key, spline, clamp or dedicated locating system may be more appropriate.
The load path should determine the fastening architecture.
Dog point set screws and dowel pins can both engage locating holes, but they serve different purposes.
A dog point set screw combines a threaded installation mechanism with a projecting locating feature.
A dowel pin is a dedicated locating component designed for a specific fit and mechanical function.
| Feature | Dog Point Set Screw | Dowel Pin |
|---|---|---|
| Installation | Threaded | Fit into prepared holes |
| Adjustment | Can support threaded adjustment | Depends on locating design |
| Locating feature | Projecting dog point | Pin body |
| Main design priority | Positioning and retention | Controlled location |
| Shear performance | Must be evaluated for the specific geometry | Must be evaluated for the specified pin and joint |
| Removal | Through threaded operation | Depends on fit and accessibility |
A dog point should not be substituted for a dowel pin solely because both have cylindrical geometry.
Where significant shear transfer or high-precision permanent location is required, a dedicated locating system may be preferable.
ISO 4028 is an important international reference for metric hexagon socket dog point set screws.
DIN 915 is a commonly recognized German designation associated with the corresponding product type.
These references are useful for standard configurations within their applicable scope.
An extra-long dog point may fall outside the dimensional requirements of a standard product.
In that case, the customer drawing should identify the required thread, overall length, projection geometry and other controlled characteristics.
A standard designation may be used as a reference where appropriate, but it should not replace the custom drawing.
For applicable inch-series socket set screws, ASME B18.3 may be relevant.
The exact thread, point configuration and dimensional requirements must be confirmed.
Metric threads, UNC threads, UNF threads and British Whitworth thread systems are not directly interchangeable.
For example, a metric set screw cannot be substituted for an inch-series screw simply because the nominal diameters appear similar.
The RFQ should identify the thread system, size, pitch or threads per inch, tolerance and applicable specification.
Stainless steel is often selected where corrosion resistance, material compatibility or environmental exposure is important.
However, the correct grade depends on the application.
A2 is a common austenitic stainless fastener material designation.
It may be suitable for selected industrial machinery, automation systems and general corrosion-resistant applications.
Its suitability should be evaluated against the actual environment and mechanical requirements.
A4 stainless steel contains molybdenum in the applicable material family and may offer improved resistance in certain corrosive environments.
It may be considered for selected outdoor, chemical-exposure or marine-adjacent equipment.
However, A4 stainless steel is not universally resistant to all corrosive conditions.
For special drawing-based components, customers may specify materials such as AISI 303 or AISI 316.
These material designations should be evaluated according to the manufacturing method and required mechanical properties.
A machined custom fastener should not automatically be assigned a standard fastener property designation without confirming the applicable requirements.
| Application | Potential Material Approach | Main Consideration |
|---|---|---|
| General industrial machinery | Suitable A2 stainless fastener | Mechanical and environmental requirements |
| Selected corrosive environments | A4 stainless fastener | Chemical and chloride exposure |
| Precision custom components | Drawing-specified stainless material | Machining and dimensional requirements |
| Aluminum housings | Compatible stainless fastener | Host thread strength and galvanic corrosion |
| Repeated maintenance assemblies | Application-compatible material pairing | Wear and galling |
Stainless steel set screws are sometimes installed into aluminum housings, collars or hubs.
This material combination requires attention to several factors.
Aluminum internal threads may have different strength and wear characteristics from steel threads.
The required engagement length and installation conditions should be evaluated accordingly.
When dissimilar metals are electrically connected in the presence of a suitable electrolyte, galvanic corrosion may occur.
The risk depends on the environment, material combination, exposed surface areas and protective measures.
Repeated installation and removal may contribute to wear of the softer threaded host.
For serviceable assemblies, the maintenance frequency should be considered during design.
The dog point may engage a steel shaft while the threaded body is installed in an aluminum hub.
These two interfaces have different mechanical functions.
The design must consider both.
Stainless steel threaded components can experience galling under certain installation conditions.
Galling is adhesive wear that can occur when contacting metallic surfaces slide under pressure.
Potential contributing factors include:
High contact pressure
Excessive tightening speed
Contaminated threads
Repeated installation
Similar stainless steel mating materials
Unsuitable lubrication conditions
Damaged thread surfaces
Depending on the application, engineers may evaluate controlled tightening, suitable lubrication, compatible material pairing and appropriate installation procedures.
Lubricants and anti-seize compounds can change the torque-to-contact-force relationship.
Their use should therefore be consistent with the customer's installation specification.
Stainless steel fasteners may require passivation or other surface-treatment specifications depending on the application.
ASTM A967 is a recognized specification for chemical passivation treatments for stainless steel parts.
Where passivation is required, the applicable process and acceptance criteria should be identified in the purchasing specification.
Passivation is not a universal corrosion-proofing treatment.
Its effectiveness depends on the material, surface condition, processing history and service environment.
The threaded body must provide adequate engagement with the host component.
Required engagement depends on:
Thread size and pitch
Host material
Thread depth
Installation torque
Applied loads
Repeated removal
Material strength
Assembly geometry
An extra-long dog point does not compensate for insufficient thread engagement.
For aluminum or other relatively soft host materials, internal thread capacity may require particular attention.
The set screw and threaded host should be evaluated as a complete system.
Extra-long dog point set screws are often used in assemblies where installation access is limited.
A fastener may be dimensionally correct but difficult to install if the tool cannot reach or engage the socket.
Important variables include:
Hex socket size
Socket depth
Driver length
Tool access angle
Clearance around the fastener
Installation torque
Tool condition
Maintenance access
The tool should engage the socket sufficiently to transmit the required installation torque.
Poor engagement can damage the drive feature.
For production equipment, the fastener should be compatible with the intended feeding, positioning and tightening process.
Production engineers should consider driver alignment, access, installation repeatability and inspection.
If the screw must be removed during maintenance, the design should preserve suitable tool access after the complete machine is assembled.
A serviceable fastener should remain accessible throughout its intended maintenance life.
Industrial automation systems often require repeatable mechanical positioning.
Extended dog point set screws may be considered where a prepared locating feature is recessed inside the assembly.
Potential applications include:
Robotic positioning mechanisms
Adjustable fixtures
Machine-tool locating components
Conveyor assemblies
Automated changeover systems
Actuator components
Sensor positioning mechanisms
Compact mechanical indexing devices
A dog point engaging a controlled hole can provide a defined locating interface.
However, the actual repeatability depends on clearance, wear, component stiffness and manufacturing tolerances.
Machine fixtures may require repeated removal and installation.
In these applications, the dog point and mating hole should be evaluated for wear and service life.
The screw's socket and geometry should be compatible with the production tooling.
The design should avoid unnecessary complexity that increases assembly time or rework.
Gear hubs, pulleys, shaft collars and couplings may require mechanical positioning relative to a shaft.
An extended dog point can be useful when the locating feature is recessed.
Potential applications include:
Gear hubs
Timing pulleys
Shaft collars
Couplings
Conveyor rollers
Rotary mechanisms
Drive assemblies
However, the dog point should not automatically be selected as the primary torque-transfer element.
For high torque, reversing loads or critical rotating equipment, the complete connection should be evaluated.
A dedicated key, spline, clamp or other connection may be required.
Machine fixtures frequently require repeatable location of removable components.
Extended dog point set screws may support positioning where the locating feature is not directly accessible.
Potential applications include:
Fixture plates
Adjustable stops
Tooling mechanisms
Changeover fixtures
Locating assemblies
Machine setup components
The design should consider wear of the dog point and mating hole during repeated operation.
Precision instruments may require compact locating components.
Potential applications include optical alignment mechanisms, sensor assemblies, measurement equipment and laboratory instruments.
For miniature configurations, tip diameter, hole diameter, thread size and socket accessibility become particularly important.
Customer drawings should identify critical dimensions for non-standard designs.
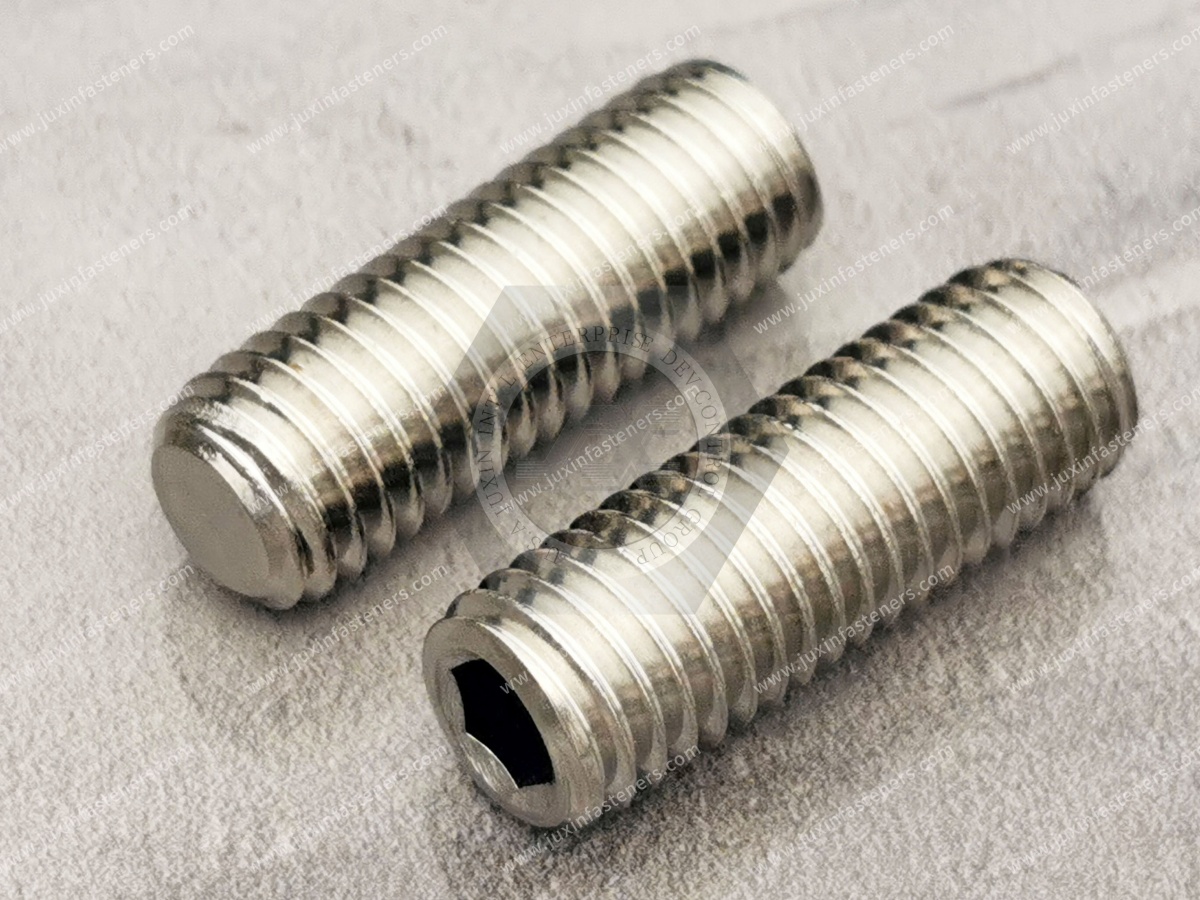
Extended dog point set screws may be used in selected automotive and transportation equipment for positioning, fixtures and non-structural mechanical functions.
Potential requirements include vibration resistance, corrosion compatibility, repeatable location, compact installation and serviceability.
The fastener should be evaluated according to its actual function.
A positioning set screw should not automatically be classified as suitable for safety-critical structural retention.
| Observed Problem | Potential Cause | Engineering Review |
|---|---|---|
| Dog point does not enter hole | Misalignment or incorrect dimensions | Hole position and tip diameter |
| Excessive assembly force | Interference or edge contact | Clearance and entry geometry |
| Tip bending | Lateral load on projection | Unsupported length and load path |
| Tip bottoming | Insufficient hole depth | Projection and hole dimensions |
| Positional movement | Excessive clearance or wear | Locating interface |
| Thread stripping | Insufficient host thread capacity | Material and engagement |
| Socket damage | Poor tool engagement | Socket geometry and installation |
| Galling | Adhesive thread wear | Material pairing and tightening |
| Corrosion | Unsuitable material interface | Environment and protection |
| Vibration-related loosening | Inadequate retention strategy | Complete assembly validation |
Failure analysis should consider the fastener, mating hole, threaded host and installation process together.
Replacing the screw with a longer or stronger version may not resolve a problem caused by incorrect hole geometry or misalignment.
OEM fastener selection should consider the complete production process rather than only the component price.
Manufacturing engineers and production managers should evaluate installation accessibility, assembly repeatability, tool compatibility, inspection and rework.
A well-designed dog point and mating hole should allow predictable engagement within the intended assembly tolerances.
The socket must be accessible to the selected installation equipment.
Poor tool access can increase cycle time and damage risk.
If the locating feature is damaged during installation, rework may require replacement or machining of the mating component.
The cost of a damaged hub or precision shaft can be significantly more important than the cost of the set screw.
Total installed cost may include:
Fastener purchase price
Tooling and installation labor
Assembly cycle time
Inspection
Rework
Scrap
Replacement mating components
Packaging and logistics
The preferred solution should balance mechanical performance with production efficiency.
Standard dog point set screws can satisfy many applications.
However, deep recessed assemblies may require special dimensions.
Custom requirements may include:
Extra-long dog point projection
Special tip diameter
Non-standard overall length
Custom metric or inch thread
Special socket configuration
Stainless steel material selection
Drawing-controlled tolerances
Special surface treatment
Customer-specific inspection requirements
Production packaging specifications
JUXIN FASTENERS can evaluate custom drawing-based fastener requirements according to the customer's specifications, material, quantity and application.
Manufacturing feasibility, tooling requirements and delivery conditions should be confirmed during quotation.
For extended dog point applications, the tip geometry is often a critical functional characteristic.
Depending on the drawing, inspection may include:
Thread diameter and pitch
Overall length
Dog point diameter
Dog point length
End geometry
Concentricity or runout where specified
Socket dimensions
Surface condition
Material identification
Specified finish or treatment
Tip diameter and projection length directly influence engagement with the mating hole.
These dimensions should be controlled according to the approved drawing.
Thread conformity should be verified using appropriate gauges or measurement methods.
Where material traceability is required, the purchasing specification should identify the necessary records.
Customer-specific dimensional reports or other quality documents should be agreed during supplier qualification.
Procurement and supplier-development teams should evaluate whether the supplier can understand and maintain the required configuration.
Relevant factors include drawing interpretation, standard knowledge, thread manufacturing, tip geometry control and material selection.
Relevant factors include dimensional inspection, thread verification, material control, lot identification and documentation.
Relevant factors include quotation accuracy, packaging, production planning, repeat-order support and delivery requirements.
For custom extra-long dog point set screws, maintaining the correct drawing revision is particularly important.
A product with the correct thread and overall length may still be unsuitable if the projection geometry differs.
| Selection Factor | Engineering Priority | Production Priority | Procurement Priority |
|---|---|---|---|
| Dog point diameter | Mating-hole fit | Repeatable engagement | Drawing conformity |
| Dog point length | Correct locating reach | Avoid bottoming | Critical dimension control |
| Hole geometry | Alignment and location | Assembly consistency | Drawing coordination |
| Thread | Host engagement | Installation repeatability | Correct standard |
| Material | Mechanical and corrosion compatibility | Galling and handling | Material specification |
| Socket | Tool engagement | Cycle time and access | Dimensional consistency |
| Surface treatment | Environmental suitability | Assembly compatibility | Specification control |
| Documentation | Functional verification | Quality assurance | Supplier qualification |
A complete RFQ should provide the technical and commercial information necessary to evaluate the actual application.
| RFQ Category | Information to Provide |
|---|---|
| Product | Extra-long dog point or extended-tip set screw |
| Standard | ISO 4028, DIN 915, ASME B18.3 or custom drawing |
| Thread | Metric, UNC, UNF or specified system |
| Overall dimensions | Thread diameter, pitch and overall length |
| Dog point | Projection length, diameter and end geometry |
| Socket | Drive type, size and depth |
| Material | Stainless steel grade and applicable requirements |
| Mating hole | Diameter, depth, position and tolerances |
| Host material | Hub, collar or housing material |
| Mating component | Shaft or locating component material |
| Application | Positioning, indexing or retention |
| Loads | Torque, axial force, vibration or other relevant loading |
| Environment | Temperature, moisture and chemical exposure |
| Quality | Critical inspection and documentation requirements |
| Quantity | Sample quantity, initial order and annual forecast |
| Packaging | Production and logistics requirements |
| Delivery | Destination and requested schedule |
Providing the mating-hole dimensions is especially important for non-standard dog point configurations.
It is a headless threaded fastener with an extended projecting tip designed to engage a prepared locating feature, often in a recessed assembly.
A dog point enters a locating hole or recess, while a flat point normally contacts a mating surface.
Yes. They are relevant references for metric hexagon socket dog point set screws. Custom extra-long projections may require additional drawing specifications.
Not automatically. Load capacity depends on the tip, mating hole, materials, engagement geometry and actual service loads.
Not without engineering evaluation. Their installation methods and load-bearing functions may differ substantially.
They may be used in suitable designs, but host thread strength, galvanic corrosion and repeated maintenance should be considered.
Thread dimensions, overall length, tip diameter, projection length, socket geometry and mating-hole requirements are commonly important.
Yes, for suitable positioning and retention functions. The complete assembly must be evaluated for torque, vibration and other loads.
Provide the drawing, material specification, mating-hole dimensions, required quantity, application and inspection requirements.
Stainless steel extra-long dog point set screws provide a specialized solution for recessed positioning and locating applications in industrial machinery,
automation equipment, fixtures and precision mechanical assemblies.
Their main advantage is the ability to engage a prepared locating feature beyond the reach of a conventional short projection.
However, successful application requires more than selecting a longer screw.
The dog point diameter, projection length, mating-hole geometry, alignment, thread engagement, material compatibility and installation process must be engineered together.
A longer projection does not automatically increase holding strength, and a dog point should not be treated as a universal replacement for a structural locating pin.
For design engineers, the priority is correct geometric engagement and a suitable load path.
For manufacturing engineers and production managers, the priority is repeatable installation, controlled alignment, accessible tooling and reduced rework.
For procurement and supply chain teams, the priority is an accurate drawing, critical dimension control, appropriate quality documentation and reliable repeat sourcing.
The best OEM fastening solution begins with the mechanical function and continues through drawing control, manufacturing evaluation, inspection and production supply.
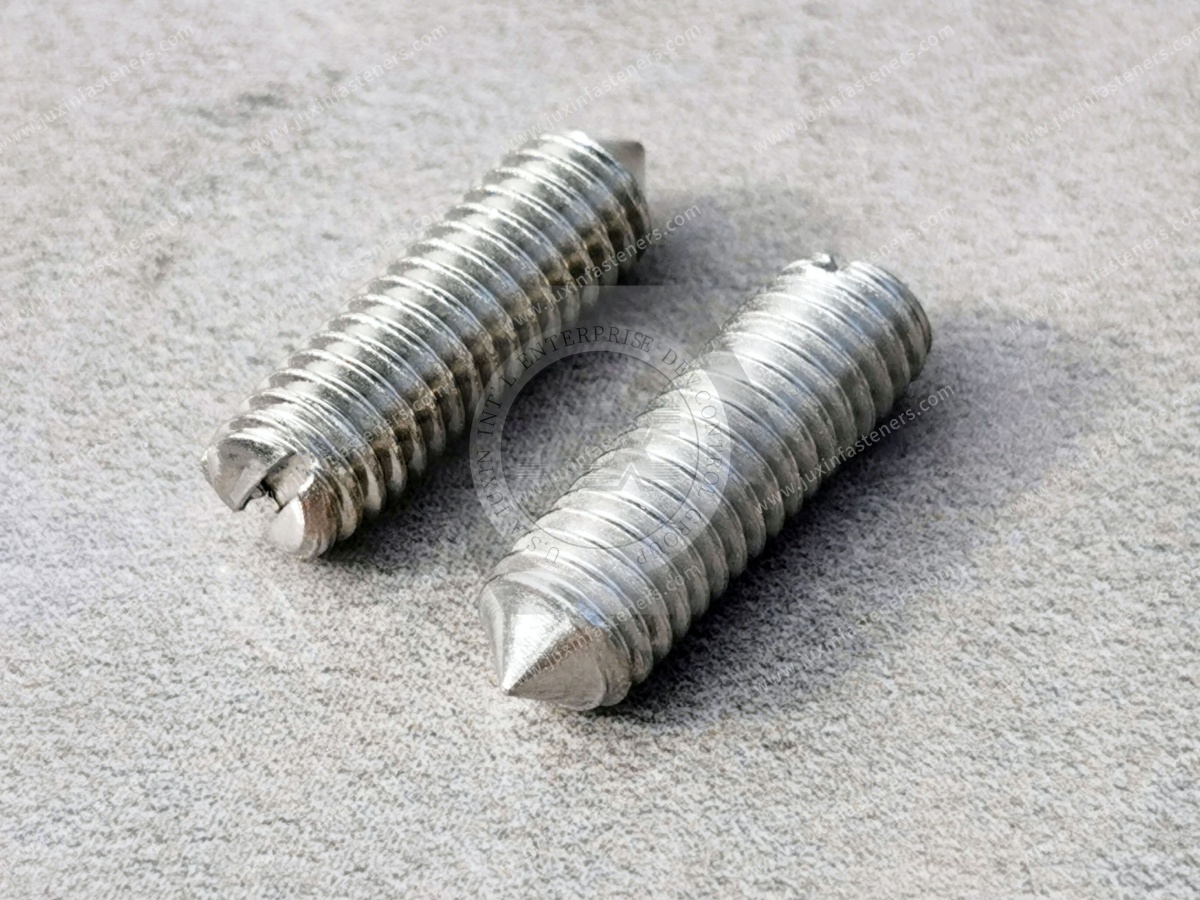
JUXIN FASTENERS supports international OEM and industrial customers requiring stainless steel set screws, precision fastening components and custom drawing-based mechanical hardware.
Relevant requirements may include:
Stainless steel dog point set screws
ISO 4028 and DIN 915 configurations
Custom extra-long dog point screws
Extended-tip set screws for recessed assemblies
Metric and inch-thread set screws
Precision miniature locating screws
Special stainless steel fasteners
Drawing-based OEM components
Please send your drawing or specification together with the required material, thread, overall length, dog point dimensions and quantity.
For application-specific designs, include the mating-hole dimensions, host material, installation method and operating conditions wherever available.
This information provides a stronger basis for technical evaluation, sample planning and commercial quotation.
Company: JUXIN FASTENERS
Website: https://www.juxinfasteners.com/
Email: info@juxinfasteners.com
Contact JUXIN FASTENERS for custom stainless steel extra-long dog point set screws, precision locating fasteners, drawing evaluation and OEM bulk RFQ inquiries.
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY



