
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Oct. 21, 2023
Starlock-style washers and star-type push-on retainers are compact retaining fasteners used to provide axial retention on compatible shafts, pins and studs without requiring a conventional threaded nut.
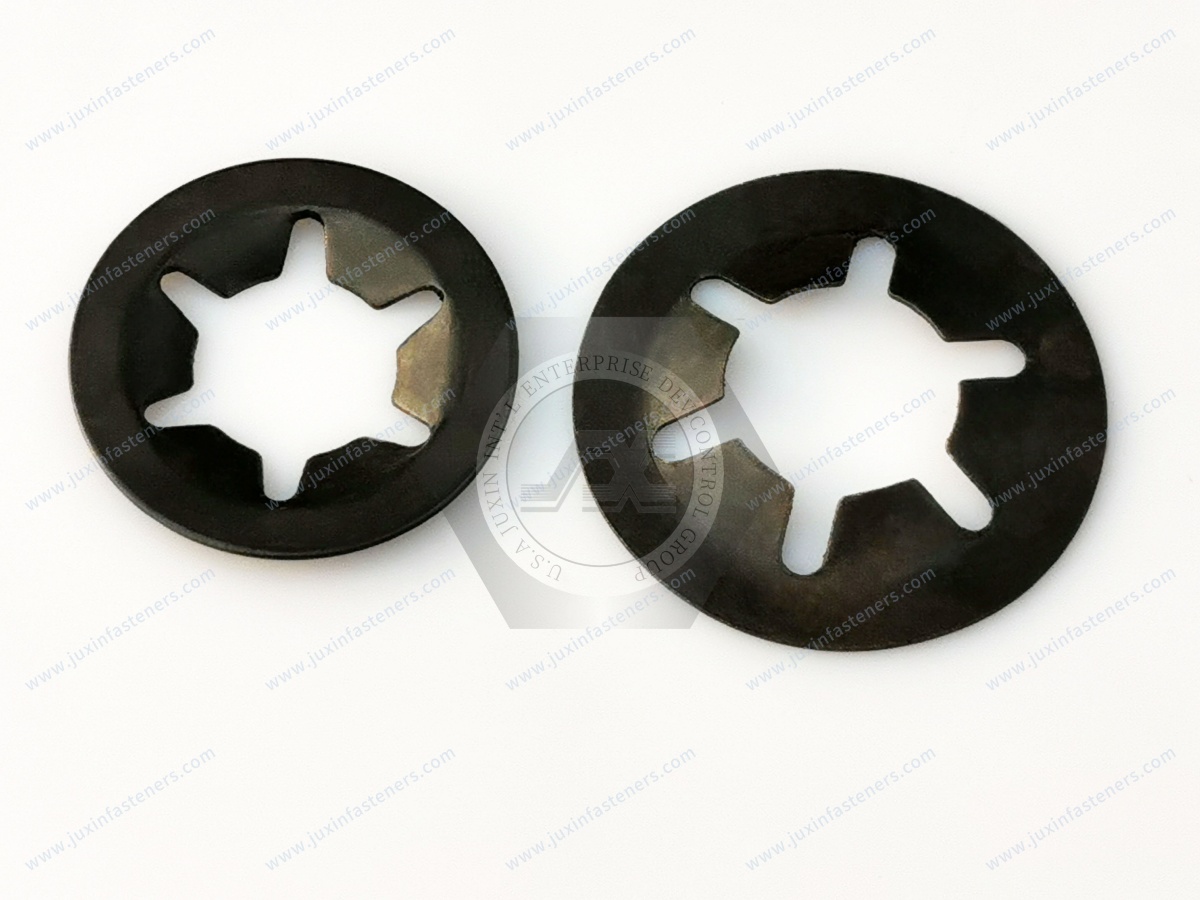
Their characteristic feature is an internal pattern of resilient teeth or fingers arranged around the center opening.
During installation, these gripping features deflect as the retainer is pushed onto the mating shaft. After installation, the tooth geometry resists movement in the reverse axial direction.
Depending on supplier terminology and product geometry, related components may be described as:
Starlock washers;
Starlock retaining washers;
star-type retaining washers;
push-on retaining washers;
push-on shaft retainers;
toothed shaft retainers;
push-on retainers;
press-on retaining fasteners.
The older expression "plum blossom retaining ring" may appear in translated product descriptions because of the visual shape of the internal teeth,
but it is not the preferred technical search term for international OEM sourcing.
For engineering purposes, the important question is not what the component looks like.
The important question is:
How does the retainer interact with the mating shaft, and can that interface provide the required axial retention for the application?
JUXIN FASTENERS supplies standard and custom retaining fasteners, stamped components, washers and application-specific fasteners for industrial and OEM programs.
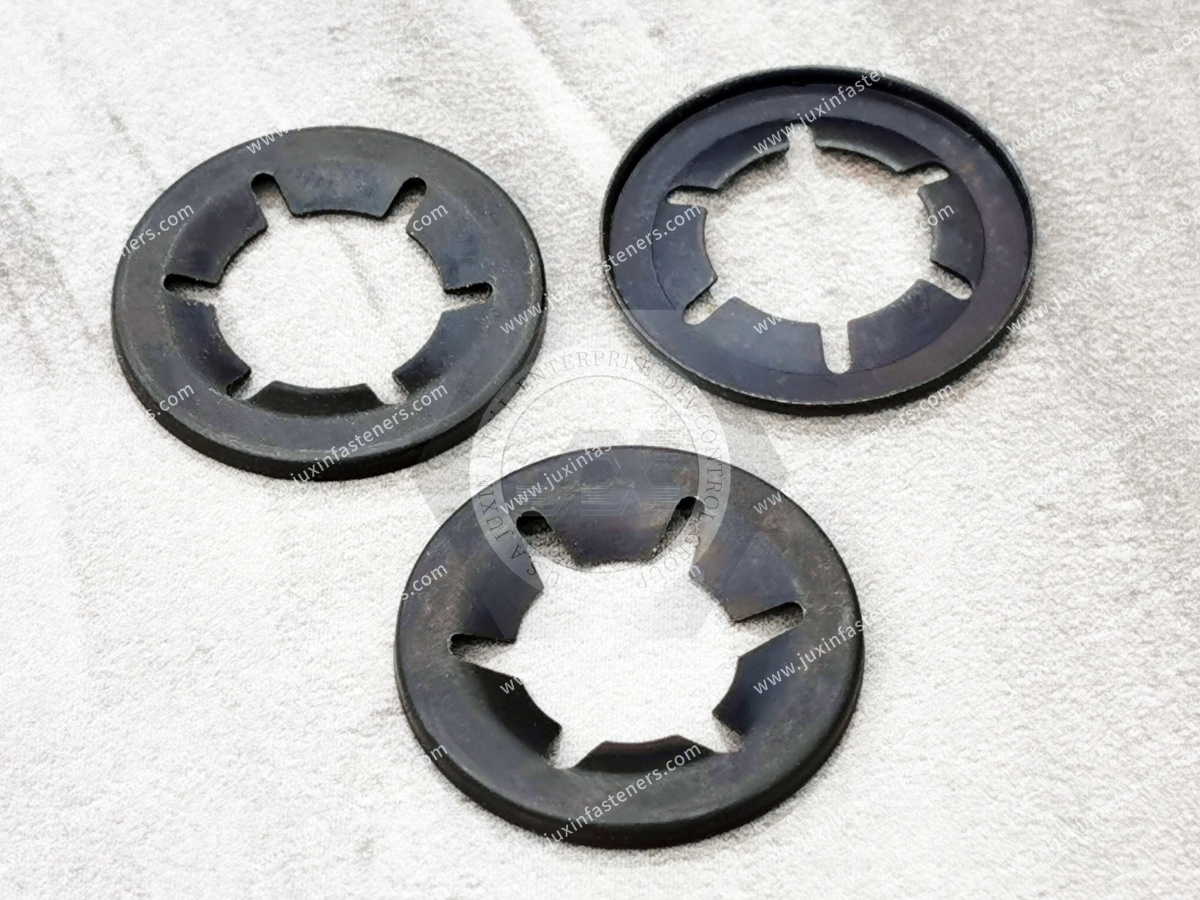
A Starlock-style retaining washer is a push-on fastener with inward-facing elastic gripping features.
It is installed axially onto a compatible shaft, pin or stud.
Unlike a conventional threaded nut, it normally does not depend on mating threads.
Unlike many conventional circlips or retaining rings, some push-on retaining washer designs do not require a machined retaining groove.
This can make them attractive for compact and high-volume assemblies where simplified shaft geometry and fast installation are important.
The basic mechanism involves controlled deformation of the internal teeth.
During installation:
the retaining washer is aligned with the shaft;
axial force pushes it over the shaft diameter;
the internal teeth deflect;
the washer reaches its intended installed position;
the tooth geometry resists reverse axial movement.
The resulting retention is created by the interaction between the retainer and the mating shaft.
Therefore, the retainer should not be specified independently from the shaft.
A common sourcing mistake is to specify only:
"8 mm Starlock washer"
or:
"10 mm star retaining ring."
Nominal shaft diameter is important, but it is not the complete specification.
Actual performance can also depend on:
shaft diameter tolerance;
retainer opening geometry;
tooth geometry;
retainer material;
material thickness;
shaft material;
shaft hardness;
shaft surface finish;
coating;
installation position;
required axial retention.
For OEM applications, these parameters should be considered together.
The internal gripping teeth are the primary functional feature of a star-type push-on retainer.
Important design variables can include:
number of teeth;
tooth length;
tooth width;
tooth angle;
tooth thickness;
tooth root geometry;
central opening diameter;
formed tooth profile.
Changing one of these variables can affect installation and retention behavior.
This is why two visually similar retaining washers should not automatically be considered interchangeable.
During installation, each tooth must deform enough to pass over the shaft.
After installation, the teeth must retain appropriate engagement with the mating surface.
If the design is too compliant, retention may be insufficient.
If the interference is excessive, potential consequences can include:
excessive installation force;
permanent retainer deformation;
shaft marking;
coating damage;
assembly difficulty.
The correct geometry is therefore a balance rather than simply "more gripping force."
Push-on retaining washers rely on an interference relationship.
That means shaft dimensional variation can directly affect assembly behavior.
A shaft toward the larger end of its permitted tolerance may increase installation force.
A shaft toward the smaller end may reduce engagement.
For production programs, testing only one nominal shaft may not represent the complete manufacturing condition.
Where retention is function-critical, engineers should consider the expected dimensional range of both mating components.
The shaft is part of the retaining mechanism.
A hardened steel shaft, stainless steel pin, aluminum shaft and molded polymer post can interact differently with the same tooth geometry.
Material and hardness can influence:
tooth penetration or indentation;
installation force;
removal resistance;
shaft marking;
wear;
repeated assembly behavior.
The mating component therefore belongs in the fastener-selection process.
Surface finish and coating can also influence the interface.
Examples include:
uncoated steel;
plated steel;
stainless steel;
anodized aluminum;
painted or coated components;
molded polymer shafts.
If the shaft coating performs an important corrosion or cosmetic function, the possibility of local tooth contact or coating disturbance should be considered.
This distinction is particularly important for push-on retaining fasteners.
Installation force describes the force required to press the retainer into position.
Axial retention or removal resistance describes its ability to resist movement after installation under defined conditions.
Increasing interference can increase installation force, but it should not simply be assumed that maximizing interference creates the optimum assembly.
A useful design must satisfy both manufacturing and service requirements.
Retention performance cannot responsibly be assigned solely from nominal shaft diameter.
It depends on the complete interface, including:
retainer geometry;
material;
thickness;
shaft diameter;
shaft tolerance;
shaft hardness;
surface condition;
installation depth;
load direction.
For application-specific OEM assemblies, representative testing provides more useful information than a generalized holding-force claim.
Commercial terminology can create confusion.
Both products provide axial retention, but the installation interface can be very different.
A conventional external retaining ring typically engages a groove machined into a shaft.
A star-type push-on retaining washer can use internal teeth to grip a compatible shaft directly.
Therefore, when specifying the component, it is useful to distinguish between:
groove-based retention
and
push-on interference-based retention.
A circlip is normally installed into a defined groove.
Its installed axial location is largely established by that groove.
A push-on retaining washer may avoid groove machining, but its performance depends more directly on the shaft-to-retainer interference relationship.
The choice affects:
shaft manufacturing;
installation;
removal;
serviceability;
component cost;
axial positioning.
An E-clip also normally engages a groove.
It can often be installed radially from the side.
A Starlock-style push-on washer is generally installed axially over the shaft.
This makes installation access an important selection factor.
If axial access is restricted but radial access is available, an E-clip architecture may be more appropriate.
These product families overlap.
"Push-on nut" is a broad commercial description for retaining fasteners pressed onto shafts or studs.
A star-type retaining washer is a more specific geometry within the broader push-on retaining-fastener family.
In a website architecture, this distinction is useful:
Push-On Nuts & Shaft Retainers → Product Family
Star-Type / Starlock-Style Retaining Washers → Specific Product Geometry
This prevents multiple pages from competing for exactly the same search intent.
A threaded nut requires mating threads.
A push-on retaining washer can eliminate that threaded interface in suitable applications.
Potential manufacturing advantages include:
simplified shaft geometry;
reduced component count;
faster assembly;
compact axial packaging.
However, a push-on retainer is not a universal replacement for a threaded nut.
If the joint requires controlled preload, high structural clamping force or repeated disassembly, a threaded fastening system may be more appropriate.
Many push-on star-type retaining washer designs are intended to grip a compatible shaft without the conventional retaining groove used by circlips or E-clips.
This can eliminate a machining or forming operation on the mating shaft.
Whether that produces a meaningful cost advantage depends on:
shaft manufacturing method;
production volume;
assembly method;
required retention;
service requirements.
Suitable spring steels can provide the elastic behavior required for the internal gripping features.
Material selection should consider:
formability;
elastic properties;
required mechanical behavior;
heat treatment where applicable;
corrosion protection;
operating environment.
Surface treatments can be specified according to application requirements.
Stainless steel may be selected where corrosion resistance is important.
Potential uses can include appropriate:
outdoor equipment;
appliances;
HVAC equipment;
electrical equipment;
industrial machinery.
However, stainless steel should not automatically be described as superior for every application.
The selected grade, mechanical properties, forming behavior and mating shaft should all be considered.
The previous version of this article associated stainless steel directly with food and pharmaceutical compliance.
That is too broad.
A stainless steel retaining component may be suitable for some equipment in these industries, but material selection alone does not establish:
food-contact compliance;
hygienic design;
pharmaceutical compliance;
cleanability;
contamination control.
Those requirements depend on the complete equipment design and applicable specifications.
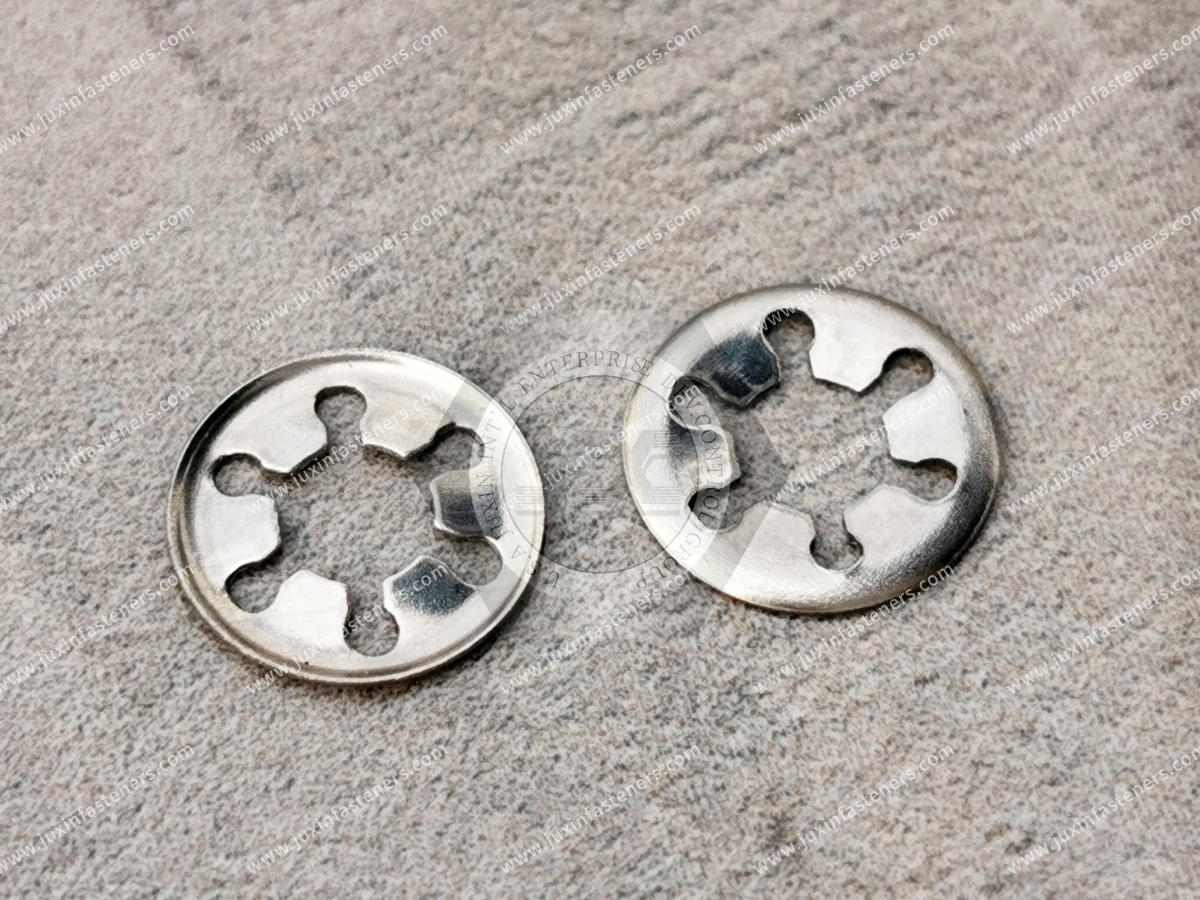
For non-stainless retainers, an appropriate surface treatment may be used where corrosion protection is required.
Selection should consider:
indoor or outdoor service;
humidity;
condensation;
chemicals;
temperature;
mating material;
required service life.
The retainer should be considered together with the shaft and surrounding assembly.
Reuse should not automatically be assumed.
The internal teeth are deliberately deformed during installation.
Removal can further alter:
tooth angle;
tooth shape;
elastic behavior;
central opening geometry.
The mating shaft may also be marked.
If the product requires repeated servicing, another retaining method may provide a more predictable solution.
A push-on retainer is easy to install in many applications, but removal can be a different engineering problem.
Depending on the design, removal may:
require a dedicated tool;
deform the retainer;
damage the fastener;
mark the shaft;
make reuse inappropriate.
Design engineers should therefore consider the complete product lifecycle, not just initial assembly speed.
Push-on retainers require axial access to the shaft during installation.
The installer or automated tool must be able to approach the shaft end and apply controlled axial force.
This seemingly simple requirement can determine whether a push-on retainer is practical in the final assembly sequence.
Installation tooling should apply force to an appropriate region of the retaining washer.
Poorly designed tooling can:
bend the outer body;
distort the internal teeth;
install the washer at an angle;
damage the shaft;
create inconsistent installation depth.
For high-volume OEM production, the fastener and installation tool should be considered together.
A retaining washer may need to seat against:
the retained component;
a shaft shoulder;
a spacer;
another defined assembly feature.
The installed position should be controlled by the product architecture.
Continuing to apply excessive installation force after seating can damage the retainer or mating component.
Star-type push-on retainers can be used in suitable automotive assemblies requiring economical axial retention.
Potential application areas can include certain:
trim assemblies;
shields;
brackets;
pins;
linkage components;
other non-threaded retaining interfaces.
The exact application must follow the approved drawing and validation requirements.
Safety-critical assemblies require application-specific engineering review.
Household and commercial appliances often contain compact shafts, pins and mechanisms produced in high volumes.
Push-on retaining washers can be considered for suitable:
fan assemblies;
rollers;
actuating mechanisms;
brackets;
appliance subassemblies.
Fast installation can be particularly valuable where assembly-cycle efficiency matters.
Certain motors and electromechanical assemblies may use compact retaining components for suitable shafts and internal mechanisms.
However, designers should distinguish between:
general axial retention
and
precision bearing location or preload control.
A general push-on washer should not automatically be specified as a bearing-retention component without evaluating the mechanical system.
Electrical equipment can use push-on retainers in mechanical subassemblies involving:
shafts;
pins;
brackets;
actuators;
equipment hardware.
If conductivity, grounding or insulation matters, material and surface finish should be evaluated as part of the electrical design.
Fans, actuators, dampers and other HVAC mechanisms can contain shafts and pins requiring compact axial retention.
Environmental considerations may include:
condensation;
temperature cycling;
corrosion;
vibration.
The retainer material and surface protection should be selected accordingly.
Outdoor equipment can expose retaining fasteners to:
moisture;
dirt;
vibration;
temperature cycling;
corrosive environments.
A suitable push-on retainer can simplify assembly, but environmental protection should be evaluated together with the mating shaft.
Rollers, guides and lightweight mechanical systems can use push-on retainers where the required axial load and service conditions are appropriate.
If components require frequent replacement or maintenance, serviceability should be considered before choosing a permanent or semi-permanent push-on design.
Push-on retaining washers can be particularly attractive in high-volume production because they may eliminate:
thread machining;
retaining-groove machining;
separate threaded nuts;
nut-running operations.
Potential advantages include:
reduced assembly steps;
short installation cycle;
compact packaging;
automation potential.
But a lower assembly cost is only valuable if the retaining system reliably performs its required function.
For automated assembly, engineers should consider:
component orientation;
feeder compatibility;
installation direction;
installation force;
shaft alignment;
seating detection;
part-to-part dimensional variation.
A retaining washer that performs well in manual prototype assembly may still require optimization for automated production.
Two retainers for the same nominal shaft can have different tooth geometry and performance.
Excessive interference can increase installation force and shaft damage.
The shaft and tooth materials interact mechanically.
Material should be selected for the actual environment and mechanical requirements.
Removal can permanently alter the retaining geometry.
Groove-mounted rings and push-on toothed retainers use different interfaces and should be specified separately.
Use the following sequence when evaluating a star-type retaining washer.
Determine what must be held axially and why.
Specify:
diameter;
tolerance;
material;
hardness where relevant;
surface condition.
Establish the required retention behavior.
Determine whether avoiding a groove or thread provides a meaningful manufacturing benefit.
Decide whether the retainer must be removable or reusable.
Establish manual or automated installation requirements.
Match environmental and mechanical requirements.
Test production-representative retainers with representative shafts where application performance is important.
For an accurate quotation or custom development project, provide:
drawing or physical sample;
shaft diameter;
shaft tolerance;
shaft material;
shaft hardness where relevant;
shaft coating or surface finish;
retainer outside diameter;
retainer material;
material thickness;
required finish;
installed position;
axial retention requirement where specified;
installation-force requirement where specified;
operating environment;
application;
order quantity;
estimated annual demand;
packaging requirements.
A mating shaft sample can be especially useful for replacement and reverse-engineering projects.
A custom design may be appropriate when an OEM requires:
non-standard shaft diameter;
proprietary outer geometry;
special internal tooth configuration;
controlled installation behavior;
application-specific retention;
special material;
specific corrosion protection;
high-volume automated assembly.
The development process should begin with the functional shaft interface.
When an original drawing is unavailable, a replacement can be evaluated from:
existing sample;
shaft dimensions;
retainer dimensions;
material analysis where required;
application requirements;
installation method;
retention requirements.
Used samples require caution because their teeth may already have been permanently changed during installation or removal.
Whenever possible, an unused sample provides better dimensional information.
Star-type retaining washers are often suited to high-volume stamping and forming.
Manufacturing considerations can include:
material strip thickness;
blanking geometry;
internal tooth formation;
forming sequence;
material properties;
heat treatment where required;
surface treatment;
burr control;
dimensional inspection.
For large OEM quantities, tooling design and material utilization can materially affect production economics.
Inspection should focus on dimensions and characteristics that affect actual assembly performance.
Depending on the design, these can include:
central opening geometry;
tooth profile;
material thickness;
outside diameter;
flatness or formed geometry;
material condition;
coating.
Where retention is critical, dimensional inspection can be supplemented by agreed functional testing.
A Starlock-style washer is a push-on retaining fastener with internal gripping teeth designed to provide axial retention on a compatible shaft, pin or stud.
No conventional mating thread is required for typical push-on retaining washer designs.
Many push-on designs can operate without the conventional retaining groove required by circlips or E-clips.
Its internal teeth deflect during installation and then resist reverse axial movement through their interaction with the shaft.
No. Circlips generally engage a defined groove, while push-on retaining washers use an interference-based gripping interface.
It belongs to the broader push-on retaining-fastener family, but the star-type internal-tooth geometry describes a more specific product configuration.
Removal may be possible depending on the design, but it can deform the retainer or mark the shaft. Reuse should not be assumed.
Some push-on retaining concepts may be used with suitable polymer posts or shafts, but tooth geometry, shaft material and retention requirements must be evaluated together.
Stainless steel may be suitable for certain corrosion-resistant applications depending on geometry and mechanical requirements.
Retention depends on retainer geometry, material, thickness, shaft diameter, tolerance, hardness, surface condition and installation.
Yes. JUXIN FASTENERS supports drawing-based and sample-based development of custom stamped retaining fasteners for OEM and industrial applications.
A star-type retaining washer may look like a simple stamped component, but its performance is controlled by a precise mechanical interface.
The key relationship is:
internal tooth geometry + retainer material + shaft diameter + shaft tolerance + shaft material + installation condition.
For engineers, understanding this interface helps determine whether a push-on retaining washer, E-clip, circlip, threaded nut or another retaining technology is appropriate.
For procurement and supplier-development teams, providing both the retaining component specification and mating-shaft information can significantly reduce sourcing errors.
JUXIN FASTENERS supports global OEM, ODM, engineering, procurement, sourcing and supplier-development teams with standard and custom retaining fasteners,
stamped components and application-specific fastening solutions.
If you have a drawing, send the drawing.
If the original drawing is unavailable, send the existing retaining washer together with the mating shaft dimensions or physical sample.
For new OEM development, provide the shaft diameter and tolerance, material, surface condition, required retention behavior, installation method and estimated annual demand.
We can support technical review, sample evaluation, manufacturing feasibility review, custom development, quotation and volume production sourcing.
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Previous: Long Tab Washers Guide
 MORE NEWS

Sep. 27, 2026

Sep. 27, 2026

Sep. 27, 2026
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY