
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Mar. 29, 2026
Threaded Inserts for Plastic: Boss Design, Installation Methods and OEM Selection Guide
Plastic components are widely used in automotive electronics, electrical enclosures, industrial machinery,
robotics and precision equipment because they support lightweight construction, design flexibility and efficient manufacturing.
However, creating reliable threaded connections in plastic requires different engineering considerations from fastening metal components.
Directly formed or tapped plastic threads may be suitable for certain assemblies, but repeated screw installation,
elevated temperatures, sustained loading and limited thread engagement can introduce performance risks.
Threaded inserts for plastic provide a metal internal thread within a plastic component,
allowing designers to use machine screws while transferring fastening loads through the insert-to-polymer interface.
Depending on the application, engineers may select heat-set threaded inserts, ultrasonic inserts, self-tapping inserts, press-in inserts or molded-in threaded inserts.
Each installation method requires different hole geometry, material compatibility, production equipment and validation procedures.
This guide explains how to select and design threaded inserts for plastic components, with particular attention to boss dimensions, pilot holes,
pull-out resistance, torque-out performance, installation repeatability and total assembly cost.
Juxin Fasteners welcomes inquiries for thread insert nuts, plastic threaded inserts,
custom threaded bushings and OEM fastening components, with product specifications and manufacturing feasibility confirmed against customer drawings.
Why Use Threaded Inserts in Plastic Components?
Plastic materials generally behave differently from metals under concentrated mechanical loading.
Their strength, stiffness, creep resistance and thermal expansion characteristics depend on polymer chemistry, reinforcement, temperature, moisture and manufacturing conditions.
A screw installed directly into plastic may create or engage threads in the surrounding polymer.
For certain applications, this is an economical solution.
However, applications involving frequent servicing or machine-screw connections may benefit from a separate threaded insert.
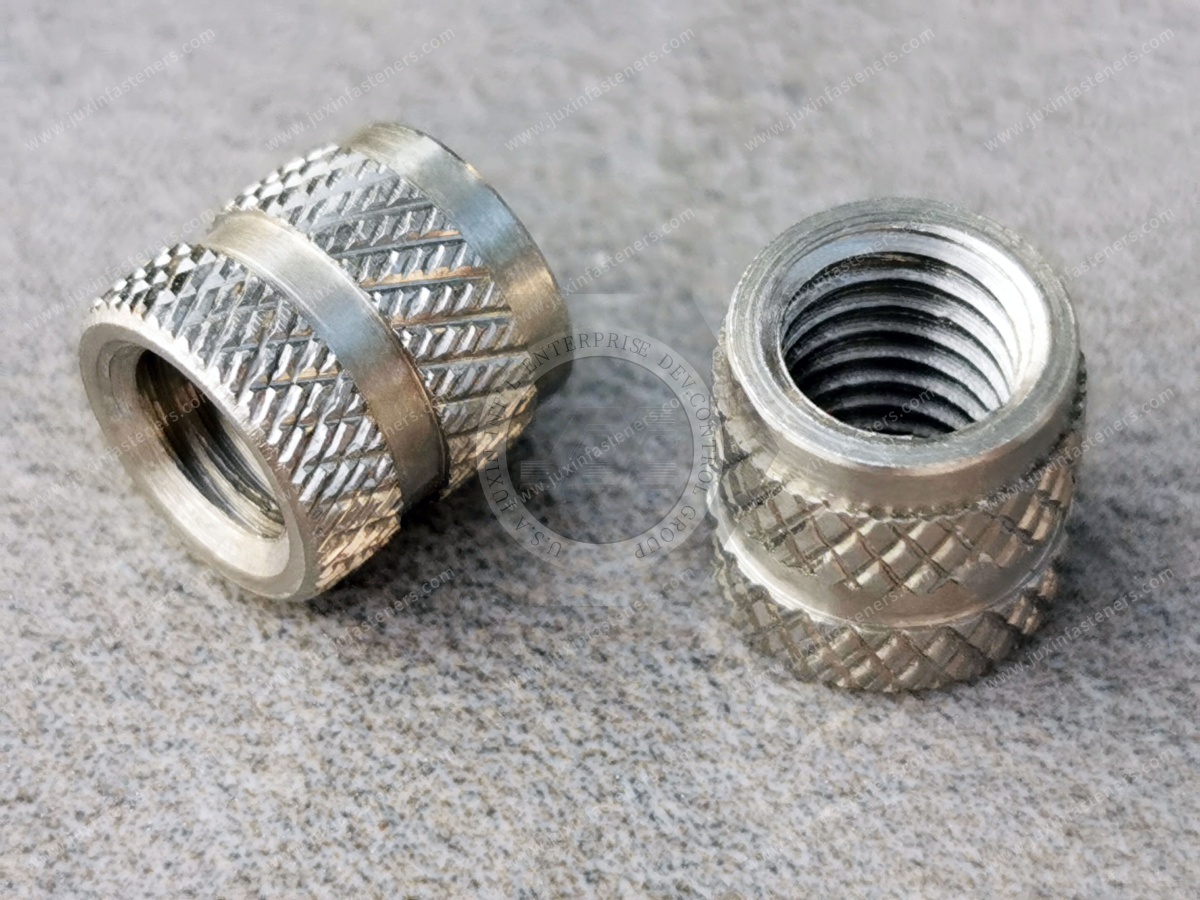
Common Problems with Direct Plastic Threads
Thread stripping during assembly
Progressive thread wear after repeated removal
Boss cracking from excessive installation stress
Reduced joint preload caused by polymer creep
Dimensional changes caused by temperature or moisture
Inconsistent assembly torque
Damage caused by cross-threading or incorrect screw engagement
How a Threaded Insert Changes the Load Path
A threaded insert provides a metal internal thread for the mating screw.
The screw engages the metal insert, while the insert transfers load into the surrounding plastic through external knurls, threads, ribs, undercuts or molded retention features.
The load path can be described as:
Machine screw → Internal insert thread → Insert retention geometry → Plastic boss or surrounding component
This distinction is important.
Although a metal insert may improve internal thread durability, the overall joint can still fail through insert pull-out, insert rotation or cracking of the surrounding plastic.
Engineering Principle
The strength of a threaded insert assembly is determined by both the metal insert and the polymer structure retaining it.
Key Benefits of Threaded Inserts for Plastic
Improved Internal Thread Durability
Metal internal threads can better tolerate repeated engagement with suitable machine screws than many directly formed plastic threads.
This is especially useful in serviceable products.
Improved Assembly Repeatability
A properly selected insert can provide a more consistent internal thread interface.
However, consistent tightening torque does not automatically guarantee consistent clamp load.
Joint friction, plastic compression and assembly conditions must also be considered.
Potentially Higher Pull-Out and Torque-Out Resistance
Appropriate insert retention geometry can improve resistance to axial extraction and rotation compared with unsuitable direct-thread designs.
Actual performance depends on the plastic material, insert geometry, hole preparation and installation process.
Repeated Maintenance and Repair
Threaded inserts are useful for:
Removable electrical enclosure covers
Electronic module mounting
Equipment access panels
Serviceable machine guards
Industrial control housings
Replaceable mechanical components
Important Limitation: Plastic Creep Remains Relevant
Installing a metal insert does not eliminate creep or stress relaxation in the surrounding polymer.
If the joint compresses plastic under sustained load, clamp force may still decrease over time.
For critical assemblies, engineers should consider load distribution, compression limiters, washers, joint geometry and appropriate preload validation.
Common Types of Threaded Inserts for Plastic
Different insert designs serve different manufacturing processes.
Heat-Set Threaded Inserts
Heat-set inserts are generally designed for compatible thermoplastic components.
A heated installation tip transfers heat to the metal insert, softening the surrounding polymer.
The insert is pressed into a prepared hole, allowing softened plastic to flow around its external retention features.
After cooling, the surrounding material helps retain the insert.
Typical Advantages
Suitable for selected thermoplastics
Controlled installation depth
Compatibility with automated insertion equipment
Potentially good pull-out and torque-out performance
Post-molding installation
Engineering Considerations
Polymer softening behavior
Insert temperature
Installation force
Dwell time
Cooling conditions
Boss geometry
Insert alignment
Tool-tip design
Common Failure Risks
Excessive temperature or pressure may damage the boss.
Insufficient heat may prevent adequate polymer flow around the insert.
Incorrect installation depth can affect mating-component fit.
Typical Applications
ABS electronic housings
Polycarbonate enclosures
Suitable nylon components
Automotive interior electronics
Industrial control modules
Compatibility must be established for the actual polymer grade.
Ultrasonic Threaded Inserts
Ultrasonic insertion uses high-frequency mechanical vibration to generate localized heat at the insert-to-plastic interface.
The softened polymer flows around the insert retention features during installation.
Potential Advantages
Integration into automated manufacturing
Short installation cycles in suitable applications
Controlled insertion depth
Reduced need for externally heated installation tips
Engineering Considerations
Ultrasonic frequency and amplitude
Applied force
Insert geometry
Polymer behavior
Installation time
Equipment tuning
Boss support
Potential Failure Risks
Incorrect process parameters may produce incomplete insertion, local material degradation, boss cracking or inconsistent retention.
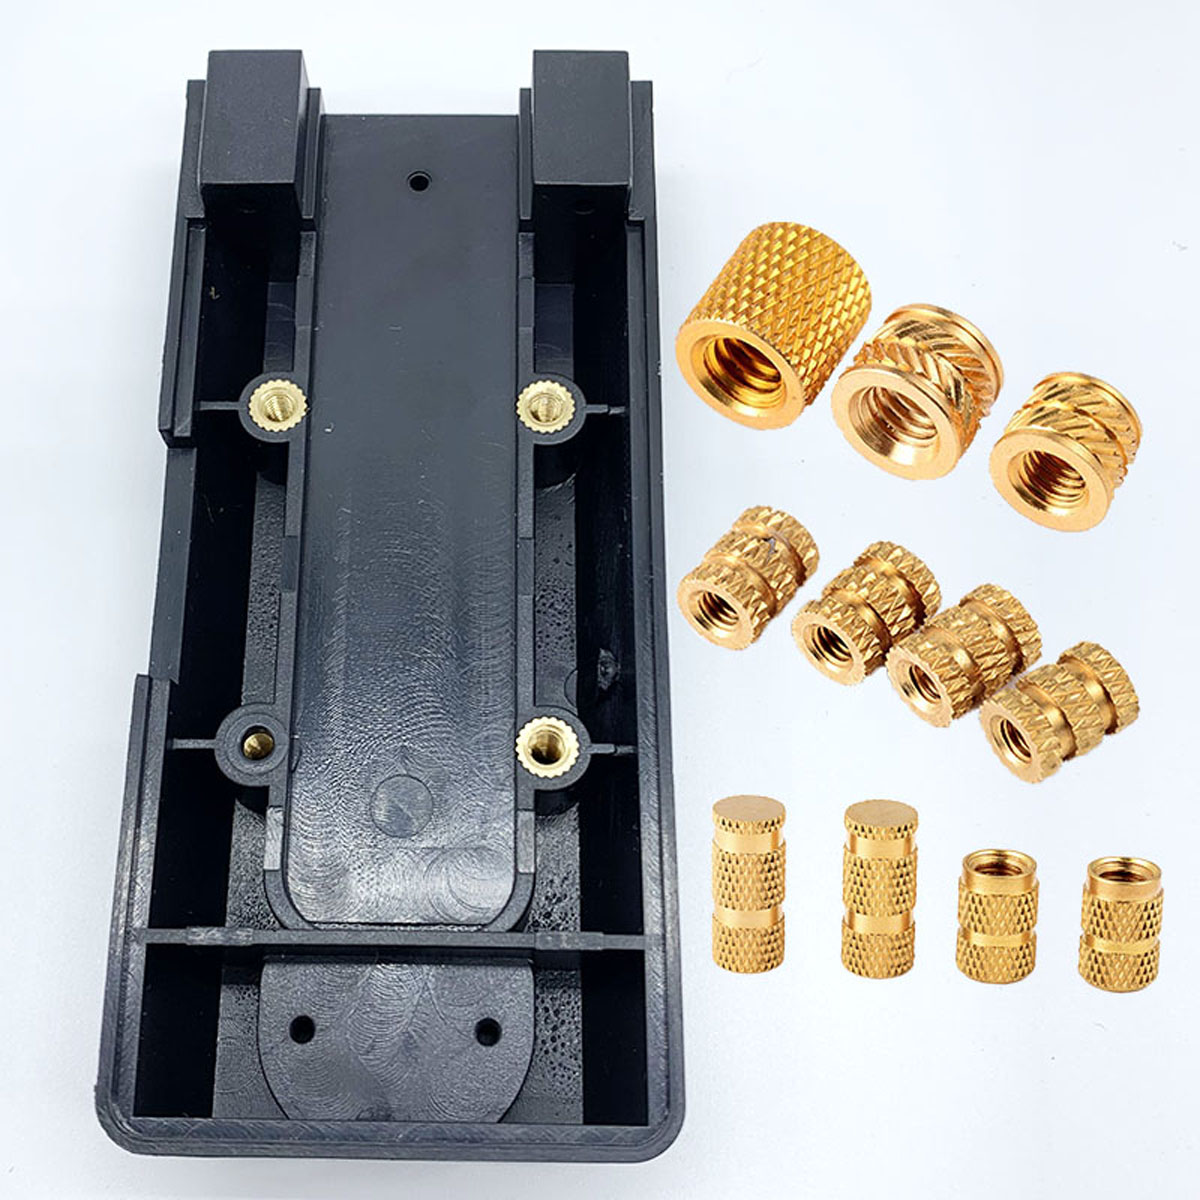
Heat-Set vs Ultrasonic Inserts
Both methods can be effective.
The best process depends on the polymer, insert geometry, equipment availability, production volume and required retention performance.
Neither method should be described as universally stronger without comparative testing.
Self-Tapping Threaded Inserts
Self-tapping inserts are installed into prepared holes using an external cutting or thread-forming geometry.
Depending on the design, the insert cuts or forms engagement features in the surrounding plastic.
Typical Advantages
Post-molding installation
No dedicated heating process
Suitability for selected repair and industrial assembly applications
Potential use in suitable plastics and soft materials
Engineering Considerations
Pilot hole diameter
Hole depth
External insert thread geometry
Installation torque
Polymer hardness
Boss wall thickness
Installation alignment
Common Failure Risks
Boss splitting
Excessive installation torque
Incomplete seating
Insert rotation
Reduced pull-out resistance
Damage caused by incorrect pilot hole dimensions
Important Selection Point
A self-tapping insert is not necessarily the best choice for every plastic.
Brittle polymers, thin bosses and highly reinforced materials may require special evaluation.
Press-In Threaded Inserts
Press-in inserts use external knurls, ribs or interference features to engage a prepared plastic hole.
They are installed through mechanical pressure.
Potential Advantages
Simple installation process
No external heating operation
Suitability for selected production-line applications
Possible low equipment complexity
Engineering Limitations
Press-in installation introduces radial stresses into the plastic.
If the boss is too thin or the interference is excessive, cracking or deformation may occur.
Typical Applications
Plastic equipment housings
Electrical components
Lightweight assemblies
Selected low- or moderate-load threaded attachment points
Performance depends on the insert and substrate design.
Molded-In Threaded Inserts
Molded-in inserts are positioned in the injection mold before the plastic is injected.
Molten polymer flows around the insert and its retention geometry.
After cooling, the insert becomes mechanically retained within the molded component.
Potential Advantages
No separate post-molding insertion operation
Integration into injection molding production
Potentially robust retention geometry
Suitability for selected high-volume manufacturing programs
Engineering Considerations
Mold insert positioning
Core pin design
Insert orientation
Polymer flow
Weld lines in molded plastic
Cooling shrinkage
Insert retention geometry
Mold cycle time
Risk of displaced inserts
Important Limitation
Molded-in inserts are not automatically stronger than heat-set or ultrasonic inserts.
Retention depends on the complete design and molding process.
Production Trade-Off
Molded-in inserts may reduce secondary assembly operations but introduce insert feeding, mold handling and production control requirements.
Threaded Insert Design Guidelines for Plastic Components
Reliable threaded insert performance begins with the surrounding plastic geometry.
Engineers should define the insert, pilot hole, boss, mating screw and expected loads as one system.
Pilot Hole Diameter
The pilot hole must match the selected insert design and installation method.
A hole that is too small may cause excessive installation force or boss cracking.
A hole that is too large may reduce retention or allow the insert to rotate.
Factors Affecting Pilot Hole Selection
Insert outside diameter
External knurl or thread geometry
Plastic type
Reinforcement content
Molding shrinkage
Installation temperature
Required retention performance
Engineering Recommendation
Use the dimensional requirements for the specific insert design and validate them in the actual molded component.
There is no universal pilot hole diameter suitable for all threaded inserts of the same internal thread size.
Hole Depth Requirements
Blind-hole depth must accommodate the insert, installation process and mating screw.
Insufficient depth can cause bottoming during insertion or final assembly.
Excessive depth may reduce support or complicate installation control.
Check the Following
Insert overall length
Insert installation depth
Blind-hole bottom clearance
Mating screw engagement
Screw tip clearance
Molded-hole tolerance
Any required counterbore
Engineering Note
Generic hole-depth multipliers should not replace the drawing requirements for the selected insert.
Plastic Boss Diameter
The boss must contain sufficient material around the insert to resist radial installation stress and service loading.
Important Variables
Insert outside diameter
Boss outside diameter
Minimum wall thickness
Polymer strength
Reinforcement
Installation method
Expected pull-out load
Applied tightening torque
A larger boss may improve structural support, but excessive wall thickness can also introduce injection-molding defects such as sink marks or uneven cooling.
Design Trade-Off
The boss must be strong enough to retain the insert while remaining manufacturable.
Why a Universal Boss Diameter Rule Is Unreliable
Two inserts with the same internal thread can have different outside diameters and retention geometries.
Likewise, an unfilled ABS boss and a glass-filled nylon boss may respond differently to the same installation conditions.
Therefore, boss diameter should be determined from the insert design, polymer data and application testing rather than from one fixed multiplier.
Boss Height and Insert Engagement
Boss height must support the insert's intended engagement length.
Insufficient boss height may reduce retention or leave inadequate surrounding material.
Excessive height may increase material consumption, molding complexity or dimensional variation.
Boss Reinforcement and Rib Design
Supporting ribs may improve boss stability.
However, ribs should be designed with appropriate wall thickness, fillets and molding considerations.
Poor rib geometry can introduce stress concentration, sink marks or warpage.
Counterbores and Recessed Installation
Some inserts require a counterbore or lead-in feature.
These may support:
Insert alignment
Headed insert seating
Flush installation
Controlled insertion depth
Counterbore dimensions must follow the selected product geometry.
Flush Installation and Protrusion Control
Insert height affects the fit between the plastic component and the mating part.
A protruding insert may interfere with assembly.
An excessively recessed insert may reduce available screw engagement or create unintended joint geometry.
Engineering Recommendation
Specify allowable insert protrusion or recess in the component drawing.
Do not apply a universal protrusion tolerance without confirming the assembly requirements.
Thread Engagement and Screw Length
The mating screw must engage enough internal threads to support the required loading without bottoming.
Verify
Screw thread specification
Insert internal thread length
Effective engagement
Mating component thickness
Washer thickness, if applicable
Screw tip clearance
Installation tolerance
Metric and Inch Thread Compatibility
Metric internal threads should be specified using the applicable ISO metric thread system.
Unified inch threads should be identified using the applicable ASME B1.1 designation.
Metric and UNC/UNF threads are not directly interchangeable.
For reference only, M4 nominal diameter is approximately 0.157 inch and M6 is approximately 0.236 inch.
These conversions do not establish interchangeability or confirm the availability of an inch-thread equivalent.
Plastic Threaded Insert Installation Methods
Installation process control is critical for consistent production.
Mechanical Installation
Mechanical methods include press-in and self-tapping insertion.
Key Process Variables
Hole dimensions
Installation force
Installation torque
Tool alignment
Insertion depth
Component support
Potential Production Issues
Misalignment
Boss cracking
Excessive installation force
Inconsistent seating
Insert rotation
Heat Installation
Heat-set installation requires a controlled thermal process.
Key Process Variables
Tip temperature
Contact time
Applied force
Installation depth
Cooling behavior
Potential Production Issues
Overheating
Polymer degradation
Incomplete material flow
Insert tilt
Boss deformation
Ultrasonic Installation
Ultrasonic insertion requires equipment settings appropriate to the polymer and insert.
Key Process Variables
Vibration amplitude
Installation force
Process time
Energy input
Insertion depth
Component support
Potential Production Issues
Local cracking
Incomplete insertion
Thermal degradation
Inconsistent retention
Molded-In Installation
Molded-in inserts require coordination with the injection molding process.
Key Process Variables
Insert positioning
Mold temperature
Injection pressure
Polymer flow
Cooling conditions
Insert retention in the mold
Potential Production Issues
Insert movement
Molded-in stress
Incorrect orientation
Poor polymer filling
Dimensional variation
Plastic Material Compatibility
Plastic threaded insert performance depends strongly on the actual polymer grade.
ABS — Acrylonitrile Butadiene Styrene
ABS is commonly used in electronics housings, automotive interior components and industrial enclosures.
Design Considerations
Boss wall thickness
Heat-set installation conditions
Dimensional stability
Impact resistance
Service temperature
PC — Polycarbonate
Polycarbonate is used where impact resistance and dimensional performance are important.
Design Considerations
Installation stress
Stress cracking
Thermal process compatibility
Chemical exposure
Boss geometry
PA — Polyamide / Nylon
Polyamide is common in engineering components.
Design Considerations
Moisture absorption
Dimensional changes
Reinforcement content
Installation temperature
Long-term creep
POM — Polyoxymethylene
POM is used in precision mechanical components.
Design Considerations
Material-specific insert retention
Installation method
Low-friction behavior
Dimensional requirements
PP and PE — Polypropylene and Polyethylene
These polymers may require special attention because their stiffness, creep behavior and retention characteristics differ from those of many engineering plastics.
Design Considerations
Creep
Boss deformation
Thermal behavior
Insert retention
Long-term load performance
Glass-Filled Engineering Plastics
Glass reinforcement may improve stiffness and dimensional performance.
However, it can also influence:
Local brittleness
Installation force
Material flow around the insert
Boss cracking
Tool wear
Engineering Principle
Compatibility should be evaluated for the specific polymer grade, reinforcement level and molding conditions—not simply the general material family.
Mechanical Performance: Pull-Out, Torque-Out and Joint Reliability
Threaded insert qualification should focus on the installed assembly.
Pull-Out Resistance
Pull-out resistance measures the force required to extract the insert from the surrounding plastic under defined test conditions.
Factors Affecting Pull-Out Performance
Insert geometry
Engagement length
Polymer strength
Boss dimensions
Hole geometry
Installation quality
Temperature
Loading rate
Torque-Out Resistance
Torque-out resistance measures resistance to rotation of the insert relative to the surrounding plastic.
Factors Affecting Torque-Out Performance
Knurl geometry
External thread design
Insert outside diameter
Polymer behavior
Installation process
Boss support
Important Distinction
Torque-out resistance is not the same as recommended screw tightening torque.
A safe assembly torque must consider the screw, internal thread, insert retention, plastic component and complete joint.
Repeated Assembly Performance
Threaded inserts may improve serviceability when machine screws are repeatedly installed and removed.
However, repeated assembly performance still depends on:
Screw material
Thread geometry
Tightening torque
Thread wear
Insert retention
Plastic creep
Maintenance practices
Vibration Resistance
A metal threaded insert does not inherently prevent screw loosening.
Vibration resistance depends on the complete joint design, preload, loading conditions and any specified locking method.
Thermal Cycling
Plastic and metal expand at different rates.
Repeated temperature changes can influence insert retention, stress distribution and joint preload.
Design Considerations
Coefficient of thermal expansion
Operating temperature range
Polymer creep
Insert geometry
Assembly preload
Environmental exposure
Common Failure Modes and Prevention
| Failure mode | Possible cause | Engineering response |
|---|---|---|
| Insert pull-out | Insufficient retention or weak boss | Review geometry, material and installation |
| Insert rotation | Inadequate anti-rotation engagement | Review knurl, hole and process |
| Boss cracking | Excessive radial stress | Review wall thickness and installation |
| Thread stripping | Excessive torque or insufficient engagement | Review screw and internal thread |
| Insert tilt | Poor alignment | Improve tooling and positioning |
| Insert protrusion | Incorrect insertion depth | Control stroke and seating |
| Plastic creep | Sustained stress or temperature | Review joint design and preload |
| Thermal damage | Excessive installation energy | Optimize process settings |
| Assembly loosening | Inadequate joint preload | Validate complete fastening system |
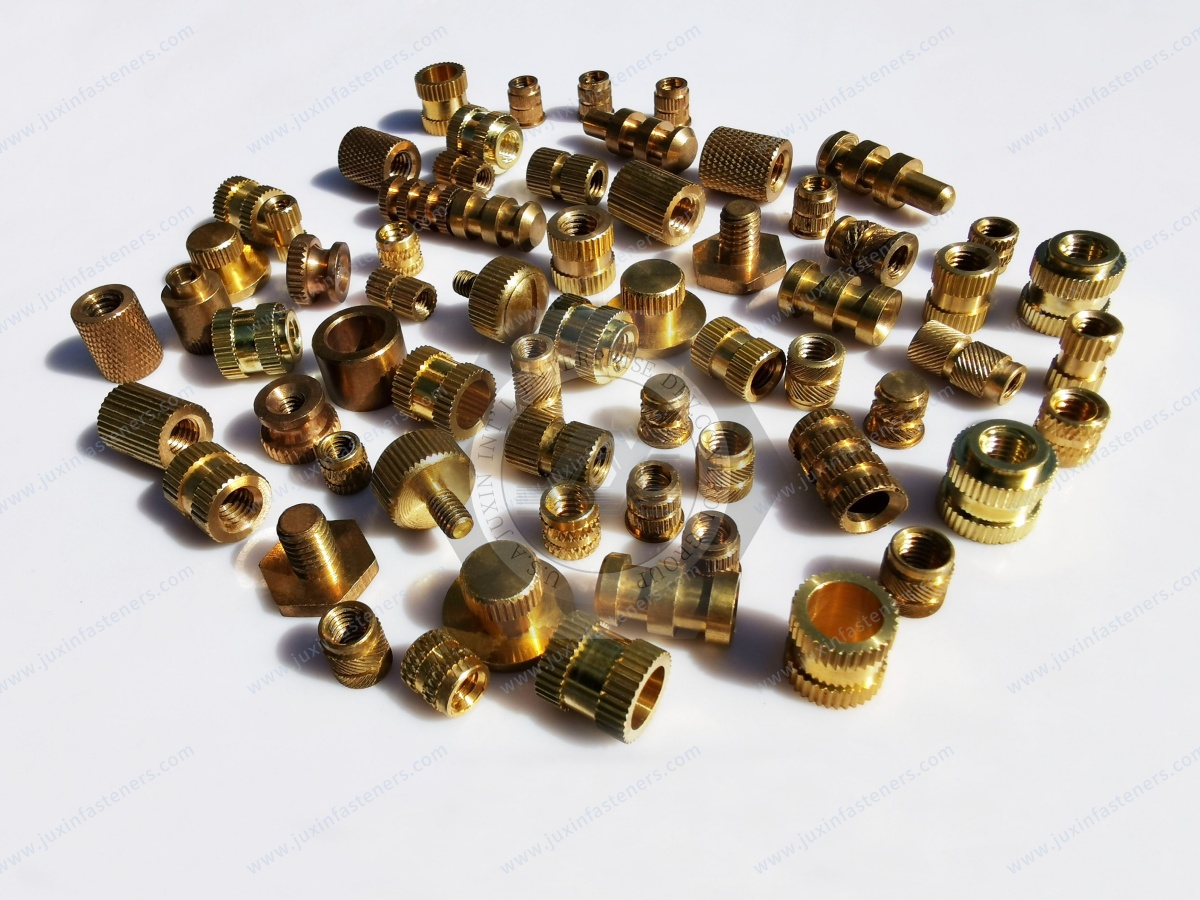
Information Gain: Why a Stronger Metal Insert Does Not Always Produce a Stronger Joint
A metal insert may have sufficient internal thread strength while the surrounding plastic remains the limiting element.
For example, increasing the screw property class may not improve the joint if the boss fails first.
Engineering Lesson
Evaluate the weakest element in the complete load path.
Information Gain: Why Larger Inserts Are Not Always Better
A larger insert may provide more external contact area.
However, it also requires a larger hole and may increase radial stress or reduce the available boss wall thickness.
In compact housings, this can create new failure risks.
Engineering Lesson
Insert size must be balanced against the available plastic geometry.
Information Gain: Why Installation Temperature Matters
For heat-set inserts, insufficient heat may prevent adequate polymer flow.
Excessive heat may degrade the polymer or distort the boss.
The best setting depends on the actual insert and polymer.
Engineering Lesson
Installation temperature should be qualified as a process parameter rather than copied from a generic recommendation.
Information Gain: Why Tightening Torque Alone Cannot Define Joint Reliability
A tightening torque value does not directly reveal the actual clamp force.
Friction, thread condition, screw geometry and compression of plastic components influence the resulting joint.
Engineering Lesson
Where clamp force matters, validate the complete assembly rather than relying only on nominal screw torque.
Industrial Applications of Threaded Inserts for Plastic
Automotive Interior and Electronics
Plastic threaded inserts may be used in:
Dashboard assemblies
Electronic control housings
Interior mounting brackets
Switch housings
Serviceable modules
Engineering Priorities
Repeated assembly
Vibration
Thermal cycling
Dimensional stability
Production repeatability
Electric Vehicle Electronics
EV systems contain plastic and composite components that require threaded mounting points.
Potential Applications
Battery management electronics housings
Electrical covers
Charging equipment enclosures
Control module housings
Auxiliary component mounting
Engineering Priorities
Material compatibility
Thermal exposure
Electrical insulation requirements
Vibration
Service access
Assembly reliability
Important Limitation
Electrical and battery-related applications may require additional safety and environmental qualification.
General industrial inserts should not be assumed suitable for safety-critical EV assemblies without validation.
Electrical Cabinets and Electronic Equipment
Common applications include:
ABS control boxes
Polycarbonate enclosures
Sensor housings
Circuit board support structures
Industrial electronics modules
Engineering Priorities
Compact boss design
Assembly access
Screw retention
Serviceability
Enclosure integrity
Medical and Laboratory Equipment
Threaded inserts may be considered for suitable noncritical equipment housings and serviceable mechanical assemblies.
Potential Applications
Diagnostic equipment enclosures
Laboratory instrument housings
Equipment access panels
Precision mechanical covers
Engineering Priorities
Material compatibility
Cleaning exposure
Repeated servicing
Dimensional accuracy
Customer-specific qualification
Medical-device use requires appropriate application-specific approval and documentation.
Industrial Machinery and Robotics
Automation equipment frequently includes plastic covers, sensor mounts and electronic housings.
Potential Applications
Robot controller enclosures
Machine guards
Sensor housings
Equipment access covers
Automated inspection equipment
Engineering Priorities
Repeated maintenance
Installation repeatability
Vibration
Component replacement
Production efficiency
Aerospace-Related and Lightweight Equipment
Suitable threaded inserts may be evaluated for lightweight equipment housings and noncritical support applications.
However, aerospace use requires customer approval and applicable qualification.
A general industrial threaded insert specification does not establish aerospace certification.
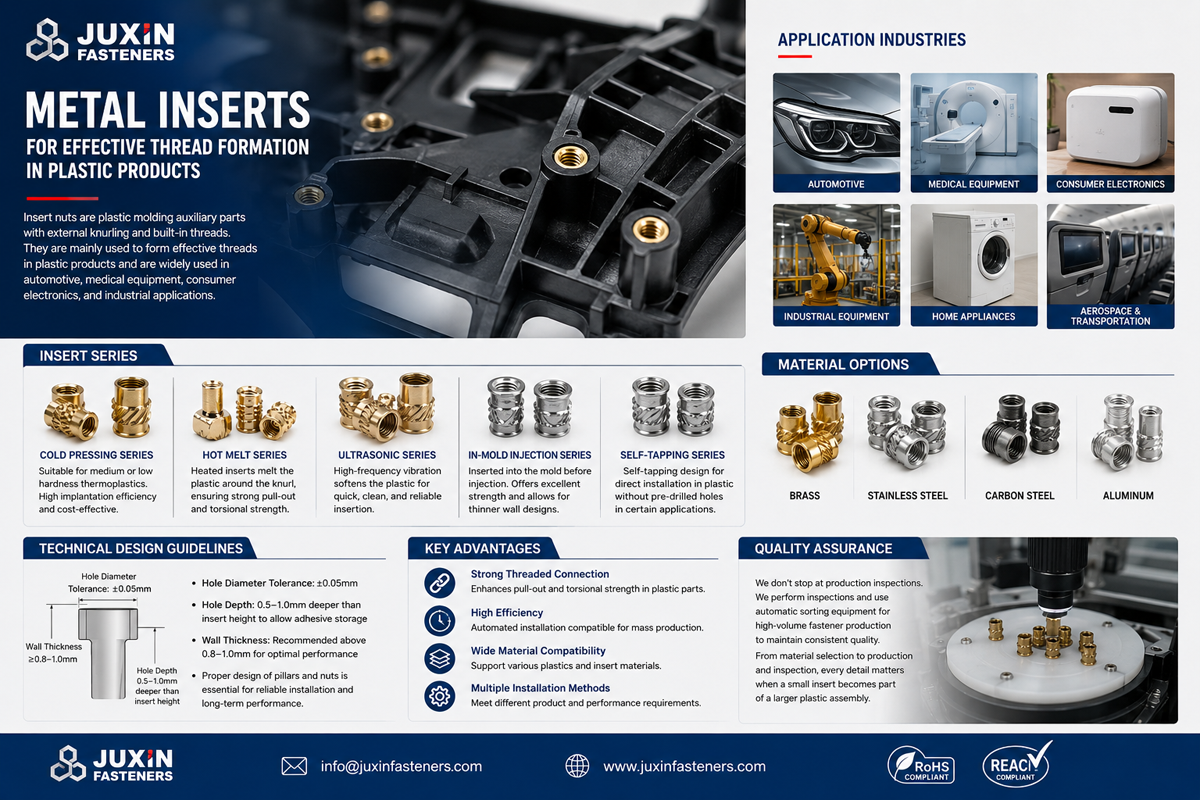
How to Select the Right Threaded Insert for Plastic
A structured selection process can reduce engineering changes and production problems.
Step 1: Identify the Plastic Material
Specify:
Polymer type
Exact grade
Reinforcement content
Relevant material properties
Service temperature
Step 2: Define the Connection Requirements
Determine:
Internal thread size
Screw specification
Required load
Tightening torque
Maintenance frequency
Environmental conditions
Step 3: Select the Installation Method
Evaluate:
Heat-set insertion
Ultrasonic insertion
Self-tapping insertion
Press-in installation
Molded-in installation
Step 4: Design the Boss and Pilot Hole
Confirm:
Hole diameter
Hole depth
Boss diameter
Boss height
Wall thickness
Counterbore
Installation clearance
Step 5: Validate Mechanical Performance
Consider:
Pull-out testing
Torque-out testing
Assembly torque verification
Repeated assembly
Thermal cycling
Environmental conditioning
Vibration where relevant
Step 6: Evaluate Production Compatibility
Consider:
Equipment availability
Cycle time
Tooling cost
Operator requirements
Automation potential
Inspection
Rework procedures
Step 7: Confirm Commercial Requirements
Evaluate:
Material options
Drawing conformity
MOQ
Prototype quantities
Annual volume
Packaging
Lead time
Long-term supply requirements
Manufacturing Efficiency: Choosing the Best Insert Installation Process
For production managers, installation method can influence total manufacturing cost.
| Installation method | Potential production advantage | Main production consideration |
|---|---|---|
| Heat-set | Controlled post-molding insertion | Temperature and dwell control |
| Ultrasonic | Potentially short cycle time | Equipment tuning and polymer compatibility |
| Self-tapping | No thermal insertion process | Torque and boss stress |
| Press-in | Simple mechanical installation | Interference and cracking risk |
| Molded-in | No separate insertion operation | Mold handling and insert positioning |
Total Installed Cost
The cost of a threaded insert assembly includes more than the insert purchase price.
Total Installed Cost = Insert Cost + Hole/Boss Preparation + Installation Labor + Equipment Allocation + Inspection + Expected Rework
This is a practical cost-model framework rather than a fixed formula for every application.
Production-Line Considerations
Insert feeding and orientation
Installation cycle time
Tool changeover
Process monitoring
Installation depth verification
Scrap and rework
Equipment maintenance
Operator training
Example Decision
For a low-volume service component, a suitable self-tapping insert may reduce dedicated equipment requirements.
For a high-volume thermoplastic housing, automated heat-set or ultrasonic installation may be commercially attractive.
For an injection-molded component with appropriate mold design, molded-in inserts may eliminate a secondary insertion step.
The final choice should be based on validated performance and total production cost.
Quality Control and Inspection for OEM Threaded Inserts
A reliable OEM supply program should define inspection requirements for both the insert and the installed assembly.
Insert-Level Inspection
Potential characteristics include:
Internal thread dimensions
Outside diameter
Overall length
Knurl or external thread geometry
Material
Surface finish
Visual defects
Assembly-Level Inspection
Potential characteristics include:
Installation depth
Insert alignment
Boss condition
Pull-out resistance
Torque-out resistance
Screw engagement
Repeated assembly performance
Relevant Technical References
Depending on the product and customer drawing, applicable standards may include:
ISO 261 and ISO 965 series: Metric thread selection and tolerances
ASME B1.1: Unified inch screw threads
ISO 2859-1: Sampling procedures for inspection by attributes, when specified
ISO 9227: Salt spray testing of metallic materials and coatings, when corrosion testing is relevant
These standards address specific technical subjects. They do not replace insert-specific installation instructions or customer-defined mechanical acceptance criteria.
Supplier Qualification and OEM Sourcing
Procurement teams should confirm whether a proposed insert supplier can meet the drawing, material and quality requirements of the project.
Product Requirements
Internal thread designation
Insert geometry
Material
Surface finish
Drawing tolerances
Installation method
Technical Requirements
Plastic substrate
Pilot hole dimensions
Boss geometry
Mechanical loads
Installation process
Inspection and testing requirements
Commercial Requirements
Prototype quantity
Annual demand
MOQ
Production schedule
Packaging
Delivery destination
Required lead time
Important Procurement Consideration
Two inserts with the same internal thread may not be interchangeable.
Differences in external geometry, installation method and retention performance can require changes to the plastic boss or production tooling.
OEM RFQ Checklist for Plastic Threaded Inserts
| RFQ item | Required information |
|---|---|
| Product type | Heat-set, ultrasonic, self-tapping, press-in or molded-in |
| Internal thread | Metric or unified inch designation |
| Insert material | Brass, stainless steel or other specified material |
| Surface finish | Drawing requirement |
| Insert dimensions | OD, length, knurl and geometry |
| Plastic material | Exact polymer grade |
| Reinforcement | Glass fiber or other filler |
| Pilot hole | Diameter, depth and tolerance |
| Boss geometry | OD, height and wall thickness |
| Installation method | Equipment and process |
| Load requirements | Pull-out, torque-out and service loads |
| Service conditions | Temperature, humidity, chemicals |
| Assembly cycles | Expected maintenance frequency |
| Inspection | Test methods and acceptance criteria |
| Prototype demand | Sample quantity |
| Annual demand | Forecast volume |
| MOQ | Commercial confirmation |
| Lead time | Required schedule |
| Packaging | Bulk or protected packaging |
Frequently Asked Questions
What are threaded inserts for plastic?
Threaded inserts are fastening components installed into plastic parts to provide internal machine threads.
Are brass threaded inserts suitable for plastic?
Brass inserts are commonly used in plastic assemblies because of their machinability and compatibility with various insert geometries.
Suitability depends on the application and environment.
Can stainless steel threaded inserts be used in plastic?
Yes, suitable stainless steel inserts may be used where material requirements justify their selection.
Geometry, installation method and polymer compatibility must be verified.
Which is better: heat-set or self-tapping inserts?
Neither is universally better. Heat-set inserts are often considered for compatible thermoplastics,
while self-tapping inserts may suit applications where mechanical installation is preferred.
How do I determine the correct pilot hole diameter?
Use the selected insert's dimensional requirements and validate the hole in the actual plastic component.
What boss diameter should I use for a threaded insert?
Boss diameter depends on insert outside diameter, polymer properties, installation method and required loads.
A universal multiplier is not sufficient for final design.
How can threaded insert pull-out strength be improved?
Possible measures include optimizing insert retention geometry, boss dimensions, polymer selection, hole preparation and installation parameters.
Do threaded inserts prevent screw loosening?
Not inherently. Joint preload, vibration, loading conditions and any locking method must be evaluated separately.
Are threaded inserts suitable for repeated assembly?
They can improve internal thread durability, but repeated assembly performance must be validated for the complete joint.
Can metric threaded inserts replace UNC or UNF inserts?
No. Metric and unified inch thread systems are not directly interchangeable.
Juxin Fasteners: OEM Threaded Insert Solutions for Plastic Components
Juxin Fasteners welcomes drawing-based inquiries for industrial threaded inserts and customized fastening components.
Relevant product categories include:
Thread insert nuts
Plastic threaded inserts
Self-tapping threaded inserts
Press-in threaded inserts
Molded-in insert designs
Custom threaded bushings
OEM precision fastening components
Availability of particular materials, dimensions, insert geometries, installation designs and production quantities must be confirmed against project requirements.
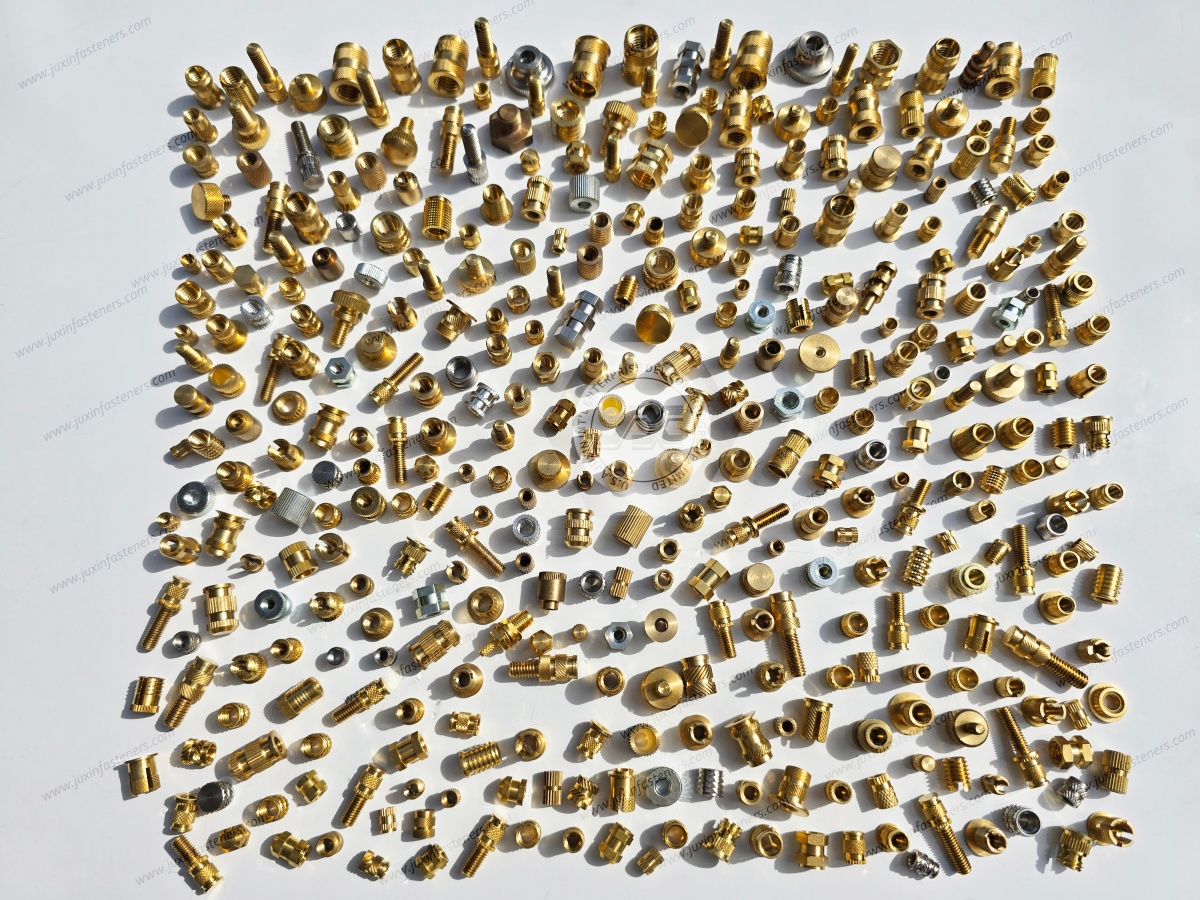
Request a Custom Threaded Insert RFQ
Are you developing a plastic housing, sourcing brass threaded inserts for injection-molded parts, evaluating self-tapping threaded inserts,
or looking for a supplier of custom OEM thread insert nuts?
Juxin Fasteners welcomes inquiries from design engineers, mechanical engineers, manufacturing engineers, production managers,
purchasing specialists, procurement managers, supplier development teams and supply chain managers.
For technical evaluation and quotation, please provide:
Product drawing + internal thread specification + insert material + plastic material + boss geometry + pilot hole dimensions
+ installation method + load requirements + environmental conditions + inspection requirements + prototype quantity + annual demand + packaging + delivery schedule.
Our team can review the supplied requirements and confirm product availability, technical feasibility and quotation conditions.
Company: Juxin Fasteners
Website: https://www.juxinfasteners.com/
Email: info@juxinfasteners.com
Send your drawings and OEM RFQ to Juxin Fasteners for threaded insert selection, technical confirmation and quotation.
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY



