Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809
Unified inch screw threads remain important across North American industrial equipment, HVAC systems, machinery, electrical enclosures,
legacy equipment and many global OEM assemblies designed around inch-series hardware.
Where a removable fastening point is required near an accessible sheet-metal edge, inch clip-on nuts can provide an efficient mechanically
installed solution without requiring a loose nut to be manually positioned behind the panel.
Product Specification
Unified inch screw threads remain important across North American industrial equipment, HVAC systems, machinery,
electrical enclosures, legacy equipment and many global OEM assemblies designed around inch-series hardware.
Where a removable fastening point is required near an accessible sheet-metal edge,
inch clip-on nuts can provide an efficient mechanically installed solution without requiring a loose nut to be manually positioned behind the panel.
Depending on the product geometry, inch-series clip-on fasteners can include:
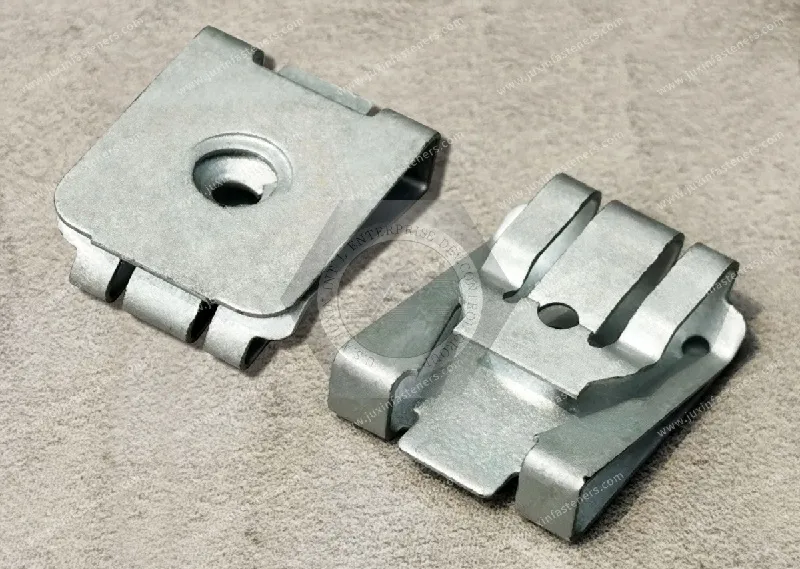
inch U-nuts;
inch J-nuts;
inch spring nuts;
barrel-style clip nuts;
clip-on nuts for tapping screws;
flanged-edge clip nuts;
other drawing-based edge-mounted fasteners.
However, an inch thread designation alone does not define the complete fastener.
A sourcing request such as:
“Need 1/4-20 clip nut”
still leaves several critical engineering variables undefined.
For OEM sourcing, JUXIN FASTENERS recommends a complete selection path:
Thread Designation → TPI → Thread Architecture → Mating Screw → Actual Panel Thickness → Hole Setback → Throat Depth → Clip Geometry → Installation Envelope → Material → Finish
This reduces the risk of approving a component that has the correct thread but does not fit the actual sheet-metal assembly.
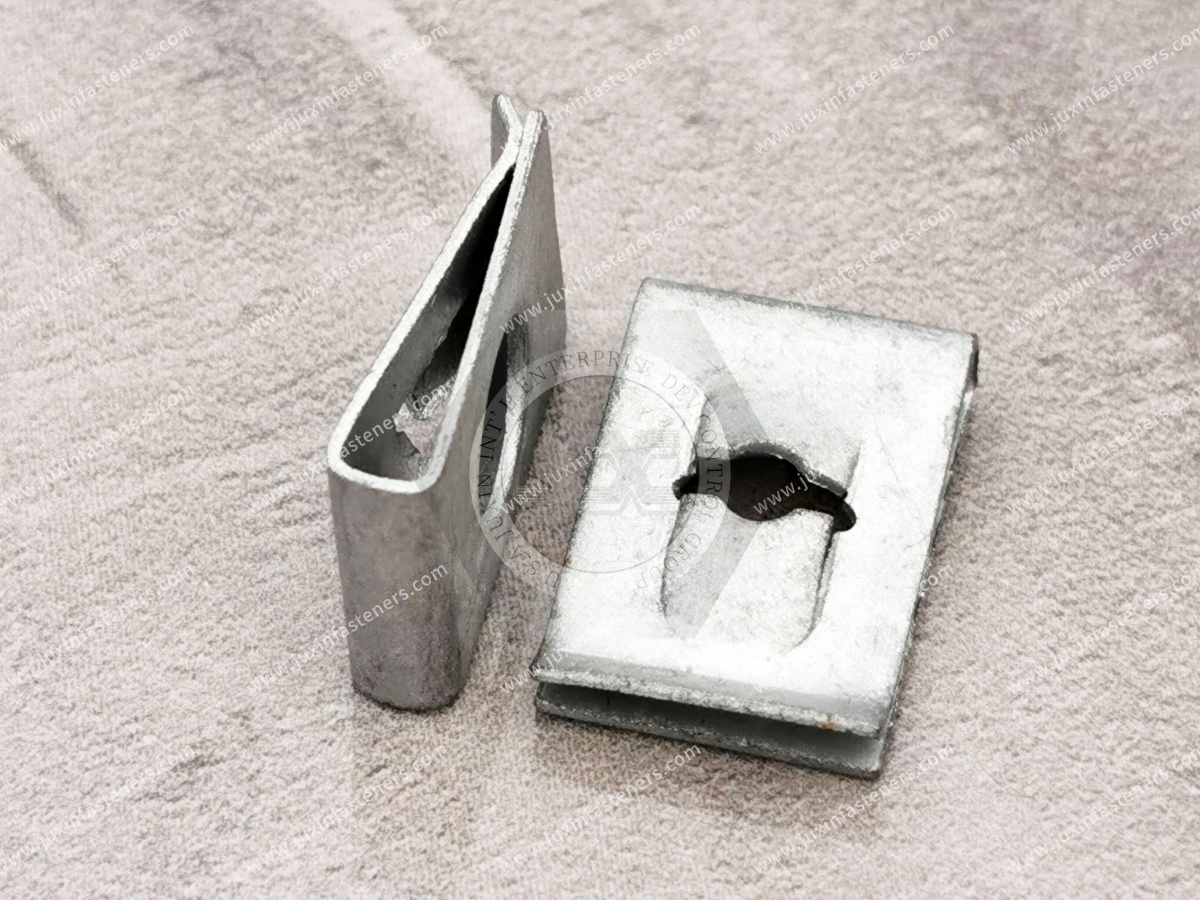
An inch clip-on nut is an edge-mounted fastener designed around an inch-series screw or screw interface.
Depending on the design, it may use:
a formed screw-thread feature;
a captive threaded element;
a barrel-style threaded feature;
a screw-engaging spring feature;
another product-specific architecture.
The fastener is generally installed from an accessible sheet-metal edge and positions the screw-engaging feature relative to the required mounting location.
This means that thread size and clip geometry must be specified together.
Unified inch screw threads are widely used in North American and international industrial equipment.
Common terminology includes:
UNC — Unified National Coarse;
UNF — Unified National Fine;
thread diameter;
threads per inch, or TPI;
thread class.
ASME B1.1 is an important reference for Unified Inch Screw Threads within its scope.
However, a thread standard defines the screw-thread system.
It does not define every U-nut, J-nut or clip-on nut body.
A proprietary or drawing-based clip-on nut can use a Unified inch thread while the spring-clip geometry remains controlled by the component drawing.
In an inch thread designation, the diameter and threads-per-inch value work together to identify the thread.
For example, two threads with the same nominal diameter can use different TPI values.
For sourcing, engineers should therefore identify:
nominal thread designation;
TPI;
UNC, UNF or other applicable series;
thread class where relevant;
mating screw specification.
Do not order an inch clip-on nut from nominal diameter alone.
UNC and UNF use different pitch relationships within the Unified thread system.
UNC provides a coarser pitch for a given nominal diameter than UNF.
UNF provides a finer pitch with more threads per inch.
Those differences can influence the geometry of the threaded interface and other joint-design considerations.
However, the correct series should normally follow the actual mating screw and engineering requirements.
Gemini's original draft stated that UNC provides greater resistance to thread stripping in formed spring cages as a general rule.
That is too broad.
Thread stripping depends on the complete threaded interface, including:
thread geometry;
material;
engagement;
mating screw;
thread construction;
loading;
manufacturing quality.
A UNC designation alone does not establish stripping strength.
The actual clip-on nut design must be evaluated.
Another common assumption is that fine threads should be selected for vibration-prone equipment.
That should not be generalized.
Resistance to self-loosening under transverse vibration can depend on:
preload;
joint stiffness;
friction;
clamp length;
mating surfaces;
external loading;
locking strategy;
screw and nut geometry.
Therefore:
UNF ≠ Vibration-Proof
and:
Inch Clip-On Nut ≠ Self-Locking Fastener
unless a specific locking function is separately designed and validated.
Even if the nominal screw diameter remains the same, changing thread series changes the mating interface.
An alternate clip-on nut should match the required screw specification.
Procurement should not approve a substitution based only on nominal diameter.
Where a conventional Unified thread is used, thread class may be relevant to the mating interface.
However, not every clip-on fastener uses the same type of threaded construction.
The applicable thread requirement should therefore be confirmed from:
customer drawing;
product drawing;
mating screw;
actual clip-nut architecture.
Do not assign a generic ASME thread class to every clip-on fastener without confirming that it applies.
Inch fastening systems can include both numbered screw sizes and fractional-inch diameters.
Commercial clip-on nut families may therefore be encountered across multiple inch-series thread designations.
However, JUXIN FASTENERS should not publish a fixed list such as #8-32, #10-24, 1/4-20, 5/16-18 and 3/8-16 as universal availability
across every clip geometry unless the exact product data confirms those combinations.
Availability can depend on:
clip geometry;
thread architecture;
panel thickness;
throat depth;
material;
finish;
tooling;
production quantity.
For OEM sourcing, provide the actual required thread designation and drawing.
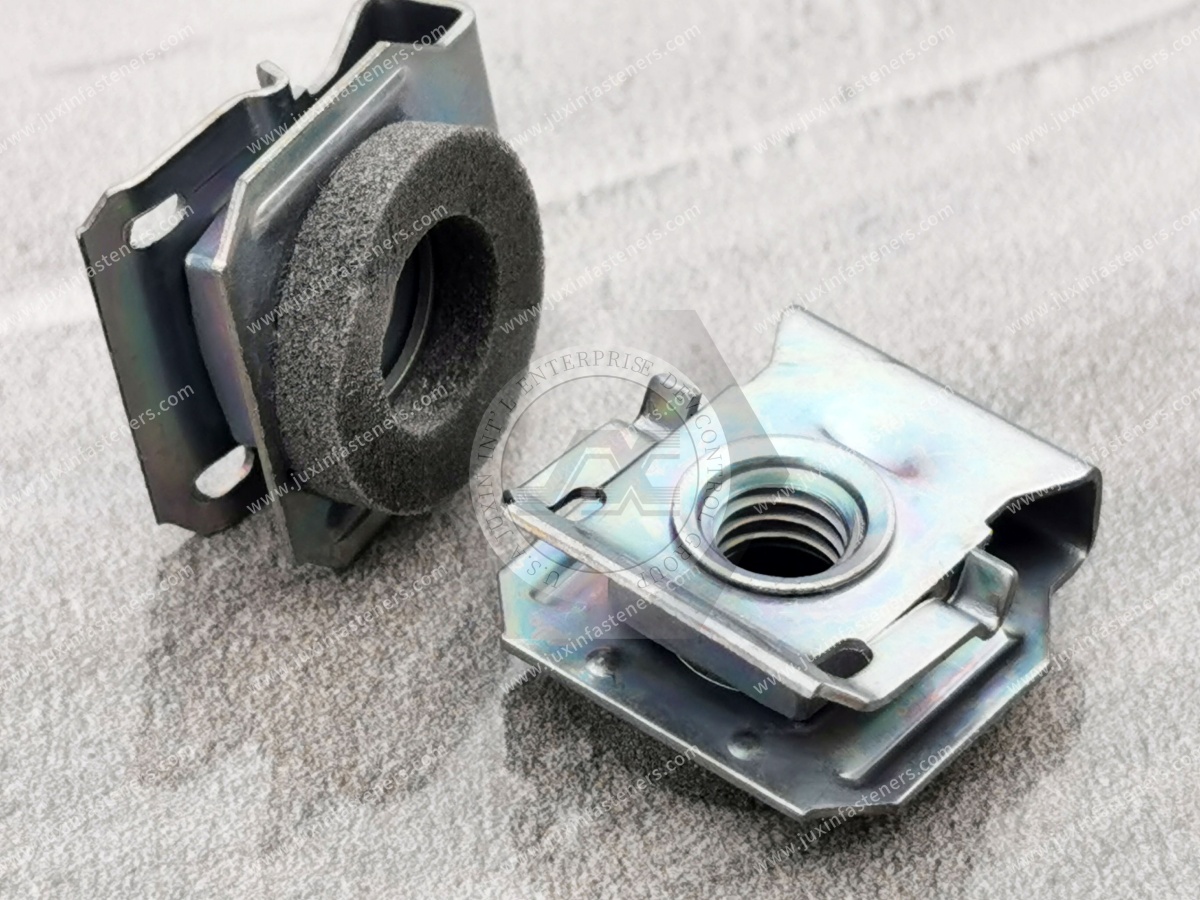
A barrel-style clip nut may provide a different threaded geometry from a stamped spring nut.
A captive hex configuration can differ again.
A tapping-screw clip operates through another screw-engagement principle.
Therefore, there is no single universal thread-engagement rule for all inch clip-on nuts.
The correct engagement should be evaluated for the specific product and mating screw.
Gemini's original draft stated that the mating screw must completely pass through the spring thread profile.
That is not universally required.
Correct screw length depends on:
thread architecture;
joint stack;
required engagement;
backside clearance;
adjacent components;
enclosed geometry where applicable.
The correct engineering question is:
Does the screw provide the required engagement and clamp the intended assembly without unwanted bottoming or interference?
A clip-on nut can have the correct UNC or UNF thread while the selected screw is still too short or too long for the assembly.
Engineers should evaluate:
joint stack thickness;
washer thickness where applicable;
thread engagement;
fastener geometry;
screw protrusion;
backside clearance;
nearby components.
This is particularly important in compact equipment enclosures.
An inch clip-on nut must fit the actual sheet-metal panel.
Panel thickness influences how the clip is installed and how its geometry interacts with the sheet after installation.
If the panel is outside the intended condition for the selected clip, possible problems can include:
difficult installation;
incomplete seating;
permanent deformation;
altered pre-assembly retention;
thread misalignment;
coating damage.
Thread size does not solve a panel-fit problem.
Sheet-metal gauge numbers can create sourcing ambiguity.
A gauge number is not a universal physical thickness independent of material and gauge system.
The same gauge designation can correspond to different actual thicknesses depending on the material and convention being used.
For international OEM sourcing, it is therefore safer to provide:
panel material;
nominal actual thickness;
minimum thickness where relevant;
maximum thickness where relevant.
For inch-series drawings, actual thickness can be specified in decimal inches.
A metric equivalent may also be added for supplier communication where useful, but the controlling drawing dimension should remain clear.
An RFQ stating:
“16 gauge panel”
may be ambiguous without the panel material and governing sheet convention.
A better requirement identifies:
Material + Actual Thickness + Tolerance
This is especially important when sourcing across different countries and supplier systems.
Every clip-on nut geometry can have its own panel-thickness capability.
A generic website should not invent a universal fractional or decimal-inch grip range.
The correct panel range must come from:
confirmed product data;
drawing;
customer specification;
prototype validation.
This prevents a generic catalog number from becoming an unintended engineering guarantee.
The actual clip may be installed after the panel receives:
paint;
powder coating;
plating;
another finish.
The assembly may also contain:
overlapping sheets;
folded layers;
hems;
flanges.
Therefore, the relevant fit condition is:
Finished Clip + Finished Panel
rather than only nominal bare-sheet thickness.
For an edge-mounted clip, the fastening feature must align with the intended panel hole.
The edge-to-hole-center relationship is therefore critical.
If the selected clip has the wrong reach, possible consequences include:
screw-starting difficulty;
thread misalignment;
clip displacement;
incomplete seating;
production rework.
A 1/4-20 thread cannot compensate for an incorrect hole setback.
The clip throat or reach controls how far the thread center sits from the accessible panel edge.
A useful geometric relationship is:
Panel Edge → Clip Entry → Clip Throat/Reach → Thread Center → Panel Hole
This is one of the most important dimensions when replacing an existing inch clip nut.
Two suppliers may both quote a 1/4-20 U-nut.
One can still position the thread center differently from the other.
If the existing panel hole is already fixed, even a small geometric difference can prevent correct alignment.
For alternate supplier qualification:
Thread Match + Geometry Match
is required.
An inch clip-on nut occupies physical space around the sheet-metal edge.
Engineers should evaluate:
overall length;
width;
height;
upper-leg geometry;
lower-leg geometry;
threaded-feature height;
screw protrusion.
Nearby:
wiring;
PCBs;
insulation;
brackets;
ducting;
sensors;
may restrict the available envelope.
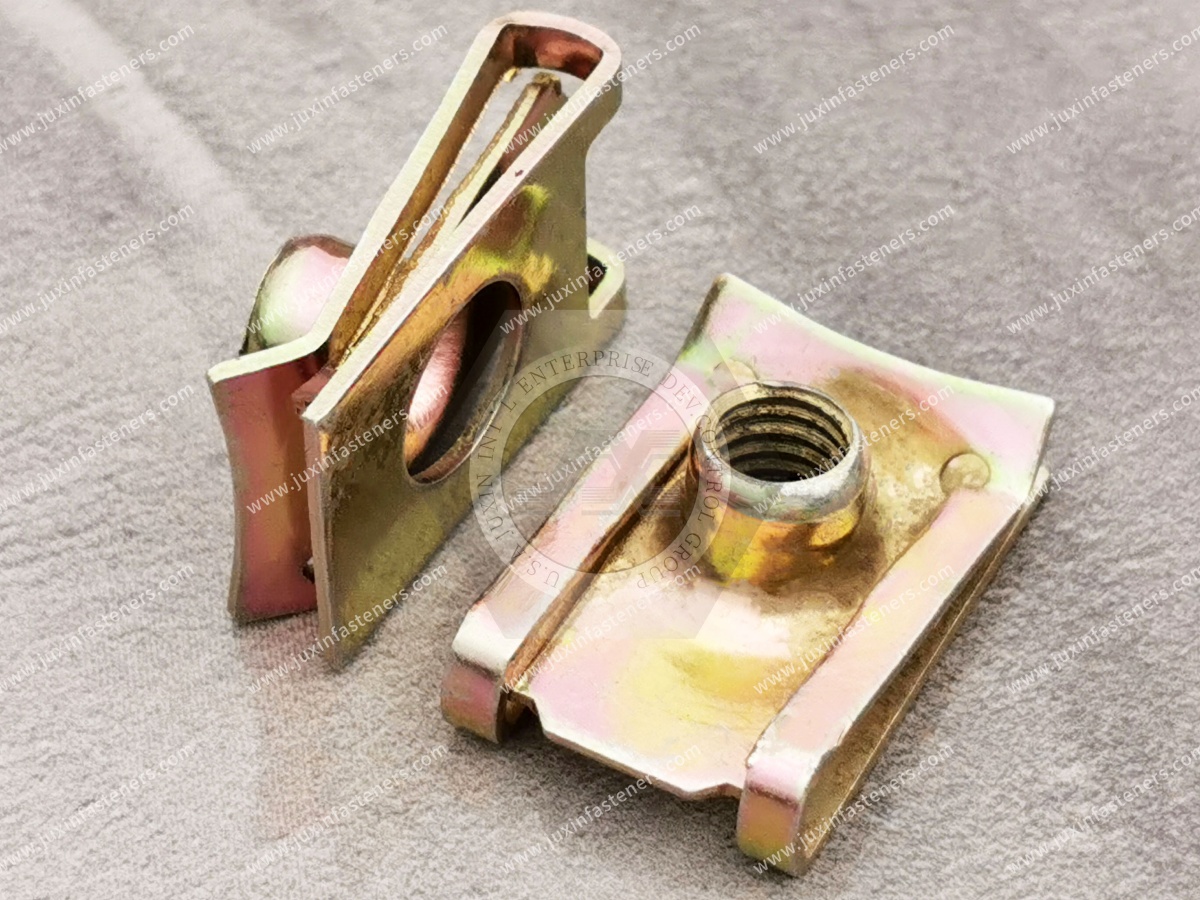
UNC or UNF thread selection does not determine whether a U-nut or J-nut is appropriate.
Clip geometry should follow:
panel edge geometry;
hole setback;
throat depth;
installation direction;
clearance;
mating component position.
For a detailed geometry comparison, see the JUXIN FASTENERS guide U-Nuts vs J-Nuts: Geometric Selection for Edge-Mounted Sheet Metal at /solutions/u-nuts-vs-j-nuts-geometry.
Barrel-style clip nuts can use a different threaded architecture and envelope from other spring-nut designs.
Selection can depend on:
thread engagement;
panel thickness;
hole location;
clip geometry;
backside clearance.
For further engineering guidance, see Strong-Grip Clip-On Barrel Nuts: U-Nuts, Multi-Thread Engagement & Panel Fastening Solutions at /solutions/strong-grip-clip-on-barrel-nuts-u-nuts.
Folded and flanged sheet metal adds further variables.
The engineer may need to consider:
base sheet thickness;
effective stack thickness;
flange width;
bend radius;
return geometry;
hole setback;
installation direction.
For detailed flange selection, see Clip-On Nuts for Flanged Edges: Fastening Folded Sheet-Metal Panels at /solutions/clip-on-nuts-for-flanged-edges.
Clip retention concerns the ability of the fastener to remain positioned on the panel before and during screw installation.
Joint strength concerns the completed screw-fastener-panel assembly.
Final joint behavior can depend on:
mating screw;
thread engagement;
panel material;
panel thickness;
fastener geometry;
tightening process;
clamp load;
tensile loading;
shear loading;
vibration;
corrosion.
An inch thread designation does not define joint strength.
This is one of the most useful procurement principles for inch clip-on nuts.
Two components can both be described as:
1/4-20 clip nuts
while differing in:
U/J/barrel geometry;
panel thickness range;
hole setback;
throat depth;
overall width;
overall height;
thread architecture;
material;
coating;
installation direction.
Therefore:
Same Thread ≠ Same Clip-On Nut
and:
Same Thread ≠ Automatic Supplier Interchangeability
When an OEM needs an alternate source for a legacy inch clip nut, the original part number may no longer provide enough engineering information.
A useful reverse-engineering comparison can include:
existing sample;
existing drawing;
thread designation;
TPI;
panel thickness;
edge-to-hole-center dimension;
overall geometry;
material;
finish.
This gives supplier development a much stronger basis for evaluating an alternative.
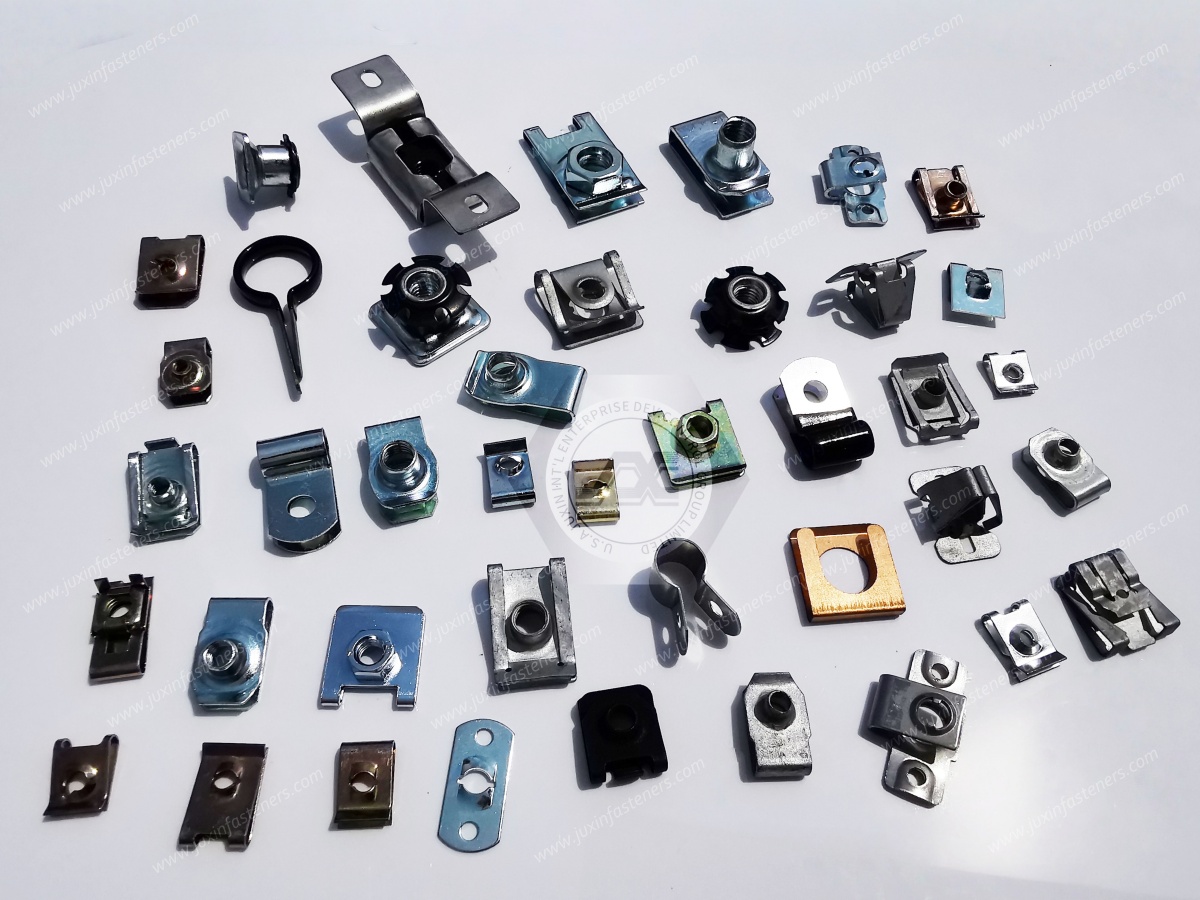
Many U-nuts and J-nuts look similar in online catalogs.
A photograph may not reveal:
throat-depth difference;
clip opening;
thread architecture;
panel range;
material thickness;
coating thickness.
For production substitution, use dimensional and application data.
Metric and inch clip-on nuts can look nearly identical while using incompatible screw threads.
A metric M-series screw should not be assumed to mate with a Unified inch nut because the nominal diameters appear similar.
Likewise, an inch screw should not be forced into a metric thread.
The thread system should be verified explicitly.
For metric applications, see Metric Clip-On Nuts: Thread Size, Panel Thickness & OEM Sourcing Guide at /solutions/metric-clip-nuts-selection.
Sometimes an OEM redesign involves changing from inch to metric hardware.
That should be treated as an engineering change, not merely a purchasing substitution.
Review:
screw diameter;
pitch;
clearance hole;
clip thread architecture;
hole setback;
panel geometry;
screw length;
mating components;
tooling;
BOM documentation.
A visually similar metric part is not automatically a drop-in replacement.
Depending on the product and project, material options can include:
carbon steel;
spring steel;
stainless steel.
Material selection should follow:
product geometry;
forming requirements;
panel fit;
corrosion environment;
customer specification.
Material should not be used as a shortcut for unverified vibration or structural performance.
Carbon and spring steel can be suitable for many industrial applications when the correct material condition and surface protection are specified.
For more information, see Carbon Steel Clip-On Nuts: Material Grades, Coatings & OEM Selection at /solutions/carbon-steel-clip-on-nuts-material-coating-guide.
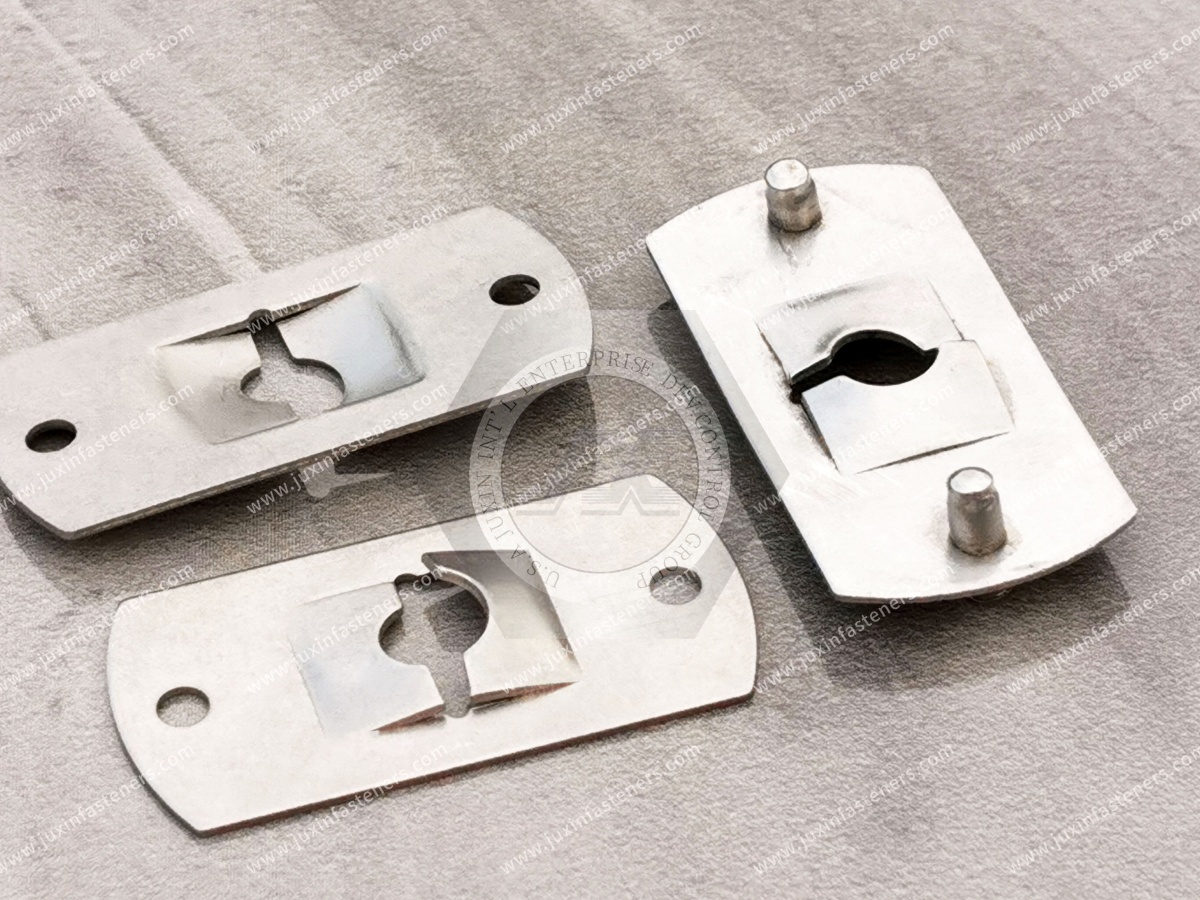
Stainless steel may be selected where the project requires stainless material characteristics.
JUXIN FASTENERS product information includes stainless steel options in relevant clip-on nut families, including SUS304 and SUS316 options.
Exact grade, inch thread and geometry availability should be confirmed for the requested product.
Potential project-specific surface treatments can include:
zinc-based coating systems;
phosphate-based finishes;
other customer-specified treatments.
For applicable JUXIN FASTENERS projects, trivalent chromium zinc plating can be specified where required.
The RFQ should define relevant requirements such as:
coating system;
passivation;
coating thickness where specified;
corrosion test;
acceptance criteria;
RoHS/REACH requirements where applicable.
Coating buildup can affect:
clip opening;
contact surfaces;
internal threads;
tight clearances.
Panel paint or powder coating can also change the installation condition.
This reinforces the importance of validating the finished fastener against the finished production panel.
Higher-strength or higher-hardness steel spring components may require hydrogen embrittlement risk evaluation when certain electrochemical processing routes are used.
However, post-plating baking is not a universal requirement with one universal process for every inch clip-on nut.
Where applicable, the requirement should follow the actual:
material;
hardness;
coating process;
component geometry;
customer specification.
Inch clip-on nuts can be considered for:
fabricated enclosures;
equipment chassis;
brackets;
service covers;
access panels;
folded structures.
For fabricators, early fastener selection can reduce the risk of designing a panel hole that does not match available clip geometry.
Inch-series hardware remains relevant in many HVAC systems.
Suitable clip-on nut applications can include:
equipment housings;
blower covers;
control enclosures;
service panels;
access covers.
Selection should consider:
panel thickness;
flange geometry;
corrosion environment;
service access;
mating screw.
The clip-on nut itself should not be assumed to create an airtight joint, waterproof connection or vibration-isolated assembly.
Potential applications include:
machine covers;
access panels;
control enclosures;
internal brackets;
non-structural guards.
For safety-related guards or highly loaded joints, the complete fastening system requires application-specific evaluation.
The words “inch spring nut” do not establish a heavy-duty or structural rating.
Inch clip-on nuts can be considered for suitable:
cabinet frames;
control panels;
internal brackets;
access covers;
equipment housings.
The fastener should not automatically be treated as a grounding, bonding or EMI component.
Those functions require separate design.
Legacy and current commercial equipment may continue to use inch-series hardware for:
housings;
brackets;
removable covers;
internal chassis;
service access.
For replacement sourcing, preserving the existing geometry can be as important as preserving the screw thread.
Some automation equipment and imported/legacy machinery can contain a mixture of metric and inch fasteners.
This creates a particularly important maintenance risk.
Technicians and procurement teams should verify the thread system rather than selecting replacement clips from visual similarity.
| Specification Variable | Engineering Question |
|---|---|
| Thread designation | What exact inch screw is used? |
| TPI | What threads-per-inch value must match? |
| Thread series | UNC, UNF or another specified series? |
| Thread architecture | Formed thread, barrel, captive nut or tapping-screw interface? |
| Panel material | Steel, stainless, aluminum or another sheet material? |
| Actual panel thickness | What finished minimum/maximum thickness must fit? |
| Hole setback | What is the edge-to-hole-center dimension? |
| Throat depth | Can the clip position the thread correctly? |
| Clip geometry | U-nut, J-nut, flange clip or another design? |
| Screw length | Is engagement adequate without interference? |
| Material | Carbon/spring steel or stainless? |
| Finish | What corrosion specification applies? |
| Installation direction | From which edge and side is the clip installed? |
| Envelope | Is there adequate clearance around the clip and screw? |
This provides much more engineering value than a simple fractional thread-size catalog.
A reliable sourcing workflow is:
Mating Screw → Unified Thread Designation → TPI → Actual Panel Thickness → Hole Setback →
Throat Depth → Clip Geometry → Material → Finish → Prototype Fit → Joint Validation → Production Drawing
This sequence helps prevent a purchasing search from bypassing the engineering interface.
When comparing an existing inch clip nut with a proposed alternative, verify:
customer part number;
drawing revision;
thread designation;
TPI;
thread series;
thread architecture;
thread class where applicable;
actual panel thickness;
panel tolerance;
hole setback;
throat depth;
overall dimensions;
clip opening;
installation direction;
mating screw;
screw length;
material;
coating;
inspection requirements.
The unit price comparison should come after technical interchangeability has been established.
When submitting an RFQ to JUXIN FASTENERS at info@juxinfasteners.com, provide as much of the following information as available:
2D engineering drawing;
3D CAD model where relevant;
existing physical sample;
reference photograph;
current supplier part number;
customer part number;
U-nut, J-nut, barrel or other geometry;
exact inch thread designation;
TPI;
UNC, UNF or other required series;
thread class where applicable;
mating screw specification;
mating screw length;
washer or joint-stack information where relevant;
panel material;
nominal actual panel thickness;
minimum and maximum panel thickness where applicable;
panel thickness tolerance;
panel coating condition;
hole diameter;
hole setback;
throat or reach dimension;
flange or edge geometry;
surrounding clearance;
installation direction;
material requirement;
surface treatment;
trivalent chromium zinc requirement where applicable;
coating thickness where specified;
RoHS/REACH requirements where applicable;
corrosion test method where required;
required exposure duration where specified;
corrosion acceptance criteria;
hydrogen embrittlement control requirement where applicable;
prototype/sample quantity;
production order quantity;
annual demand;
packaging requirements;
labeling requirements;
inspection requirements;
customer-specific specifications.
A generic purchasing search may begin with:
“1/4-20 clip nut supplier”
but an engineering-controlled RFQ should eventually become:
“We need this 1/4-20 thread configuration, for this finished panel thickness, at this hole setback and throat depth,
with this clip geometry, material, finish, screw length and annual demand.”
The complete commercial sourcing path is:
Inch Fastener Search → Mating Screw → Thread Designation & TPI → Panel Condition → Hole Setback → Clip Reach → Geometry
→ Material → Surface Treatment → Prototype Fit → Joint Validation → Approved Drawing → Production RFQ → Repeat Supply
This is the difference between finding a similar-looking clip and sourcing an interchangeable OEM component.
For drawing-based inch clip-on nuts, UNC clip nuts, UNF clip nuts, inch U-nuts, inch J-nuts, fractional spring nuts and other OEM sheet-metal fasteners, contact JUXIN FASTENERS at info@juxinfasteners.com.
Providing the actual thread designation, TPI, panel material and thickness, hole setback,
fastener geometry and annual demand allows JUXIN FASTENERS to evaluate the requirement much more accurately than specifying a fractional screw size alone.
Product Packaging
Packaging Standard
At Juxin Fasteners, we apply standardized export packaging to ensure product protection, traceability, and compliance with international logistics requirements.
1. Standard Export Packaging
Unless otherwise specified, all products will be packed according to our factory standard export packaging, which includes:
Moisture-resistant inner protection
Poly bag or small box packing as required
Reinforced export cartons
Clear labeling with part number, specification, batch number, and quantity
Palletizing for sea or air shipment when necessary
Our standard packaging is designed to ensure safe transportation, efficient warehousing, and long-distance international shipping.
2. Customized Packaging Options
We also provide customized packaging solutions according to customer requirements, including but not limited to:
Private labeling
Customized barcodes
Specific carton dimensions
Retail packaging
Special pallet configuration
Customer-specific marking and identification
So that you know, customized packaging may involve additional costs and extended lead time depending on the complexity of the requirements.
3. Compliance & Quality Assurance
All packaging processes are controlled under our ISO 9001 quality management system to ensure consistency, traceability, and product integrity throughout the supply chain.
Product Pictures
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY