
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Aug. 21, 2026
Self-Clinching Studs for EV Battery Packs and Aluminum Enclosures
Electric vehicle battery packs integrate structural housings, battery modules, electrical distribution systems, thermal management equipment, sensors, cable routing, protective covers, and service-related components.
These assemblies require fastening solutions that combine reliable mechanical attachment with efficient manufacturing and controlled environmental performance.
Self-clinching studs for EV battery packs provide permanently retained external threads in compatible sheet metal components.
They are installed by pressing an engineered retention feature into a prepared hole, allowing the surrounding sheet material to deform and mechanically lock the stud in place.
For suitable aluminum battery trays, fabricated steel enclosures, auxiliary brackets, and internal mounting panels, self-clinching studs can reduce the need for loose hardware and eliminate welding heat during fastener installation.
However, battery pack applications require careful engineering assessment.
A self-clinching stud is not automatically suitable for a structural battery module connection, crash-load path, high-voltage insulation boundary, or sealing-critical enclosure penetration.
The correct fastening solution depends on substrate material, sheet thickness, hardness, hole preparation, installation force, mechanical retention, corrosion protection, environmental exposure, and production requirements.
JUXIN FASTENERS supplies self-clinching studs and related sheet metal fastening products for industrial and automotive OEM applications.
Customer-specific battery enclosure requirements can be reviewed using drawings, material specifications, installation conditions, and purchasing forecasts.
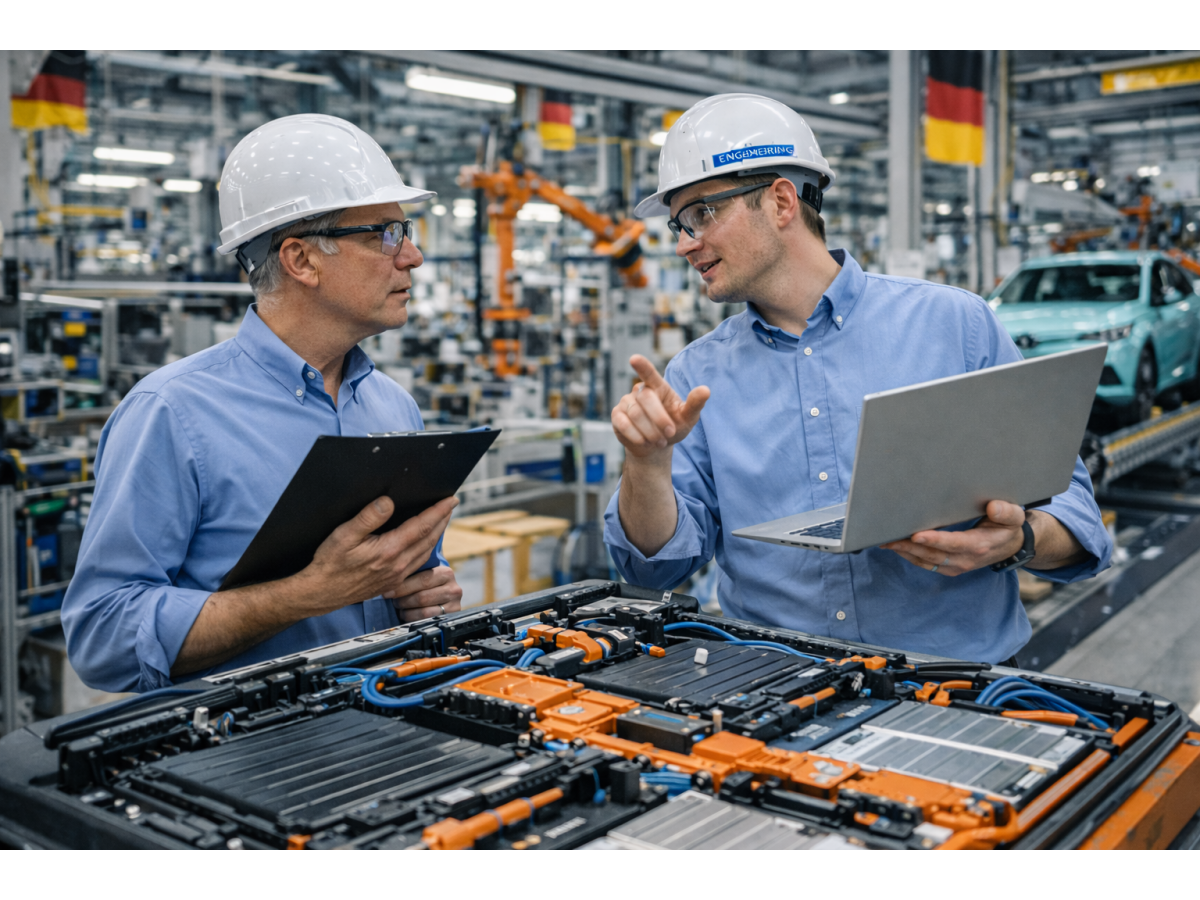
Where Self-Clinching Studs Fit in EV Battery Pack Design
Battery packs contain different categories of mechanical connections, and these should not be treated as interchangeable.
A stud supporting a small cable bracket may have very different mechanical and environmental requirements from a connection retaining a battery module or joining the enclosure to the vehicle structure.
Auxiliary Mounting Applications
Self-clinching studs may be considered for suitable secondary mounting points, including:
Battery management system support brackets.
Cable routing and harness retention brackets.
Sensor mounting brackets.
Auxiliary electrical component supports.
Internal equipment mounting panels.
Non-primary protective covers.
Secondary thermal management brackets.
Service-related sheet metal accessories.
Lightweight support brackets attached to compatible enclosure components.
These applications may benefit from a fixed threaded projection that simplifies positioning and assembly.
The stud must still be validated against the actual loading conditions and production process.
Battery Tray and Enclosure Panel Applications
Aluminum battery trays and fabricated enclosure panels may contain suitable sheet metal regions for mechanically retained fasteners.
Self-clinching studs can be considered where the panel provides sufficient material thickness and hardness compatibility, and where pressing equipment has the necessary installation access.
The term "battery tray" can refer to a fabricated sheet metal component, an extrusion-based assembly, a casting, or a hybrid construction.
Conventional self-clinching studs should not be assumed compatible with all of these manufacturing methods.
A cast aluminum wall or thick extrusion may require a different fastening approach from a thin formed aluminum panel.
Battery Covers and Service Panels
Battery covers may require repeatable fastening points for removable components.
A self-clinching stud can provide a fixed external thread for suitable brackets or cover-related hardware.
However, cover sealing, joint preload, service cycles, and environmental exposure must be considered independently.
A clinched stud does not automatically seal the installation hole or guarantee that a mating nut will remain secure under vibration.
Primary Structural and Safety-Critical Connections
Battery module retention, enclosure-to-vehicle mounting, crash protection, and structural load transfer can be safety-critical functions.
Standard self-clinching studs should not be selected for these connections solely on the basis of nominal thread size or catalog retention values.
Any proposed use requires engineering evaluation of the complete joint, including structural loading, fatigue, crash conditions, substrate behavior, manufacturing variation, and applicable vehicle requirements.
How Self-Clinching Studs Work in Battery Enclosure Sheet Metal
A self-clinching stud contains a threaded shank and engineered retention features near the head.
During installation, the stud is positioned in a correctly prepared hole and compressed into the panel using suitable pressing equipment.
The surrounding sheet material flows into the retention features, forming a mechanical interlock.
The resulting connection is intended to resist rotation and axial displacement.
Retention Geometry
Depending on the stud design, retention features may include ribs, serrations, knurls, or an annular groove.
These features are not decorative.
Their dimensions and tolerances influence the mechanical engagement between the stud and the sheet.
Pushout Resistance
Pushout resistance measures the force required to displace the installed fastener axially from the sheet under a defined test condition.
The value depends on the fastener geometry, substrate material, sheet thickness, hole dimensions, and installation quality.
It should not be confused with the tensile strength of the stud itself.
Torque-Out Resistance
Torque-out resistance measures the installed fastener's resistance to rotation within the sheet.
This is particularly important when a mating nut is tightened or removed.
A stud may have sufficient thread strength but inadequate torque-out resistance if the substrate or installation process is unsuitable.
Joint Strength vs. Fastener Retention
The completed battery enclosure connection must be evaluated as a system.
Potential limiting factors include:
Stud tensile strength.
Stud shear strength.
Mechanical retention in the sheet.
Local sheet deformation.
Sheet pull-through.
Mating nut strength.
Joint preload.
Bracket stiffness.
Fatigue and vibration.
A high-strength stud does not compensate for inadequate sheet retention.
Self-Clinching Studs for Aluminum Battery Trays
Aluminum is widely used in battery enclosure design because of its favorable strength-to-weight characteristics and manufacturing flexibility.
However, aluminum alloys differ significantly in hardness, strength, temper, and deformation behavior.
These differences directly influence self-clinching installation.
Aluminum Alloy and Temper
An aluminum sheet specified only as "aluminum" does not provide enough information for fastener selection.
The engineering drawing should identify the actual alloy and temper where relevant.
Different tempers of the same alloy may respond differently to installation force and material displacement.
Sheet Thickness
Self-clinching studs require sufficient substrate material to flow into their retention features.
There is no universal minimum sheet thickness for every clinching stud.
The required thickness must be determined from the selected fastener's specification and the actual panel material.
A design that works in a relatively thick mounting panel may not provide adequate retention in a thinner enclosure wall.
Substrate Hardness
The sheet material must be capable of deforming into the stud's retention geometry.
If the substrate is too hard for the selected stud, incomplete seating or inadequate retention may occur.
If the substrate is too soft or thin, excessive local deformation may also be a concern.
The fastener and sheet must be evaluated together.
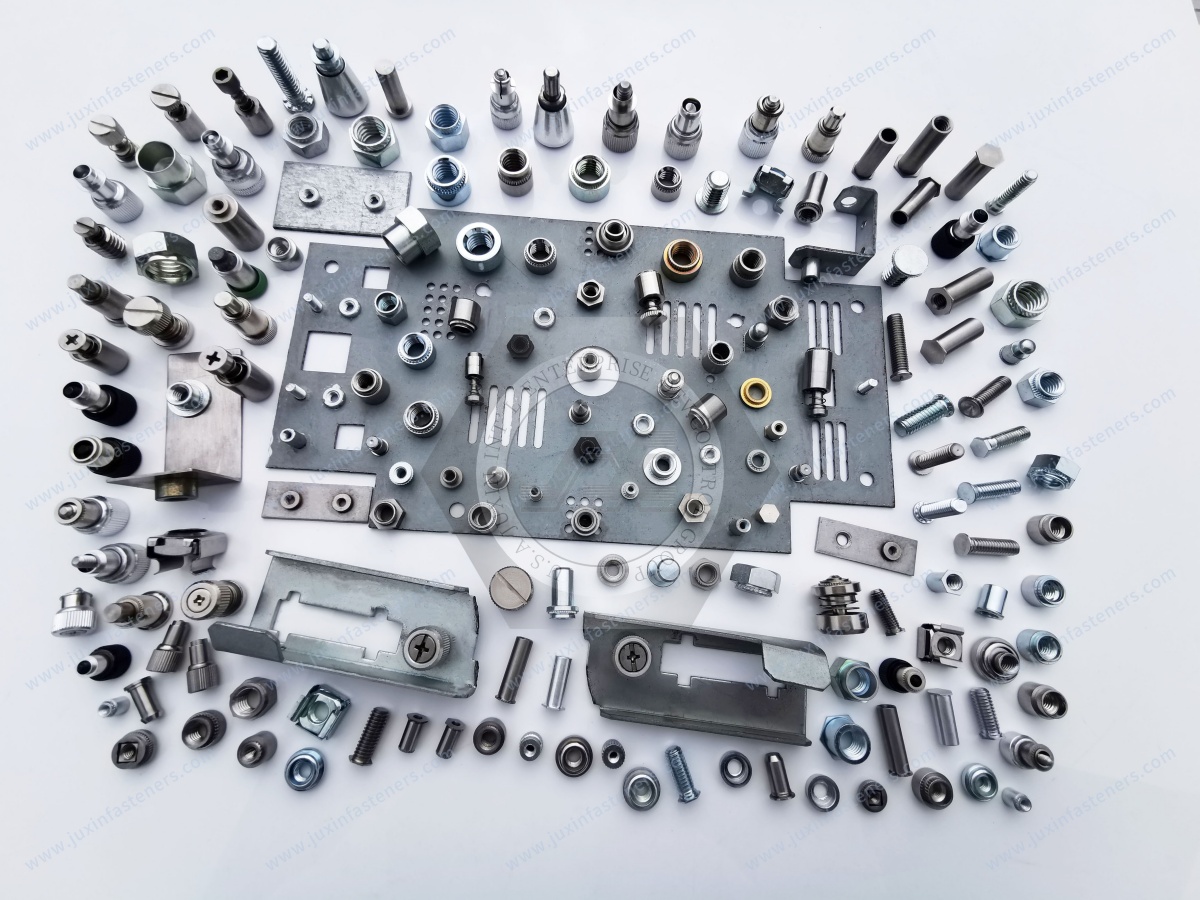
Stud Material and Hardness
Carbon steel, stainless steel, and other fastener material options may be considered according to the product design.
The fastener's material and hardness must be compatible with the clinching process.
Selecting a stronger or harder stud does not automatically produce a better connection.
Aluminum Battery Tray Design Review
Before approving a self-clinching stud for an aluminum tray, the design team should confirm:
Aluminum alloy and temper.
Actual sheet thickness and tolerance.
Substrate hardness.
Installation-hole diameter and tolerance.
Fastener retention geometry.
Required installation force.
Stud position and edge distance.
Pushout and torque-out requirements.
Service loading.
Coating and corrosion protection.
Assembly sequence.
Press tooling access.
These parameters are more informative than thread size alone.
Installation-Hole Design and Edge Distance
The prepared hole is a critical part of the self-clinching connection.
Hole Diameter
An oversized hole may reduce the amount of material available to engage the stud's retention features.
An undersized hole may increase installation force or cause panel damage.
The hole diameter and tolerance must follow the selected fastener's approved specification.
Hole Preparation
Punching, drilling, or other hole-making processes may produce burrs, tapered edges, or local deformation.
These conditions can affect seating and retention.
The hole preparation process should be controlled according to the selected fastener's installation requirements.
Unapproved countersinking or excessive chamfering may remove material needed for reliable clinching.
Edge Distance
Installation close to a panel edge, bend, embossed feature, or adjacent hole can cause local distortion.
The minimum edge distance should be determined from the selected fastener's technical requirements and validated for the actual panel.
Stud Perpendicularity
Incorrect alignment can interfere with mating bracket installation and introduce undesirable loading.
The installation fixture should control stud position and perpendicularity according to the assembly tolerance requirements.
Access for Press Installation
Conventional self-clinching studs generally require suitable support and controlled pressing access.
A stud that can be installed in a flat sheet before fabrication may be difficult to install after the battery tray becomes a closed or partially enclosed structure.
The fastening method should therefore be selected together with the manufacturing sequence.
Battery Enclosure Sealing and Fastener Penetrations
Battery pack enclosures may require protection against water, dust, road contaminants, and other environmental exposure.
A conventional self-clinching stud normally requires a prepared hole.
The mechanical interlock created during pressing is not equivalent to a validated environmental seal.
Through-Hole Leakage Risk
Where a stud is installed through an enclosure boundary, the installation region may form a potential leakage path.
The enclosure design should account for:
Hole geometry.
Contact interfaces.
Surface coatings.
Sealant or gasket arrangements.
Temperature variation.
Mechanical loading.
Water exposure.
Manufacturing tolerances.
The complete assembly must be evaluated against the project's ingress protection requirements.
Sealing-Critical Locations
For sealing-critical battery enclosure joints, engineers may need to consider alternative fastening designs.
One option is a closed-end sealed rivet nut where an internal thread and one-sided installation are required.
JUXIN FASTENERS provides an engineering guide to Sealed Rivet Nuts for EV Battery Pack Trays.
A closed-end rivet nut can help reduce a direct passage through the fastener body, but its installation does not automatically guarantee enclosure sealing.
The complete joint still requires suitable sealing elements and validation.
Concealed-Head Fastener Alternatives
Where the outer panel surface must remain uninterrupted, a concealed-head self-clinching stud may be considered.
Such designs require a compatible blind recess or specially prepared installation feature.
The panel must provide sufficient thickness for the selected geometry.
A concealed-head stud is not a direct replacement for a conventional through-hole clinching stud.
The engineering team should evaluate the actual panel construction, retention requirements, and environmental performance.
Galvanic Corrosion in Aluminum Battery Enclosures
A common battery enclosure design challenge is the combination of aluminum panels and steel fasteners.
When dissimilar metals are electrically connected in the presence of an electrolyte, galvanic corrosion may occur.
The risk depends on material pairing, surface condition, coatings, exposure, and joint geometry.
Carbon Steel Studs in Aluminum Panels
Carbon steel studs may offer practical cost and strength advantages.
However, corrosion protection should be selected for the complete assembly.
A zinc coating may improve corrosion resistance, but coating damage during installation and service must also be considered.
Stainless Steel Studs in Aluminum Panels
Stainless steel may provide improved corrosion resistance for the fastener itself.
However, stainless steel in contact with aluminum can create galvanic corrosion concerns under certain conditions.
A stainless steel fastener is not automatically the best corrosion solution for every aluminum battery tray.
Coating and Interface Protection
Depending on the design, corrosion management may involve:
Appropriate fastener coatings.
Compatible panel surface treatments.
Isolation measures where technically appropriate.
Controlled drainage and moisture exposure.
Protection of damaged coating areas.
Environmental testing of representative assemblies.
The selected protection system must also remain compatible with the clinching process.
Electrical Grounding and Isolation
Battery packs contain high-voltage systems and sensitive electrical equipment.
A metallic self-clinching stud may create an electrically conductive connection between components.
This may be useful for some grounding applications but undesirable where electrical isolation is required.
Protective Bonding
Where electrical continuity is required, the complete connection must be evaluated.
Coatings, contact pressure, oxidation, and corrosion can influence electrical performance.
A mechanically secure connection is not automatically a validated electrical bonding connection.
High-Voltage Isolation
Where isolation is required, the stud, mating hardware, surrounding panel, and insulating components must be considered together.
Electrical clearance, creepage, and dielectric performance should be evaluated according to the applicable battery system requirements.
A conventional metallic self-clinching stud does not provide electrical insulation by itself.
Thermal Cycling, Vibration and Battery Pack Reliability
Battery pack components may experience repeated temperature changes, road vibration, acceleration, braking, and service loading.
These conditions influence the complete fastening system.
Differential Thermal Expansion
Aluminum panels and steel studs expand at different rates as temperature changes.
This may influence local stresses, clamping behavior, and long-term joint performance.
The assembly should be evaluated over the intended operating temperature range.
Vibration
A permanently clinched stud provides a retained threaded attachment point.
However, it does not automatically prevent a mating nut from loosening.
Where required, the threaded joint should incorporate a suitable locking strategy.
Fatigue
Repeated loading may affect the stud, surrounding sheet, or attached bracket.
The connection should be evaluated according to its actual load path and expected service conditions.
Service and Maintenance
Battery pack service components may require repeated assembly and disassembly.
The fastening design should account for the required service cycles, thread condition, and potential torque-out loading during removal.
Material and Surface Finish Options
JUXIN FASTENERS supplies self-clinching stud products in relevant carbon steel and stainless steel configurations.
The final material and finish must be selected according to the project requirements.
Carbon Steel Self-Clinching Studs
Carbon steel may provide a practical combination of mechanical properties, manufacturability, and cost.
Suitable surface treatment should be considered where corrosion exposure is expected.
Heat-Treated Carbon Steel
Heat treatment may be specified where the selected product design requires particular mechanical properties.
However, the resulting hardness must remain compatible with the substrate and installation method.
Stainless Steel Self-Clinching Studs
Stainless steel may be considered for applications requiring enhanced corrosion resistance.
The exact grade must be confirmed.
Different stainless steel grades have different mechanical and corrosion characteristics.
Zinc-Plated Carbon Steel
Zinc plating may be selected for certain carbon steel fasteners.
The required coating specification, thickness, and compatibility with the installation process should be established before production.
Material Compliance
Battery and automotive customers may require documentation concerning material composition, restricted substances, or coating compliance.
Any claimed RoHS, REACH, or customer-specific compliance must be supported by applicable documentation.
JUXIN Self-Clinching Stud Product Options
JUXIN FASTENERS offers product configurations relevant to suitable sheet metal fastening applications.
Flush-Head Self-Clinching Studs
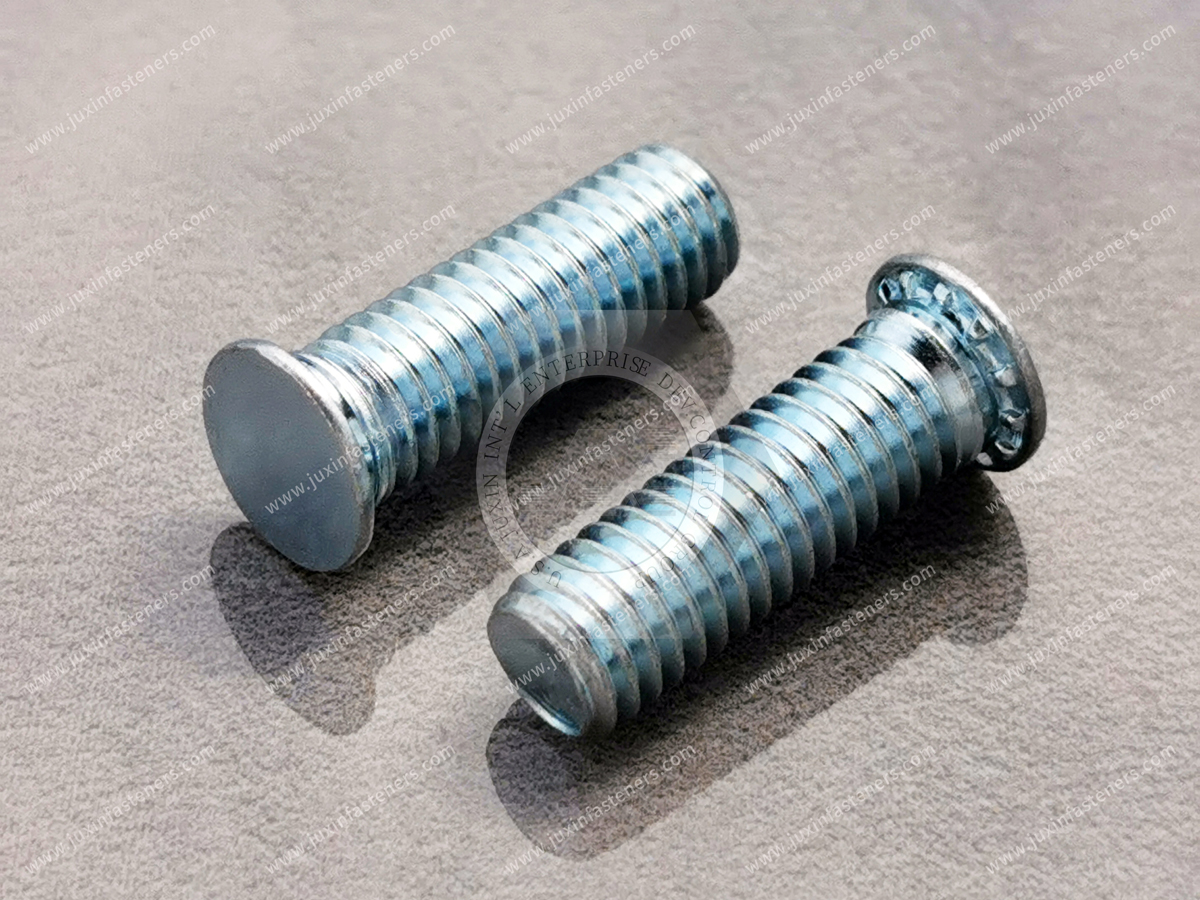
Flush-head studs provide an external threaded projection while allowing the head to seat flush with the designated sheet surface when correctly installed.
JUXIN offers Flush-Head Studs JX-FH for compatible sheet metal applications.
The actual substrate hardness, minimum sheet thickness, hole size, and installation requirements must match the selected specification.
Stainless Steel Flush-Head Studs
For projects evaluating stainless steel configurations, JUXIN offers Flush-Head Studs JX-FHS.
Stainless steel material selection does not eliminate the need to verify compatibility with the aluminum or steel substrate.
Custom Stud Configurations
Customer-specific projects may require particular thread lengths, head dimensions, retention geometries, materials, or surface treatments.
These requirements should be defined through approved drawings and technical specifications.
Availability and manufacturing feasibility must be confirmed for the requested design and quantity.
Metric and Inch Thread Specifications
Battery pack fastening projects may use ISO metric or Unified inch-series threads.
Relevant thread standards include ISO 261 and ISO 965 for metric threads and ASME B1.1 for Unified threads.
Metric, UNC, UNF, BSW, and BSF thread systems are different and should not be treated as directly interchangeable.
For example, M6 × 1.0 and 1/4-20 UNC are not equivalent thread specifications.
The complete thread designation, tolerance, stud length, and mating hardware should be confirmed during design review.
Self-Clinching Stud Installation in Battery Tray Manufacturing
Battery enclosure production requires consistent installation quality.
The process should be defined before mass production.
Prepare the Panel
Confirm the material grade, thickness, hardness, and installation-hole dimensions.
Position the Stud
Place the stud in the prepared hole with the correct orientation.
Support the Panel
Use suitable tooling to prevent excessive local deformation.
Apply Controlled Pressing Force
The pressing force should allow the surrounding material to flow into the retention features.
Insufficient force may produce incomplete seating.
Excessive force may damage the panel or fastener.
Inspect the Installation
Verify head seating, stud alignment, thread condition, and panel deformation.
Validate Retention
Where required, test pushout and torque-out performance using representative production panels.
Installation Before or After Coating
The production sequence may affect retention and corrosion performance.
For many designs, installing self-clinching studs before final painting or coating may be appropriate.
However, the correct sequence depends on the fastener, panel material, and finishing process.
Installing a stud after coating may damage the protective finish.
Installing before coating may require thread protection or additional process controls.
The sequence should be established through manufacturing validation.
Automated Pressing and Battery Pack Production Efficiency
High-volume battery enclosure production may benefit from automated or semi-automated fastener installation.
The process can involve:
Automatic stud feeding.
Orientation control.
Panel positioning.
Pressing.
Force or displacement monitoring.
Visual or dimensional inspection.
Part transfer.
The selected stud geometry should be compatible with the feeding and pressing equipment.
Pressing Force Monitoring
Force-displacement monitoring may help identify abnormal installation conditions.
However, it does not automatically prove that every installed stud meets its required mechanical retention.
The process should be supported by appropriate validation and inspection.
Production Tolerances
Battery trays may contain multiple fastening points.
Stud positioning, perpendicularity, and projection length can influence downstream assembly.
Tolerance accumulation should be considered when multiple brackets or covers are installed simultaneously.
Cycle Time
The total installation cycle includes feeding, positioning, pressing, inspection, and transfer.
Production managers should evaluate the complete process rather than the pressing time alone.
Tooling Maintenance
Worn tooling or misalignment may cause variation in installation quality.
The production control plan should address tooling condition and preventive maintenance.
Common Battery Enclosure Clinching Stud Failure Modes
Insufficient Torque-Out Resistance
The stud rotates when a mating nut is tightened.
Potential causes include incorrect hole diameter, unsuitable sheet hardness, incomplete installation, or inadequate retention geometry.
Insufficient Pushout Resistance
The stud is displaced from the panel under axial loading.
Potential causes include insufficient sheet thickness, poor material flow, incorrect installation, or excessive loading.
Panel Distortion
Excessive pressing force or inadequate tooling support causes local deformation.
Panel Cracking
Unsuitable substrate conditions or installation parameters damage the panel.
Stud Misalignment
Incorrect tooling or positioning causes the stud to lean, interfering with downstream assembly.
Thread Damage
Handling or pressing equipment damages the external thread.
Coating Damage and Corrosion
Installation or service damages protective coatings, allowing corrosion at the fastener interface.
Leakage at an Enclosure Penetration
A fastening point crosses the sealing boundary without an appropriate sealing strategy.
Mating Nut Loosening
Vibration or incorrect joint design allows the nut to loosen even though the stud remains retained.
Unapproved Structural Use
A conventional clinching stud is used in a battery pack connection requiring higher structural or safety performance than the fastener has been validated to provide.
Each failure mode should be addressed through design review, manufacturing controls, and appropriate testing.
Self-Clinching Studs vs. Other Battery Enclosure Fasteners
Battery enclosure designers should compare fastening methods according to installation access, substrate compatibility, sealing, serviceability, and mechanical requirements.
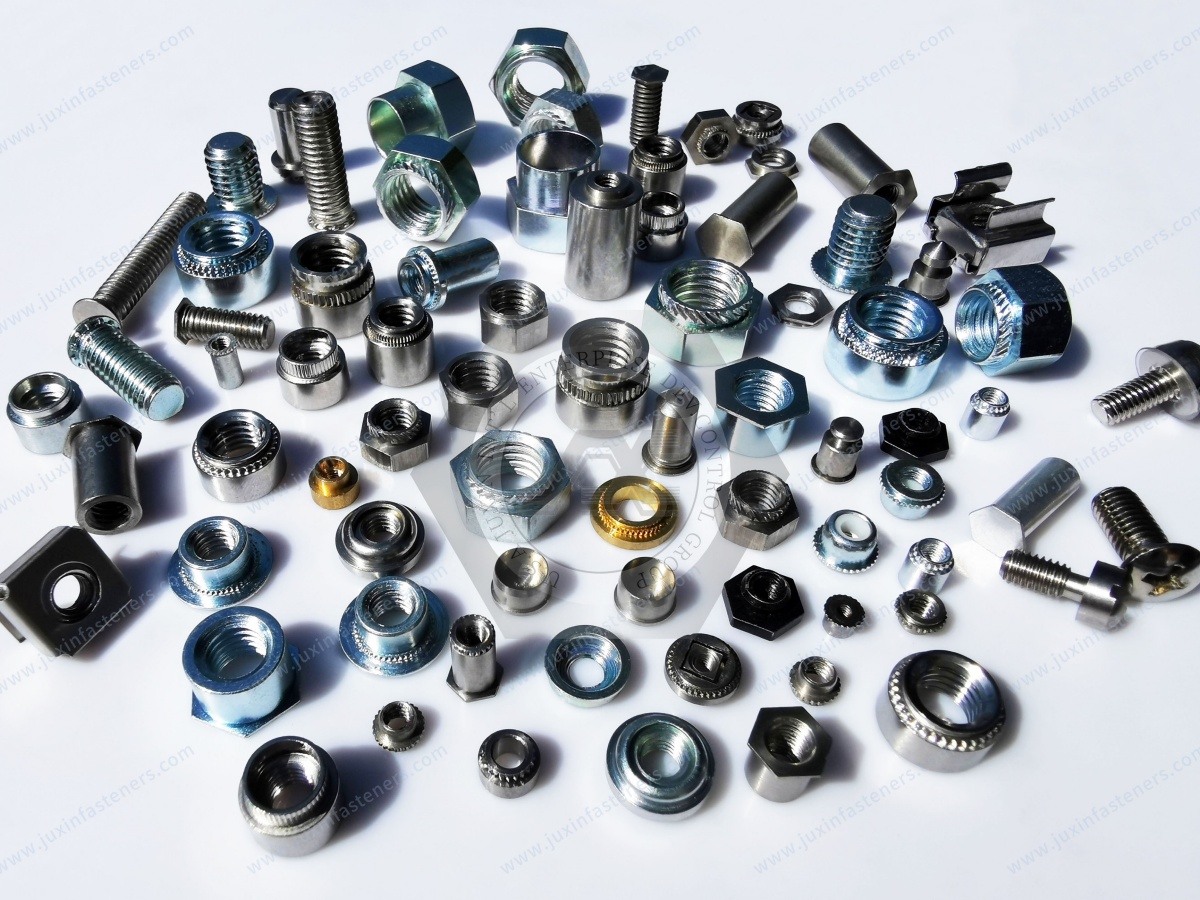
| Fastening Method | Main Advantage | Important Limitation |
|---|---|---|
| Self-clinching stud | Permanent external thread without welding heat | Requires compatible sheet material and pressing access |
| Self-clinching nut | Permanent internal thread | Requires compatible sheet and installation conditions |
| Concealed-head stud | Can preserve an uninterrupted exterior panel surface | Requires suitable blind recess and sufficient panel thickness |
| Sealed rivet nut | Blind-side internal thread with potential sealing integration | Complete sealing performance requires validation |
| Welded stud | External thread attached by welding | Weldability, heat input and welding quality must be controlled |
| Threaded insert | Internal thread in a suitable substrate | Installation method and substrate compatibility vary |
| Conventional bolt and nut | Removable joint | May require access to both sides and additional assembly operations |
A self-clinching stud may be preferred for an accessible aluminum mounting panel where a fixed threaded projection simplifies assembly.
A sealed rivet nut may be more appropriate where the design requires an internal thread, blind-side installation, and integration into an enclosure sealing system.
A different engineered connection may be necessary for primary battery structural joints.
Battery Pack Fastener Quality Control and OEM Validation
EV battery system suppliers may require documented quality and process controls.
The required scope depends on the customer, component, and application.
Incoming Fastener Inspection
Typical checks may include:
Thread diameter and pitch.
Stud length.
Head dimensions.
Retention geometry.
Material identification.
Surface finish.
Lot identification.
Installed Fastener Inspection
Checks may include:
Correct seating.
Stud perpendicularity.
Installation position.
Thread condition.
Panel deformation.
Required mechanical retention.
Mechanical Testing
Depending on the project, testing may include pushout, torque-out, tensile, shear, or other specified evaluations.
The test method and acceptance criteria should be defined in the approved engineering specification.
There is no universal pushout or torque-out value suitable for every battery enclosure self-clinching stud.
Environmental Validation
Relevant projects may require corrosion, temperature cycling, vibration, or ingress protection testing.
The applicable requirements should be determined from the complete battery enclosure design.
PPAP and Customer-Specific Documentation
Automotive OEMs and Tier suppliers may require Production Part Approval Process documentation or other customer-specific records.
The required scope must be agreed before production.
Any certification, test result, or approval must be supported by actual documentation.
Traceability
Customers may require traceability between delivered fastener lots, material records, inspection results, and shipment information.
Packaging and labeling should support correct identification and efficient production handling.
Battery Enclosure Fastener Procurement and Supplier Qualification
For purchasing managers and supplier development teams, the objective is not simply to purchase a stud with the correct thread.
The selected fastener must be compatible with the approved battery enclosure design and manufacturing process.
Drawing-Based Supplier Evaluation
A complete RFQ should identify:
Fastener drawing.
Thread size and standard.
Stud length.
Head and retention geometry.
Material and finish.
Aluminum or steel substrate grade.
Sheet thickness and hardness.
Installation-hole dimensions.
Required mechanical performance.
Environmental requirements.
Quality documentation.
Purchasing quantities.
Alternative Supplier Qualification
A replacement self-clinching stud should not be approved solely because its nominal thread and length match the existing product.
Differences in retention geometry, hardness, head dimensions, and installation requirements may change performance.
The alternative should be validated using representative production panels and the approved installation process.
MOQ and Production Volume
MOQ depends on the product configuration, material, finish, tooling requirements, and purchasing quantity.
For custom battery enclosure studs, buyers should communicate prototype quantities, initial production volumes, and annual forecasts.
Lead Time and Supply Planning
Lead time depends on manufacturing requirements, material availability, surface treatment, and order volume.
For recurring OEM programs, buyers should consider delivery schedules, specification control, quality consistency, and supply continuity.
Total Installed Cost
A battery enclosure fastener cost comparison should include:
Fastener unit price.
Hole preparation.
Press tooling.
Installation labor.
Automation.
Inspection.
Scrap and rework.
Surface treatment.
Packaging.
Logistics.
Downstream assembly time.
The lowest unit price does not necessarily produce the lowest total manufacturing cost.
Engineering and Procurement Checklist for Battery Pack Clinching Studs
| Evaluation Area | Required Information |
|---|---|
| Battery application | Tray accessory, cover bracket, sensor mount or cable support |
| Structural function | Secondary attachment or safety-critical connection |
| Fastener type | Standard, flush-head, concealed-head or custom stud |
| Thread | Metric or Unified size, pitch and tolerance |
| Geometry | Stud length, head dimensions and retention features |
| Substrate | Aluminum or steel grade, thickness and hardness |
| Installation hole | Diameter, tolerance, burr condition and edge distance |
| Pressing | Tooling, force, access and installation sequence |
| Retention | Pushout and torque-out requirements |
| Service loading | Tension, shear, vibration and thermal cycling |
| Environmental design | Corrosion, coating and sealing boundary |
| Electrical design | Grounding, isolation and clearance |
| Quality | Inspection, testing, documentation and traceability |
| Procurement | MOQ, annual demand, lead time and packaging |
This checklist helps battery pack engineering, manufacturing, and purchasing teams establish a consistent technical specification before approving a fastening solution.
JUXIN FASTENERS – Self-Clinching Stud Supply for EV Battery Enclosures
JUXIN FASTENERS supplies self-clinching studs and related sheet metal fastening products for suitable EV battery pack, automotive, and industrial OEM applications.
Relevant product options include:
Carbon steel self-clinching studs.
Stainless steel self-clinching studs.
Flush-head self-clinching studs.
Customer-defined stud lengths.
Metric and Unified thread configurations.
Specified surface treatments.
Related self-clinching nuts.
Related sealed rivet nut fastening solutions.
Related JUXIN Products and Engineering Solutions
Flush-Head Self-Clinching Studs JX-FH
Stainless Steel Flush-Head Studs JX-FHS
Self-Clinching Fasteners for Sheet Metal
Sealed Rivet Nuts for EV Battery Pack Trays
These product and engineering pages help customers compare compatible fastening approaches according to their actual battery enclosure requirements.
JUXIN FASTENERS can review customer drawings, material specifications, sheet thickness, installation conditions, and purchasing quantities to evaluate suitable product configurations.
Application-specific structural validation, battery safety requirements, environmental testing, PPAP documentation, and customer approvals must be confirmed separately where applicable.
Request an EV Battery Pack Self-Clinching Stud Technical Review or OEM RFQ
Are you sourcing self-clinching studs for aluminum battery trays, battery enclosure panels, battery cover accessories, cable management brackets, sensors, or auxiliary mounting components?
JUXIN FASTENERS welcomes inquiries from EV manufacturers, battery pack suppliers, enclosure fabricators, automotive Tier suppliers, engineering teams, production managers, procurement departments, and international supplier development professionals.
For an accurate technical review and quotation, please provide:
Available 2D drawings or 3D CAD models.
Required stud type and thread specification.
Stud length and retention geometry.
Aluminum or steel substrate grade.
Sheet thickness and hardness.
Installation-hole diameter and tolerance.
Required pushout and torque-out performance.
Service loads and vibration requirements.
Electrical isolation or grounding requirements.
Corrosion and sealing requirements.
Temperature and environmental conditions.
Material and surface finish specifications.
Customer-specific quality and documentation requirements.
Estimated order quantity and annual demand.
Target delivery schedule.
If you are evaluating an alternative to an existing battery enclosure fastener, please include the original drawing and installation specification.
Our objective is to help customers select technically appropriate fastening products that support reliable battery enclosure assembly, efficient production, and consistent OEM procurement.
JUXIN FASTENERS
Website: https://www.juxinfasteners.com
Email: info@juxinfasteners.com
Send your technical drawings and RFQ to discuss your EV battery pack self-clinching stud requirements.
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY



