
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Aug. 21, 2026
Automotive Self-Clinching Studs for Sheet Metal and OEM Assemblies
Automotive manufacturers increasingly use lightweight stamped metal components, fabricated brackets, electronic enclosures, and modular assemblies.
These components often require reliable externally threaded attachment points without adding unnecessary welding, tapping, or loose fastener handling operations.
Automotive self-clinching studs, also called press-in studs or clinch studs, provide a mechanical fastening solution for compatible sheet metal components.
A self-clinching stud is installed into a precisely prepared hole using controlled pressing force.
The fastener's engineered retention features displace the surrounding sheet material, creating a mechanical interlock that resists rotation and axial pushout.
Unlike welded studs, self-clinching studs do not require welding heat during installation.
This can be valuable for automotive components where localized heat input, panel distortion, or additional welding operations are undesirable.
However, successful installation depends on the relationship between the stud design, sheet material, hardness, thickness, hole dimensions, and pressing conditions.
A self-clinching stud that performs well in mild steel may not achieve the same retention in a harder steel or a different aluminum alloy.
For design engineers, the primary considerations include fastening geometry, substrate compatibility, mechanical retention, and joint reliability.
Manufacturing engineers and production managers must also evaluate punching accuracy, press tooling, installation force, automation, and production consistency.
Procurement and supplier development teams require accurate drawings, approved alternatives, material and coating specifications, cost information, and stable supply planning.
JUXIN FASTENERS supplies self-clinching studs and related sheet metal fasteners for automotive and industrial OEM applications.
Customer-specific designs can be reviewed according to the required thread, material, stud length, retention geometry, installation conditions, and purchasing quantities.
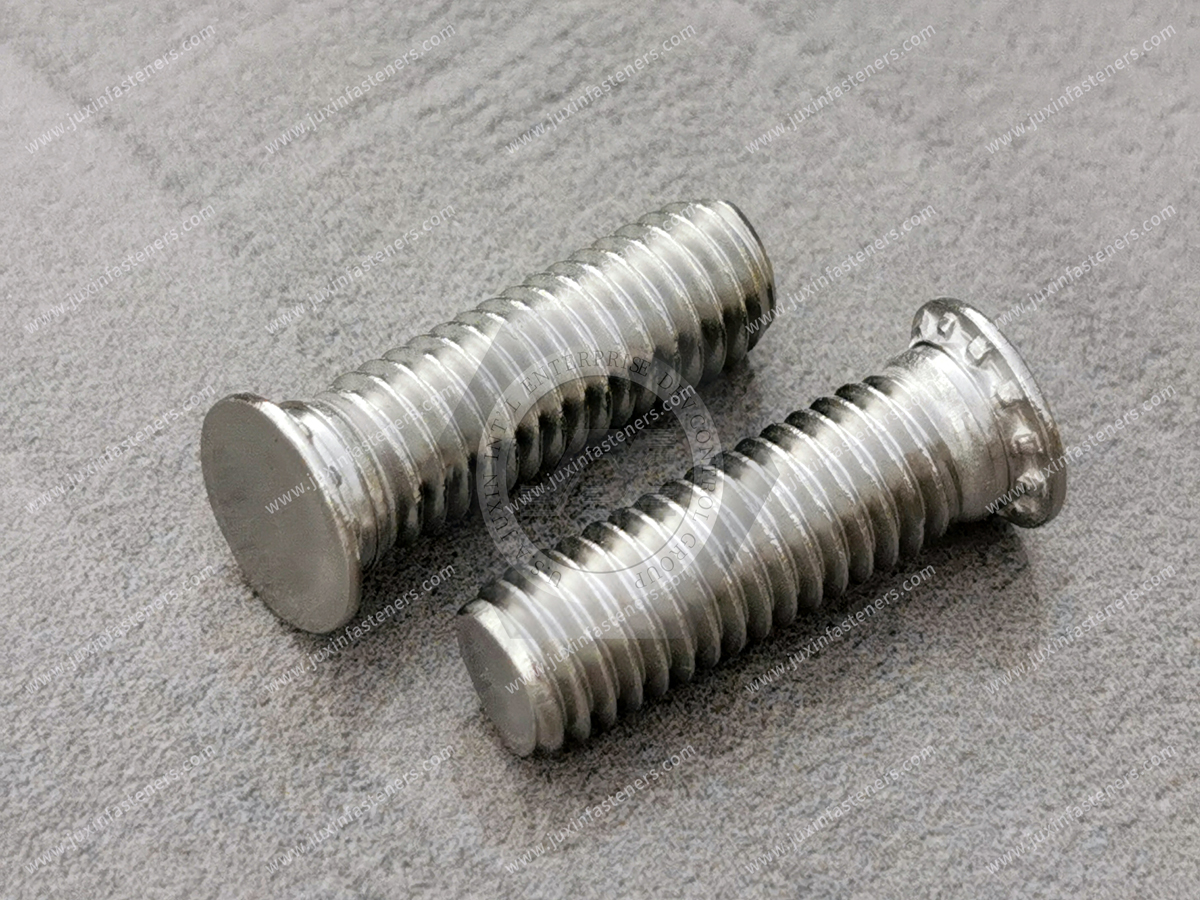
What Are Automotive Self-Clinching Studs?
A self-clinching stud is an externally threaded fastener designed to become permanently retained in a suitable metal sheet.
The stud is installed into a prepared hole using a press or other appropriate squeezing equipment.
During installation, the sheet material plastically deforms around the fastener's retention features.
This produces a mechanical interlock that holds the stud in position and resists movement during subsequent assembly.
The resulting threaded projection can be used with a compatible nut to mount brackets, covers, electrical components, and other automotive assemblies.
Typical applications include:
Automotive stamped brackets.
Interior sheet metal panels.
Electronic control unit housings.
Electrical mounting plates.
HVAC equipment accessories.
Sensor support brackets.
Fabricated equipment covers.
Suitable EV enclosure components.
Non-primary underbody accessories.
Self-clinching studs are not universal replacements for welded studs, bolts, or rivet nuts.
Their suitability depends on the actual substrate and connection requirements.
How Self-Clinching Studs Create Mechanical Retention
The retention mechanism is the defining feature of a self-clinching stud.
Unlike a conventional bolt inserted through a hole, a self-clinching stud is designed to mechanically engage the parent sheet.
The fastener may incorporate a knurled section, serrations, ribs, an undercut, an annular groove, or another engineered retention feature.
The exact geometry depends on the product design.
Material Displacement During Installation
When the stud is pressed into the prepared hole, the surrounding sheet material flows into the designed retention region.
This plastic deformation creates resistance to axial movement and rotation.
The process requires the sheet material to deform sufficiently without excessive cracking or damage.
The fastener must also be suitable for the installation force and substrate material.
Pushout Resistance
Pushout resistance describes the force required to displace the installed fastener axially from the sheet under a defined test condition.
The measured resistance depends on the stud geometry, sheet material, thickness, hole preparation, and installation process.
A stud's nominal thread size alone does not determine its pushout resistance.
Torque-Out Resistance
Torque-out resistance describes the torque required to cause the installed fastener to rotate relative to the sheet under a defined test condition.
This is particularly important when a mating nut is tightened or removed.
The torque-out performance must be compatible with the intended assembly process.
The required installation torque of the mating nut should not be confused with the torque-out resistance of the clinched stud.
Axial Tensile Joint Capacity
Pushout resistance is not the same as the tensile capacity of the completed threaded joint.
Depending on load direction, the joint may be limited by stud strength, sheet deformation, local pull-through, nut engagement, or another failure mode.
Engineers should evaluate the actual load path and required service performance.
Why Automotive Manufacturers Use Self-Clinching Studs
Self-clinching studs can provide manufacturing advantages when properly integrated into the sheet metal design.
Potential benefits include:
Permanent externally threaded attachment points.
No welding heat during installation.
Reduced risk of welding-related distortion.
Elimination of separate nuts at selected mounting points.
Compatibility with controlled press installation.
Repeatable fastening geometry.
Suitability for automated or semi-automated production.
Potential reduction in downstream assembly operations.
These benefits are application-dependent.
For example, a self-clinching stud eliminates a welding operation but still requires a correctly prepared installation hole and access for pressing equipment.
The total manufacturing process should be evaluated before selecting the fastener.
Automotive Applications for Self-Clinching Studs
Automotive assemblies contain numerous metal panels and fabricated components requiring threaded mounting points.
Self-clinching studs may be considered where the panel material and geometry permit reliable mechanical installation.
Automotive Body and Interior Components
Potential applications include:
Interior support brackets.
Instrument panel accessories.
Metal trim support components.
Non-primary body brackets.
Interior equipment mounting plates.
Serviceable metal covers.
For these applications, designers should evaluate sheet thickness, local stiffness, stud projection, and downstream assembly clearance.
A self-clinching stud should not be assumed suitable for a crash-critical or primary structural body connection without specific engineering validation.
Automotive Electronic Control Housings
Electronic control units and other vehicle electronics often use compact fabricated metal housings.
Self-clinching studs can provide retained mounting points for suitable covers, brackets, and internal support components.
Important considerations include:
Available installation space.
Sheet material and thickness.
Stud length.
Electrical clearance.
Corrosion protection.
Assembly torque.
Vibration.
Service access.
A protruding stud must not interfere with electrical components or required insulation distances.
Sensor and Instrument Mounting Brackets
Automotive sensors may be mounted using fabricated steel or aluminum brackets.
A self-clinching stud can provide a permanent threaded projection for suitable mounting arrangements.
The design must account for vibration, bracket stiffness, positional tolerance, and the required sensor alignment.
The fastening point should not introduce excessive deformation that affects sensor positioning.
Automotive HVAC and Auxiliary Equipment
HVAC modules, ventilation equipment, and other auxiliary systems may use sheet metal brackets and mounting panels.
Self-clinching studs may simplify the attachment of selected components.
However, the fastener must be evaluated for thermal cycling, vibration, and the expected service environment.
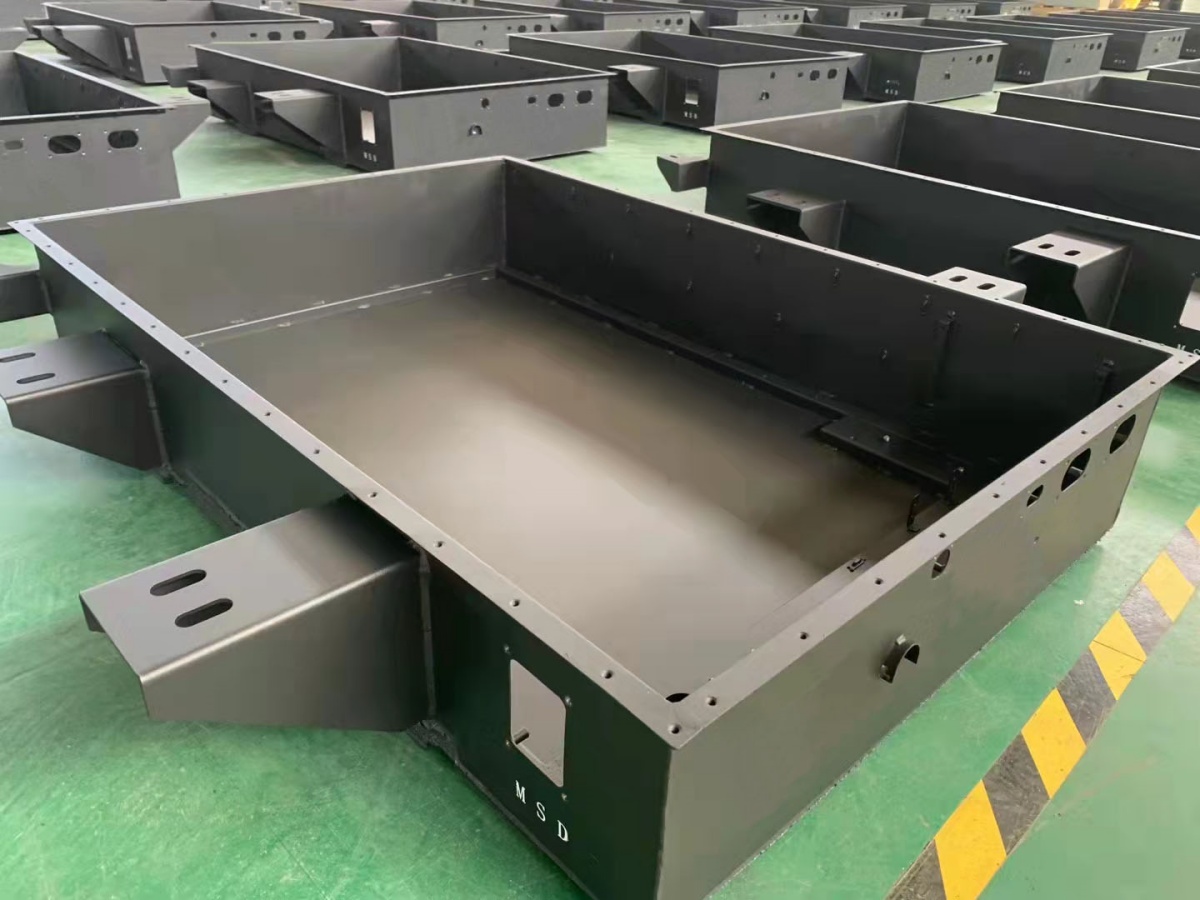
EV Battery Enclosures and Electrified Vehicle Components
Electric vehicle battery systems and related equipment may use aluminum or steel enclosures, covers, brackets, and electrical mounting panels.
Self-clinching studs may be considered for suitable non-primary attachments.
Potential applications include:
Auxiliary mounting brackets.
Electrical equipment panels.
Cable management supports.
Sensor brackets.
Serviceable covers.
Secondary enclosure components.
However, battery enclosures may be subject to demanding structural, sealing, thermal, electrical, and crash requirements.
A self-clinching stud should not be assumed suitable for a battery pack structural joint or sealing-critical connection without application-specific engineering validation.
Battery Enclosure Sealing Considerations
A conventional self-clinching stud is installed into a prepared hole.
This installation does not automatically create a watertight or hermetically sealed connection.
Where the stud is located in a sealed enclosure boundary, the complete assembly must be evaluated for leakage, corrosion, and environmental performance.
Alternative fastening arrangements may be more appropriate where a through-hole is unacceptable.
Electrical Isolation and Grounding
Self-clinching studs are metallic fastening components.
Their installation can influence electrical continuity and clearance.
Where grounding or protective bonding is required, the complete joint must be validated.
Where electrical isolation is required, the stud and mating components must not compromise the intended insulation system.
Round-Head Self-Clinching Studs for Automotive Sheet Metal
Round-head self-clinching studs are commonly used in sheet metal assemblies where a permanent threaded projection is required.
Many designs incorporate a knurled or serrated retention section beneath the head.
During installation, the surrounding sheet material flows into the retention geometry.
This creates a mechanical connection that resists rotation and axial displacement.
Manufacturing Advantages of Round-Head Designs
Round-head studs may be suitable for efficient high-volume production using cold-heading or other appropriate manufacturing processes.
For suitable standard geometries, cold heading can provide efficient material utilization and repeatable dimensions.
Potential advantages include:
Efficient fastener production.
Consistent head geometry.
Compatibility with controlled press installation.
Suitability for high-volume OEM purchasing.
Potentially competitive unit costs.
The actual manufacturing process and cost depend on the selected stud design and production quantity.
Knurl Geometry and Retention Performance
The knurl or serration geometry influences how the sheet material engages with the stud.
An incorrectly specified retention feature may reduce torque-out or pushout performance.
For custom automotive applications, the fastener drawing should define the relevant retention dimensions and tolerances.
A nominal thread specification is not sufficient to define the complete clinching stud.
Hex-Head Self-Clinching Studs and Anti-Rotation Designs
Hex-head or hexagonal retention configurations may be considered for specialized OEM applications.
The geometry can provide mechanical resistance to rotation when properly matched to the substrate and installation arrangement.
However, a hexagonal design does not automatically provide greater torque-out resistance than every round-head clinching stud.
Performance depends on:
Retention geometry.
Sheet material.
Sheet thickness.
Installation-hole configuration.
Installation force.
Stud material.
Required assembly torque.
The correct choice should be based on the actual design and validated performance.
Round-Head vs. Hex-Head Stud Selection
| Evaluation | Round-Head Design | Hex-Head Design |
|---|---|---|
| Retention principle | Typically uses knurls, serrations or other retention features | Uses an engineered polygonal or related retention geometry |
| Manufacturing | May be suitable for efficient cold-heading production | Manufacturing depends on the specific geometry |
| Anti-rotation | Depends on design and substrate | Depends on design and substrate |
| Installation | Requires compatible hole and pressing arrangement | Requires compatible hole and pressing arrangement |
| OEM suitability | Common sheet metal applications | Specialized or drawing-defined applications |
Neither configuration should be selected solely from its head shape.
Flush-Head and Concealed-Head Stud Options
Automotive equipment designers may require fastening points that minimize external protrusion or preserve a smooth visible surface.
Different self-clinching stud designs can address these requirements.
Flush-Head Self-Clinching Studs
Flush-head studs are designed to create a threaded attachment point while keeping the installed head flush with the specified sheet surface when correctly installed.
JUXIN FASTENERS offers Flush-Head Studs JX-FH for compatible sheet metal applications.
The required sheet thickness, hardness, hole geometry, and installation method must match the selected product.
Concealed-Head Self-Clinching Studs
Concealed-head studs use a different installation concept.
They may be installed into a prepared blind or recessed feature, allowing the opposite surface to remain visually uninterrupted.
JUXIN FASTENERS offers Concealed-Head Studs.
These products require specific panel preparation and should not be treated as direct substitutes for conventional through-hole clinching studs.
For automotive enclosures, the selection should consider available material thickness, visible-surface requirements, manufacturing operations, and retention performance.
Sheet Material Hardness and Clinching Compatibility
One of the most important engineering considerations is the hardness relationship between the stud and the sheet material.
Self-clinching installation depends on the substrate material deforming into the fastener's retention geometry.
If the sheet is too hard relative to the fastener design, sufficient material flow may not occur.
This can reduce retention performance or damage the fastener or panel.
Mild Steel and Low-Carbon Steel Sheet
Mild steel may be suitable for many self-clinching stud designs.
However, the exact sheet grade, hardness, thickness, and surface condition must be confirmed.
The installation requirements should follow the selected fastener's technical data.
Aluminum Sheet Metal
Aluminum sheet is used in lightweight automotive components.
Some self-clinching stud designs are suitable for compatible aluminum alloys.
However, aluminum grades differ in hardness, strength, and deformation behavior.
The selected fastener must be evaluated against the actual alloy and temper.
Stainless Steel Sheet
Stainless steel sheet may be harder than mild steel or aluminum.
A standard clinching stud intended for softer sheet metal may not provide suitable retention in stainless steel.
A fastener specifically designed for the selected stainless steel substrate may be required.
Advanced High-Strength Steel
Automotive manufacturers increasingly use advanced high-strength steel (AHSS) in structural components.
The hardness and mechanical behavior of these materials can limit conventional self-clinching installation.
A standard clinching stud should not be assumed suitable for AHSS.
Where the substrate is too hard for reliable clinching, engineers may need to consider another fastener design or joining process.
Minimum Sheet Thickness and Hole Design
Self-clinching stud performance depends strongly on the available sheet thickness and installation-hole geometry.
There is no universal minimum sheet thickness applicable to every stud design.
The correct value depends on the selected fastener and substrate.
Installation-Hole Diameter
The hole must be manufactured according to the specified tolerance.
An oversized hole may reduce the amount of material available for mechanical engagement.
An undersized hole may cause excessive installation force, distortion, or damage.
The hole should be defined on the engineering drawing.
Hole Quality and Burr Control
Punching or drilling can create burrs, tapered edges, and local deformation.
These conditions may affect fastener seating and retention.
The hole should be prepared according to the fastener manufacturer's installation requirements.
Uncontrolled deburring, countersinking, or chamfering may remove material needed for proper clinching.
Edge Distance and Nearby Features
Stud installation near a sheet edge, bend, embossment, or another hole may cause local deformation.
The required edge distance depends on the fastener design and substrate.
Designers should also consider the space required for the pressing tooling.
Installation Direction
The installation direction and supported side of the panel are important.
The fastener should be pressed into the sheet using the intended tooling arrangement.
A stud should not be installed in reverse orientation unless the product is specifically designed for that method.
Correct Installation Process for Automotive Self-Clinching Studs
A controlled installation process is essential for consistent retention.
Prepare the Sheet Metal
Create the installation hole according to the approved drawing.
Verify the material grade, thickness, hole diameter, and relevant surface condition.
Position the Stud
Place the stud in the prepared hole with the correct orientation.
Ensure the fastener is aligned with the installation tooling.
Apply Controlled Pressing Force
Use a suitable press or installation system to apply the required axial force.
The pressing operation should allow the sheet material to flow into the retention geometry.
Excessive force can damage the stud or panel.
Insufficient force can produce incomplete seating and inadequate retention.
Inspect the Installed Fastener
After installation, inspect the stud for correct seating, alignment, thread condition, and panel deformation.
Where required, perform mechanical retention testing according to the approved control plan.
Avoid Hammer Installation
Self-clinching studs are designed for controlled pressing rather than uncontrolled impact installation.
Hammering may produce uneven material flow, damaged threads, or unreliable retention.
Press Tooling and Automotive Production Automation
Automotive production requires repeatable installation across large numbers of components.
Self-clinching studs may be integrated into manual, semi-automated, or automated pressing systems.
Press Tooling and Support
The tooling must support the panel and apply force in the correct direction.
Inadequate support can cause local sheet deformation or incorrect seating.
The tooling should be compatible with the stud head, thread projection, and surrounding component geometry.
Automatic Feeding and Orientation
Automated installation may require stud feeding, orientation, positioning, and verification.
The fastener geometry should be reviewed against the feeding equipment.
A stud that installs successfully in a manual press may require additional evaluation for automated feeding.
Installation Force Monitoring
Suitable pressing systems may monitor force, displacement, or other process variables.
These measurements can help identify installation variation.
However, a force-displacement signature alone does not prove that every installed stud meets its required pushout or torque-out performance.
Mechanical validation remains important.
Cycle Time and Production Efficiency
The total installation cycle includes feeding, positioning, pressing, inspection, and part transfer.
A fast pressing operation does not automatically mean that the complete station is efficient.
Production managers should evaluate equipment availability, reject rates, tooling maintenance, and downstream assembly effects.
Installation Before or After Surface Coating
The production sequence can affect clinching performance.
For many applications, installation is performed before final coating or painting.
However, the appropriate sequence depends on the fastener design and finishing requirements.
Coating thickness and surface treatment can influence fit, installation, and corrosion behavior.
Installation into pre-coated panels should be evaluated for possible coating damage.
Automotive Self-Clinching Stud Materials and Surface Finishes
JUXIN FASTENERS offers self-clinching stud options in carbon steel and stainless steel, with material and surface treatment selection based on the application.
Carbon Steel Self-Clinching Studs
Carbon steel is commonly used for automotive sheet metal fastening applications.
It can provide a practical combination of mechanical properties, manufacturability, and cost.
Heat treatment may be specified where required by the product design.
However, the selected hardness must remain compatible with the intended substrate and clinching mechanism.
Stainless Steel Self-Clinching Studs
Stainless steel may be considered where corrosion resistance is important.
The appropriate grade depends on the operating environment and required mechanical properties.
JUXIN FASTENERS offers Flush-Head Studs JX-FHS in stainless steel configurations.
The actual material grade and installation compatibility should be confirmed for the selected product.
Zinc-Plated Carbon Steel
Zinc plating can provide corrosion protection for carbon steel fasteners.
The required coating type and thickness should be defined according to the customer's specification.
The finished fastener must remain compatible with the installation process and mating thread.
Galvanic Corrosion in Mixed-Material Assemblies
When dissimilar metals are connected in the presence of moisture, galvanic corrosion may occur.
This is relevant for automotive assemblies combining steel fasteners and aluminum panels.
The complete assembly should be evaluated, including coatings, exposed surfaces, and service conditions.
RoHS and Material Compliance
Customers may require compliance with applicable substance restrictions such as RoHS or REACH.
The exact requirements depend on the product, market, and customer specification.
Compliance should be supported by appropriate material and finish documentation where required.
A general material description should not be treated as proof of compliance.
Metric, UNC and UNF Thread Options
Automotive self-clinching studs may be specified with ISO metric or Unified inch-series threads.
Relevant thread standards include ISO 261 and ISO 965 for metric threads and ASME B1.1 for Unified threads.
Metric, UNC, UNF, BSW, and BSF thread systems are not directly interchangeable.
For example, M6 × 1.0 and 1/4-20 UNC are different thread specifications.
A similar nominal diameter does not establish compatibility with the mating nut.
The complete thread specification, tolerance, stud length, and mating hardware should be confirmed during design review.
Mechanical Performance: Pushout, Torque-Out and Joint Loading
Automotive self-clinching studs must be evaluated according to their actual mechanical function.
Pushout Resistance
Pushout resistance is influenced by the retention geometry, sheet material, thickness, and installation conditions.
The required resistance should be established according to the application.
Torque-Out Resistance
Torque-out resistance is particularly important when the mating nut is tightened or removed.
The required assembly torque should remain compatible with the installed fastener's retention performance.
Tensile and Shear Loads
The completed joint may experience axial tension, transverse shear, or combined loading.
The connection should be evaluated as a system rather than using stud material strength alone.
Vibration and Fatigue
Automotive components experience vibration and repeated service loads.
A permanently clinched stud does not automatically prevent the mating nut from loosening.
Where necessary, the joint should incorporate an appropriate locking method.
Panel Deformation and Pull-Through
Thin sheet metal may deform locally under load.
The panel geometry and local stiffness should be considered.
In some applications, reinforcement or a different fastening method may be required.
Self-Clinching Studs vs. Welded Studs vs. Rivet Nuts
Different fastening methods offer different advantages.
| Evaluation | Self-Clinching Stud | Welded Stud | Rivet Nut |
|---|---|---|---|
| Threaded feature | External thread | Usually external thread | Internal thread |
| Installation | Controlled pressing | Welding | Mechanical expansion |
| Heat input | No welding heat | Welding heat required | No welding heat |
| Hole requirement | Prepared hole normally required | Depends on stud and welding process | Prepared hole required |
| Access | Press tooling generally requires support access | Depends on welding process | Many types allow one-sided installation |
| Substrate limitation | Sheet hardness and thickness critical | Weldability and thickness critical | Grip range and deformation critical |
| Typical use | Factory sheet metal assemblies | Compatible welded metal assemblies | Thin-wall and blind-access assemblies |
The correct solution depends on the panel material, manufacturing sequence, access, mechanical loads, and service requirements.
For a panel already assembled into a closed enclosure, a blind rivet nut may be easier to install than a conventional self-clinching stud.
For a panel where welding heat is undesirable but press access is available, a self-clinching stud may be a suitable alternative.
For an application where the panel cannot provide sufficient clinching material flow, a welded or other engineered fastening solution may be more appropriate.
Common Self-Clinching Stud Installation Failures
Stud Rotation During Nut Tightening
Insufficient retention may allow the stud to rotate.
Possible causes include incorrect hole size, unsuitable sheet hardness, incomplete installation, or inadequate retention geometry.
Prevention: Verify the fastener specification and validate torque-out performance.
Stud Pushout
The fastener may be displaced axially from the sheet.
Possible causes include insufficient sheet thickness, poor material flow, incorrect installation, or excessive service loading.
Prevention: Validate pushout resistance using representative production panels.
Panel Cracking or Distortion
Excessive installation force or unsuitable substrate conditions may damage the sheet.
Prevention: Use compatible fastener geometry and controlled pressing equipment.
Incorrect Hole Diameter
An oversized or undersized hole may compromise installation.
Prevention: Control hole dimensions and inspect the punching or drilling process.
Incomplete Head Seating
The stud may not seat correctly against the sheet.
Prevention: Verify tooling alignment, installation force, and panel support.
Thread Damage
Improper tooling or handling can damage the external thread.
Prevention: Protect the threaded portion during pressing and material handling.
Corrosion at the Fastener Interface
Dissimilar metals or coating damage may contribute to corrosion.
Prevention: Select suitable materials and finishes and validate environmental performance.
Automotive Quality Control and OEM Production Validation
Automotive customers may require documented product and process controls.
The exact requirements depend on the component, customer, and project.
Incoming Fastener Inspection
Checks may include:
Thread diameter and pitch.
Stud length.
Head dimensions.
Retention geometry.
Material identification.
Surface finish.
Lot identification.
Installed Fastener Inspection
Checks may include:
Head seating.
Stud perpendicularity.
Thread condition.
Hole and panel deformation.
Position accuracy.
Required mechanical retention.
Mechanical Validation
Depending on the application, testing may include pushout, torque-out, tensile, or other defined performance tests.
The test method and acceptance criteria should be established by the approved engineering specification.
There is no universal pushout or torque-out value applicable to every self-clinching stud of the same thread size.
PPAP and Customer-Specific Requirements
Automotive OEMs and Tier suppliers may require Production Part Approval Process (PPAP) documentation or other customer-specific approval records.
The applicable requirements should be agreed before production.
Any claimed qualification or certification must be supported by the relevant documentation.
Traceability and Production Consistency
For recurring automotive production, traceability may connect delivered fastener lots with material records, inspection results, and shipment information.
Packaging and labeling should support correct identification and line-side handling.
OEM Automotive Self-Clinching Stud Procurement
Automotive purchasing teams should evaluate technical compatibility, production feasibility, supplier capability, and total installed cost.
Drawing-Based Supplier Development
A complete RFQ should include:
Product drawing.
Thread size and standard.
Stud length.
Head and retention geometry.
Sheet material and thickness.
Installation-hole dimensions.
Required mechanical performance.
Material and surface finish.
Quality documentation.
Estimated annual demand.
Alternative Supplier Qualification
A replacement stud should not be approved solely because its thread size and length match the original.
Differences in retention geometry, hardness, head dimensions, and installation requirements may affect performance.
The alternative should be validated using the actual production panel and approved installation process.
MOQ, Lead Time and Volume Planning
MOQ and lead time depend on the product geometry, material, finish, tooling requirements, and purchasing quantity.
For high-volume automotive programs, procurement teams should communicate annual forecasts, initial order quantities, and delivery schedules.
This supports more accurate supplier planning and quotation.
Total Installed Cost
The cost comparison should include:
Fastener unit price.
Hole preparation.
Press tooling.
Installation labor.
Automation.
Inspection.
Scrap and rework.
Packaging.
Logistics.
Downstream assembly time.
A lower fastener unit price does not necessarily produce a lower total assembly cost.
Engineering and Procurement Checklist for Automotive Clinch Studs
| Evaluation Area | Required Information |
|---|---|
| Application | Bracket, panel, electrical housing, EV enclosure or auxiliary component |
| Stud type | Round-head, hex-head, flush-head or concealed-head |
| Thread | Metric or Unified size, pitch and tolerance |
| Geometry | Stud length, head dimensions and retention features |
| Sheet material | Steel, stainless steel or aluminum grade |
| Sheet thickness | Actual thickness and tolerance |
| Hardness | Substrate hardness and fastener compatibility |
| Installation hole | Diameter, tolerance and edge distance |
| Pressing | Tooling, force, access and installation sequence |
| Mechanical performance | Pushout, torque-out and service loads |
| Finish | Plating, corrosion protection and compliance |
| Quality | Inspection, validation and traceability |
| Procurement | Quantity, MOQ, lead time and packaging |
This checklist helps engineering, manufacturing, and purchasing teams establish a consistent technical specification before approving a fastener.
Automotive Self-Clinching Stud Supplier – JUXIN FASTENERS
JUXIN FASTENERS supplies self-clinching studs and related sheet metal fastening products for automotive and industrial OEM applications.
Our relevant product portfolio includes:
Round-head self-clinching studs.
Drawing-defined hex-head clinching stud configurations.
Flush-head self-clinching studs.
Concealed-head self-clinching studs.
Carbon steel clinch studs.
Stainless steel clinch stud options.
Zinc-plated configurations.
Metric and Unified thread specifications.
Customer-defined lengths and retention geometries.
Related self-clinching nuts and sheet metal fasteners.
Related JUXIN product and engineering pages:
Self-Clinching Studs for Sheet Metal Fabrication
Concealed-Head Self-Clinching Studs
Self-Clinching Fasteners for Sheet Metal
JUXIN FASTENERS can review customer drawings, material requirements, sheet thickness, installation conditions, and purchasing quantities to evaluate suitable product configurations.
Automotive-specific qualification, PPAP documentation, special testing, and customer approval requirements must be confirmed separately where applicable.
Request an Automotive Self-Clinching Stud Technical Review or OEM RFQ
Are you sourcing self-clinching studs for automotive sheet metal, stamped brackets, electrical housings, sensor mounts, HVAC components, or EV-related assemblies?
JUXIN FASTENERS welcomes inquiries from automotive OEMs, Tier suppliers, design engineers, manufacturing engineers, production teams, purchasing departments, and international supplier development professionals.
For an accurate technical review and quotation, please provide:
Available 2D drawings or 3D CAD models.
Required stud type and thread specification.
Stud length and retention geometry.
Sheet material, thickness and hardness.
Installation-hole diameter and tolerance.
Required pushout and torque-out performance.
Installation equipment and production conditions.
Material and surface finish requirements.
Customer-specific quality and documentation requirements.
Estimated order quantity and annual demand.
Target delivery schedule.
If you are evaluating an alternative to an existing self-clinching stud, please include the original drawing and installation specification.
Our objective is to help customers select technically appropriate press-in fastening solutions that support reliable automotive assembly, efficient production, and consistent OEM procurement.
JUXIN FASTENERS
Website: https://www.juxinfasteners.com
Email: info@juxinfasteners.com
Send your technical drawings and RFQ to discuss your automotive self-clinching stud requirements.
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY



